Optical Sorting Technology Solutions

All Categories

optical sorting technology

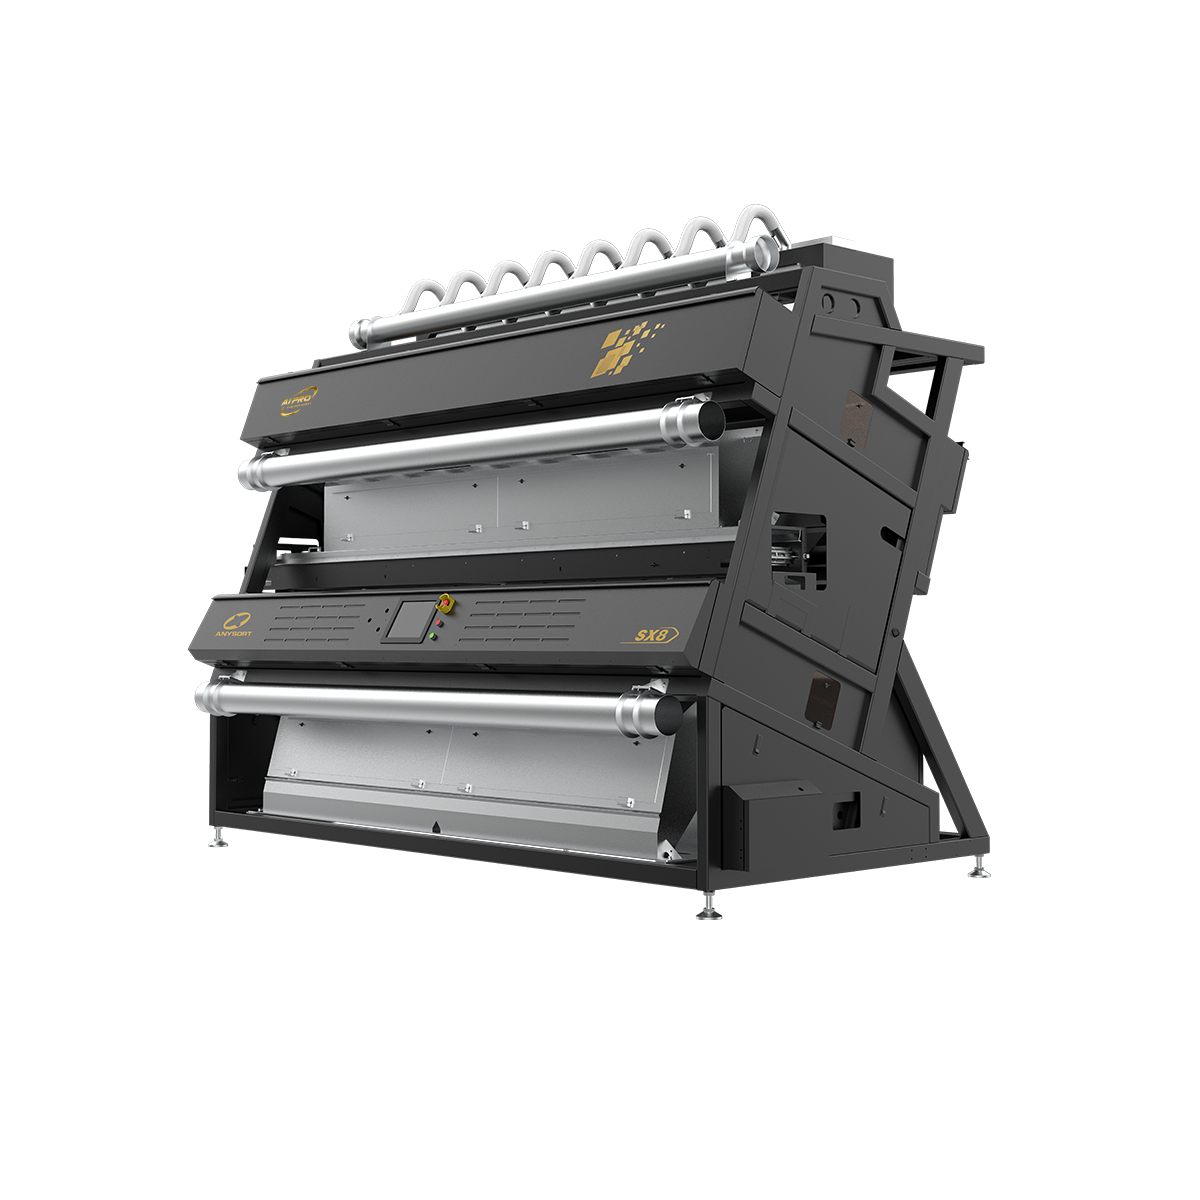
Optical sorting technology represents a revolutionary advancement in material separation and quality control systems. This innovative technology uses advanced optical sensors and artificial intelligence to identify and sort materials based on their physical and chemical properties with exceptional precision. Optical sorting technology operates by capturing high-resolution images of individual particles or products as they move along a conveyor belt, then analyzing these images in real-time to make instantaneous sorting decisions. The core functionality of optical sorting technology involves detecting color variations, size differences, shape irregularities, and material composition distinctions that human operators might miss. Modern optical sorting technology incorporates multi-spectral imaging, near-infrared detection, and machine learning algorithms to achieve sorting accuracy rates exceeding 99 percent. These systems process thousands of items per minute, making optical sorting technology ideal for high-volume industrial applications. The technological features of optical sorting technology include rapid processing speeds, non-destructive analysis, and automated ejection mechanisms that remove unwanted materials instantly. Optical sorting technology finds widespread application across numerous industries, including food processing, recycling facilities, mining operations, pharmaceutical manufacturing, and agricultural production. Whether sorting agricultural commodities by quality, removing contaminants from recycled materials, or ensuring pharmaceutical product consistency, optical sorting technology delivers reliable performance. The integration of optical sorting technology into production lines enhances product quality, reduces waste, and improves operational efficiency, making it an essential tool for modern manufacturing and processing operations.

Popular Products

Optical sorting technology delivers substantial advantages that directly benefit your bottom line and operational performance. The most significant advantage involves dramatically increased sorting accuracy and consistency that surpasses manual inspection capabilities. Optical sorting technology removes human error from quality control processes, ensuring every product meets your exact specifications without variation. Your production team can trust that optical sorting technology maintains uniform quality standards throughout entire production runs, protecting your brand reputation and customer satisfaction levels. Operational benefits include substantial labor cost reduction, as optical sorting technology automates previously manual sorting tasks. You eliminate the need for extensive quality control staff while simultaneously increasing throughput and processing capacity. Optical sorting technology operates continuously without fatigue, maintaining peak performance during extended shifts and maximizing your production facility utilization. Another crucial advantage centers on waste reduction and material recovery optimization. Optical sorting technology precisely separates recyclable materials, allowing you to recover valuable resources and reduce disposal costs significantly. For food producers, optical sorting technology removes defective products before packaging, preventing costly recalls and customer dissatisfaction. Environmental benefits emerge naturally, as optical sorting technology minimizes waste stream contamination and maximizes material recovery rates. Application suitability extends across diverse industries with remarkable versatility. Whether you process agricultural products, manage recycling operations, or manufacture consumer goods, optical sorting technology adapts to your specific requirements. The technology handles various material types, sizes, and characteristics, providing flexible solutions for different production challenges. Decision-useful context reveals that optical sorting technology represents a smart investment delivering measurable returns through improved efficiency, reduced waste, enhanced product quality, and decreased operational costs. Your customers receive consistently superior products, while your operation achieves greater profitability and sustainability credentials that increasingly matter in today's competitive marketplace.

Latest News

How to Choose the Right Tea Color Sorter for Your Needs?

01

Aug

How to Choose the Right Tea Color Sorter for Your Needs?

Selecting the right tea color sorter is one of the most critical decisions tea processors face when modernizing their operations. A tea color sorter directly impacts product quality, operational efficiency, and market competitiveness. The wrong choic...
View More
How Much Does a Color Sorter Machine Cost?

12

Aug

How Much Does a Color Sorter Machine Cost?

Understanding the investment required for a color sorter machine is essential for businesses in agriculture, food processing, and recycling sectors. The cost of a color sorter machine varies significantly based on capacity, technology sophistication,...
View More
How Can a Nuts Sorter Improve Your Production?

15

Aug

How Can a Nuts Sorter Improve Your Production?

A nuts sorter represents one of the most significant investments a food processing operation can make to enhance production quality and operational efficiency. The modern nuts sorter uses advanced imaging and sensor technology to identify and separat...
View More
Top AI Color Sorter Manufacturers in China (2026)

30

Aug

Top AI Color Sorter Manufacturers in China (2026)

The global demand for precision sorting technology has surged dramatically, with color sorter machine manufacturers in China leading innovation across agricultural and industrial sectors. Chinese color sorter machine manufacturers have established th...
View More

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

optical sorting technology

Exceptional Sorting Precision and Accuracy

Exceptional Sorting Precision and Accuracy

Optical sorting technology achieves unmatched sorting precision through advanced sensor arrays and artificial intelligence systems. Every item receives detailed optical analysis, with optical sorting technology detecting minute differences invisible to human inspectors. The precision of optical sorting technology reduces quality variations and ensures only acceptable products reach customers. This technological advantage directly impacts your profitability by minimizing customer returns and complaints related to product quality. Optical sorting technology maintains consistency across millions of sorting decisions, automatically adjusting to slight variations in product characteristics. Your production team benefits from the reliability that optical sorting technology provides, knowing that quality standards remain consistently met. Industries relying on strict quality requirements, including pharmaceuticals and food production, depend on optical sorting technology to maintain regulatory compliance. The advanced detection capabilities of optical sorting technology identify contaminants, defects, and foreign materials with speed and reliability that human inspectors cannot match, even when working in ideal conditions.
Real-Time Processing and Maximum Throughput

Real-Time Processing and Maximum Throughput

Optical sorting technology processes hundreds or thousands of items every single minute, dramatically exceeding manual sorting capabilities. This processing power means optical sorting technology enables production facilities to handle significantly larger volumes without expanding workforce requirements. Your investment in optical sorting technology immediately increases capacity without proportional increases in operational costs. The real-time decision-making capability of optical sorting technology means zero production delays or bottlenecks caused by sorting procedures. Optical sorting technology continuously evaluates each item and makes instantaneous ejection decisions, maintaining smooth production flow. This efficiency advantage of optical sorting technology translates directly into increased annual output and revenue potential. Facilities implementing optical sorting technology typically report production increases of 30-50 percent while reducing per-unit processing costs. The speed advantage of optical sorting technology becomes particularly valuable during peak production seasons or when fulfilling large customer orders. Your business gains competitive advantages through optical sorting technology's ability to deliver larger volumes faster than competitors still relying on manual methods.
Cost Reduction and Improved Sustainability Performance

Cost Reduction and Improved Sustainability Performance

Optical sorting technology delivers measurable financial benefits through multiple cost reduction pathways. Labor expenses decrease substantially as optical sorting technology automates sorting tasks previously requiring human workers. Optical sorting technology operational costs remain predictable and stable, unlike labor expenses subject to wage increases and staffing variability. Material waste reduction represents another significant cost advantage, as optical sorting technology minimizes loss of valuable raw materials through contamination or improper sorting. Recycling operations leveraging optical sorting technology recover higher-value material streams, increasing revenue from recovered resources. Optical sorting technology also reduces environmental impact by maximizing material recovery rates and minimizing waste sent to landfills. Your facility achieves stronger sustainability credentials through optical sorting technology implementation, supporting corporate environmental goals and appealing to environmentally conscious customers. The combination of reduced operational expenses and increased material recovery makes optical sorting technology an investment that pays dividends while advancing environmental responsibility objectives.

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

Copyright © 2026 Anhui Jiexun Optoelectronic Technology Co., Ltd. All rights reserved.  -  Privacy policy