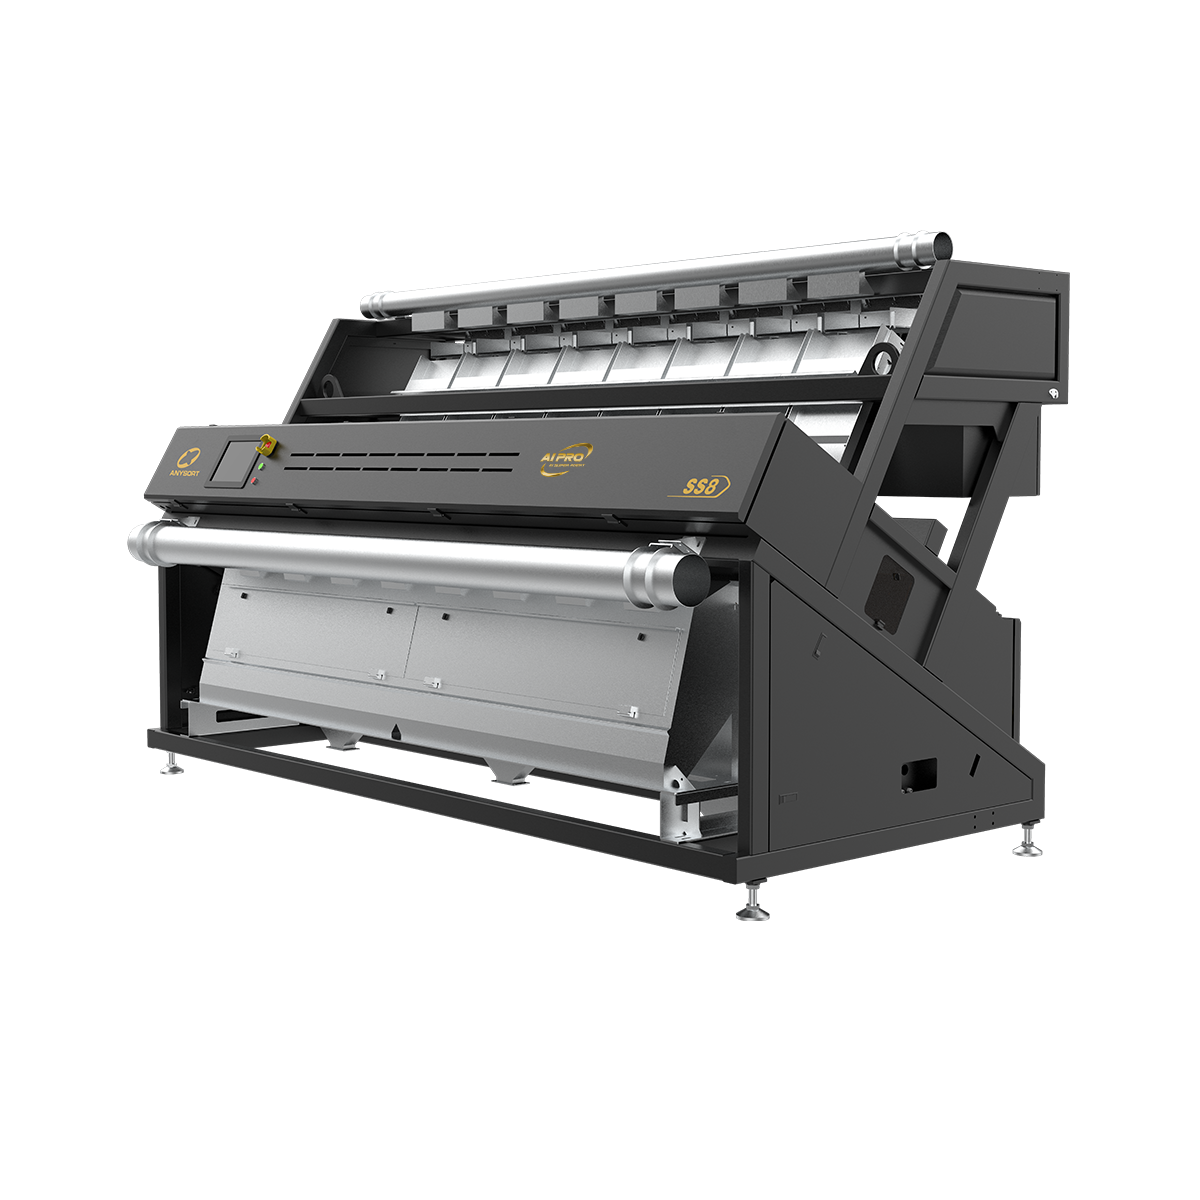
best optical sorter
The best optical sorter represents cutting-edge technology designed to revolutionize material separation and quality control across multiple industries. This advanced sorting system uses sophisticated optical sensors and artificial intelligence to identify, classify, and separate materials with exceptional precision and speed. The best optical sorter combines high-resolution cameras with specialized lighting systems to capture detailed images of each item passing through the sorting mechanism. Advanced algorithms analyze these images in real-time, detecting color variations, size differences, shape irregularities, and material composition characteristics. The technology behind the best optical sorter enables operators to remove defective products, foreign materials, and contaminated items automatically, ensuring only high-quality materials proceed through production lines. Modern optical sorters feature multiple sorting lanes, allowing simultaneous processing of various material streams. These systems integrate seamlessly with existing production infrastructure and provide customizable sorting parameters to meet specific industry requirements. The best optical sorter delivers consistent, reliable results while significantly reducing manual labor and human error. Industries including food processing, recycling, mining, pharmaceuticals, and manufacturing rely on this best optical sorter technology to maintain product quality standards and optimize operational efficiency. The system's adaptability makes it suitable for processing diverse materials from grains and vegetables to plastic pellets and mineral ores. Real-time performance monitoring and data analytics provide valuable insights into production efficiency and material quality metrics.

 EN