 EN
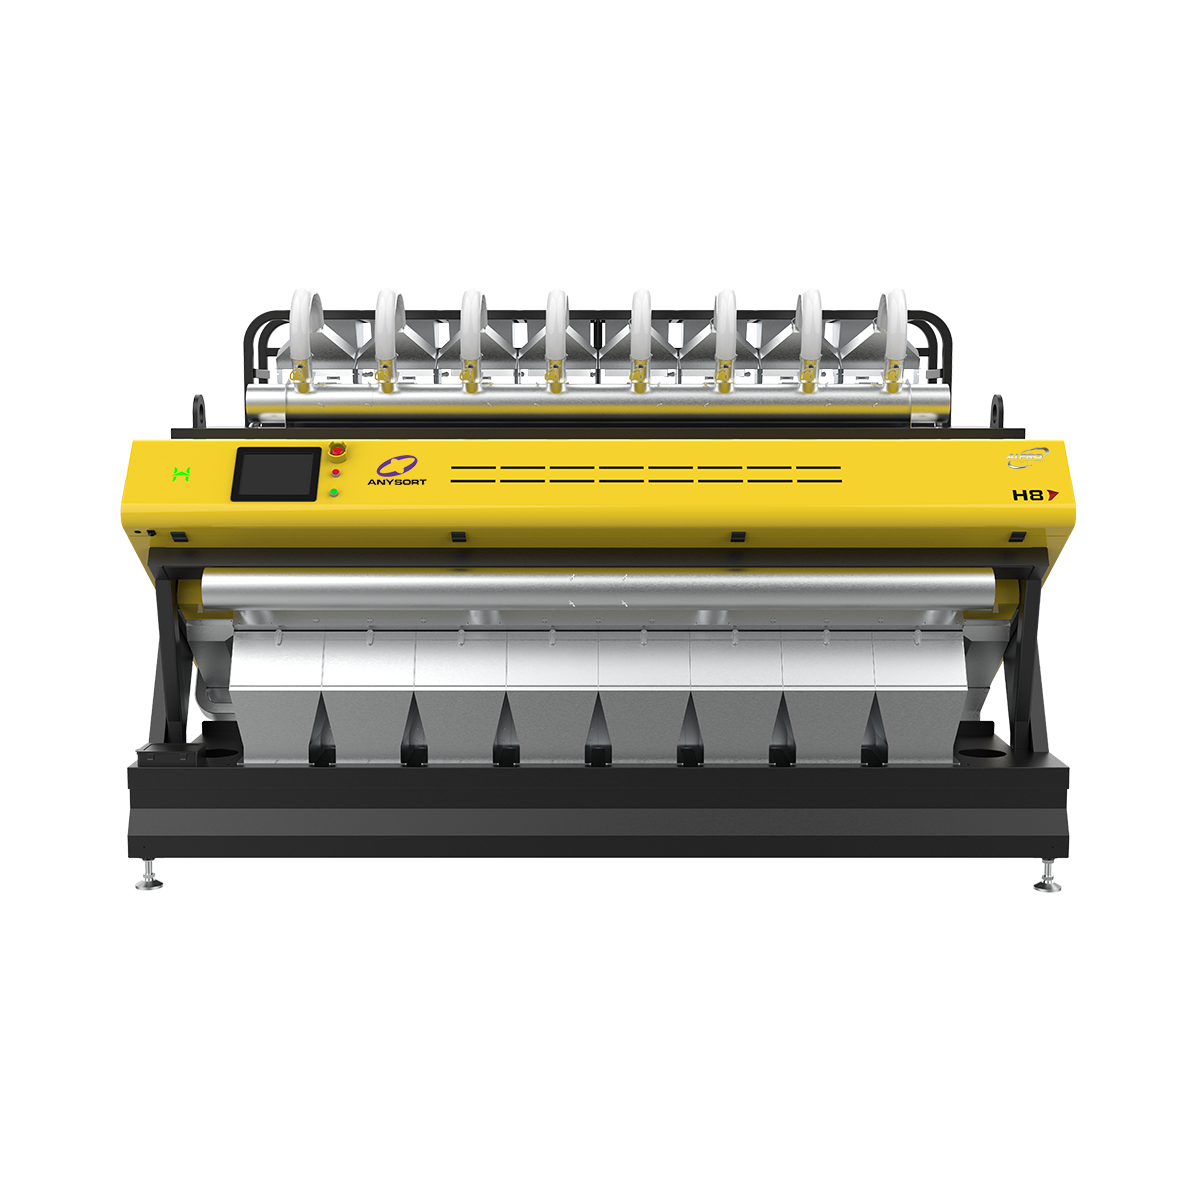
The global demand for precision sorting technology has surged dramatically, with color sorter machine manufacturers in China leading innovation across agricultural and industrial sectors. Chinese color sorter machine manufacturers have established themselves as pioneers in developing advanced sorting solutions that combine artificial intelligence with optical sensing technology. These manufacturers serve industries ranging from grain processing to recycling, offering machines that dramatically improve product quality while reducing operational costs. Understanding the landscape of leading color sorter machine manufacturers helps businesses make informed decisions when selecting sorting equipment for their operations.
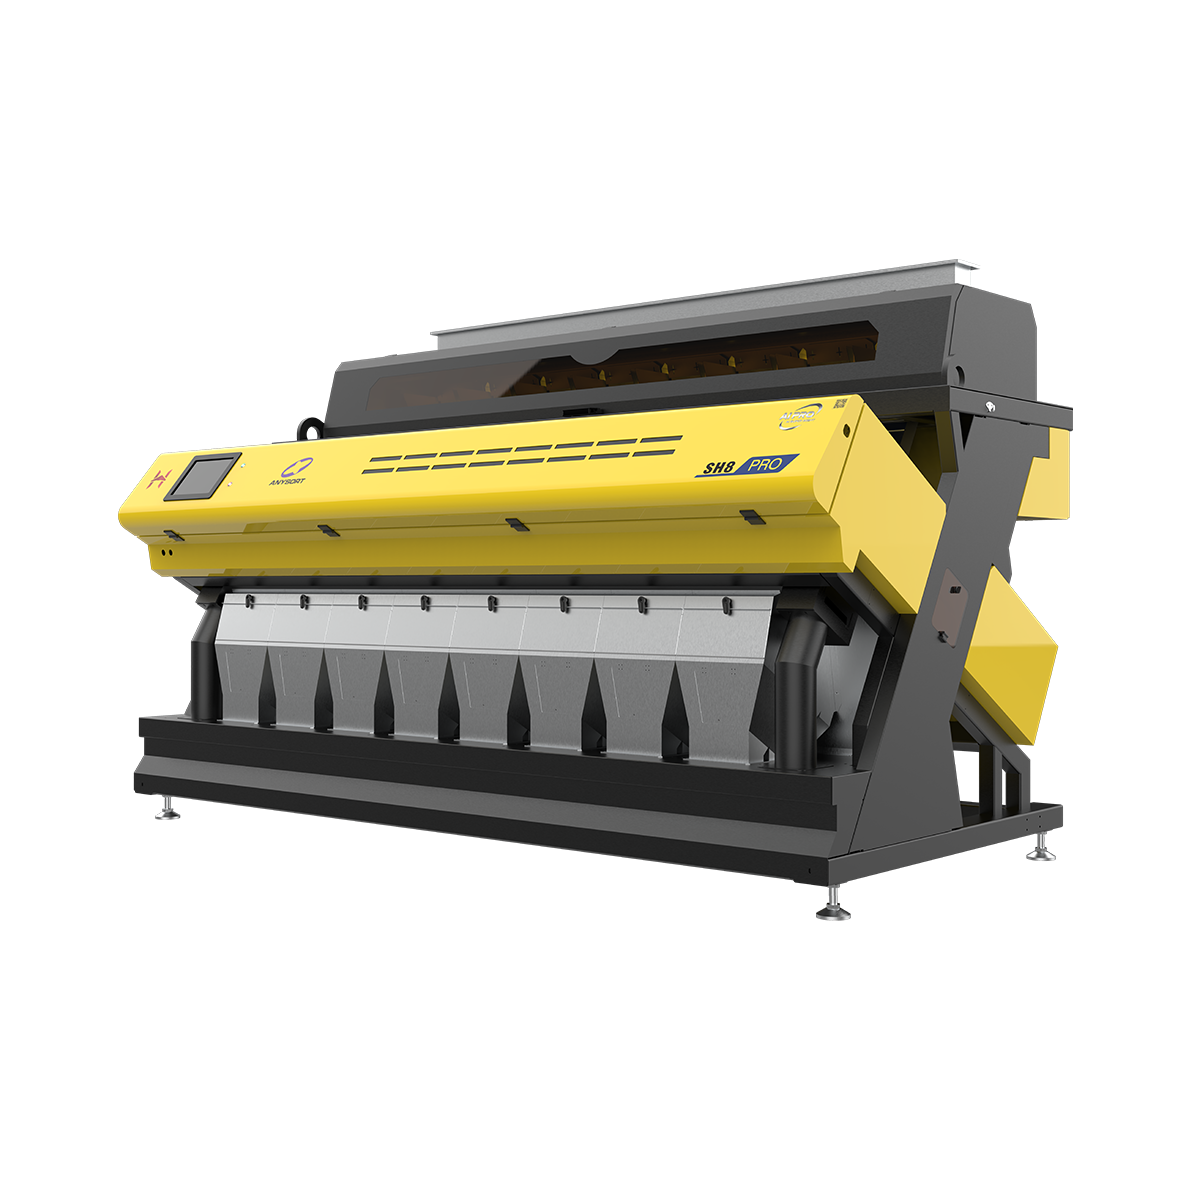
China has become the manufacturing hub for color sorter machine manufacturers because of substantial investments in research and development, cost-effective production capabilities, and access to comprehensive supply chains. The competitive environment among color sorter machine manufacturers has driven continuous technological advancement, resulting in machines that offer superior sorting accuracy, faster processing speeds, and improved reliability. When evaluating color sorter machine manufacturers, it is essential to assess their technical expertise, product specifications, customer support infrastructure, and proven track record in your specific industry vertical.
Key Innovation Areas Among Color Sorter Machine Manufacturers
Artificial Intelligence and Machine Learning Integration
Modern color sorter machine manufacturers integrate sophisticated artificial intelligence systems that enable machines to learn and adapt to sorting requirements in real time. These AI-powered color sorter machine manufacturers develop systems capable of distinguishing between hundreds of color variations and defect patterns with exceptional precision. The color sorter machine manufacturers utilizing machine learning algorithms achieve higher throughput rates while maintaining consistent quality standards across diverse product types. Advanced color sorter machine manufacturers continuously improve their AI models by collecting data from thousands of installations worldwide, creating increasingly intelligent sorting solutions.
Multi-Spectrum Sensor Technology
Leading color sorter machine manufacturers employ multi-spectrum imaging technology that captures data across visible and near-infrared wavelengths. Color sorter machine manufacturers investing in sensor innovation can detect defects invisible to single-spectrum systems, including internal damage, moisture content variations, and quality inconsistencies. These advanced color sorter machine manufacturers provide sorting capabilities that traditional optical systems cannot match. The technology differentiation among color sorter machine manufacturers reflects their commitment to solving complex industrial sorting challenges.
Applications Driving Demand for Color Sorter Solutions
Agricultural Processing and Grain Sorting
Agricultural applications represent the largest market segment for color sorter machine manufacturers globally. Color sorter machine manufacturers serve rice mills, grain processors, and legume sorting facilities with machines designed to remove discolored grains, damaged kernels, and foreign materials. The efficiency gains achieved by color sorter machine manufacturers in this sector directly impact product quality and mill profitability. Color sorter machine manufacturers continue to develop specialized solutions for regional crops, adapting their machines to handle crops like paddy rice, maize, soybeans, and specialty grains.
Industrial Material Recycling and Processing
Color sorter machine manufacturers increasingly serve recycling facilities and materials recovery operations sorting plastics, minerals, and waste streams. Advanced color sorter machine manufacturers enable recyclers to achieve higher material purity levels, opening access to premium markets. The application flexibility of modern color sorter machine manufacturers makes them valuable across diverse recycling workflows. Color sorter machine manufacturers working with recycling companies have developed systems that handle irregular shapes, varying transparencies, and contaminated material streams.
Evaluating Color Sorter Machine Manufacturers for Your Needs
Technical Specifications and Performance Metrics
When comparing color sorter machine manufacturers, examine throughput capacity measured in tons per hour, sorting accuracy rates, and the number of color channels available. Reliable color sorter machine manufacturers provide transparent performance data validated through third-party testing. Color sorter machine manufacturers offering modular designs allow capacity upgrades without complete system replacement. The processing speed capabilities of different color sorter machine manufacturers directly impact your return on investment timeline.
Support Infrastructure and Implementation Partnership
Choosing among color sorter machine manufacturers requires assessing their technical support availability, training programs, and spare parts distribution networks. Experienced color sorter machine manufacturers maintain regional service centers and provide remote diagnostic capabilities for rapid issue resolution. The best color sorter machine manufacturers understand your specific production requirements and customize solutions accordingly. Long-term success with color sorter machine manufacturers depends on their commitment to ongoing support, software updates, and system optimization throughout the machine lifecycle.
Future Trends Among Color Sorter Machine Manufacturers
Cloud Connectivity and Data Analytics
Leading color sorter machine manufacturers are integrating cloud connectivity features enabling real-time monitoring and predictive maintenance capabilities. Forward-thinking color sorter machine manufacturers collect anonymized performance data to identify optimization opportunities and alert operators to potential issues before failures occur. Digital integration among color sorter machine manufacturers transforms sorting machines from standalone equipment into connected nodes within comprehensive quality management systems. The color sorter machine manufacturers developing advanced cloud platforms gain competitive advantages through superior customer insights.
Sustainability and Energy Efficiency
Environmental considerations increasingly influence purchasing decisions, prompting color sorter machine manufacturers to develop energy-efficient models. Progressive color sorter machine manufacturers reduce power consumption through optimized LED systems, efficient pneumatic designs, and intelligent processing algorithms. Sustainable practices among color sorter machine manufacturers appeal to environmentally conscious enterprises seeking to reduce their operational carbon footprint. Color sorter machine manufacturers emphasizing sustainability contribute to circular economy objectives while lowering operational expenses.
FAQ
What distinguishes leading Chinese color sorter machine manufacturers from competitors?
Leading Chinese color sorter machine manufacturers differentiate through continuous AI innovation, superior sensor technology, and extensive technical support infrastructure. These manufacturers combine affordable pricing with cutting-edge capabilities that rival international competitors. Their commitment to research and development, combined with rapid product iteration cycles, enables color sorter machine manufacturers to introduce advanced features faster than many established international firms.
How do color sorter machine manufacturers determine the right system for my application?
Professional color sorter machine manufacturers conduct detailed consultations assessing your material types, production volumes, quality requirements, and space constraints. They analyze your specific sorting challenges and recommend machine configurations from their product portfolio that optimize performance for your requirements. Reputable color sorter machine manufacturers provide trial periods or demonstrations allowing you to evaluate equipment before purchase commitment.
What is the typical lifespan of systems from color sorter machine manufacturers?
Well-engineered color sorter machine manufacturers design systems with operational lifespans of 8–12 years under normal operating conditions. Longevity depends on maintenance quality, operating environment conditions, and material handling practices. Leading color sorter machine manufacturers provide spare parts availability for extended periods, ensuring equipment can be serviced and updated throughout its working life.