Optical Separator: Precision Material Sorting

All Categories

optical separator

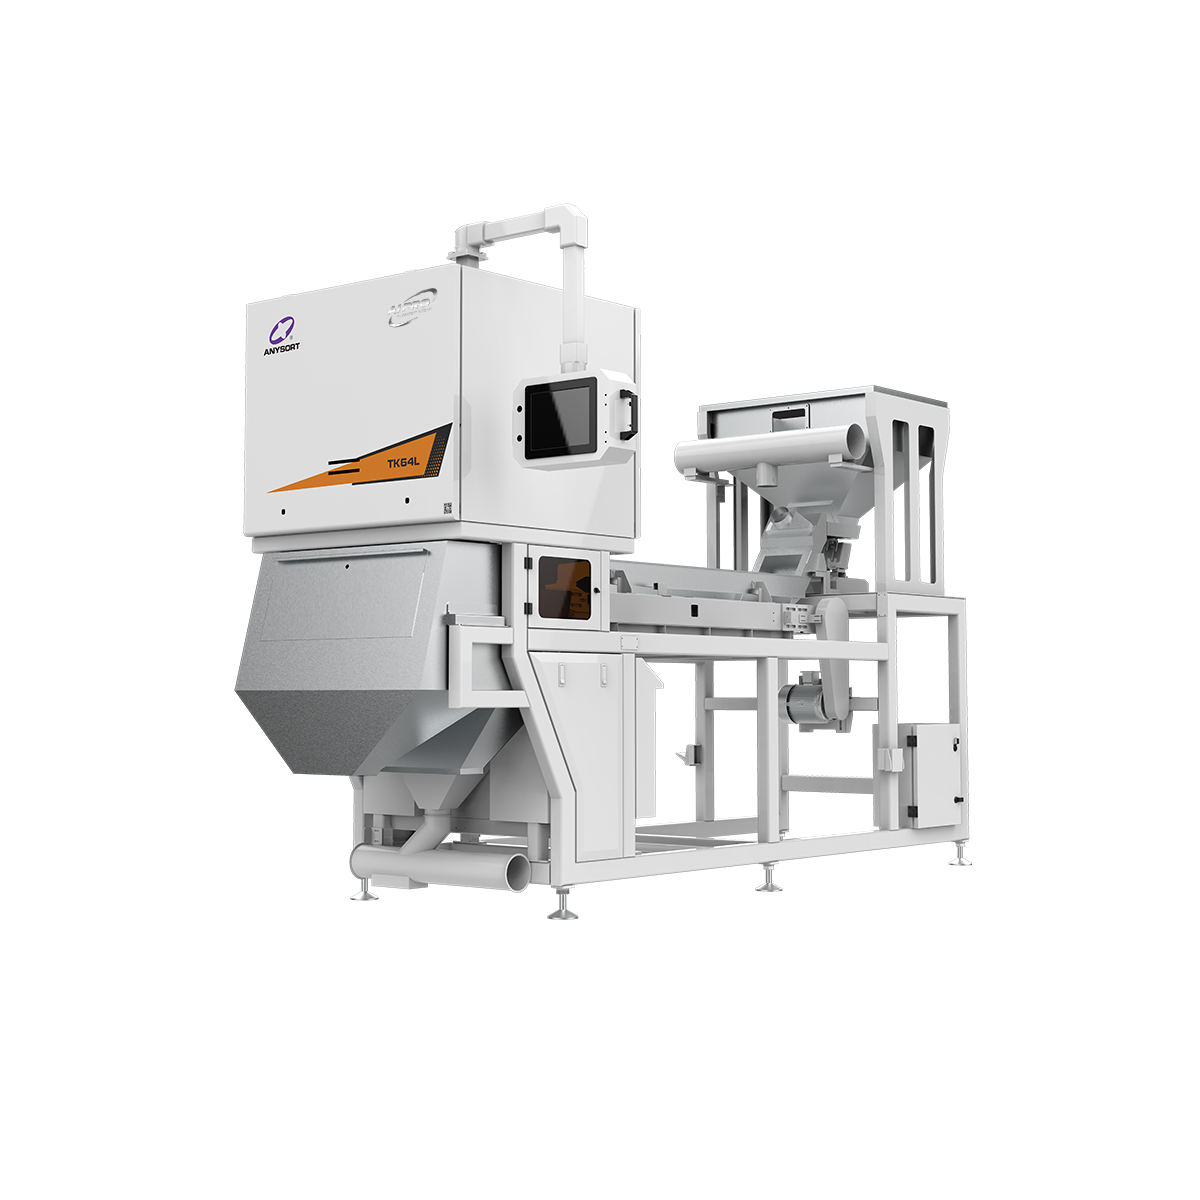
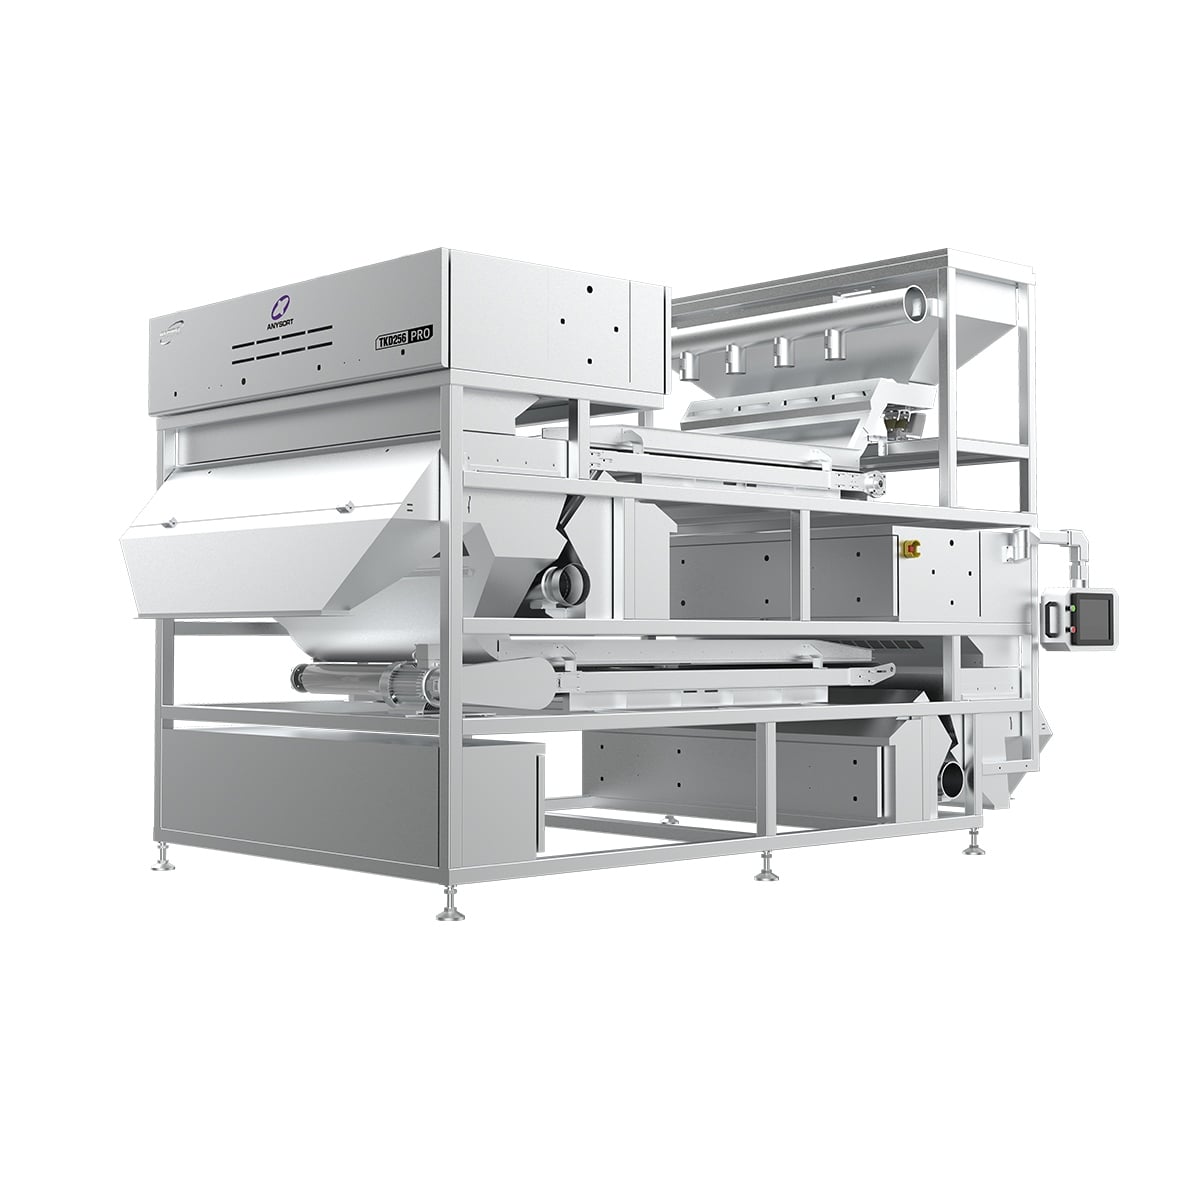
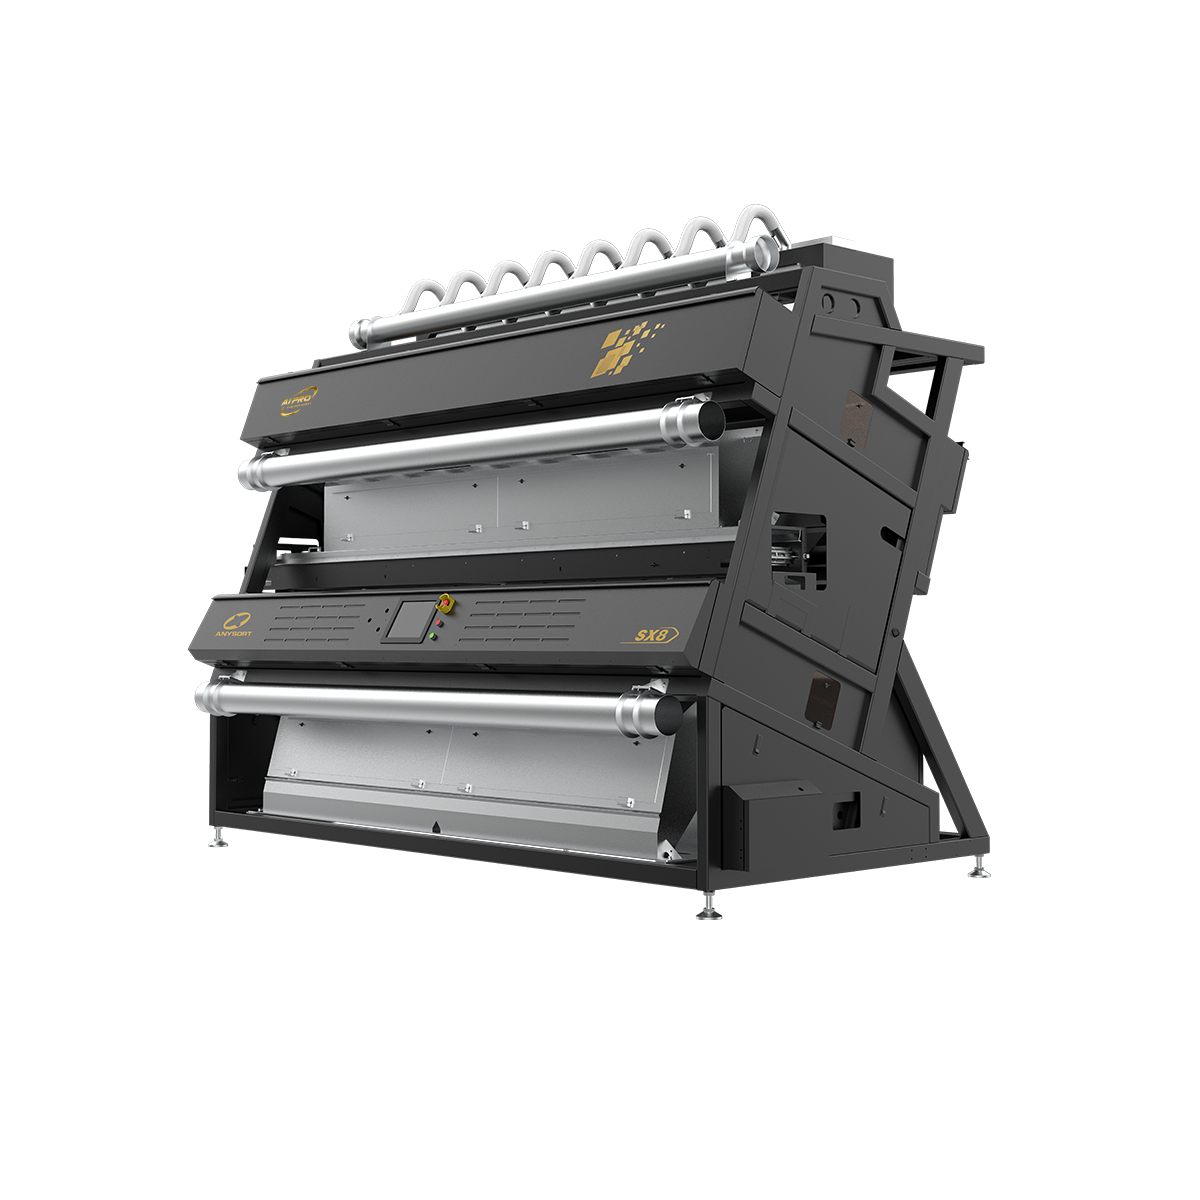
An optical separator is a sophisticated sorting device that uses advanced light-based technology to distinguish and separate materials based on their optical properties. This innovative equipment represents a breakthrough in material sorting, offering precision and efficiency that traditional mechanical methods cannot match. The optical separator works by analyzing how different materials reflect, absorb, or transmit light, enabling accurate identification and separation of items at remarkable speeds. The core function of an optical separator is to automate the sorting process across multiple industries. An optical separator can process thousands of items per minute, identifying subtle differences in color, shape, and material composition that human operators would miss. Technological features of an advanced optical separator include high-resolution cameras, sophisticated image recognition algorithms, and real-time processing capabilities. These components work in harmony to ensure consistent, reliable separation results. Applications for an optical separator span numerous sectors including food processing, recycling, mining, agriculture, and manufacturing. In food processing, an optical separator removes defective or foreign materials from grains, nuts, and other products. Recycling facilities use an optical separator to sort plastics, metals, and other materials with unprecedented accuracy. The versatility of an optical separator makes it an essential tool for businesses seeking to improve product quality, reduce waste, and enhance operational efficiency while maintaining stringent industry standards.

Popular Products

Choosing an optical separator delivers transformative benefits that directly impact your bottom line and operational performance. First and foremost, an optical separator dramatically improves sorting accuracy, eliminating manual labor inefficiencies and human error. This precision ensures that only quality materials move forward in your production process, protecting your brand reputation and customer satisfaction. The operational benefits of an optical separator are substantial and immediate. By automating the sorting process, an optical separator reduces labor costs significantly while increasing throughput capacity. Your team can focus on higher-value tasks rather than repetitive, tedious sorting work. An optical separator operates continuously without fatigue, delivering consistent results throughout your production day, which directly translates to increased profitability. From an application perspective, an optical separator adapts to your specific industry requirements. Whether you're processing food products, managing recycling operations, or handling agricultural commodities, an optical separator customizes its sorting parameters to meet your exact specifications. The flexibility of an optical separator means you can upgrade your capabilities without replacing entire systems. For decision-making purposes, an optical separator provides clear competitive advantages. Investment in an optical separator typically pays for itself within months through waste reduction, improved product quality, and reduced labor expenses. Real-time quality assurance from an optical separator protects your production integrity and ensures compliance with industry regulations. The scalability of an optical separator means it grows with your business, making it a smart long-term investment that delivers measurable returns and positions your company as an industry leader committed to excellence and innovation.

Tips And Tricks

What Factors Affect Tea Color Sorter Performance and Accuracy?

05

Aug

What Factors Affect Tea Color Sorter Performance and Accuracy?

The precision of a tea color sorter directly determines the quality consistency of finished tea products. Understanding the factors that influence tea color sorter performance and accuracy is essential for tea processors seeking to maintain competiti...
View More
How Does Nuts Sorter Technology Ensure Quality?

19

Aug

How Does Nuts Sorter Technology Ensure Quality?

The global nuts processing industry relies on precision and consistency to meet strict quality standards and regulatory requirements. A nuts sorter has become indispensable for processors seeking to eliminate defects, contaminants, and substandard pr...
View More
How does optical sorting technology detect defective rice grains?

22

Aug

How does optical sorting technology detect defective rice grains?

Modern rice processing demands precision and consistency, which is why understanding the detection mechanisms behind advanced equipment has become essential for producers. A rice color sorter represents one of the most significant technological break...
View More
How Do Color Sorters Improve Product Quality?

26

Aug

How Do Color Sorters Improve Product Quality?

Product quality stands as a critical differentiator in competitive industrial markets, and achieving consistency at scale requires more than manual oversight. A color sorter represents one of the most effective technologies for identifying and removi...
View More

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

optical separator

Precision Light-Based Detection Technology

Precision Light-Based Detection Technology

The optical separator employs cutting-edge light-based detection systems that identify materials with exceptional accuracy. This optical separator uses multiple light wavelengths and advanced sensors to analyze each item's unique optical signature within milliseconds. The technology behind an optical separator enables detection of defects, contamination, and material composition differences that remain invisible to the human eye. This precision ensures that your final products meet the highest quality standards while minimizing waste throughout your production process. By investing in an optical separator, you guarantee consistent quality control that protects your brand reputation and customer loyalty.
High-Speed Processing and Increased Throughput

High-Speed Processing and Increased Throughput

An optical separator processes materials at remarkable speeds, handling thousands of items per minute without compromising accuracy. This exceptional performance means an optical separator significantly increases your production capacity without requiring additional facility space or equipment. The speed of an optical separator allows you to meet demanding market deadlines while maintaining premium quality standards. Compared to traditional sorting methods, an optical separator delivers productivity gains that directly translate to reduced per-unit processing costs. The efficiency of an optical separator enables you to maximize resource utilization, improve delivery timelines, and capture additional market opportunities while maintaining operational excellence and customer satisfaction.
Versatile Multi-Industry Applications and Adaptability

Versatile Multi-Industry Applications and Adaptability

An optical separator's sophisticated technology adapts seamlessly across diverse industries and product types. Whether sorting food products, recycling materials, mining operations, or agricultural commodities, an optical separator customizes its parameters for optimal performance. This optical separator's versatility means you can expand your product lines or enter new markets without replacing core infrastructure. The adaptability of an optical separator makes it an intelligent investment for growing businesses seeking flexibility and long-term value. With programmable sorting criteria, an optical separator evolves with your business needs, ensuring your equipment investment remains relevant and valuable for years to come.

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

Copyright © 2026 Anhui Jiexun Optoelectronic Technology Co., Ltd. All rights reserved.  -  Privacy policy