optical grain sorter
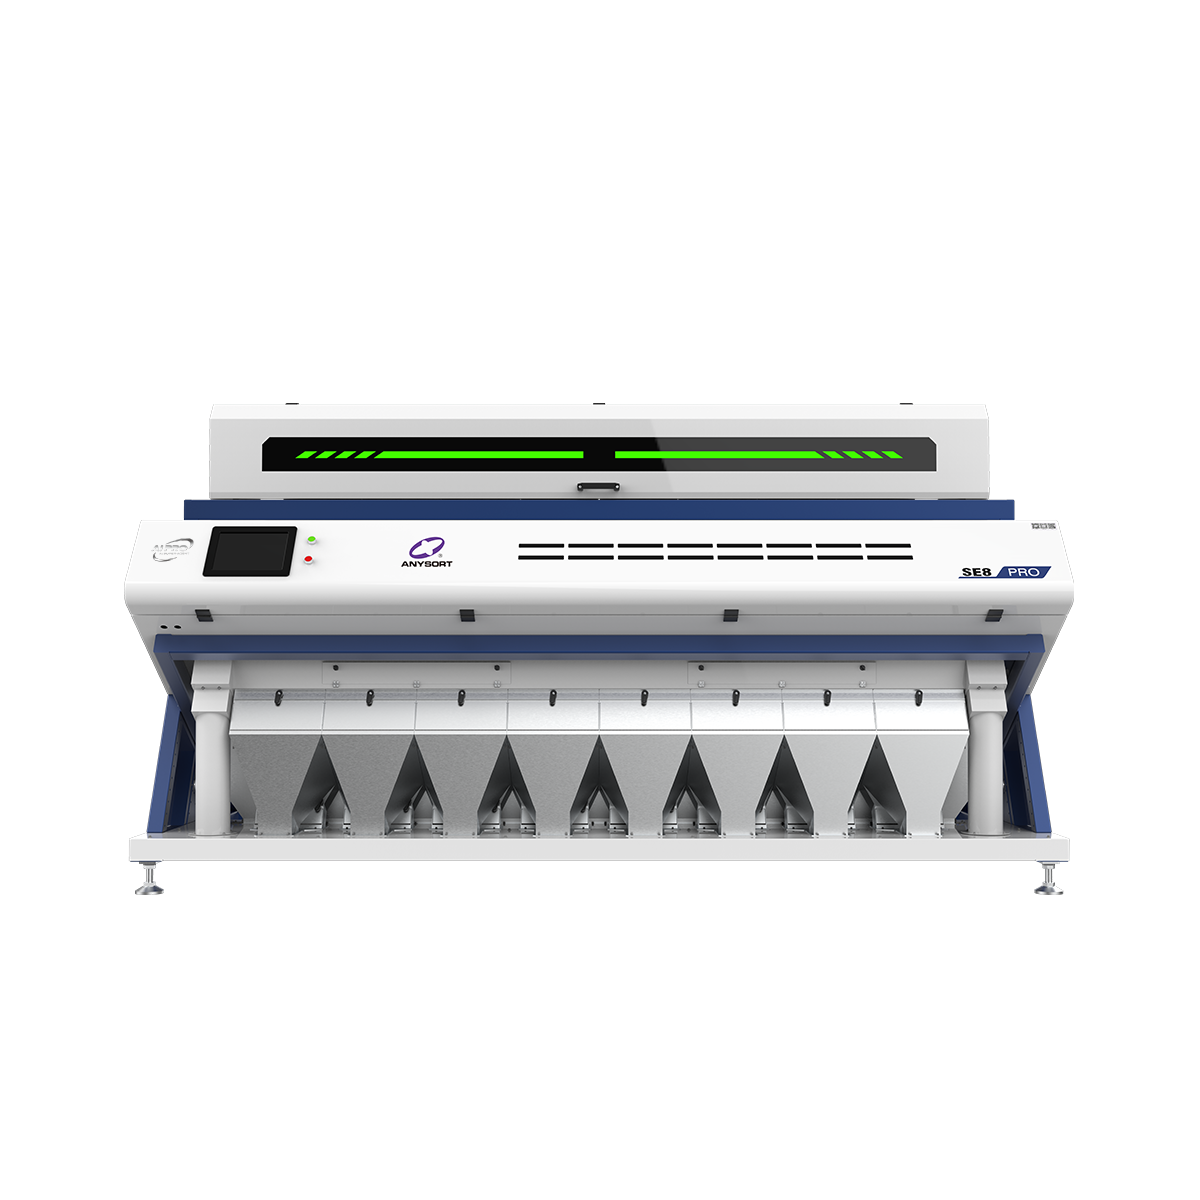
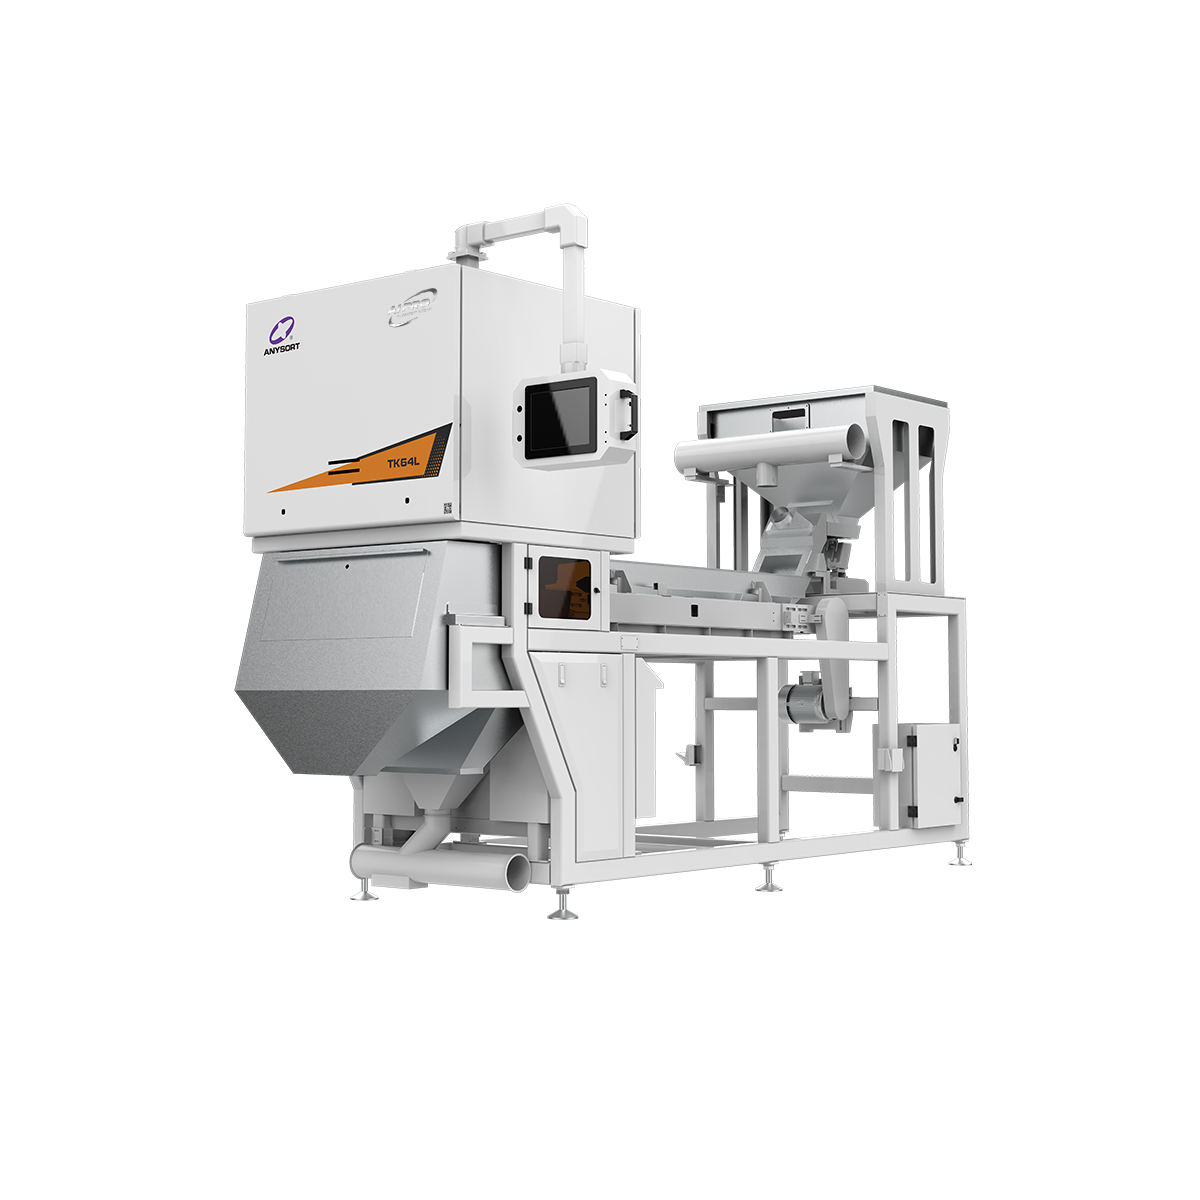
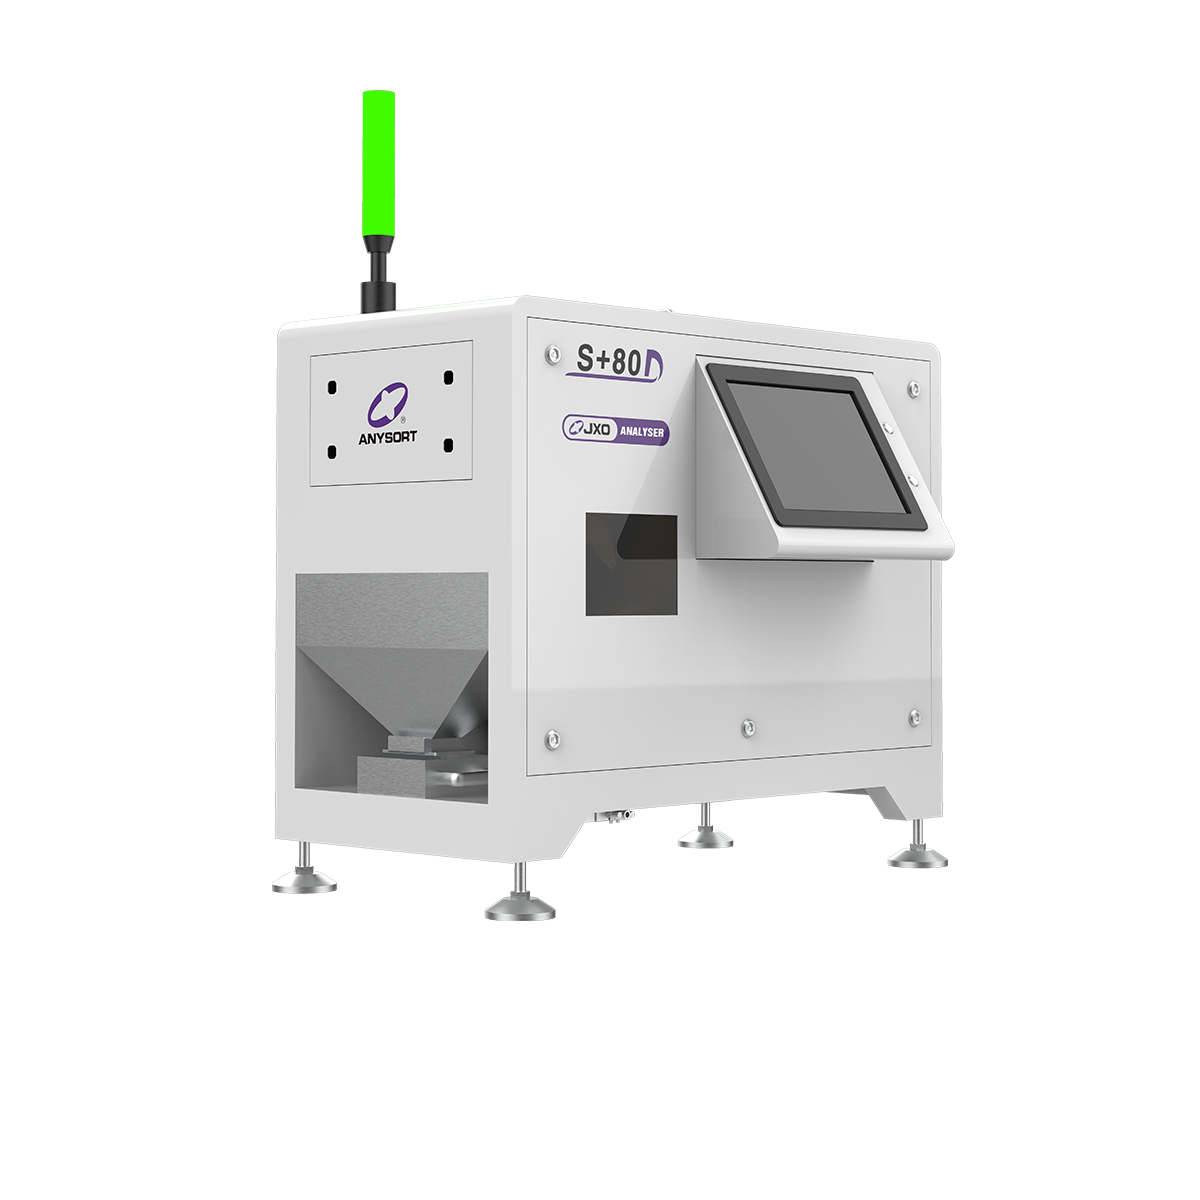
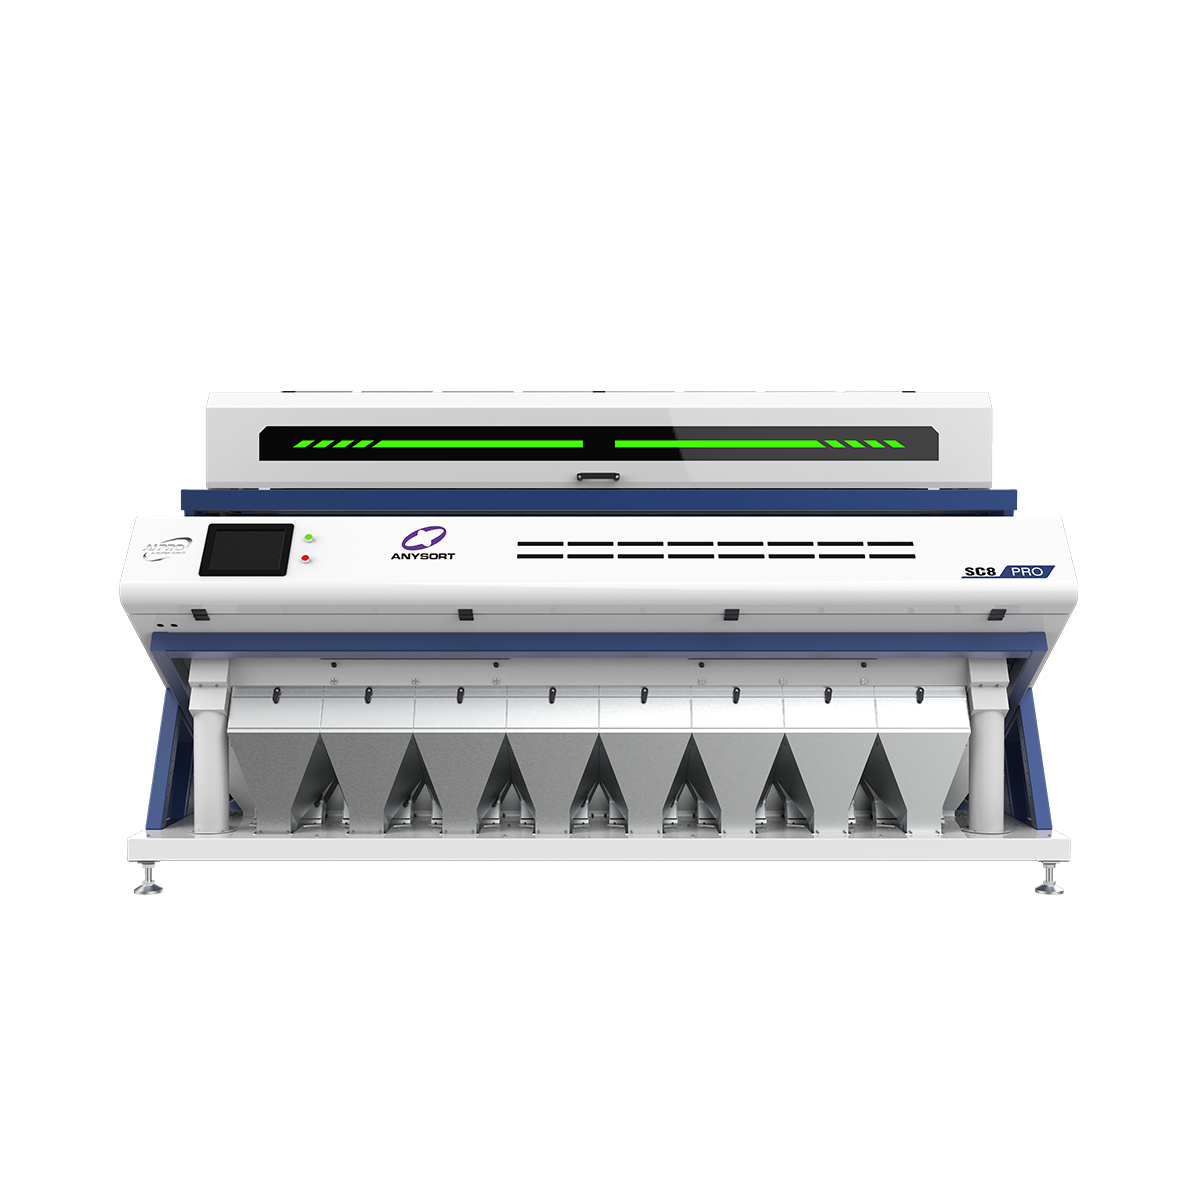
An optical grain sorter is an advanced machine that automatically separates and classifies grains based on quality, color, and physical characteristics. This innovative optical grain sorter uses cutting-edge sensor technology to inspect each grain individually, ensuring consistent product quality. The optical grain sorter operates by capturing high-resolution images of grains as they pass through the sorting chamber, analyzing these images in real-time to identify defects, discoloration, and foreign materials. An optical grain sorter is essential for grain processing facilities seeking to improve efficiency and reduce manual labor costs. The primary functions of an optical grain sorter include detecting broken kernels, removing discolored grains, eliminating foreign objects, and sorting by size specifications. Modern optical grain sorter systems integrate artificial intelligence and machine learning algorithms to enhance accuracy and adaptability to different grain varieties. The technological features of an optical grain sorter encompass high-speed cameras, LED lighting systems, pneumatic ejection mechanisms, and sophisticated processing software. Applications for an optical grain sorter span across rice mills, wheat processing plants, legume facilities, and seed production centers. By implementing an optical grain sorter, businesses achieve higher throughput rates while maintaining superior grain quality standards. The optical grain sorter represents a significant investment in automation technology that delivers measurable returns through improved product consistency and reduced waste throughout the entire grain processing operation.

 EN