Optical Sorter Market: Solutions

All Categories

optical sorter market

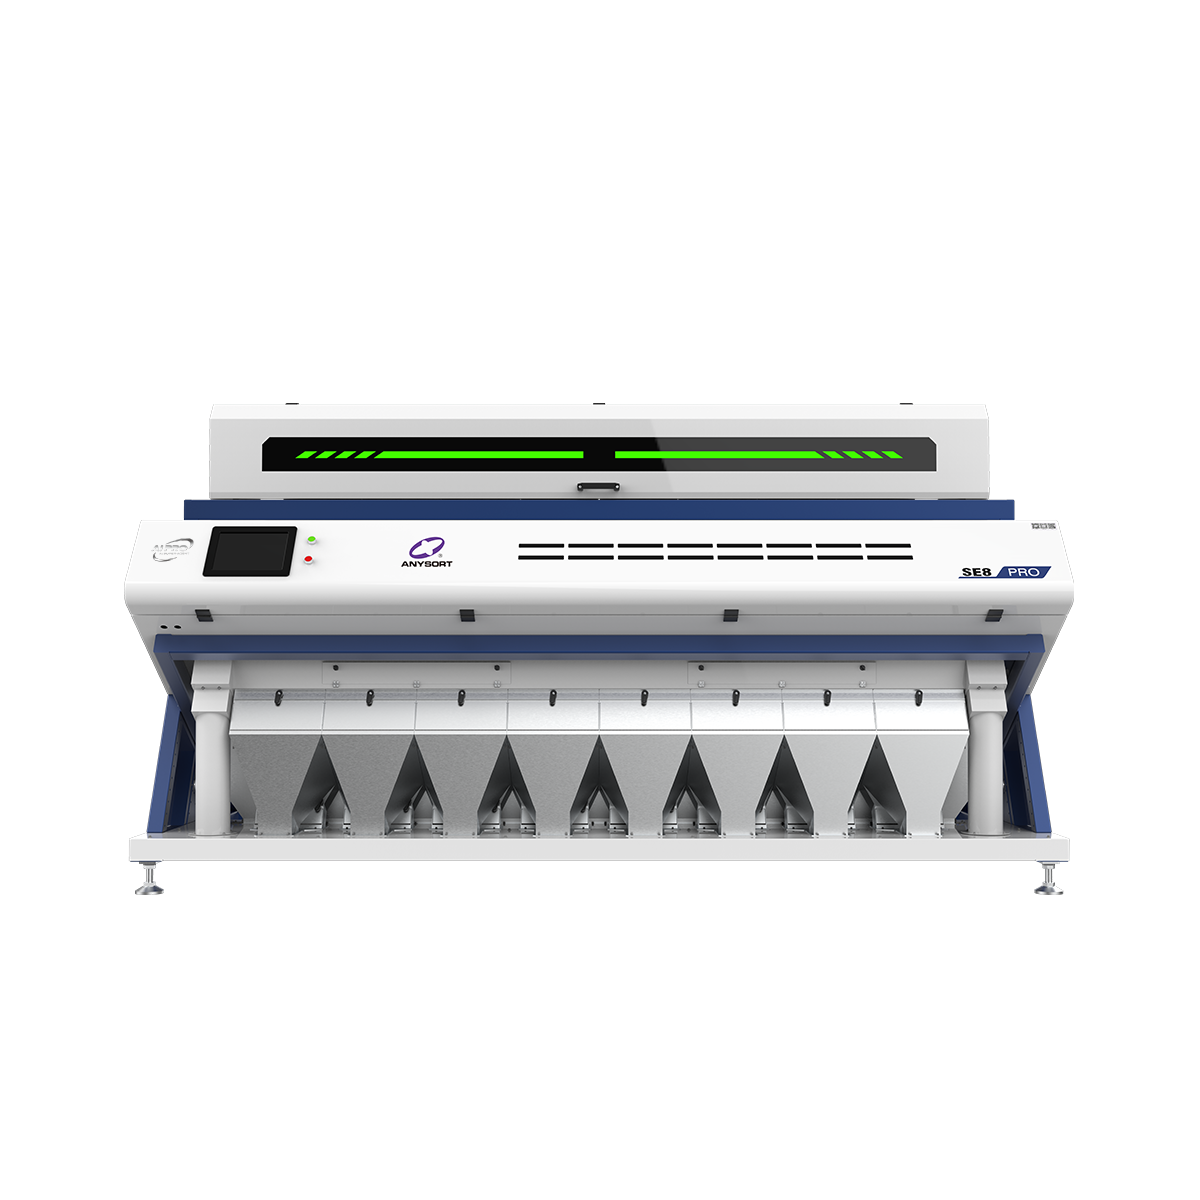
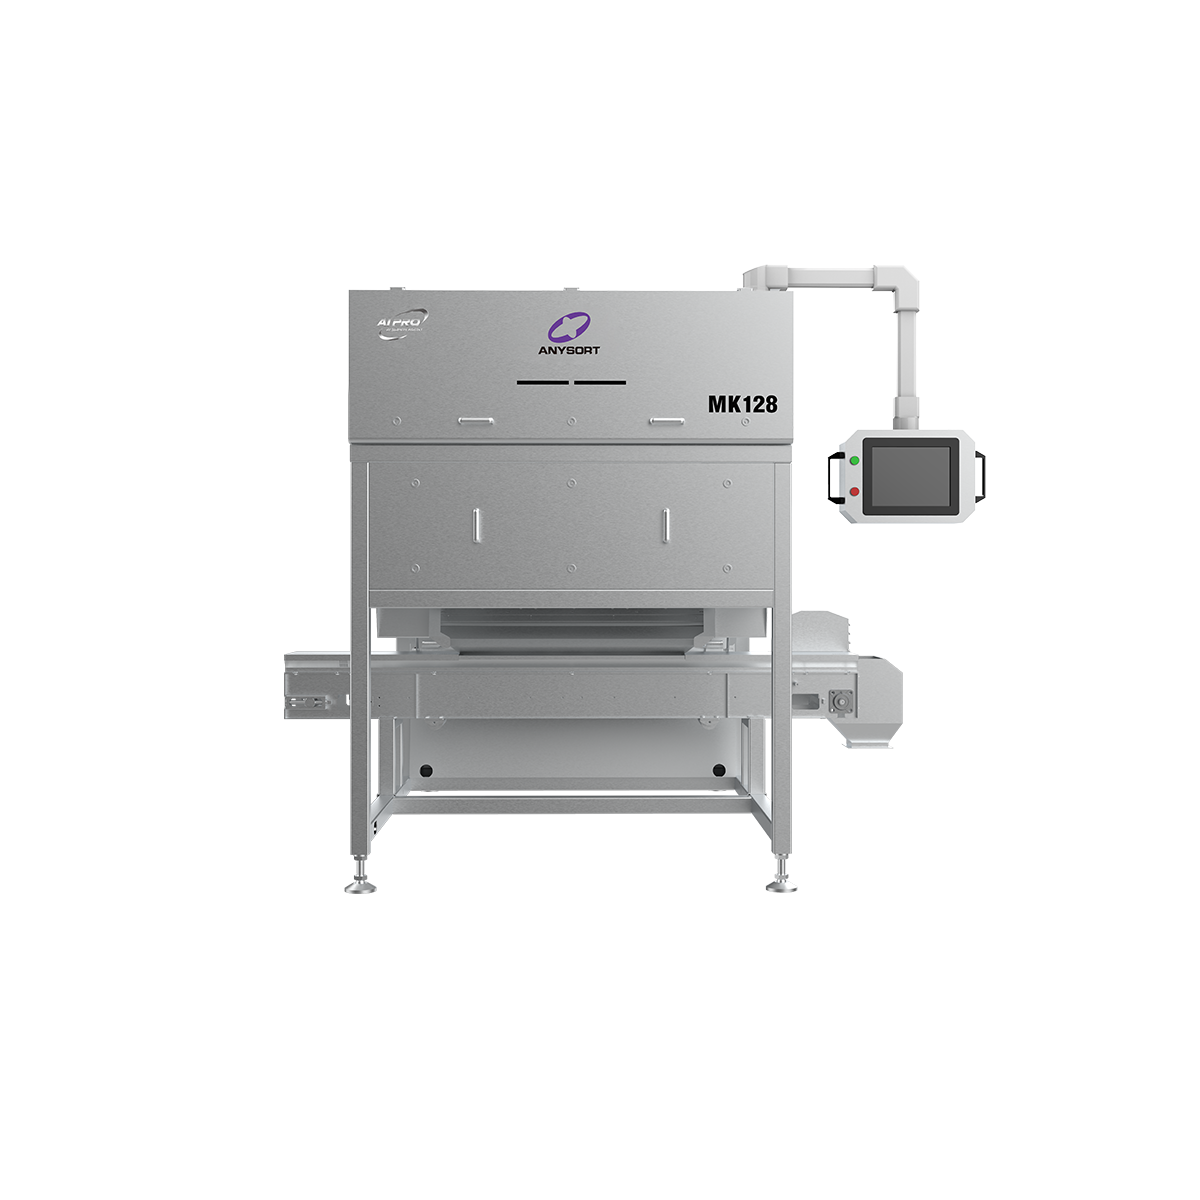
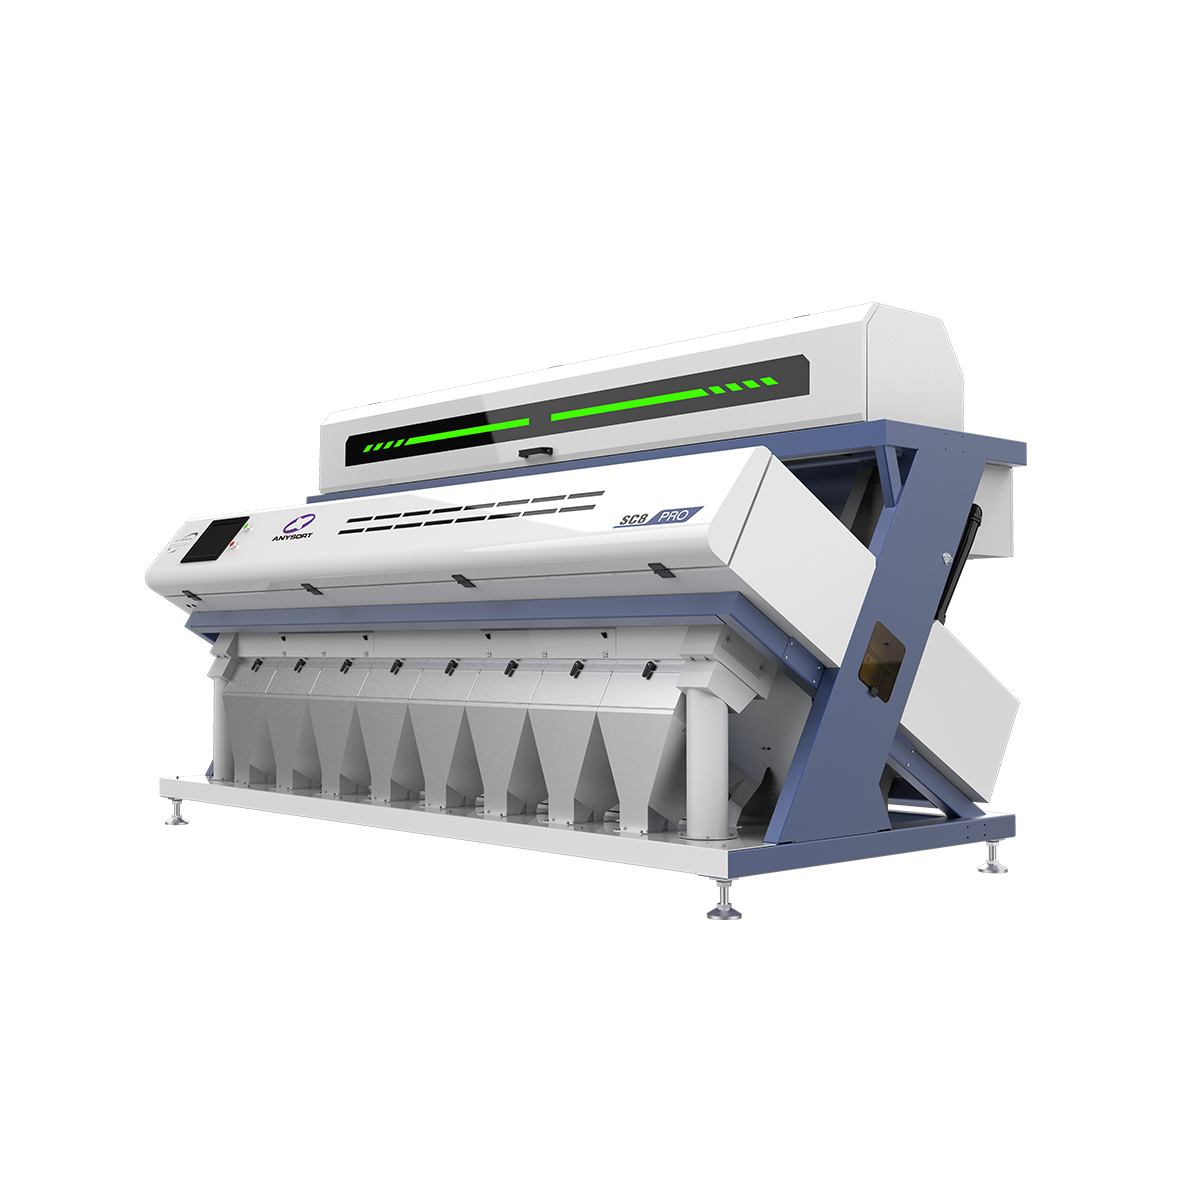
The optical sorter market represents a transformative technology revolutionizing material sorting and classification processes across numerous industries. An optical sorter market solution utilizes advanced imaging and sensor technology to detect, analyze, and separate materials based on color, size, shape, and composition with exceptional precision and speed. These intelligent machines employ sophisticated algorithms and real-time processing capabilities to identify contaminants, defects, and variations that human operators might miss. Optical sorter market systems function by scanning products moving along conveyor belts at high speeds. Multiple cameras and sensors capture detailed images from various angles, while artificial intelligence processes this data instantaneously. The system then triggers pneumatic or mechanical ejection mechanisms to remove unwanted items with remarkable accuracy. This optical sorter market technology finds extensive applications in food processing, recycling, mining, agriculture, and manufacturing sectors. Key technological features include high-resolution imaging systems, multi-spectral sensors, machine learning algorithms, and rapid response mechanisms. The optical sorter market demonstrates remarkable versatility, handling everything from grains and nuts to plastics and minerals. Modern optical sorter market equipment integrates seamlessly with existing production lines, offering flexible configurations for different operational requirements. This continuous innovation within the optical sorter market ensures businesses maintain competitive advantages while improving product quality and operational efficiency significantly.

New Products

The optical sorter market delivers substantial practical benefits that directly enhance business performance and customer satisfaction. By automating the sorting process, companies dramatically reduce labor costs while minimizing human error in material classification. This automation leads to faster processing speeds, allowing facilities to handle larger volumes without proportional increases in staffing expenses. Operational benefits of choosing an optical sorter market solution include improved product consistency and quality assurance. These systems identify and remove defective items before they reach consumers, protecting brand reputation and reducing liability concerns. The optical sorter market technology enables businesses to recover valuable materials that manual sorting might overlook, effectively increasing revenue from waste streams. Application suitability represents another compelling advantage of the optical sorter market. Whether processing agricultural products, recycled materials, or manufactured goods, these systems adapt to diverse requirements. Food processors benefit from contamination detection that ensures consumer safety, while recycling facilities increase material purity and market value through precise separation. Decision-useful product context shows that the optical sorter market investment delivers rapid return on investment through improved throughput and reduced waste. Energy-efficient operations minimize environmental impact and operational costs simultaneously. The optical sorter market technology provides real-time data analytics, enabling operators to monitor performance metrics and optimize processes continuously. Long-term reliability and minimal maintenance requirements make these systems economically attractive, ensuring businesses achieve sustainable competitive advantages while maintaining strict quality standards throughout their operations.

Practical Tips

How can rice color sorters improve grain quality?

08

Aug

How can rice color sorters improve grain quality?

Rice color sorters represent a transformative technology in modern grain processing, fundamentally changing how producers maintain and enhance the quality of their rice output. By utilizing advanced optical scanning and artificial intelligence, a ric...
View More
How Much Does a Color Sorter Machine Cost?

12

Aug

How Much Does a Color Sorter Machine Cost?

Understanding the investment required for a color sorter machine is essential for businesses in agriculture, food processing, and recycling sectors. The cost of a color sorter machine varies significantly based on capacity, technology sophistication,...
View More
How does optical sorting technology detect defective rice grains?

22

Aug

How does optical sorting technology detect defective rice grains?

Modern rice processing demands precision and consistency, which is why understanding the detection mechanisms behind advanced equipment has become essential for producers. A rice color sorter represents one of the most significant technological break...
View More
How Do Color Sorters Improve Product Quality?

26

Aug

How Do Color Sorters Improve Product Quality?

Product quality stands as a critical differentiator in competitive industrial markets, and achieving consistency at scale requires more than manual oversight. A color sorter represents one of the most effective technologies for identifying and removi...
View More

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

optical sorter market

Advanced Imaging and Sensor Integration

Advanced Imaging and Sensor Integration

The optical sorter market excels through cutting-edge imaging technology that captures comprehensive product data with extraordinary precision. Multiple high-resolution cameras simultaneously scan materials from different angles, creating detailed three-dimensional profiles. These sensors detect minute variations in color, texture, and composition that would be invisible to human inspectors. Multi-spectral imaging capabilities within the optical sorter market extend beyond visible light, identifying internal quality factors and hidden defects. Infrared sensors detect temperature variations indicating spoilage or damage, while X-ray technology penetrates opaque materials to assess internal structure. The optical sorter market systems process millions of data points per second, ensuring no product escapes thorough evaluation. This technological sophistication enables the optical sorter market to achieve contamination detection rates exceeding 99 percent accuracy. Real-time image processing combined with sophisticated algorithms means sorting decisions occur within milliseconds, maintaining production line speeds while guaranteeing quality. The integration of artificial intelligence continuously improves accuracy through machine learning adaptation.
Efficiency and Cost Reduction

Efficiency and Cost Reduction

Investing in the optical sorter market generates immediate financial returns through dramatic efficiency improvements. Automated sorting eliminates manual labor expenses while processing material volumes that would require extensive staff resources. The optical sorter market reduces operational costs by decreasing sorting time and improving throughput capacity, allowing facilities to achieve greater output with existing infrastructure. Waste reduction represents a critical financial advantage of the optical sorter market. By accurately identifying valuable materials within waste streams, companies recover products previously discarded. This capability transforms waste management from a cost center into a profit center. The optical sorter market enables recycling facilities to achieve higher material purity standards, commanding premium prices in commodity markets. Energy efficiency further enhances the financial case for optical sorter market adoption. Modern systems optimize power consumption while maintaining peak performance, reducing facility operating costs substantially. The optical sorter market delivers predictable cost savings through decreased rework, fewer product recalls, and eliminated customer complaints related to quality issues. Extended equipment lifespan minimizes replacement expenses, maximizing long-term investment value and ensuring sustained competitiveness.
Precision Quality Control and Safety Assurance

Precision Quality Control and Safety Assurance

The optical sorter market fundamentally transforms quality control by implementing objective, consistent evaluation standards. Unlike subjective human assessment, the optical sorter market technology applies identical criteria to every product, ensuring uniform quality outputs. This consistency strengthens brand reputation as customers receive predictable product excellence consistently. Food safety represents a paramount concern addressed brilliantly by the optical sorter market. Contamination detection prevents hazardous foreign materials from reaching consumers, protecting public health and company liability. The optical sorter market identifies naturally occurring defects, processing irregularities, and spoilage indicators before products enter the market, maintaining stringent safety standards throughout production. Compliance documentation provided by the optical sorter market systems creates transparent audit trails satisfying regulatory requirements. Facilities operating within the optical sorter market technology framework demonstrate commitment to quality assurance and consumer protection. This technological foundation enables businesses to confidently meet international standards while providing customers documented proof of rigorous quality protocols and safety measures throughout entire production processes.

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

Copyright © 2026 Anhui Jiexun Optoelectronic Technology Co., Ltd. All rights reserved.  -  Privacy policy