Optical Color Sorter | Industrial Sorting Technology

All Categories

optical color sorter

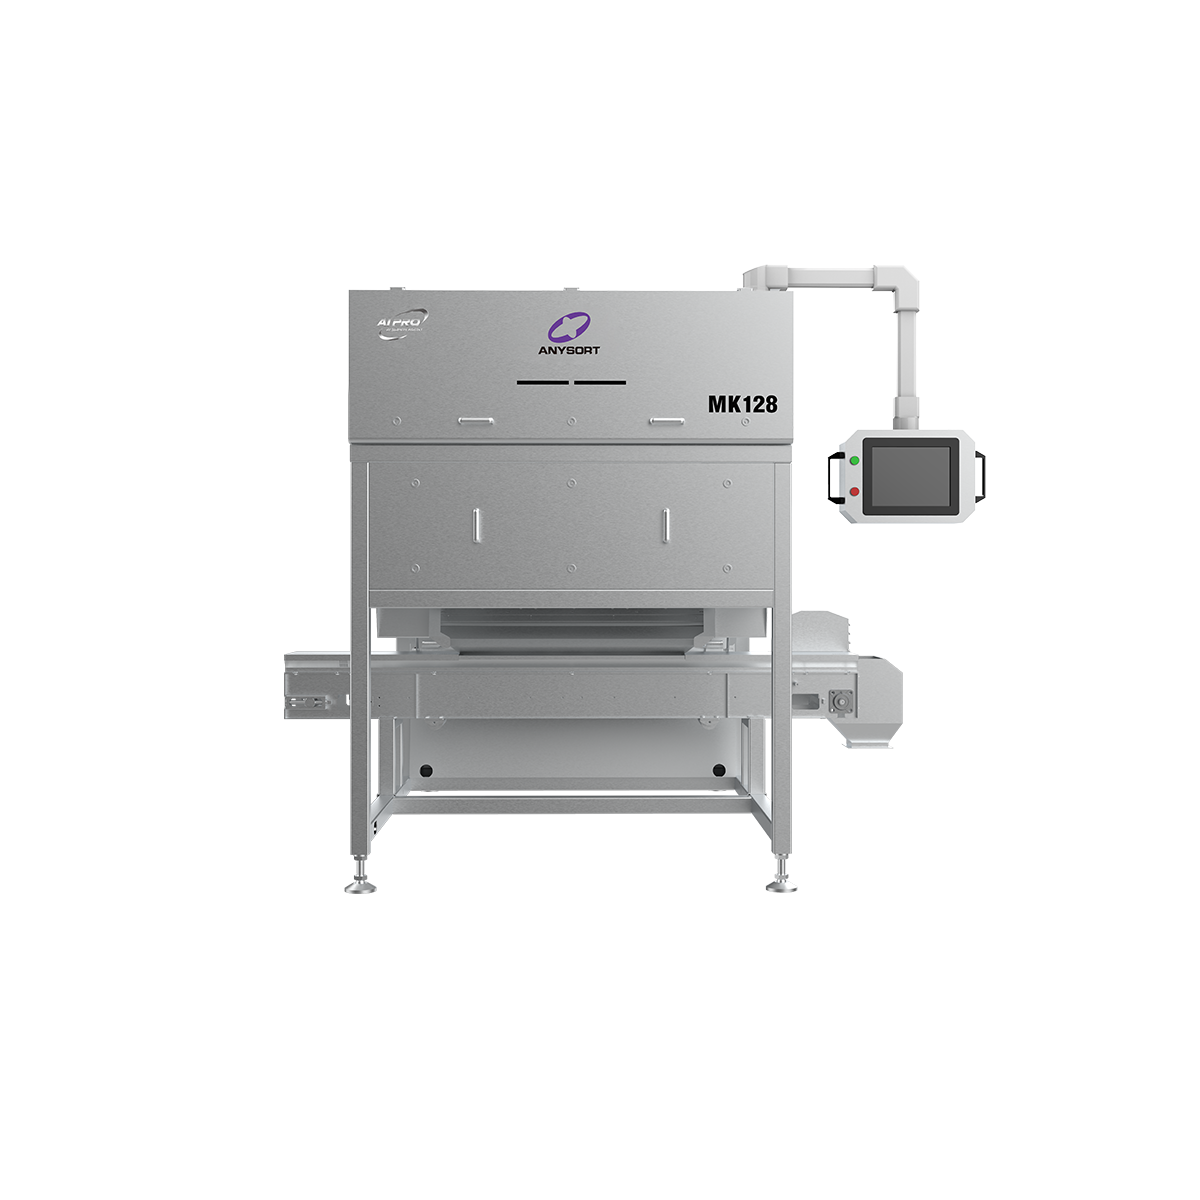
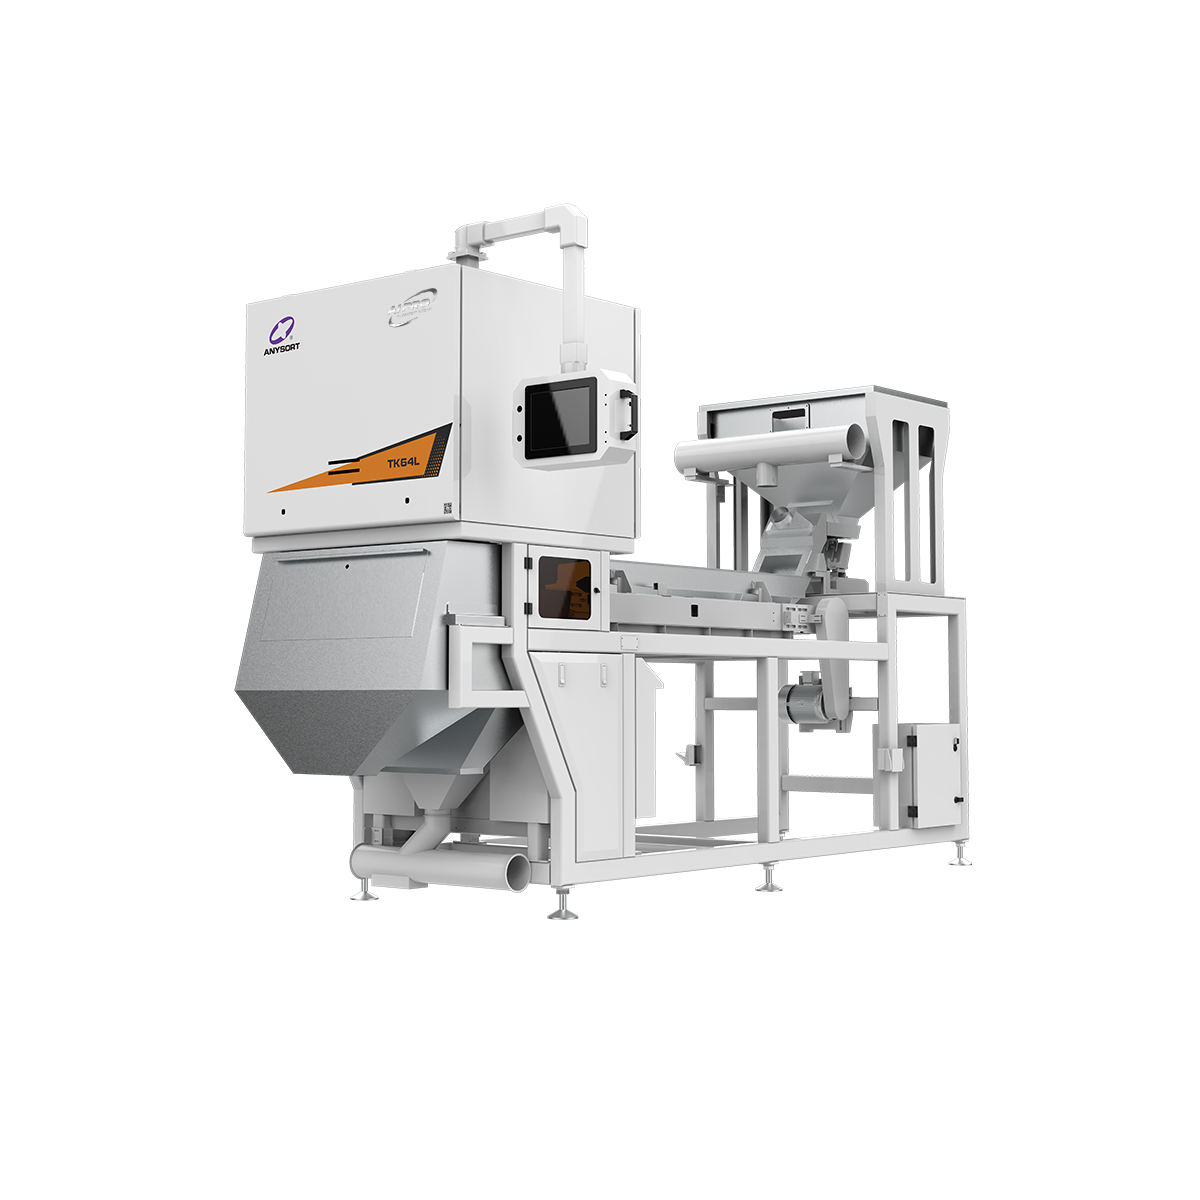
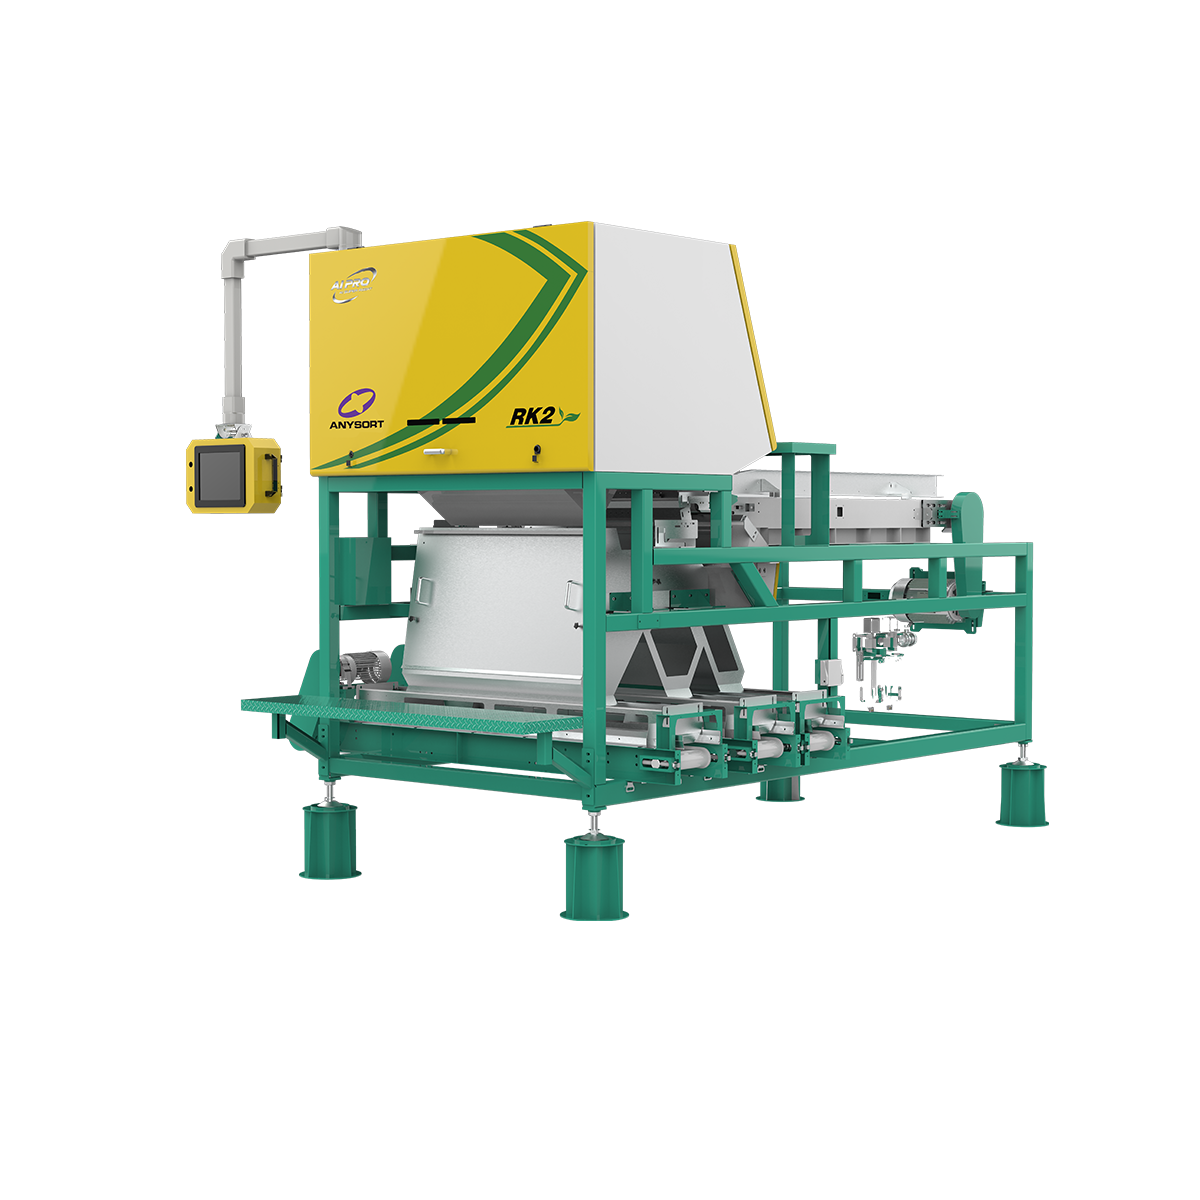
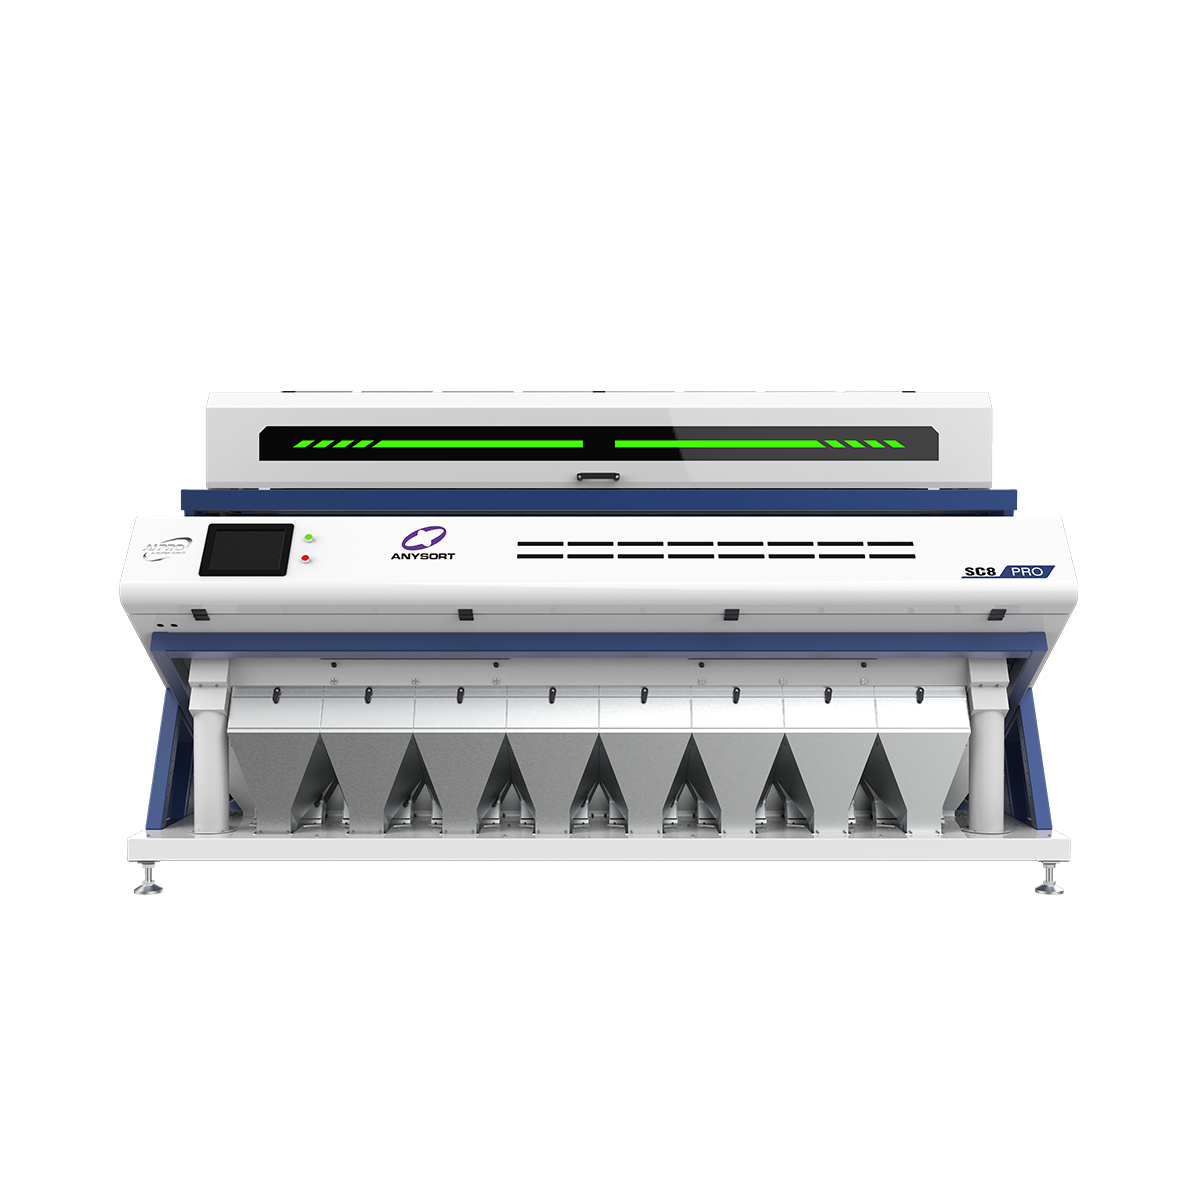
An optical color sorter is an advanced automated machine designed to separate and classify materials based on their color, composition, and quality characteristics. This innovative technology uses high-resolution cameras and sophisticated image processing algorithms to analyze each item passing through the system in real-time. The optical color sorter inspects thousands of particles per second, making sorting decisions with exceptional accuracy that far exceeds manual sorting capabilities. The primary function of an optical color sorter involves detecting defects, contamination, and color variations in various materials including grains, seeds, plastics, minerals, and recycled materials. The technology employs multi-spectral imaging and advanced sensors to identify subtle differences invisible to the human eye. Once an optical color sorter identifies undesired materials, pneumatic ejection systems remove them with precision timing. Key technological features of an optical color sorter include high-speed cameras, LED lighting systems, powerful processors, and intelligent sorting algorithms. These components work together seamlessly to deliver consistent results across different production environments. The optical color sorter can be customized to sort various materials, making it versatile for multiple industrial applications. Modern systems offer user-friendly interfaces, real-time monitoring, and detailed sorting reports that help operators optimize production quality and efficiency while reducing waste significantly.

New Product Recommendations

An optical color sorter delivers substantial operational and financial benefits to businesses across numerous industries. The most significant advantage is dramatically improved product quality through automated detection of defects and contaminants that manual inspection would miss. By implementing an optical color sorter, companies reduce waste significantly while ensuring only premium-grade materials reach customers, enhancing brand reputation and customer satisfaction. Cost reduction represents another compelling benefit of investing in an optical color sorter. While initial capital investment exists, the technology eliminates expensive manual labor costs associated with sorting operations. An optical color sorter processes materials 24/7 without fatigue, requiring minimal supervision and reducing overall production expenses substantially. Facilities experience faster sorting speeds, allowing higher throughput and increased revenue generation from the same production line. Operational efficiency improvements make an optical color sorter invaluable for modern manufacturing. The system provides real-time data analytics and performance metrics, enabling operators to make informed decisions quickly. An optical color sorter maintains consistent quality standards across every production batch, eliminating human error and variability associated with manual sorting methods. The technology integrates seamlessly into existing production lines, requiring minimal downtime during installation and setup processes. Applications span multiple industries including food processing, recycling, mining, agriculture, and plastics manufacturing. An optical color sorter proves particularly beneficial for high-volume operations where maintaining consistent quality standards is critical. Businesses gain competitive advantages through superior product quality, faster delivery times, and reduced production costs. The investment in an optical color sorter quickly pays for itself through improved efficiency and waste reduction.

Latest News

What Factors Affect Tea Color Sorter Performance and Accuracy?

05

Aug

What Factors Affect Tea Color Sorter Performance and Accuracy?

The precision of a tea color sorter directly determines the quality consistency of finished tea products. Understanding the factors that influence tea color sorter performance and accuracy is essential for tea processors seeking to maintain competiti...
View More
How can rice color sorters improve grain quality?

08

Aug

How can rice color sorters improve grain quality?

Rice color sorters represent a transformative technology in modern grain processing, fundamentally changing how producers maintain and enhance the quality of their rice output. By utilizing advanced optical scanning and artificial intelligence, a ric...
View More
How Much Does a Color Sorter Machine Cost?

12

Aug

How Much Does a Color Sorter Machine Cost?

Understanding the investment required for a color sorter machine is essential for businesses in agriculture, food processing, and recycling sectors. The cost of a color sorter machine varies significantly based on capacity, technology sophistication,...
View More
How Can a Nuts Sorter Improve Your Production?

15

Aug

How Can a Nuts Sorter Improve Your Production?

A nuts sorter represents one of the most significant investments a food processing operation can make to enhance production quality and operational efficiency. The modern nuts sorter uses advanced imaging and sensor technology to identify and separat...
View More

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

optical color sorter

Advanced Detection Technology for Superior Accuracy

Advanced Detection Technology for Superior Accuracy

Modern optical color sorter systems utilize cutting-edge multi-spectral imaging technology that detects minute variations in color, composition, and structural integrity. The cameras capture detailed images of each particle, processing information through artificial intelligence algorithms that learn and adapt to specific sorting requirements. An optical color sorter achieves accuracy rates exceeding 99.9 percent, identifying defects, discoloration, and contamination invisible to human operators. This precision ensures that only materials meeting strict quality specifications pass through, protecting your brand reputation. The optical color sorter's detection capabilities extend beyond visible light, incorporating infrared and other sensor types to identify hidden defects. Businesses utilizing this technology experience significant reductions in customer complaints and product returns. The advanced optical color sorter systems provide detailed sorting reports and real-time monitoring dashboards.
High-Speed Processing and Maximum Throughput

High-Speed Processing and Maximum Throughput

An optical color sorter processes thousands of individual items every second, delivering exceptional throughput that increases production capacity without expanding facility footprint. The system's speed capabilities depend on material type and sorting complexity, but modern optical color sorter units handle up to fifteen tons per hour efficiently. This rapid processing translates directly into higher revenues and faster order fulfillment for businesses managing time-sensitive production schedules. The optical color sorter maintains consistent speed across all operational hours, providing reliable performance that manual sorting cannot match. Facilities experience substantial reductions in production bottlenecks when implementing advanced optical color sorter technology. Energy-efficient designs ensure that high-speed operation does not result in excessive utility costs. The optical color sorter's processing capabilities scale to meet growing business demands without requiring equipment replacement.
Easy Integration and User-Friendly Operation

Easy Integration and User-Friendly Operation

Installing an optical color sorter into existing production environments requires minimal modifications and causes virtually no operational disruption. The systems feature intuitive control interfaces designed for operators with varying technical expertise levels. An optical color sorter connects to standard electrical supplies and integrates with automated conveyor systems through simple mechanical attachments. Training requirements for optical color sorter operation remain minimal, allowing existing staff to quickly master system functions and troubleshooting procedures. The optical color sorter provides real-time monitoring through intuitive dashboards displaying sorting performance metrics and material statistics. Maintenance procedures are straightforward, with accessible components and clear diagnostic systems helping operators identify potential issues immediately. The optical color sorter offers reliable performance with minimal downtime, supported by comprehensive manufacturer documentation and technical support teams available to address questions.

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

Copyright © 2026 Anhui Jiexun Optoelectronic Technology Co., Ltd. All rights reserved.  -  Privacy policy