optical sorting equipment
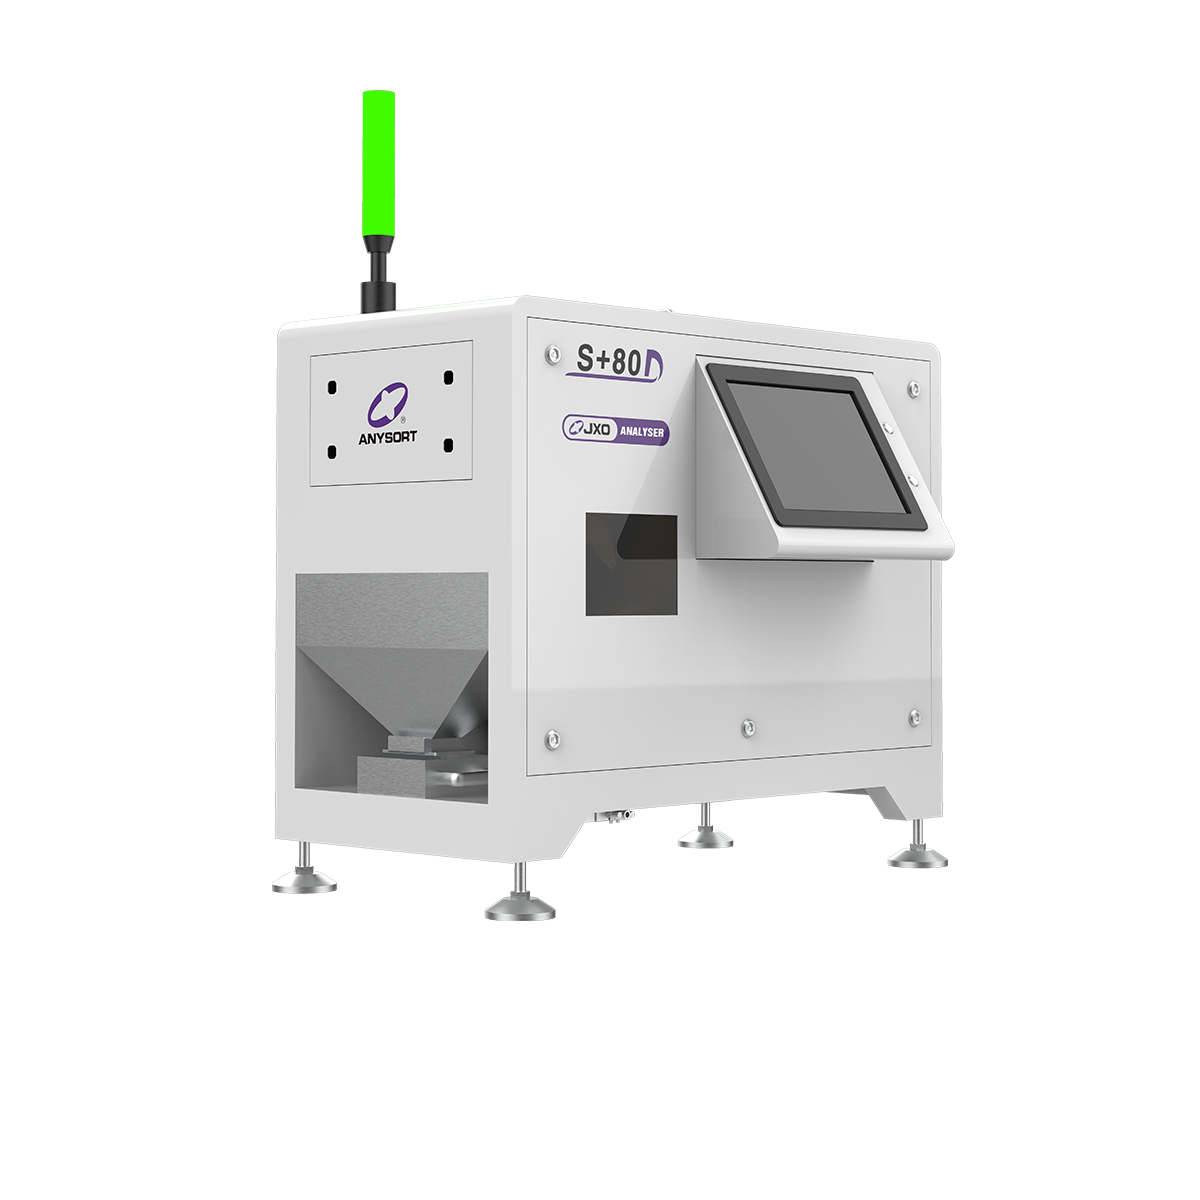
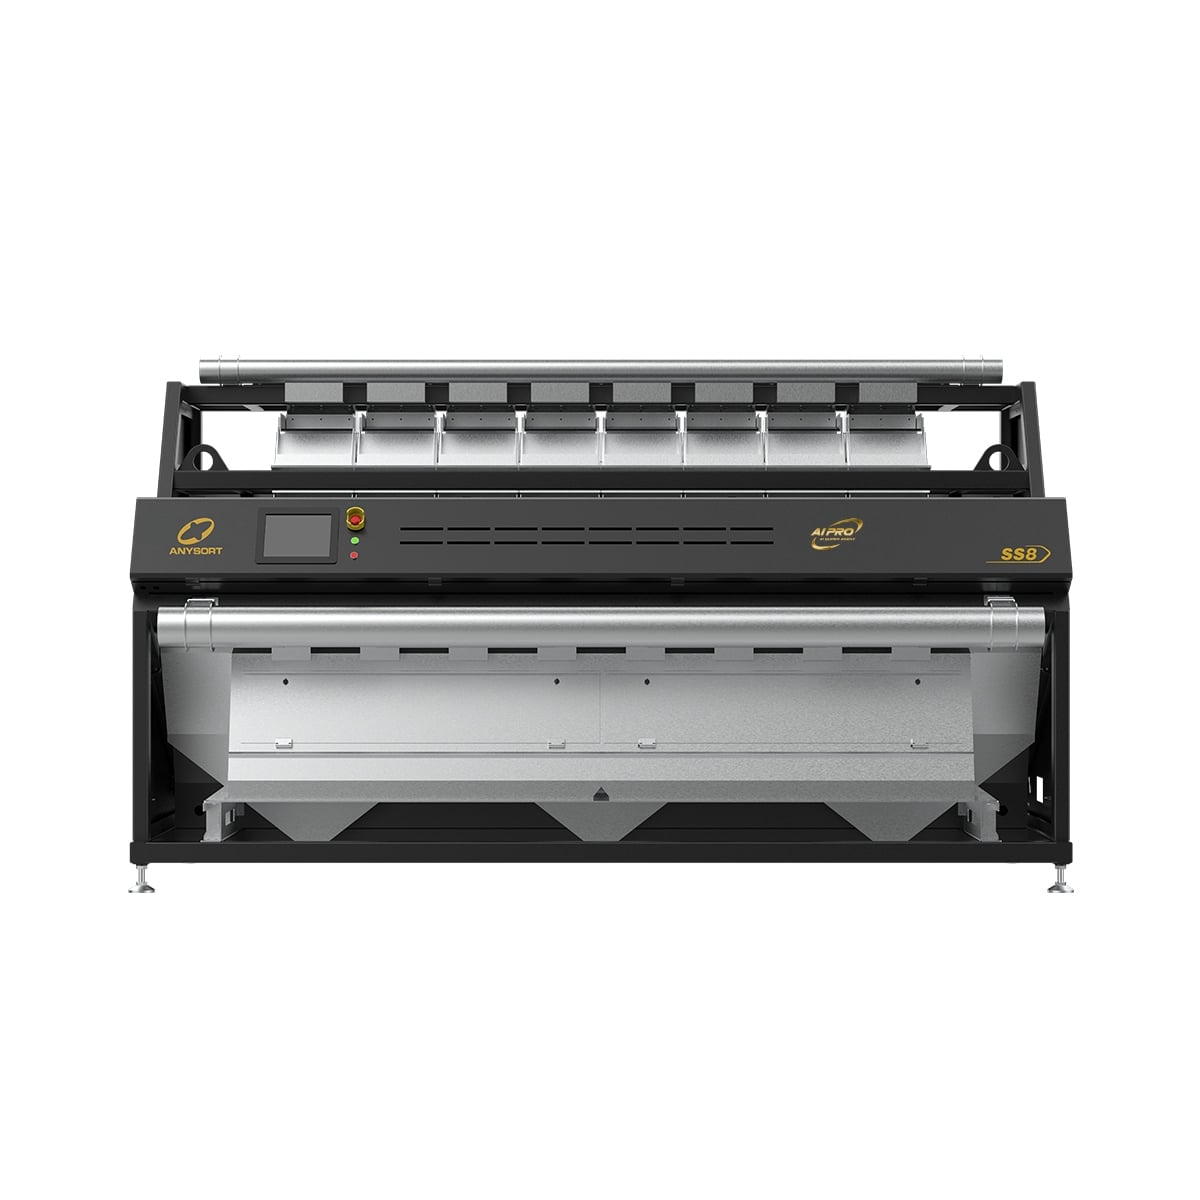
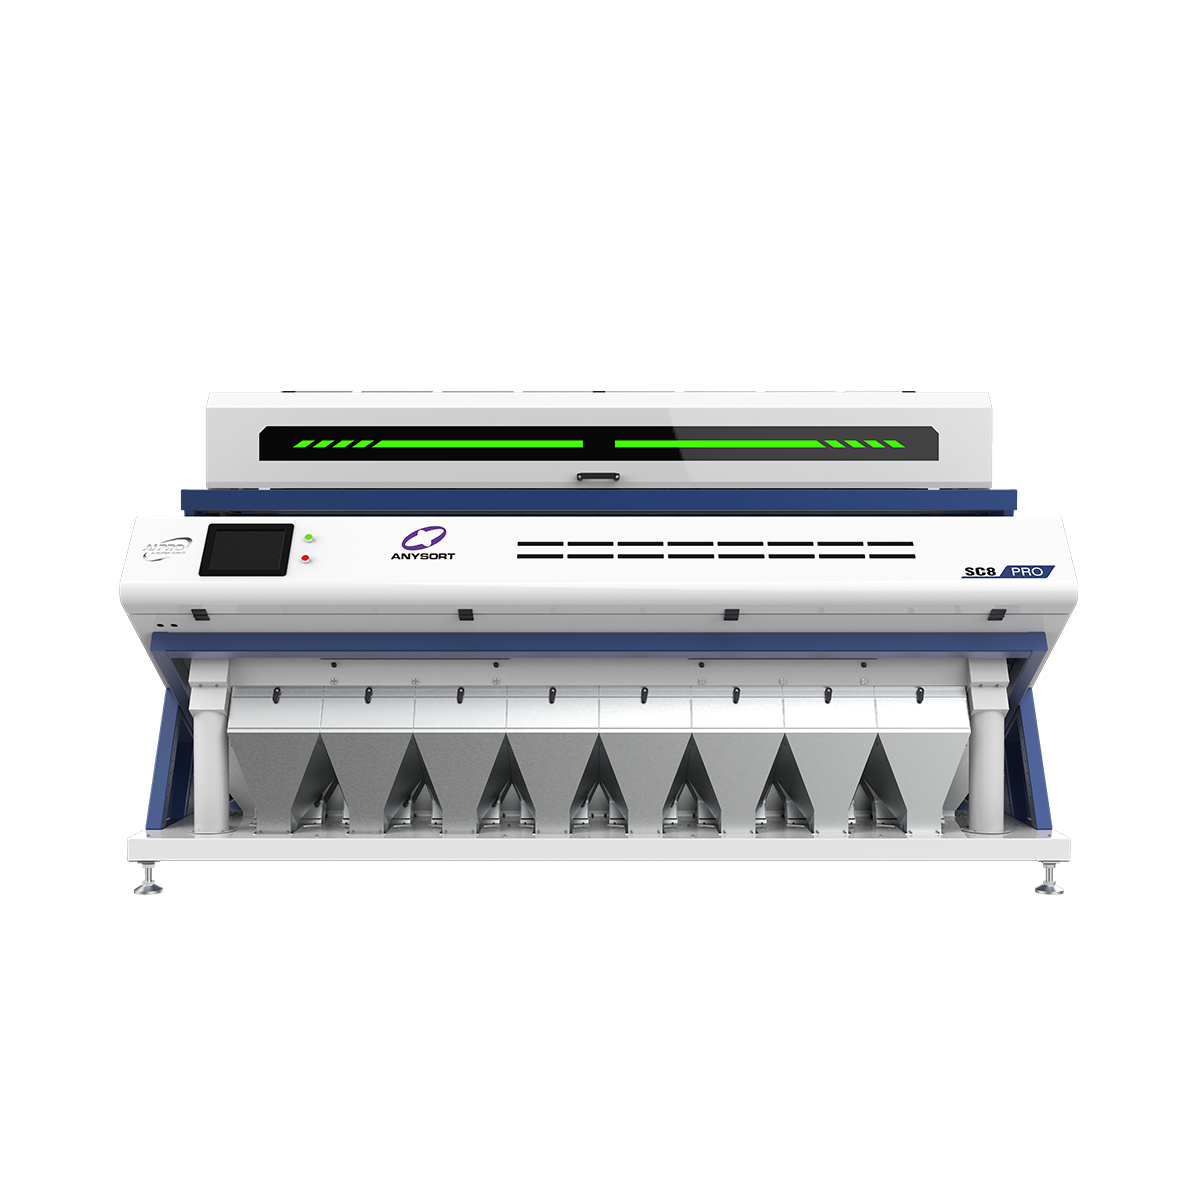
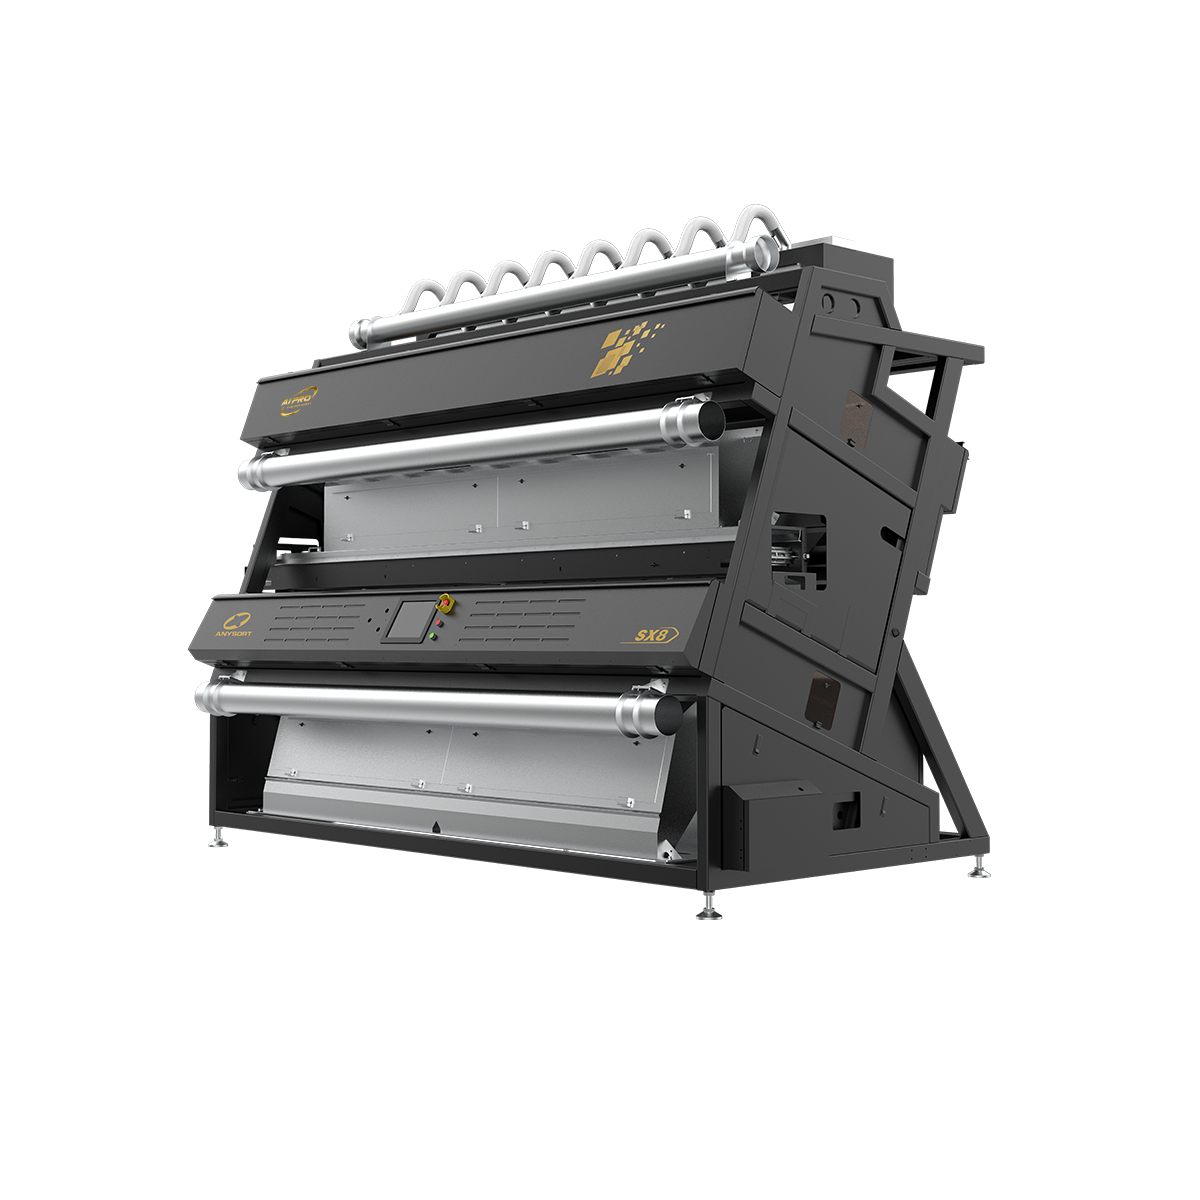
Optical sorting equipment represents a revolutionary advancement in material separation technology, designed to automatically identify and sort items based on their optical properties. This sophisticated machinery uses advanced camera systems and artificial intelligence to analyze materials in real-time, ensuring precise categorization without human intervention. Optical sorting equipment operates by capturing high-resolution images of passing materials, then employing complex algorithms to detect color variations, size differences, and material composition. The core function of optical sorting equipment is to remove contaminated, damaged, or unwanted items from production streams with remarkable accuracy. Modern optical sorting equipment integrates multiple sensor technologies, including visible light cameras, infrared sensors, and laser detection systems, enabling comprehensive material analysis. The technological features of optical sorting equipment include high-speed processing capabilities, allowing thousands of items per minute to pass through inspection. Advanced optical sorting equipment systems use machine learning to continuously improve sorting accuracy and adapt to changing material characteristics. These machines find applications across numerous industries, including food processing, recycling facilities, mining operations, and pharmaceutical manufacturing. The versatility of optical sorting equipment makes it invaluable for quality control, contamination removal, and material recovery processes. By implementing optical sorting equipment, businesses can significantly enhance product quality while reducing waste and operational costs associated with manual sorting procedures.

 EN