Optical Sorting Machine Price Guide

All Categories

optical sorting machine price

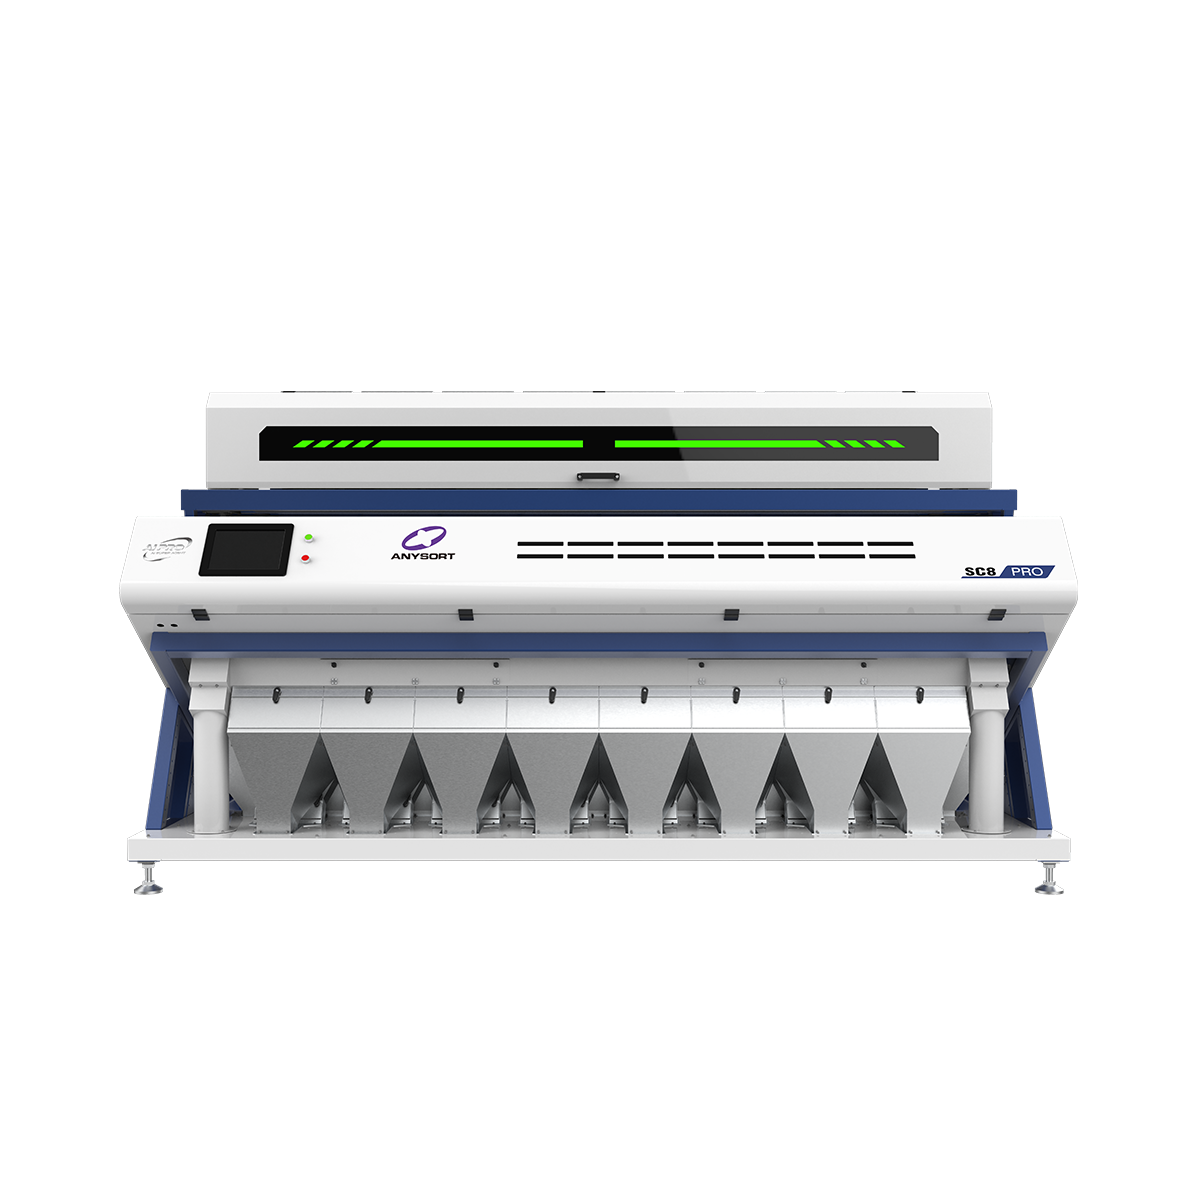
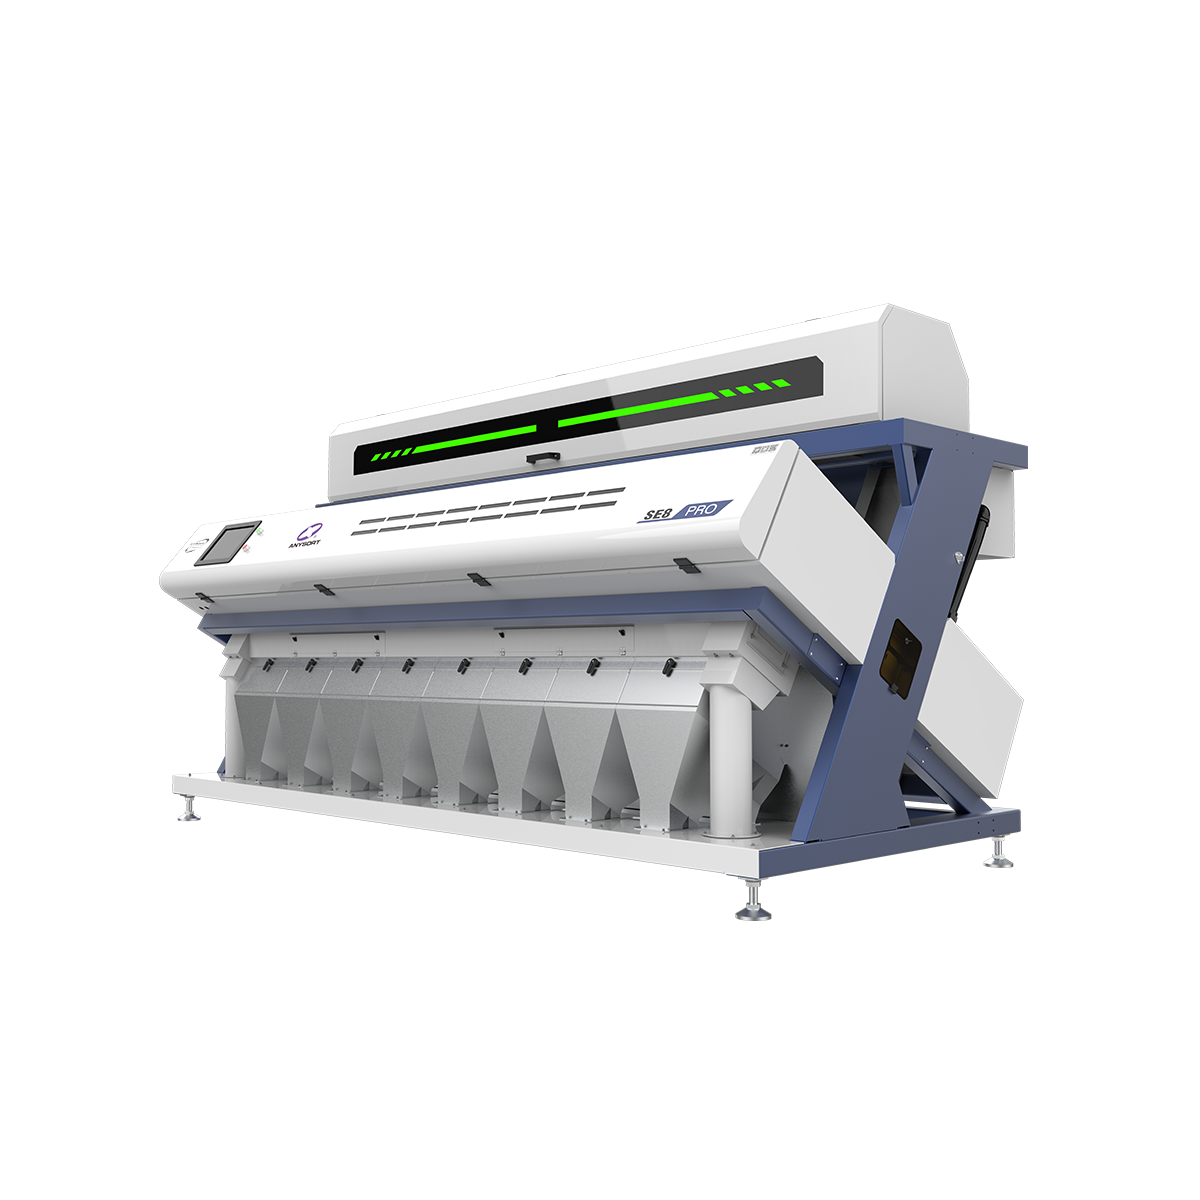
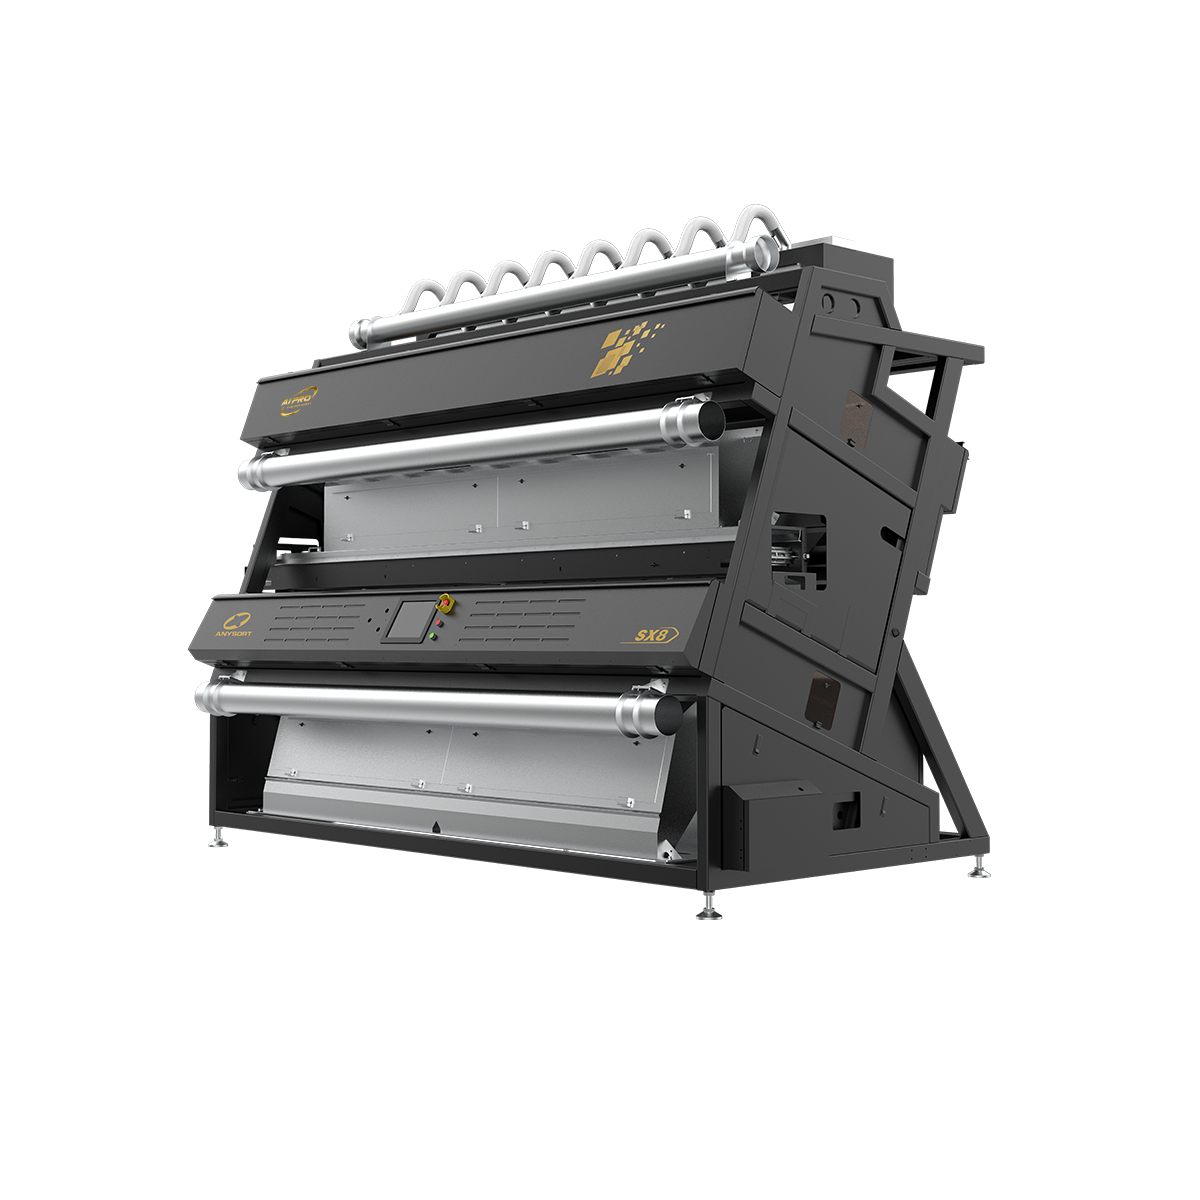
Understanding optical sorting machine price is essential for businesses seeking efficient waste management and material separation solutions. An optical sorting machine price reflects the investment required for advanced automated technology that revolutionizes how industries process recyclable materials, agricultural products, and industrial waste. This equipment uses sophisticated camera systems and artificial intelligence to identify and separate materials based on color, shape, size, and material composition with remarkable accuracy. The optical sorting machine price varies depending on machine capacity, sorting accuracy levels, and specific application requirements. Modern optical sorting machines operate by scanning materials on conveyor belts, analyzing each item through high-resolution imaging, and using pneumatic ejectors to remove unwanted materials automatically. This technology significantly reduces manual labor costs while improving sorting precision. The optical sorting machine price investment pays dividends through increased material recovery rates, reduced contamination, and enhanced operational efficiency. Industries including recycling facilities, food processing plants, mining operations, and pharmaceutical companies benefit from optical sorting technology. The optical sorting machine price encompasses equipment that handles diverse materials from plastic polymers to mineral ore. Understanding factors affecting optical sorting machine price helps buyers make informed purchasing decisions that align with their production goals and budget constraints.

New Product Recommendations

The optical sorting machine price delivers substantial value through multiple operational benefits that transform material processing workflows. When considering optical sorting machine price, businesses gain access to automation technology that eliminates human error in material identification and separation. The economic advantage of investing in optical sorting machine price becomes evident through reduced labor expenses and increased throughput rates that exceed manual sorting by up to 300 percent. Operational benefits include consistent sorting accuracy that maintains quality standards across production runs without fatigue-related performance degradation. The optical sorting machine price investment provides flexibility across applications, handling everything from municipal waste streams to premium food grading operations. Businesses reduce contamination rates significantly, protecting downstream processing equipment and improving final product quality. The practical benefit of optical sorting machine price adoption includes 24/7 operational capability, allowing facilities to maximize production during extended shifts without quality compromise. Decision-useful context shows that optical sorting machine price enables rapid ROI achievement through material recovery value and disposal cost reduction. Environmental benefits align with sustainability goals, as optical sorting machine price technology maximizes material recovery while minimizing landfill contributions. Application suitability extends across industries, from beverage container recycling to pharmaceutical tablet inspection. The buyer value proposition clearly demonstrates how optical sorting machine price represents a strategic investment generating measurable returns through improved efficiency, reduced waste, and enhanced product quality metrics that directly impact profitability and competitive positioning.

Latest News

How to Choose the Right Tea Color Sorter for Your Needs?

01

Aug

How to Choose the Right Tea Color Sorter for Your Needs?

Selecting the right tea color sorter is one of the most critical decisions tea processors face when modernizing their operations. A tea color sorter directly impacts product quality, operational efficiency, and market competitiveness. The wrong choic...
View More
How Much Does a Color Sorter Machine Cost?

12

Aug

How Much Does a Color Sorter Machine Cost?

Understanding the investment required for a color sorter machine is essential for businesses in agriculture, food processing, and recycling sectors. The cost of a color sorter machine varies significantly based on capacity, technology sophistication,...
View More
How Can a Nuts Sorter Improve Your Production?

15

Aug

How Can a Nuts Sorter Improve Your Production?

A nuts sorter represents one of the most significant investments a food processing operation can make to enhance production quality and operational efficiency. The modern nuts sorter uses advanced imaging and sensor technology to identify and separat...
View More
Which factors should you consider when selecting a rice color sorter?

29

Aug

Which factors should you consider when selecting a rice color sorter?

Selecting the right rice color sorter is a critical decision that directly impacts your grain processing efficiency, product quality, and long-term profitability. A rice color sorter removes discolored, damaged, and foreign particles from rice batche...
View More

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

optical sorting machine price

Advanced Optical Recognition Technology

Advanced Optical Recognition Technology

The optical sorting machine price includes state-of-the-art imaging systems utilizing multiple camera angles and spectral analysis capabilities. This technology identifies material properties invisible to human inspection, enabling precise sorting of similar-looking items with different compositions. High-resolution sensors capture detailed information about each object, while processing algorithms analyze this data instantaneously to make accurate separation decisions. The optical sorting machine price encompasses specialized lighting systems that illuminate materials under controlled conditions, enhancing detection accuracy for transparent, translucent, and opaque materials alike. Advanced software continuously learns from operational data, improving sorting performance over time. This intelligent optical sorting machine price investment ensures consistent identification of contamination, defects, and material variations across thousands of items per minute, maintaining quality standards that manual inspection cannot achieve.
Cost-Effective Material Recovery Solutions

Cost-Effective Material Recovery Solutions

Investing in optical sorting machine price yields significant financial returns through enhanced material recovery efficiency. Facilities using optical sorting machine price technology recover 15-25 percent more valuable materials compared to traditional sorting methods, directly improving bottom-line profitability. The optical sorting machine price model reduces operational costs by minimizing labor requirements while increasing processing volume substantially. Material buyers reward higher-purity sorted streams with premium pricing, offsetting the optical sorting machine price investment quickly. Energy-efficient designs mean the optical sorting machine price operating costs remain competitive with manual labor while delivering superior results. Reduced contamination improves buyer satisfaction and repeat business relationships, creating stable revenue streams that justify the optical sorting machine price expenditure over time.
Versatile Applications Across Industries

Versatile Applications Across Industries

The optical sorting machine price offers remarkable adaptability across diverse industrial applications and material types. Recycling operations utilize optical sorting machine price systems to separate plastics by resin type, recover aluminum and metals, and process mixed waste streams efficiently. Food processing facilities employ optical sorting machine price technology for quality control, removing defective products and foreign materials with precision. Mining and mineral industries leverage optical sorting machine price equipment to concentrate valuable ore and remove waste rock early in processing. Agricultural operations use optical sorting machine price systems for grain grading, seed sorting, and removing damaged produce before packaging. Pharmaceutical manufacturers implement optical sorting machine price inspection for tablet verification and capsule quality assurance, ensuring regulatory compliance.

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

Copyright © 2026 Anhui Jiexun Optoelectronic Technology Co., Ltd. All rights reserved.  -  Privacy policy