Optical Sorting Equipment Manufacturer

All Categories

optical sorting equipment manufacturer

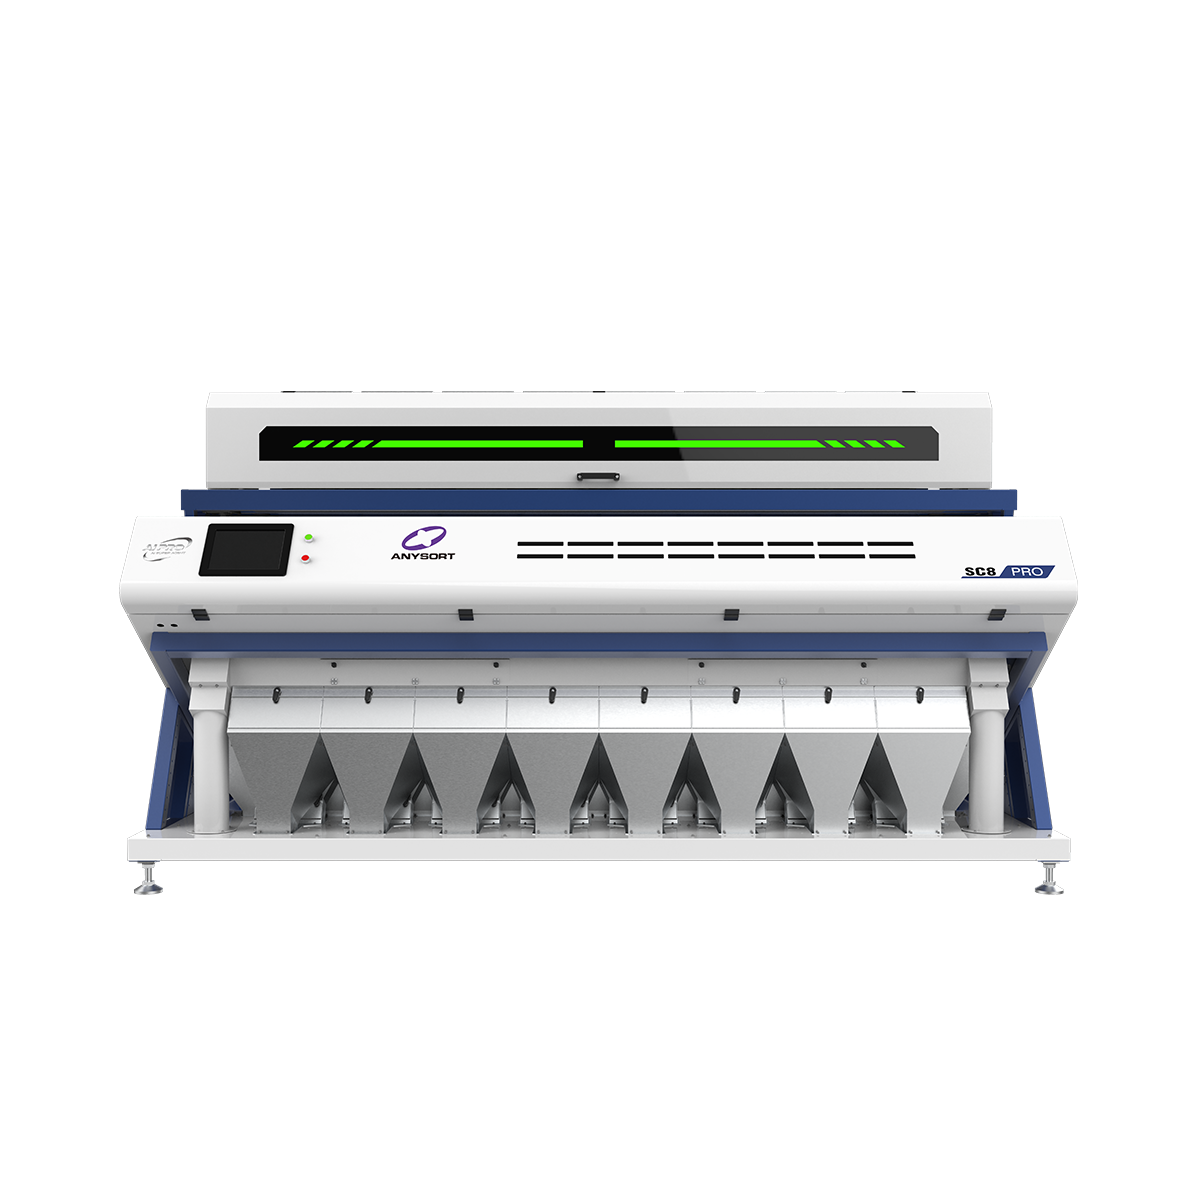
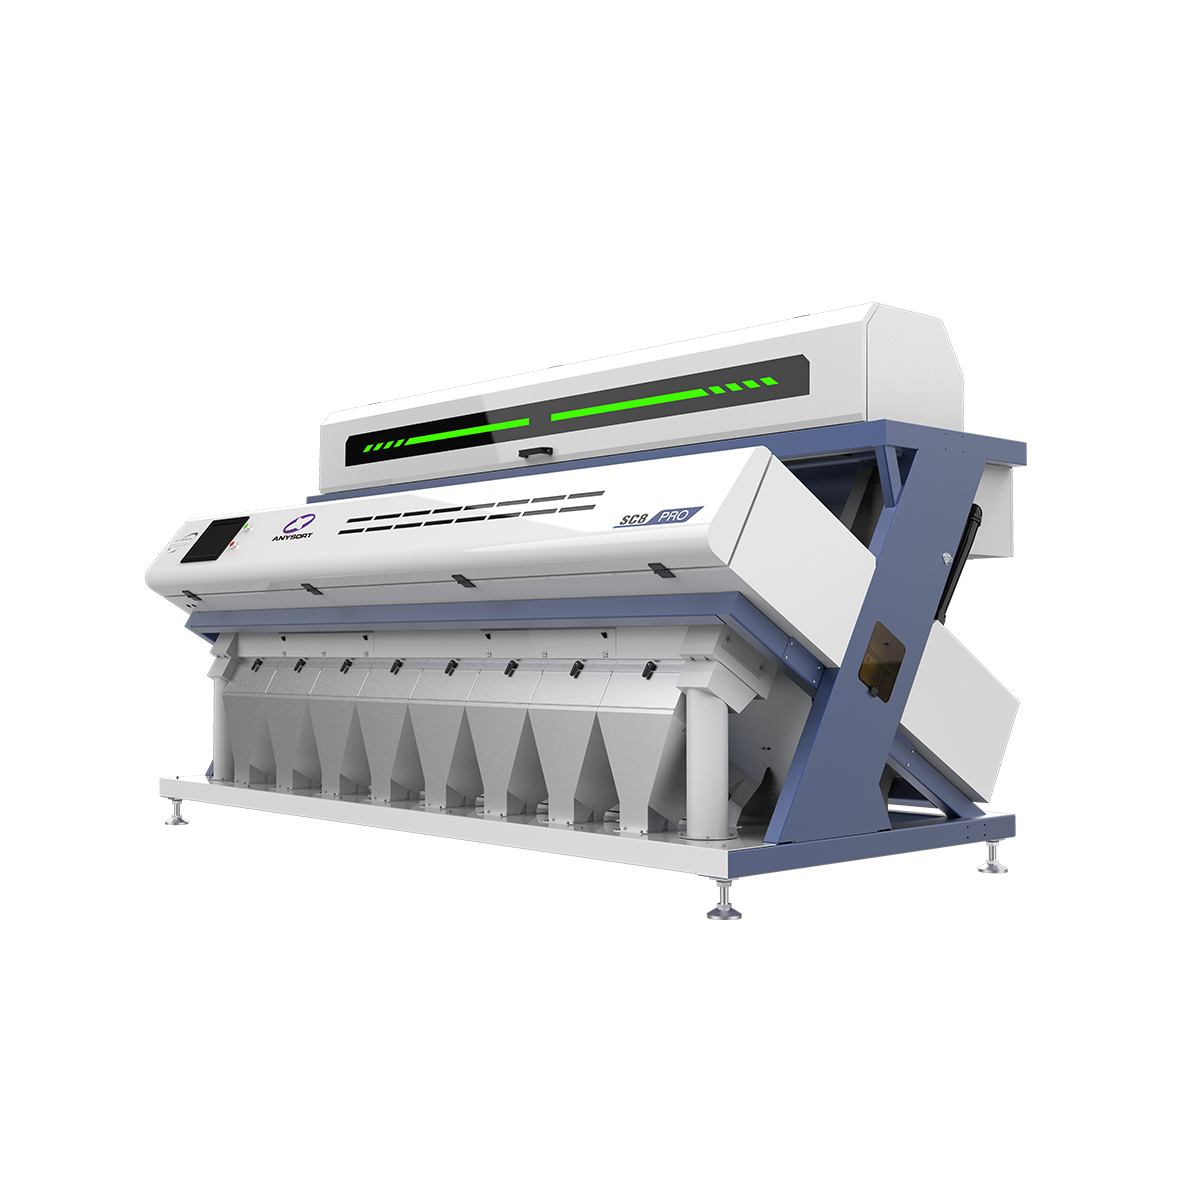
An optical sorting equipment manufacturer specializes in producing advanced machinery that uses cutting-edge vision technology to automatically separate and classify materials with exceptional precision. The optical sorting equipment manufacturer leverages sophisticated camera systems and artificial intelligence algorithms to identify subtle differences in material properties, color, shape, and density that human operators would miss. These machines process thousands of items per minute, making them indispensable in modern industrial operations. The core function of an optical sorting equipment manufacturer's products is to enhance product quality while reducing contamination and waste. Technological features include high-resolution imaging sensors, real-time data processing, and automated rejection systems that instantly remove non-conforming items from production lines. The optical sorting equipment manufacturer integrates machine learning capabilities that continuously improve sorting accuracy over time. Applications span across diverse industries including food processing, recycling, mining, agriculture, and pharmaceuticals. In food manufacturing, these systems detect foreign objects, discoloration, and defects in grains, nuts, and frozen products. Recycling facilities benefit from optical sorting to separate plastics, metals, and glass with remarkable efficiency. Agricultural producers use this technology to grade produce and remove damaged items before packaging. The optical sorting equipment manufacturer's solutions significantly boost operational efficiency by minimizing manual labor, reducing product loss, and ensuring consistent quality standards that meet regulatory requirements and consumer expectations across global markets.

New Product Releases

Choosing products from a leading optical sorting equipment manufacturer delivers transformative operational benefits that directly impact your bottom line. These systems dramatically increase production efficiency by processing materials at speeds manual sorting cannot match, allowing you to handle higher volumes without expanding your workforce significantly. The accuracy provided by an optical sorting equipment manufacturer eliminates human error, ensuring that every item meets your quality specifications consistently. You reduce product waste and contamination incidents that damage your reputation and profitability. Cost savings accumulate quickly through reduced labor expenses, lower rejection rates, and minimized losses from contamination or quality failures. An optical sorting equipment manufacturer's technology adapts to your specific material types and sorting criteria, making these solutions versatile across different product lines and production environments. Integration with existing production infrastructure proves straightforward, meaning minimal disruption to current operations during installation. Real-time monitoring and data reporting give you complete visibility into sorting performance and product quality metrics, enabling informed decisions about your processes. Compliance with industry standards and food safety regulations becomes automatic through consistent, documented sorting results that satisfy auditors and regulators. Maintenance requirements remain reasonable, with most optical sorting equipment manufacturer systems featuring durable components and user-friendly service protocols. Your investment pays dividends through enhanced competitiveness, improved customer satisfaction from better quality products, and stronger market positioning. These machines scale efficiently whether you operate a small facility or large industrial operation, growing alongside your business needs without requiring complete system replacement.

Latest News

What Factors Affect Tea Color Sorter Performance and Accuracy?

05

Aug

What Factors Affect Tea Color Sorter Performance and Accuracy?

The precision of a tea color sorter directly determines the quality consistency of finished tea products. Understanding the factors that influence tea color sorter performance and accuracy is essential for tea processors seeking to maintain competiti...
View More
How to Choose the Right Tea Color Sorter for Your Needs?

01

Aug

How to Choose the Right Tea Color Sorter for Your Needs?

Selecting the right tea color sorter is one of the most critical decisions tea processors face when modernizing their operations. A tea color sorter directly impacts product quality, operational efficiency, and market competitiveness. The wrong choic...
View More
How Can a Nuts Sorter Improve Your Production?

15

Aug

How Can a Nuts Sorter Improve Your Production?

A nuts sorter represents one of the most significant investments a food processing operation can make to enhance production quality and operational efficiency. The modern nuts sorter uses advanced imaging and sensor technology to identify and separat...
View More
How does optical sorting technology detect defective rice grains?

22

Aug

How does optical sorting technology detect defective rice grains?

Modern rice processing demands precision and consistency, which is why understanding the detection mechanisms behind advanced equipment has become essential for producers. A rice color sorter represents one of the most significant technological break...
View More

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

optical sorting equipment manufacturer

Advanced Vision Technology for Unmatched Precision

Advanced Vision Technology for Unmatched Precision

The optical sorting equipment manufacturer incorporates state-of-the-art imaging sensors and computational systems that detect anomalies invisible to human inspection. Each unit features high-resolution cameras capturing multiple perspectives of every item simultaneously, while sophisticated algorithms analyze color gradients, shape characteristics, and material composition in real-time. This optical sorting equipment manufacturer technology processes visual data at millisecond intervals, enabling sorting at extreme speeds without sacrificing accuracy. The machine learning capabilities continuously refine detection parameters based on accumulated data, improving performance over months and years of operation. You benefit from near-perfect sorting accuracy that eliminates subjective judgment and human fatigue effects. Contamination risks drop dramatically when foreign objects, pest damage, or defective items face instantaneous identification and removal. This precision translates directly to enhanced product quality that strengthens customer loyalty and reduces liability exposure from shipping defective merchandise.
Exceptional Throughput and Operational Scalability

Exceptional Throughput and Operational Scalability

An optical sorting equipment manufacturer provides solutions handling massive material volumes that would require prohibitively expensive manual labor. Modern systems process hundreds of kilograms or thousands of individual items per minute, dramatically expanding your production capacity without proportional cost increases. The optical sorting equipment manufacturer's equipment scales seamlessly across facilities of different sizes, from specialized boutique producers to large-scale industrial operations. You implement systems matching your current needs while maintaining flexibility to upgrade capacity as your business grows. Throughput rates remain consistent regardless of shift length or operator fatigue, providing predictable production scheduling and reliable delivery timelines. Processing speed improvements free up valuable floor space previously occupied by sorting personnel or equipment. Energy consumption remains efficient despite high-speed operation, supporting your sustainability objectives while controlling operating costs. This scalable approach means you avoid the substantial investment disruption of complete equipment replacement when expanding production.
Reduced Costs and Enhanced Environmental Responsibility

Reduced Costs and Enhanced Environmental Responsibility

An optical sorting equipment manufacturer's systems deliver compelling financial returns through multiple cost reduction channels. Labor expenses decrease substantially as automated sorting replaces manual processes that require extensive training and ongoing supervision. Material waste drops significantly when sorting accuracy improves, protecting your raw material investments and improving your profit margins. The optical sorting equipment manufacturer technology minimizes the reject rates that represent pure financial loss, transforming marginal materials into saleable products. Water consumption and chemical usage decrease when contamination prevention eliminates downstream reprocessing requirements. Your environmental footprint shrinks through improved waste management and resource efficiency, aligning with corporate sustainability commitments increasingly demanded by consumers and regulators. Regulatory compliance costs diminish when consistent, documented sorting results satisfy safety and quality inspections automatically. Long-term maintenance expenses remain predictable and manageable, with the optical sorting equipment manufacturer providing transparent cost structures and reliable service support. Investment payback periods typically compress to two or three years through cumulative savings and improved product yield.

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

Copyright © 2026 Anhui Jiexun Optoelectronic Technology Co., Ltd. All rights reserved.  -  Privacy policy