optical grader
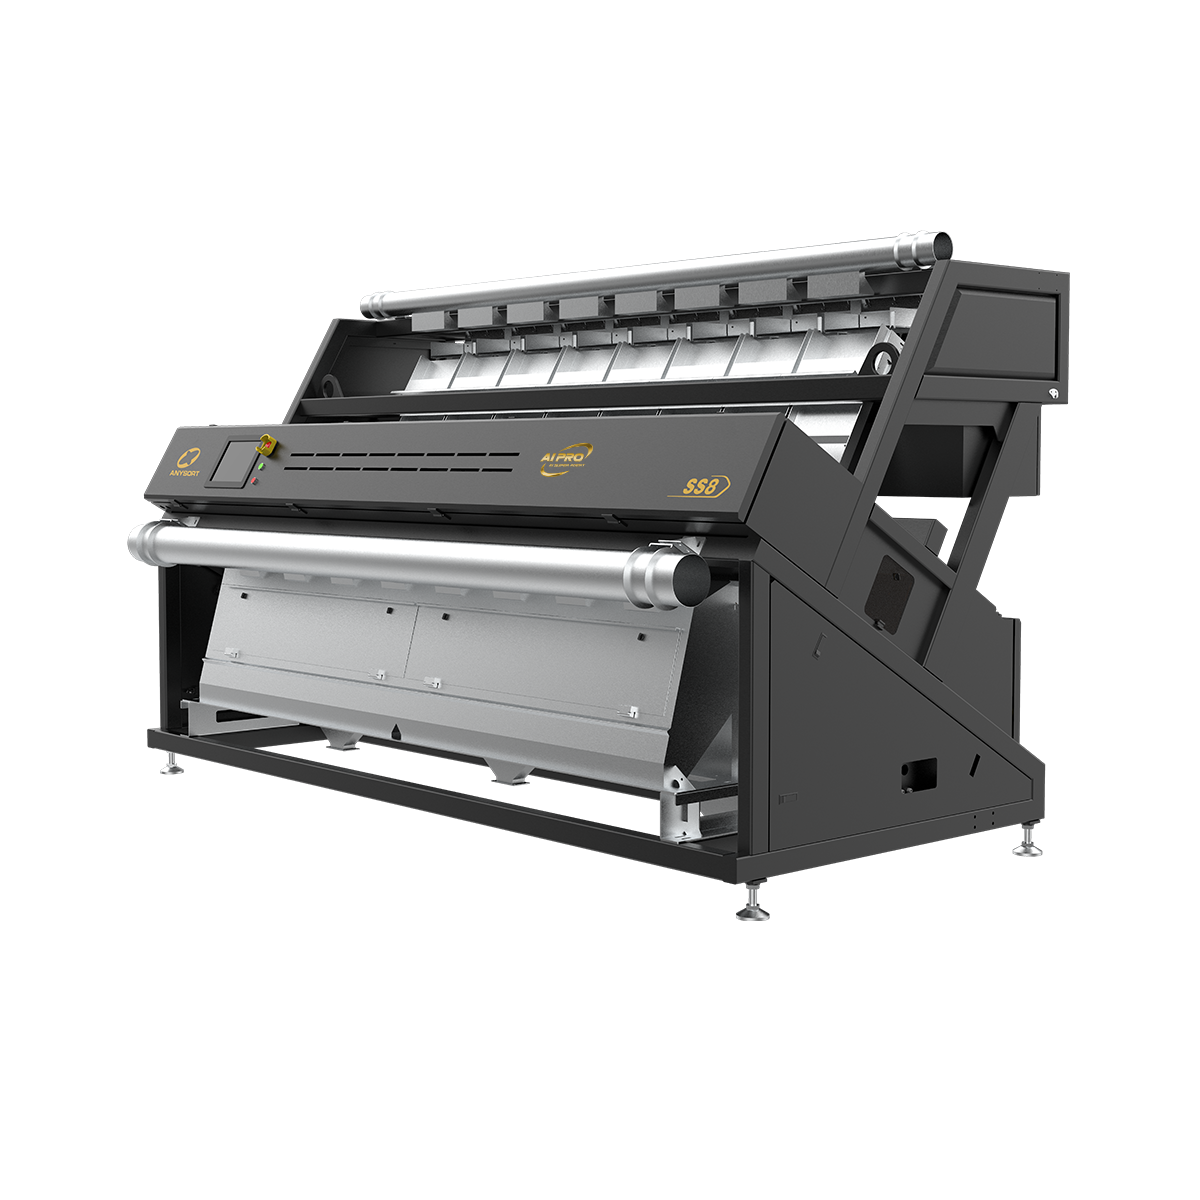
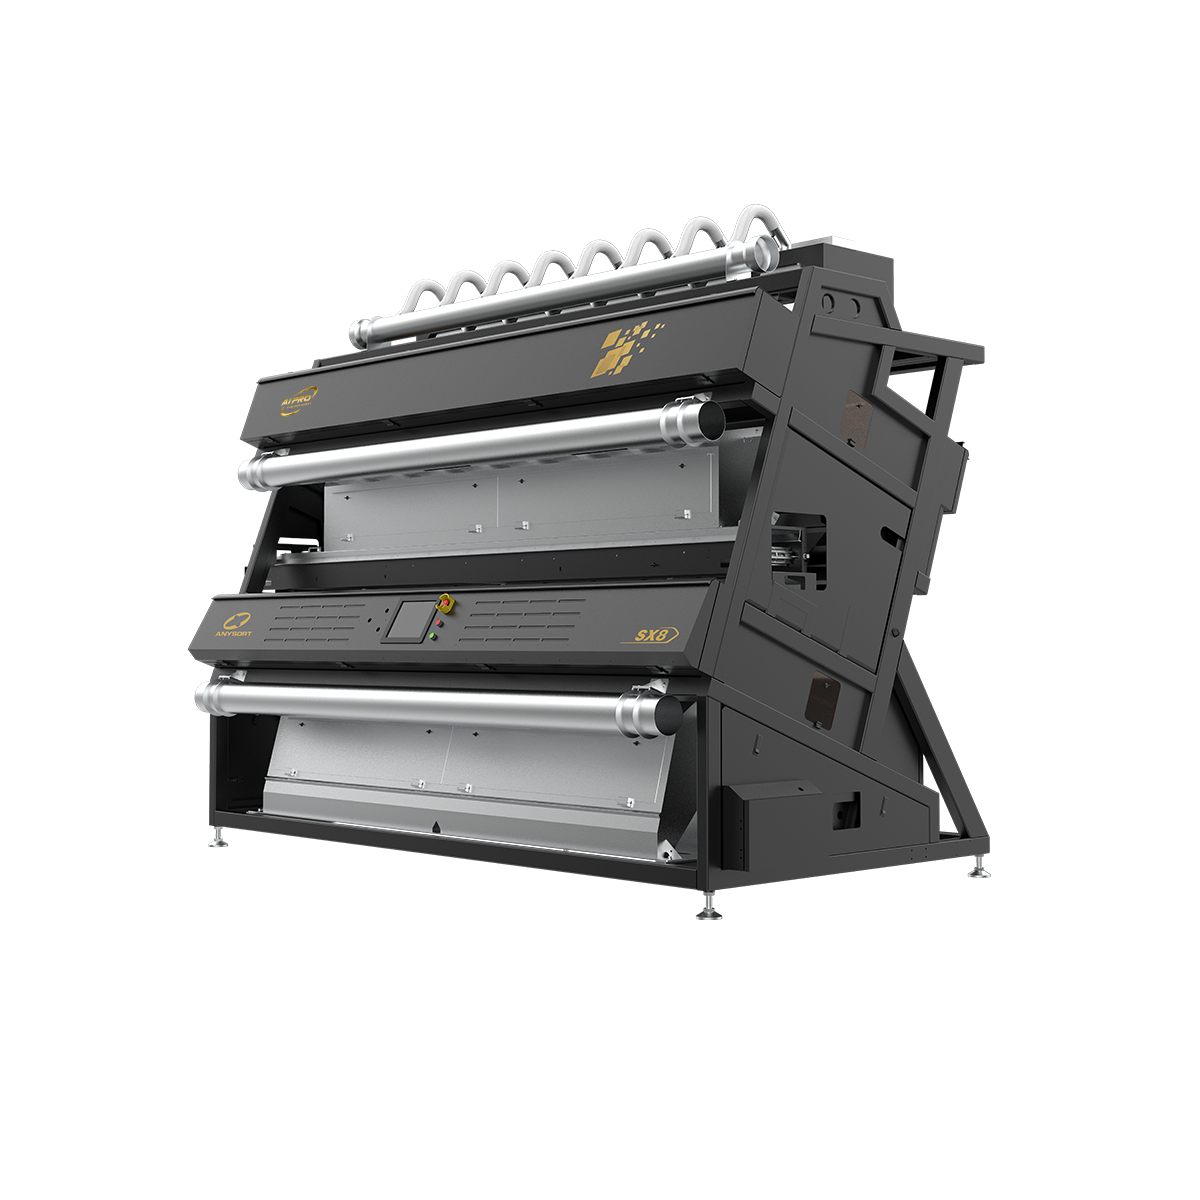
An optical grader represents a sophisticated sorting technology that revolutionizes quality control across multiple industries. This advanced optical grader system utilizes cutting-edge imaging and artificial intelligence to automatically detect, analyze, and categorize products based on predefined quality standards. The optical grader works by capturing high-resolution images of items as they pass through the system, then employing machine learning algorithms to identify defects, color variations, size inconsistencies, and other quality parameters in real-time.
The core functionality of an optical grader involves continuous product inspection without requiring manual intervention. The optical grader technology combines high-speed cameras with sophisticated software to process thousands of items per minute, ensuring consistent quality standards throughout production. Whether grading agricultural products, minerals, recycled materials, or manufactured goods, the optical grader delivers precise classification results that human operators cannot match in speed or accuracy.
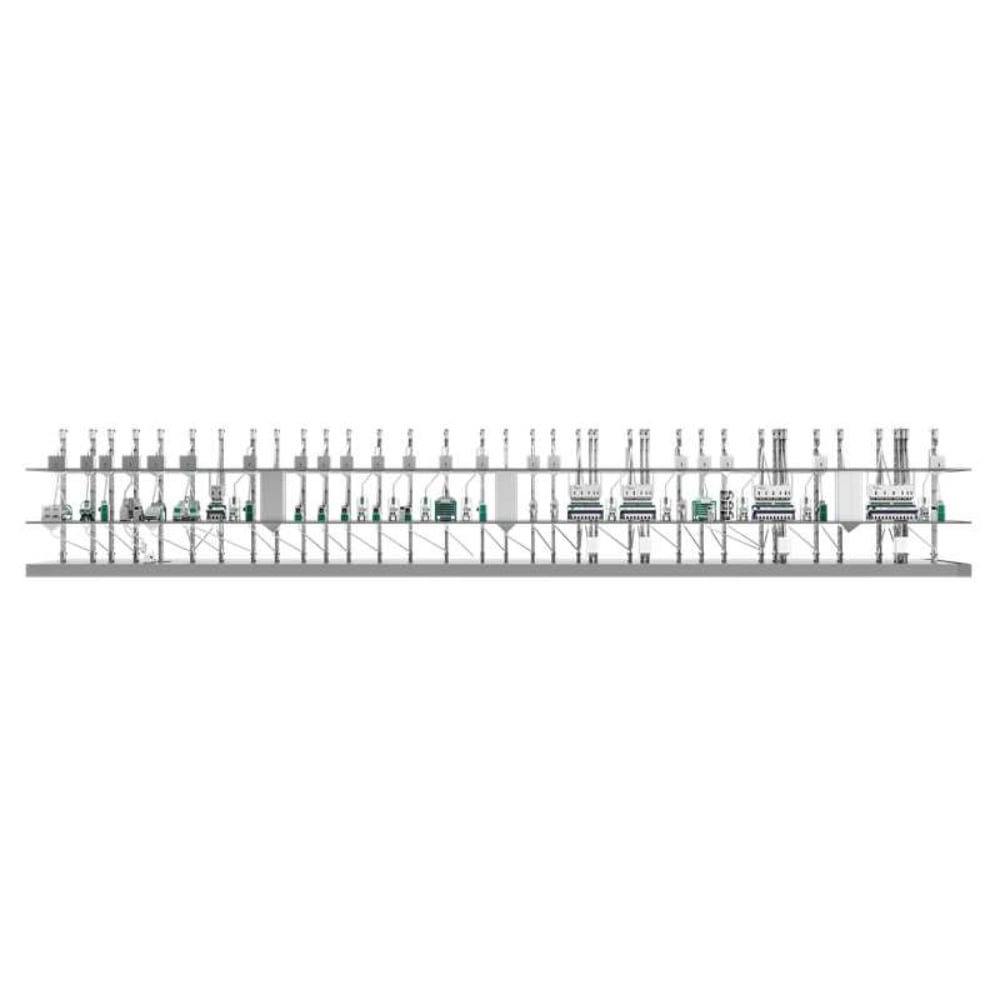
Key technological features of an optical grader include multi-spectral imaging capabilities, adjustable sorting parameters, and seamless integration with existing production lines. The optical grader can be customized to specific industry requirements, making it versatile for diverse applications. Modern optical grader systems offer intuitive interfaces, minimal calibration time, and comprehensive data logging for traceability and quality assurance documentation.

 EN