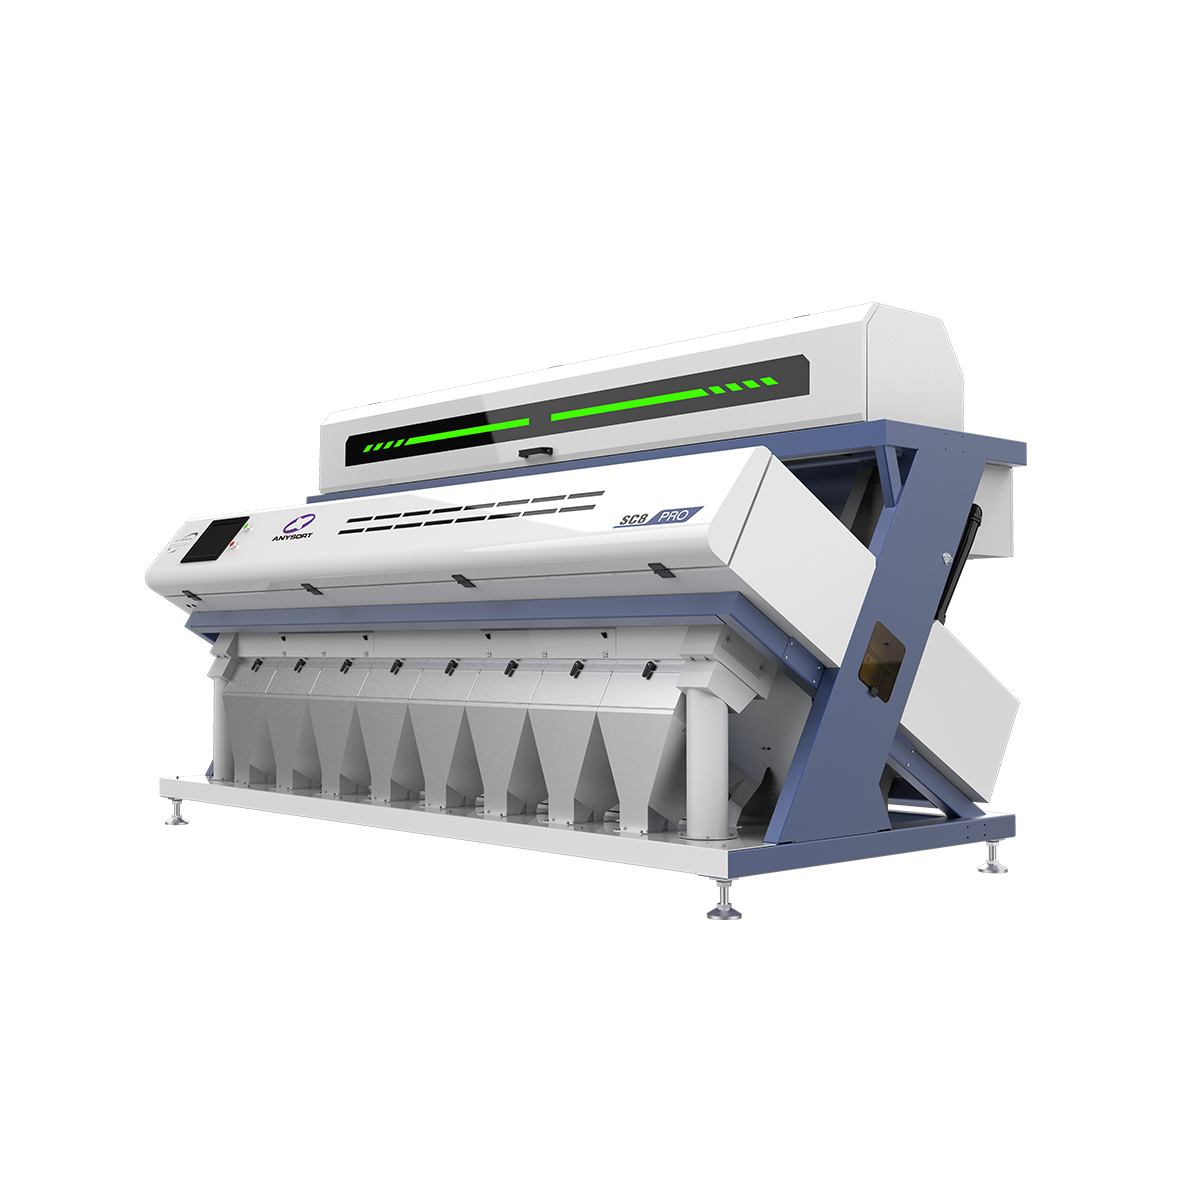
optical sorting machine manufacturers
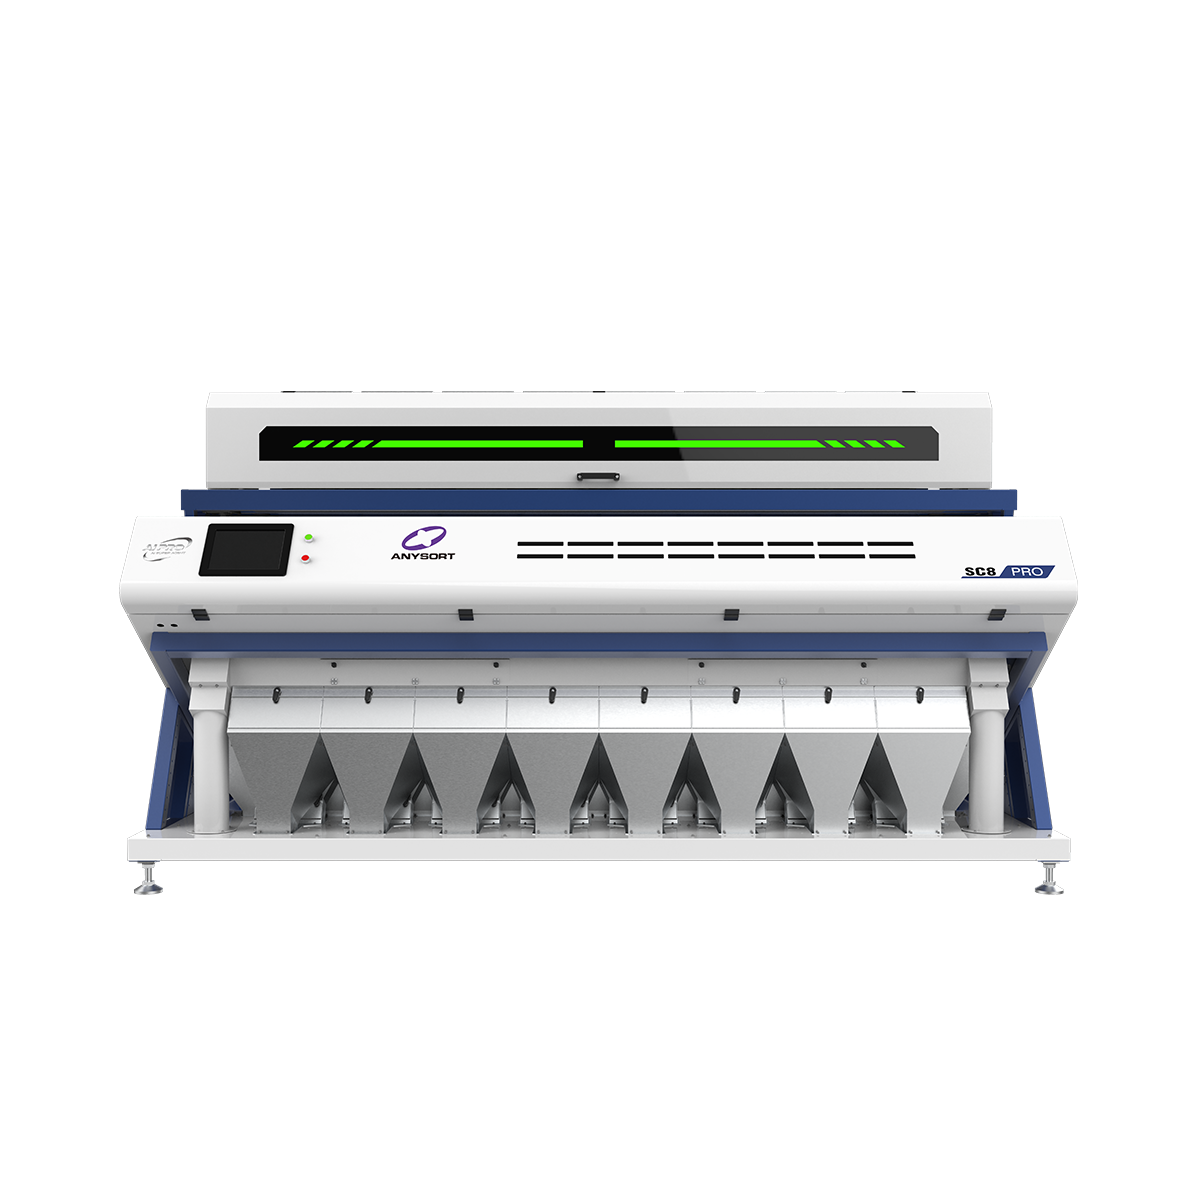
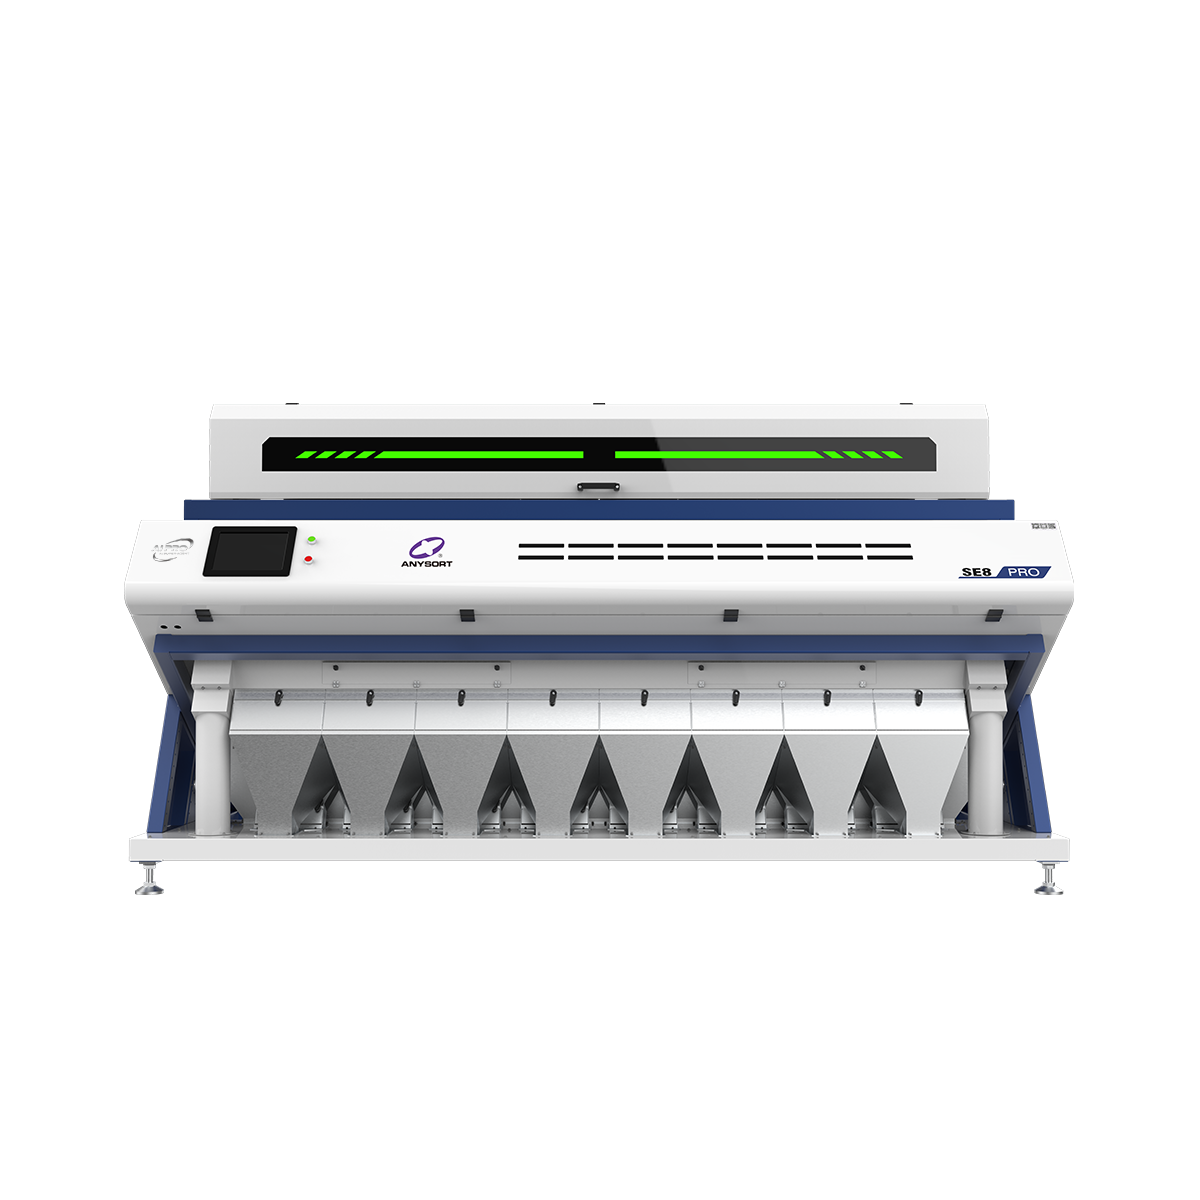
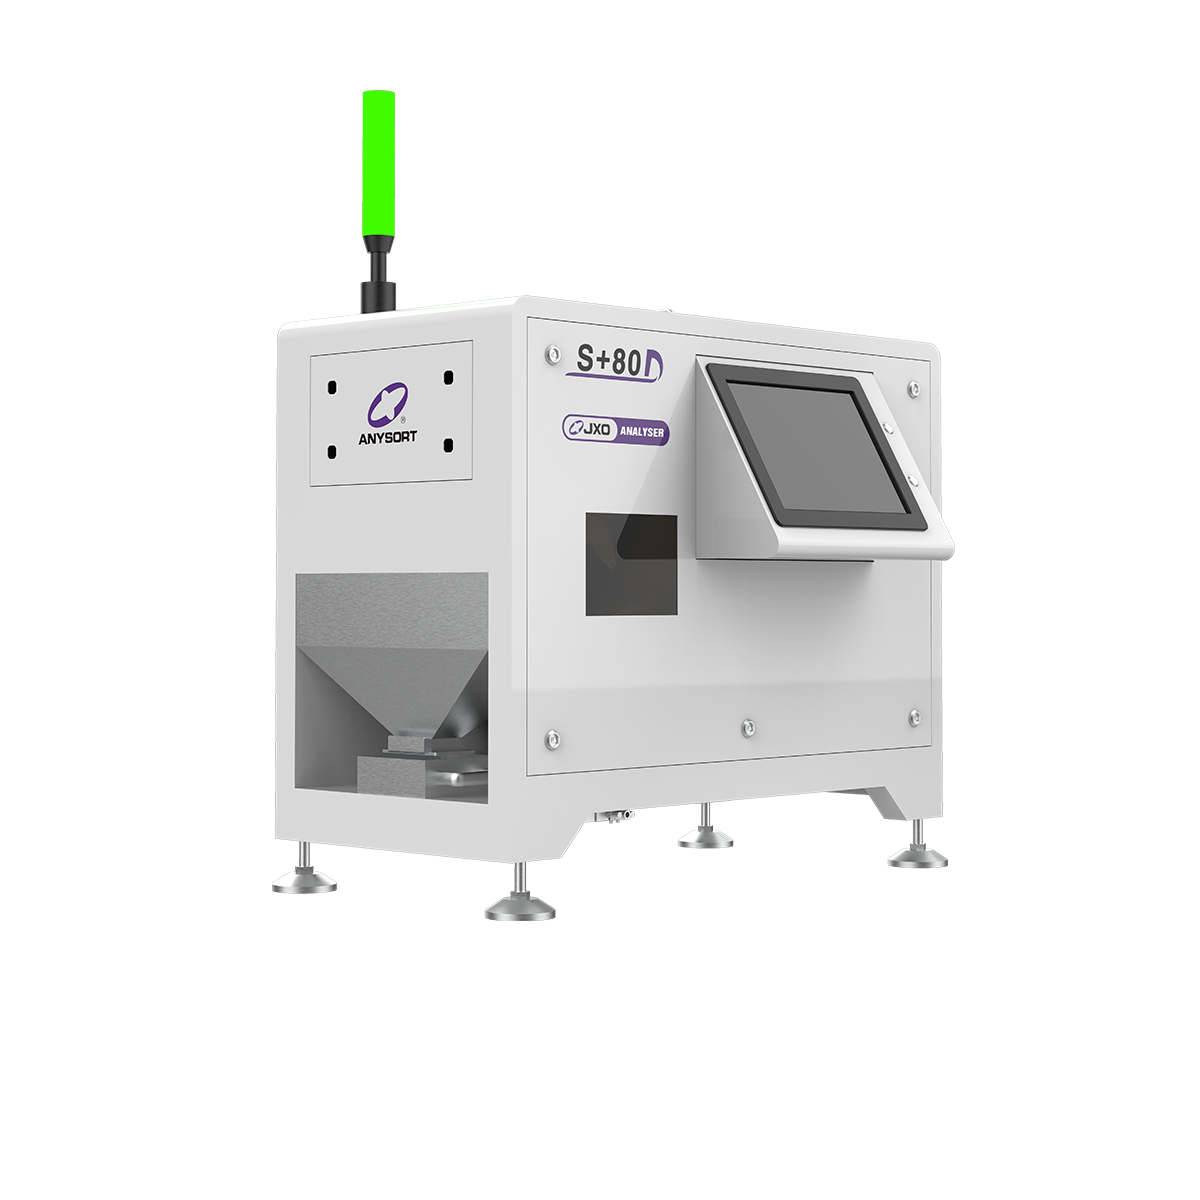
Optical sorting machine manufacturers design and produce advanced equipment that revolutionizes material separation across multiple industries. These sophisticated systems utilize cutting-edge optical technology to detect, analyze, and separate materials based on color, shape, size, and composition with remarkable precision. Leading optical sorting machine manufacturers integrate high-resolution cameras, artificial intelligence, and specialized algorithms to achieve sorting accuracy exceeding 99 percent. The machines process thousands of items per minute, dramatically increasing operational efficiency compared to manual sorting methods. Optical sorting machine manufacturers serve diverse sectors including food processing, recycling, mining, agriculture, and pharmaceutical industries. Their equipment handles everything from grains and nuts to plastic waste and mineral ores. The technological features include LED lighting systems, real-time image processing, and automated rejection mechanisms that remove contaminants instantaneously. These machines significantly reduce product waste while improving quality consistency. Optical sorting machine manufacturers continuously innovate to meet evolving market demands, incorporating machine learning capabilities and IoT connectivity. The systems provide detailed sorting reports and performance analytics, enabling operators to optimize production processes. By choosing equipment from reputable optical sorting machine manufacturers, businesses gain access to reliable technology that enhances productivity, reduces labor costs, and maintains stringent quality standards throughout their operations.

 EN