Optical Food Sorting Platform | Quality Control

All Categories

optical food sorting platform

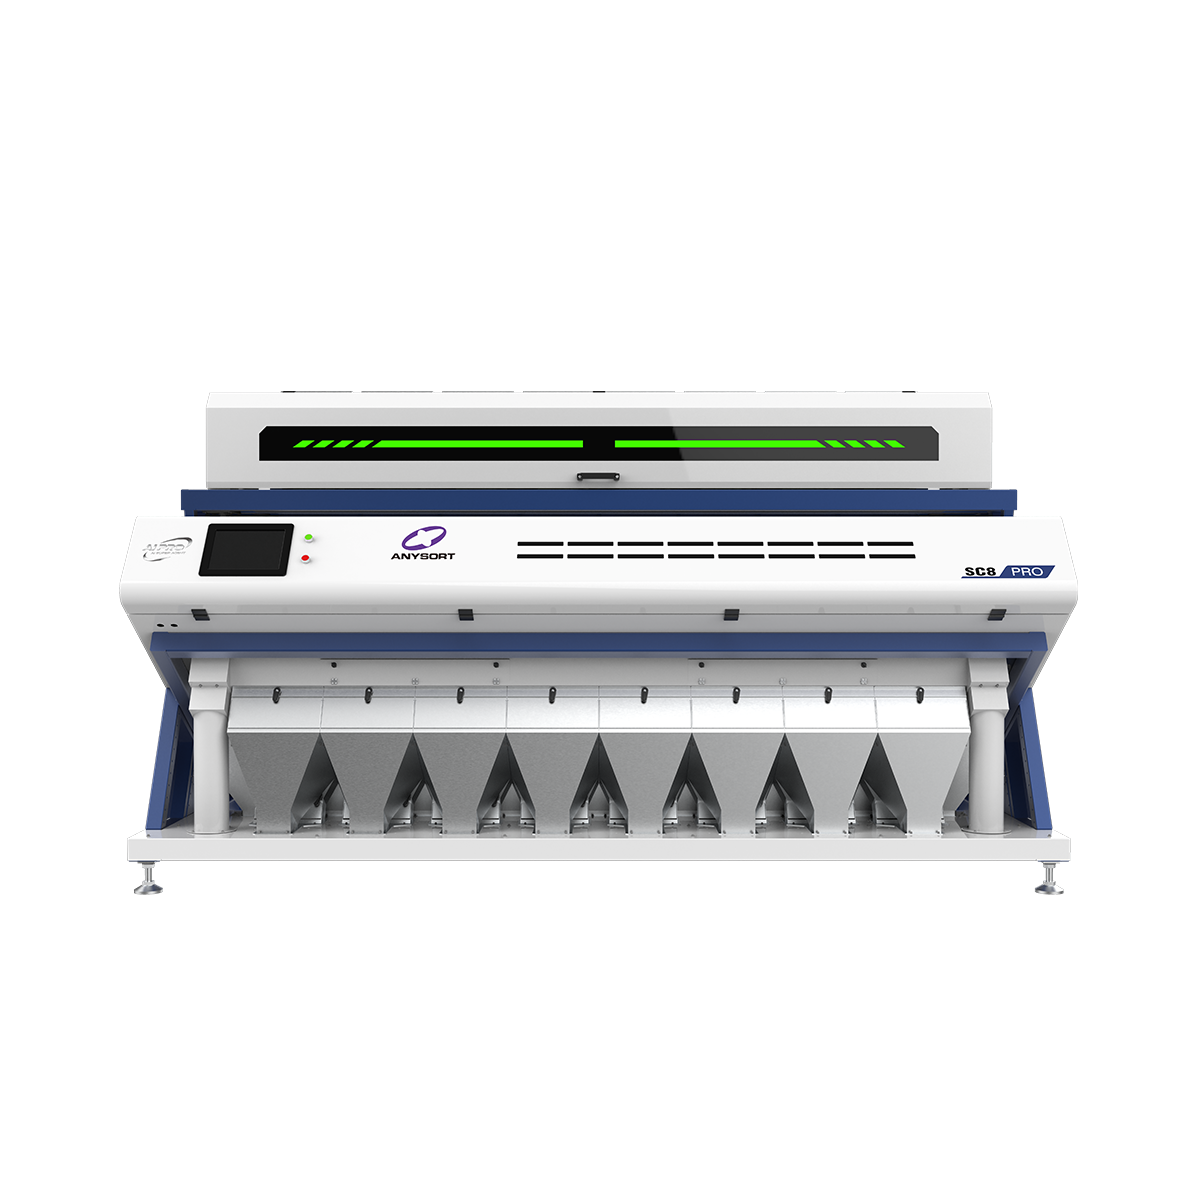
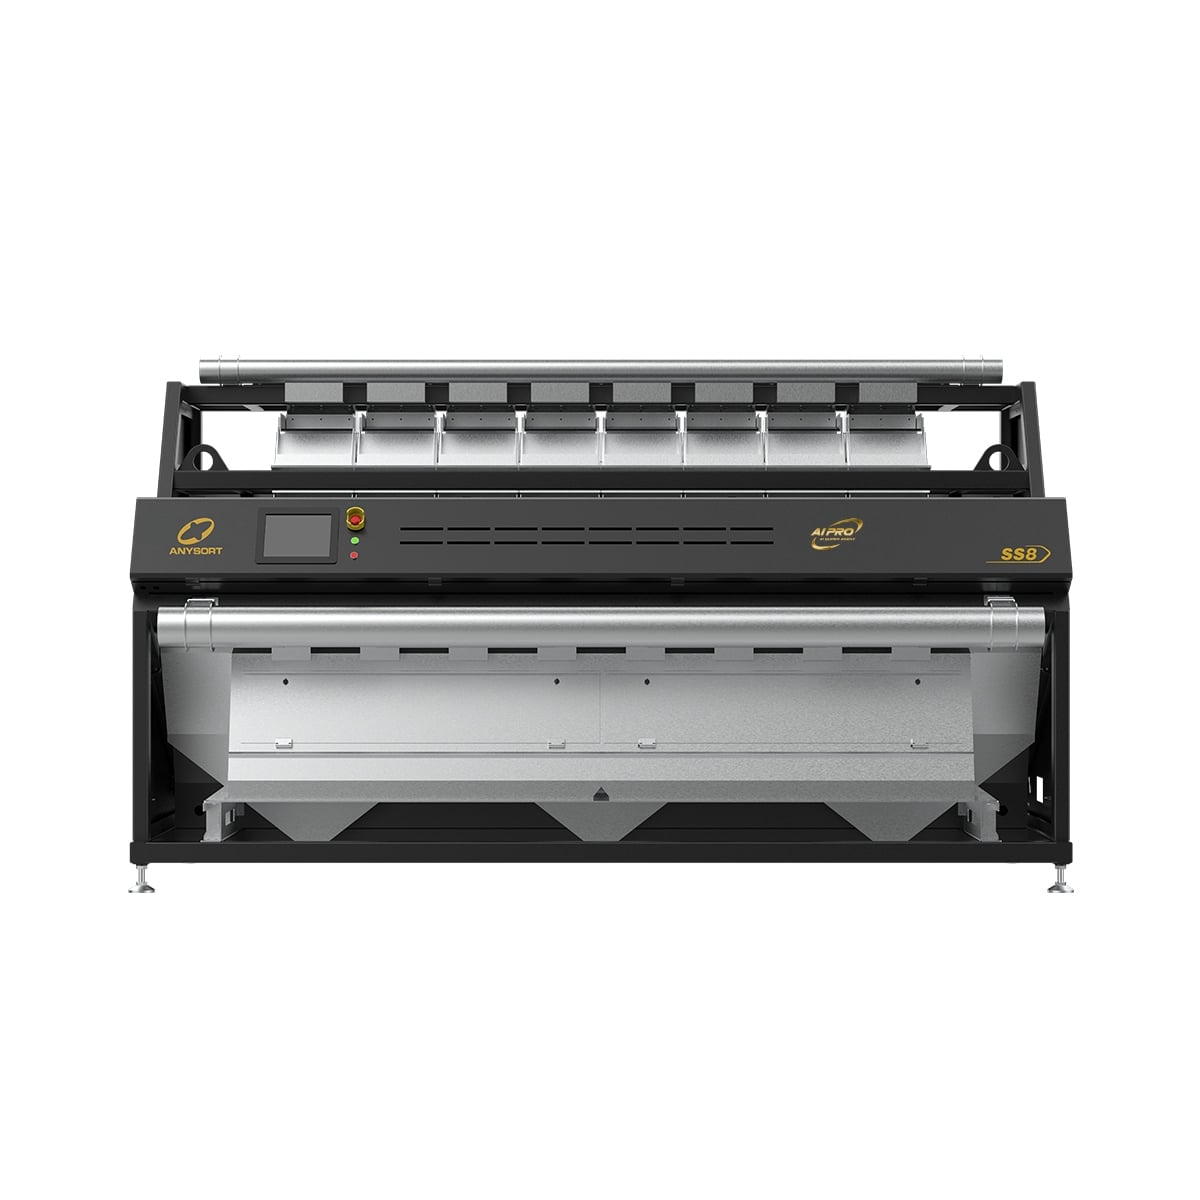
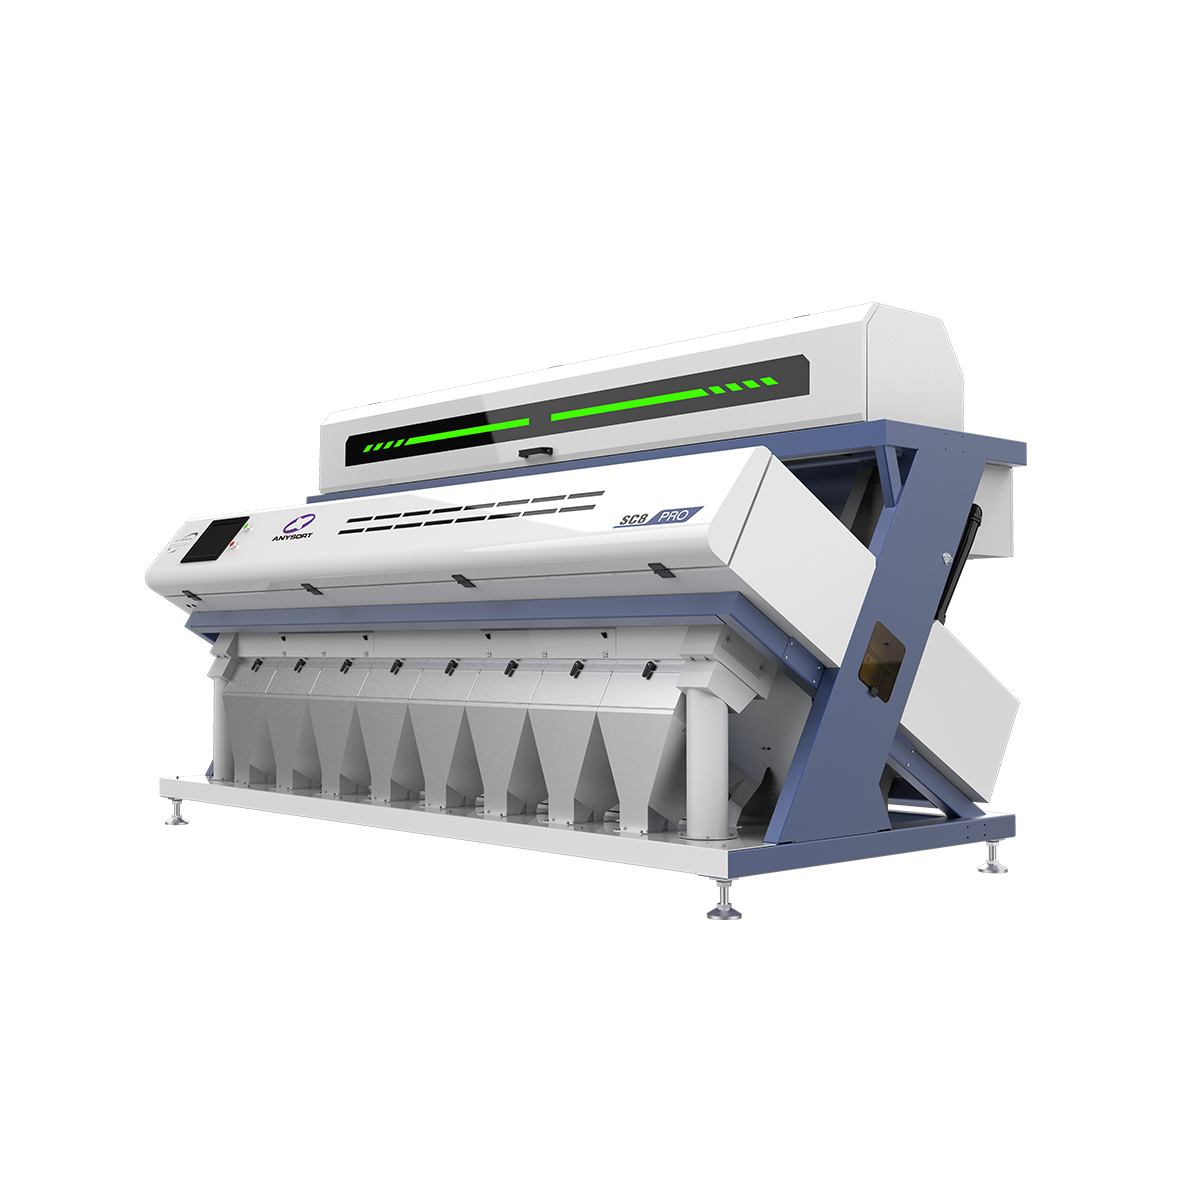
An optical food sorting platform represents a revolutionary technology that transforms how food processing facilities manage quality control and product consistency. This advanced system utilizes cutting-edge optical scanning and artificial intelligence to automatically detect and remove defective items from production lines with exceptional precision. The optical food sorting platform employs high-resolution cameras and sophisticated imaging algorithms to analyze each product individually, identifying contaminants, discoloration, damage, and irregularities that human inspectors might miss. The core functionality of an optical food sorting platform includes real-time product analysis, automatic rejection of substandard items, and comprehensive data logging for traceability. The platform integrates seamlessly with existing production equipment, requiring minimal line modifications while delivering maximum efficiency gains. Using advanced spectral analysis and machine learning capabilities, the optical food sorting platform can process thousands of items per minute, maintaining consistent quality standards throughout production runs. Applications span across diverse food industries, including grains, nuts, pulses, rice, dried fruits, and vegetables. The optical food sorting platform serves food manufacturers, processors, and exporters who demand premium quality assurance. Installation is straightforward, with user-friendly interfaces allowing operators to customize sorting parameters based on specific product requirements. The technology significantly reduces labor costs, minimizes waste, and ensures compliance with international food safety standards while enhancing overall operational efficiency and product reputation.

New Products

The optical food sorting platform delivers transformative benefits that directly enhance your bottom line and operational excellence. First, it dramatically reduces manual inspection costs by automating quality control processes that traditionally required extensive human labor. Your facility can process significantly higher volumes while maintaining superior quality standards without proportional increases in staffing expenses. Operational efficiency improvements are substantial and immediate. An optical food sorting platform works continuously without fatigue, maintaining consistent performance across all shifts and production cycles. The system operates at exceptional speeds, processing hundreds of items per minute while making accurate sorting decisions instantaneously. This reliability translates directly into higher throughput and reduced production bottlenecks that typically slow conventional sorting methods. Quality assurance reaches unprecedented levels with the optical food sorting platform. By detecting defects invisible to human eyes, including internal damage, subtle discoloration, and contamination, you ensure only premium products reach customers. This capability strengthens brand reputation, reduces returns, and builds customer loyalty through consistent excellence. The optical food sorting platform offers remarkable flexibility across product types and specifications. Operators easily adjust sorting parameters to accommodate different items, sizes, and quality thresholds without requiring extensive recalibration or downtime. This adaptability maximizes equipment utilization across your entire product portfolio. Cost savings extend beyond labor reduction. The platform minimizes product waste by precisely identifying salvageable items while removing only genuinely defective products. Enhanced traceability features provide comprehensive documentation for regulatory compliance and quality audits, reducing administrative burden and strengthening accountability throughout your supply chain operations.

Tips And Tricks

What Factors Affect Tea Color Sorter Performance and Accuracy?

05

Aug

What Factors Affect Tea Color Sorter Performance and Accuracy?

The precision of a tea color sorter directly determines the quality consistency of finished tea products. Understanding the factors that influence tea color sorter performance and accuracy is essential for tea processors seeking to maintain competiti...
View More
How Much Does a Color Sorter Machine Cost?

12

Aug

How Much Does a Color Sorter Machine Cost?

Understanding the investment required for a color sorter machine is essential for businesses in agriculture, food processing, and recycling sectors. The cost of a color sorter machine varies significantly based on capacity, technology sophistication,...
View More
How Can a Nuts Sorter Improve Your Production?

15

Aug

How Can a Nuts Sorter Improve Your Production?

A nuts sorter represents one of the most significant investments a food processing operation can make to enhance production quality and operational efficiency. The modern nuts sorter uses advanced imaging and sensor technology to identify and separat...
View More
Top AI Color Sorter Manufacturers in China (2026)

30

Aug

Top AI Color Sorter Manufacturers in China (2026)

The global demand for precision sorting technology has surged dramatically, with color sorter machine manufacturers in China leading innovation across agricultural and industrial sectors. Chinese color sorter machine manufacturers have established th...
View More

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

optical food sorting platform

Advanced Optical Recognition Technology

Advanced Optical Recognition Technology

The optical food sorting platform incorporates state-of-the-art imaging sensors and artificial intelligence algorithms that analyze products with extraordinary precision. These sophisticated optical systems capture detailed visual information from multiple angles, enabling the platform to identify even microscopic defects that escape human detection. The machine learning capabilities continuously improve accuracy through exposure to diverse product variations and sorting scenarios. This technological foundation allows the optical food sorting platform to distinguish between minor surface blemishes and serious quality issues, making intelligent sorting decisions based on customizable criteria. The system adapts to different lighting conditions, product sizes, and material compositions, ensuring reliable performance across your entire production environment. High-speed processing capabilities enable the platform to evaluate thousands of items per minute while maintaining exceptional accuracy rates exceeding ninety-eight percent, guaranteeing consistent quality control without compromising throughput or reliability in demanding food processing operations.
Seamless Integration and User-Friendly Operation

Seamless Integration and User-Friendly Operation

Installing an optical food sorting platform into your existing production line requires minimal disruption to current operations. The system features modular design that adapts to various conveyor configurations and facility layouts without demanding expensive infrastructure modifications. Integration specialists work closely with your team to ensure smooth deployment while maintaining production schedules throughout the transition process. Operators interact with the optical food sorting platform through intuitive touchscreen interfaces requiring minimal training. The system displays real-time performance metrics, sorting statistics, and diagnostic information in clear, accessible formats. Customizable sorting parameters allow quick adjustments between different products or quality standards without technical expertise. Comprehensive support systems include remote monitoring capabilities, enabling maintenance teams to identify potential issues proactively and schedule service during planned downtime, maximizing equipment availability and minimizing costly production interruptions while supporting your operational goals.
Measurable Cost Savings and ROI Benefits

Measurable Cost Savings and ROI Benefits

Investment in an optical food sorting platform generates compelling financial returns through multiple revenue channels. Labor cost reductions represent the most immediate benefit, as automated quality control eliminates expensive manual inspection positions while reducing overall staffing requirements. These savings accumulate substantially over time, particularly in high-volume facilities processing thousands of items daily across multiple shifts. Waste reduction becomes another significant financial advantage when deploying an optical food sorting platform. Precise defect detection minimizes rejection of acceptable products while ensuring genuinely defective items are removed consistently. This improved accuracy directly translates into higher yield rates and reduced material losses. Enhanced product quality reduces customer complaints, returns, and warranty claims, protecting revenue and strengthening market position. Additionally, comprehensive documentation capabilities reduce compliance costs and potential regulatory penalties, while increased efficiency enables processing higher volumes without proportional capital investment, delivering strong ROI within the first operational year.

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

Copyright © 2026 Anhui Jiexun Optoelectronic Technology Co., Ltd. All rights reserved.  -  Privacy policy