Optical Sorter Price Guide

All Categories

optical sorter price

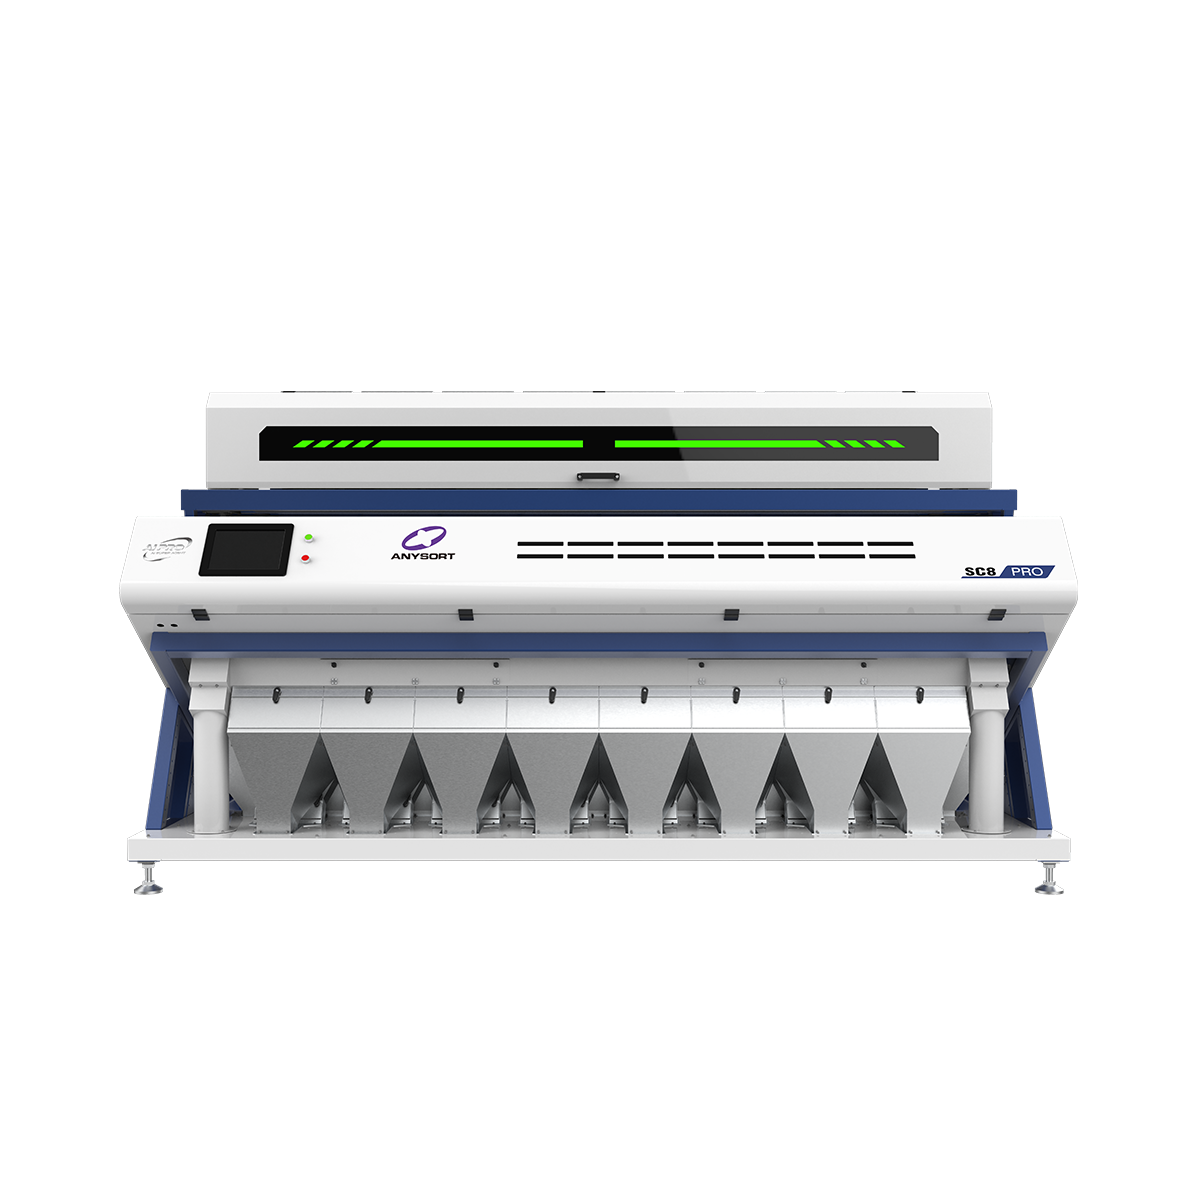
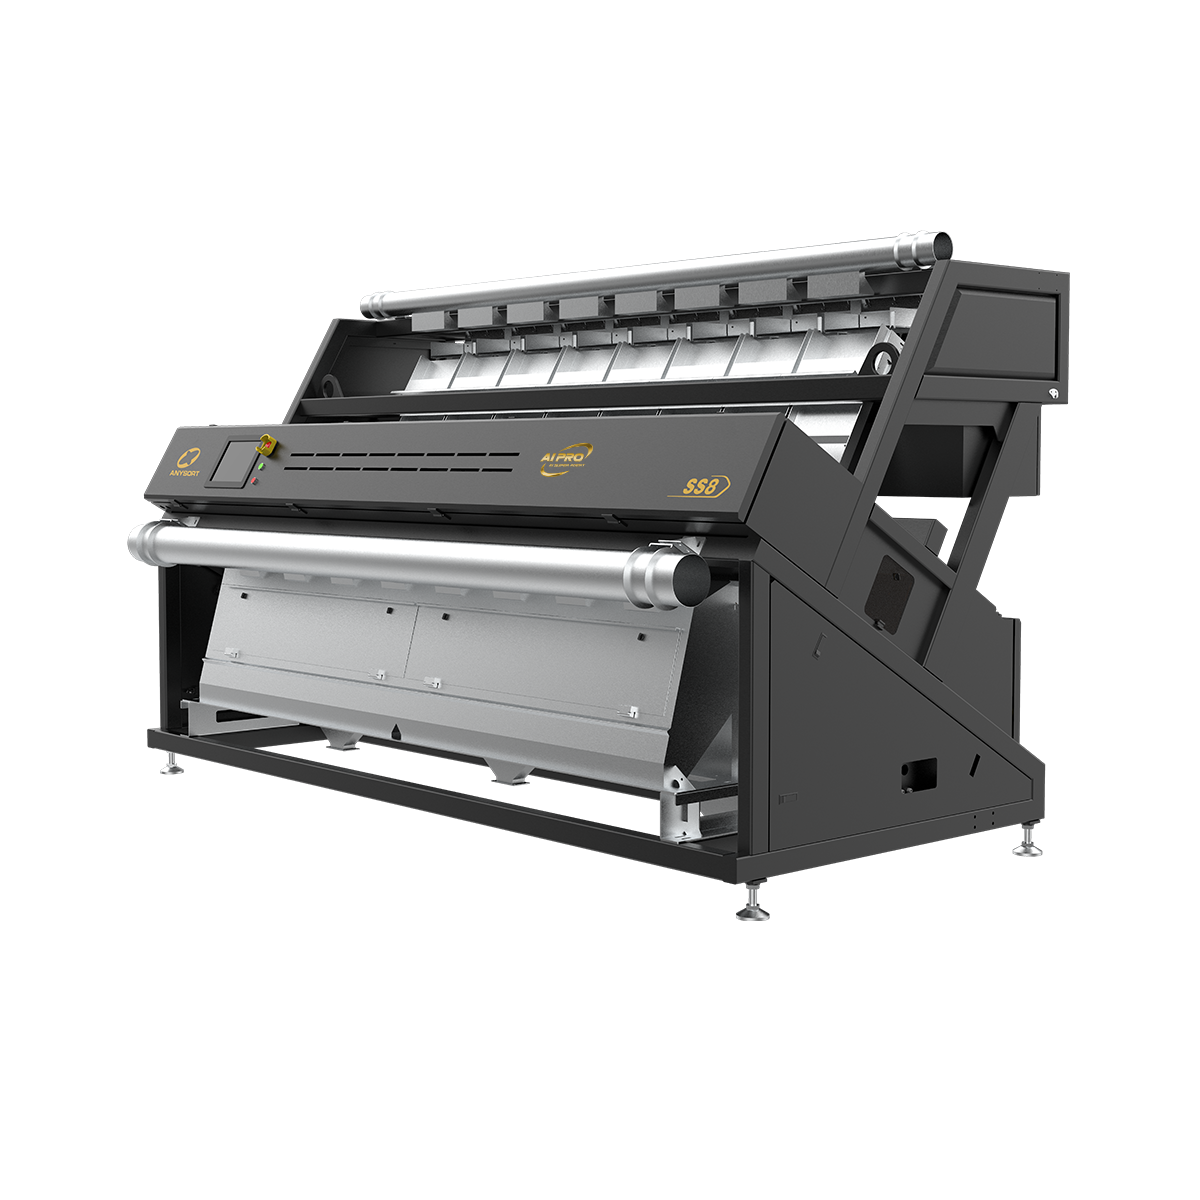
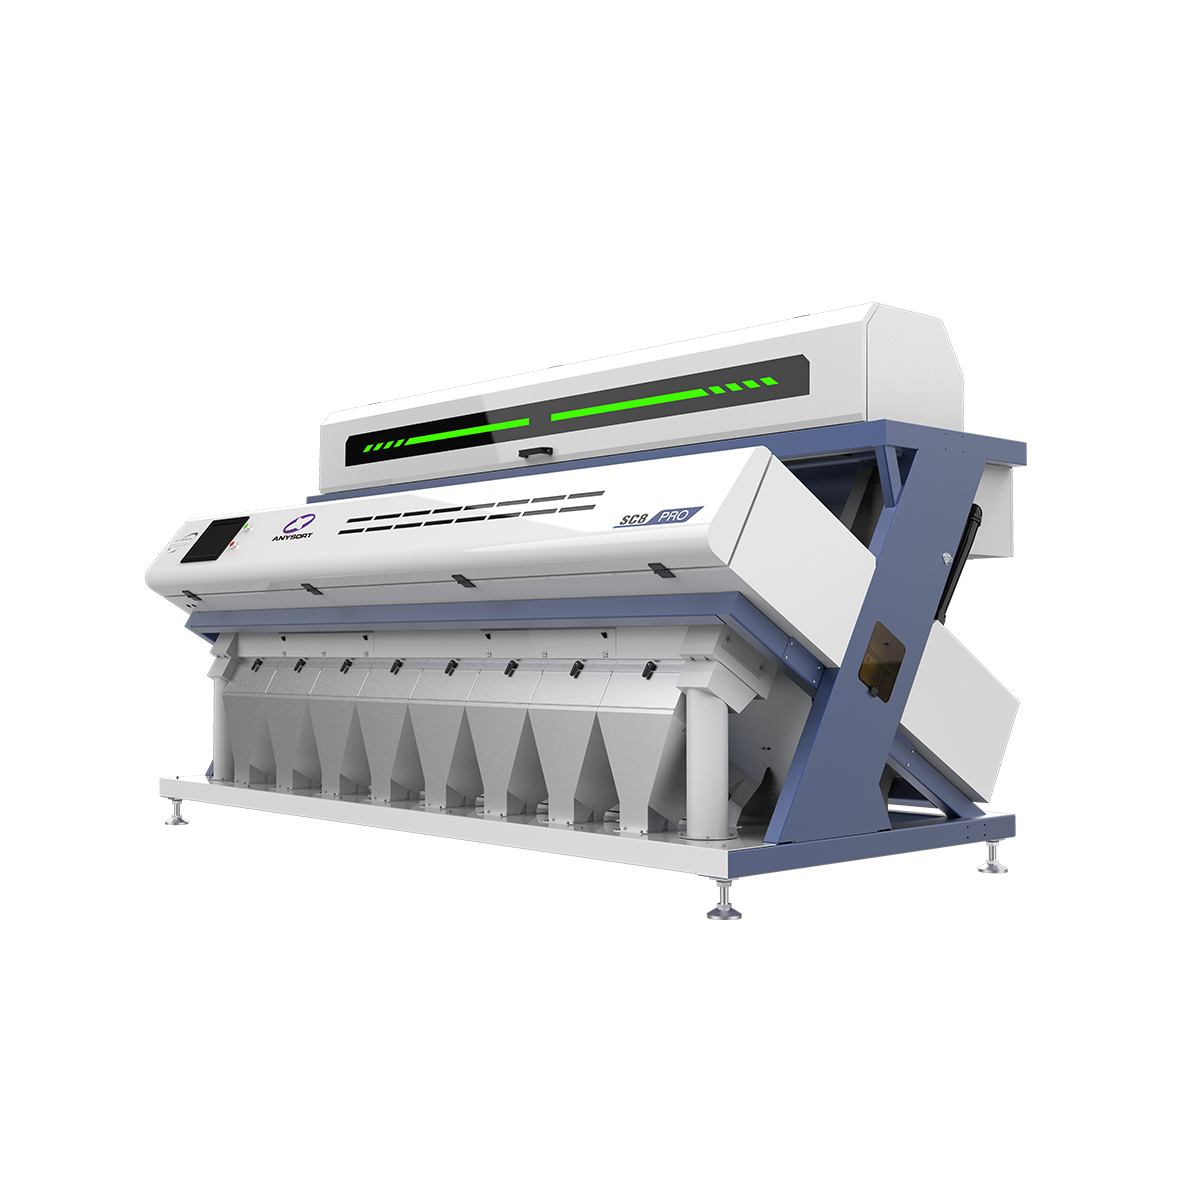
Understanding optical sorter price is essential for businesses seeking efficient sorting solutions. An optical sorter is an advanced machine that uses sophisticated visual recognition technology to automatically separate materials based on color, size, and quality characteristics. The optical sorter price varies depending on capacity, features, and technological sophistication. These machines employ high-speed cameras and artificial intelligence to analyze thousands of particles per second, making them invaluable for numerous industries. The optical sorter price reflects the investment in precision engineering and cutting-edge sensor technology. Modern optical sorters use spectral analysis and machine learning algorithms to achieve sorting accuracy exceeding 99 percent. Applications range from food processing and recycling to mining and agriculture. The optical sorter price consideration includes initial investment, operational costs, and long-term productivity gains. Understanding the optical sorter price helps organizations make informed purchasing decisions aligned with their budget and operational requirements. These systems significantly reduce manual labor, minimize product waste, and improve output quality. Companies evaluating optical sorter price should consider throughput capacity, maintenance requirements, and integration capabilities with existing production lines. The technology behind optical sorter price investments represents a significant advancement in automation and quality control.

Popular Products

Investing in an optical sorter offers remarkable operational benefits that directly impact your bottom line. The optical sorter price delivers exceptional value by automating complex sorting tasks that traditionally require extensive human labor. You gain immediate efficiency improvements, processing materials faster while maintaining superior accuracy standards. The optical sorter price investment eliminates sorting inconsistencies caused by human fatigue, ensuring uniform product quality throughout production cycles. Operational benefits include significant labor cost reductions and improved worker safety by removing personnel from repetitive, physically demanding tasks. Your production line becomes more responsive to market demands with increased throughput and flexibility. The optical sorter price becomes increasingly economical as your operation scales, with per-unit sorting costs decreasing substantially. Decision-useful context shows that modern optical sorters typically recover their investment within two to three years through productivity gains alone. These machines work continuously without breaks, maximizing utilization rates and production capacity. Application suitability spans diverse industries, from food and beverage manufacturing to recycling facilities and agricultural operations. The optical sorter price justification strengthens when considering waste reduction benefits, as these systems minimize product loss and maximize material recovery. Real-time quality monitoring capabilities ensure you maintain consistent standards that satisfy customer requirements and regulatory compliance. Your operational reliability improves dramatically, reducing downtime and maintenance costs compared to manual alternatives. The optical sorter price represents a strategic investment in your facility's competitive advantage and long-term sustainability.

Practical Tips

How to Choose the Right Tea Color Sorter for Your Needs?

01

Aug

How to Choose the Right Tea Color Sorter for Your Needs?

Selecting the right tea color sorter is one of the most critical decisions tea processors face when modernizing their operations. A tea color sorter directly impacts product quality, operational efficiency, and market competitiveness. The wrong choic...
View More
How can rice color sorters improve grain quality?

08

Aug

How can rice color sorters improve grain quality?

Rice color sorters represent a transformative technology in modern grain processing, fundamentally changing how producers maintain and enhance the quality of their rice output. By utilizing advanced optical scanning and artificial intelligence, a ric...
View More
How Does Nuts Sorter Technology Ensure Quality?

19

Aug

How Does Nuts Sorter Technology Ensure Quality?

The global nuts processing industry relies on precision and consistency to meet strict quality standards and regulatory requirements. A nuts sorter has become indispensable for processors seeking to eliminate defects, contaminants, and substandard pr...
View More
How Do Color Sorters Improve Product Quality?

26

Aug

How Do Color Sorters Improve Product Quality?

Product quality stands as a critical differentiator in competitive industrial markets, and achieving consistency at scale requires more than manual oversight. A color sorter represents one of the most effective technologies for identifying and removi...
View More

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

optical sorter price

Advanced Optical Technology and Precision Accuracy

Advanced Optical Technology and Precision Accuracy

The optical sorter price includes cutting-edge visual recognition systems that deliver unmatched sorting precision. These machines employ multispectral imaging technology combined with artificial intelligence algorithms to analyze each particle individually. The optical sorter price investment provides sorting accuracy exceeding 99 percent, ensuring only defective or misgraded materials are removed from your production line. Advanced sensors detect subtle color variations, surface defects, and size inconsistencies invisible to human inspectors. Your product quality improves immediately, as the optical sorter price yields reduced waste and consistent output standards. Real-time data analytics monitor sorting performance continuously, allowing operators to make immediate adjustments. The technology adapts to varying material characteristics, maintaining accuracy regardless of processing conditions or environmental factors. This precision capability justifies the optical sorter price by protecting your brand reputation and customer satisfaction metrics.
Significant Cost Savings and Rapid Return on Investment

Significant Cost Savings and Rapid Return on Investment

The optical sorter price becomes economically justified through substantial operational cost reductions and efficiency gains. By automating sorting processes, you eliminate labor-intensive manual work, reducing personnel costs by up to 80 percent. Most installations recover the optical sorter price investment within 24 to 36 months through productivity improvements alone. Continuous operation without breaks maximizes equipment utilization, increasing throughput while minimizing per-unit processing costs. The optical sorter price analysis shows additional savings from reduced material waste and improved product recovery rates. Energy-efficient designs minimize operating expenses while maintaining peak performance standards. Maintenance costs remain predictable and reasonable, with most systems requiring only routine calibration and sensor cleaning. The optical sorter price demonstrates compelling financial benefits, particularly for high-volume production facilities processing thousands of units daily.
Versatile Applications Across Multiple Industries

Versatile Applications Across Multiple Industries

The optical sorter price makes this technology accessible for diverse industrial applications and operational environments. Food processing facilities use optical sorters to inspect and grade produce, nuts, grains, and packaged products with exceptional consistency. Recycling operations employ the optical sorter price investment to separate plastics, metals, and other materials efficiently. Mining companies utilize this technology to sort ore concentrations and valuable minerals from waste material. Agricultural operations benefit from the optical sorter price by processing seeds, beans, and specialty crops for quality assurance. Glass and ceramic manufacturers employ optical sorting to remove contaminants and defects before packaging. The versatility of optical sorter price solutions extends to pharmaceutical and chemical applications requiring contamination detection. Industrial waste management facilities leverage this technology for material recovery and environmental compliance. Regardless of your industry, the optical sorter price offers tailored solutions that enhance productivity, ensure quality consistency, and meet regulatory requirements.

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

Copyright © 2026 Anhui Jiexun Optoelectronic Technology Co., Ltd. All rights reserved.  -  Privacy policy