key optical sorter
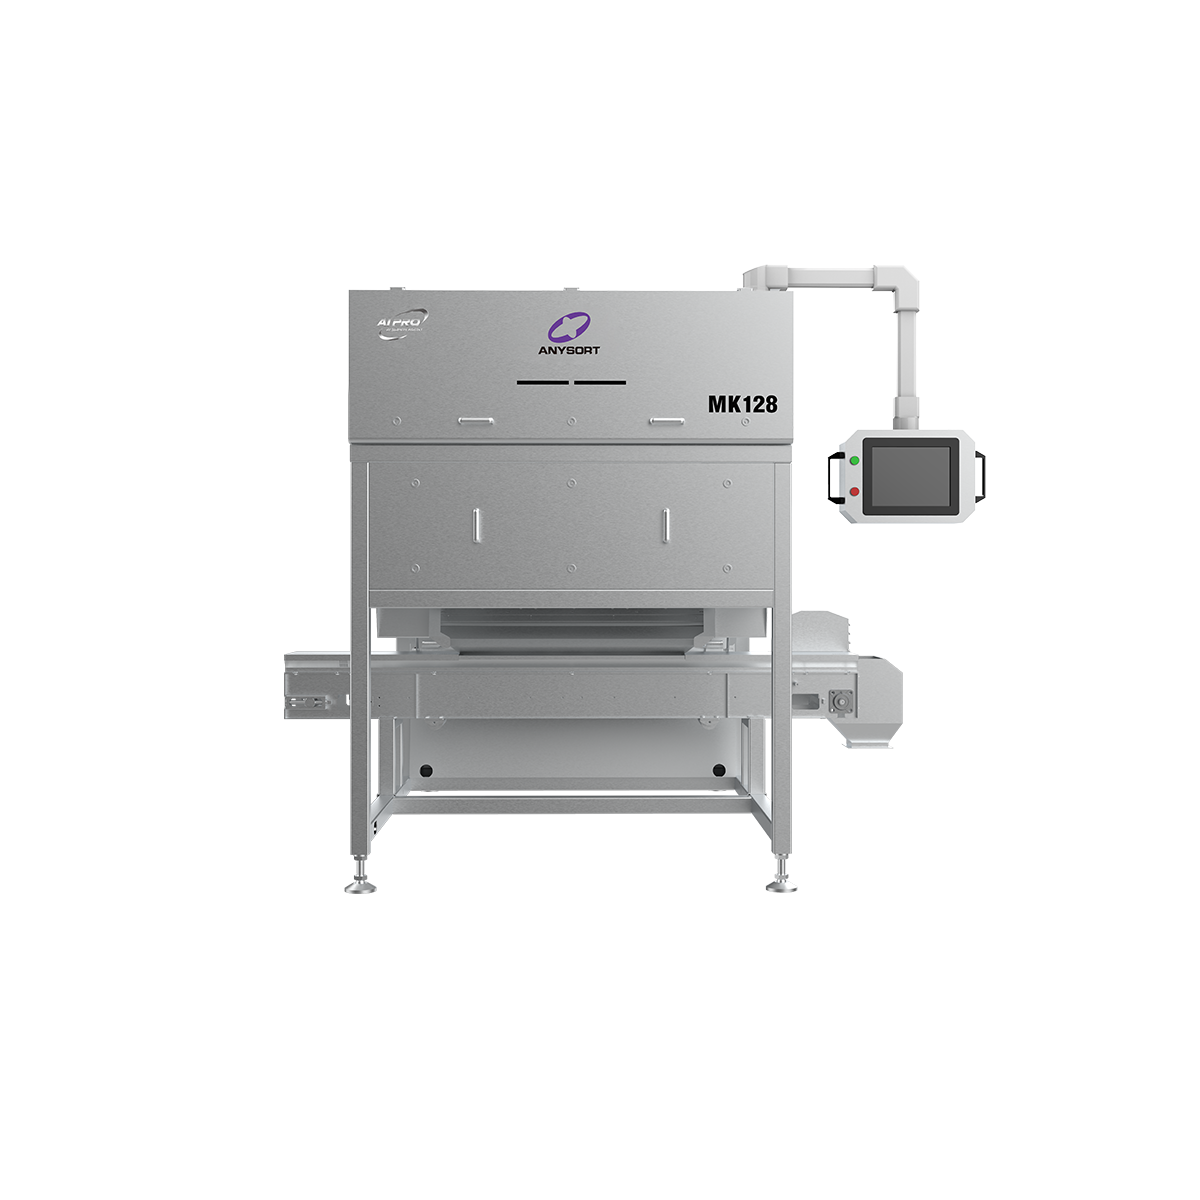
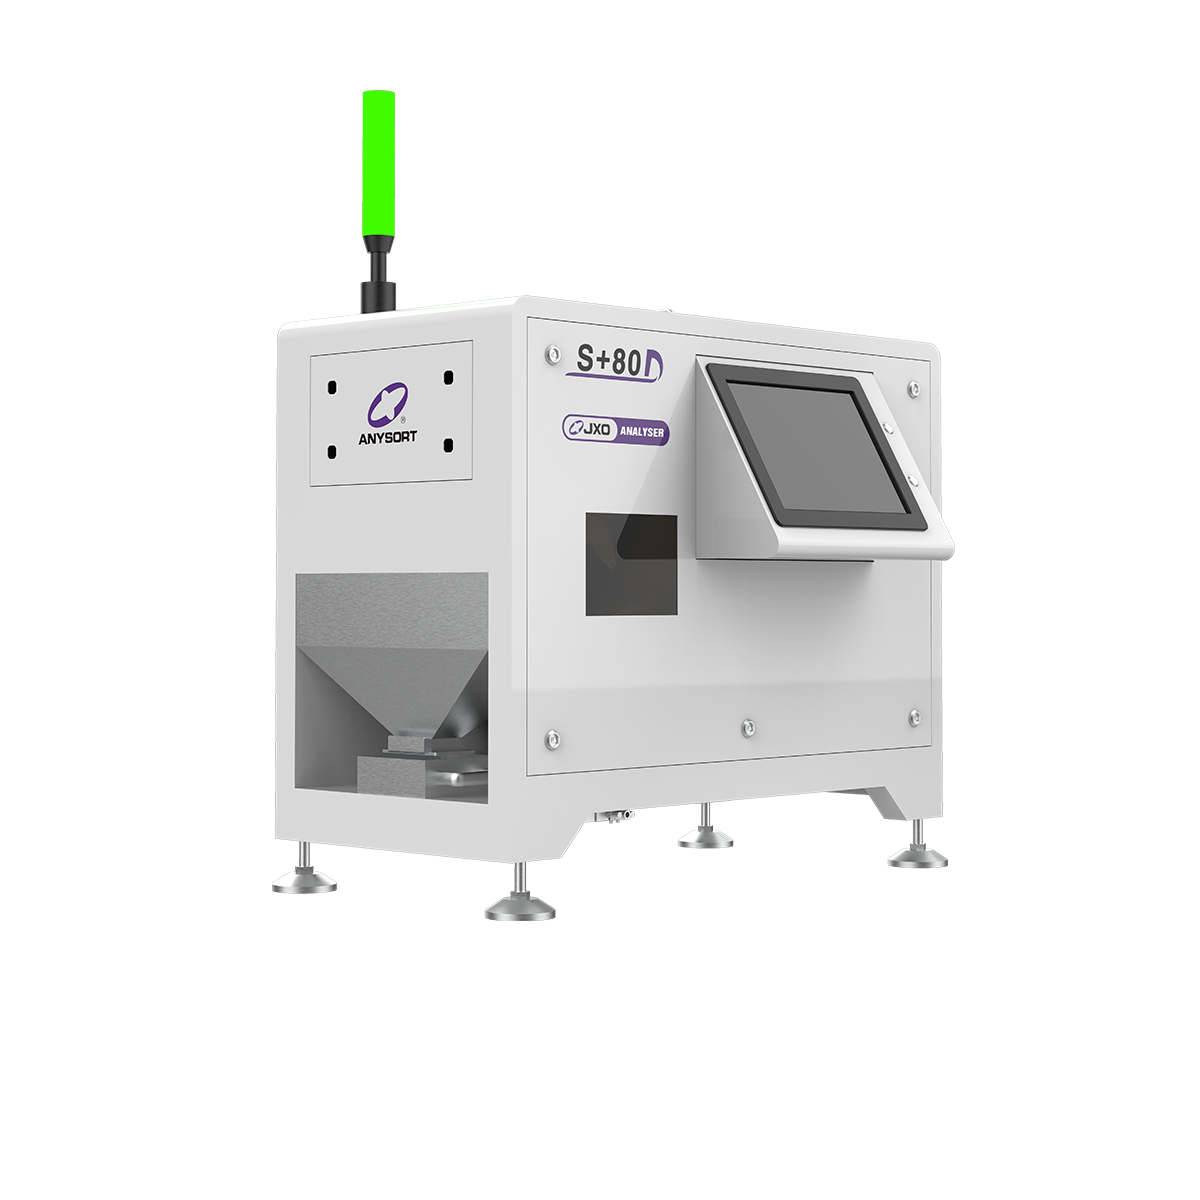
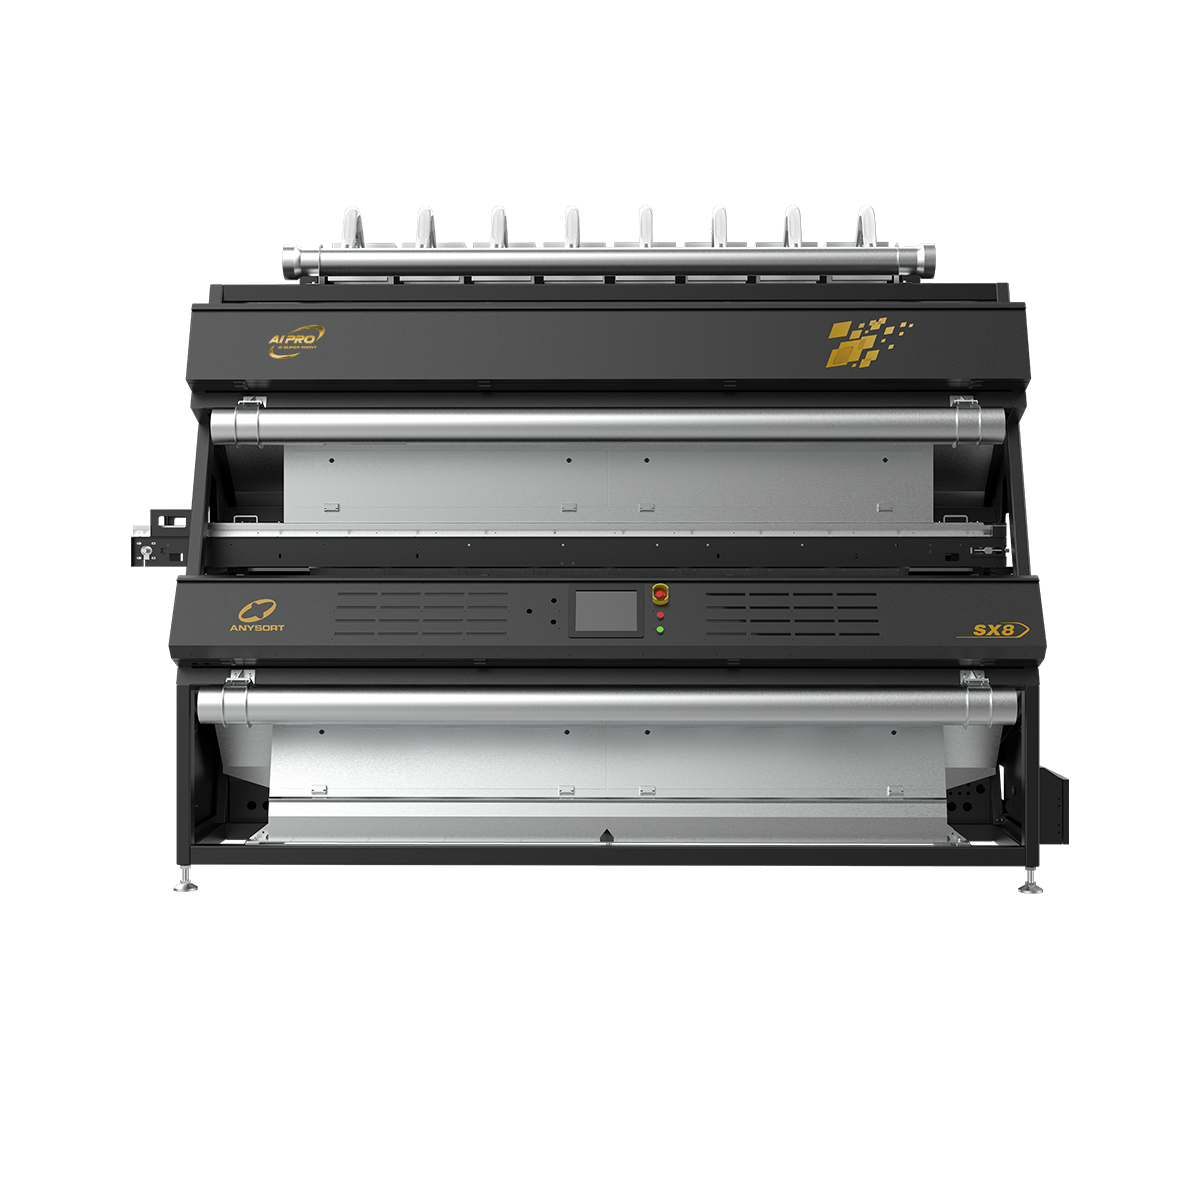
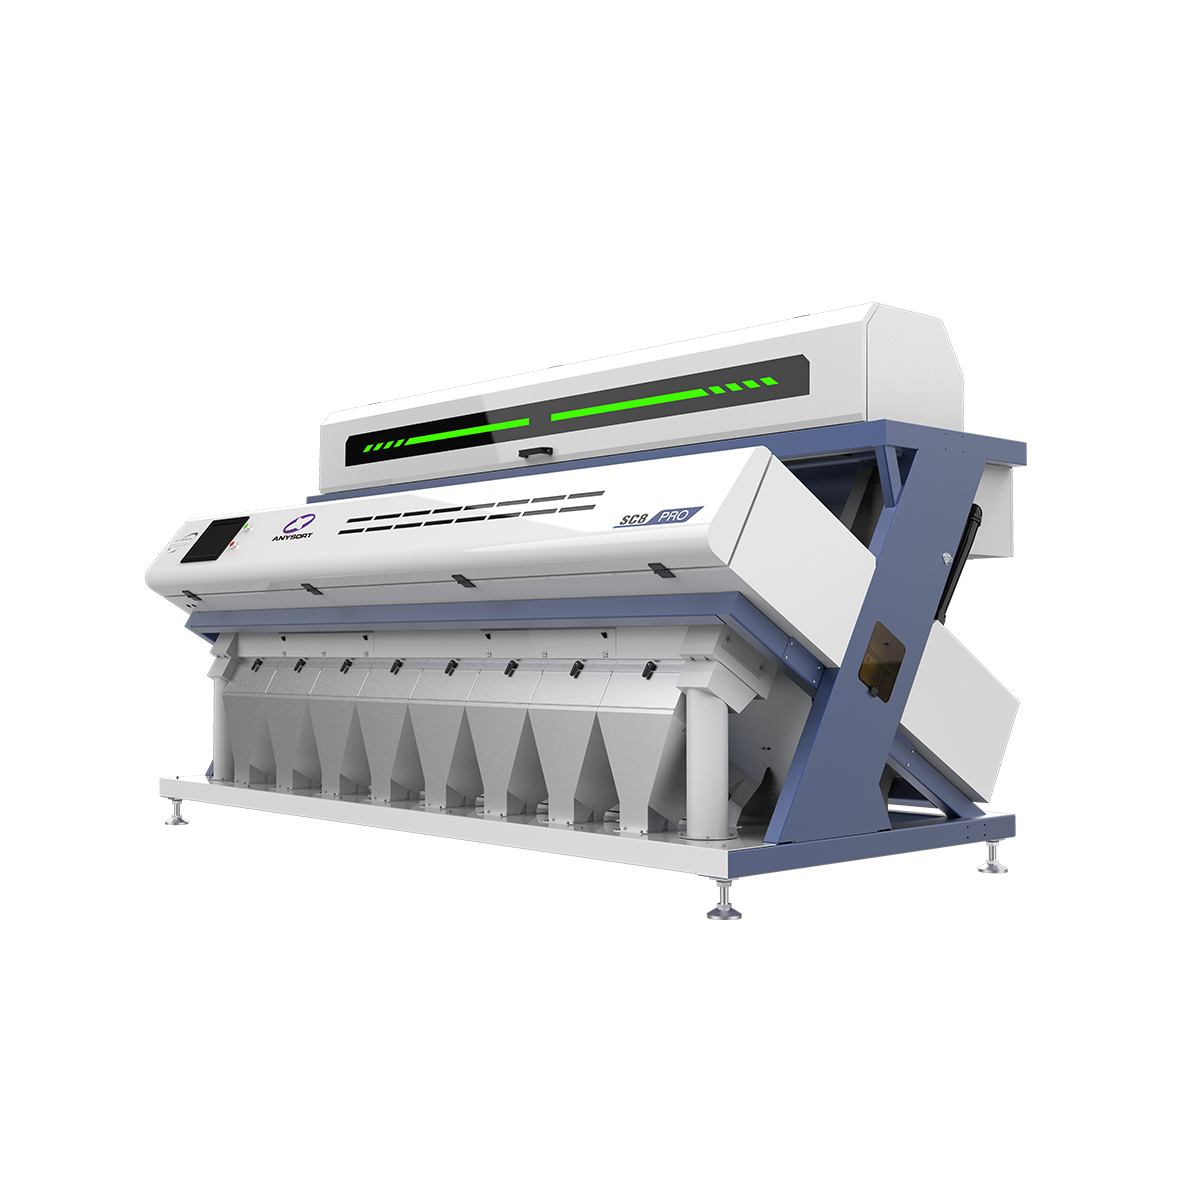
A key optical sorter represents an advanced technological solution designed to automatically identify, classify, and separate materials based on their optical properties. This key optical sorter utilizes sophisticated imaging and sensor technology to distinguish between different material types, colors, sizes, and quality grades with exceptional precision. The key optical sorter operates by scanning individual items as they pass through the sorting system, using high-speed cameras and spectral analysis to capture detailed information about each object. The key optical sorter then processes this data through artificial intelligence algorithms to make instantaneous sorting decisions, directing materials to appropriate discharge points with remarkable accuracy. Key optical sorter systems incorporate multiple technological features including LED lighting systems, high-resolution image sensors, real-time processing capabilities, and pneumatic ejection mechanisms. These components work together seamlessly to ensure consistent performance across various material types. The key optical sorter finds applications across diverse industries, including food processing, recycling, mining, grain handling, and plastic waste management. In food production, a key optical sorter efficiently removes contaminants and sorts products by quality. In recycling operations, the key optical sorter separates different plastic types and metals with high efficiency. The key optical sorter's ability to process hundreds of items per second makes it invaluable for high-volume sorting operations. Modern key optical sorter equipment features user-friendly interfaces, customizable sorting parameters, and data analytics capabilities for monitoring performance. This combination of speed, accuracy, and versatility makes the key optical sorter an essential investment for businesses seeking to optimize their material handling processes.

 EN