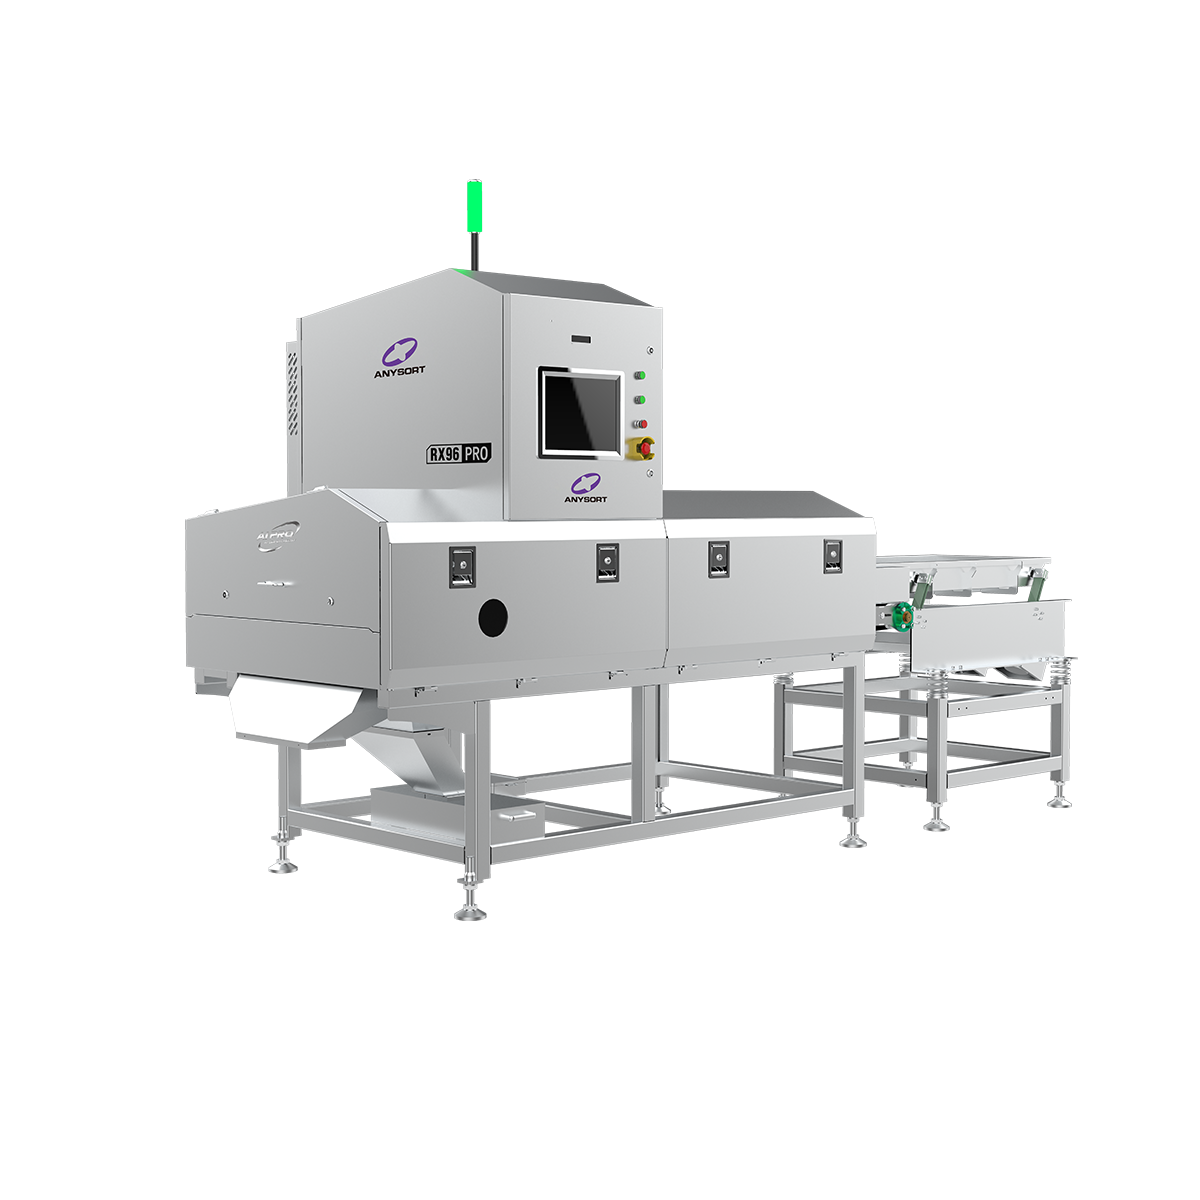
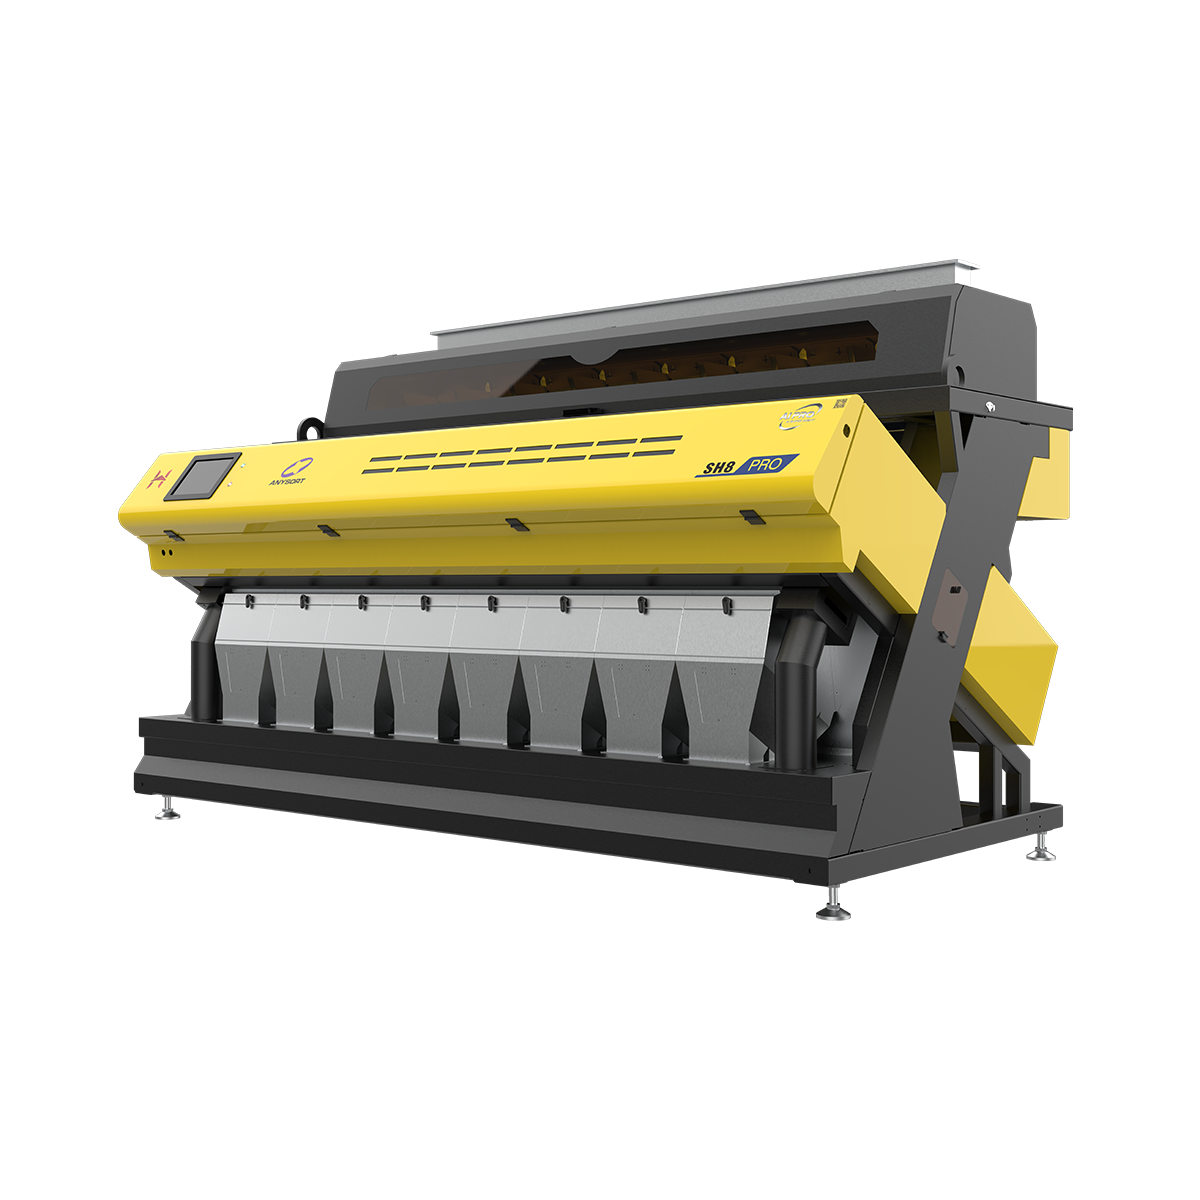
color sorter machine in china
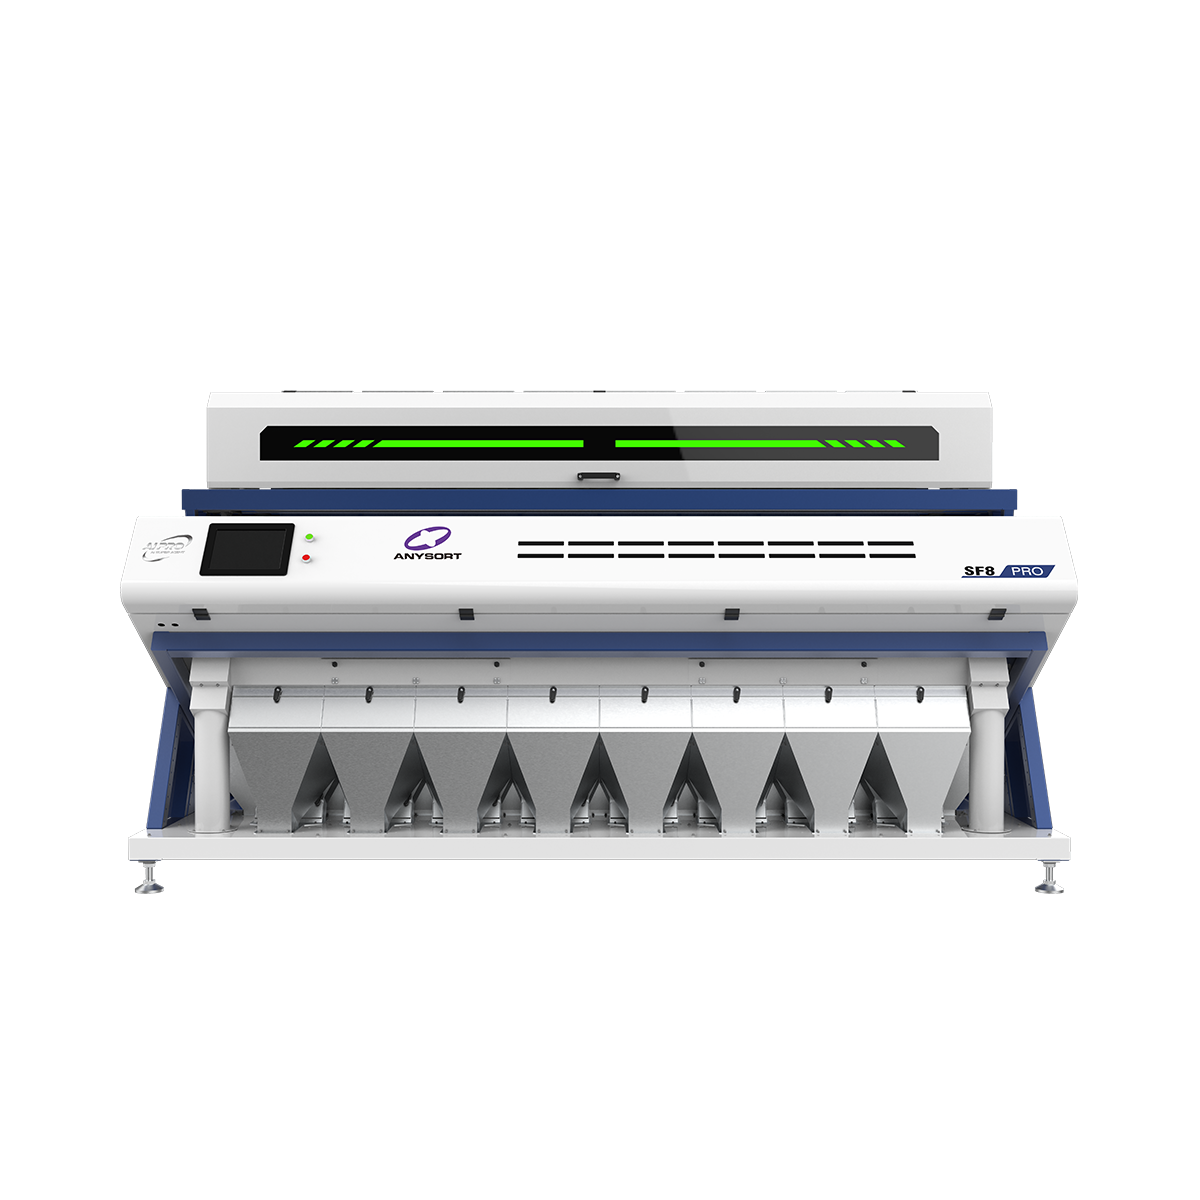
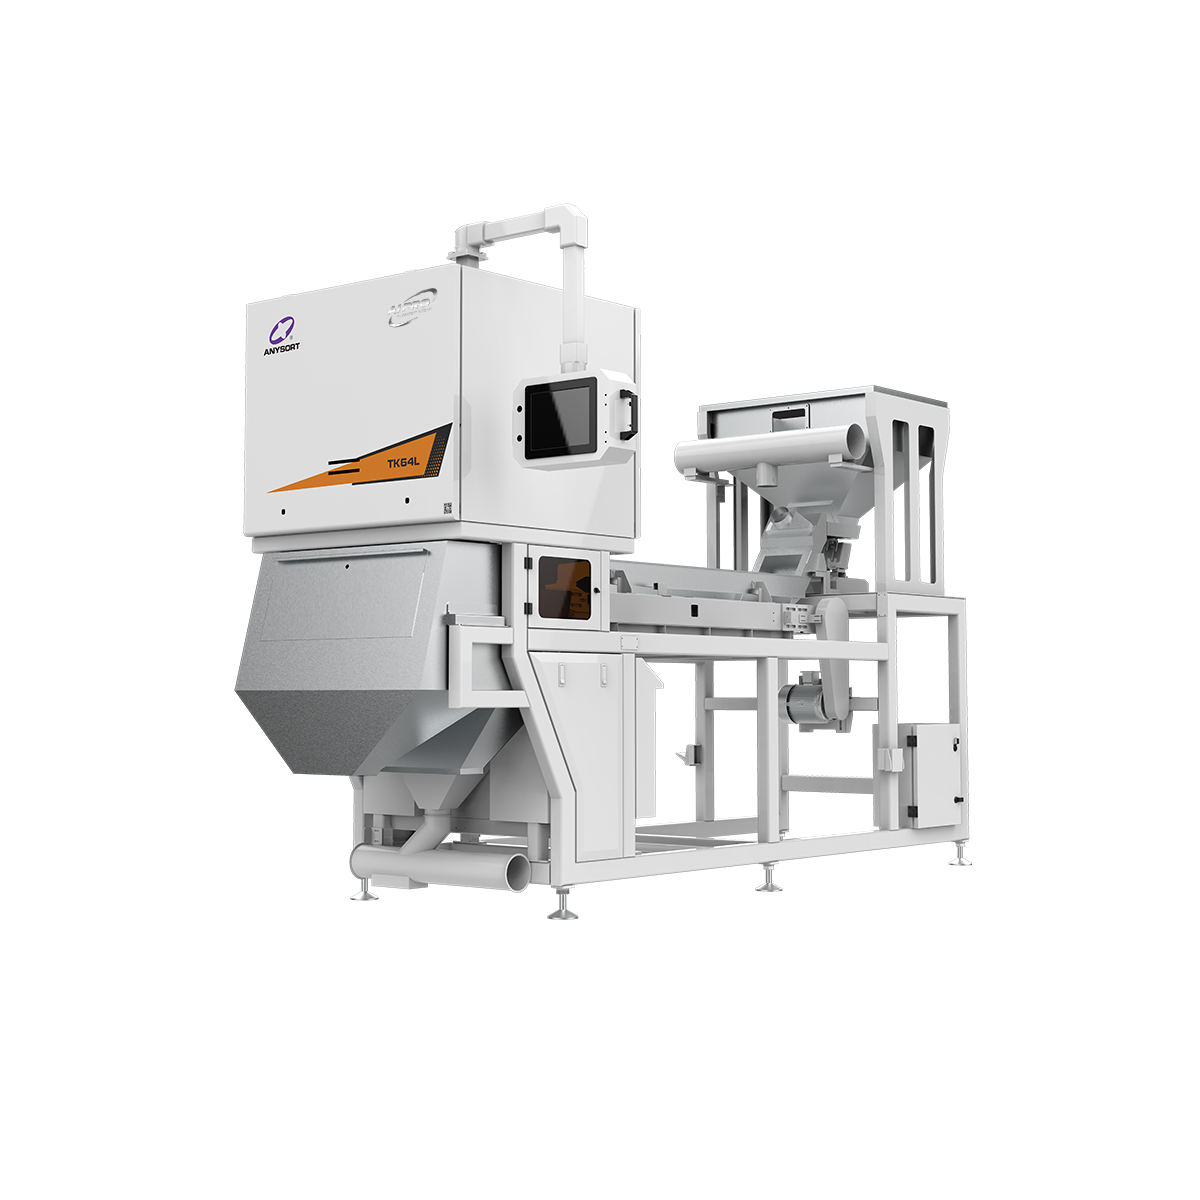
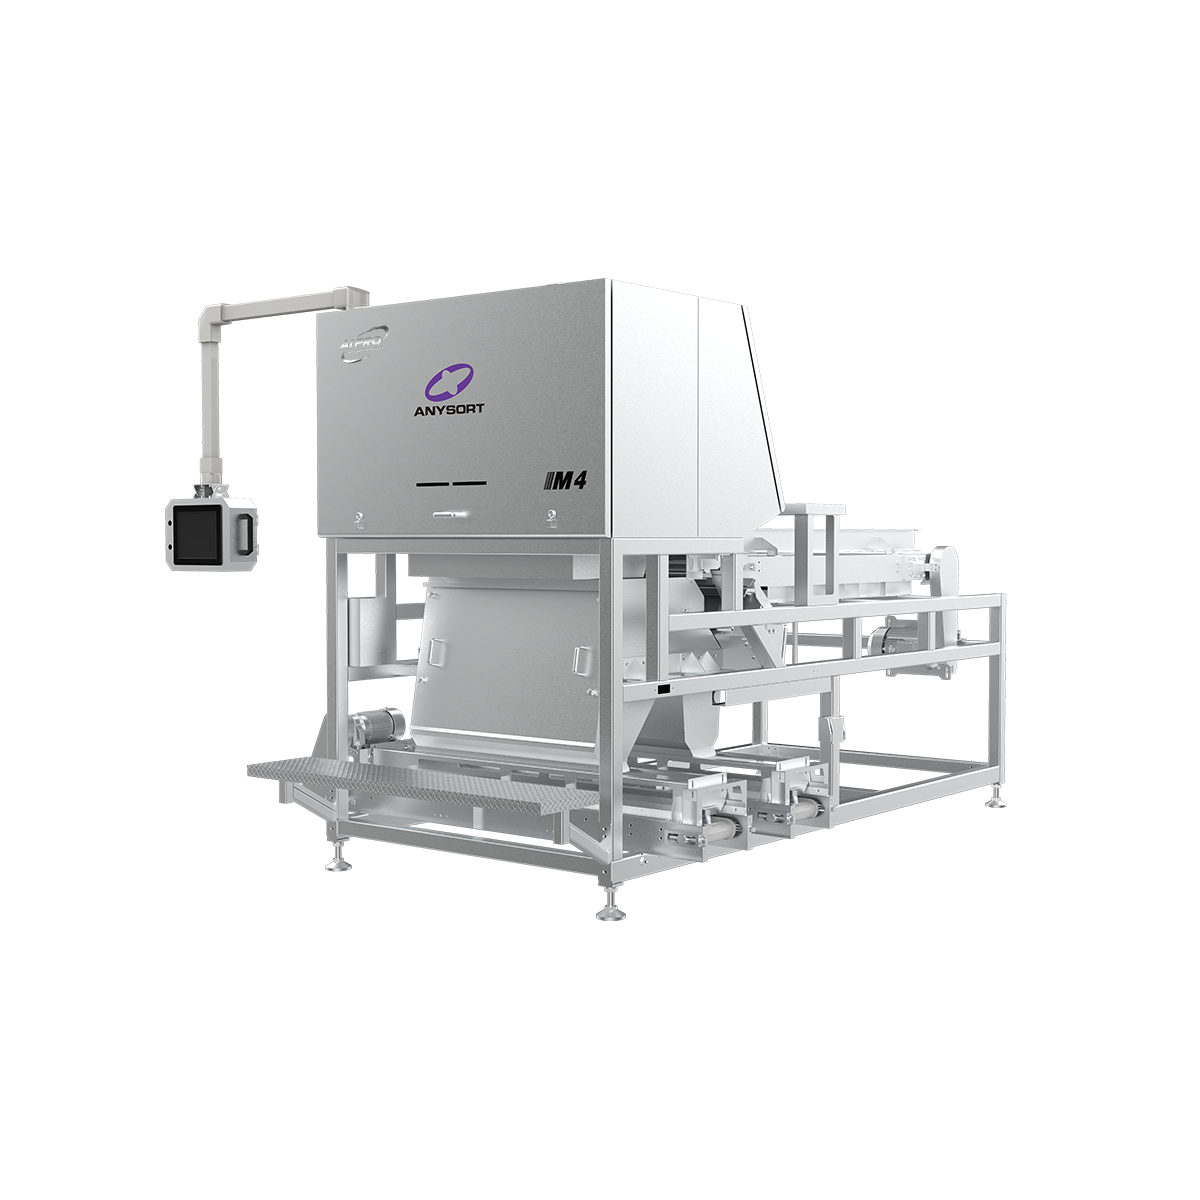
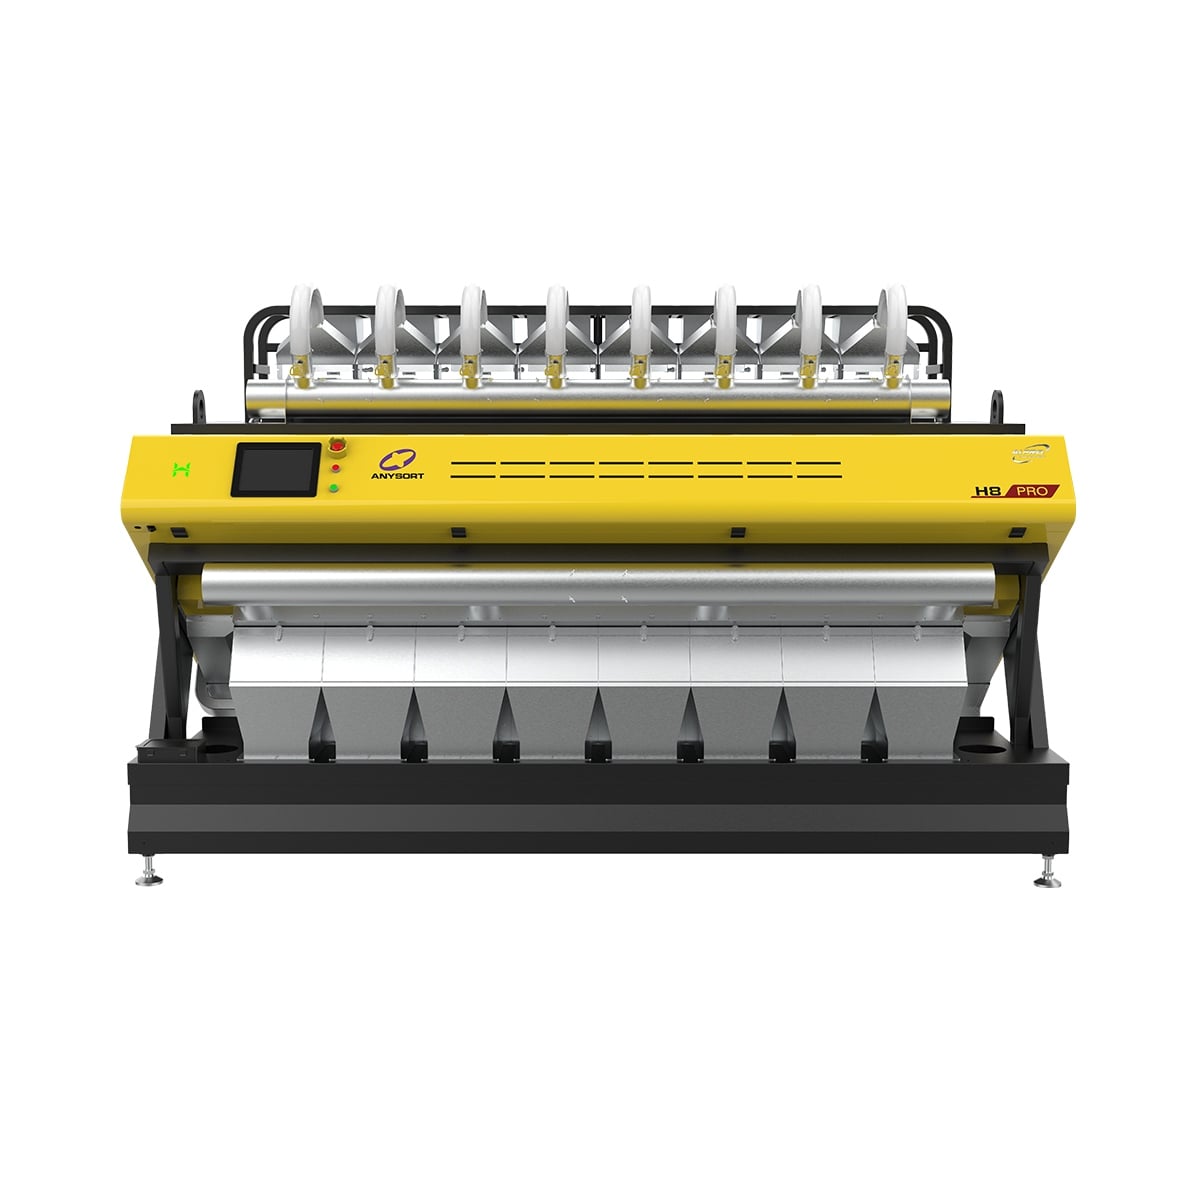
A color sorter machine in China represents cutting-edge technology in agricultural and industrial processing. This sophisticated equipment uses advanced optical sensors and artificial intelligence to automatically separate materials based on color, size, and quality characteristics. The color sorter machine in China has become essential in rice mills, food processing plants, and mineral sorting facilities across the nation.
The primary function of a color sorter machine in China involves scanning thousands of particles per second using high-resolution cameras and LED lighting systems. Each item passes through the detection zone where sensors analyze its properties and compare them against preset standards. When the system identifies defects, discoloration, or foreign materials, precision air jets instantly remove those items from the product stream.
Technological features of modern color sorter machines include multi-spectral imaging, neural network algorithms, and real-time processing capabilities. These systems can detect subtle color variations invisible to human eyes, ensuring consistent product quality. The color sorter machine in China integrates touchscreen interfaces, data logging functions, and remote monitoring capabilities for enhanced operational control.
Applications span multiple industries including rice processing, tea sorting, grain cleaning, plastic recycling, and gemstone classification. The color sorter machine in China significantly reduces labor costs while improving output consistency. Industries rely on this equipment to meet stringent international quality standards and consumer expectations. Modern installations process between 200 to 500 tons daily, making them indispensable for large-scale commercial operations seeking competitive advantages.

 EN