Corn Color Sorter | Advanced Optical Sorting

All Categories

corn color sorter

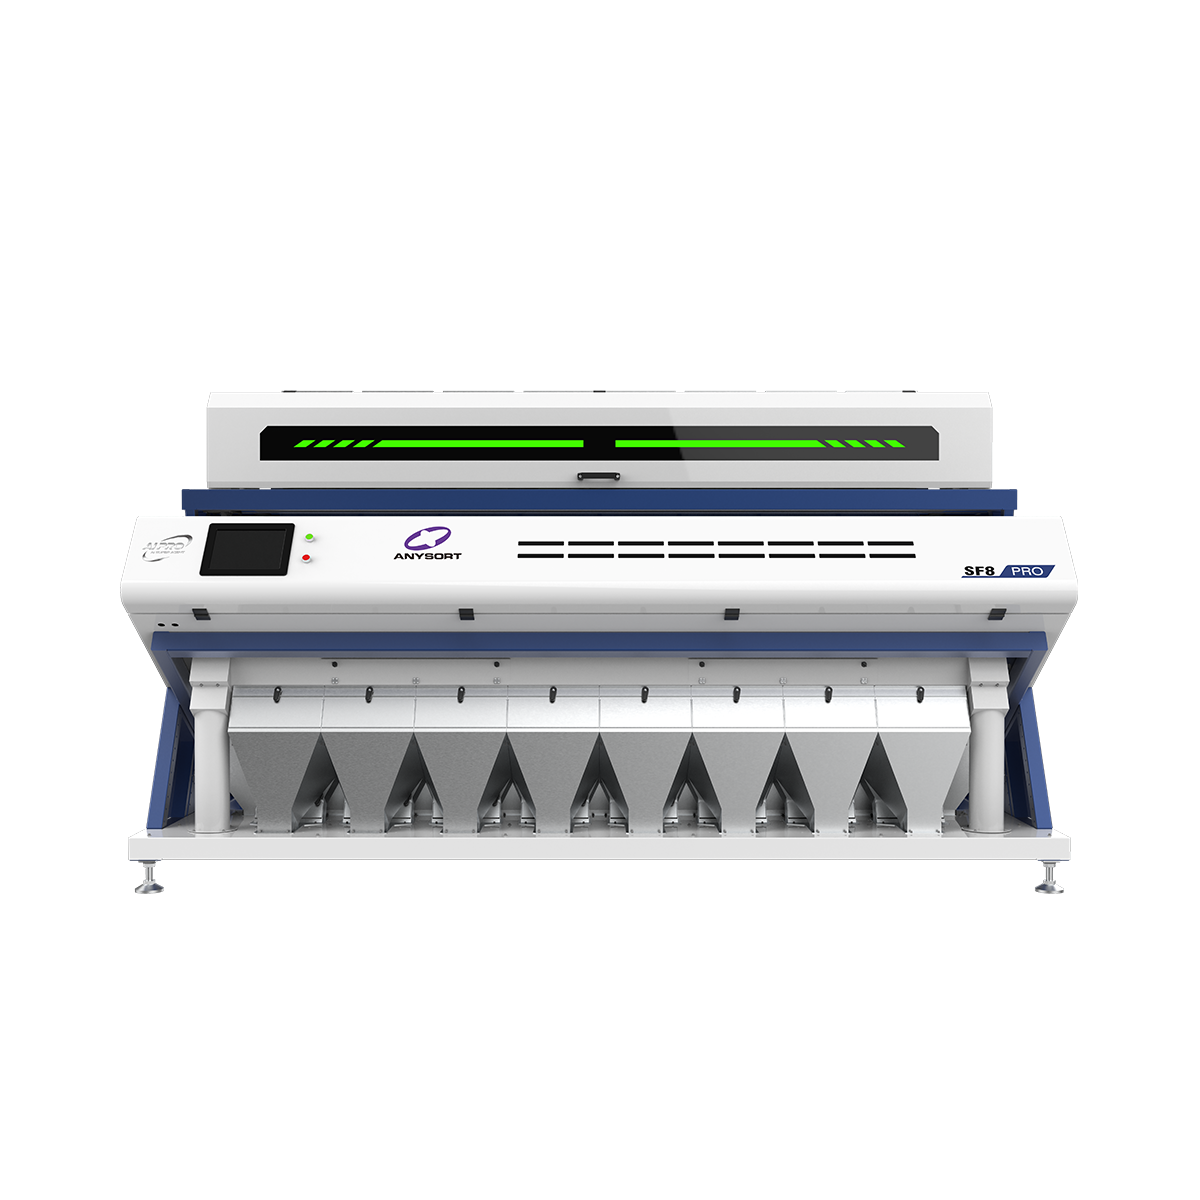
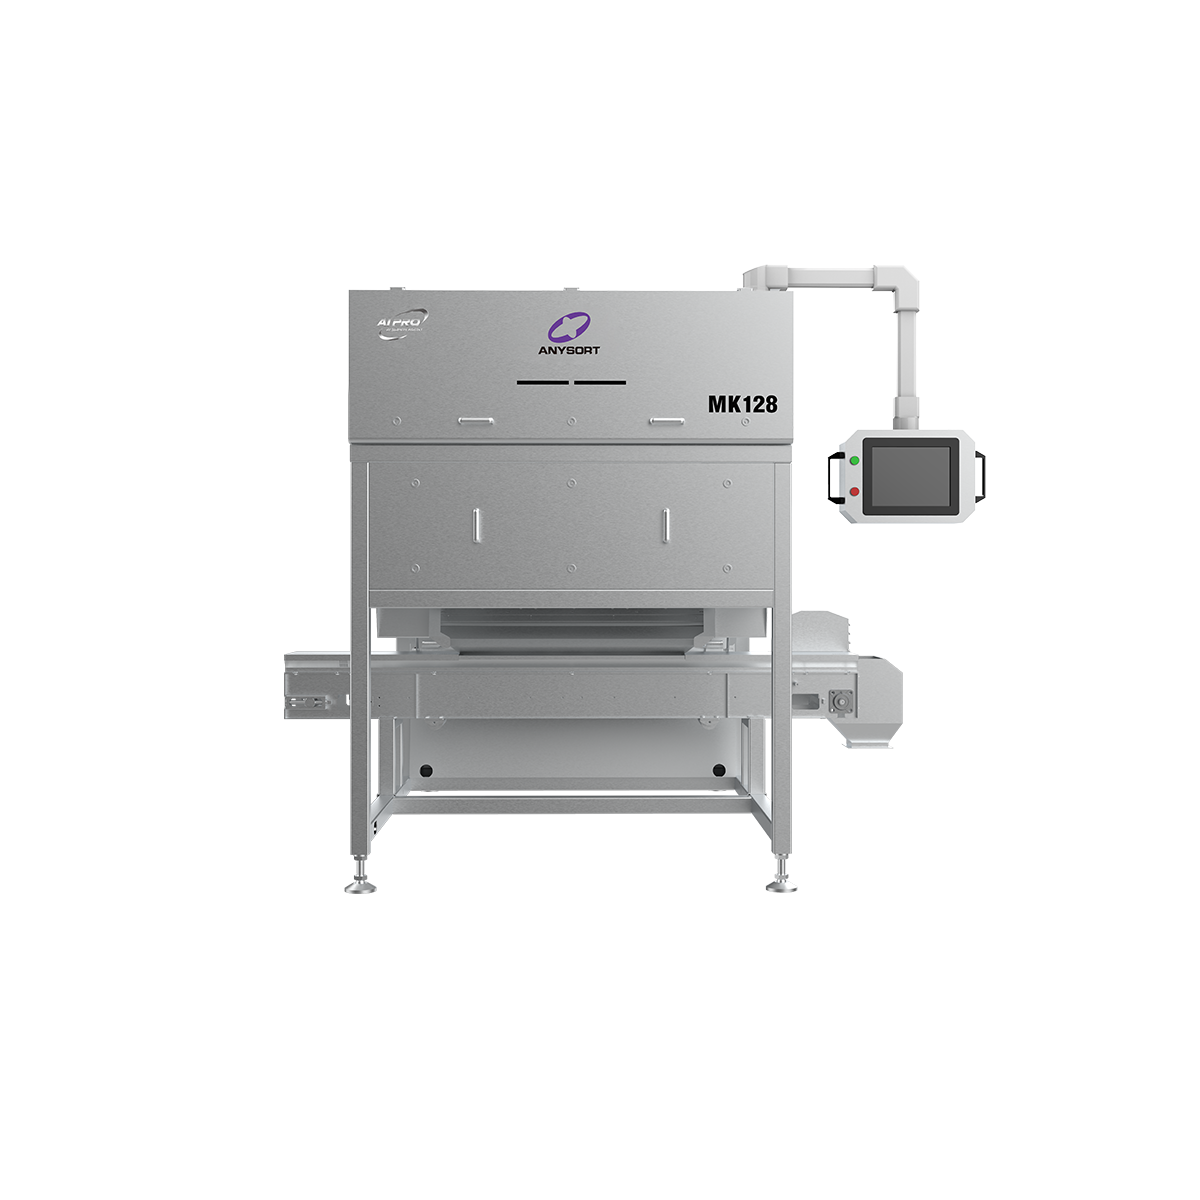
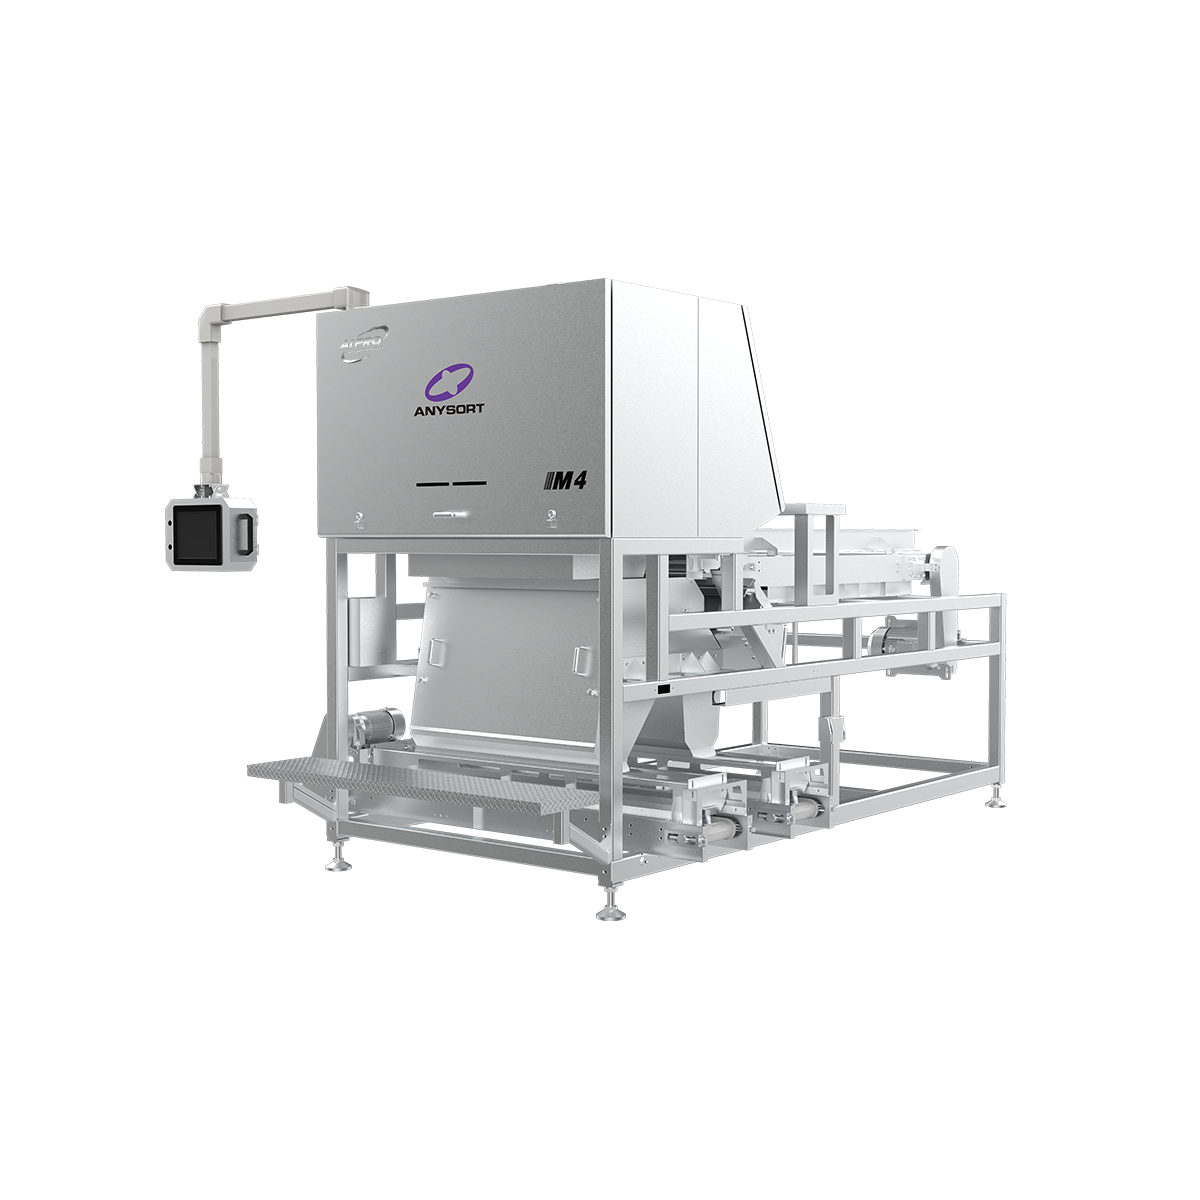
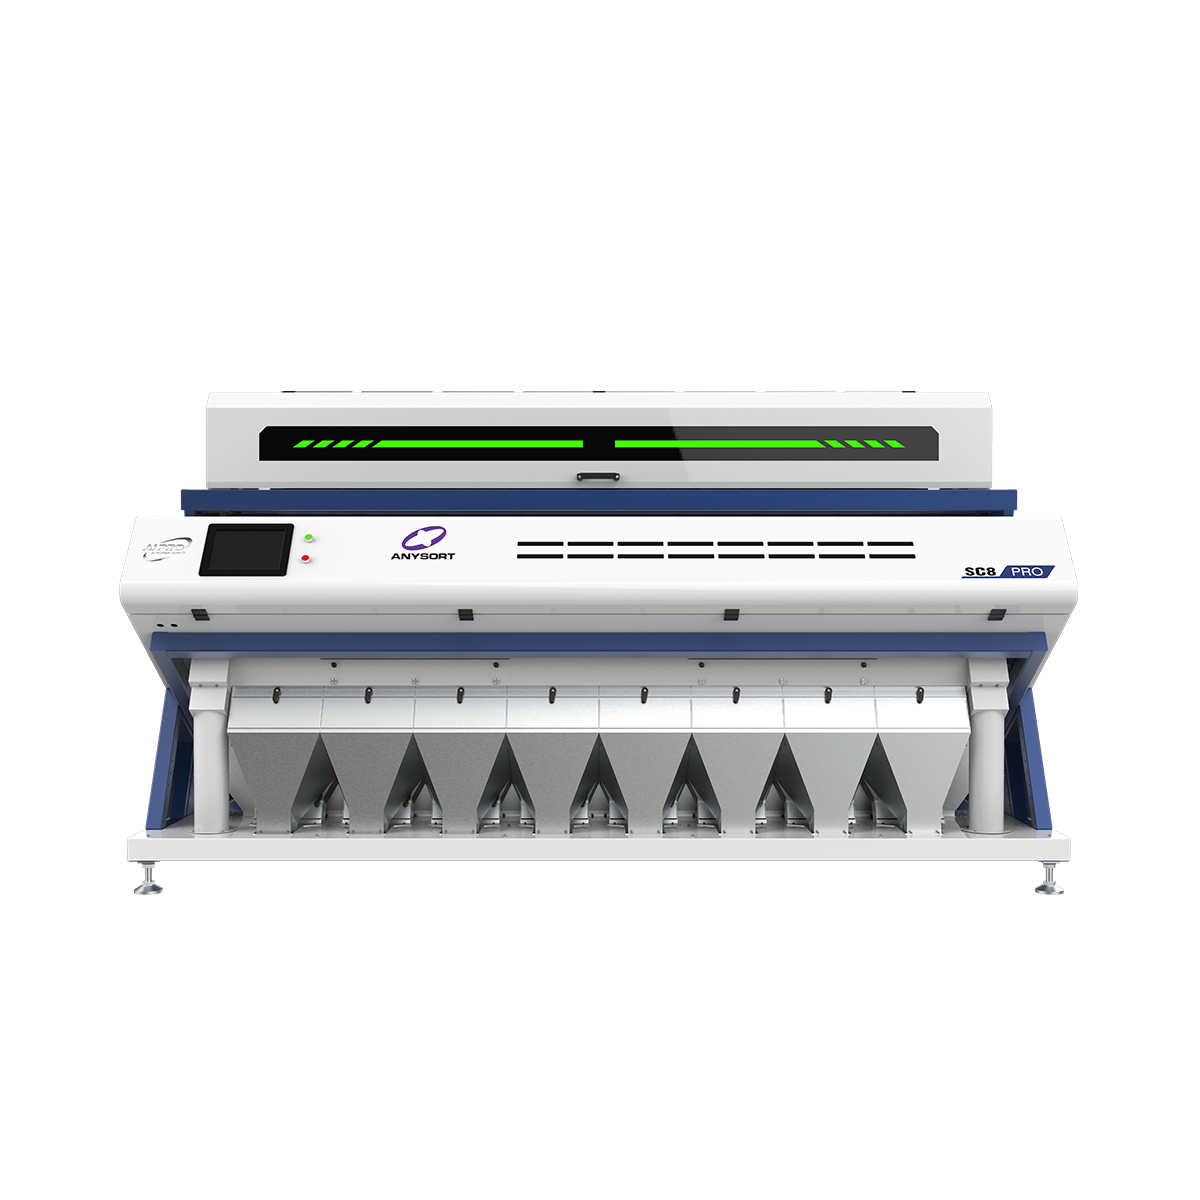
A corn color sorter is an advanced optical sorting machine designed to automatically separate and grade corn kernels based on color, quality, and visual characteristics. This sophisticated equipment uses cutting-edge sensor technology and artificial intelligence to inspect thousands of corn kernels per second, ensuring consistent quality and purity in corn processing operations. The corn color sorter operates by capturing high-resolution images of each kernel as it passes through the sorting chamber, then comparing these images against predefined quality standards to make instantaneous sorting decisions. The machine features multiple ejection channels that direct kernels into different output streams based on their color grade, defects, or contamination levels. Modern corn color sorters can detect and remove discolored kernels, foreign materials, damaged grains, and other impurities with remarkable precision. The technology integrates advanced computer vision systems, high-speed cameras, and pneumatic ejection mechanisms to achieve throughput rates ranging from 1 to 10 tons per hour depending on the model. A corn color sorter is particularly valuable in food processing, animal feed production, and ethanol manufacturing industries where maintaining consistent kernel quality directly impacts end-product performance and profitability. The equipment is built with stainless steel construction for durability and includes user-friendly interfaces that allow operators to adjust sorting parameters easily. By implementing a corn color sorter into production lines, facilities can significantly improve product consistency while reducing manual labor costs and processing waste.

New Product Releases

The primary advantage of investing in a corn color sorter is the dramatic improvement in product quality and consistency that flows directly to your bottom line. This equipment automatically removes discolored, damaged, and contaminated kernels with exceptional accuracy, ensuring your final products meet strict quality specifications every single time. You eliminate the variability associated with manual sorting, which is both time-consuming and prone to human error. A corn color sorter operates continuously at high speeds, processing massive quantities of corn throughout your production day without fatigue or performance degradation. This means you maintain uniform output quality regardless of how many hours your facility operates. The operational efficiency gains are substantial because a corn color sorter reduces the need for manual labor, allowing your team to focus on other critical production tasks. You experience lower waste rates since the machine identifies and separates marginal kernels that might otherwise compromise batch quality, ultimately maximizing your yield and profitability. Installation of a corn color sorter enhances your facility's competitive position by enabling consistent delivery of premium-grade corn products to your customers. The technology is remarkably versatile, working effectively with different corn varieties and processing requirements across multiple industries. Whether you operate a grain trading company, animal feed manufacturer, or food processing facility, a corn color sorter adapts to your specific sorting needs. The reduced labor requirements translate into significant cost savings over time, particularly when you calculate annual wages and training expenses. Most modern corn color sorter units feature intuitive software interfaces that make parameter adjustments straightforward, requiring minimal specialized training for operators. The consistent quality maintenance improves your brand reputation and customer satisfaction, leading to increased repeat business and market loyalty.

Tips And Tricks

How Much Does a Color Sorter Machine Cost?

12

Aug

How Much Does a Color Sorter Machine Cost?

Understanding the investment required for a color sorter machine is essential for businesses in agriculture, food processing, and recycling sectors. The cost of a color sorter machine varies significantly based on capacity, technology sophistication,...
View More
How Does Nuts Sorter Technology Ensure Quality?

19

Aug

How Does Nuts Sorter Technology Ensure Quality?

The global nuts processing industry relies on precision and consistency to meet strict quality standards and regulatory requirements. A nuts sorter has become indispensable for processors seeking to eliminate defects, contaminants, and substandard pr...
View More
How Do Color Sorters Improve Product Quality?

26

Aug

How Do Color Sorters Improve Product Quality?

Product quality stands as a critical differentiator in competitive industrial markets, and achieving consistency at scale requires more than manual oversight. A color sorter represents one of the most effective technologies for identifying and removi...
View More
Which factors should you consider when selecting a rice color sorter?

29

Aug

Which factors should you consider when selecting a rice color sorter?

Selecting the right rice color sorter is a critical decision that directly impacts your grain processing efficiency, product quality, and long-term profitability. A rice color sorter removes discolored, damaged, and foreign particles from rice batche...
View More

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

corn color sorter

Precision Optical Sorting Technology

Precision Optical Sorting Technology

The corn color sorter incorporates state-of-the-art optical sensors and high-resolution camera systems that capture detailed images of each individual kernel in real-time. This advanced technology can detect the most subtle color variations and surface defects that human eyes might miss, ensuring only premium-quality kernels reach your output stream. The corn color sorter uses sophisticated image processing algorithms to analyze kernel characteristics including hue, saturation, and texture, making sorting decisions with exceptional accuracy. The precision of this technology means you can achieve color uniformity levels that were previously impossible with traditional sorting methods. By implementing this optical sorting capability, your facility gains a significant quality control advantage that directly translates to customer satisfaction and product consistency. This precision optical sorting technology in a corn color sorter reduces the likelihood of quality complaints and product returns, protecting your company's reputation in the marketplace.
High-Speed Processing Capacity

High-Speed Processing Capacity

Modern corn color sorter equipment processes thousands of kernels every second, delivering throughput rates that match or exceed manual sorting operations by significant margins. The corn color sorter maintains consistent processing speeds throughout your entire production shift without the performance fluctuations associated with human operators. This high-speed capability means your facility can handle larger volumes of raw corn material while maintaining rigorous quality standards across every batch. The efficient processing speed of a corn color sorter directly reduces your production bottlenecks and allows for flexible scheduling that meets customer delivery deadlines reliably. By choosing a corn color sorter with appropriate capacity for your operation, you maximize your facility's productive potential without requiring additional floor space or complicated infrastructure modifications. The continuous operation capability ensures that your sorting line maintains steady output, reducing idle time and optimizing your overall production efficiency throughout the operational day.
Cost-Effective Waste Reduction

Cost-Effective Waste Reduction

Implementing a corn color sorter substantially reduces material waste throughout your processing operations by identifying and separating marginal-grade kernels before they enter your primary product stream. This waste reduction capability directly improves your profit margins by maximizing usable yield from each batch of raw corn material you process. The corn color sorter identifies impurities and defects early in your production process, preventing low-quality kernels from consuming further processing resources and adding unnecessary costs to your operations. By sorting corn more effectively, a corn color sorter enables you to monetize lower-grade kernels through secondary markets rather than discarding them completely. The efficiency gains translate to lower per-unit processing costs, making your products more competitive in the marketplace while maintaining superior quality standards. Additionally, the automated nature of a corn color sorter eliminates the labor expenses associated with manual sorting, providing rapid return on your investment through sustained operational savings.

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

Copyright © 2026 Anhui Jiexun Optoelectronic Technology Co., Ltd. All rights reserved.  -  Privacy policy