Cashew Color Sorting Machine Suppliers

All Categories

cashew color sorting machine suppliers

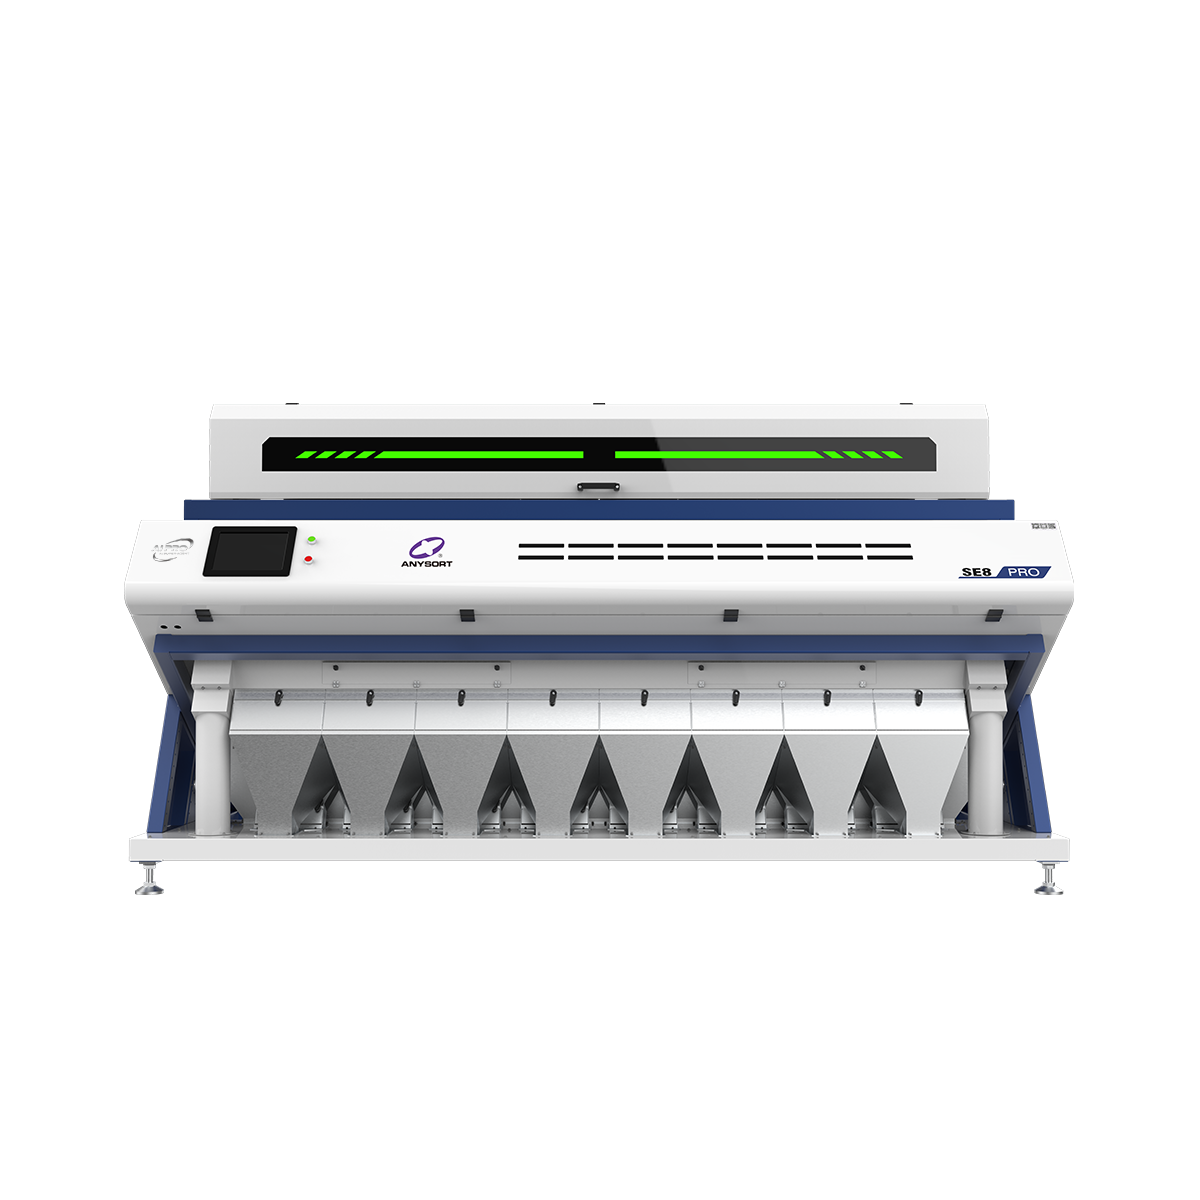
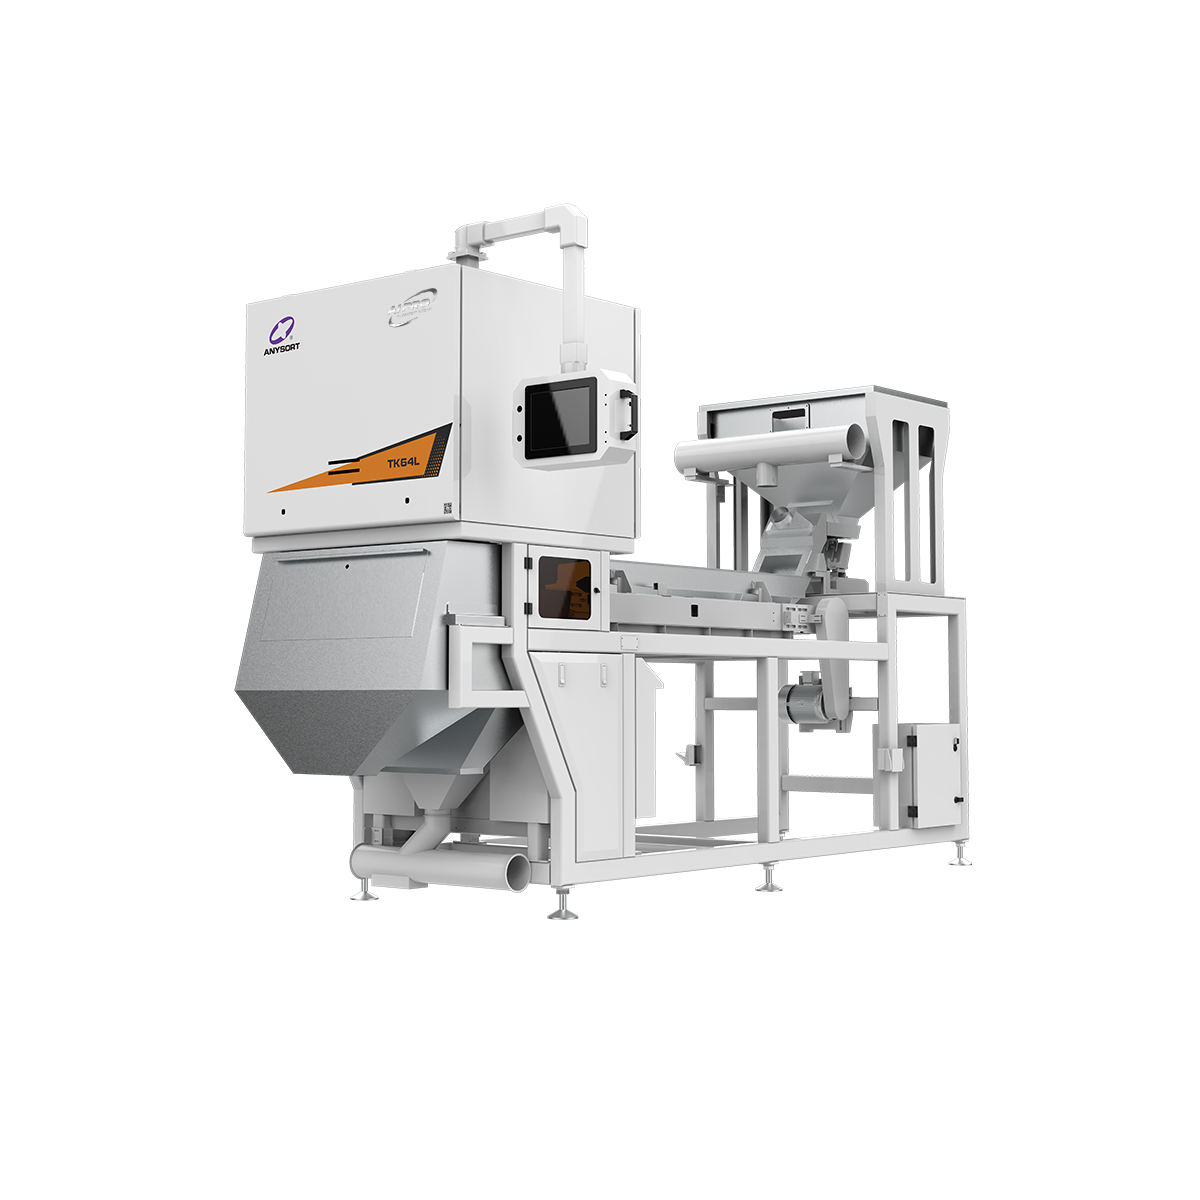
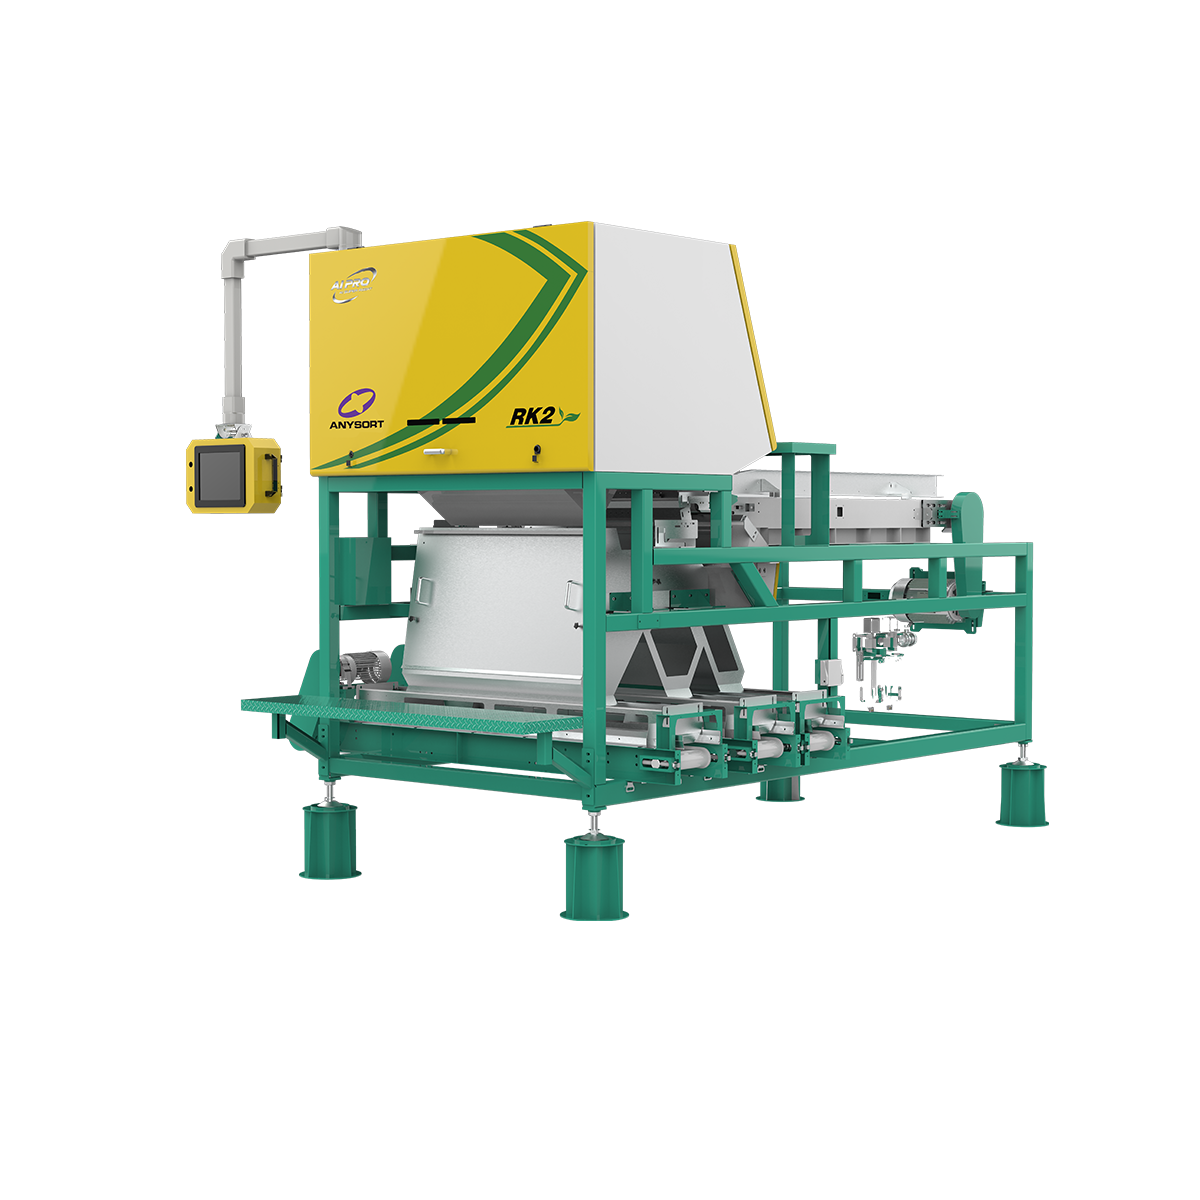
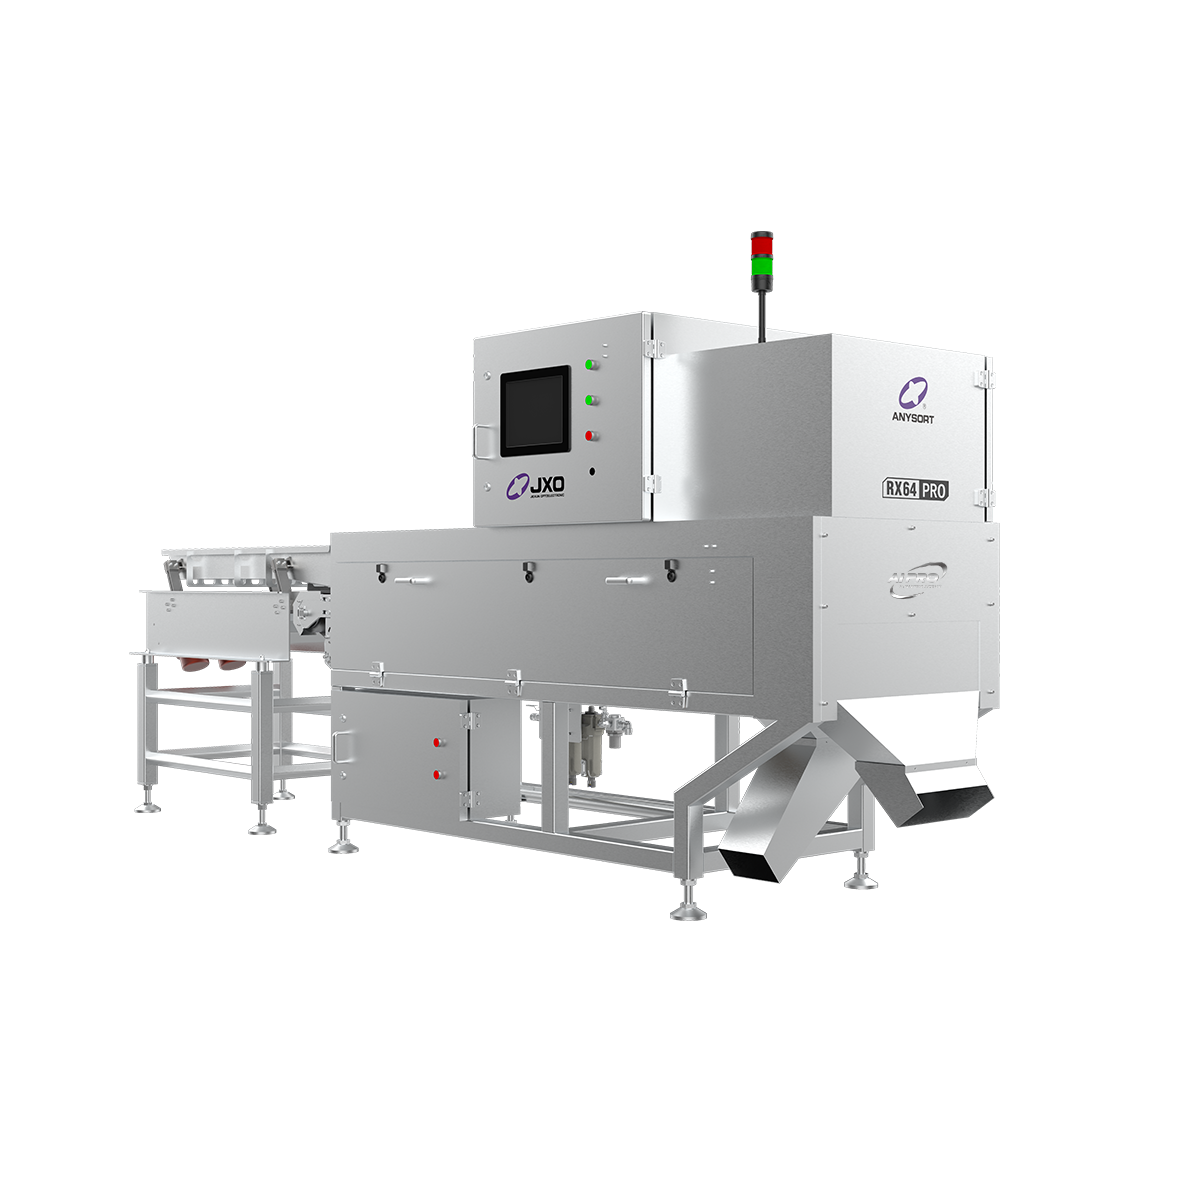
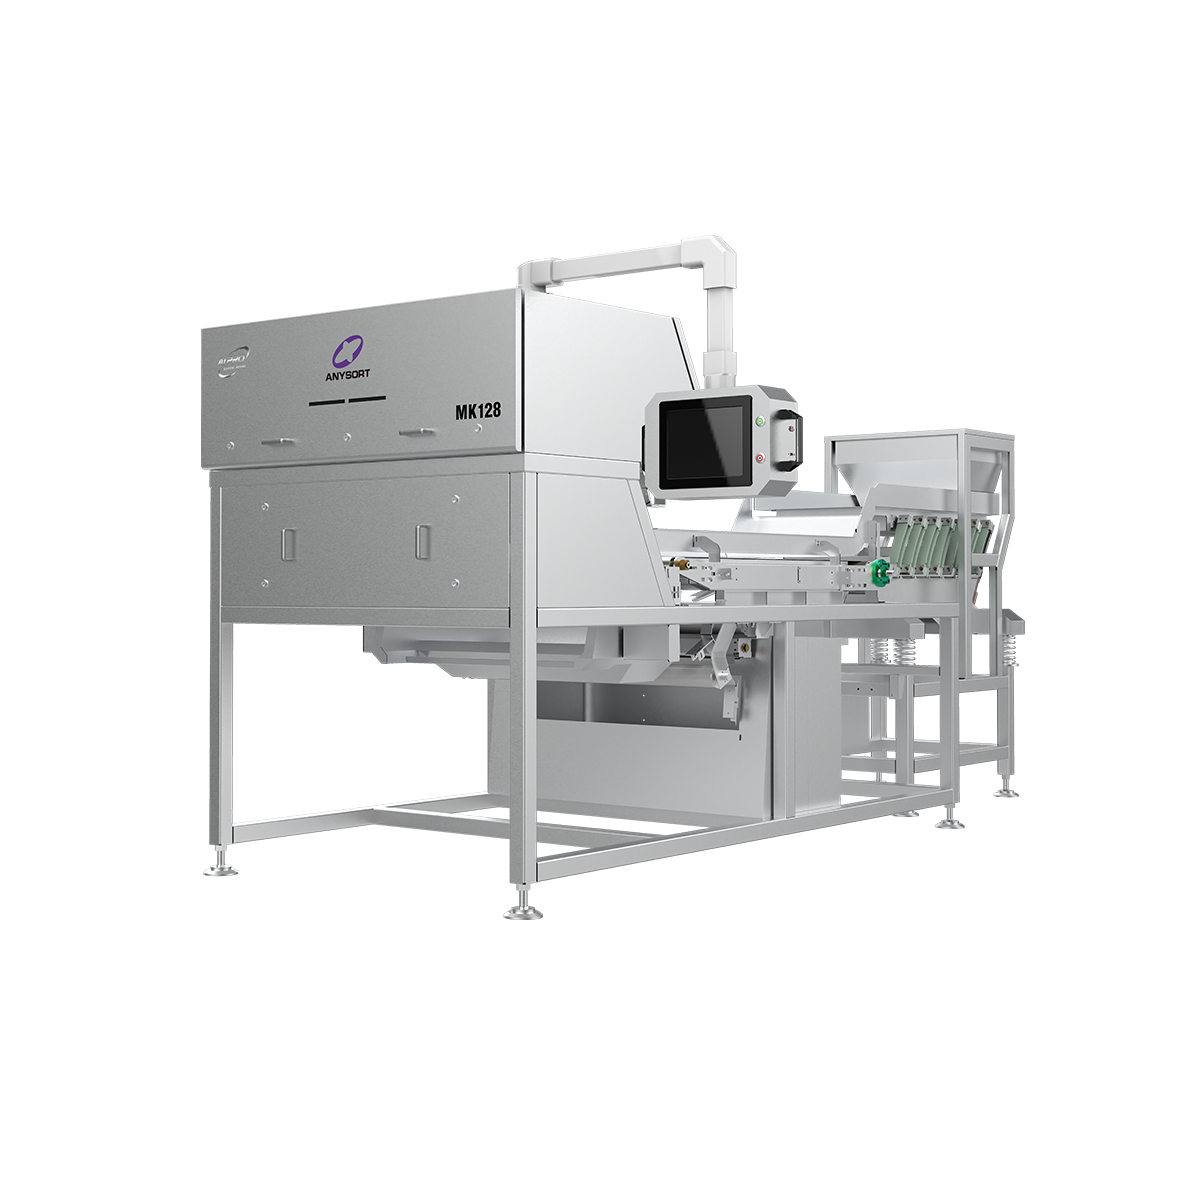
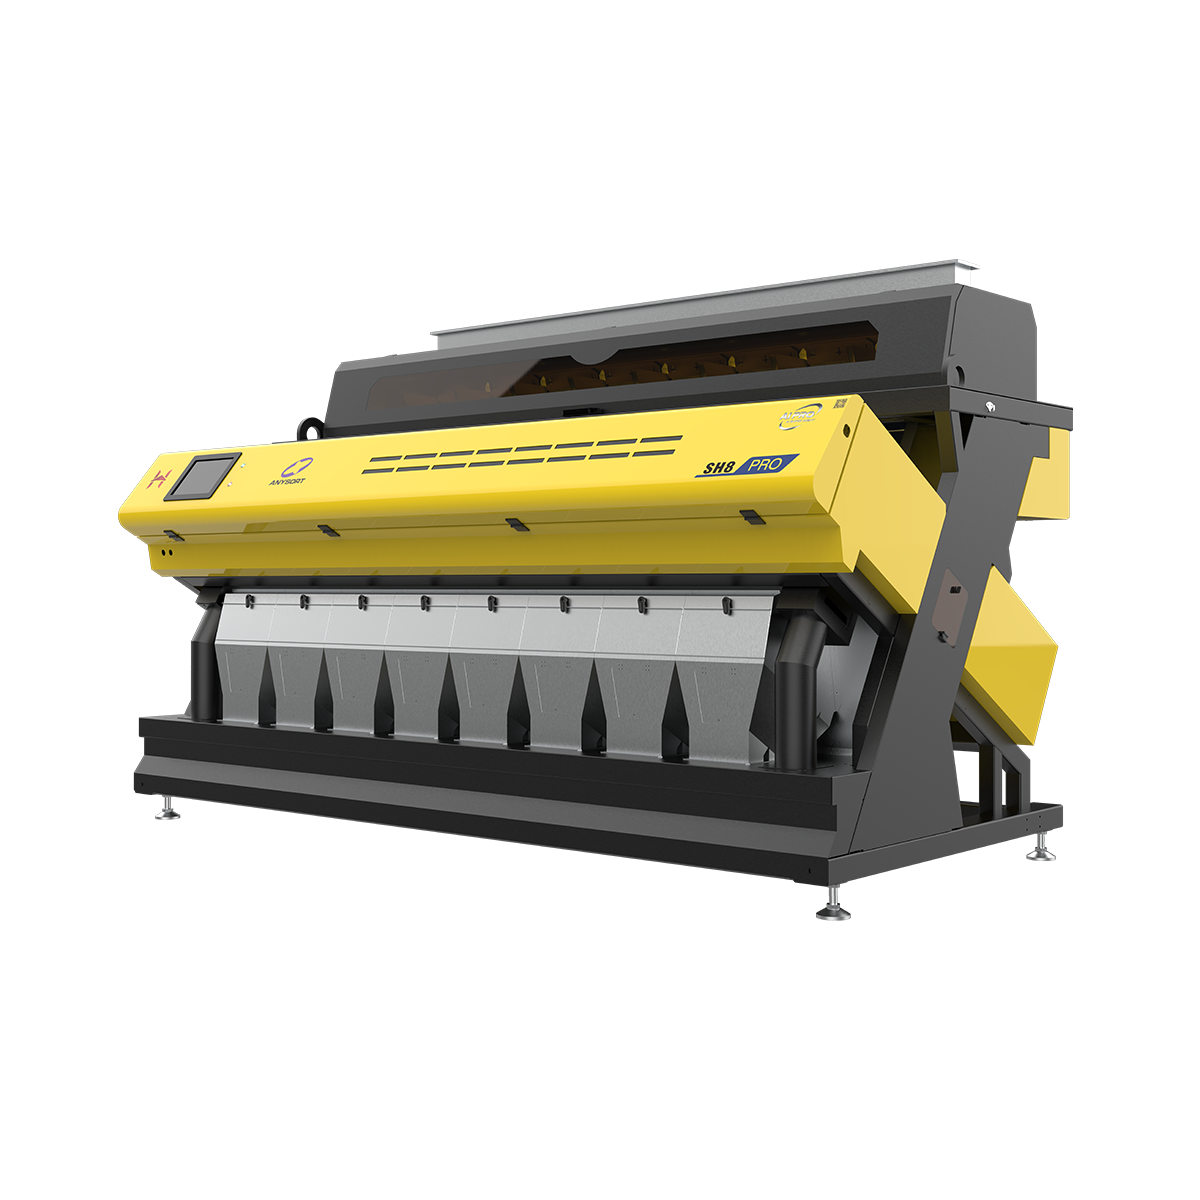
Cashew color sorting machine suppliers provide advanced optical technology solutions designed to enhance nut processing efficiency across the food industry. These specialized machines represent a critical investment for cashew processors seeking to maximize product quality and operational productivity. Cashew color sorting machine suppliers offer equipment that automatically detects and separates nuts based on color variations, defects, and quality parameters with remarkable precision. The primary function involves scanning individual cashews at high speeds, identifying discoloration, blemishes, and foreign materials that compromise final product standards. Leading cashew color sorting machine suppliers integrate multiple technological features including high-resolution cameras, artificial intelligence algorithms, and real-time sorting mechanisms. These systems utilize advanced imaging sensors that capture detailed visual data of each nut, enabling sophisticated analysis and accurate classification. The technology processes thousands of cashews per minute, significantly reducing manual sorting labor while improving consistency. Major cashew color sorting machine suppliers deploy systems with adjustable quality parameters, allowing operators to customize sorting criteria based on specific market requirements and quality standards. Applications span from small-scale processing facilities to large industrial operations, making cashew color sorting machine suppliers essential partners for businesses of all sizes. The equipment excels in removing damaged, discolored, or undersized cashews, ensuring only premium-grade nuts reach consumer markets. Reputable cashew color sorting machine suppliers provide comprehensive support, including installation, training, maintenance, and technical assistance. Their solutions directly address industry challenges related to labor costs, product consistency, and waste reduction. By partnering with established cashew color sorting machine suppliers, processors gain competitive advantages through enhanced efficiency and superior product quality standards.

New Product Recommendations

Selecting reliable cashew color sorting machine suppliers delivers transformative operational advantages that directly impact profitability and market competitiveness. First, these suppliers offer remarkable labor cost reduction by automating the sorting process that traditionally required extensive manual workforce involvement. Processing facilities experience immediate productivity gains through faster sorting speeds and continuous 24/7 operational capability that human workers cannot match. Cashew color sorting machine suppliers provide equipment delivering exceptional sorting accuracy, eliminating human error and ensuring consistent quality standards across all batches. This precision results in higher market values for sorted cashews, as premium-grade nuts command superior prices in competitive markets. The technology minimizes waste by identifying salvageable nuts and channeling only truly defective products away from premium sorting streams. Operational benefits extend to workforce flexibility, allowing employees to transition toward quality control, maintenance, and other value-added tasks requiring human expertise. Customers working with cashew color sorting machine suppliers enjoy reduced product returns and customer complaints through improved quality assurance. The systems adapt effortlessly to changing market demands and quality specifications without expensive equipment modifications. Environmental advantages emerge through optimized resource utilization and reduced processing waste. Cashew color sorting machine suppliers typically include comprehensive training programs ensuring staff proficiency and maximum equipment performance. Integration with existing facility infrastructure proves straightforward, minimizing production disruption during installation phases. Maintenance requirements remain minimal compared to traditional sorting equipment, reducing downtime and associated costs. The investment justifies itself rapidly through improved product yields and reduced operational expenses. Long-term partnerships with cashew color sorting machine suppliers provide ongoing technological improvements and upgrades. Processors gain enhanced traceability and quality documentation capabilities supporting regulatory compliance and customer transparency requirements. These practical benefits position cashew color sorting machine suppliers as essential strategic partners for modern food processing operations.

Latest News

What Factors Affect Tea Color Sorter Performance and Accuracy?

05

Aug

What Factors Affect Tea Color Sorter Performance and Accuracy?

The precision of a tea color sorter directly determines the quality consistency of finished tea products. Understanding the factors that influence tea color sorter performance and accuracy is essential for tea processors seeking to maintain competiti...
View More
How to Choose the Right Tea Color Sorter for Your Needs?

01

Aug

How to Choose the Right Tea Color Sorter for Your Needs?

Selecting the right tea color sorter is one of the most critical decisions tea processors face when modernizing their operations. A tea color sorter directly impacts product quality, operational efficiency, and market competitiveness. The wrong choic...
View More
How Much Does a Color Sorter Machine Cost?

12

Aug

How Much Does a Color Sorter Machine Cost?

Understanding the investment required for a color sorter machine is essential for businesses in agriculture, food processing, and recycling sectors. The cost of a color sorter machine varies significantly based on capacity, technology sophistication,...
View More
How Can a Nuts Sorter Improve Your Production?

15

Aug

How Can a Nuts Sorter Improve Your Production?

A nuts sorter represents one of the most significant investments a food processing operation can make to enhance production quality and operational efficiency. The modern nuts sorter uses advanced imaging and sensor technology to identify and separat...
View More

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

cashew color sorting machine suppliers

Advanced Optical Detection Technology

Advanced Optical Detection Technology

Leading cashew color sorting machine suppliers integrate state-of-the-art optical detection systems utilizing high-resolution cameras and sophisticated imaging algorithms. This technology captures detailed visual information from multiple angles, enabling precise identification of color variations, surface blemishes, defects, and discoloration invisible to human inspectors. The optical sensors work in milliseconds, processing each cashew's complete visual profile before making instantaneous sorting decisions. Cashew color sorting machine suppliers employing this technology achieve sorting accuracy exceeding 99 percent, significantly surpassing manual methods. The systems automatically adapt to varying lighting conditions and background environments, ensuring consistent performance across different operational settings. Advanced calibration features allow operators to fine-tune detection sensitivity for specific quality grades and market requirements. The technology distinguishes between minor surface marks and serious defects, preserving borderline-quality nuts while confidently removing unsuitable products. Premium cashew color sorting machine suppliers continuously upgrade their optical systems with cutting-edge innovations, maintaining technological leadership in nut processing automation.
High-Speed Processing Capacity

High-Speed Processing Capacity

Cashew color sorting machine suppliers deliver impressive throughput capabilities, processing thousands of individual nuts per minute without compromising accuracy or quality standards. Modern sorting systems from leading cashew color sorting machine suppliers handle output volumes reaching 5,000 to 10,000 nuts per minute, dramatically increasing facility productivity. This exceptional speed eliminates production bottlenecks and allows processors to handle larger volumes without expanding physical infrastructure investments. The continuous conveyor systems employed by cashew color sorting machine suppliers maintain steady nut flow while ensuring adequate processing time for reliable quality assessment. High-speed capabilities enable extended shift operations and fulfill demanding wholesale market orders efficiently. The systems maintain consistent performance throughout entire production runs, never experiencing fatigue-related accuracy degradation affecting manual sorting operations. Cashew color sorting machine suppliers design their equipment specifically for industrial-scale applications, accommodating both peak season demands and variable processing requirements. The technology scales seamlessly, adapting to facility expansion plans without requiring complete system replacement. Speed advantages translate directly into competitive market positioning and enhanced profitability metrics.
Comprehensive Support and Customization Options

Comprehensive Support and Customization Options

Reputable cashew color sorting machine suppliers distinguish themselves through exceptional customer support and flexible customization capabilities addressing unique processing requirements. These suppliers provide comprehensive installation services, professional training programs, and ongoing technical maintenance ensuring optimal equipment performance throughout operational lifespan. Cashew color sorting machine suppliers offer adjustable sorting parameters, allowing facilities to modify quality thresholds and classification criteria without hardware modifications. Customization extends to physical equipment dimensions, integration features with existing facility infrastructure, and specialized sorting capabilities for unique cashew varieties or market specifications. Technical support teams from leading cashew color sorting machine suppliers provide rapid response to operational issues, minimizing production disruptions and maintaining workflow continuity. Training programs cover equipment operation, maintenance procedures, troubleshooting techniques, and advanced feature utilization. Cashew color sorting machine suppliers increasingly offer software updates and artificial intelligence improvements remotely, continuously enhancing system capabilities without facility visits.

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

Copyright © 2026 Anhui Jiexun Optoelectronic Technology Co., Ltd. All rights reserved.  -  Privacy policy