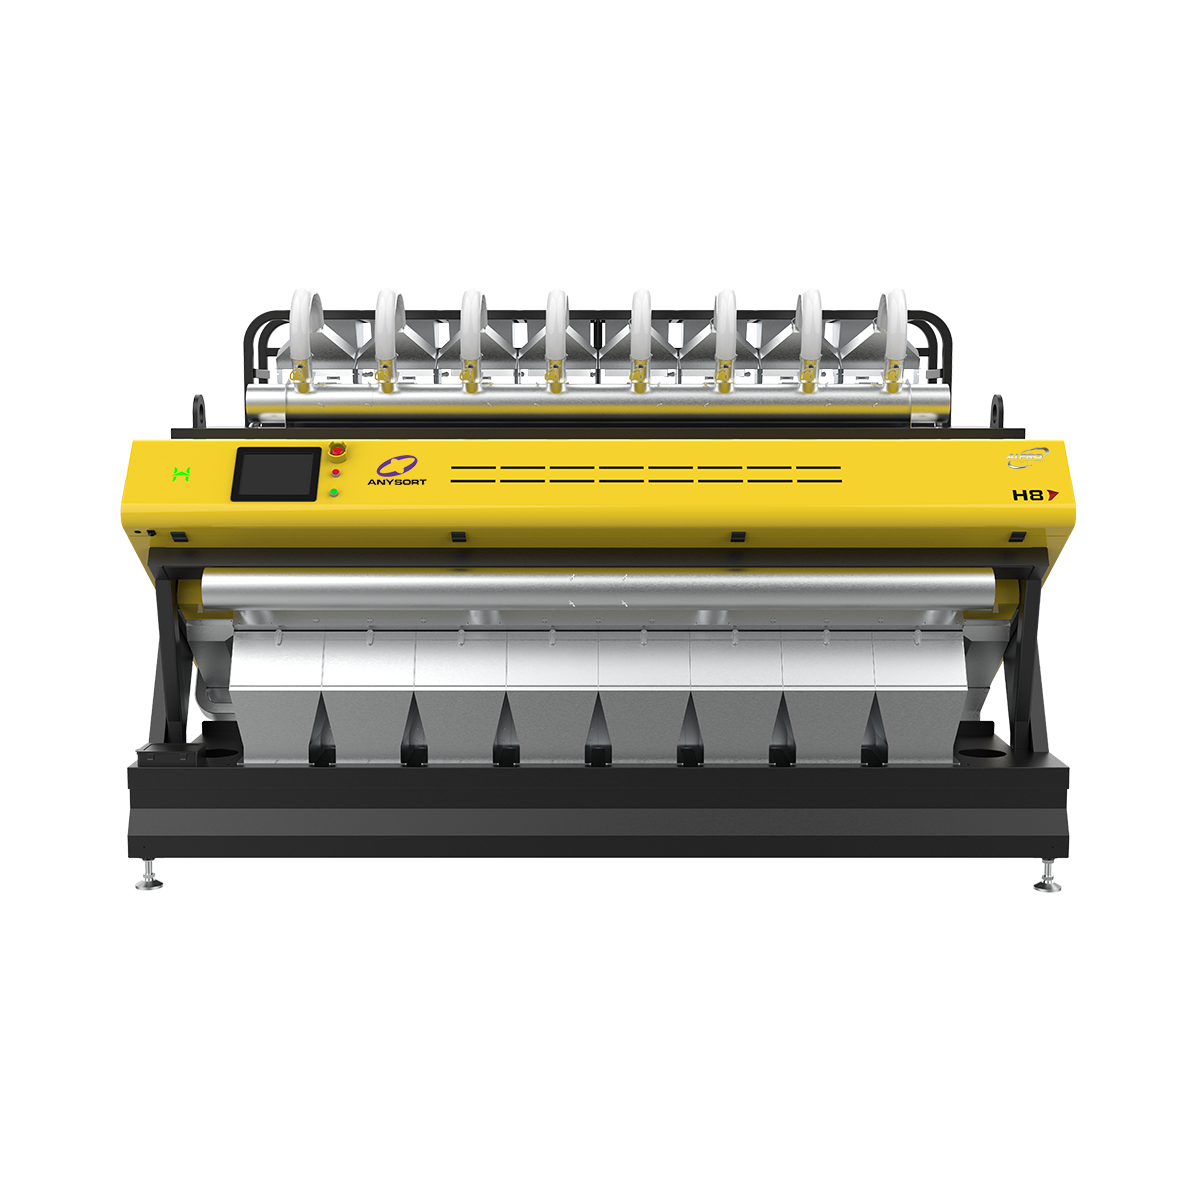
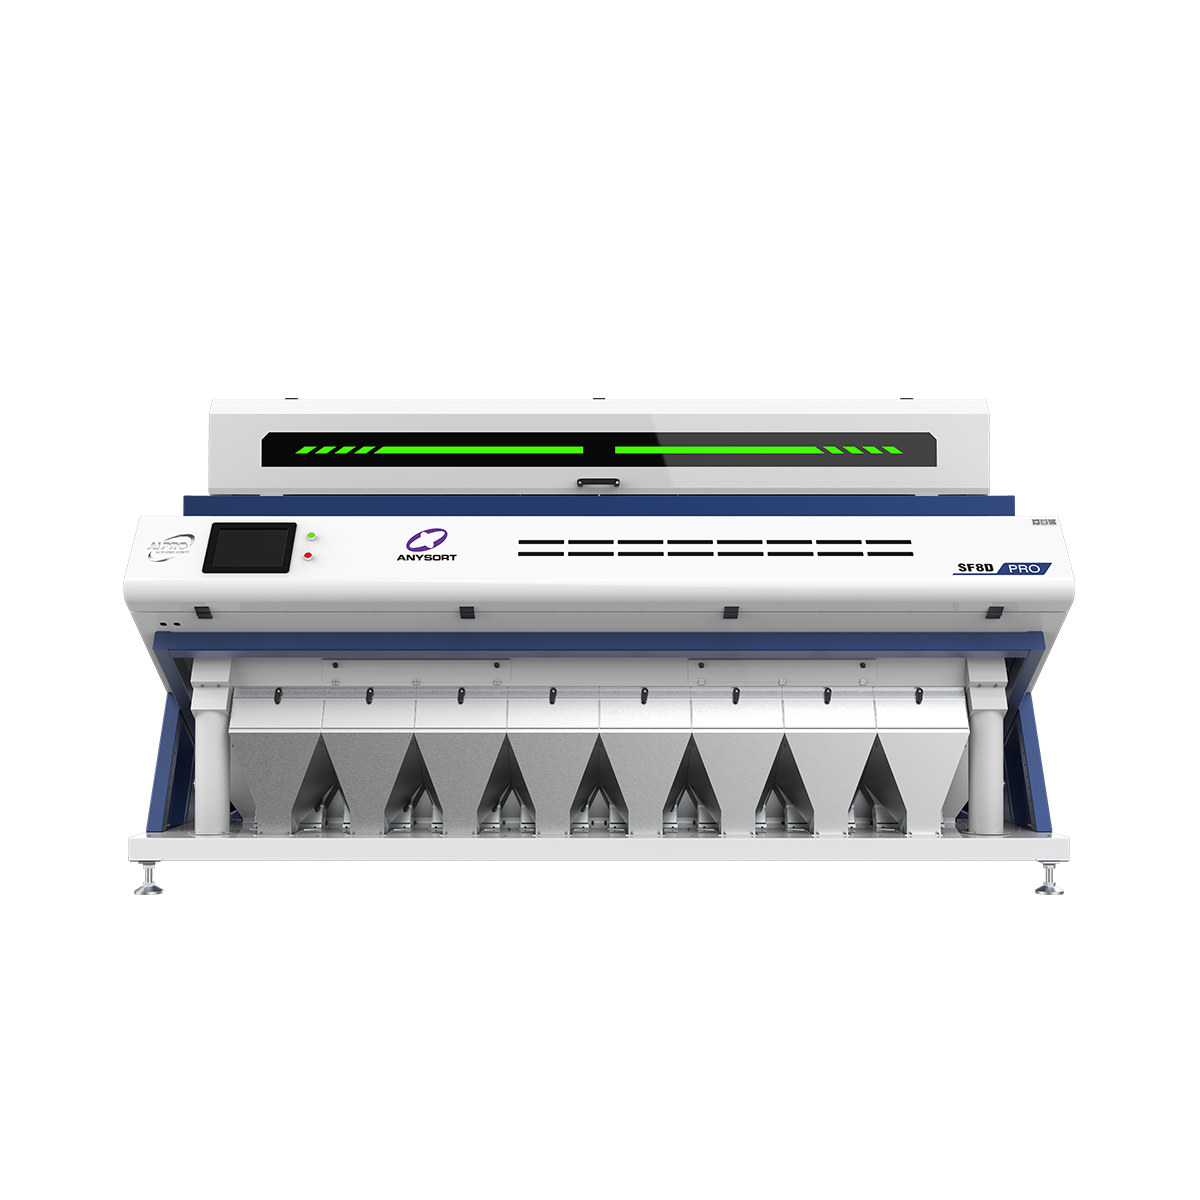
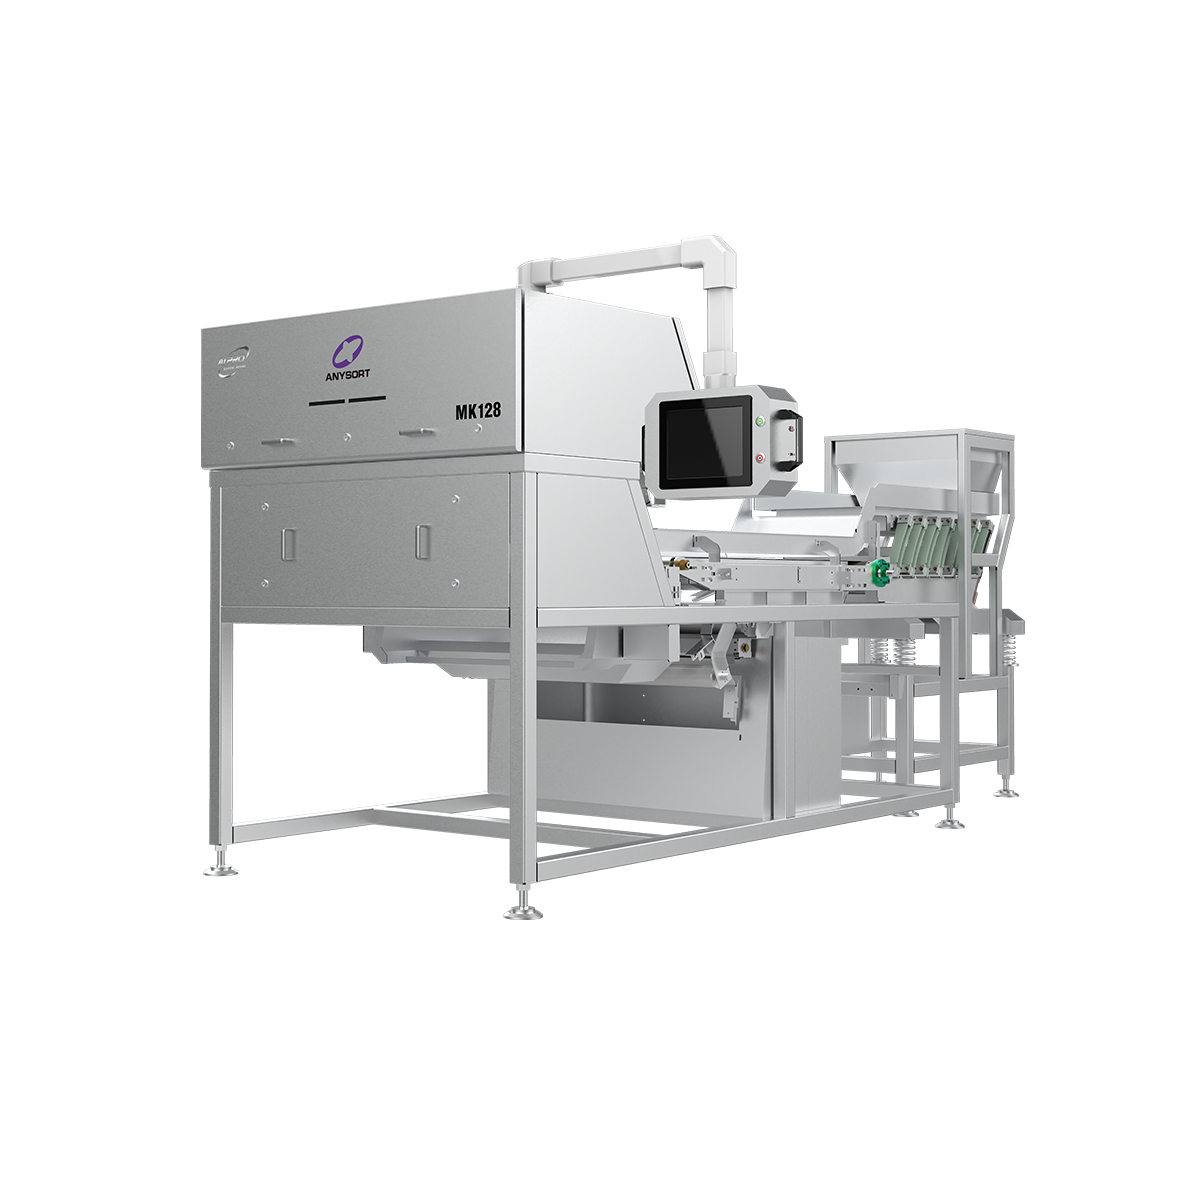
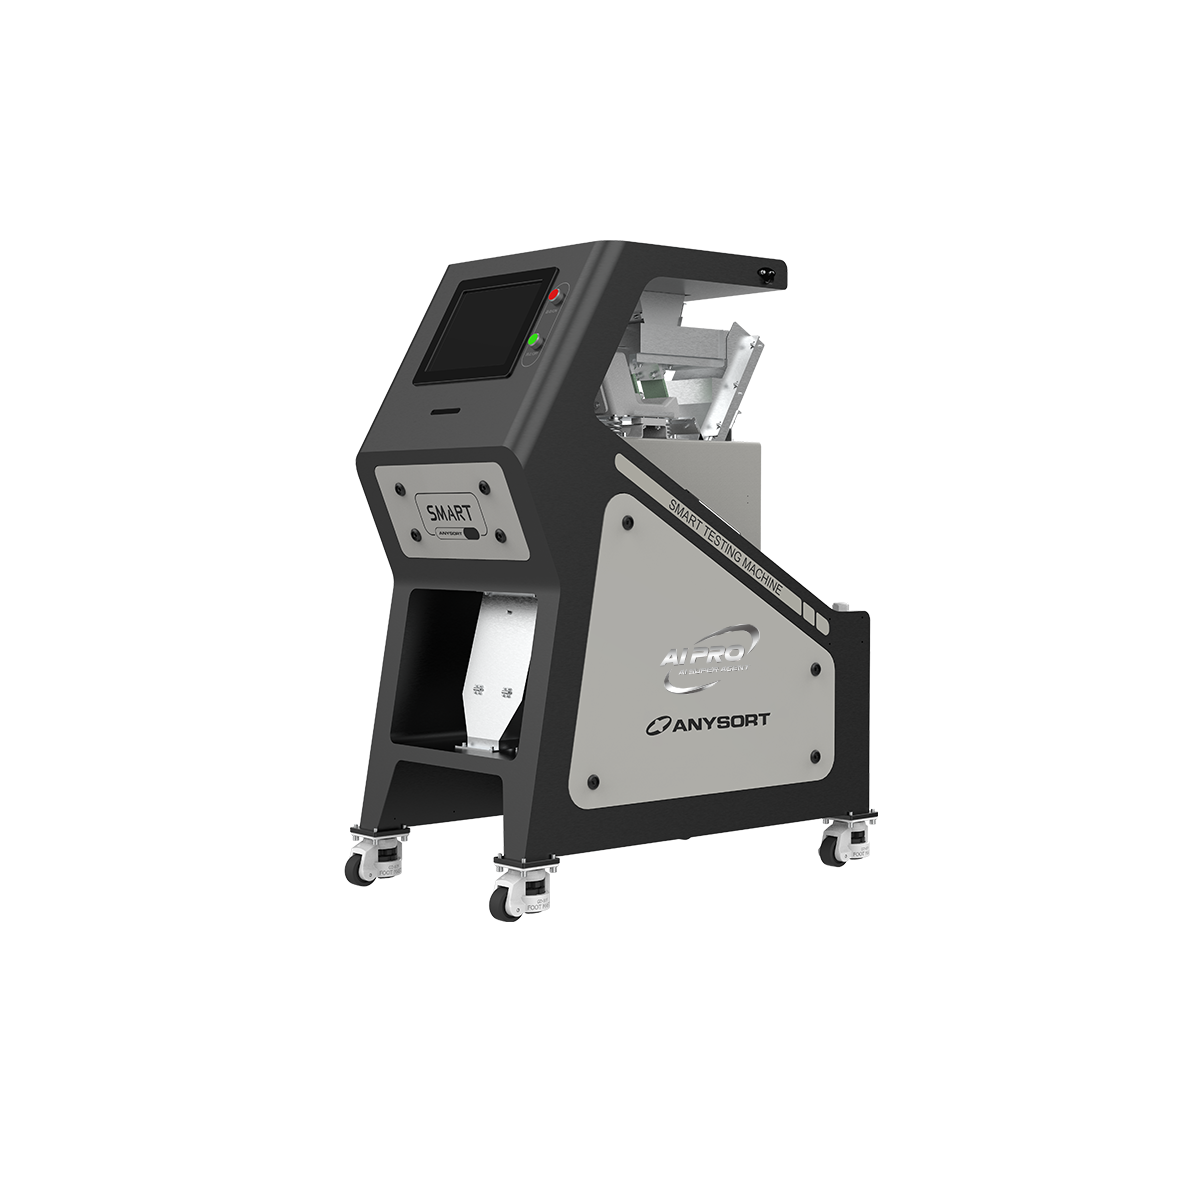
cashew color sorter machine factory
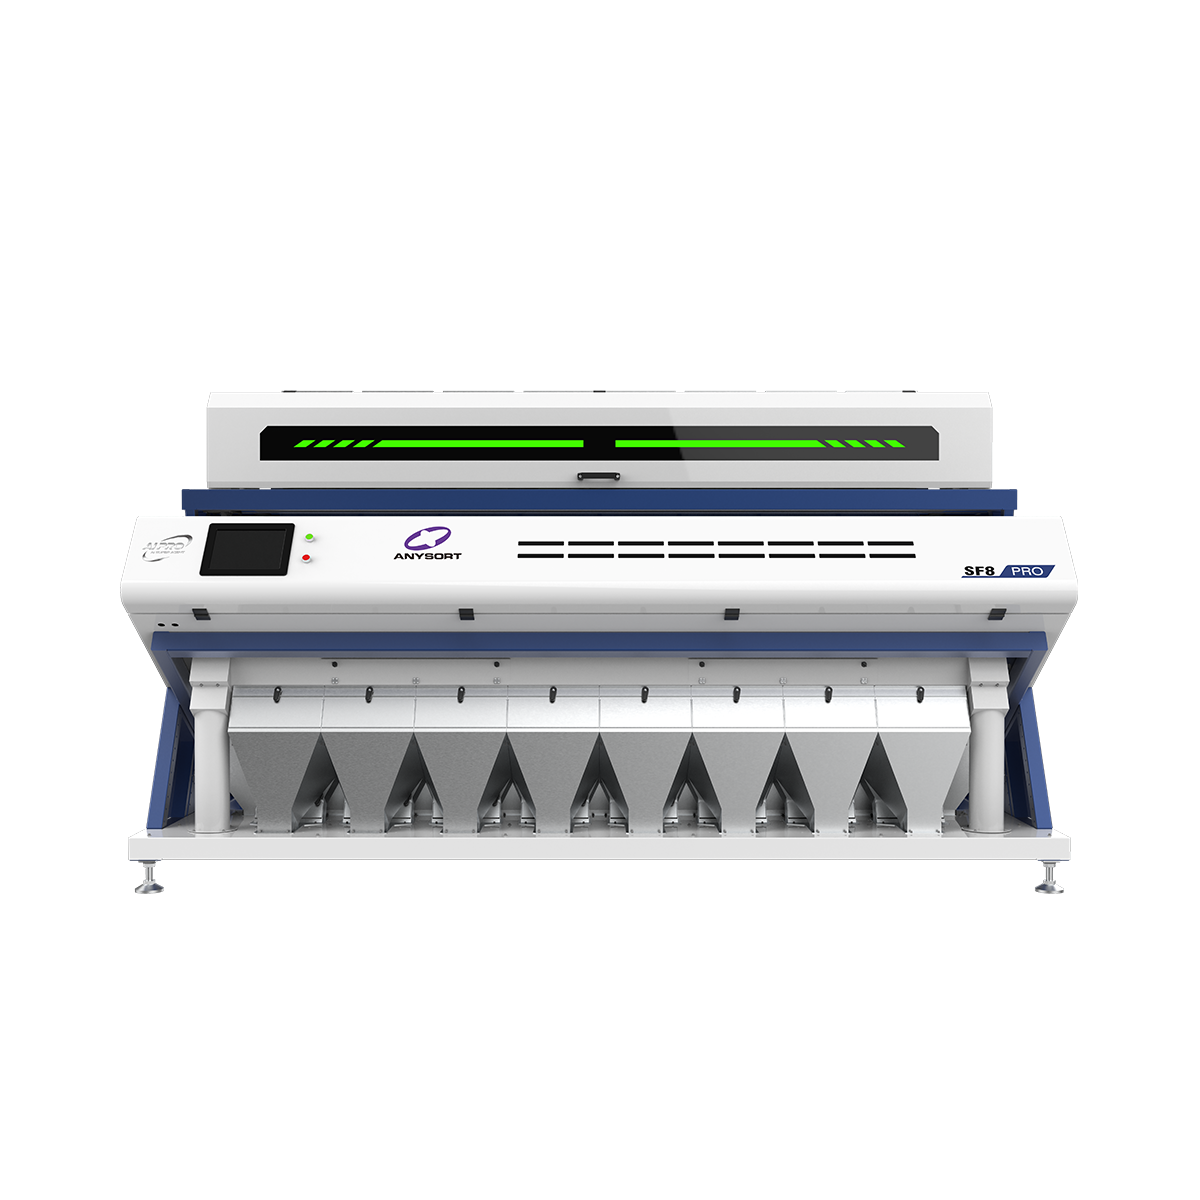
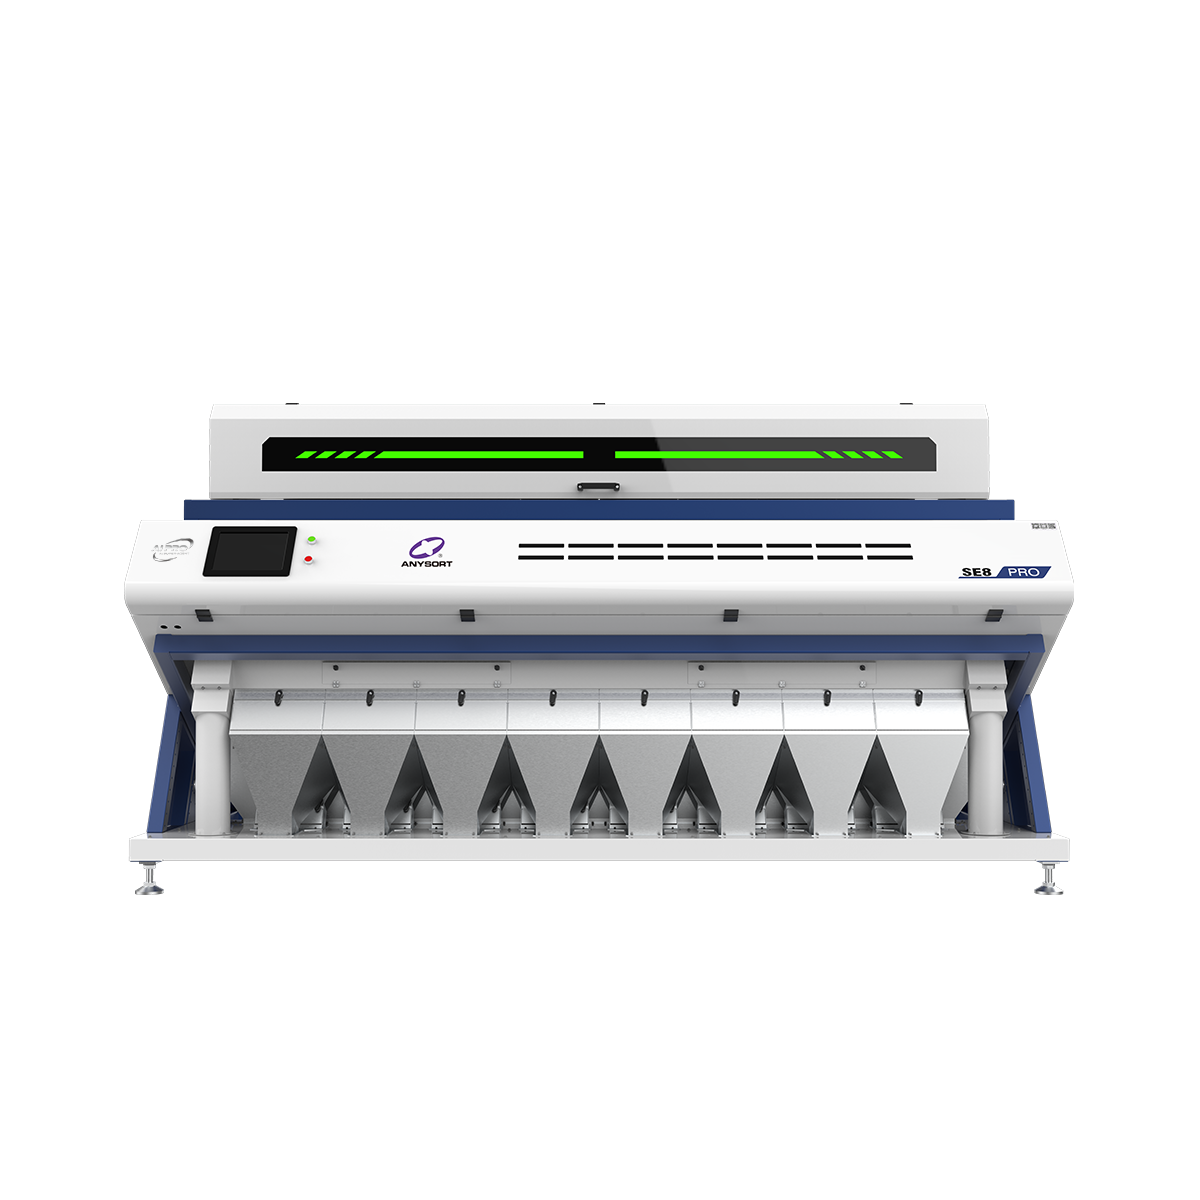
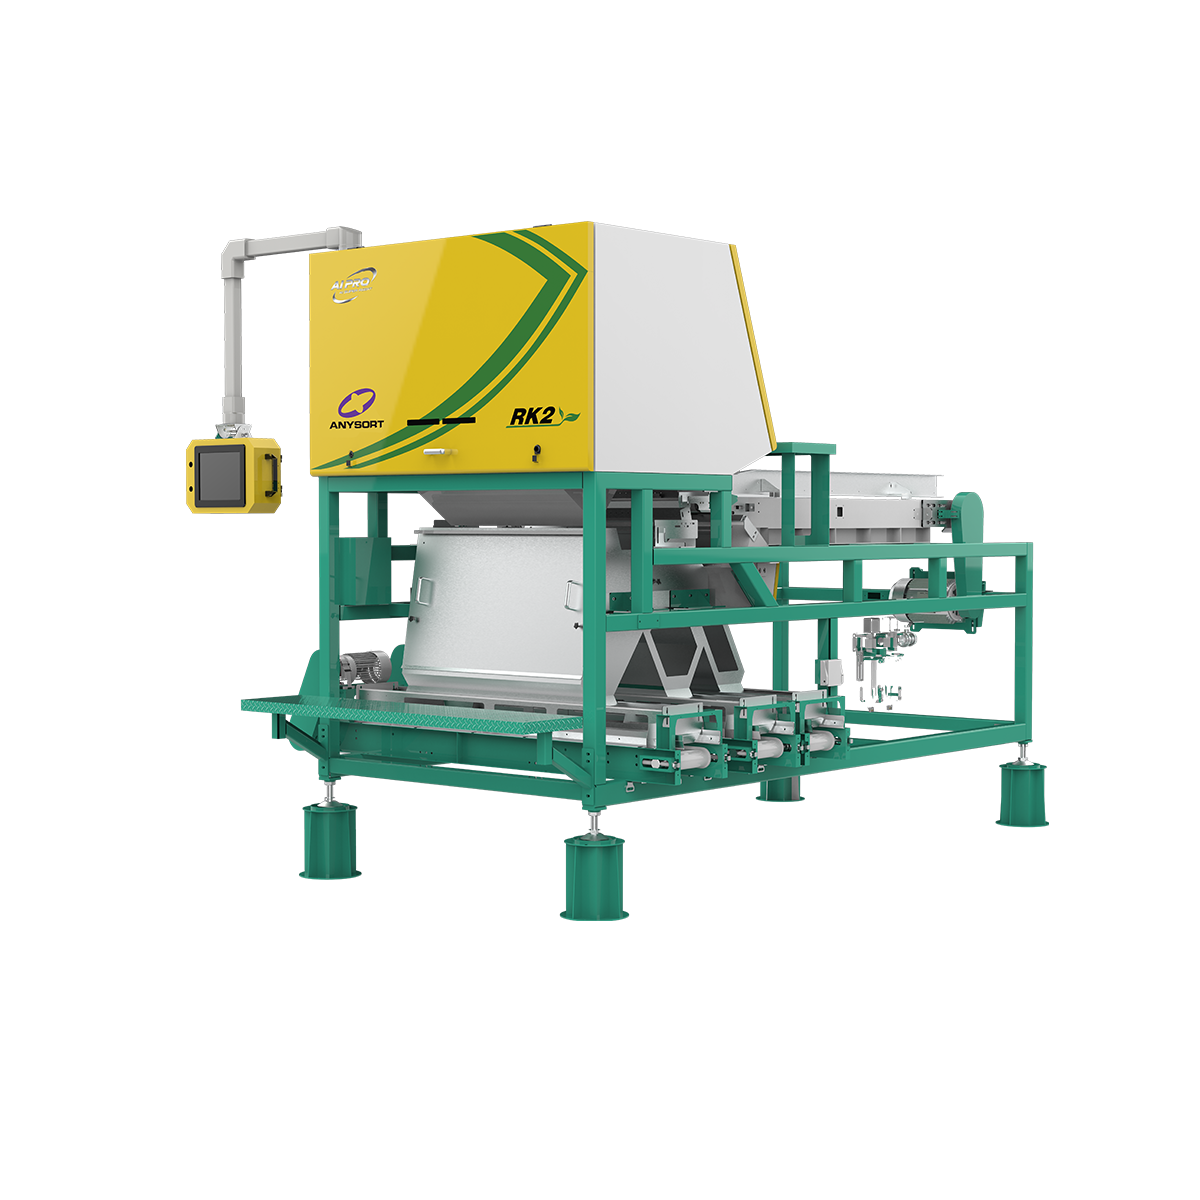
A cashew color sorter machine factory specializes in manufacturing advanced optical sorting equipment designed to separate and grade cashew nuts based on color, quality, and size. These sophisticated machines utilize cutting-edge vision technology and artificial intelligence to inspect thousands of cashew kernels per minute with exceptional accuracy. The cashew color sorter machine factory produces equipment that identifies defects, discoloration, and foreign materials that human sorters might miss, ensuring only premium-grade cashews reach the market. Modern cashew color sorter machine factory operations integrate high-resolution cameras, LED lighting systems, and intelligent algorithms to achieve precise color differentiation across multiple shade variations. The machines feature adjustable sorting parameters that accommodate different cashew varieties and customer specifications. A professional cashew color sorter machine factory combines hardware engineering with software development to deliver reliable performance in industrial processing environments. These systems reduce labor costs significantly while improving product consistency and market competitiveness. The cashew color sorter machine factory technology has become essential for cashew processors worldwide, transforming raw nuts into consistently graded products that command premium prices. Advanced models process up to 5,000 kilograms hourly while maintaining accuracy rates exceeding ninety-eight percent, making them indispensable in modern cashew processing facilities.

 EN