Multi Grain Sorting Machine | Precision Grain Processing

All Categories

multi grain sorting machine

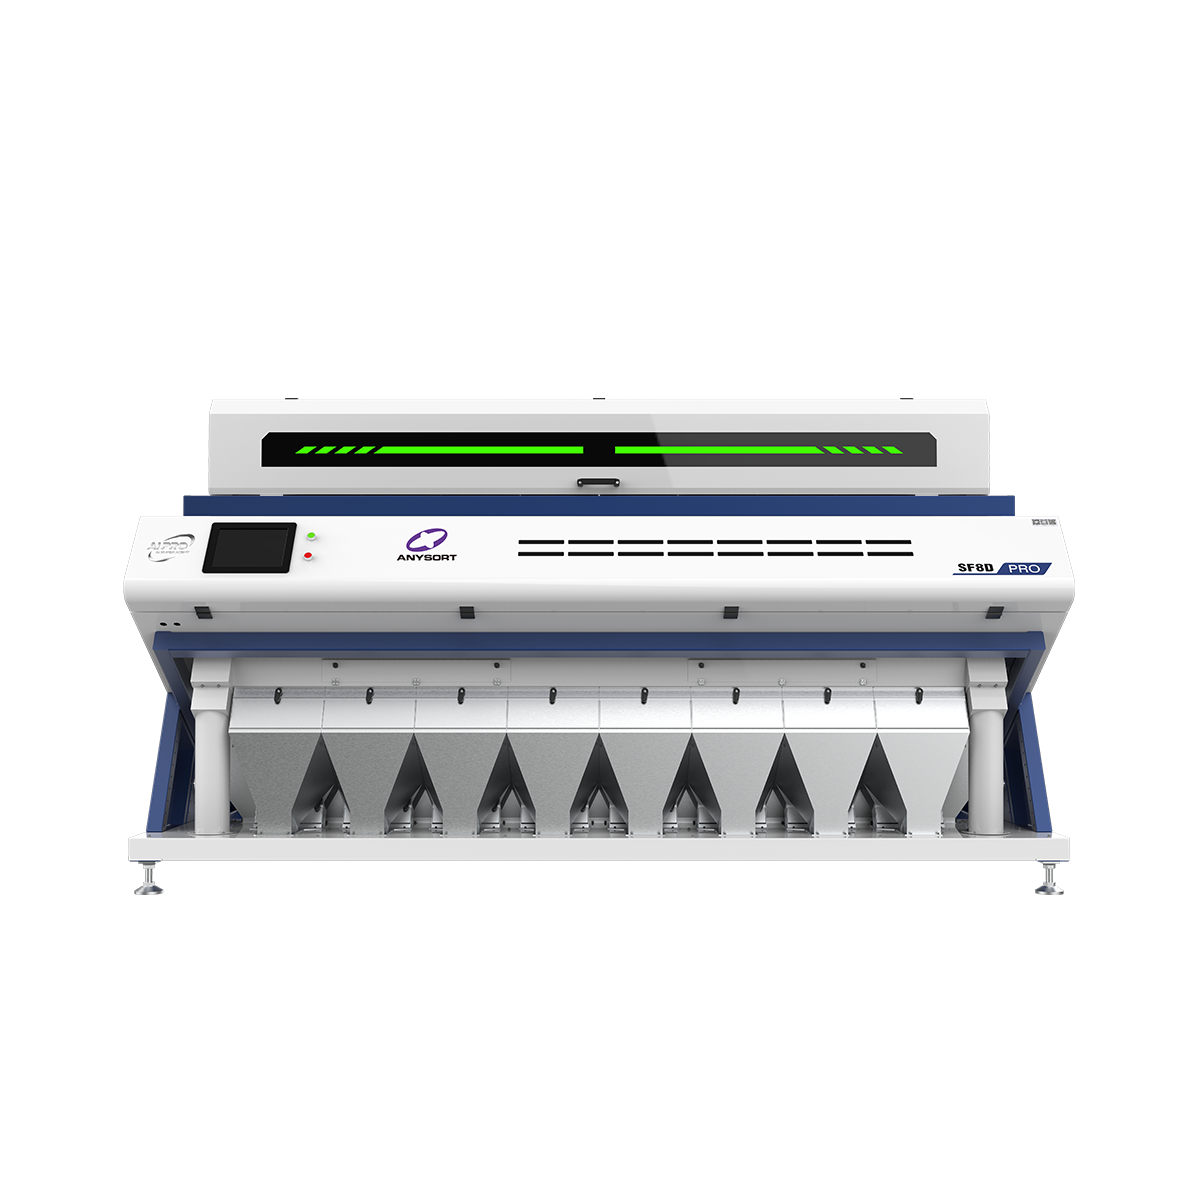
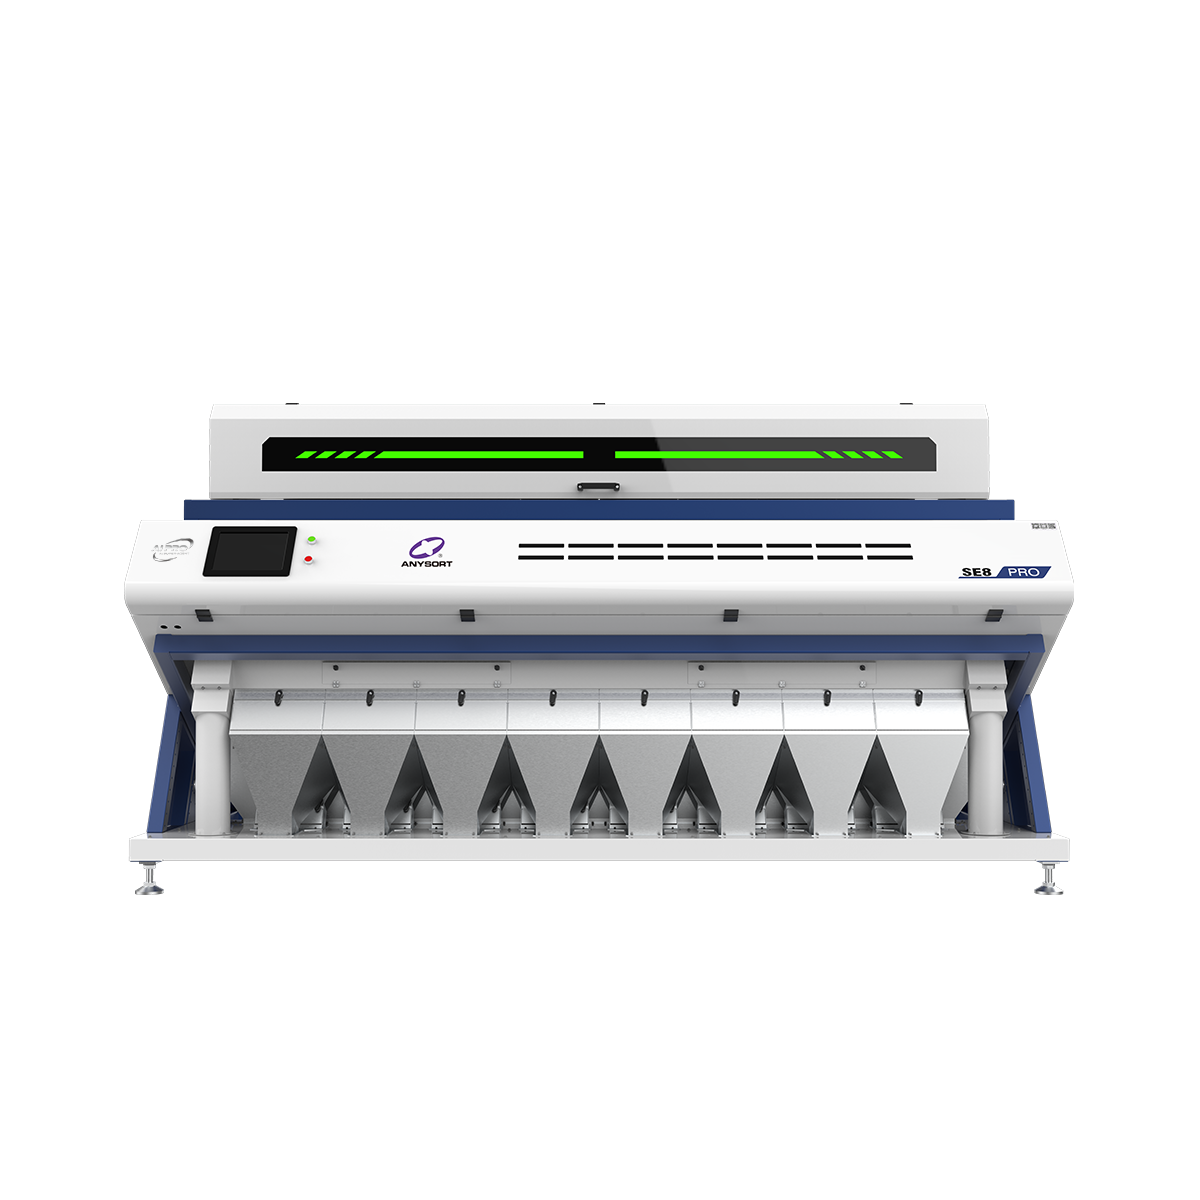
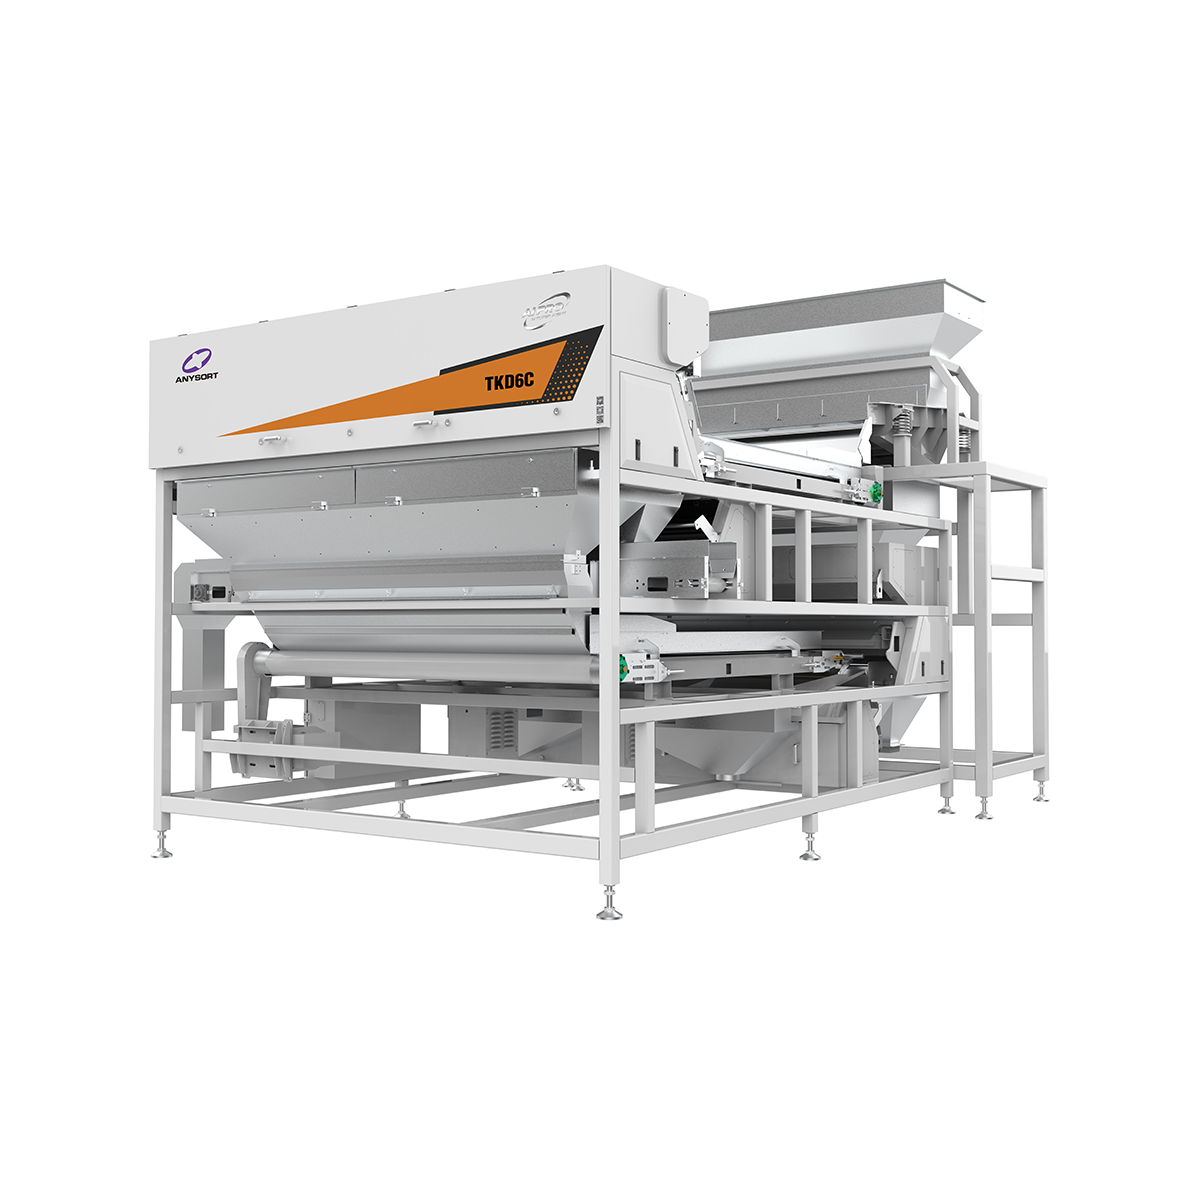
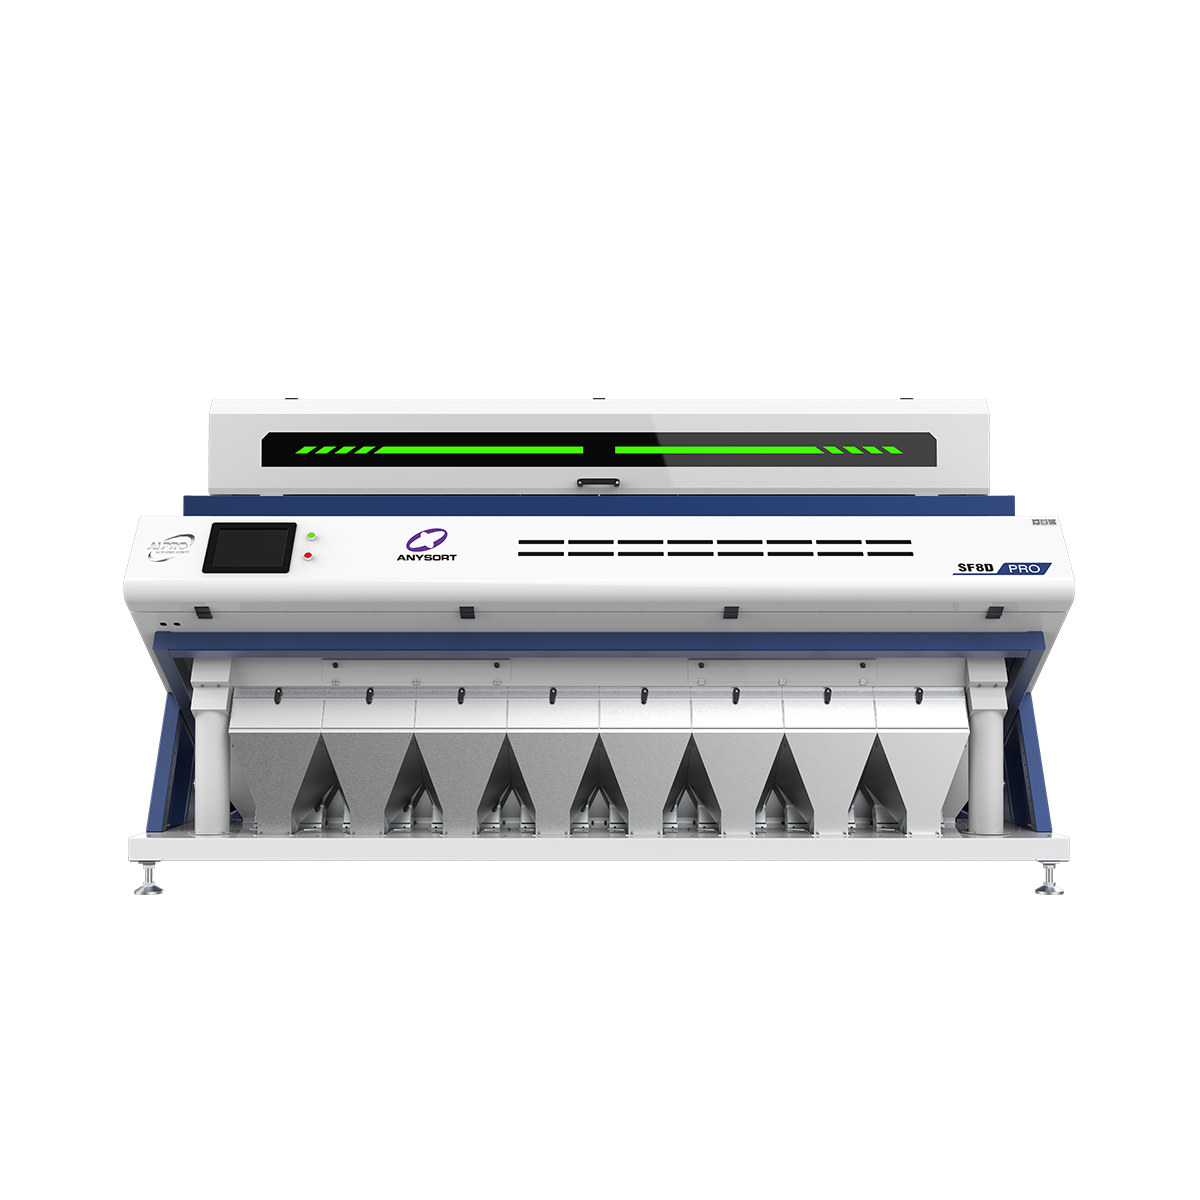
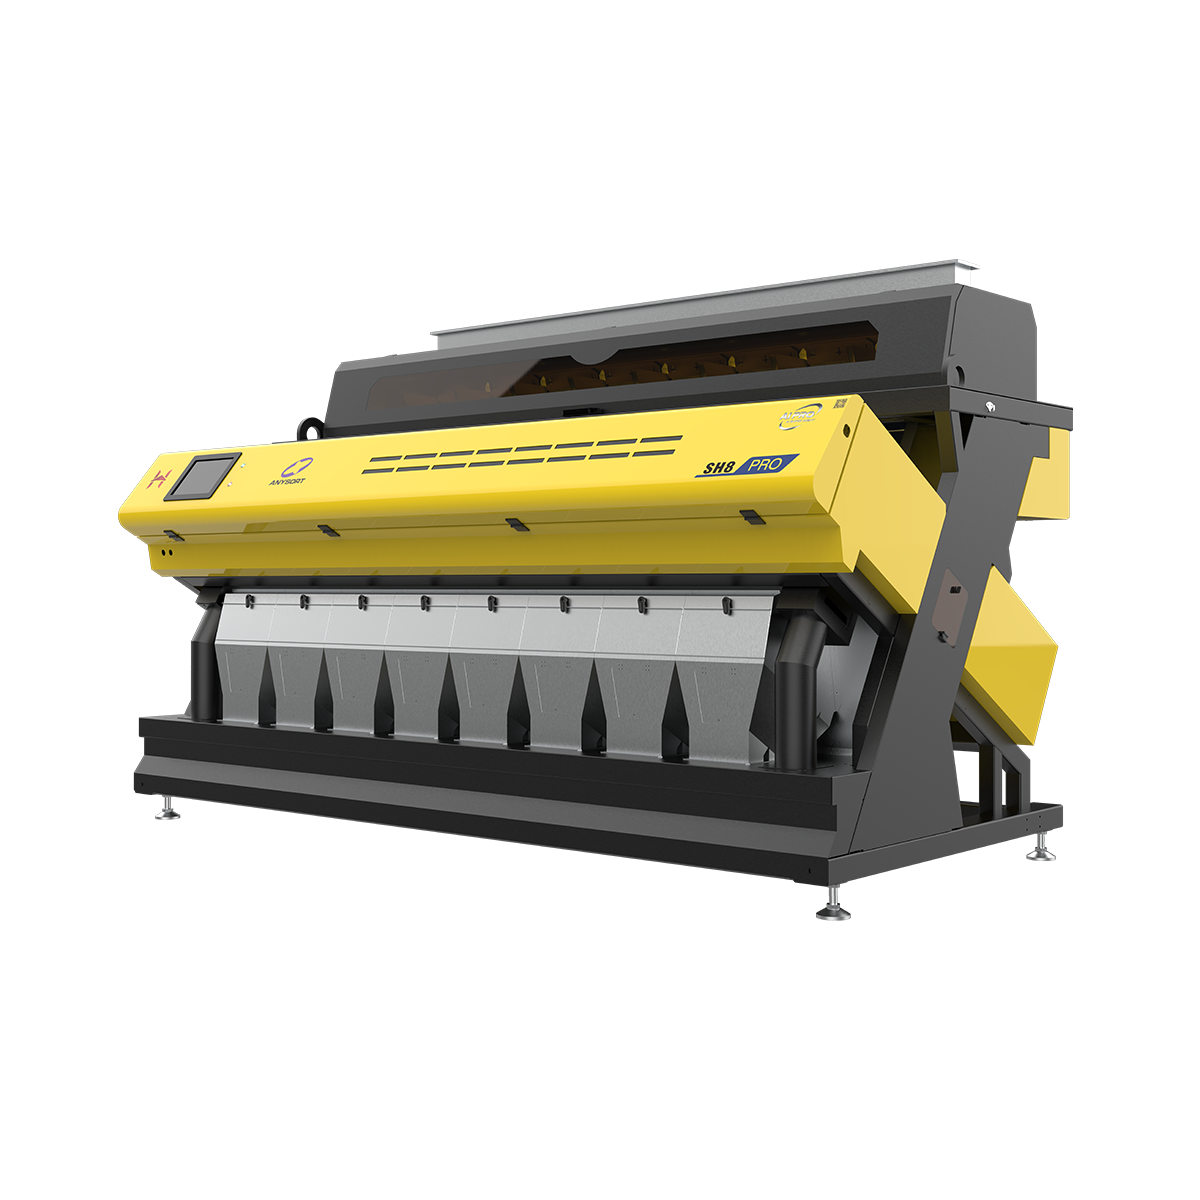
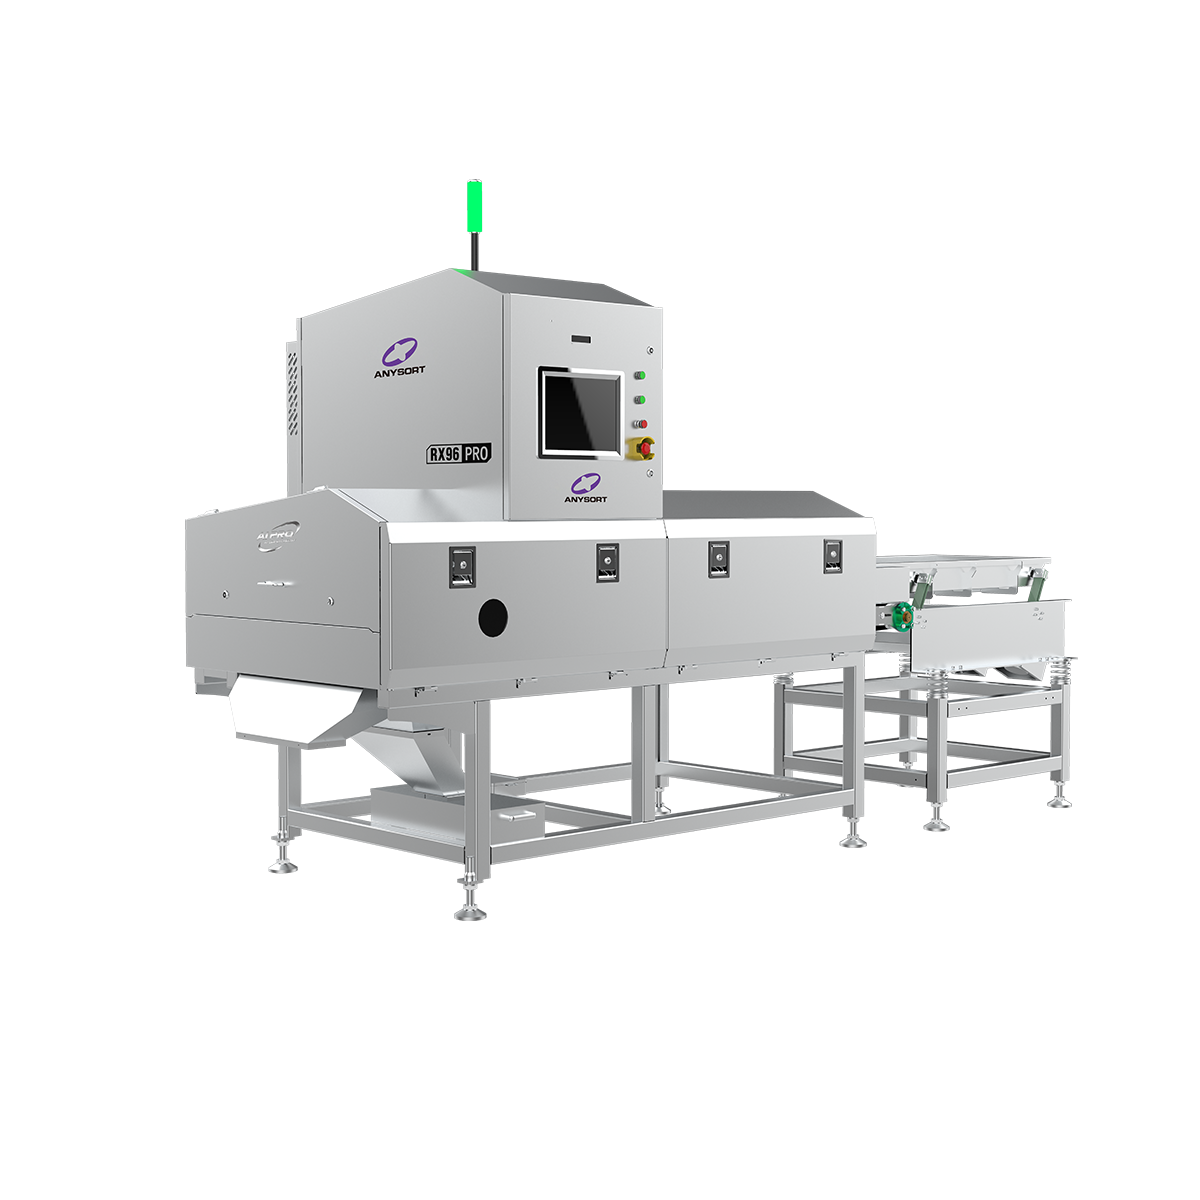
A multi grain sorting machine represents an advanced agricultural technology designed to separate and classify different types of grains with exceptional precision and efficiency. This sophisticated equipment automatically processes mixed grain samples by analyzing individual particles through optical and mechanical systems, ensuring accurate separation of wheat, barley, oats, rice, and other cereals. The multi grain sorting machine operates by conveying grain through specialized channels where sensors detect each kernel's characteristics, including size, color, and shape. Advanced imaging technology enables the machine to distinguish between quality grains and defective ones, removing foreign materials, discolored seeds, and damaged kernels with remarkable accuracy. The system's sophisticated sorting mechanism directs acceptable grains to collection bins while diverting rejected materials to separate outlets. Key technological features of the multi grain sorting machine include high-speed processing capabilities, processing up to several tons per hour depending on the model. The equipment incorporates real-time quality monitoring systems that adjust sorting parameters automatically. Multiple discharge channels allow simultaneous separation of various grain categories, maximizing productivity and reducing processing time significantly. Applications for the multi grain sorting machine extend across numerous sectors including commercial grain processing facilities, agricultural cooperatives, seed production companies, and food manufacturers. The machine proves invaluable for quality control, crop grading, contamination removal, and seed certification processes. Industries benefit from improved product quality, reduced waste, and enhanced operational efficiency when implementing this innovative sorting solution.

New Products

The multi grain sorting machine delivers substantial operational and economic benefits that directly enhance productivity and profitability for grain processing businesses. By automating the sorting process, this equipment eliminates manual labor requirements, reducing operational costs significantly while improving consistency and reliability across production batches. Operational efficiency represents a primary advantage of the multi grain sorting machine. The system processes grains rapidly, handling multiple tons hourly while maintaining superior accuracy levels impossible to achieve through manual sorting. This speed directly translates to increased throughput, allowing facilities to process larger quantities without expanding workforce requirements or facility space. Quality improvement stands as a critical buyer value proposition. The multi grain sorting machine removes defective kernels, foreign materials, and discolored grains with precision that exceeds human capabilities. This enhanced quality results in premium product grades, enabling businesses to access higher-value markets and command better pricing. Decision-useful product context shows the multi grain sorting machine works effectively across diverse grain types and processing scenarios. Whether handling wheat for flour production, barley for brewing, or seed grain for replanting, the equipment adapts to various applications. This versatility protects business investments by enabling facilities to process different commodities without purchasing multiple machines. Contamination prevention represents another significant advantage. The multi grain sorting machine identifies and removes insects, stones, metal fragments, and other hazardous materials before grains reach storage or processing stages. This protective function safeguards food safety compliance, reduces equipment damage downstream, and protects consumer safety. Maintenance simplicity and user-friendly operation mean facilities require minimal training investment. The multi grain sorting machine features intuitive controls and straightforward maintenance procedures, enabling standard staff to operate equipment effectively without specialized expertise.

Tips And Tricks

What Factors Affect Tea Color Sorter Performance and Accuracy?

05

Aug

What Factors Affect Tea Color Sorter Performance and Accuracy?

The precision of a tea color sorter directly determines the quality consistency of finished tea products. Understanding the factors that influence tea color sorter performance and accuracy is essential for tea processors seeking to maintain competiti...
View More
How Much Does a Color Sorter Machine Cost?

12

Aug

How Much Does a Color Sorter Machine Cost?

Understanding the investment required for a color sorter machine is essential for businesses in agriculture, food processing, and recycling sectors. The cost of a color sorter machine varies significantly based on capacity, technology sophistication,...
View More
How does optical sorting technology detect defective rice grains?

22

Aug

How does optical sorting technology detect defective rice grains?

Modern rice processing demands precision and consistency, which is why understanding the detection mechanisms behind advanced equipment has become essential for producers. A rice color sorter represents one of the most significant technological break...
View More
Which factors should you consider when selecting a rice color sorter?

29

Aug

Which factors should you consider when selecting a rice color sorter?

Selecting the right rice color sorter is a critical decision that directly impacts your grain processing efficiency, product quality, and long-term profitability. A rice color sorter removes discolored, damaged, and foreign particles from rice batche...
View More

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

multi grain sorting machine

Precision Optical Sorting Technology

Precision Optical Sorting Technology

The multi grain sorting machine incorporates cutting-edge optical imaging systems that analyze thousands of individual grains per second. Advanced sensors detect subtle variations in color, size, and shape characteristics that identify quality differences invisible to human inspection. This precision technology ensures consistent separation of premium-grade grains from substandard kernels, damaged seeds, and foreign materials. The multi grain sorting machine's optical system automatically adjusts to different grain varieties, eliminating the need for manual recalibration between processing batches. Food manufacturers and grain exporters particularly value this technological capability because it guarantees product uniformity and meets rigorous international quality standards. By removing defective grains before processing, the multi grain sorting machine prevents contamination that could compromise final product quality or trigger recalls, directly protecting brand reputation and customer confidence in delivered products.
High-Capacity Processing Performance

High-Capacity Processing Performance

Modern multi grain sorting machine models deliver exceptional throughput capacity, processing several tons of grain hourly while maintaining sorting accuracy throughout operations. This high-capacity performance enables grain facilities to meet demanding market orders without bottleneck delays or production constraints. The multi grain sorting machine operates continuously during peak harvest seasons when processing volume increases substantially. Multiple discharge channels enable simultaneous sorting of different grain categories, maximizing efficiency and reducing handling requirements. Agricultural cooperatives and commercial processors benefit significantly from this performance advantage, as the multi grain sorting machine eliminates manual sorting bottlenecks that traditionally limited production capacity. By dramatically increasing processing speed, this equipment enables facilities to handle expanded customer demand without proportional increases in labor costs. The multi grain sorting machine proves particularly valuable for businesses pursuing growth strategies, as equipment capacity scales with expanding market opportunities without requiring facility expansion or additional space investments.
Versatile Application Across Grain Types

Versatile Application Across Grain Types

The multi grain sorting machine demonstrates remarkable versatility, processing wheat, barley, oats, rice, legumes, and specialty grains within a single system. This multi-grain compatibility protects capital investments by enabling facilities to process diverse commodities without purchasing dedicated equipment for specific grain varieties. The multi grain sorting machine adapts quickly between different materials through intuitive parameter adjustments, eliminating extended downtime between production runs. Seed producers, grain merchants, and food processors operate the multi grain sorting machine across multiple applications, dramatically improving utilization rates and return on investment. This application flexibility proves particularly advantageous for businesses serving diverse customer bases with varying grain requirements. The multi grain sorting machine's ability to handle different grain types with consistent accuracy means facilities can maintain competitive advantages across multiple market segments simultaneously. Whether processing animal feed, human consumption grains, or certified seed stock, the multi grain sorting machine delivers reliable performance that supports comprehensive business strategy objectives.

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

Copyright © 2026 Anhui Jiexun Optoelectronic Technology Co., Ltd. All rights reserved.  -  Privacy policy