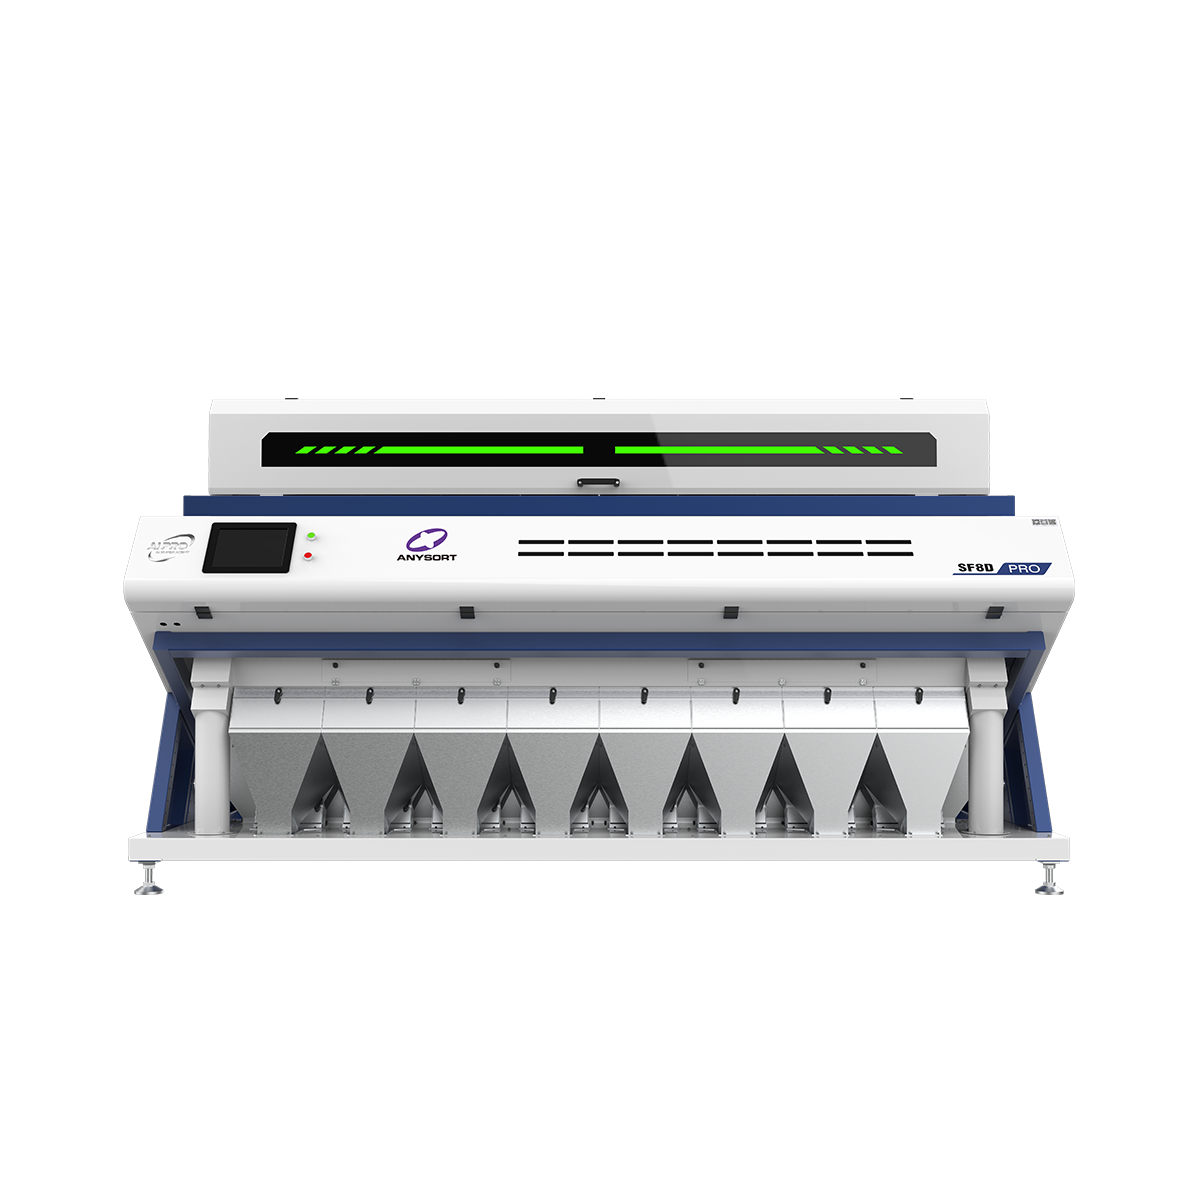
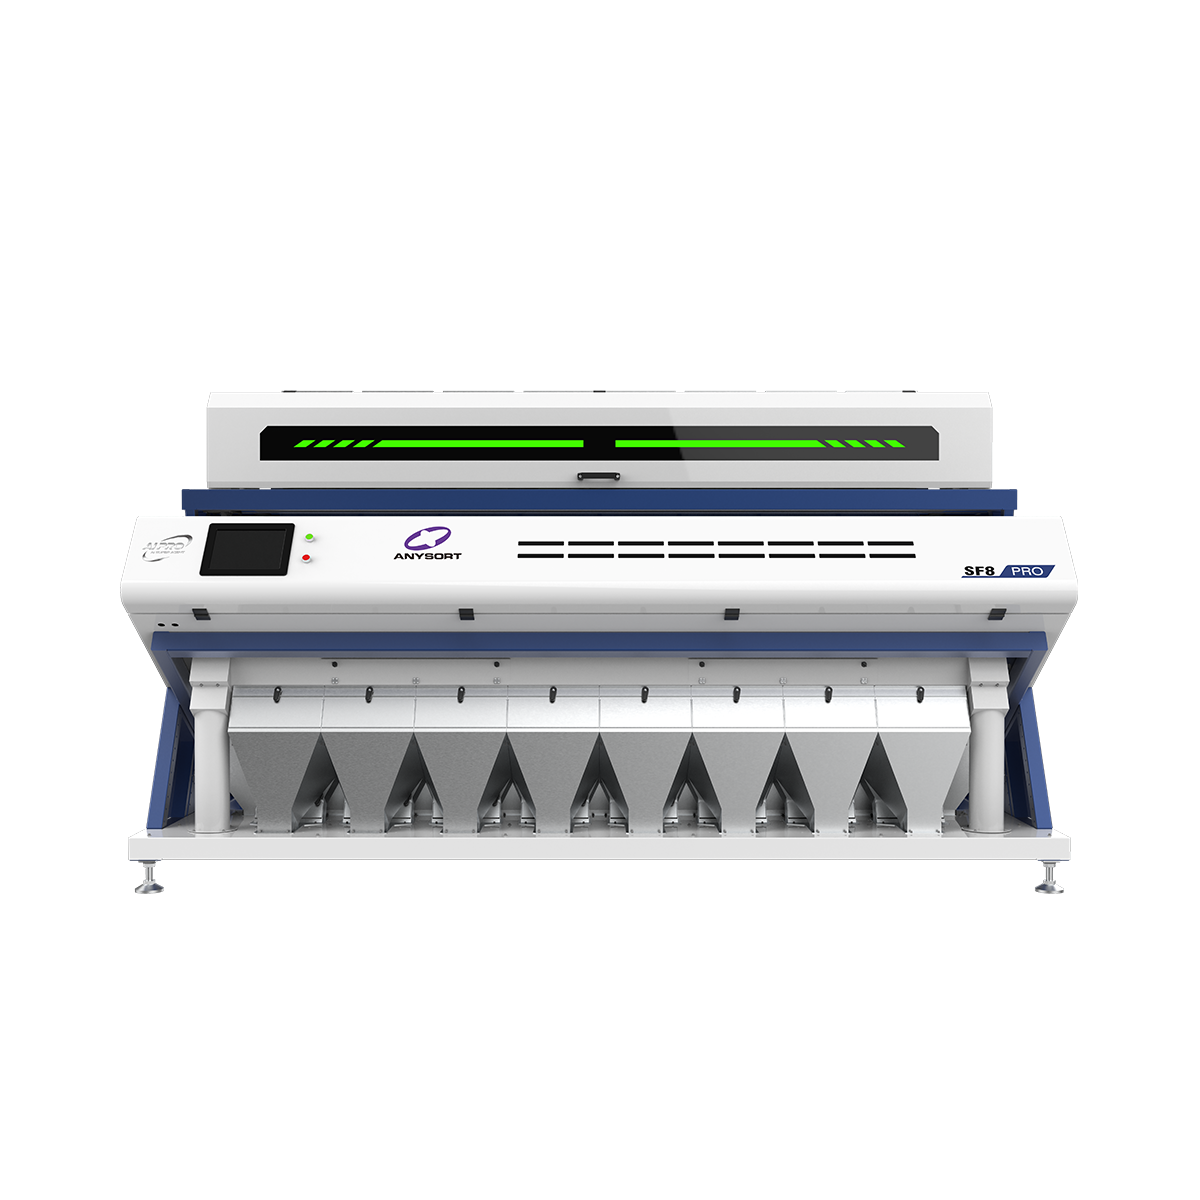
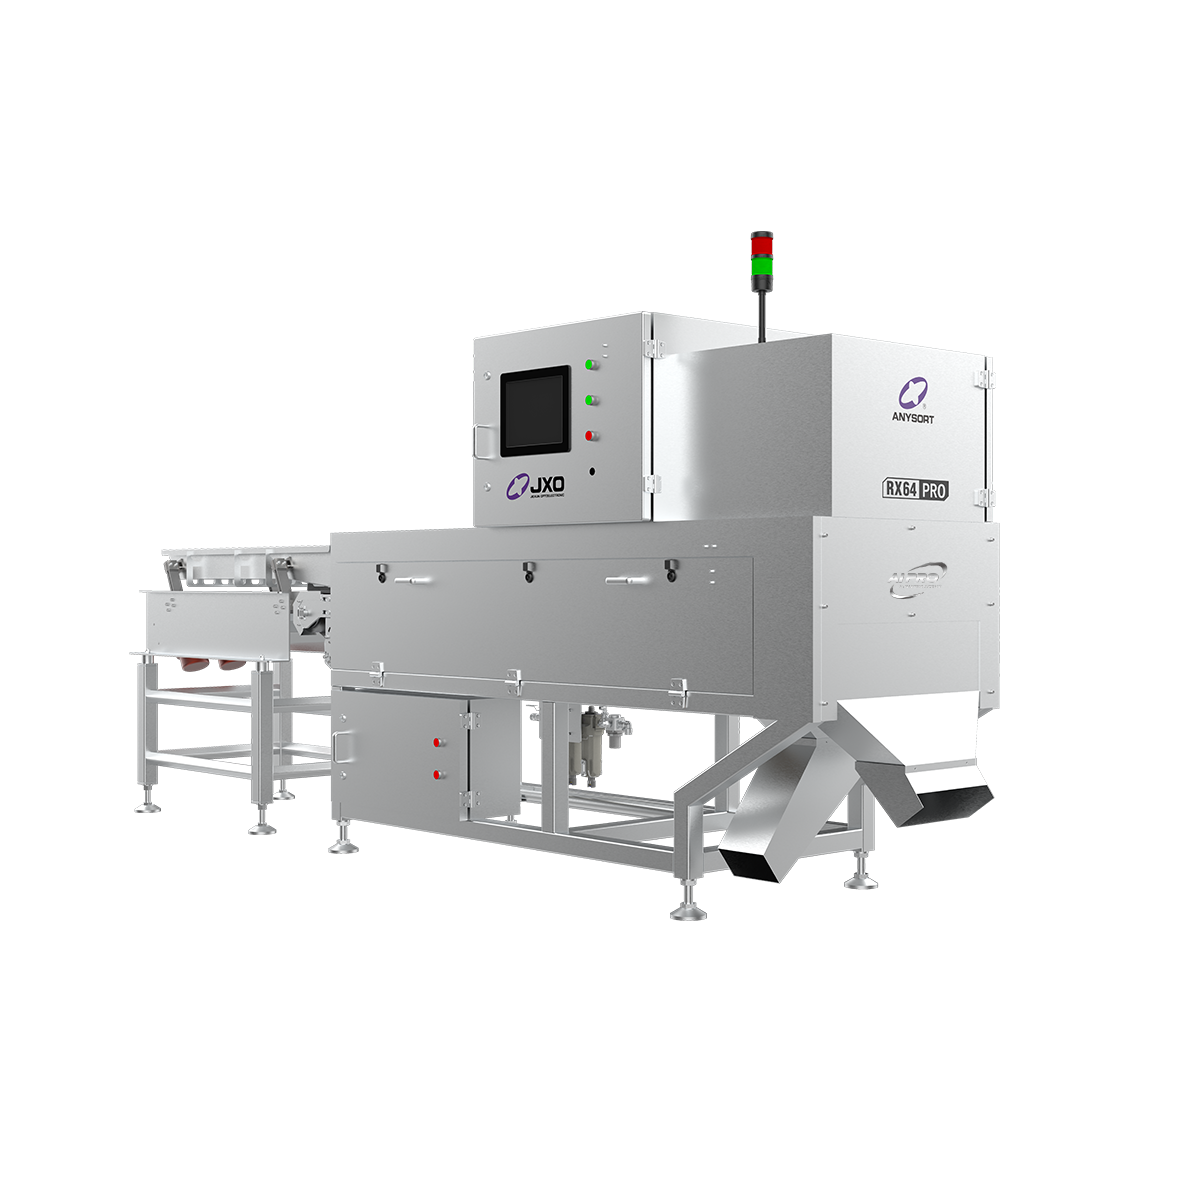
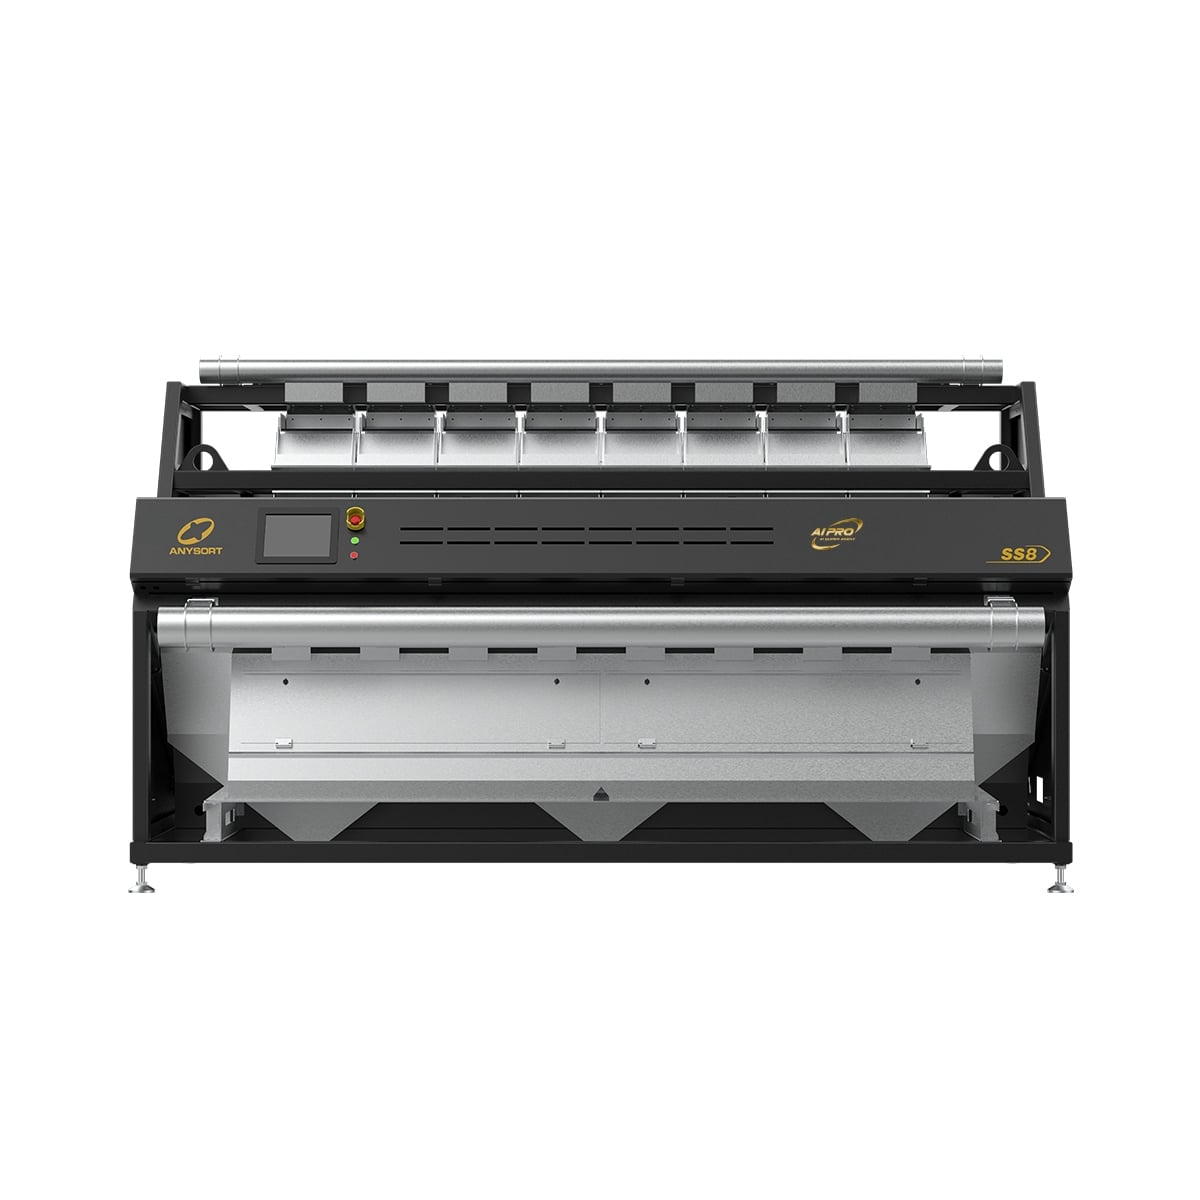
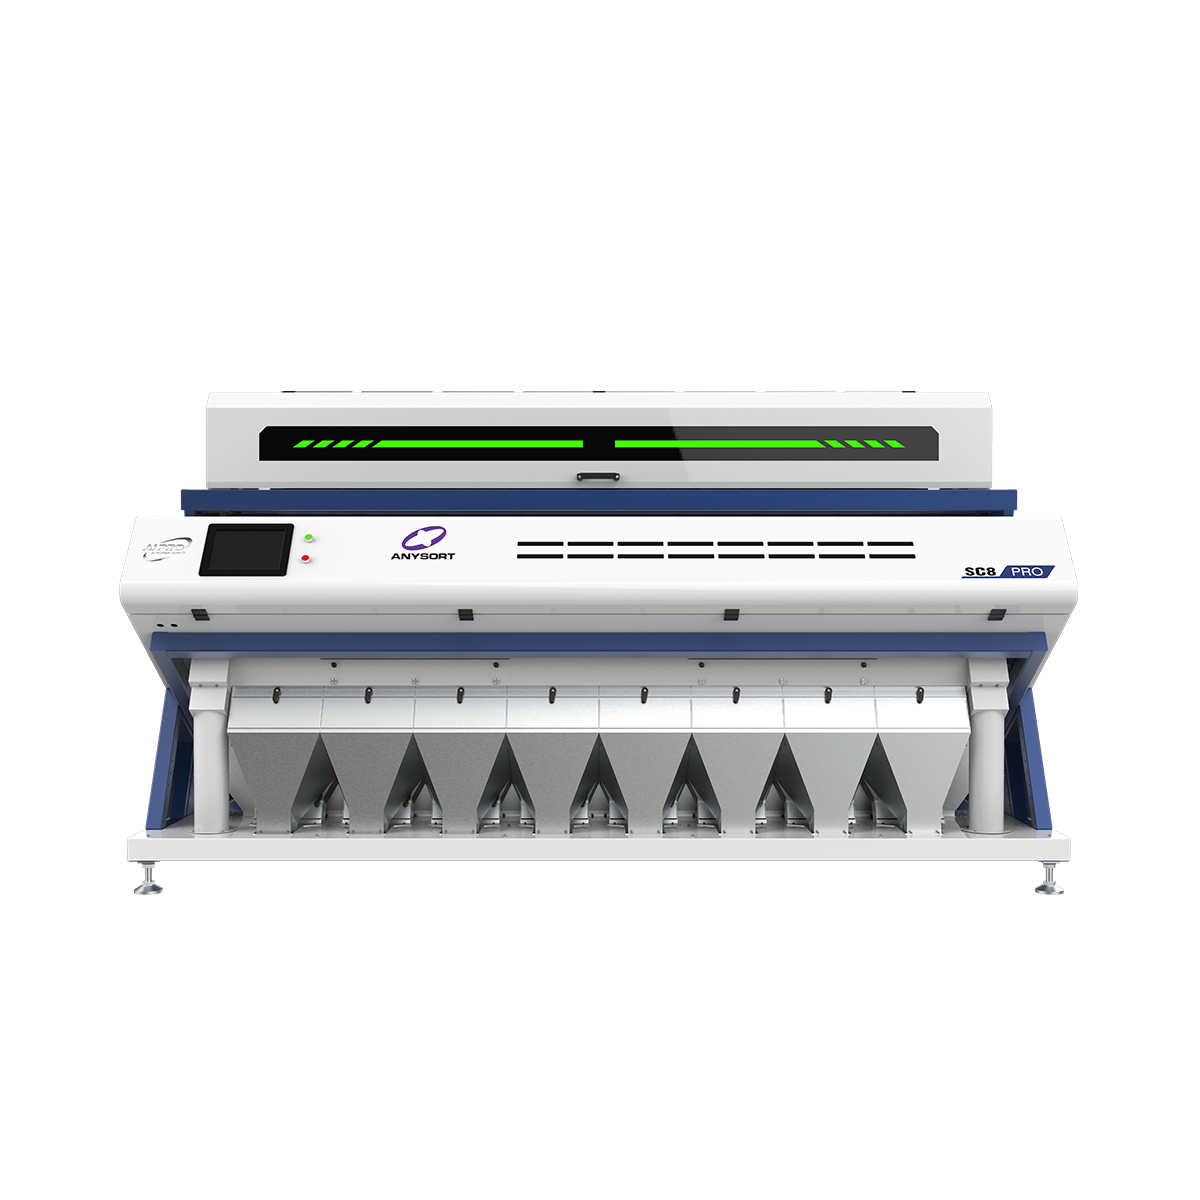
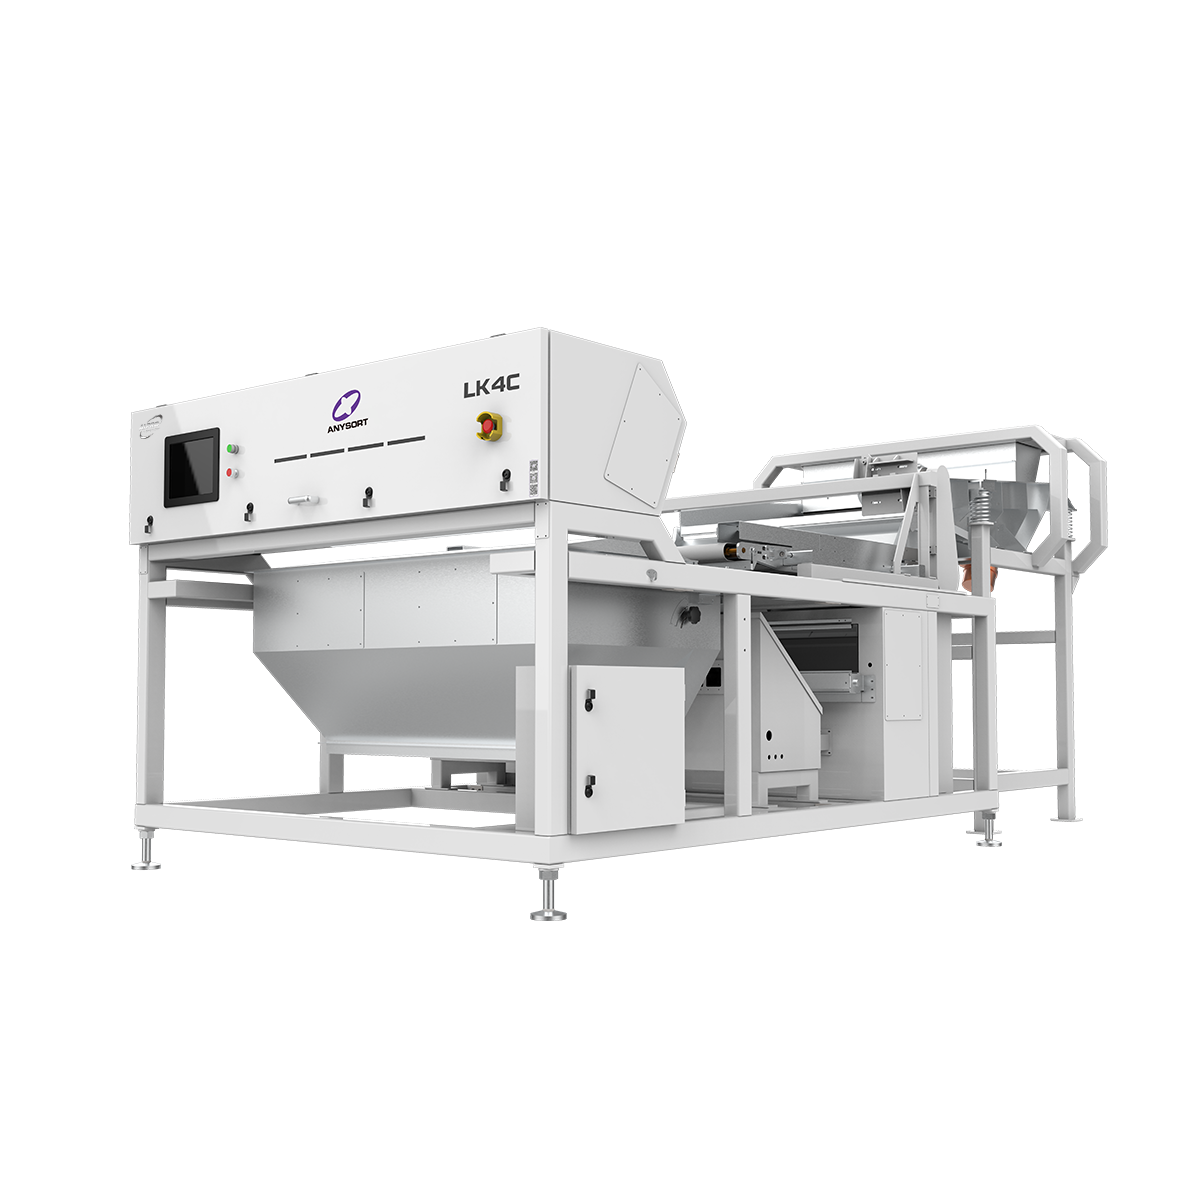
colour sorter machine
A colour sorter machine is an advanced optical sorting system designed to automatically detect, categorize, and separate materials based on their color properties. This sophisticated equipment utilizes high-speed cameras, advanced sensors, and artificial intelligence technology to achieve precise sorting accuracy at industrial scales. The colour sorter machine represents a significant advancement in material processing, offering unparalleled efficiency compared to manual sorting methods.
The primary function of a colour sorter machine involves scanning materials as they pass through the sorting chamber, capturing detailed color information, and using machine learning algorithms to identify defects, contamination, or quality variations. Once identified, the colour sorter machine activates pneumatic ejection mechanisms to remove unwanted items with millisecond precision. This automated process ensures consistent quality control and significantly increases throughput capacity.
Technologically, the colour sorter machine integrates multiple components including LED illumination systems, high-resolution imaging sensors, and rapid-response ejection valves. The colour sorter machine operates continuously, processing thousands of items per minute while maintaining exceptional accuracy levels. Modern colour sorter machines feature customizable sorting parameters, allowing operators to adjust sensitivity settings based on specific material requirements and quality standards, making this equipment versatile across numerous industries.

 EN