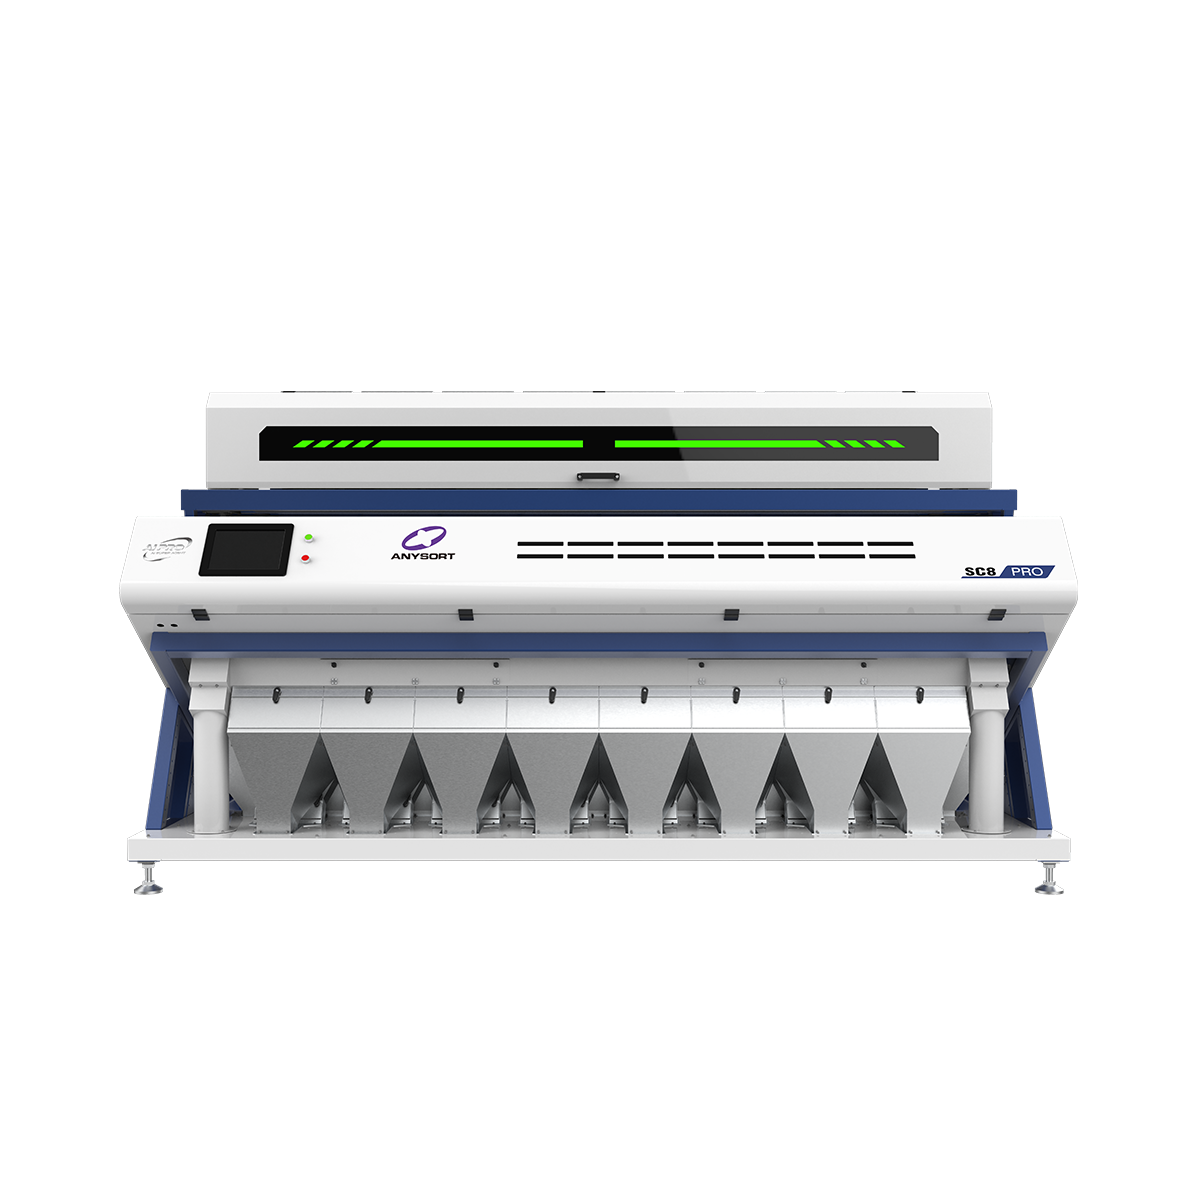
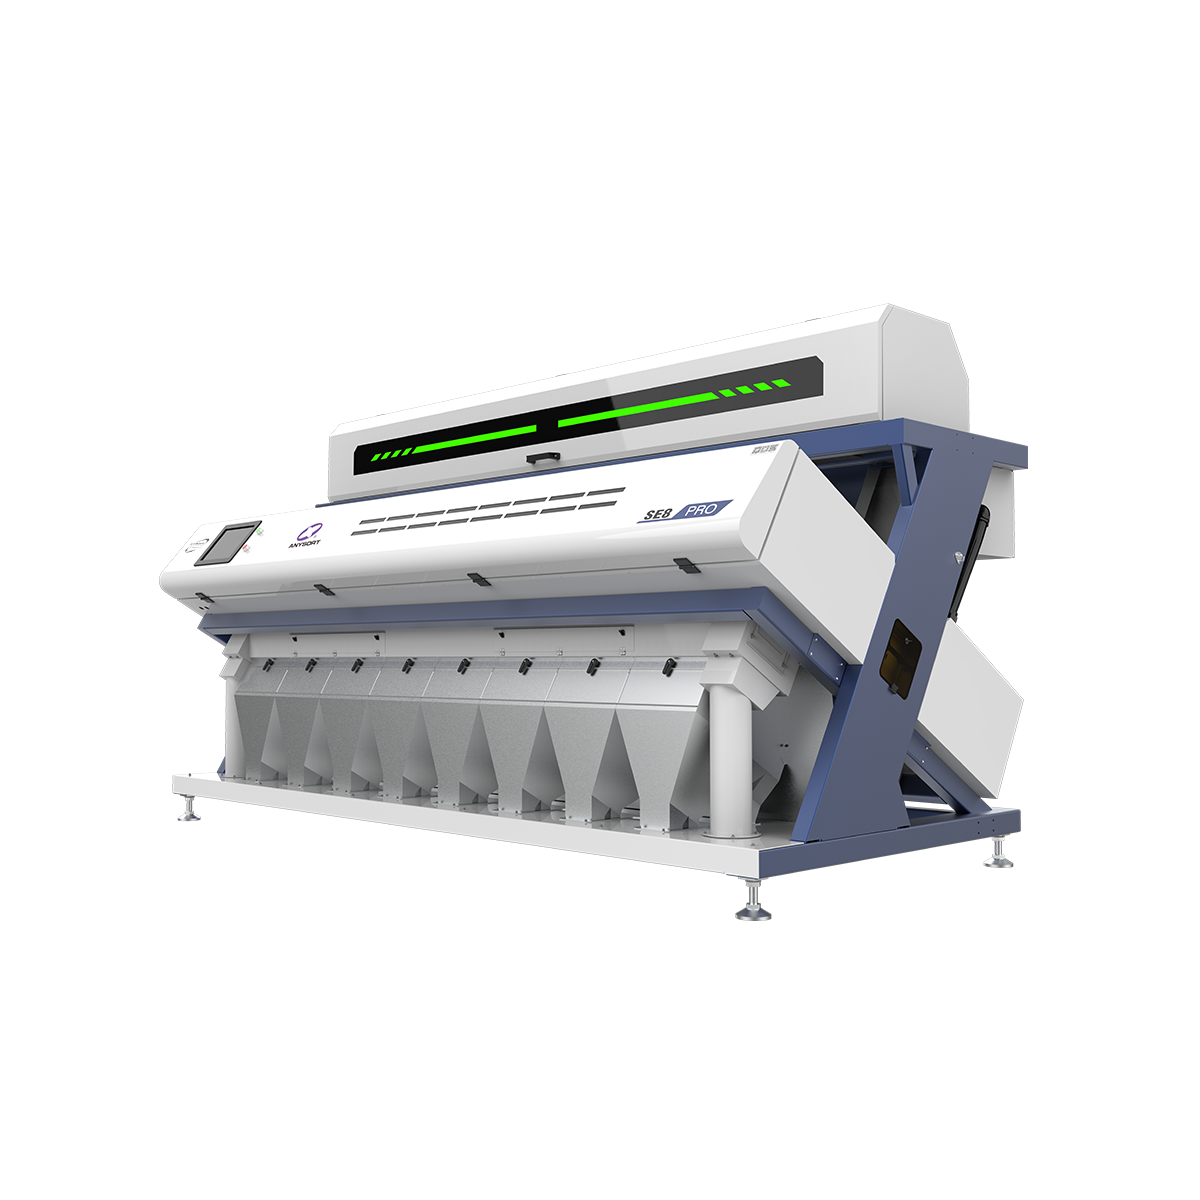
advanced optical sorter
An advanced optical sorter represents a sophisticated solution for automated material separation and classification. This cutting-edge technology uses advanced imaging systems and artificial intelligence to identify, analyze, and sort materials with exceptional precision. The advanced optical sorter operates by capturing high-resolution images of objects passing through its optical detection zone, then processing this visual data through intelligent algorithms to determine material composition, color, size, and quality characteristics.
The technological foundation of an advanced optical sorter includes multiple spectral cameras, LED lighting systems, and real-time processing capabilities. These components work together to scan each item individually, comparing it against programmed sorting parameters. The advanced optical sorter can distinguish between materials that appear similar to the human eye, making it invaluable for industries requiring strict quality control.
Applications for an advanced optical sorter span numerous sectors including food processing, recycling, mining, pharmaceuticals, and manufacturing. In food industries, this technology ensures consistent product quality by removing defects and foreign materials. The advanced optical sorter excels in recycling operations, where it accurately separates different plastic types, metals, and glass. Mining operations deploy this technology to identify valuable minerals from ore, while pharmaceutical manufacturers use it to inspect tablets and capsules for defects. Manufacturing facilities rely on an advanced optical sorter to maintain production standards and reduce waste, making it an essential investment for quality-driven businesses across multiple industries.

 EN