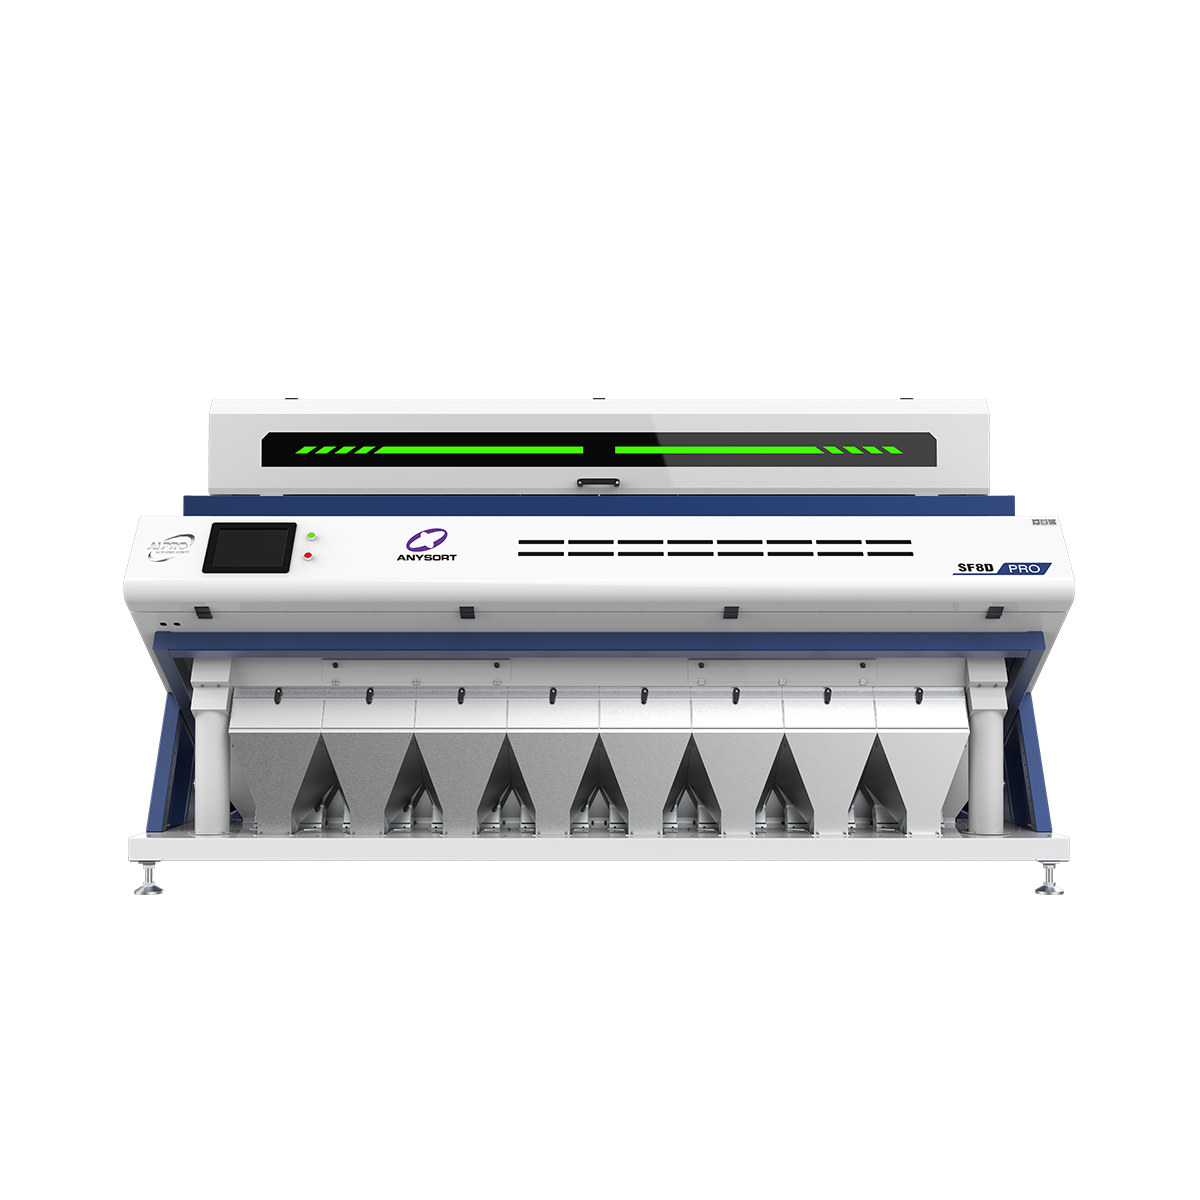
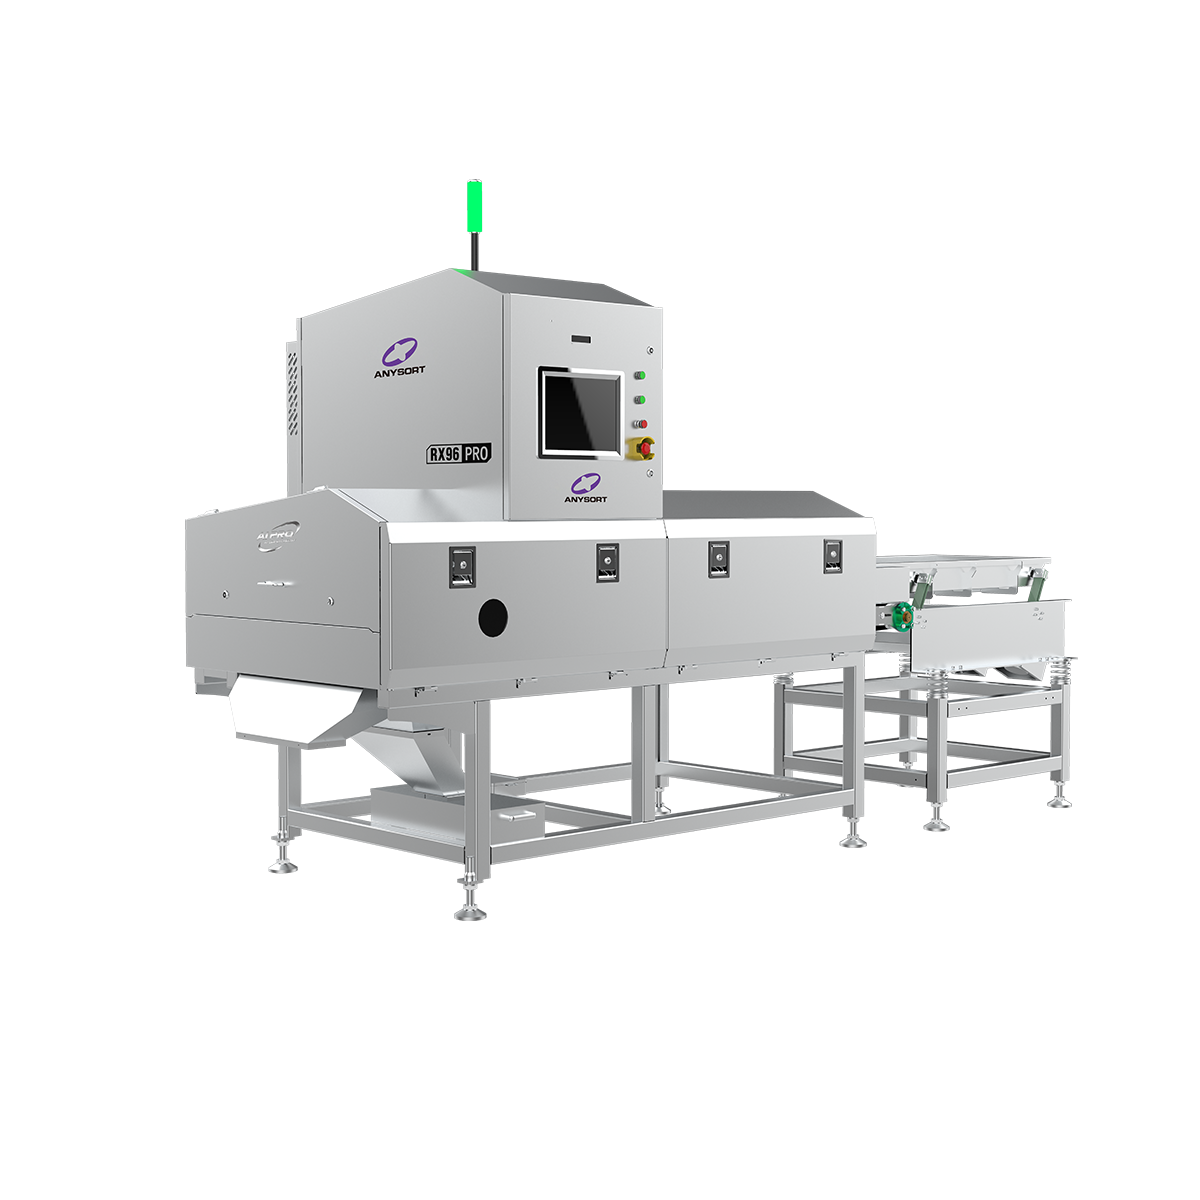
best color sorter machine
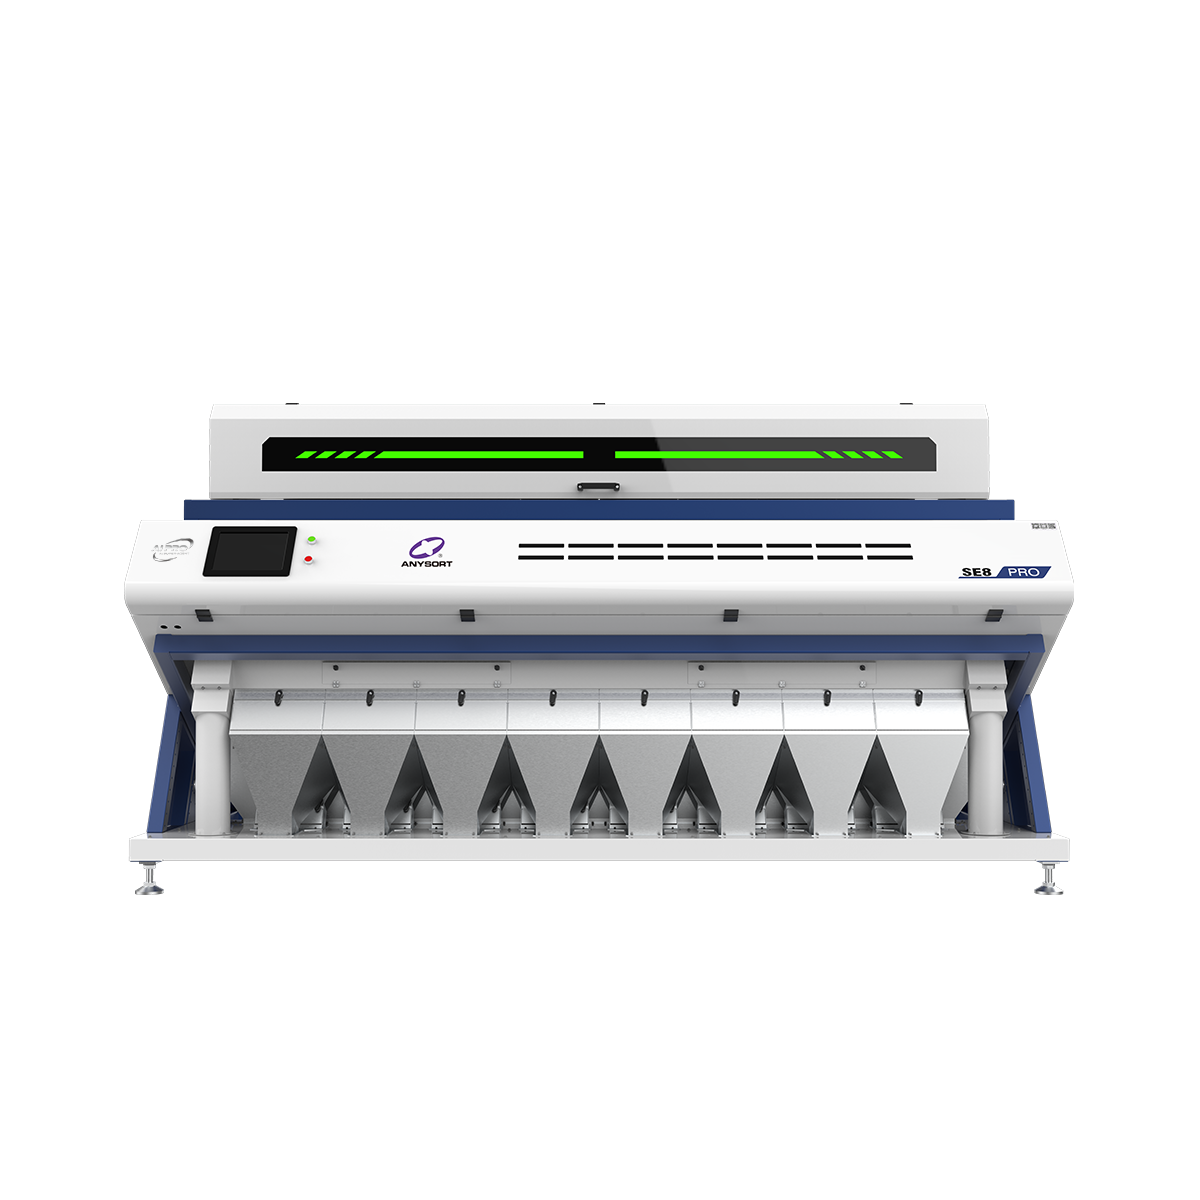
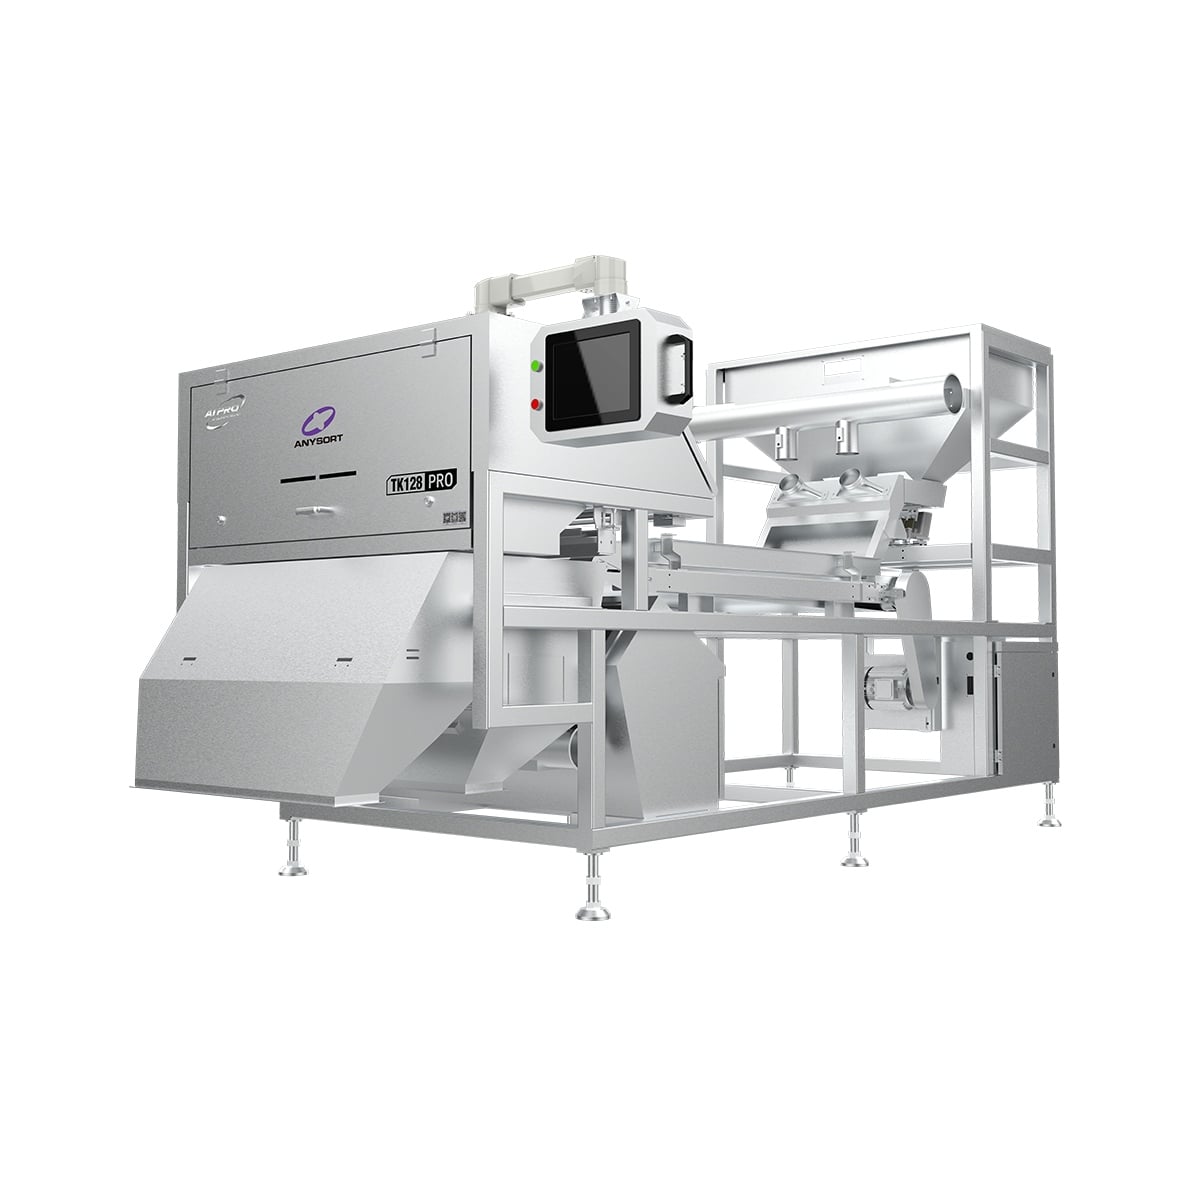
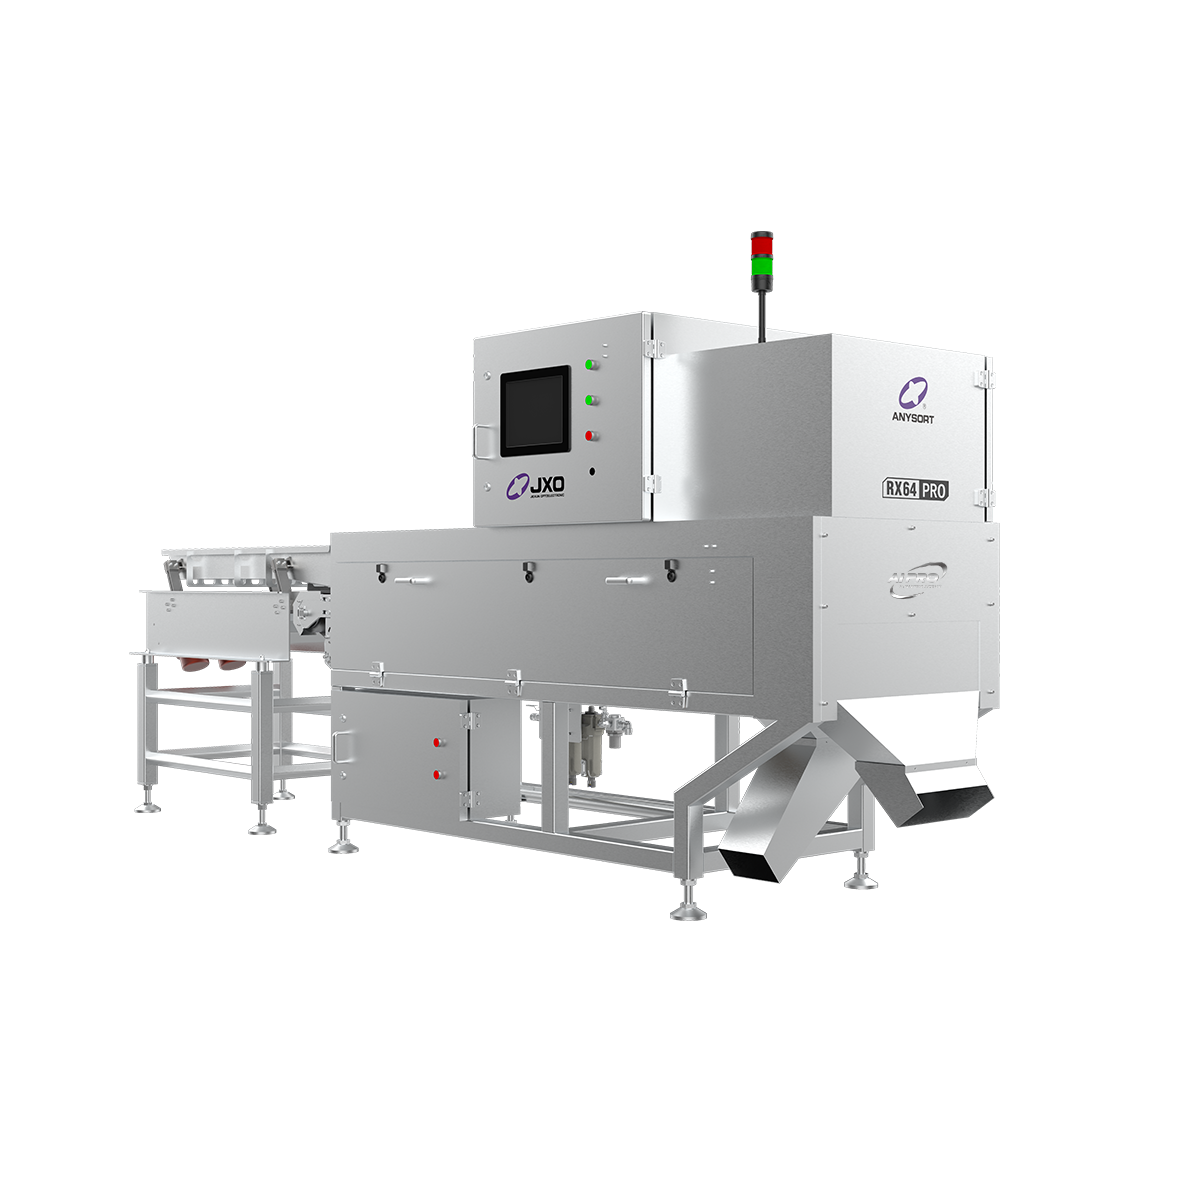
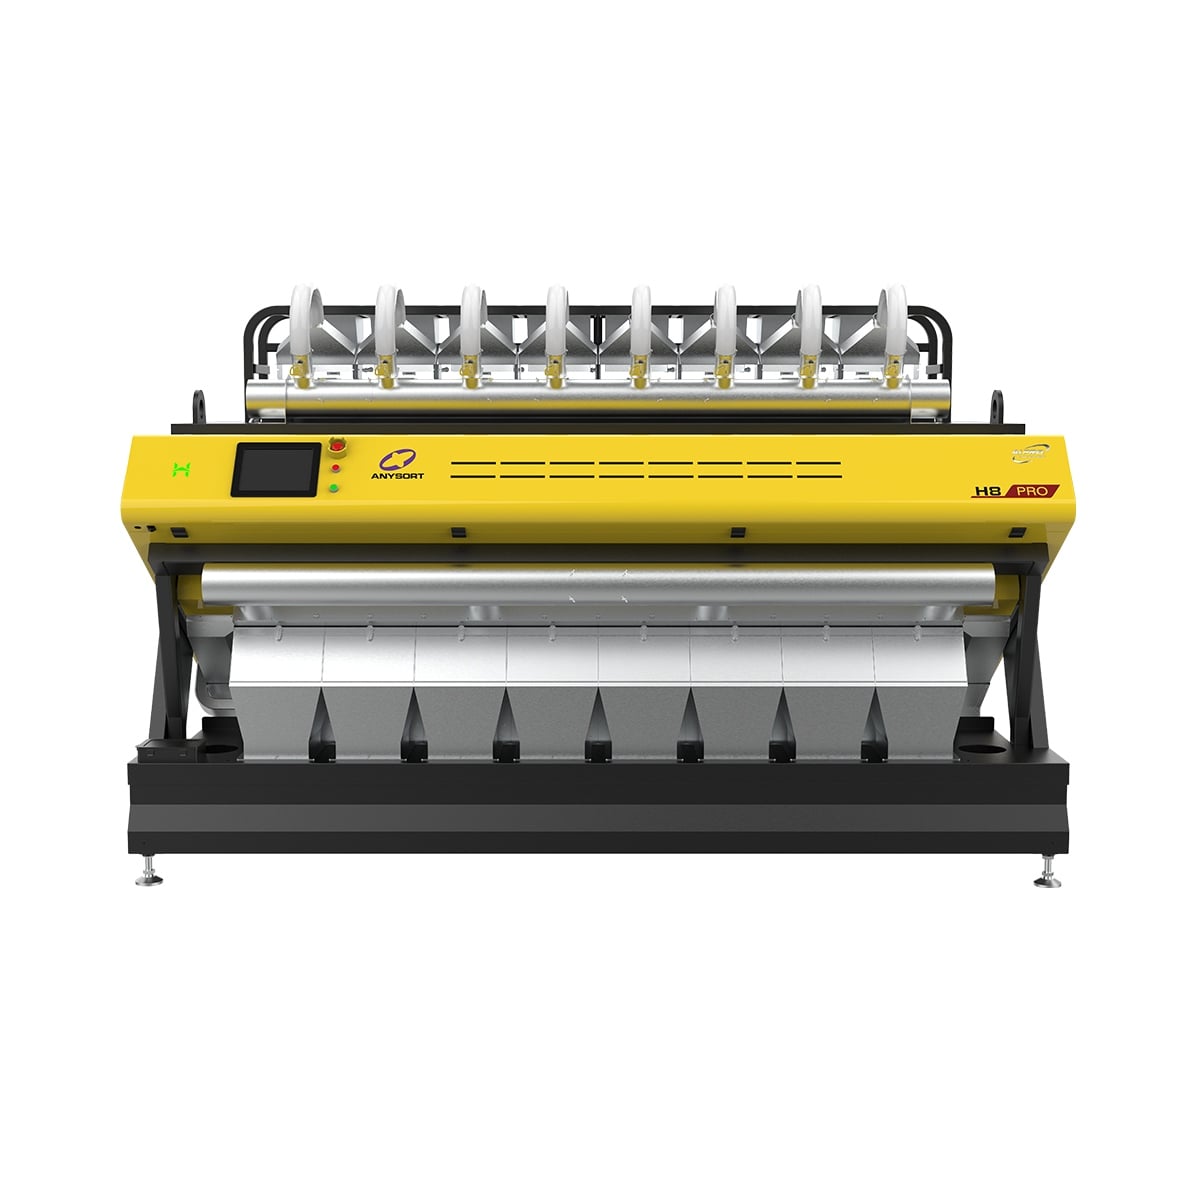
The best color sorter machine represents a revolutionary advancement in agricultural and industrial processing technology. These sophisticated devices utilize advanced optical sensors and artificial intelligence to automatically separate materials based on color, size, and quality characteristics. The best color sorter machine operates by capturing high-resolution images of each particle passing through its detection system, then using powerful algorithms to make real-time sorting decisions with exceptional accuracy. This best color sorter machine technology has become essential across multiple industries, including food processing, recycling, mining, and grain handling. The best color sorter machine employs cutting-edge imaging technology combined with precision mechanical systems to deliver consistent, reliable results. Modern units feature high-speed cameras capable of scanning thousands of particles per second, ensuring minimal waste and maximum throughput. The technology behind the best color sorter machine allows operators to customize sorting parameters for specific materials and applications. With touchscreen interfaces and intuitive controls, the best color sorter machine makes complex sorting operations accessible to operators of all skill levels. These machines significantly reduce manual labor while improving product quality and consistency. The best color sorter machine continues to evolve, incorporating machine learning capabilities that enable systems to adapt and improve performance over time. Investment in a quality best color sorter machine delivers measurable returns through increased efficiency, reduced contamination, and enhanced product value.

 EN