color sorter factory
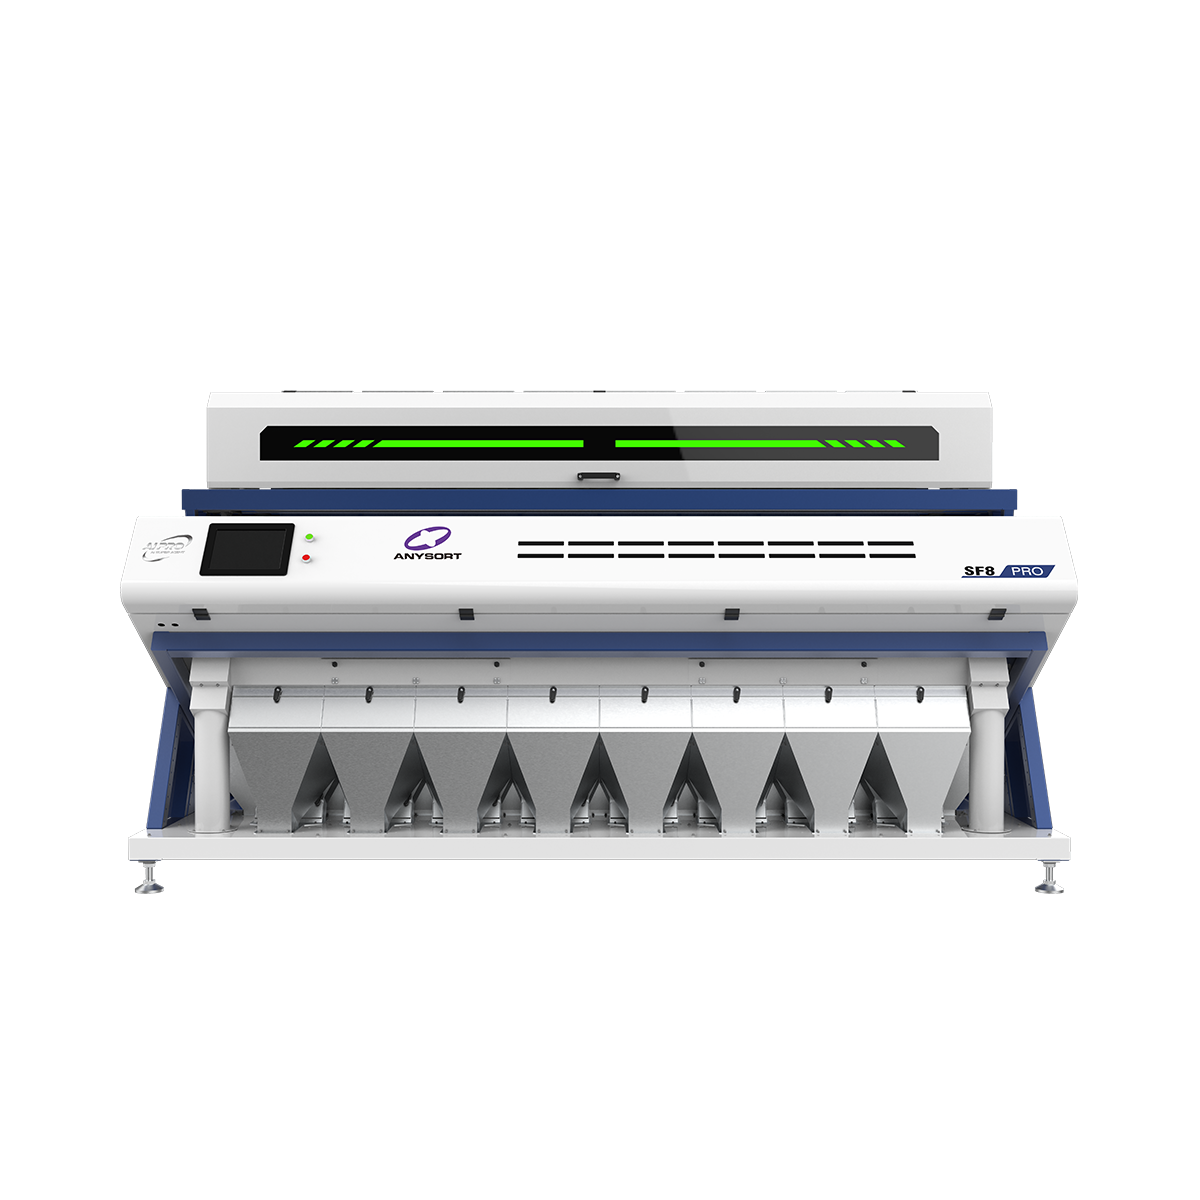
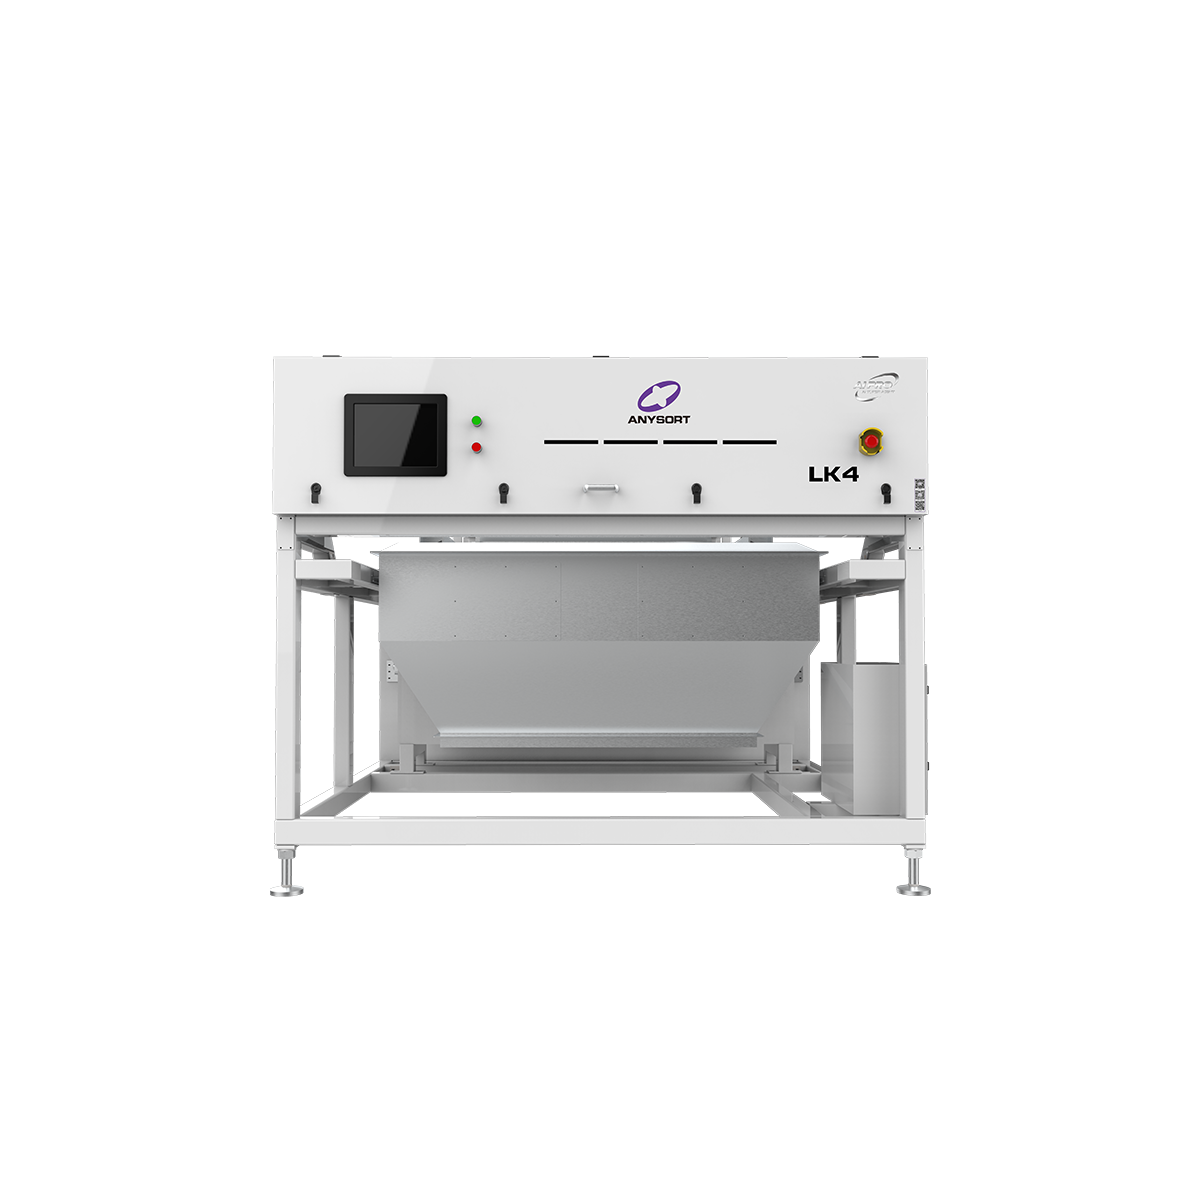
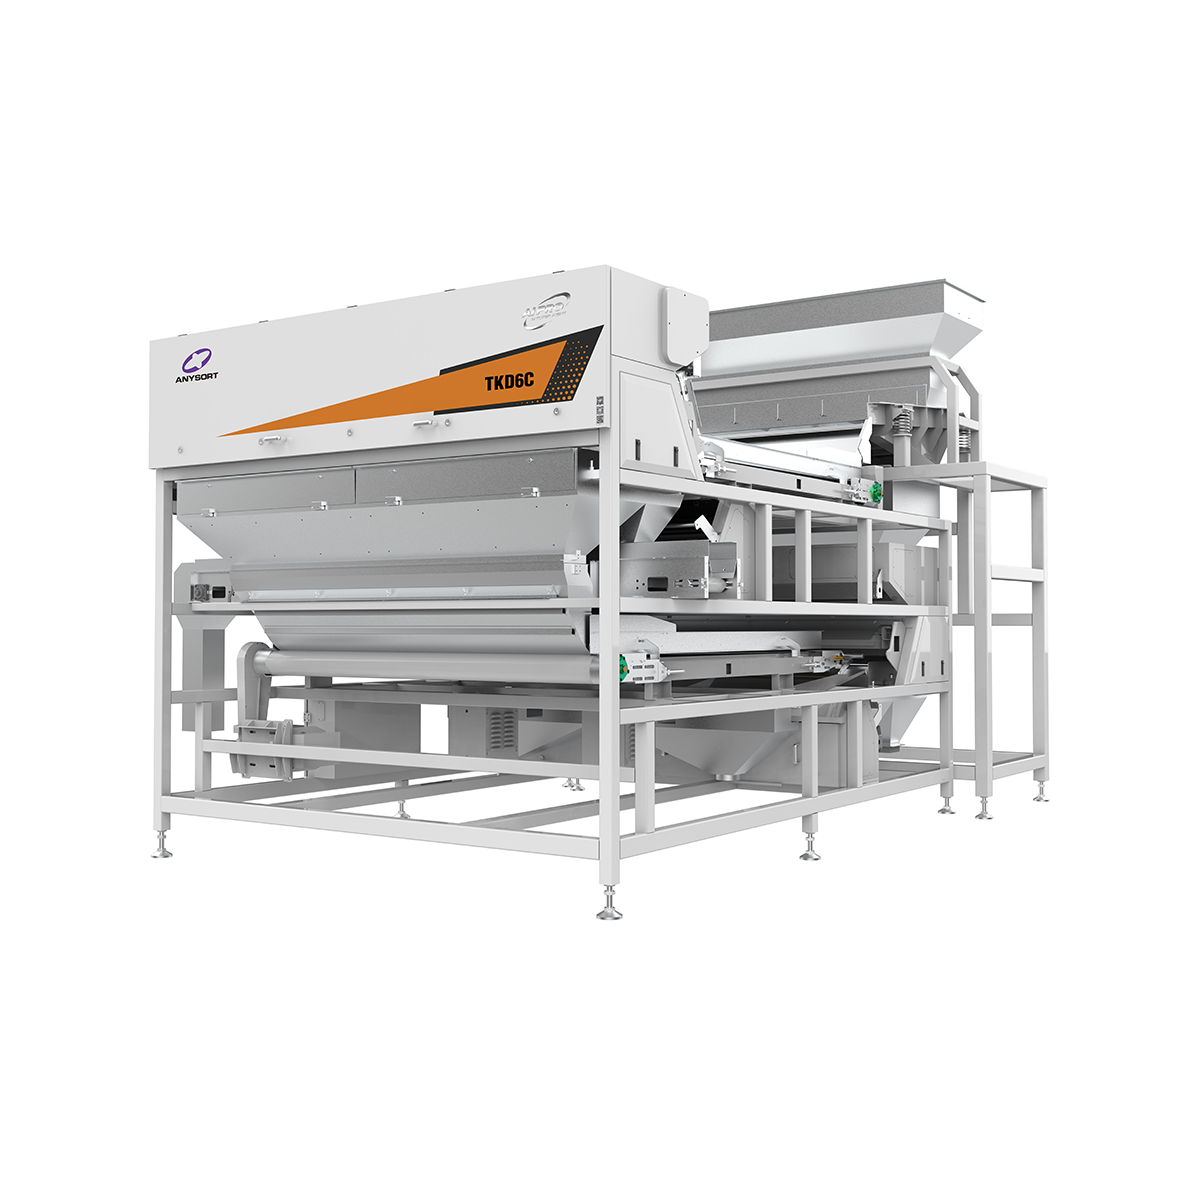
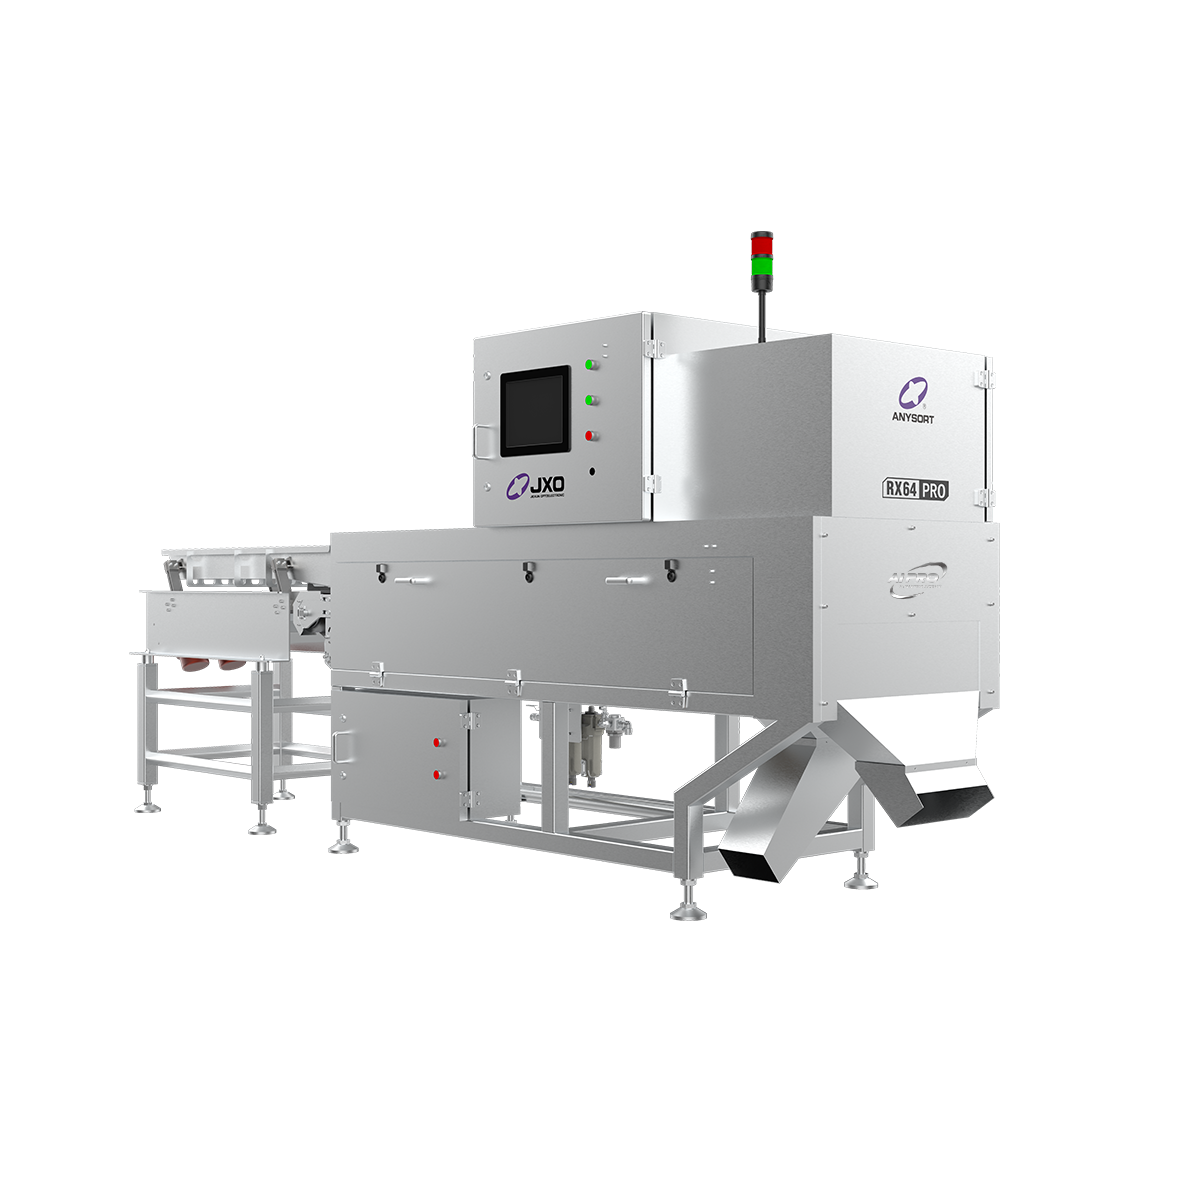
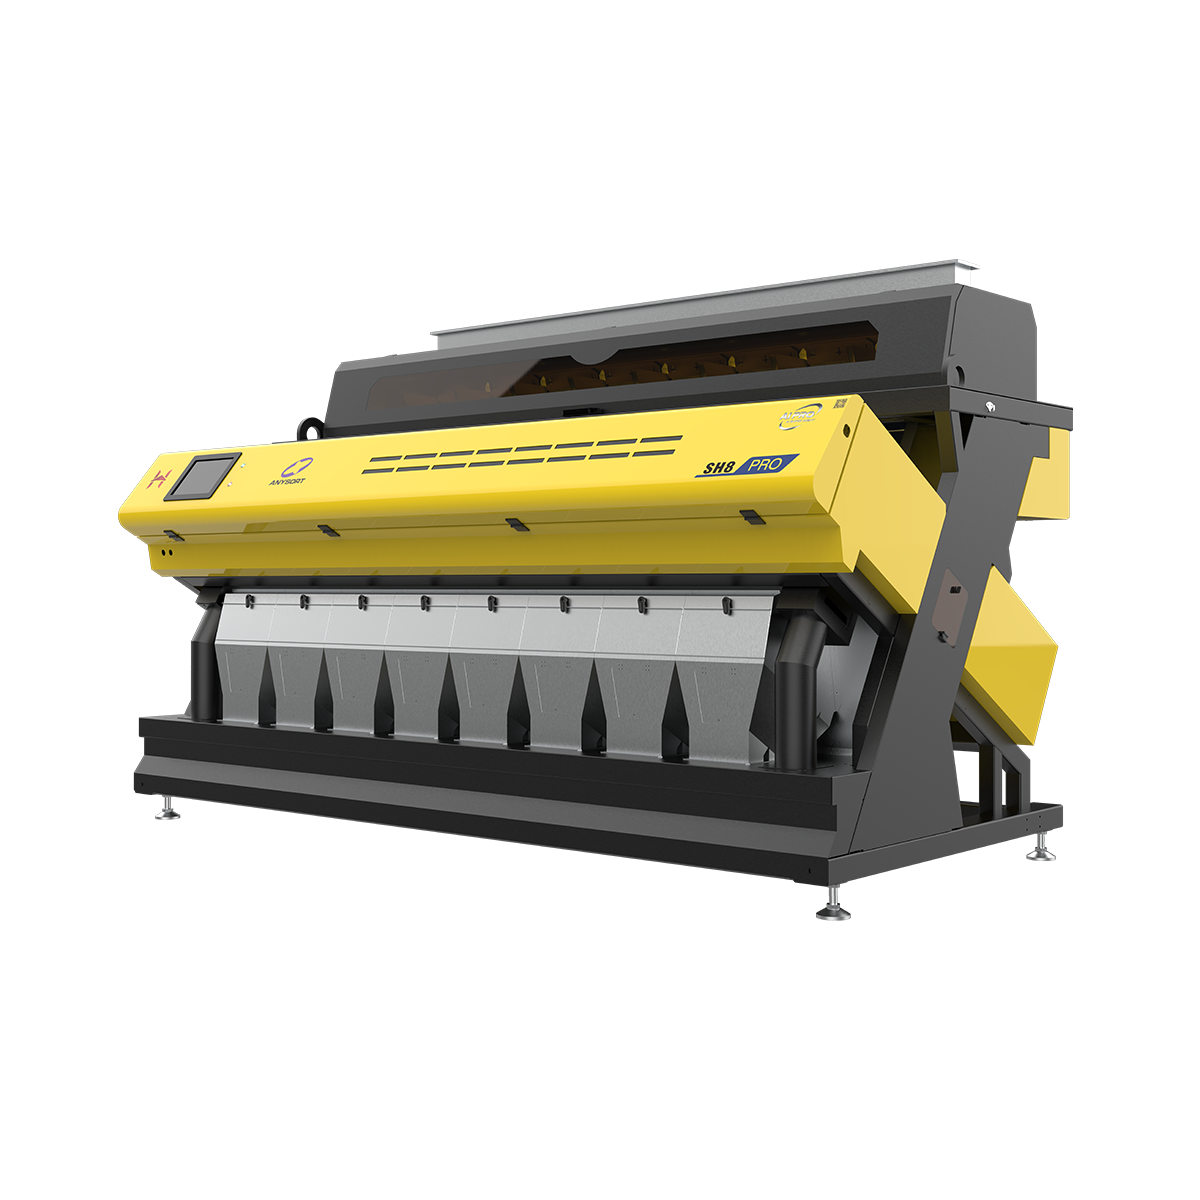
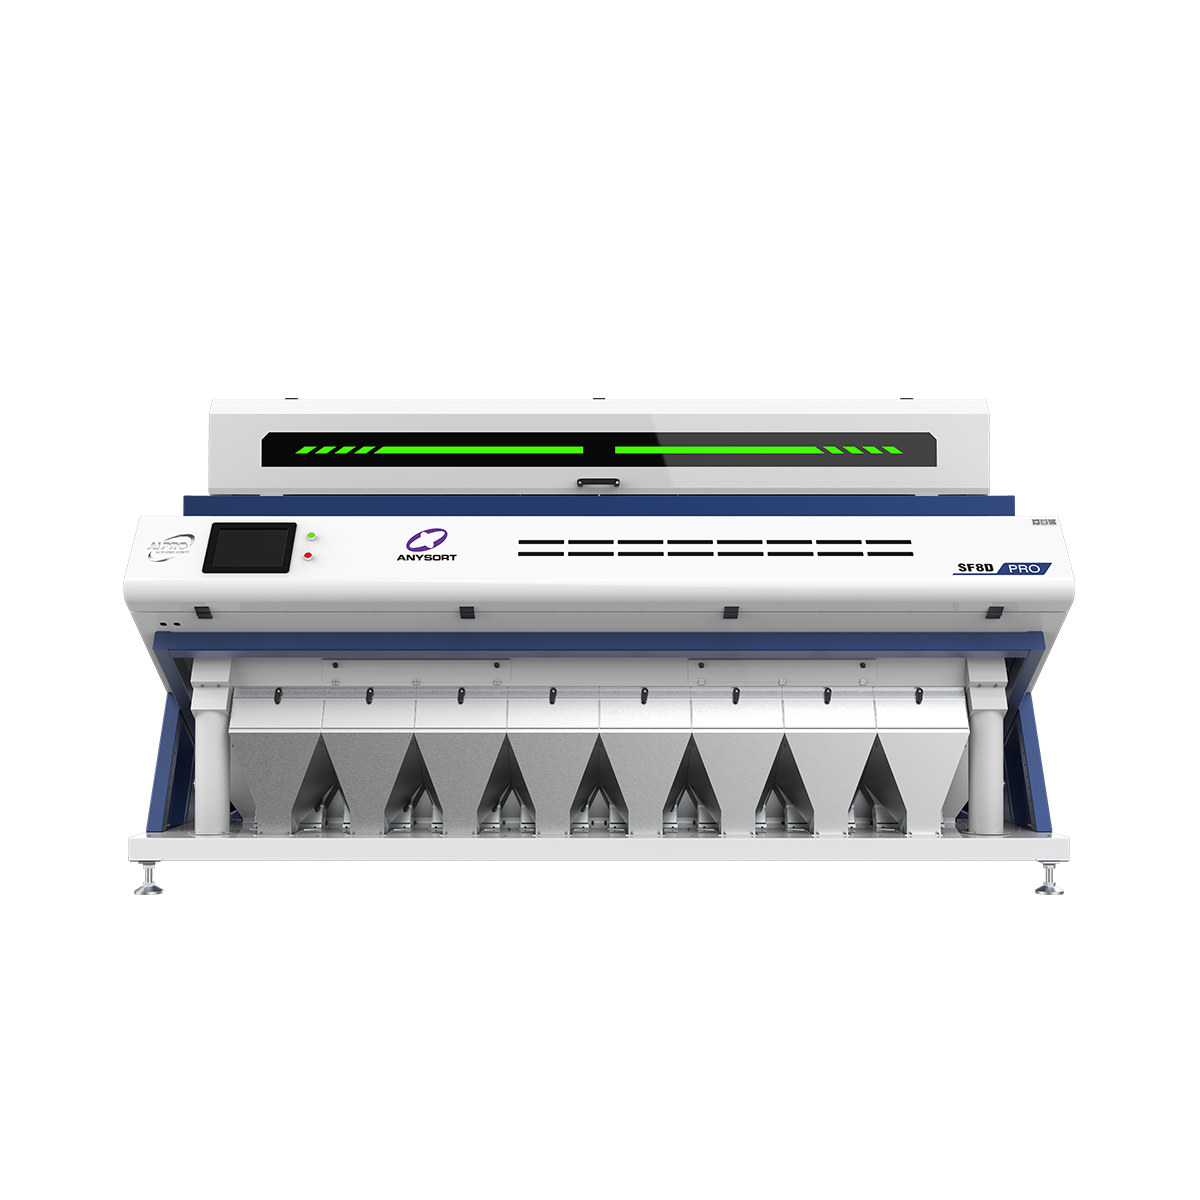
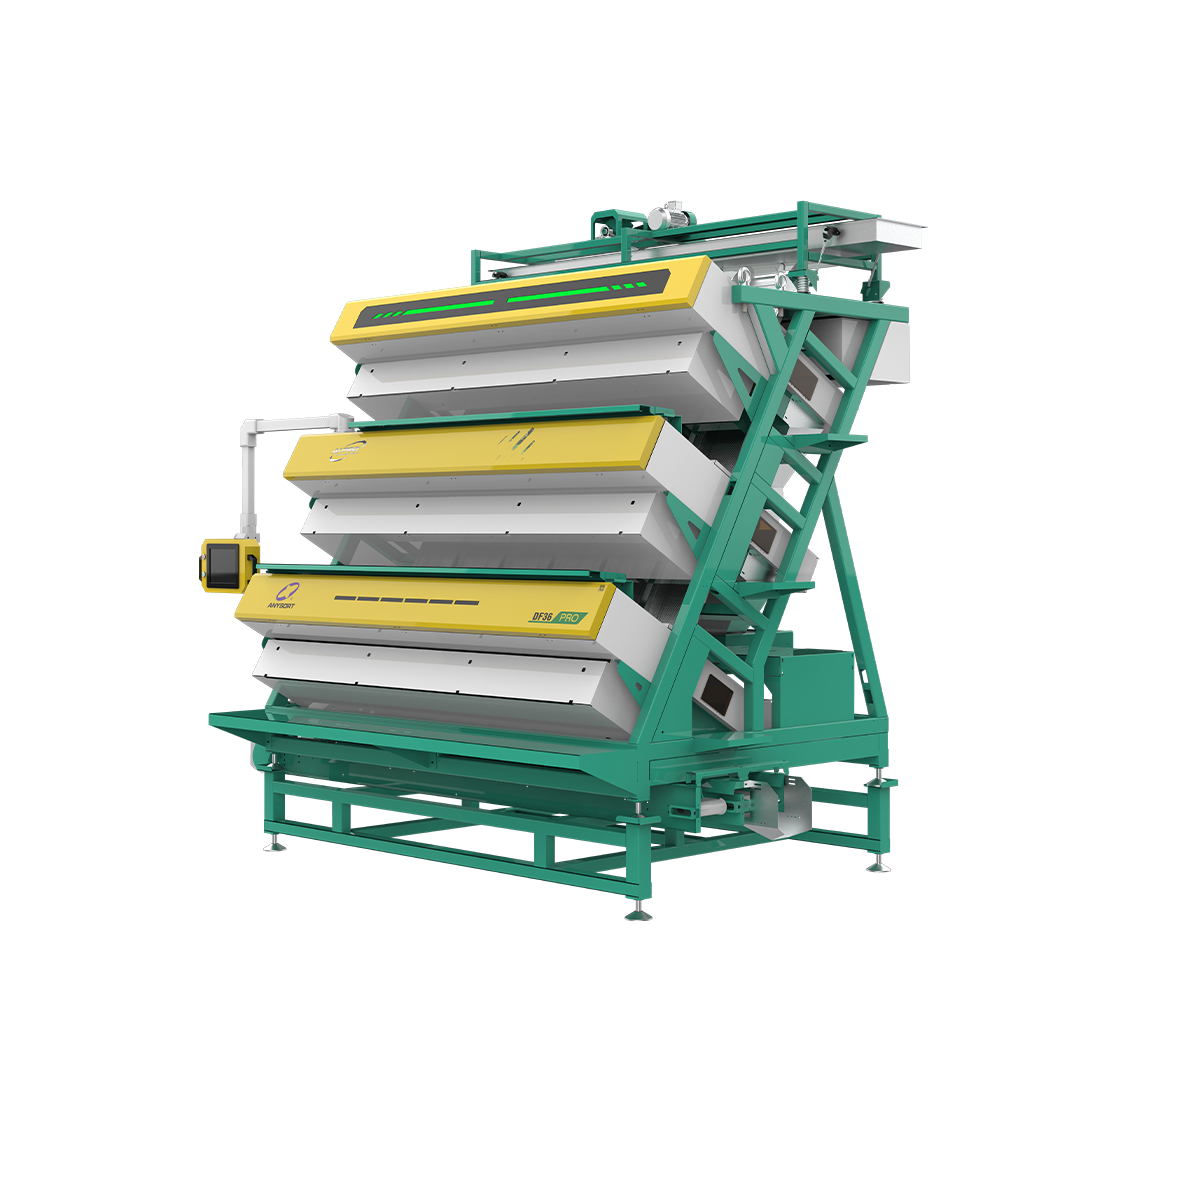
A color sorter factory represents a modern facility dedicated to manufacturing advanced optical sorting equipment designed to separate materials based on color, density, and composition. The color sorter factory produces machines that utilize sophisticated imaging technology to identify and categorize items with exceptional precision. These facilities employ cutting-edge vision systems, LED lighting, and high-speed cameras to analyze materials in real-time, ensuring accurate sorting across various industries.
The primary function of a color sorter factory involves engineering and assembling sorting machines that handle diverse materials including grains, seeds, plastics, minerals, and recycled products. Each color sorter factory designs equipment capable of processing hundreds of tons daily while maintaining quality standards that manual sorting cannot achieve. The technological features integrated into products from a color sorter factory include artificial intelligence algorithms, multi-spectral imaging, and automated ejection systems that remove defective items instantly.
Applications for equipment produced by a color sorter factory span agricultural processing, food manufacturing, recycling facilities, and mineral processing industries. A professional color sorter factory combines hardware expertise with software development to create comprehensive sorting solutions. The equipment manufactured by each color sorter factory enables businesses to improve product quality, reduce waste, and increase operational efficiency. Modern color sorter factory innovations continue evolving, incorporating machine learning and cloud connectivity for enhanced performance monitoring and data analytics capabilities.

 EN