color sorter machine manufacturers
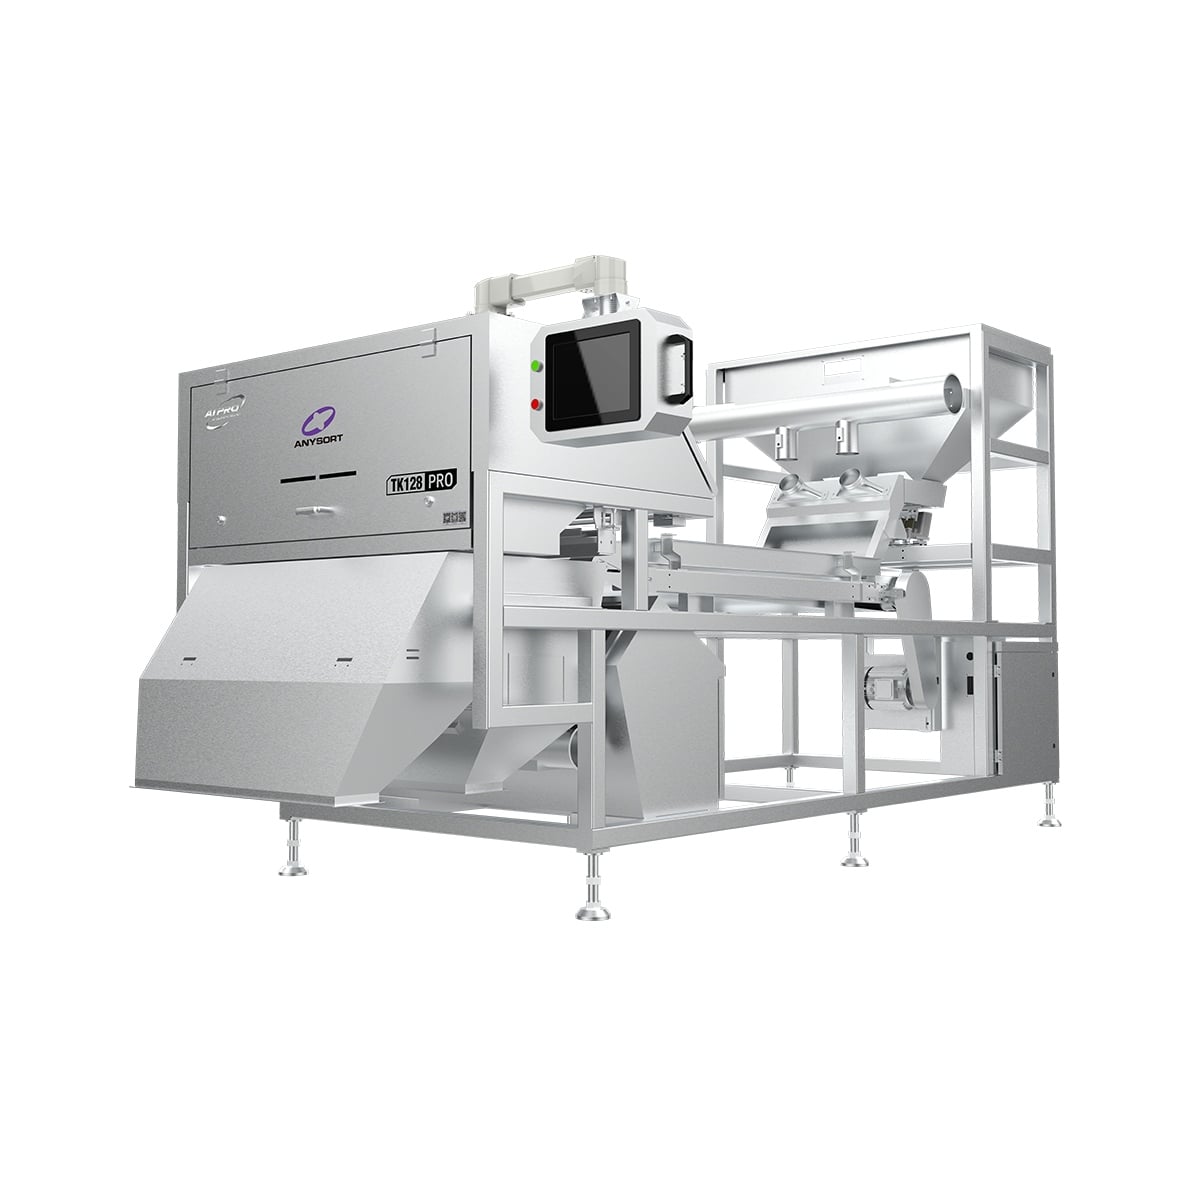
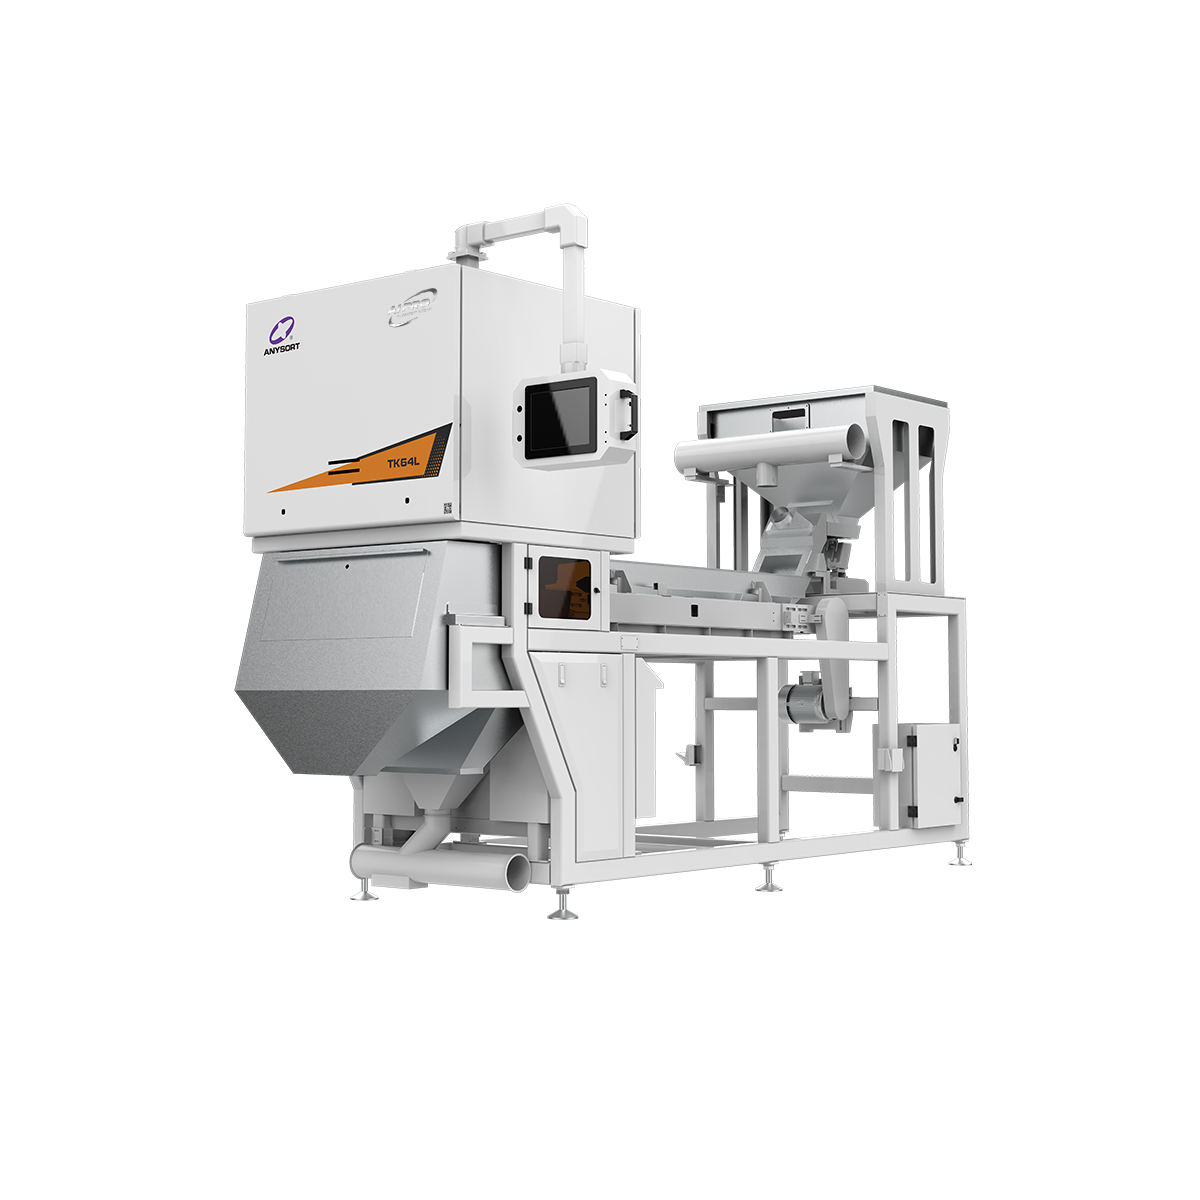
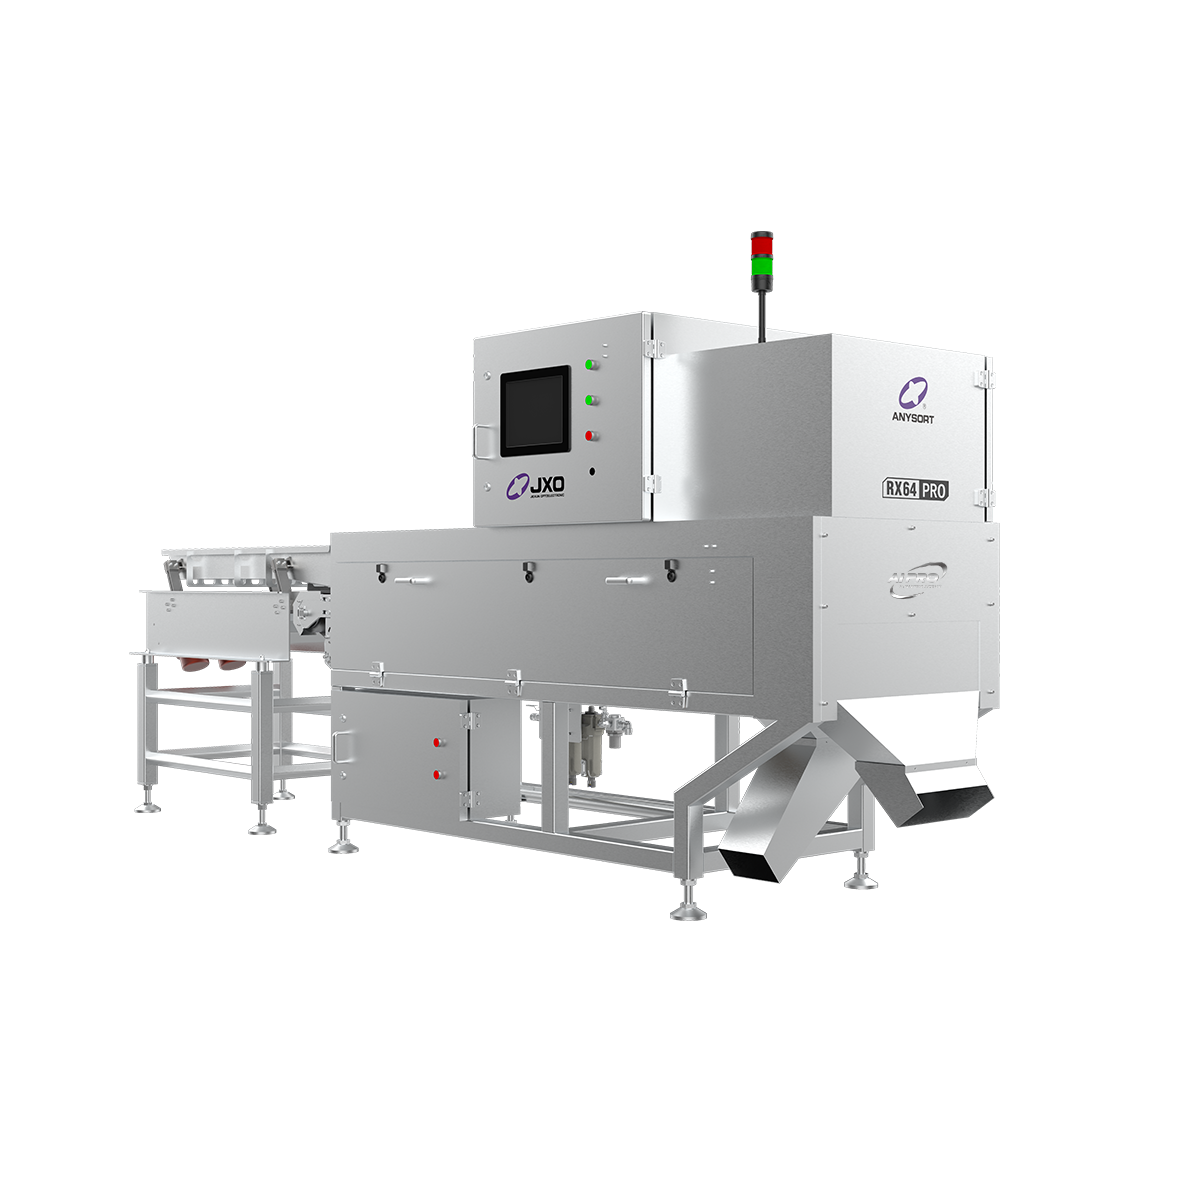
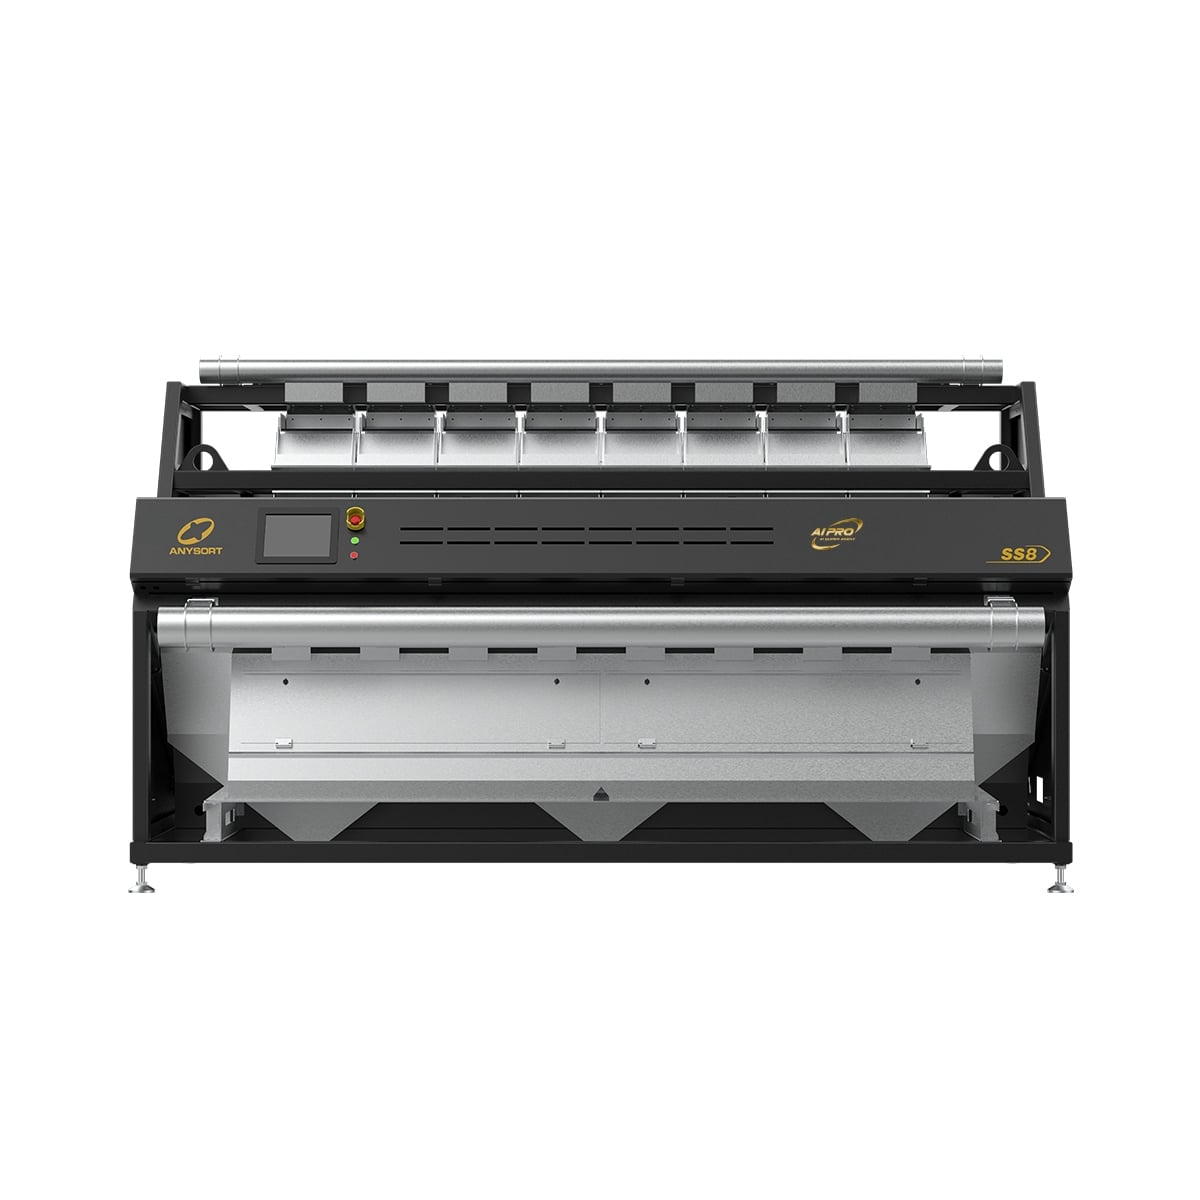
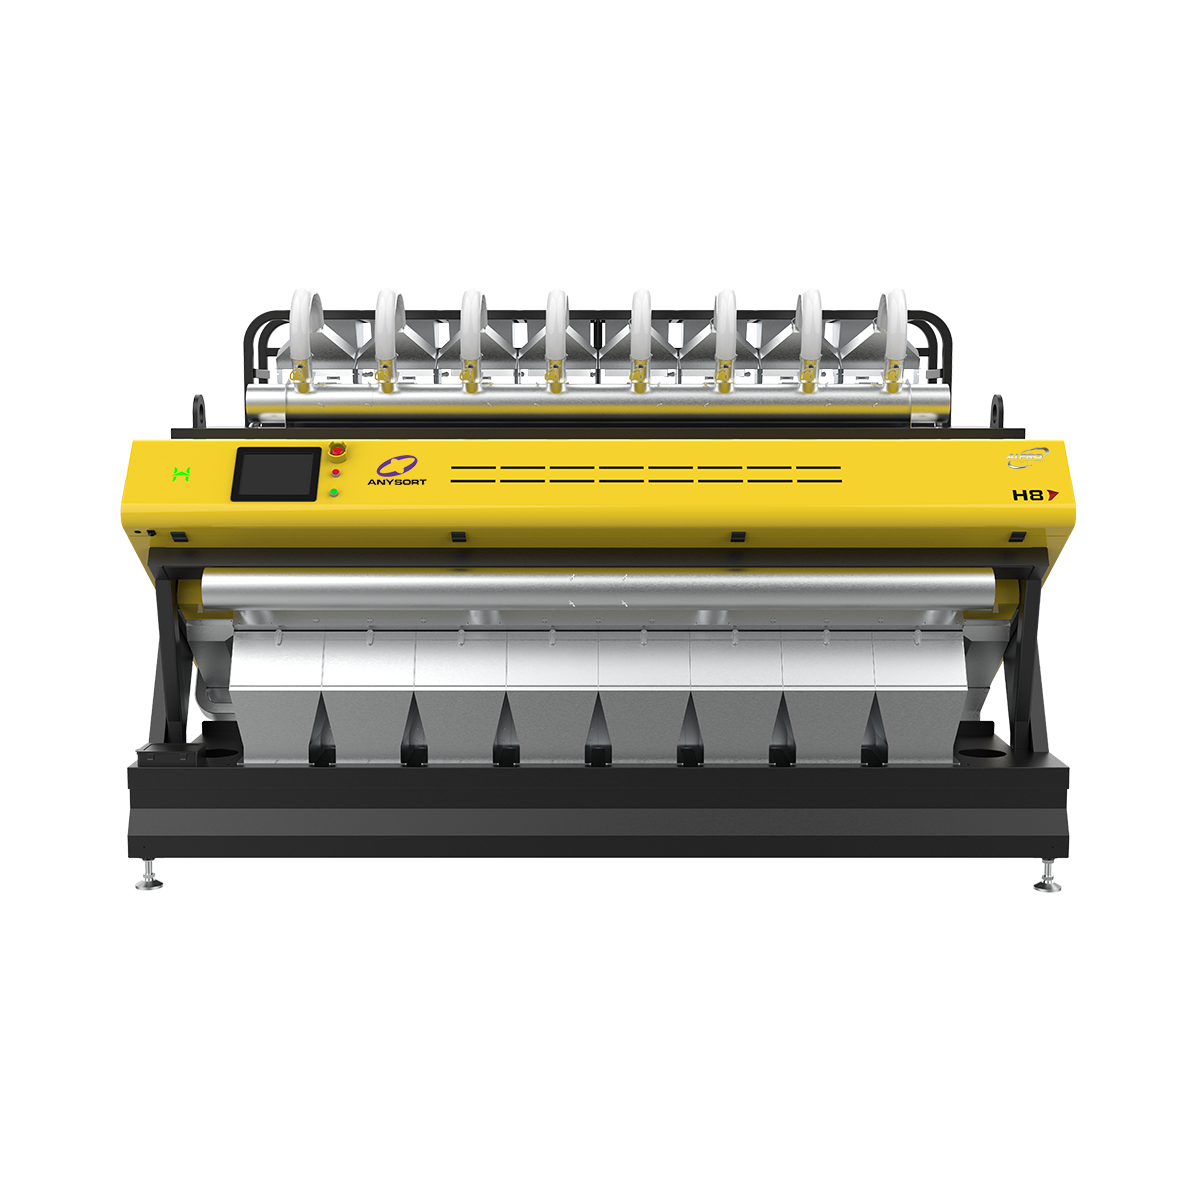
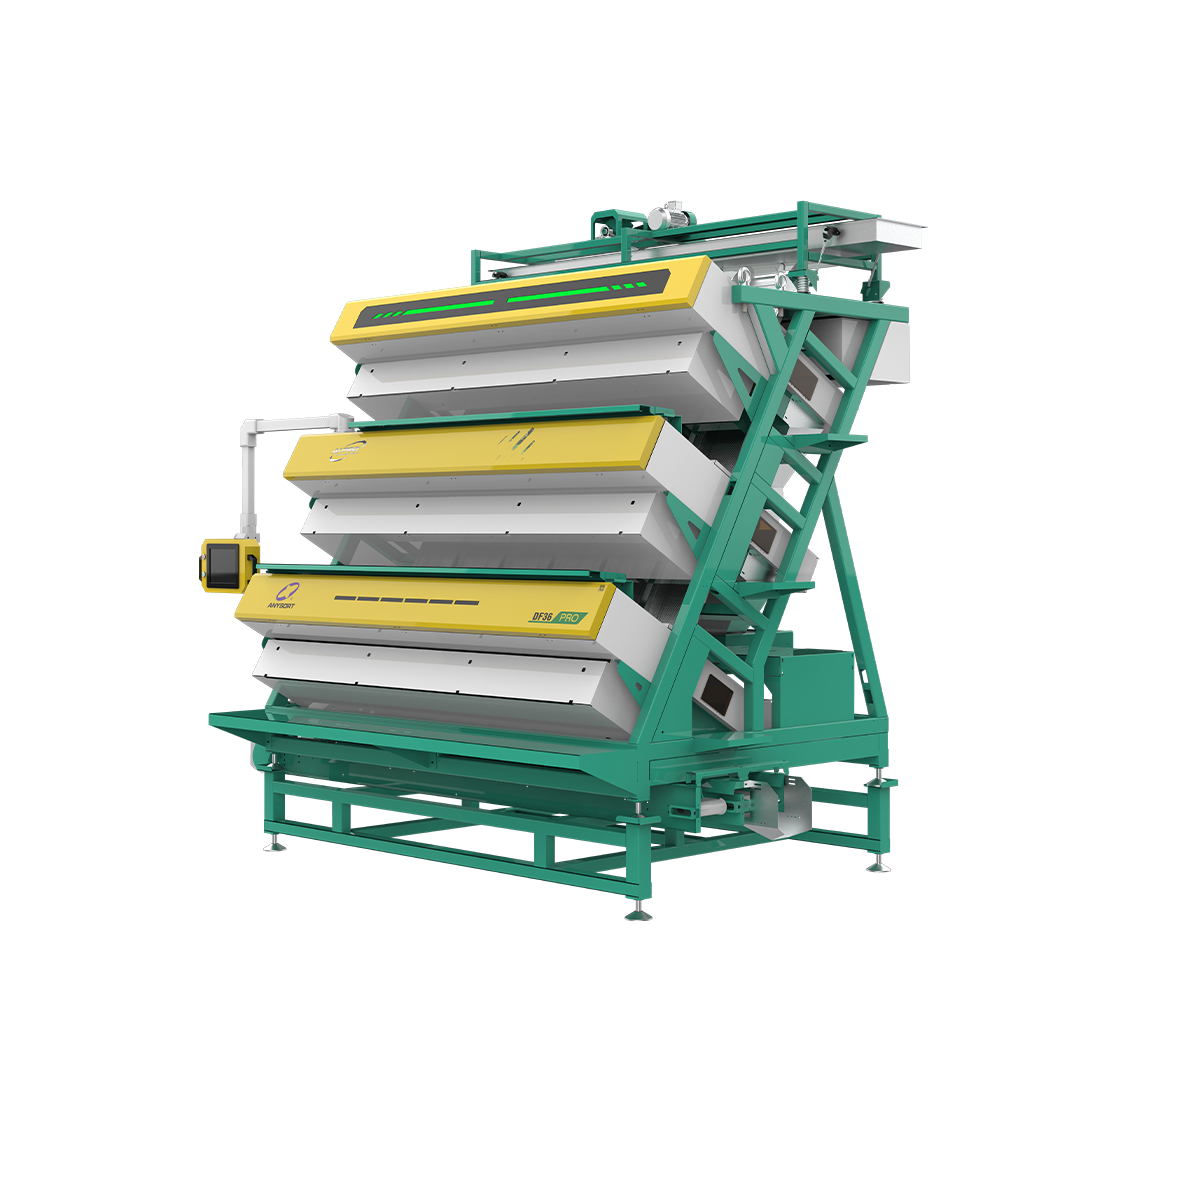
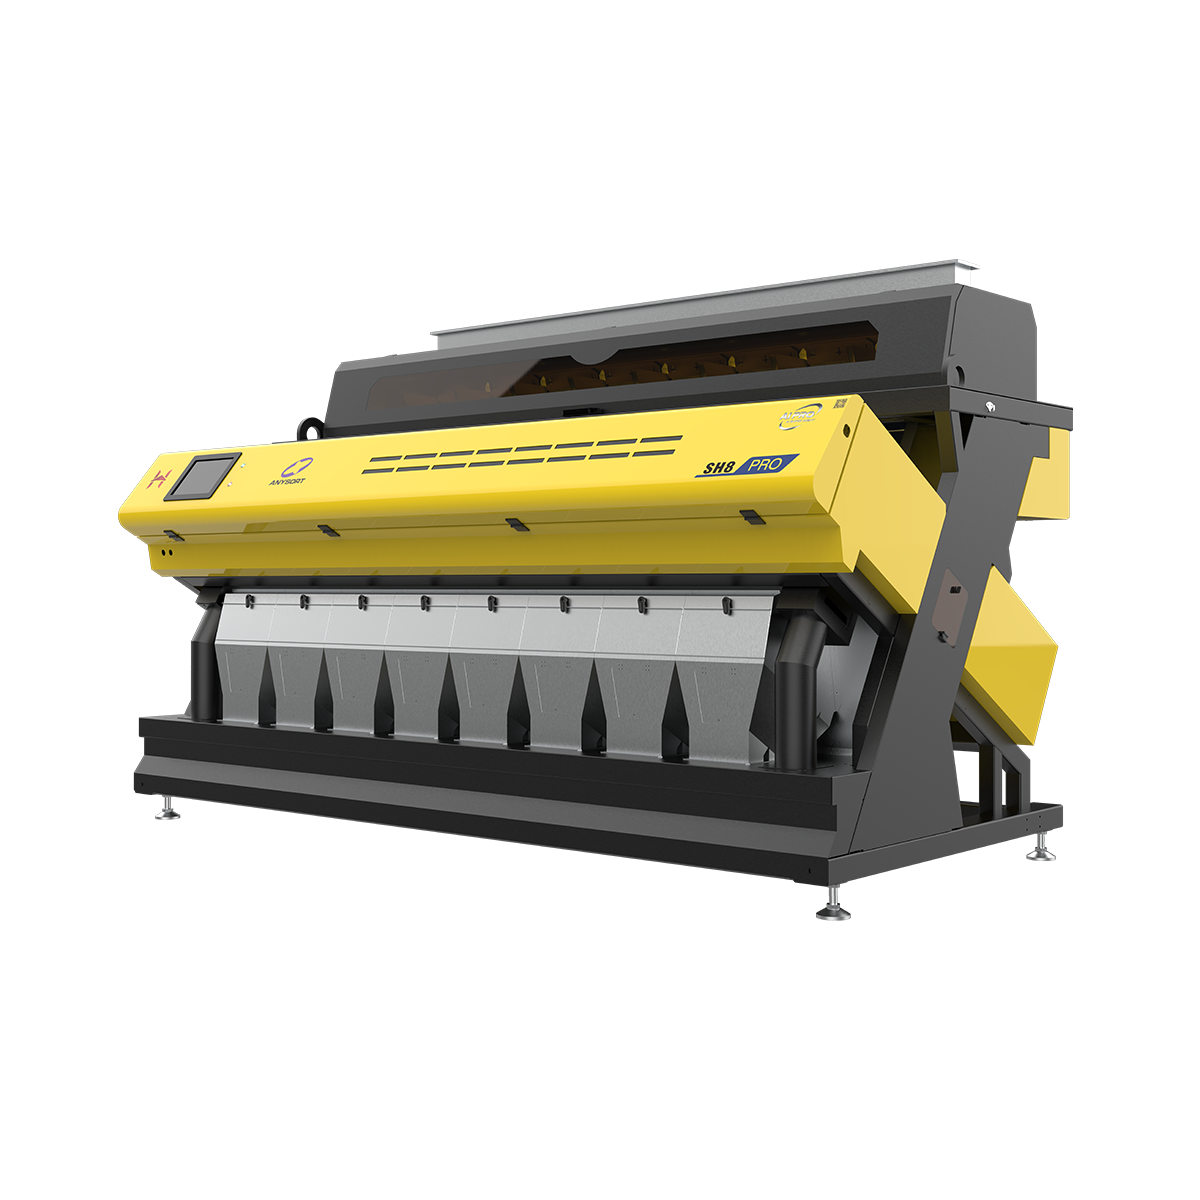
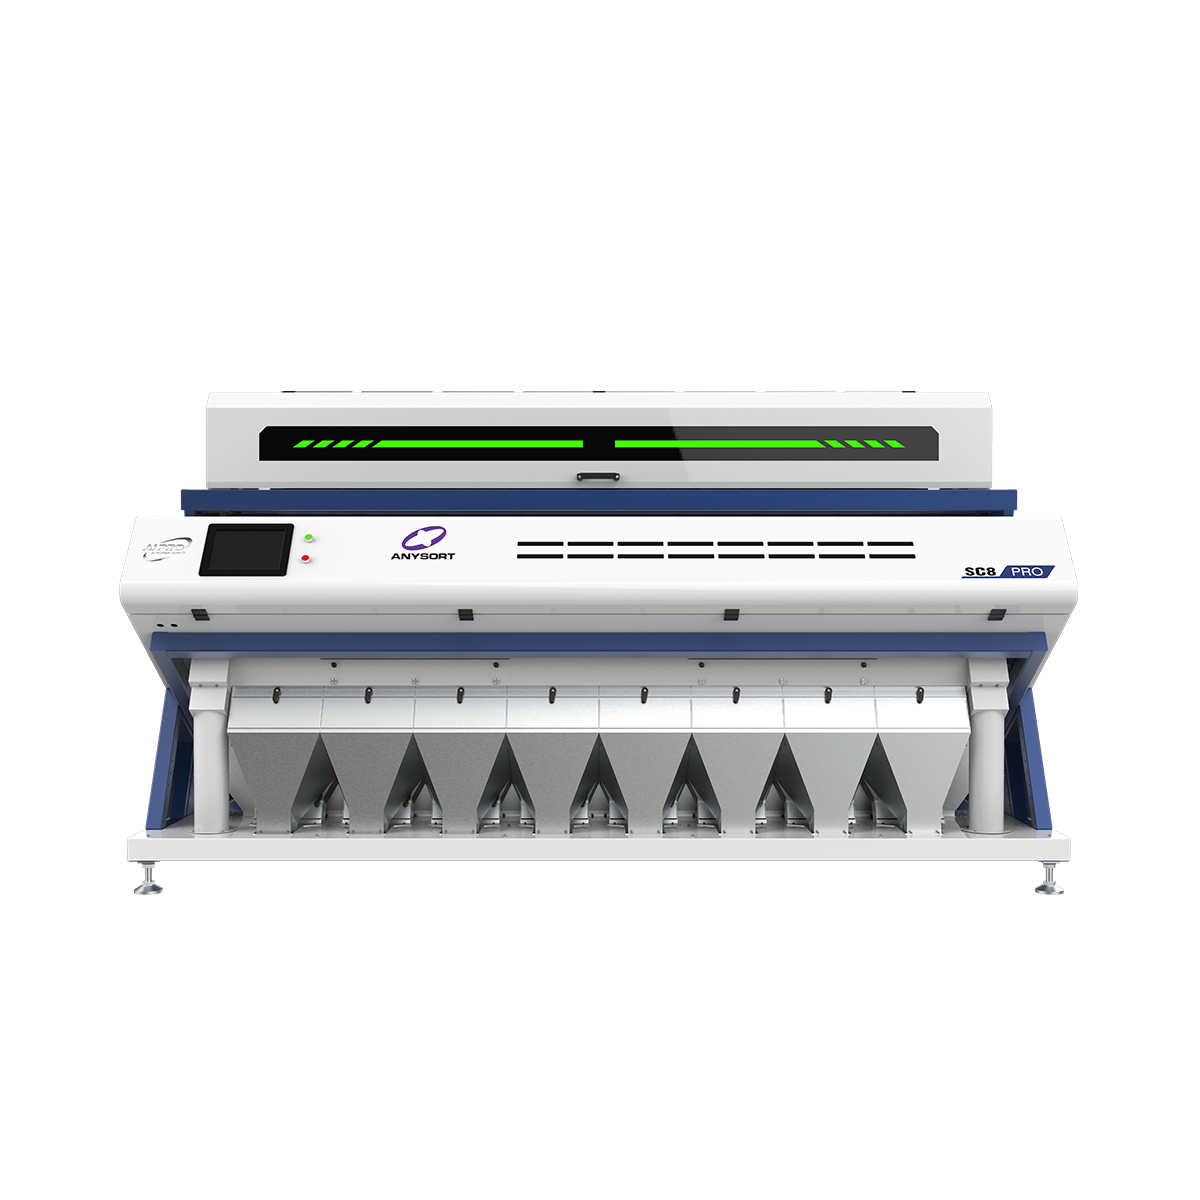
Color sorter machine manufacturers design and produce advanced optical sorting equipment that revolutionizes material processing across multiple industries. These sophisticated machines utilize cutting-edge technology to identify, separate, and sort materials based on color, shape, and quality characteristics with remarkable precision. Color sorter machine manufacturers create solutions that automate quality control processes, significantly reducing manual labor while improving accuracy and consistency.
The primary function of machines from color sorter machine manufacturers involves scanning materials at high speeds using multi-spectral cameras and advanced sensors. These systems can process thousands of items per minute, making real-time sorting decisions based on programmed specifications. Color sorter machine manufacturers equip their equipment with intelligent algorithms that distinguish between acceptable products and defects, contaminated items, or materials requiring rework.
Key technological features include LED lighting systems, powerful processing units, and precision air-jet ejection mechanisms. Color sorter machine manufacturers integrate machine learning capabilities that continuously improve sorting accuracy over time. Applications span from agricultural commodity sorting, including grains and legumes, to plastic recycling operations and food processing industries.
Color sorter machine manufacturers focus on durability, reliability, and user-friendly interfaces that require minimal training. Modern machines feature touchscreen controls, data logging capabilities, and remote monitoring options. These systems operate continuously in demanding environments, delivering exceptional performance and reducing operational downtime. By partnering with leading color sorter machine manufacturers, businesses gain access to proven technology that increases productivity and profitability while maintaining stringent quality standards.

 EN