Cashew Color Sorting Machine

All Categories

cashew color sorting machine

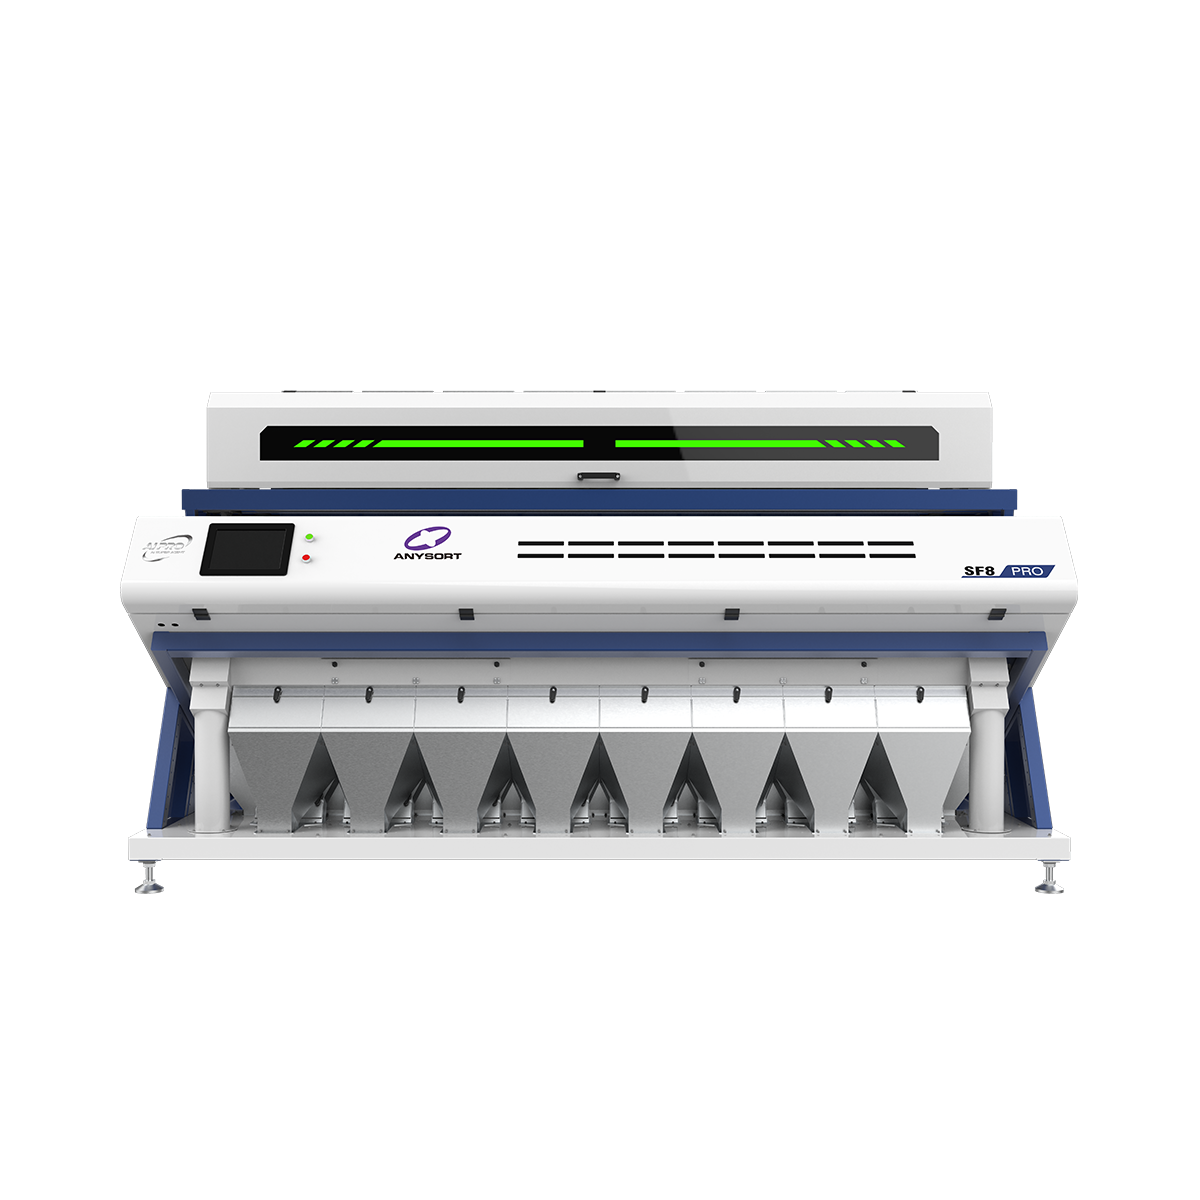
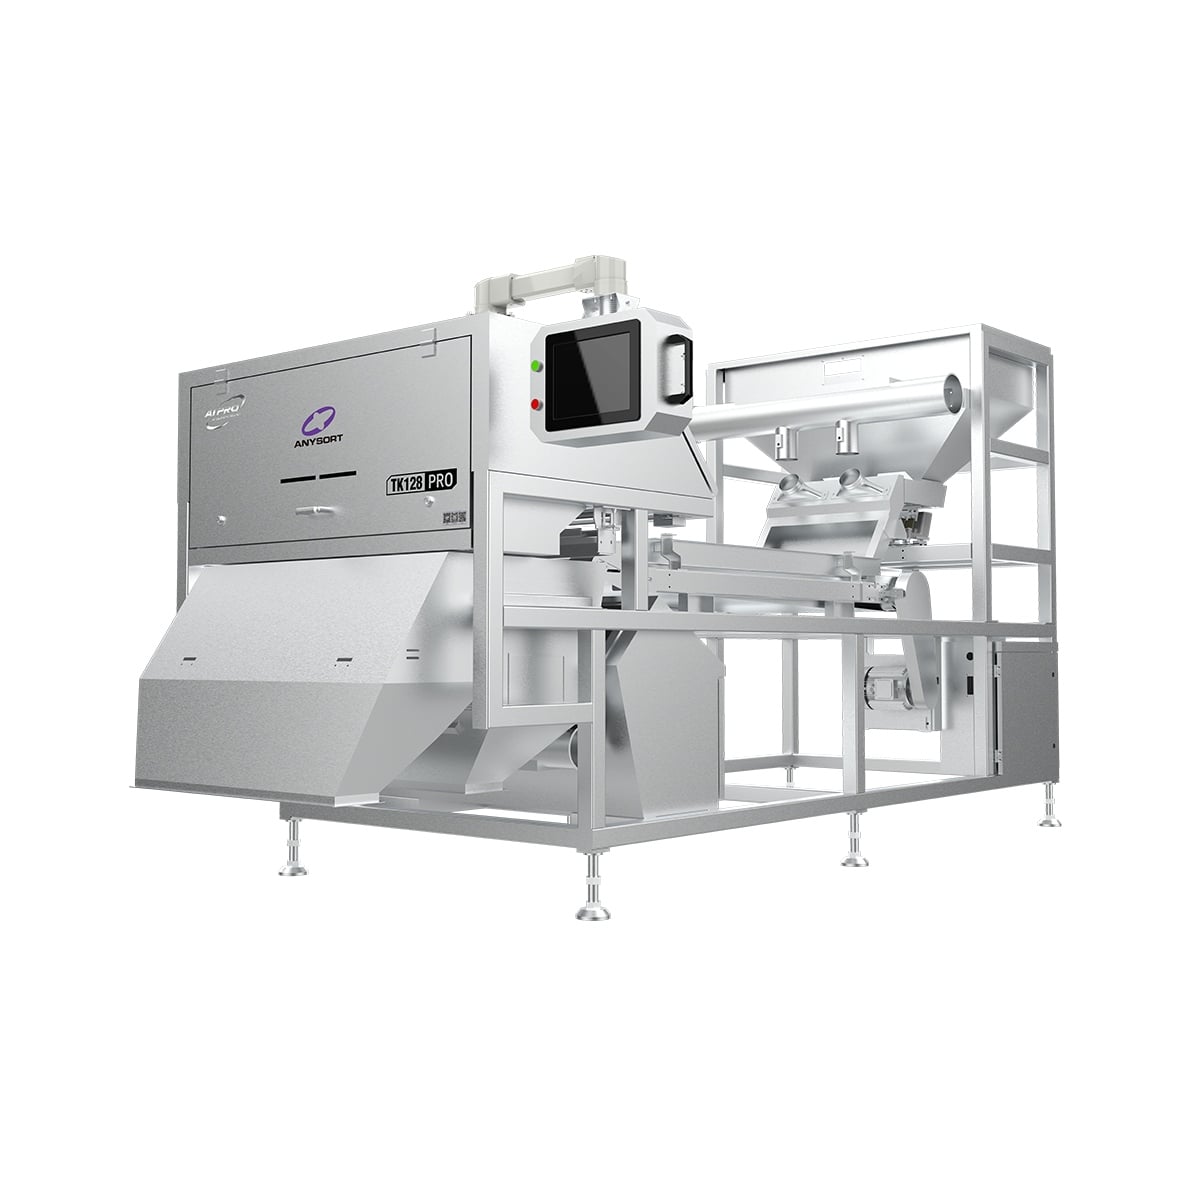
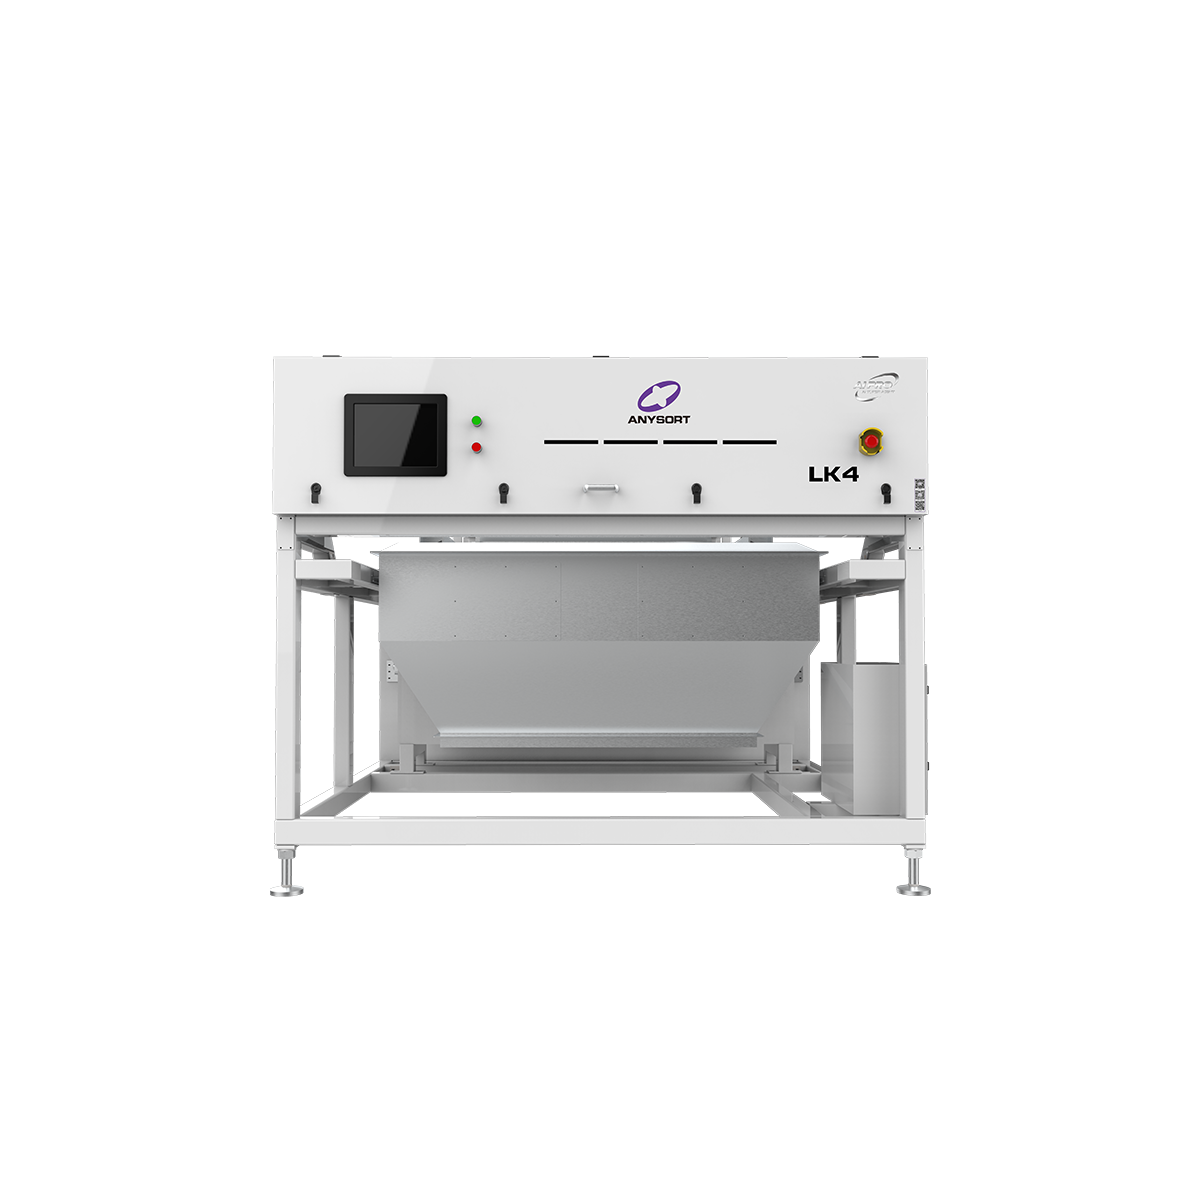
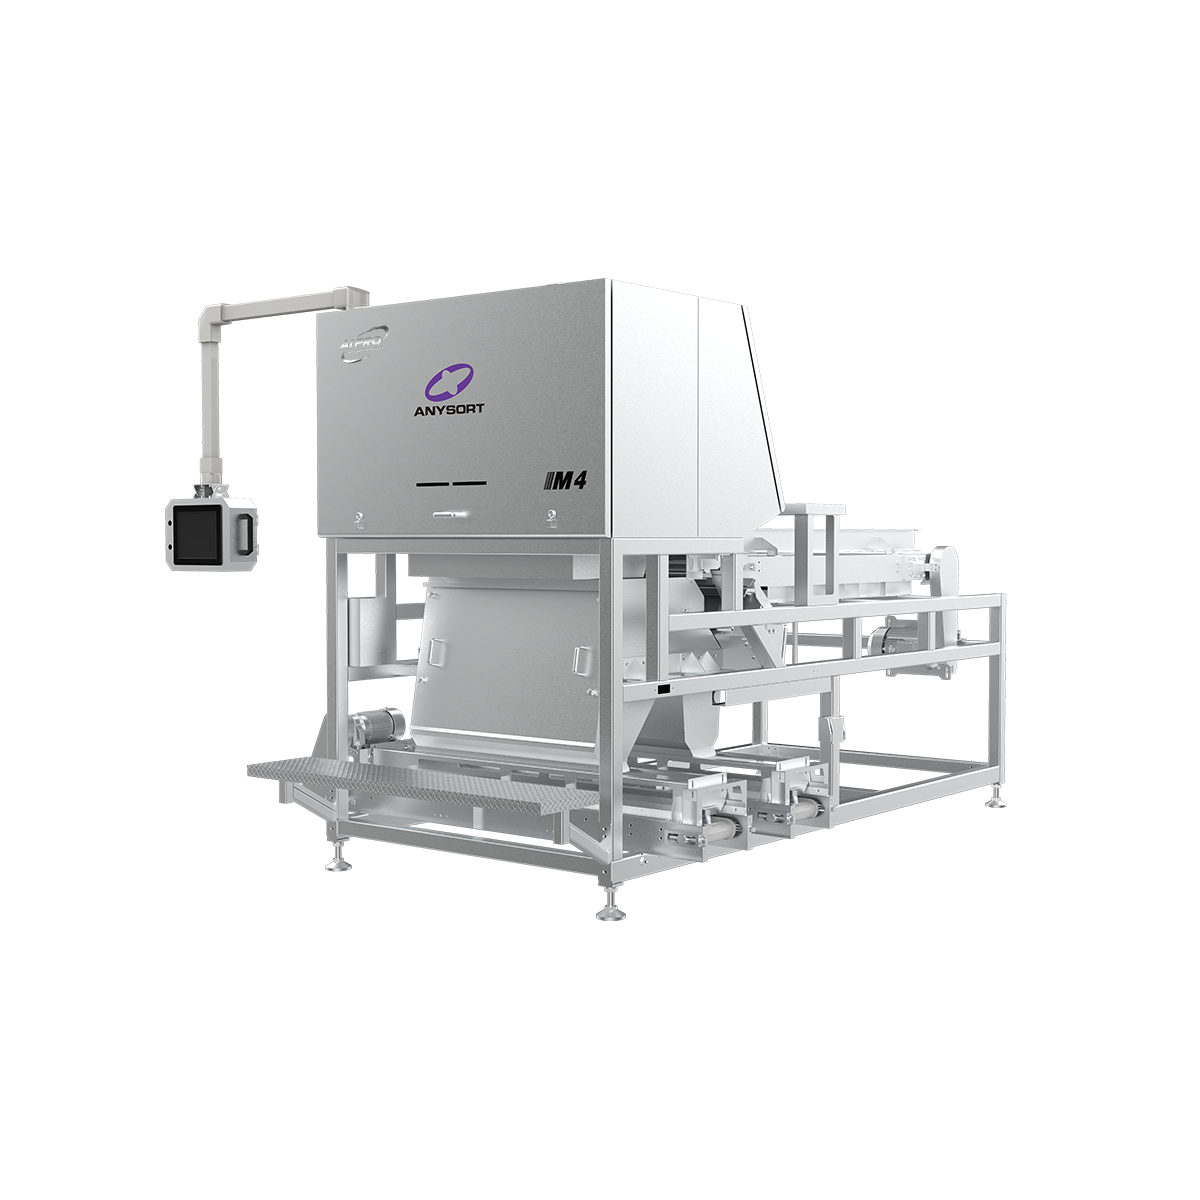
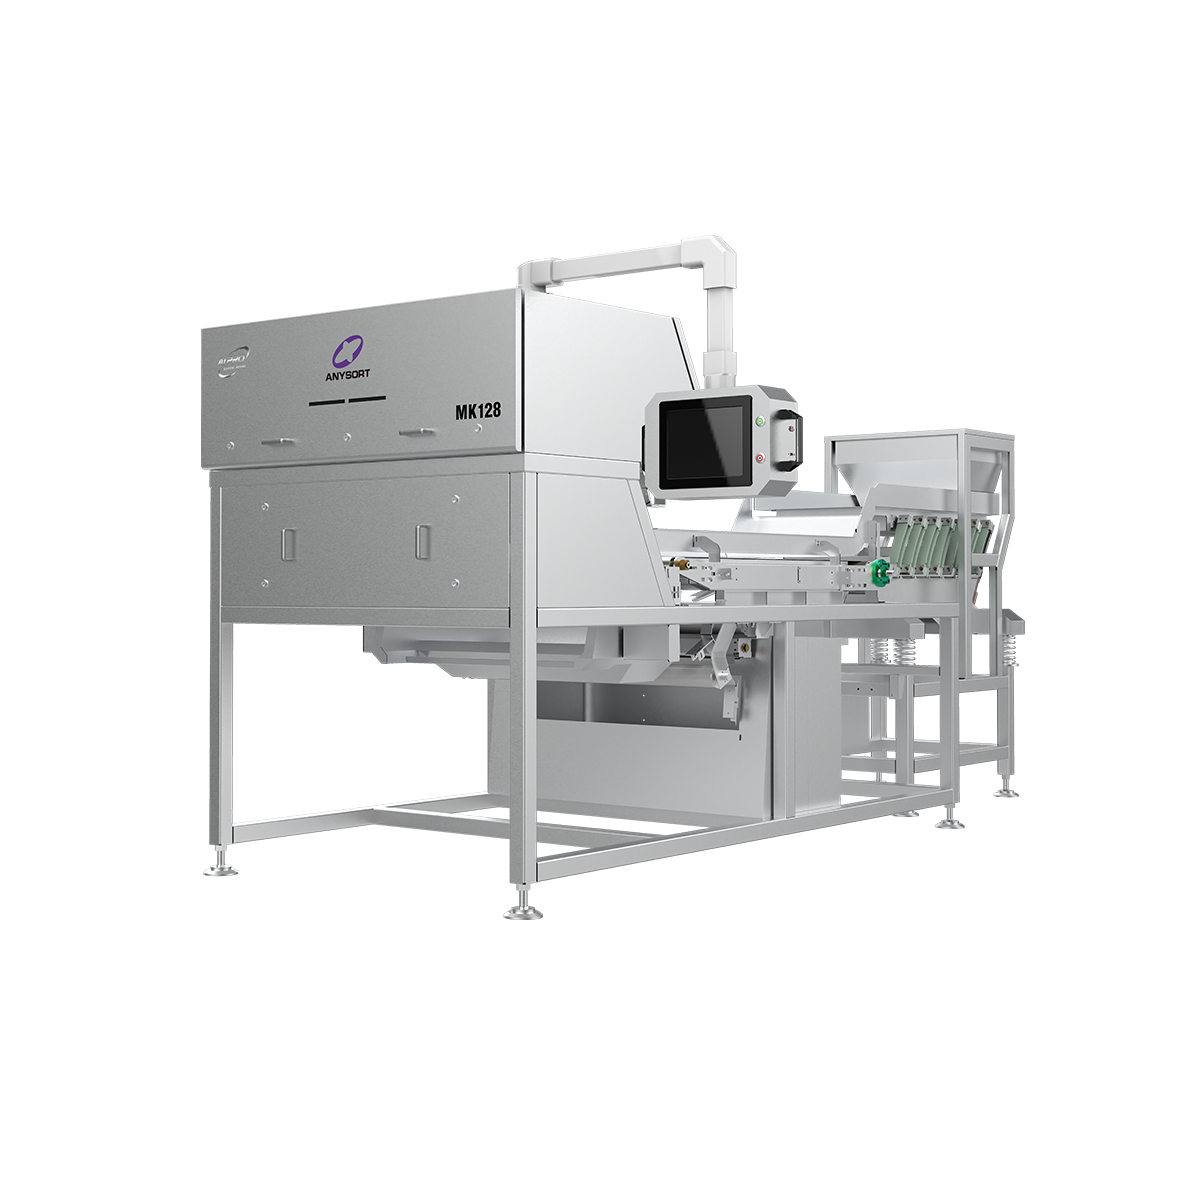
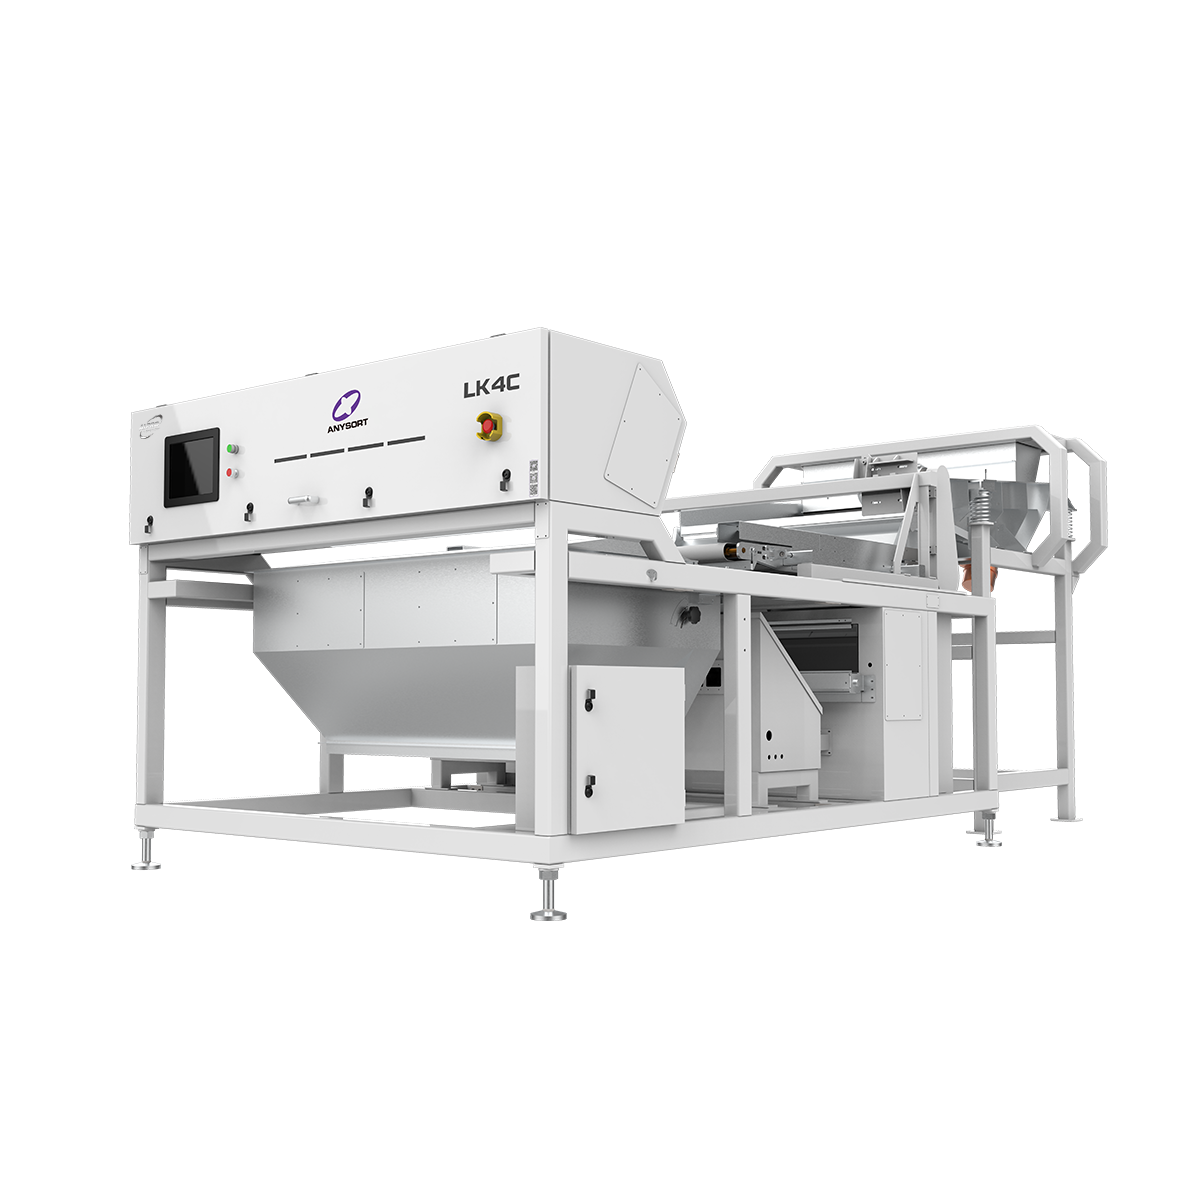
A cashew color sorting machine is an advanced optical inspection system designed to automatically classify and separate cashew nuts based on color, size, and quality characteristics. This innovative equipment represents a significant technological advancement in cashew processing, enabling producers to achieve consistent product quality and maximize yield efficiency. The cashew color sorting machine utilizes sophisticated camera technology and artificial intelligence algorithms to detect subtle color variations that human operators might miss, ensuring precise sorting of raw and roasted cashews into predefined grades. The primary function of a cashew color sorting machine is to streamline the post-harvest processing stage by eliminating defective, discolored, or substandard nuts from premium batches. Modern cashew color sorting machines feature multi-spectral imaging capabilities that capture detailed information about each nut's surface characteristics. The system processes thousands of nuts per minute, making it ideal for large-scale commercial operations. Advanced sensors within the cashew color sorting machine analyze color intensity, uniformity, and potential defects with remarkable precision. Technologically, these machines incorporate belt conveyor systems, high-resolution cameras, sophisticated sorting algorithms, and pneumatic rejection mechanisms. The cashew color sorting machine connects seamlessly to existing production lines and provides real-time data visualization through user-friendly interfaces. Processing speeds typically range from 500 to 2000 kilograms per hour, depending on the specific model. Applications span across major cashew-producing regions worldwide, including India, Vietnam, and African nations, where producers depend on this technology for competitive market positioning and quality assurance.

New Product Recommendations

The cashew color sorting machine delivers substantial operational and financial advantages to cashew processing facilities worldwide. First, it dramatically improves product consistency and market quality. By automatically removing discolored, moldy, or damaged nuts, the cashew color sorting machine ensures that only premium-grade cashews reach retail channels, significantly enhancing brand reputation and customer satisfaction. This consistency directly translates to higher market prices and increased customer loyalty. Operationally, a cashew color sorting machine reduces labor costs substantially by replacing manual sorting crews. Traditional hand-sorting processes require numerous workers, incurring significant payroll expenses and facing availability challenges. The cashew color sorting machine operates continuously without fatigue, maintaining consistent sorting accuracy throughout extended production cycles. This automation increases throughput efficiency by up to three times compared to manual methods, allowing facilities to process larger volumes with fewer staff members. The economic benefits extend beyond labor savings. By maximizing the yield of premium-grade cashews, the cashew color sorting machine increases profitability per ton processed. Reduction of waste and improved grading accuracy mean more nuts qualify for higher-value market segments. The machine's data-tracking capabilities provide detailed sorting reports, enabling producers to identify trends, optimize processing parameters, and make informed business decisions. For facility managers and quality control teams, the cashew color sorting machine offers valuable transparency. Real-time monitoring systems display sorting metrics, rejection rates, and product flow information, facilitating better inventory management. The standardized sorting criteria eliminate subjective decision-making inherent in manual processes. Additionally, compliance with international quality standards becomes significantly easier when sorting is performed consistently by technology rather than human judgment. These practical benefits make the cashew color sorting machine an essential investment for competitive cashew processors.

Tips And Tricks

How to Choose the Right Tea Color Sorter for Your Needs?

01

Aug

How to Choose the Right Tea Color Sorter for Your Needs?

Selecting the right tea color sorter is one of the most critical decisions tea processors face when modernizing their operations. A tea color sorter directly impacts product quality, operational efficiency, and market competitiveness. The wrong choic...
View More
How can rice color sorters improve grain quality?

08

Aug

How can rice color sorters improve grain quality?

Rice color sorters represent a transformative technology in modern grain processing, fundamentally changing how producers maintain and enhance the quality of their rice output. By utilizing advanced optical scanning and artificial intelligence, a ric...
View More
How Can a Nuts Sorter Improve Your Production?

15

Aug

How Can a Nuts Sorter Improve Your Production?

A nuts sorter represents one of the most significant investments a food processing operation can make to enhance production quality and operational efficiency. The modern nuts sorter uses advanced imaging and sensor technology to identify and separat...
View More
How does optical sorting technology detect defective rice grains?

22

Aug

How does optical sorting technology detect defective rice grains?

Modern rice processing demands precision and consistency, which is why understanding the detection mechanisms behind advanced equipment has become essential for producers. A rice color sorter represents one of the most significant technological break...
View More

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

cashew color sorting machine

Precision Color Detection Technology

Precision Color Detection Technology

The cashew color sorting machine employs cutting-edge multi-spectral imaging sensors capable of detecting minute color variations invisible to the human eye. This advanced optical technology captures data across multiple wavelength ranges, enabling the machine to distinguish between acceptable color variations and quality defects. The precision color detection system ensures that each nut is evaluated against customizable color standards, guaranteeing consistent grading. By utilizing real-time image processing algorithms, the cashew color sorting machine analyzes thousands of nuts per minute without compromising accuracy. This technological capability means that subtle defects such as mold spots, discoloration, and surface irregularities are captured and rejected automatically. Producers benefit from uniform product quality that meets strict international export standards. The cashew color sorting machine's precision eliminates the variability associated with manual sorting, ensuring every processed batch meets the highest quality benchmarks. This consistent excellence strengthens market position and customer confidence.
High-Speed Processing and Increased Throughput

High-Speed Processing and Increased Throughput

Modern cashew color sorting machines deliver exceptional processing speeds, handling 500 to 2000 kilograms of cashews per hour depending on the specific model and configuration. This high-speed capability enables processors to significantly increase production volume without expanding facility infrastructure or workforce. The efficient conveyor system ensures smooth nut flow throughout the sorting process, preventing jams and bottlenecks that characterize manual sorting operations. A cashew color sorting machine can process in one hour what requires an entire team of workers to accomplish manually during a full shift. This dramatic throughput improvement directly enhances facility profitability by maximizing equipment utilization and reducing processing costs per kilogram. For large-scale operations, multiple cashew color sorting machines can be integrated into comprehensive processing lines, creating automation systems that handle continuous production demands. The speed advantage becomes particularly valuable during peak harvest seasons when processing demands exceed manual sorting capacity. This technological efficiency translates directly to competitive advantages in global cashew markets.
Automated Quality Control and Waste Reduction

Automated Quality Control and Waste Reduction

The cashew color sorting machine incorporates automated rejection mechanisms that remove defective nuts instantly, minimizing waste and maximizing premium-grade yield. Pneumatic or mechanical ejection systems ensure rejected nuts are separated without damaging acceptable products. This automated quality control reduces manual inspection requirements and human error substantially. Every cashew color sorting machine maintains detailed sorting logs and statistical data, providing producers with comprehensive insights into product quality and processing performance. By systematically removing damaged, discolored, and substandard nuts before packaging, the cashew color sorting machine protects brand reputation and prevents customer returns. The significant waste reduction means more marketable product per ton processed, directly improving profitability. Additionally, the cashew color sorting machine enables processors to meet specific market requirements and customer specifications with exceptional consistency. Real-time feedback mechanisms allow operators to adjust sorting parameters based on incoming material characteristics, optimizing yield optimization continuously. This intelligent waste management system positions processors competitively in premium market segments where quality consistency commands premium pricing.

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

Copyright © 2026 Anhui Jiexun Optoelectronic Technology Co., Ltd. All rights reserved.  -  Privacy policy