corn sorting systems
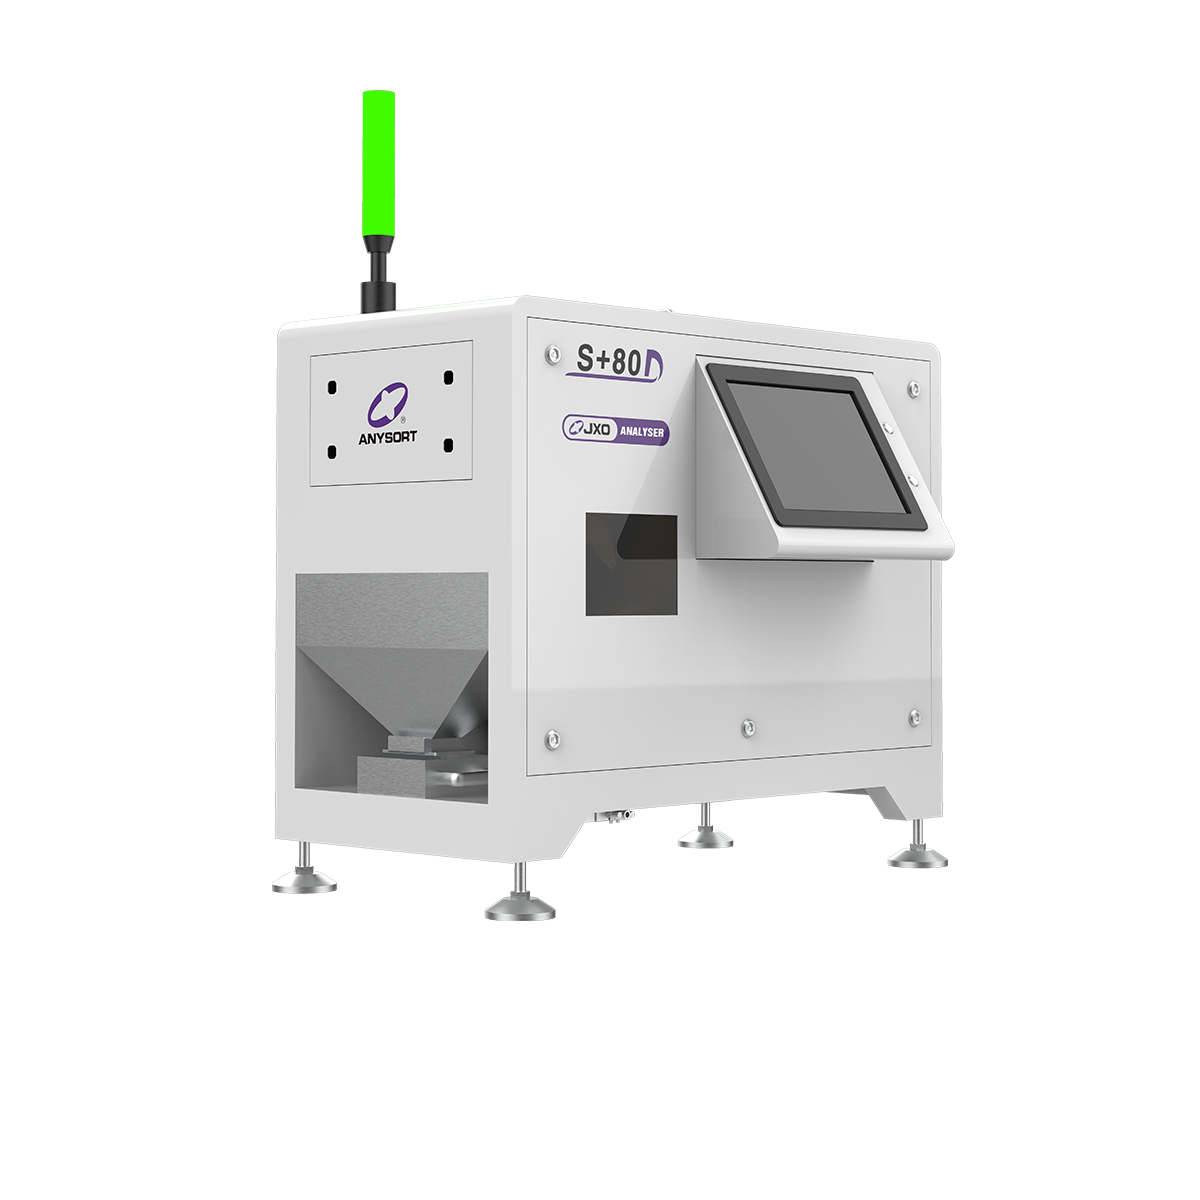
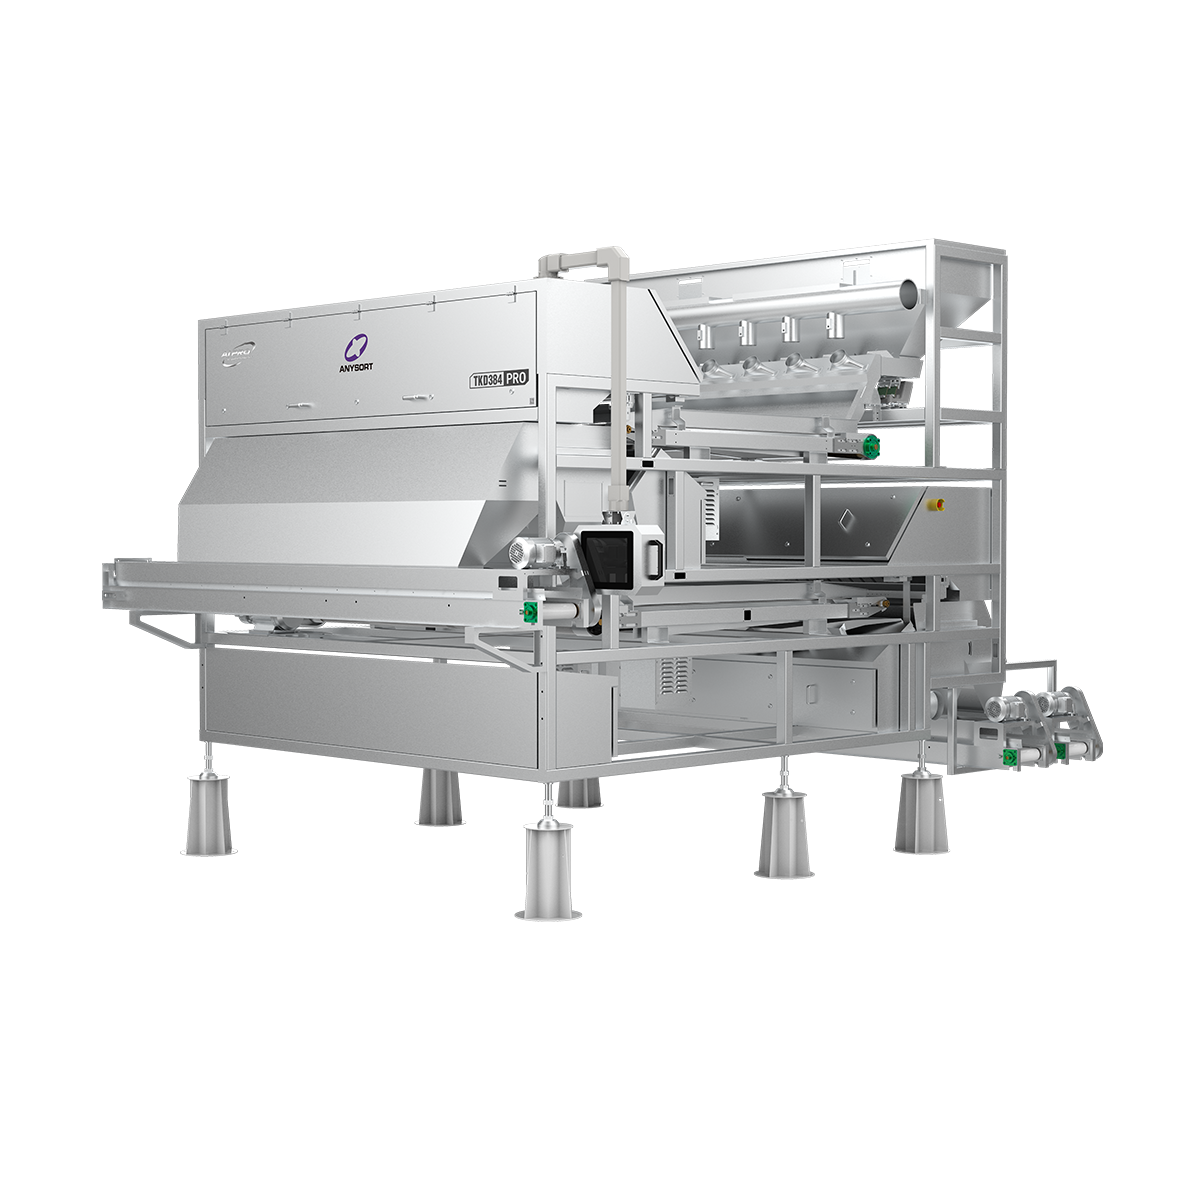
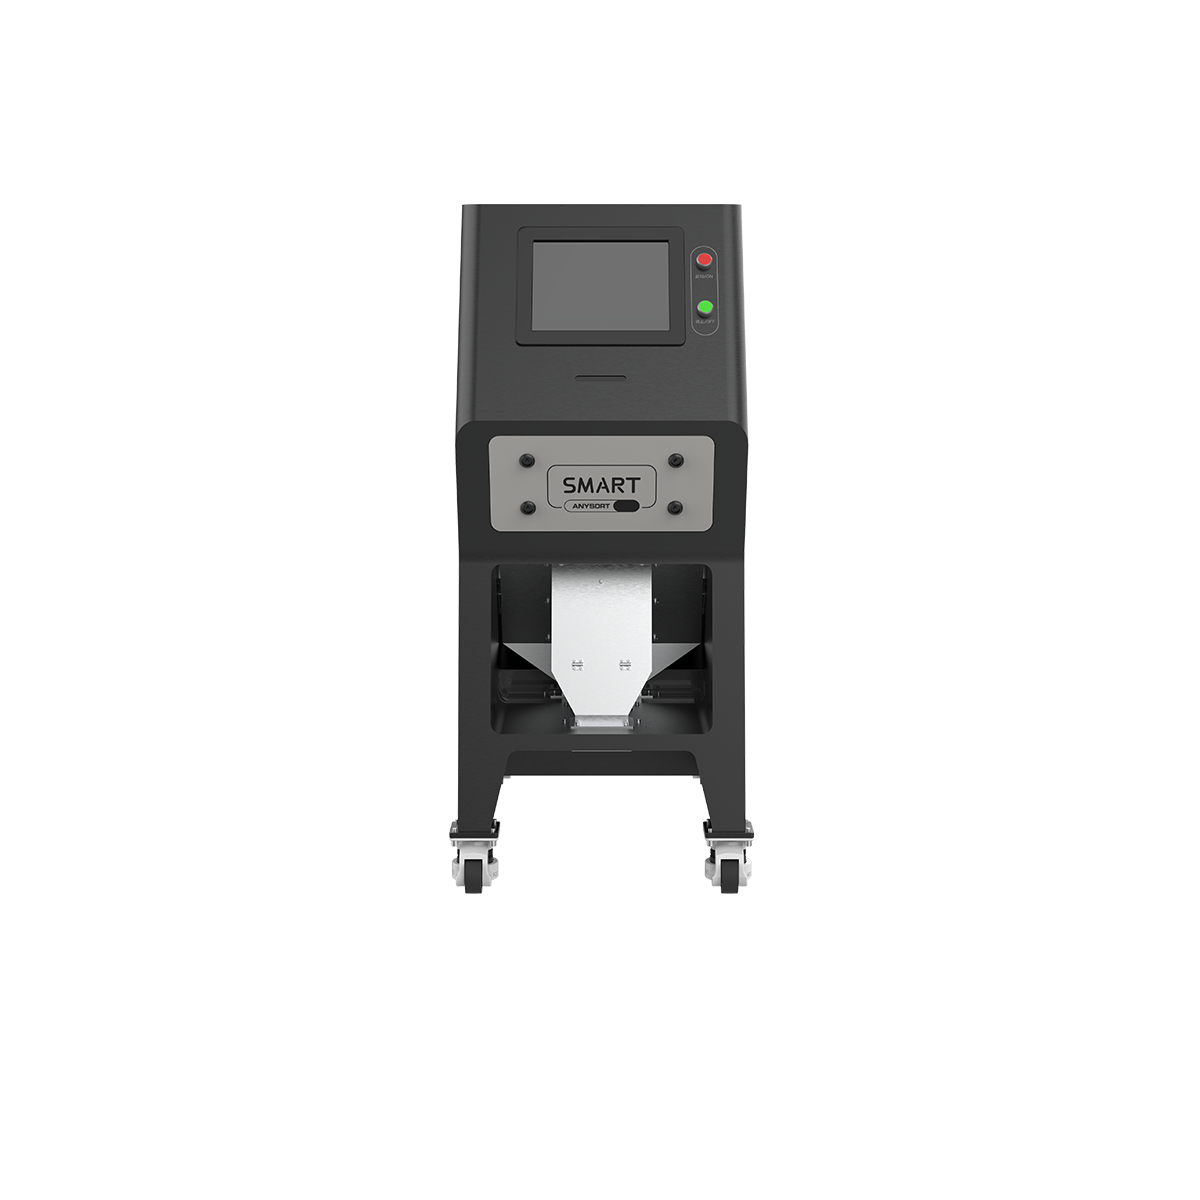
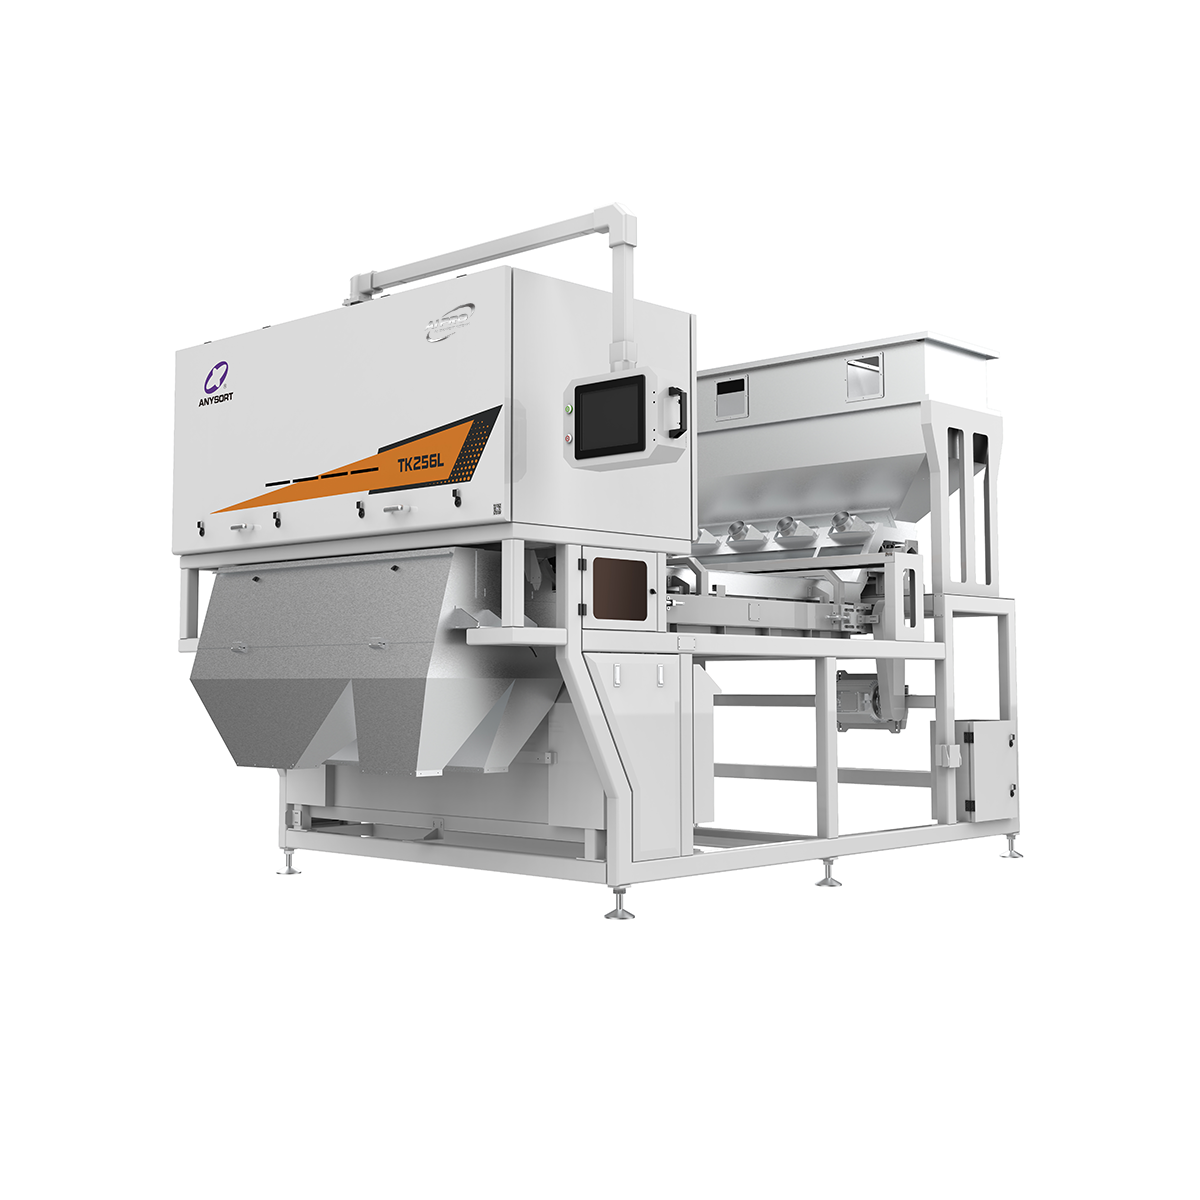
Corn sorting systems represent advanced automated solutions designed to enhance grain quality and operational efficiency in agricultural and food processing facilities. These innovative systems utilize cutting-edge optical scanning technology and artificial intelligence algorithms to identify and separate defective kernels, foreign materials, and discolored corn with exceptional precision. Modern corn sorting systems work by capturing detailed images of each kernel as it passes through the sorting chamber, then using sophisticated image analysis to detect anomalies invisible to the human eye. The primary function of corn sorting systems is to guarantee that only premium-quality corn reaches your end products, whether destined for food production, animal feed, or industrial applications. These systems operate at remarkable speeds, processing thousands of kernels per minute while maintaining consistent accuracy rates exceeding ninety-eight percent. Corn sorting systems integrate seamlessly with existing grain handling infrastructure, requiring minimal modifications to current production lines. The technological features include multi-spectrum cameras, high-speed pneumatic ejection mechanisms, and real-time quality monitoring dashboards that provide operators with comprehensive sorting data. Applications for corn sorting systems span across numerous industries, including food manufacturing, animal feed production, ethanol refineries, and specialty grain processors. By implementing corn sorting systems, facilities significantly reduce waste, improve product consistency, and enhance customer satisfaction while maintaining competitive advantages in today's demanding market landscape.

 EN