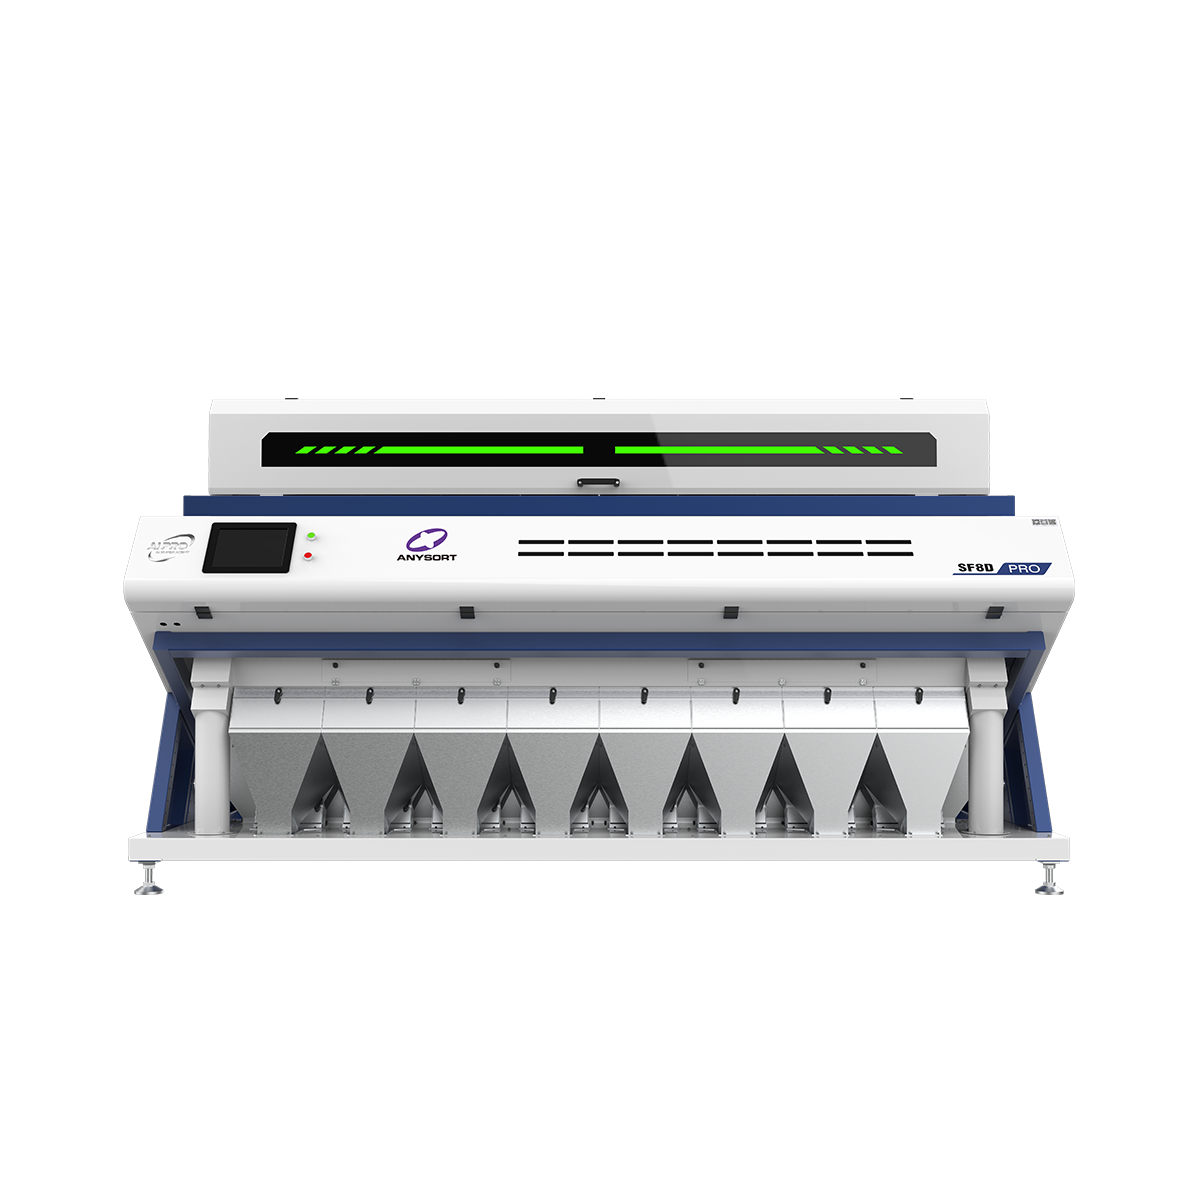
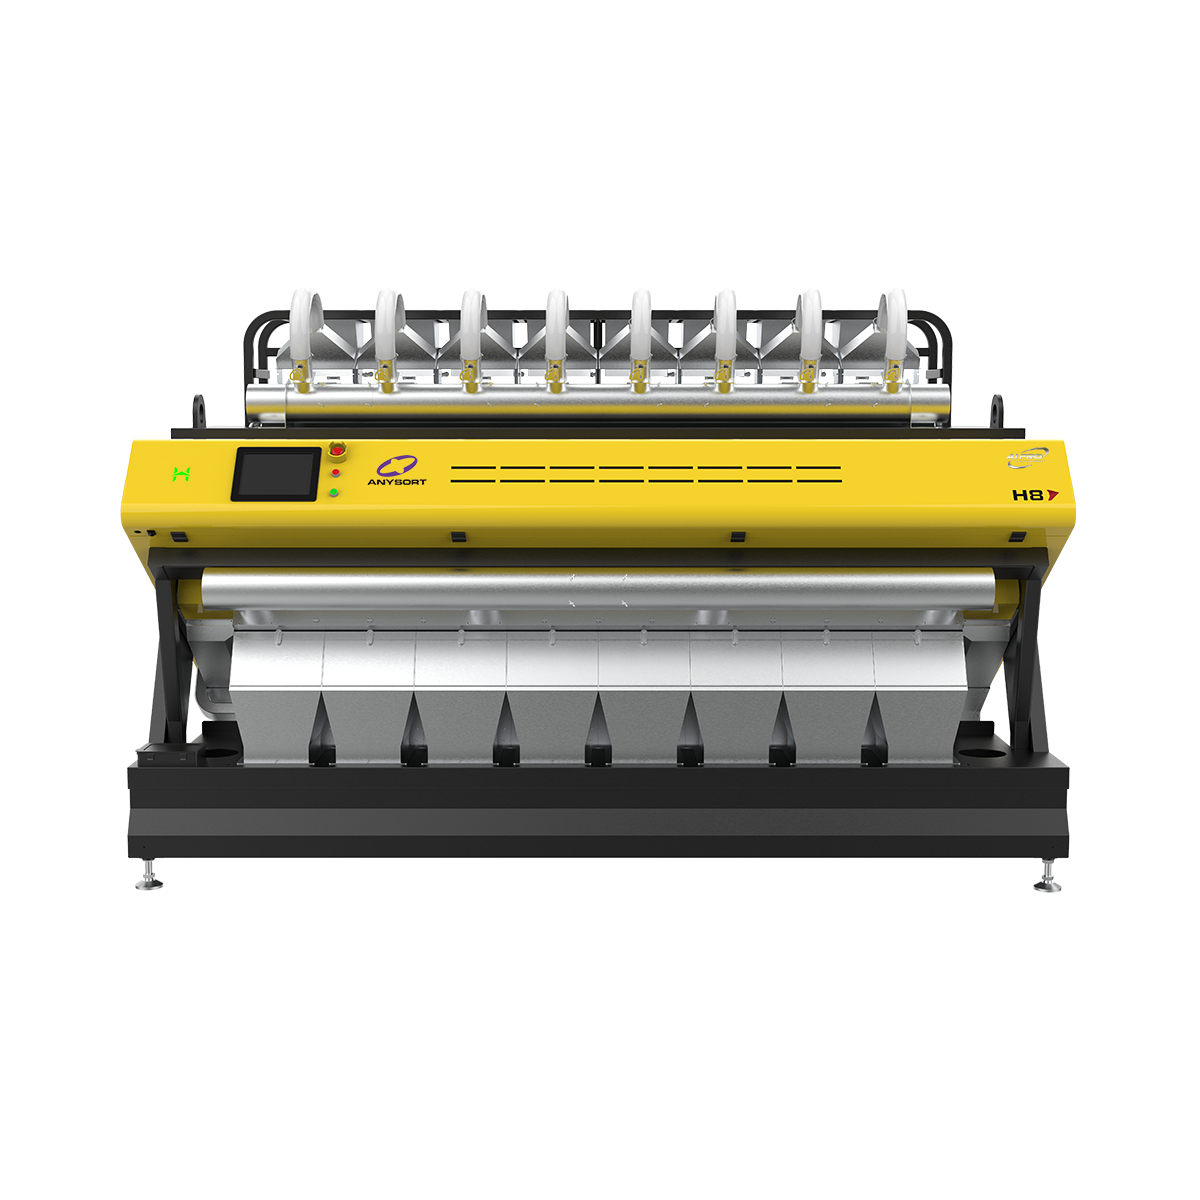
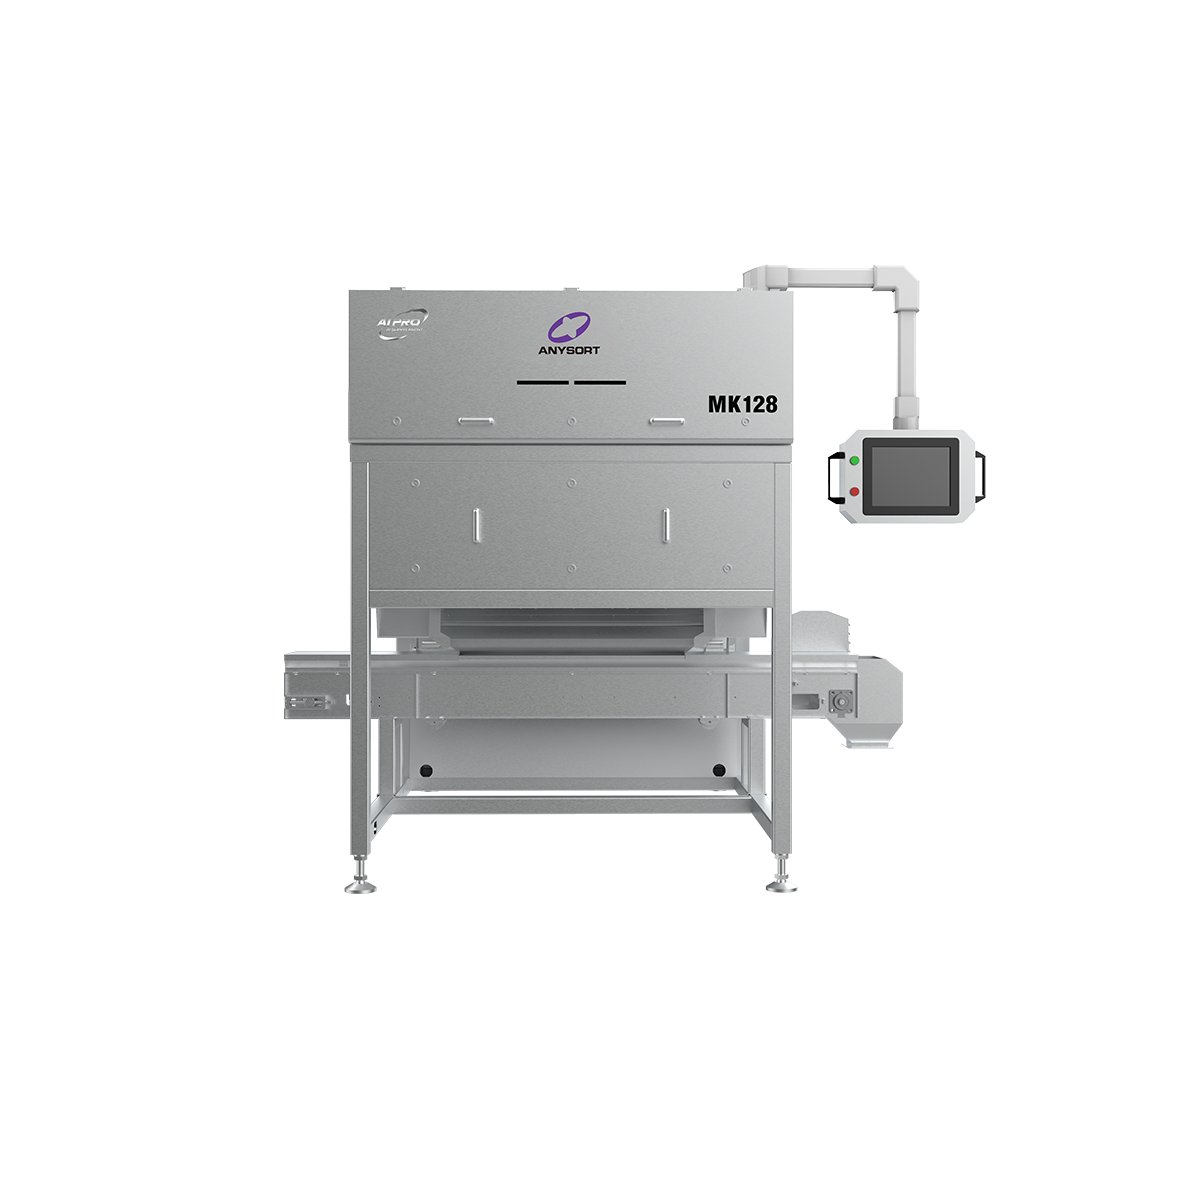
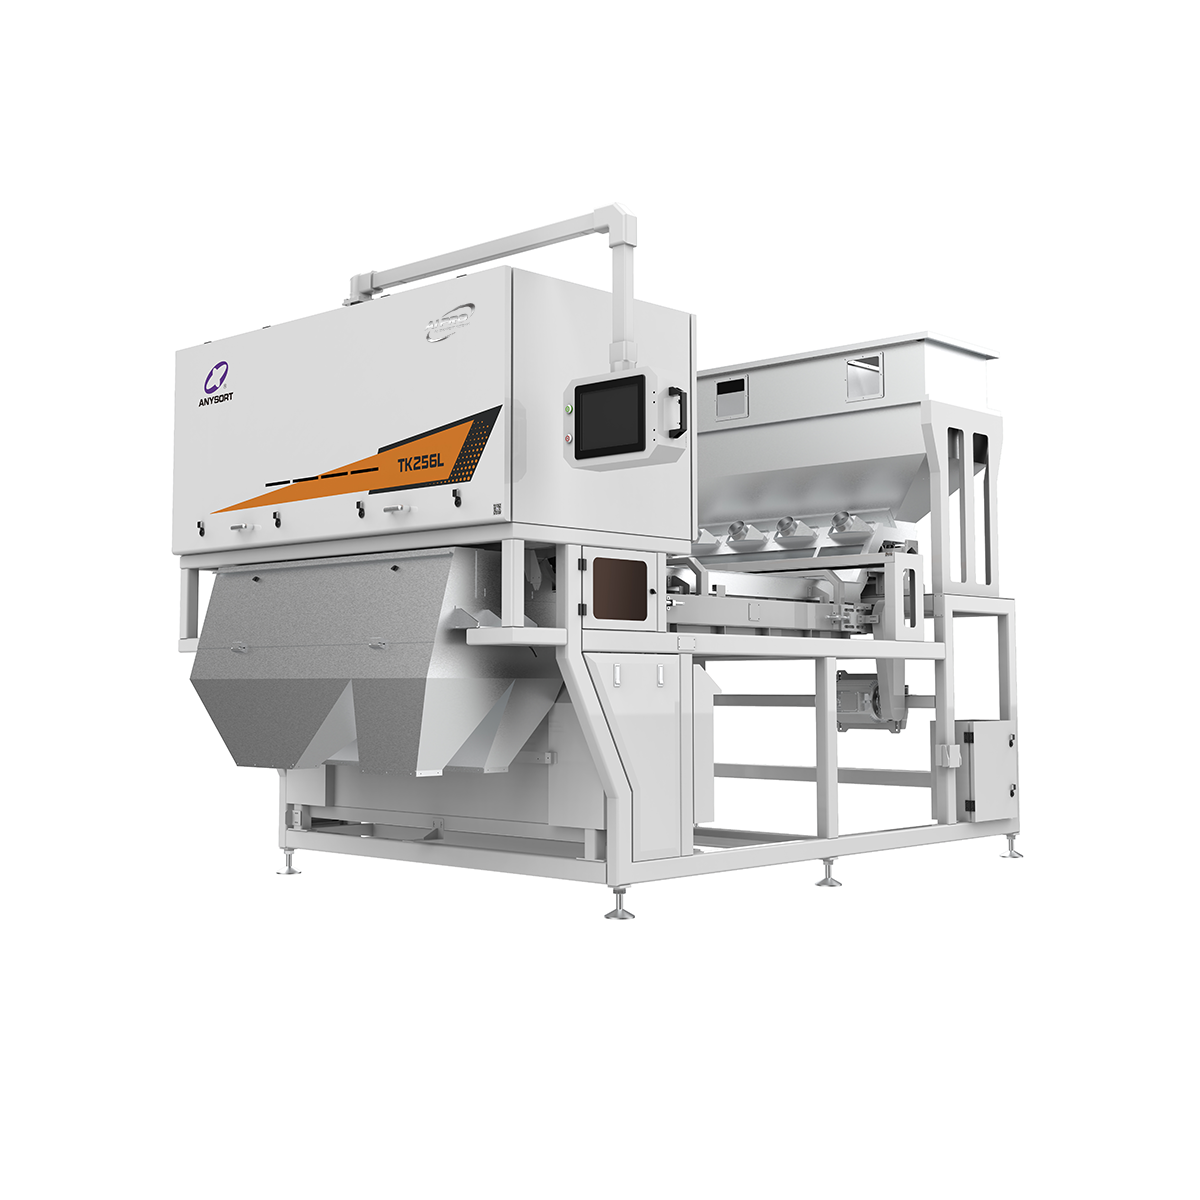
corn sorting equipment
Corn sorting equipment represents a critical technology in modern grain processing and agricultural operations. This specialized machinery automates the process of separating and grading corn kernels based on size, quality, color, and density. Modern corn sorting equipment utilizes advanced optical sensors and artificial intelligence to identify defects, foreign materials, and inferior kernels with remarkable precision.
The primary function of corn sorting equipment is to enhance grain quality while maximizing productivity in processing facilities. By removing damaged, discolored, and broken kernels, this equipment ensures that only premium-grade corn reaches market. Corn sorting equipment typically features multiple sorting lanes, enabling operators to process large volumes simultaneously.
Technological features of contemporary corn sorting equipment include high-speed cameras, infrared detection systems, and machine learning algorithms. These innovations allow the equipment to process thousands of kernels per minute while maintaining exceptional accuracy rates exceeding 99 percent. The sophisticated sensors in corn sorting equipment can distinguish between subtle color variations and detect even minor imperfections invisible to the human eye.
Applications for corn sorting equipment span various industries, including food processing, animal feed production, seed preparation, and industrial grain trading. Agricultural facilities use corn sorting equipment to meet strict quality standards demanded by international markets. The equipment also serves breweries, distilleries, and cornmeal manufacturers requiring consistent, high-quality raw materials. Investment in corn sorting equipment has become essential for competitive grain operations worldwide.

 EN