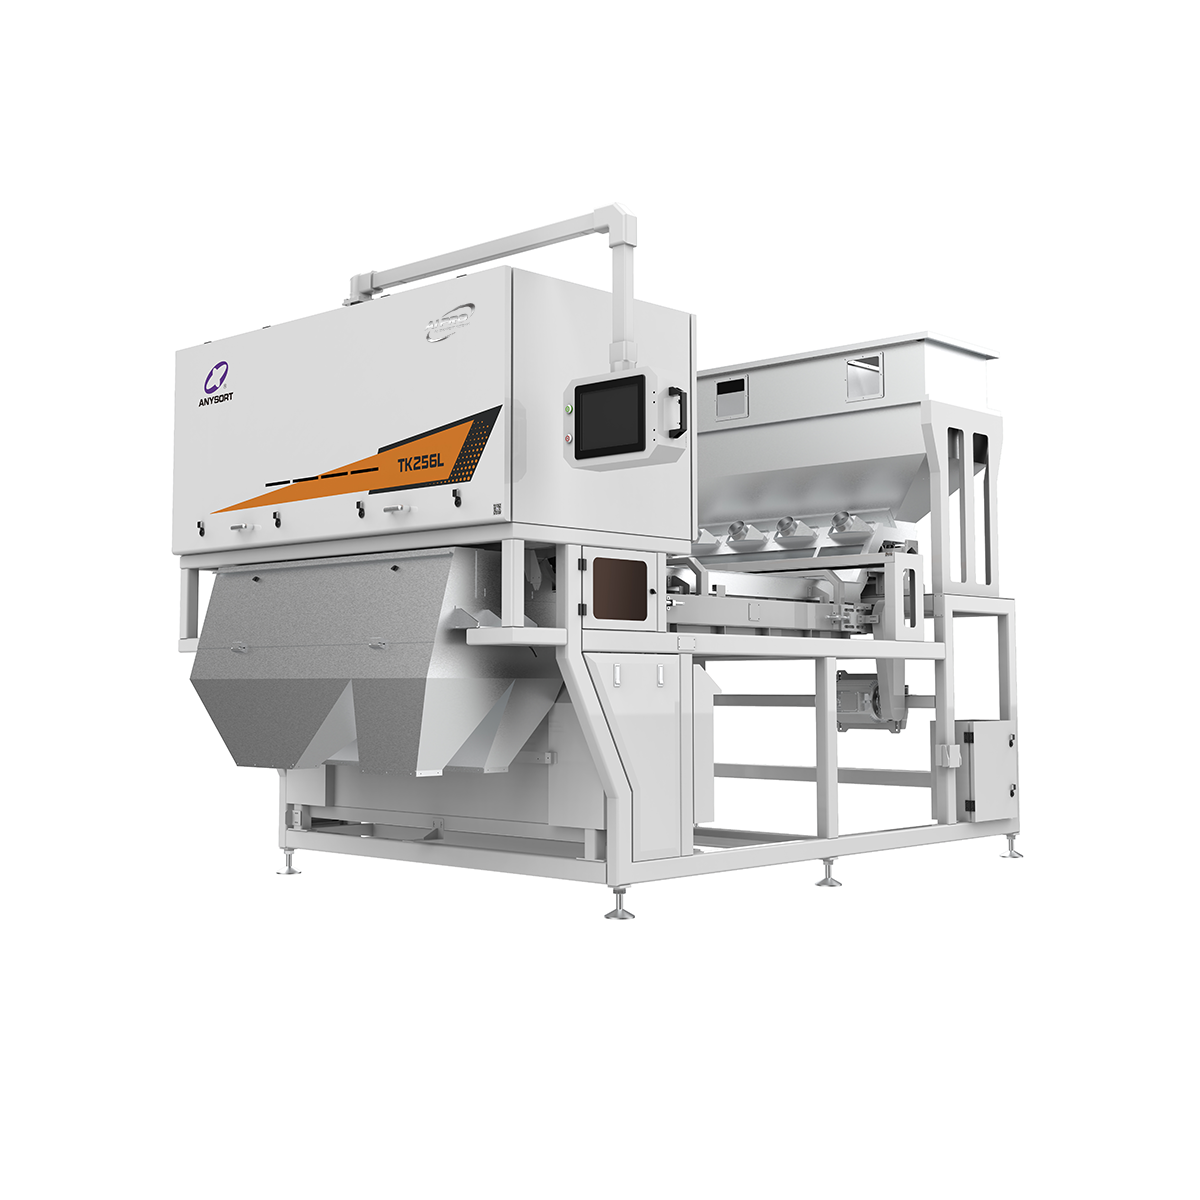
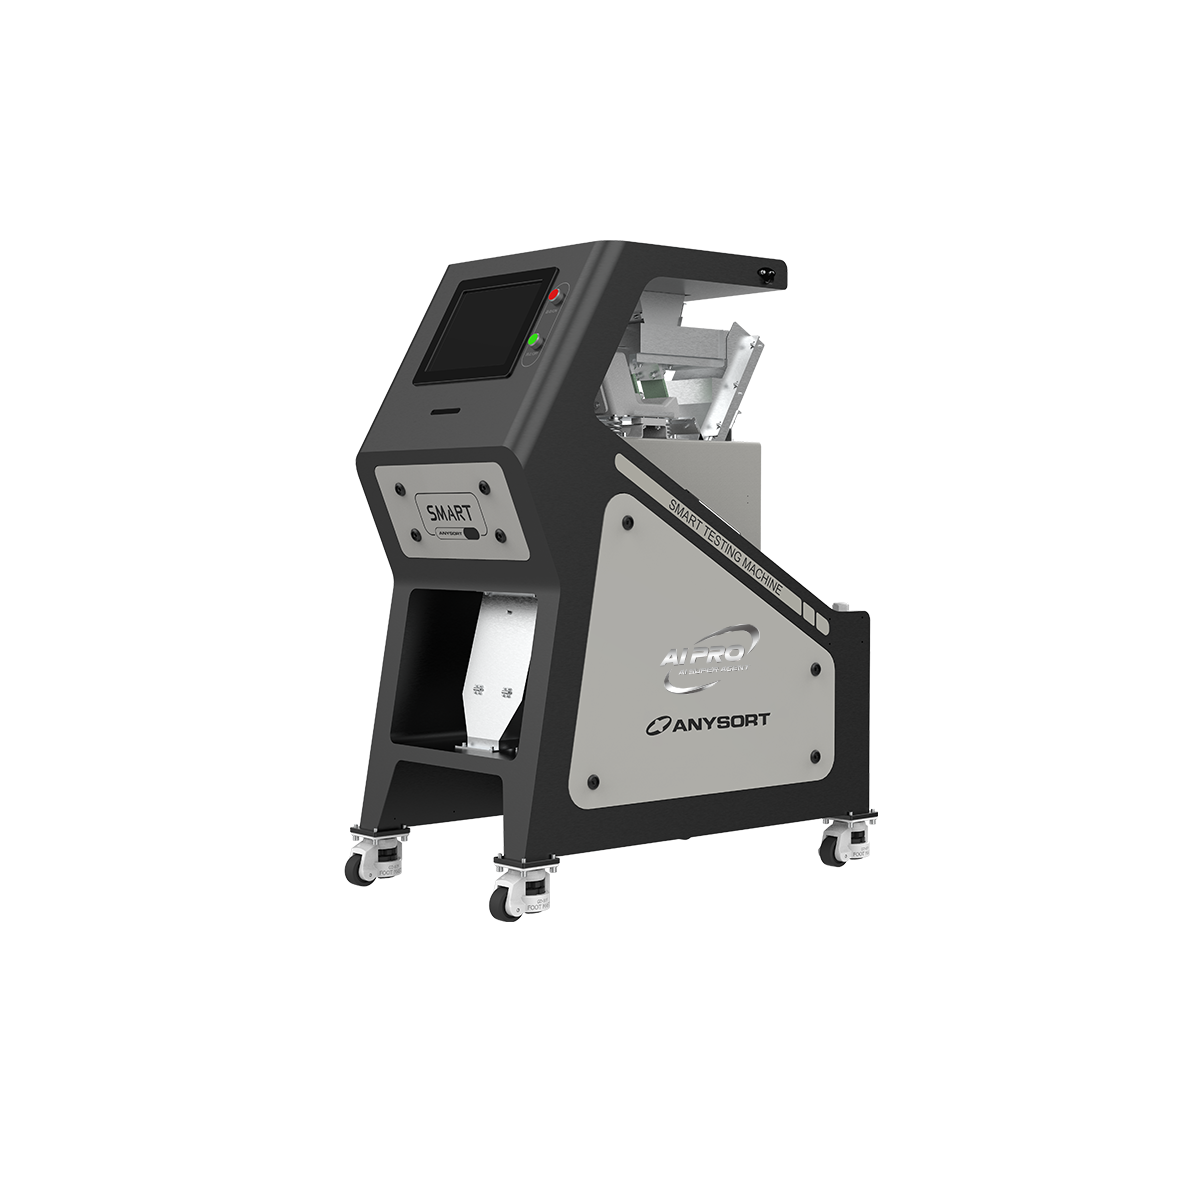
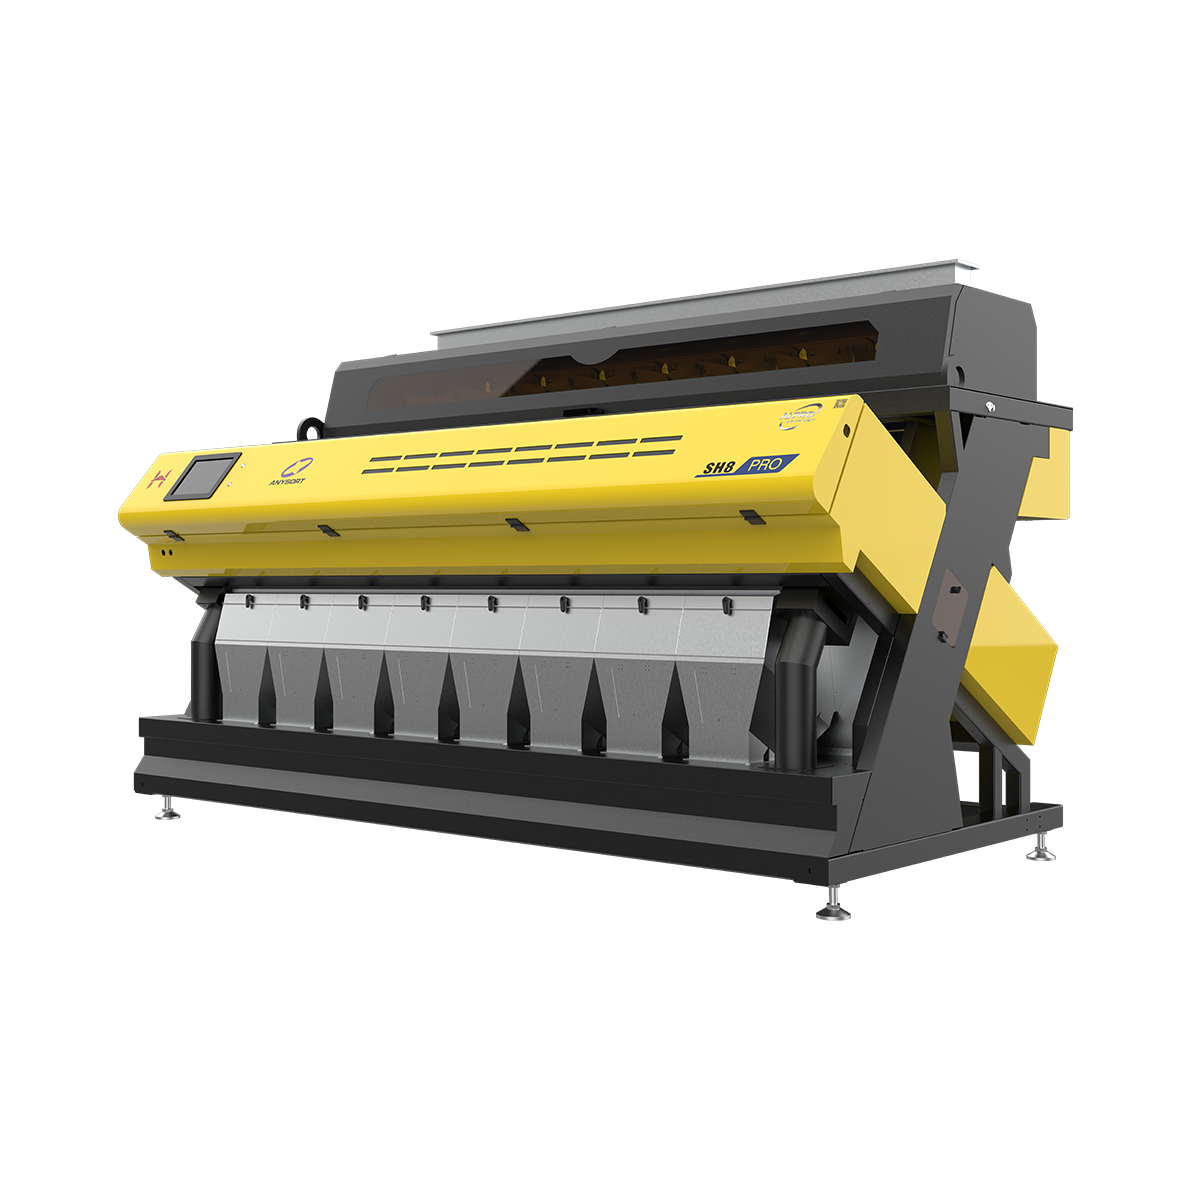
corn color sorter factory
A corn color sorter factory represents a specialized facility designed to separate and grade corn kernels based on color, quality, and physical characteristics using advanced optical sorting technology. The corn color sorter factory operates as a crucial component in agricultural processing, food production, and animal feed manufacturing industries. This facility employs high-precision imaging systems and artificial intelligence algorithms to detect and remove discolored, damaged, or foreign particles from corn batches with exceptional accuracy.
The technological foundation of a corn color sorter factory includes multispectral cameras, LED lighting systems, and pneumatic ejection mechanisms working in synchronized harmony. Modern corn color sorter factory equipment can process substantial volumes, sometimes exceeding several tons per hour, while maintaining consistent quality standards. The sorting process ensures that only premium-grade corn kernels proceed through production pipelines, significantly reducing waste and contamination risks.
Applications of corn color sorter factory systems extend across multiple sectors including food processing, biofuel production, livestock feed preparation, and grain trading. The corn color sorter factory technology eliminates manual sorting inefficiencies and human error, delivering standardized results that meet international quality benchmarks. Agricultural businesses, grain merchants, and food manufacturers invest in corn color sorter factory solutions to enhance product reliability, improve market competitiveness, and streamline operational workflows. The factory environment maximizes throughput while maintaining meticulous color differentiation standards essential for premium corn products.

 EN