Sorting Equipment | Automated Sorting Solutions

All Categories

sorting equipment

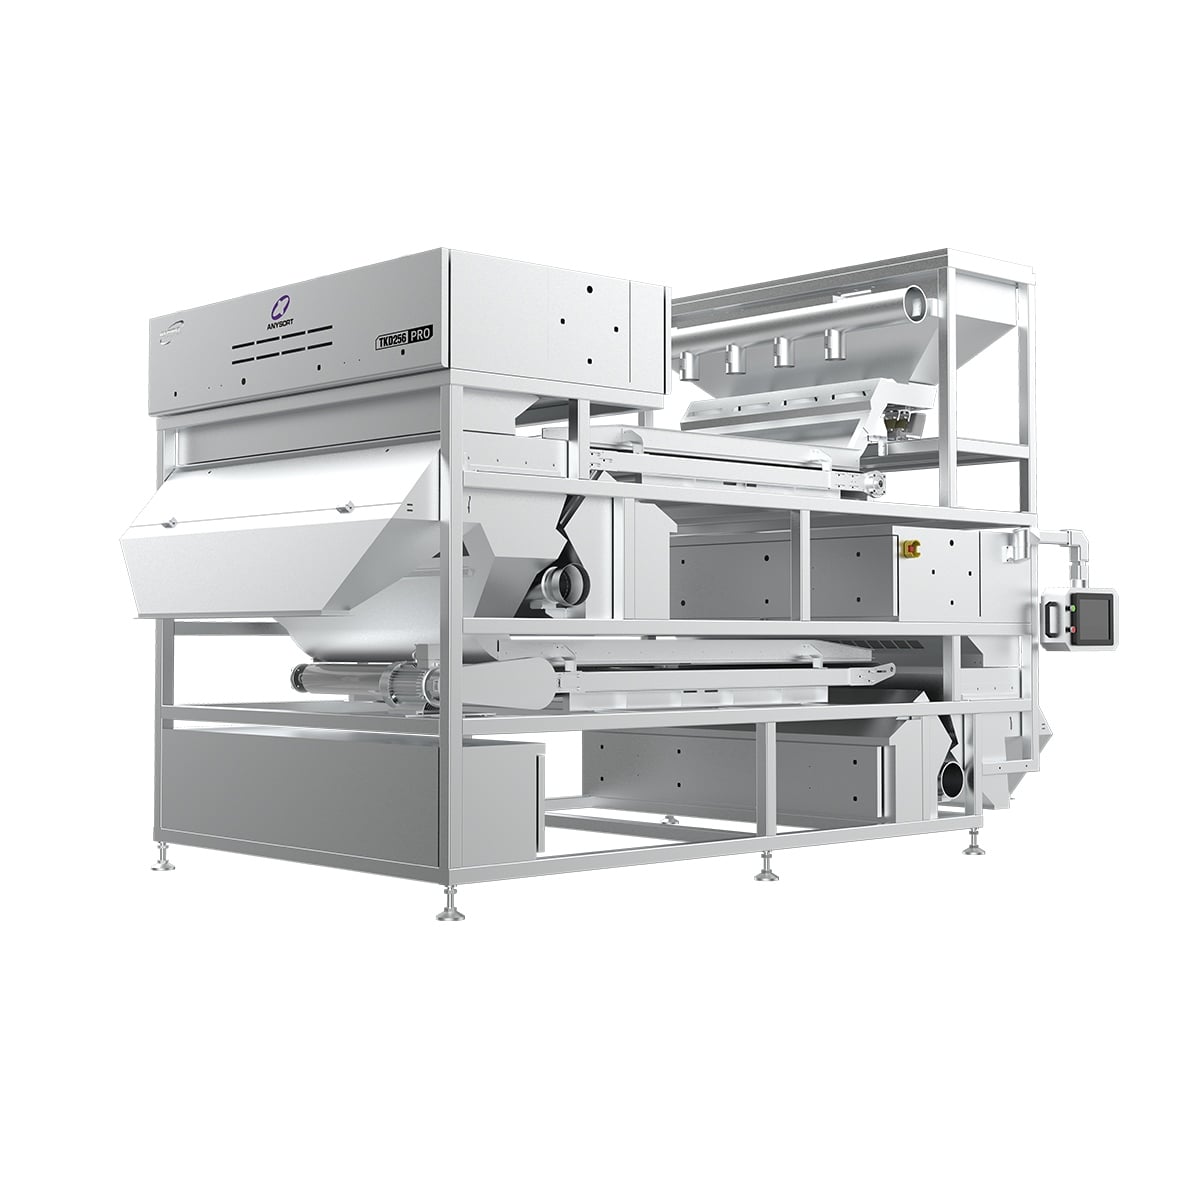
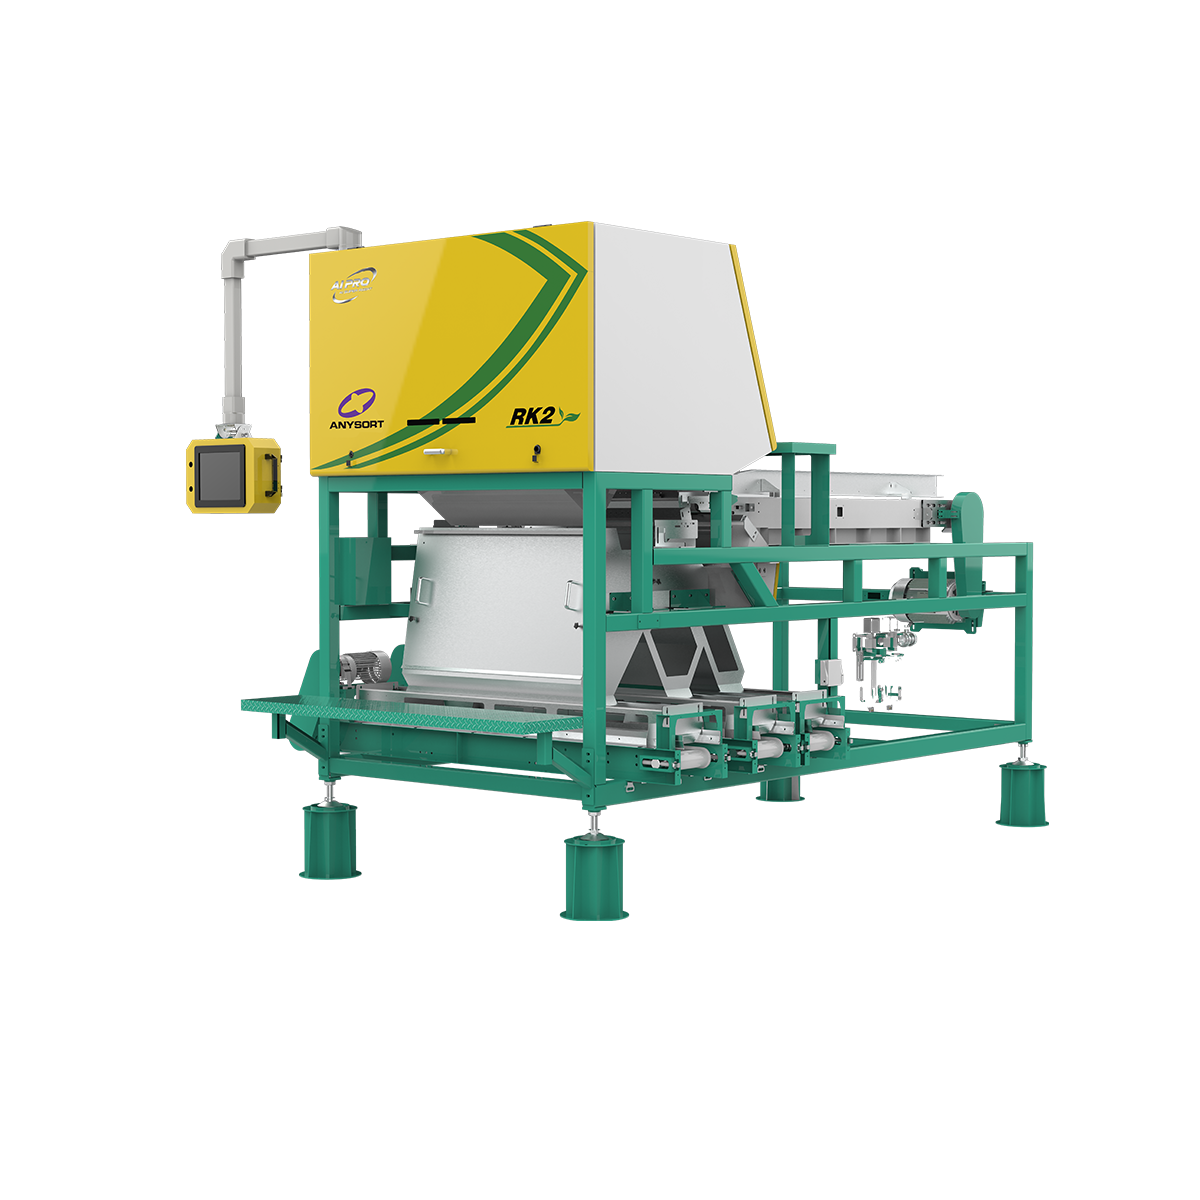
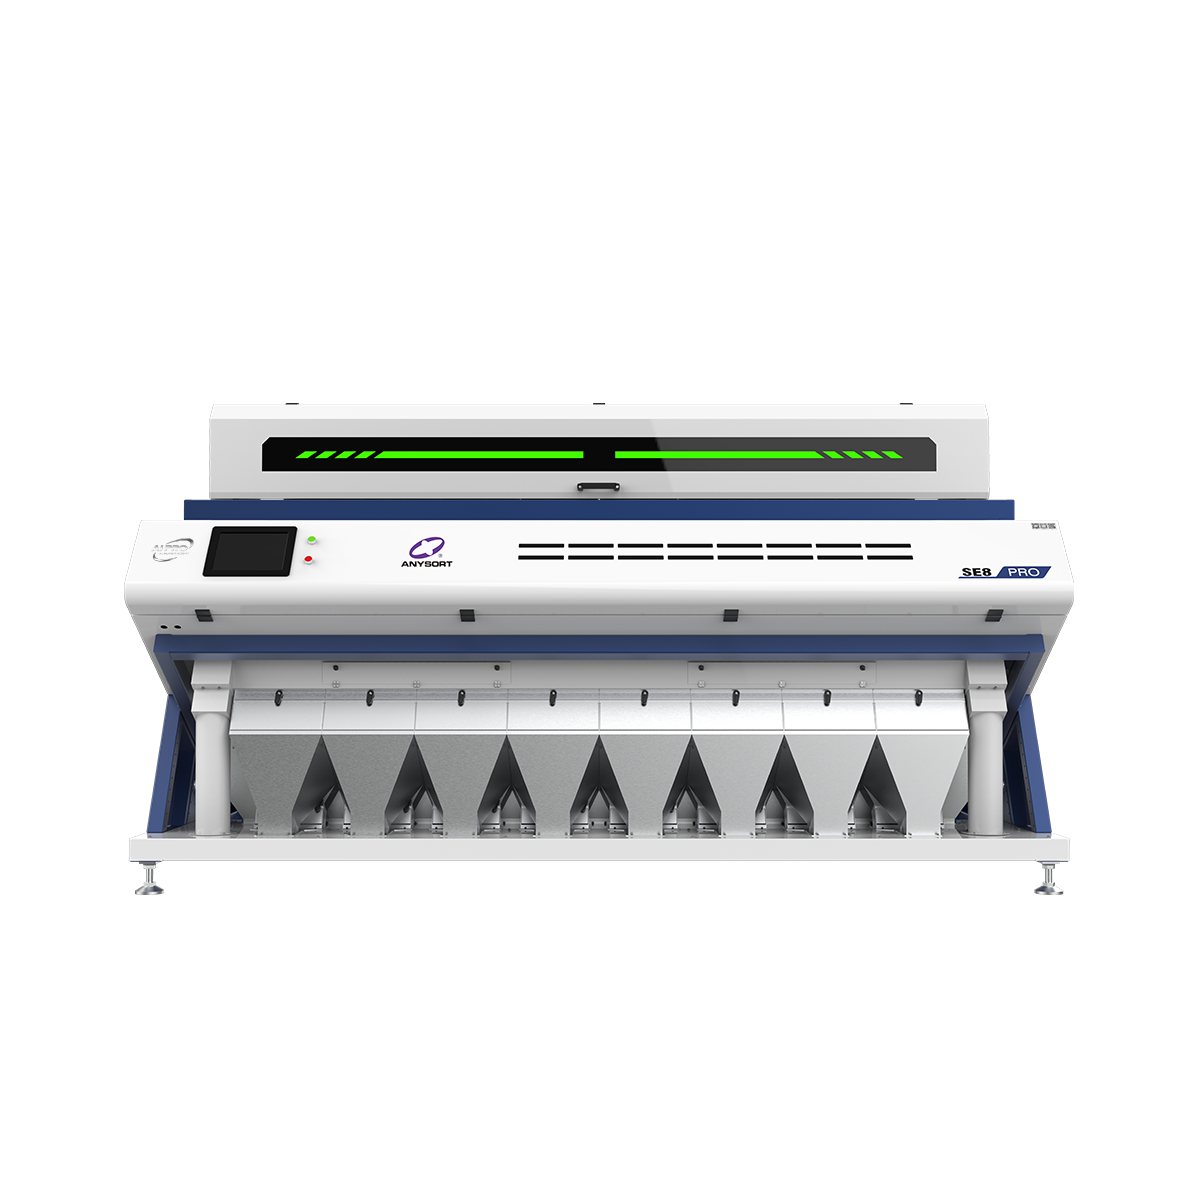
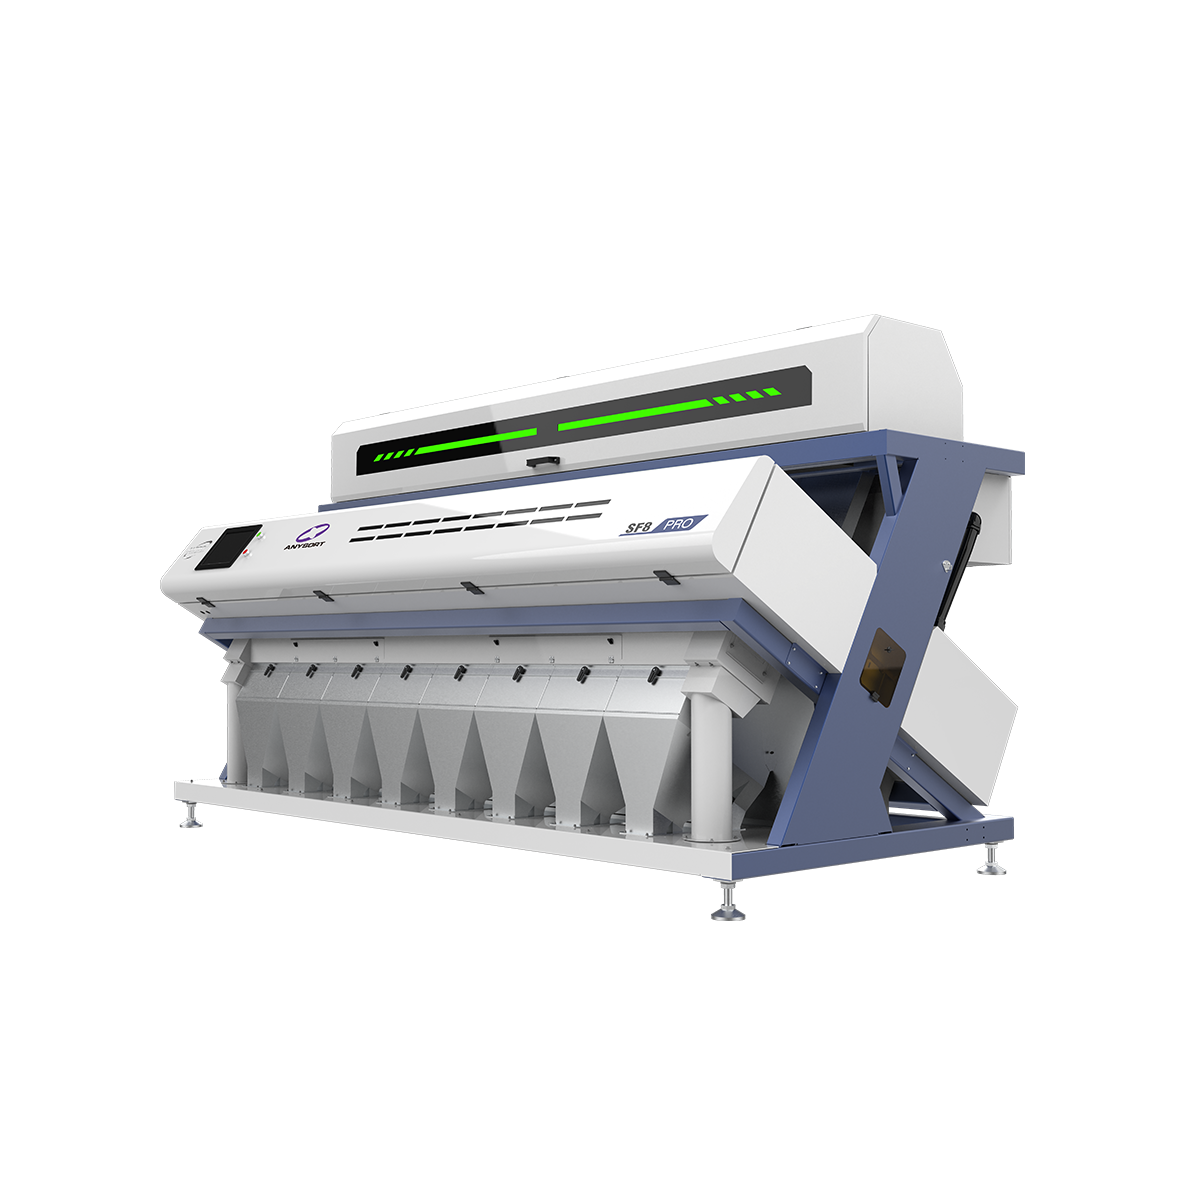
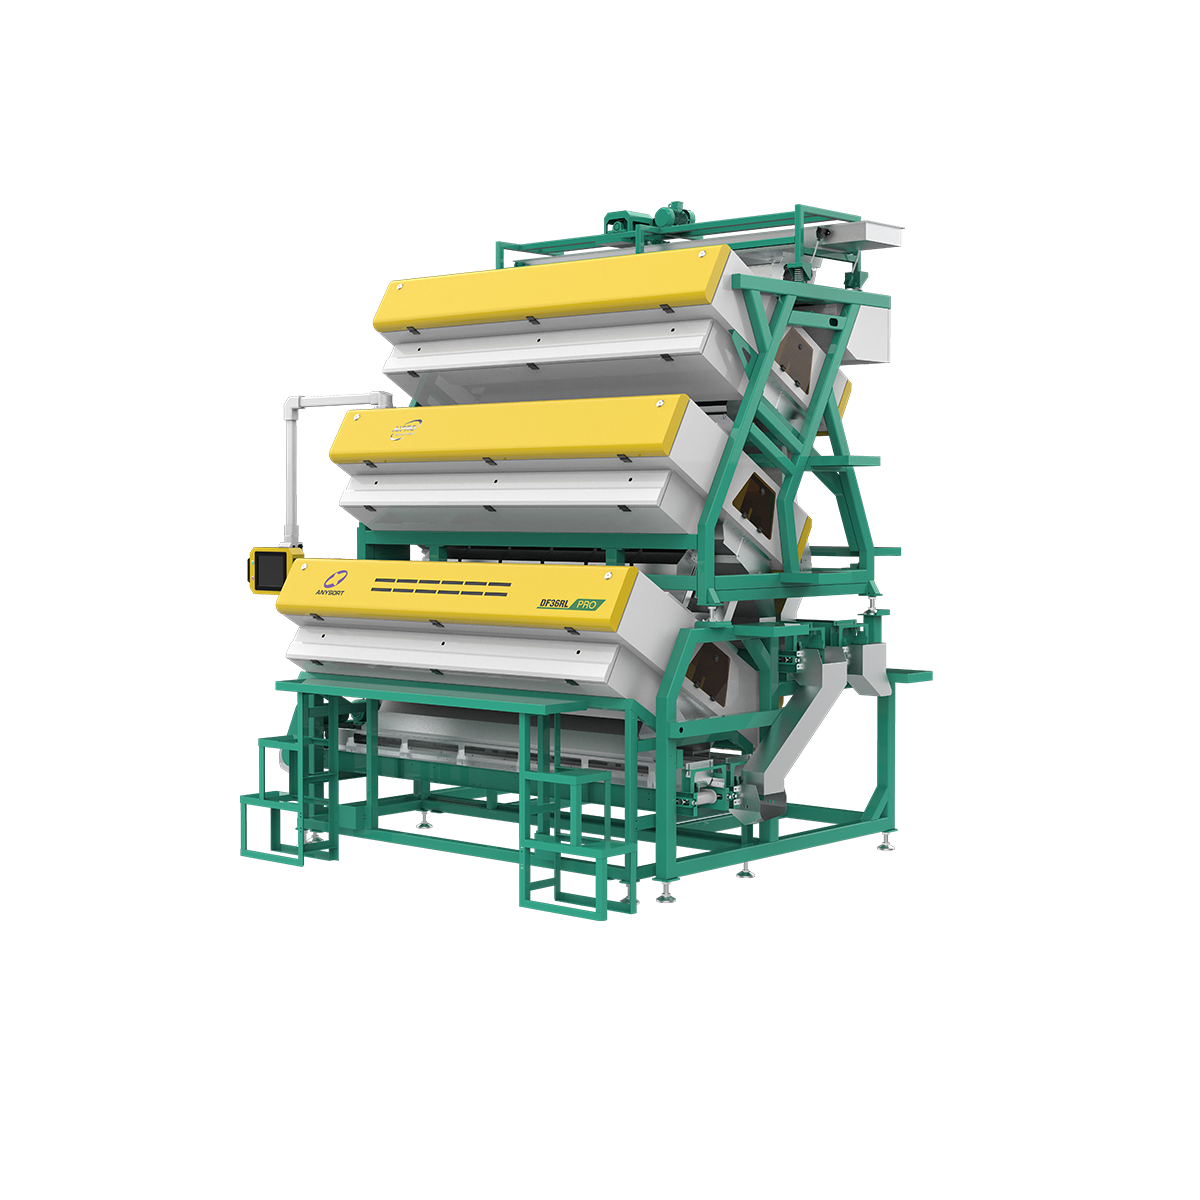
Sorting equipment represents a cornerstone technology in modern industrial operations, designed to streamline material handling and enhance operational efficiency across diverse sectors. This specialized machinery automates the process of categorizing, organizing, and separating items based on predetermined criteria, including size, weight, color, and destination. Modern sorting equipment utilizes advanced technological features such as optical scanning systems, artificial intelligence algorithms, and high-speed conveyor mechanisms to process thousands of items per hour with exceptional accuracy. The core function of sorting equipment involves receiving mixed batches of products and rapidly distributing them into appropriate categories or channels, eliminating manual labor and reducing human error significantly. Sorting equipment finds extensive applications in logistics and warehousing, where it accelerates package distribution to correct destinations. In the food industry, sorting equipment ensures quality control by removing defective products and contaminants. Manufacturing facilities rely on sorting equipment to organize components for assembly lines, while recycling centers depend on this technology to separate recyclable materials efficiently. The technological advancement in sorting equipment now includes machine learning capabilities, enabling systems to adapt and improve performance continuously. Real-time monitoring systems provide operators with comprehensive data about throughput rates, operational status, and maintenance needs. Whether handling e-commerce shipments, agricultural products, or industrial components, sorting equipment has become indispensable for businesses seeking competitive advantages through automation and precision.

New Product Releases

Sorting equipment delivers substantial practical benefits that transform operational capabilities and bottom-line performance for businesses of all sizes. The primary advantage involves dramatic efficiency gains, as sorting equipment processes items at speeds impossible for manual labor, dramatically reducing processing time and enabling businesses to handle increased volumes without proportional staffing increases. Cost reduction represents another compelling benefit, as sorting equipment minimizes labor expenses while reducing errors that lead to costly customer complaints and returns. Accuracy improvements prove invaluable, as sorting equipment maintains consistency rates exceeding 99 percent, far surpassing human performance levels and ensuring customer satisfaction. For supply chain operations, sorting equipment eliminates bottlenecks that plague manual processes, enabling faster order fulfillment and improved customer delivery times. Businesses gain operational flexibility through sorting equipment's adaptability to different product types and sorting criteria, allowing the same system to handle diverse applications with simple reconfiguration. Safety advantages emerge as sorting equipment removes workers from repetitive, physically demanding tasks that cause injuries and strain-related illnesses. Environmental benefits also matter, particularly when sorting equipment handles recycling operations, enabling businesses to achieve sustainability goals while processing materials cost-effectively. The decision to invest in sorting equipment becomes strategically sound when considering productivity multipliers—facilities typically experience 300-400 percent throughput increases compared to baseline manual operations. Integration capabilities with existing warehouse management systems ensure sorting equipment functions seamlessly within current infrastructure, maximizing return on investment while minimizing implementation disruptions.

Tips And Tricks

What Factors Affect Tea Color Sorter Performance and Accuracy?

05

Aug

What Factors Affect Tea Color Sorter Performance and Accuracy?

The precision of a tea color sorter directly determines the quality consistency of finished tea products. Understanding the factors that influence tea color sorter performance and accuracy is essential for tea processors seeking to maintain competiti...
View More
How can rice color sorters improve grain quality?

08

Aug

How can rice color sorters improve grain quality?

Rice color sorters represent a transformative technology in modern grain processing, fundamentally changing how producers maintain and enhance the quality of their rice output. By utilizing advanced optical scanning and artificial intelligence, a ric...
View More
How does optical sorting technology detect defective rice grains?

22

Aug

How does optical sorting technology detect defective rice grains?

Modern rice processing demands precision and consistency, which is why understanding the detection mechanisms behind advanced equipment has become essential for producers. A rice color sorter represents one of the most significant technological break...
View More
How Do Color Sorters Improve Product Quality?

26

Aug

How Do Color Sorters Improve Product Quality?

Product quality stands as a critical differentiator in competitive industrial markets, and achieving consistency at scale requires more than manual oversight. A color sorter represents one of the most effective technologies for identifying and removi...
View More

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

sorting equipment

Advanced Optical Recognition Technology

Advanced Optical Recognition Technology

Modern sorting equipment incorporates sophisticated optical scanning systems that identify and classify items with remarkable precision. This technology utilizes high-resolution cameras combined with artificial intelligence algorithms to analyze product characteristics in milliseconds. Sorting equipment equipped with optical recognition can distinguish between similar items based on subtle differences in appearance, color variation, and surface texture. The system continuously learns and adapts to variations, improving accuracy rates over time through machine learning integration. For businesses handling diverse product catalogs, this sorting equipment capability eliminates the need for extensive manual quality checks, redirecting staff toward more strategic tasks. The optical recognition technology proves particularly valuable in food processing, where detecting contamination or product defects becomes critical for safety compliance. Retailers benefit from sorting equipment's ability to identify mislabeled products and organize inventory by specific attributes beyond basic categorization. Investment in sorting equipment with advanced optical technology pays dividends through reduced waste, fewer customer complaints regarding product quality, and enhanced regulatory compliance documentation.
High-Throughput Capacity and Speed

High-Throughput Capacity and Speed

Sorting equipment designed for high-volume operations processes thousands of items hourly, fundamentally transforming facility productivity metrics. The conveyor systems within sorting equipment move items at controlled speeds optimized for accurate sorting while maintaining maximum throughput rates. Businesses implementing sorting equipment experience dramatic reductions in processing queues, enabling facilities to clear incoming shipments rapidly and maintain efficient warehouse operations. The speed capabilities of sorting equipment prove essential during peak seasons when order volumes surge unexpectedly, preventing backlog accumulation that frustrates customers. Modern sorting equipment accommodates variable item sizes and weights without requiring extensive downtime for recalibration, supporting diverse product portfolios efficiently. For e-commerce operations, sorting equipment speed directly impacts delivery time promises and customer satisfaction metrics. Distribution centers maximize facility space utilization when sorting equipment processes items quickly, as goods spend less time occupying warehouse floor space. The consistent performance of sorting equipment ensures predictable processing timelines, enabling accurate shipment forecasting and reliable customer communication regarding delivery windows.
Seamless System Integration and Scalability

Seamless System Integration and Scalability

Contemporary sorting equipment integrates seamlessly with warehouse management systems, conveyor networks, and inventory tracking platforms through standardized data interfaces and API connectivity. Sorting equipment communicates real-time status information to facility management dashboards, enabling proactive maintenance scheduling and performance monitoring. The modular design philosophy of modern sorting equipment allows facilities to expand capacity incrementally, adding sorting chutes or additional sorting equipment units as business demands grow without complete system replacement. Integration capabilities mean sorting equipment implementations reduce training requirements, as staff familiar with existing warehouse systems quickly adapt to equipment operation. Businesses achieve rapid deployment when sorting equipment integrates with current infrastructure, minimizing production disruptions during installation phases. The scalability inherent in properly designed sorting equipment means investments remain relevant as companies expand, supporting growth trajectories over multiple business cycles without obsolescence concerns. Advanced sorting equipment provides detailed analytics regarding sorting accuracy rates, throughput metrics, and operational efficiency, supporting data-driven decision-making across warehouse operations management.

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

Copyright © 2026 Anhui Jiexun Optoelectronic Technology Co., Ltd. All rights reserved.  -  Privacy policy