food sorting equipment
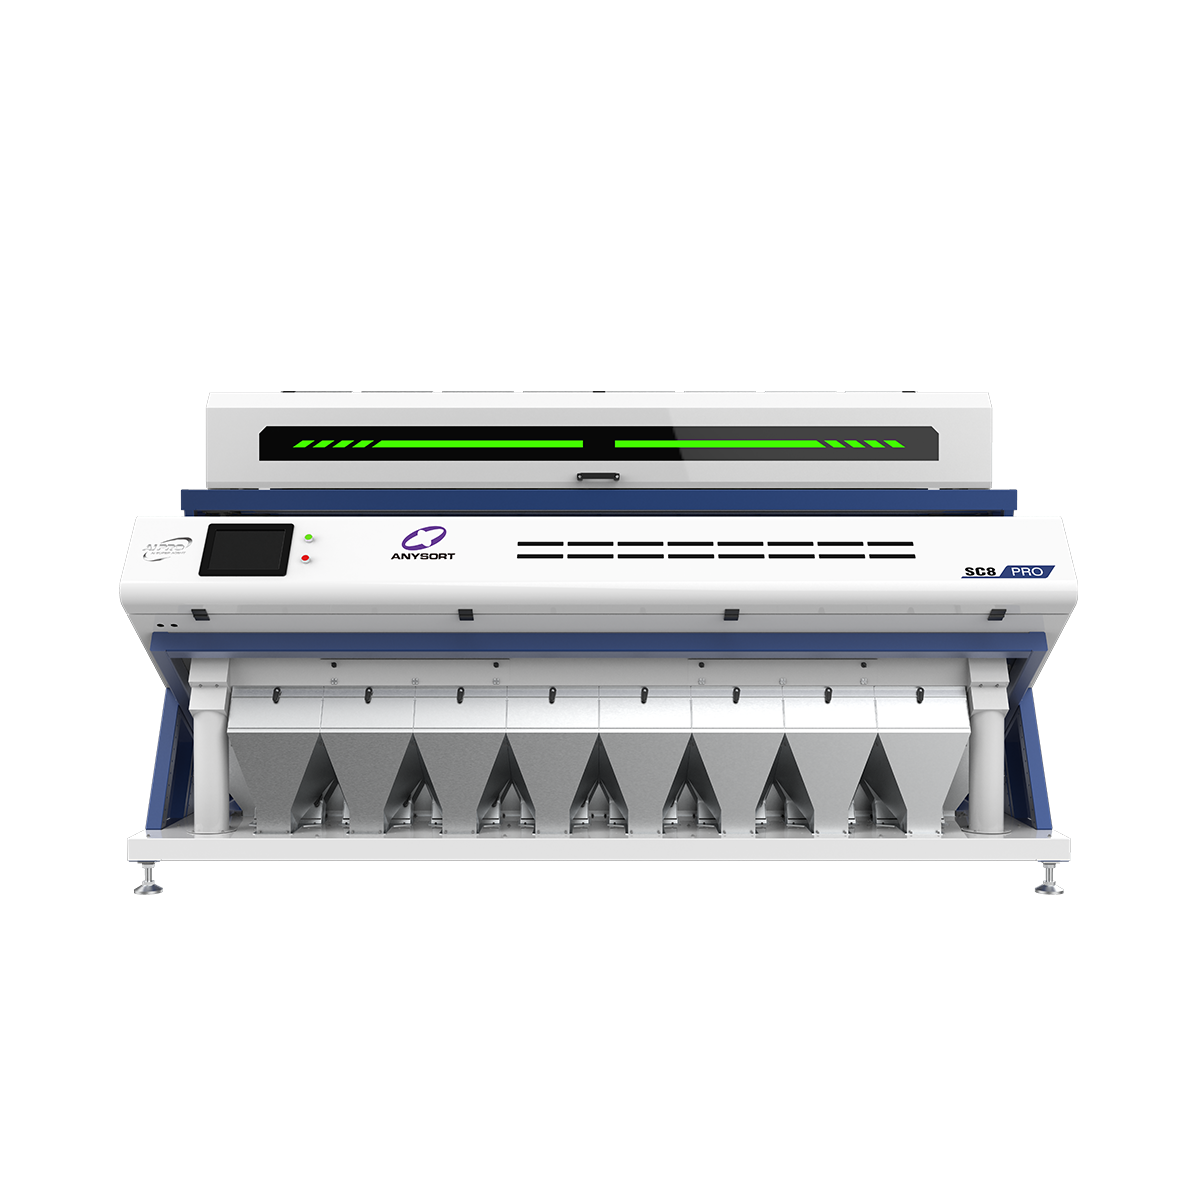
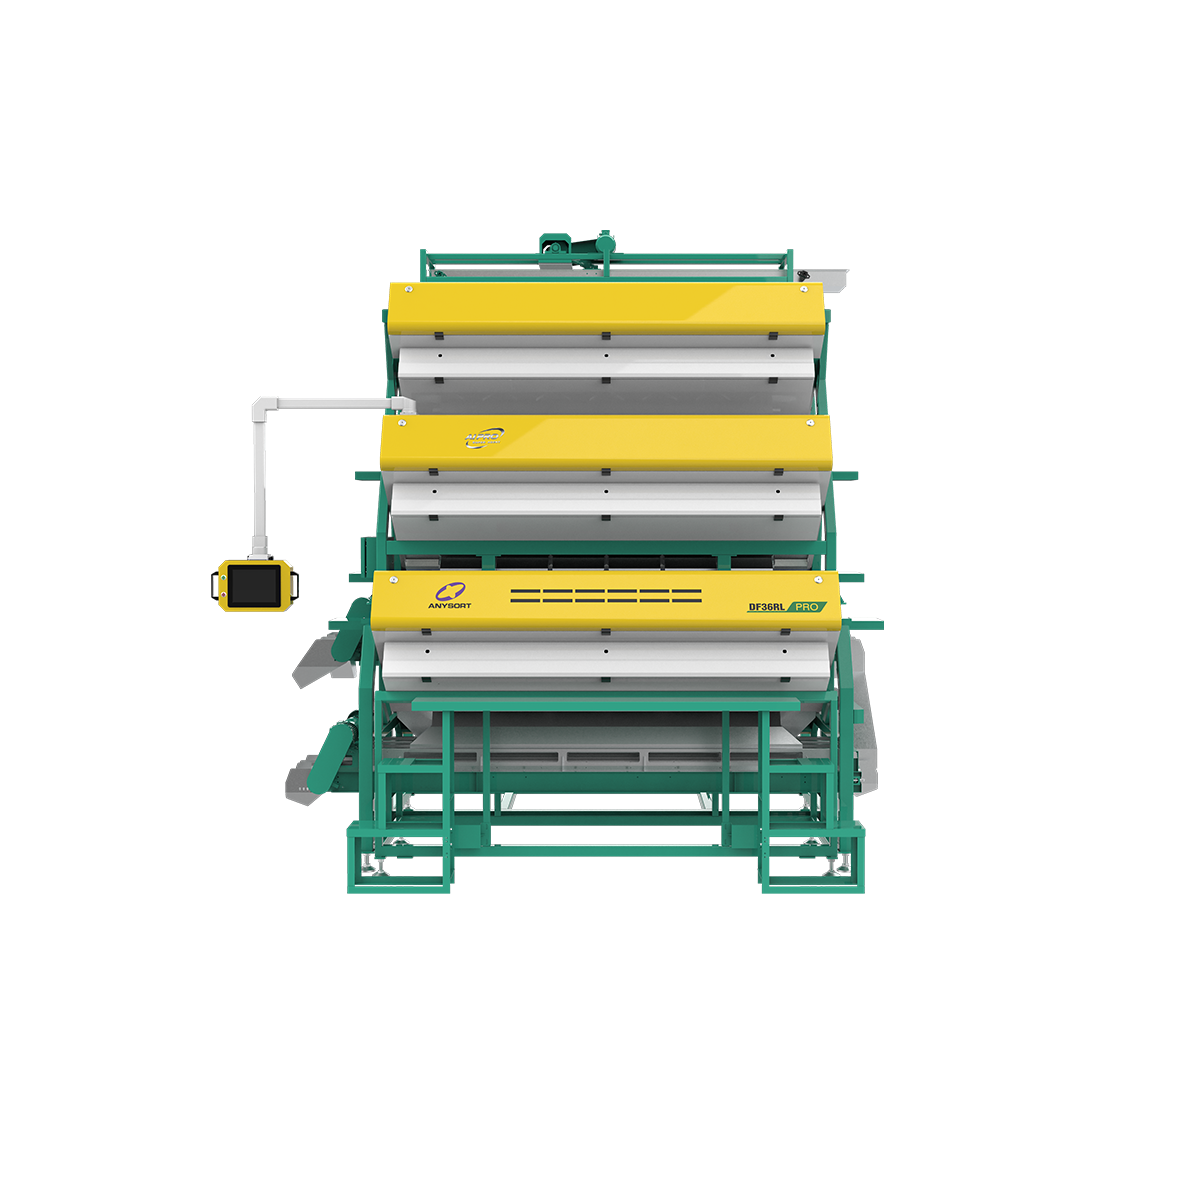
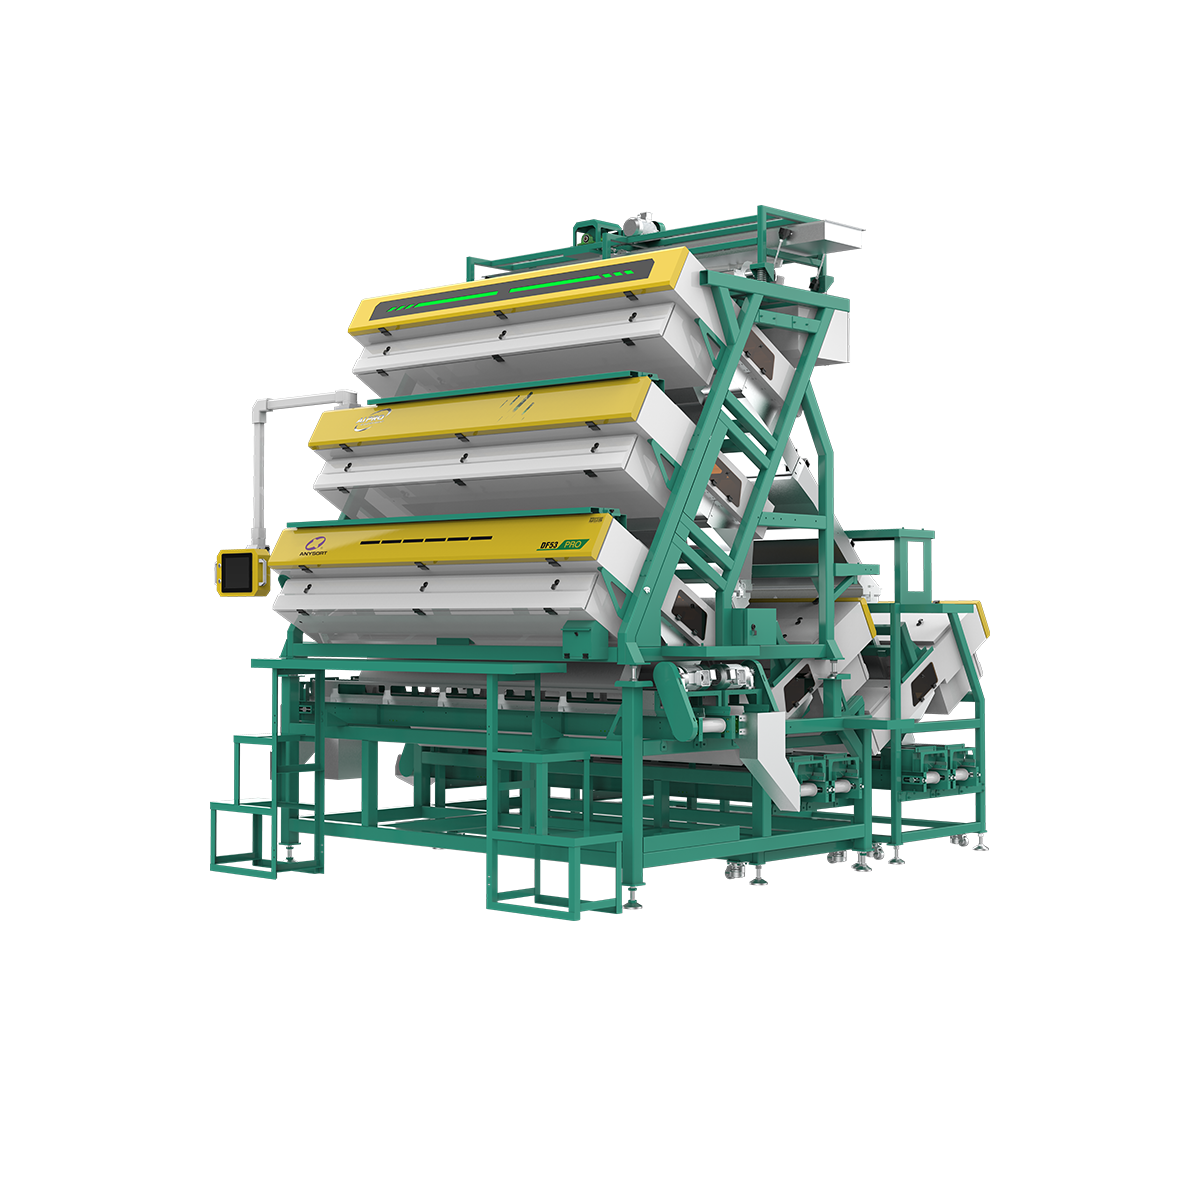
Food sorting equipment represents a critical advancement in modern food processing and quality control. This sophisticated machinery uses advanced optical sensors and artificial intelligence to automatically detect, identify, and separate food products based on size, color, weight, and defects. Food sorting equipment streamlines production lines by removing contaminants, damaged items, and substandard products with precision that manual inspection cannot achieve. The technology behind food sorting equipment incorporates high-speed cameras, spectroscopy, and machine learning algorithms that enable real-time analysis of thousands of items per minute. Food sorting equipment applications span across numerous industries, including agriculture, nuts and seeds processing, grains and cereals, frozen vegetables, fruits, and specialty food production. Modern food sorting equipment systems integrate seamlessly with existing production infrastructure, offering intuitive touchscreen controls and comprehensive data logging capabilities. The equipment operates continuously with minimal downtime, reducing labor costs while improving product consistency and safety standards. Food sorting equipment delivers exceptional reliability through durable construction designed to withstand demanding production environments. Organizations implementing food sorting equipment benefit from enhanced traceability, compliance with food safety regulations, and increased customer satisfaction through superior product quality assurance throughout the processing chain.

 EN