best sorting machines
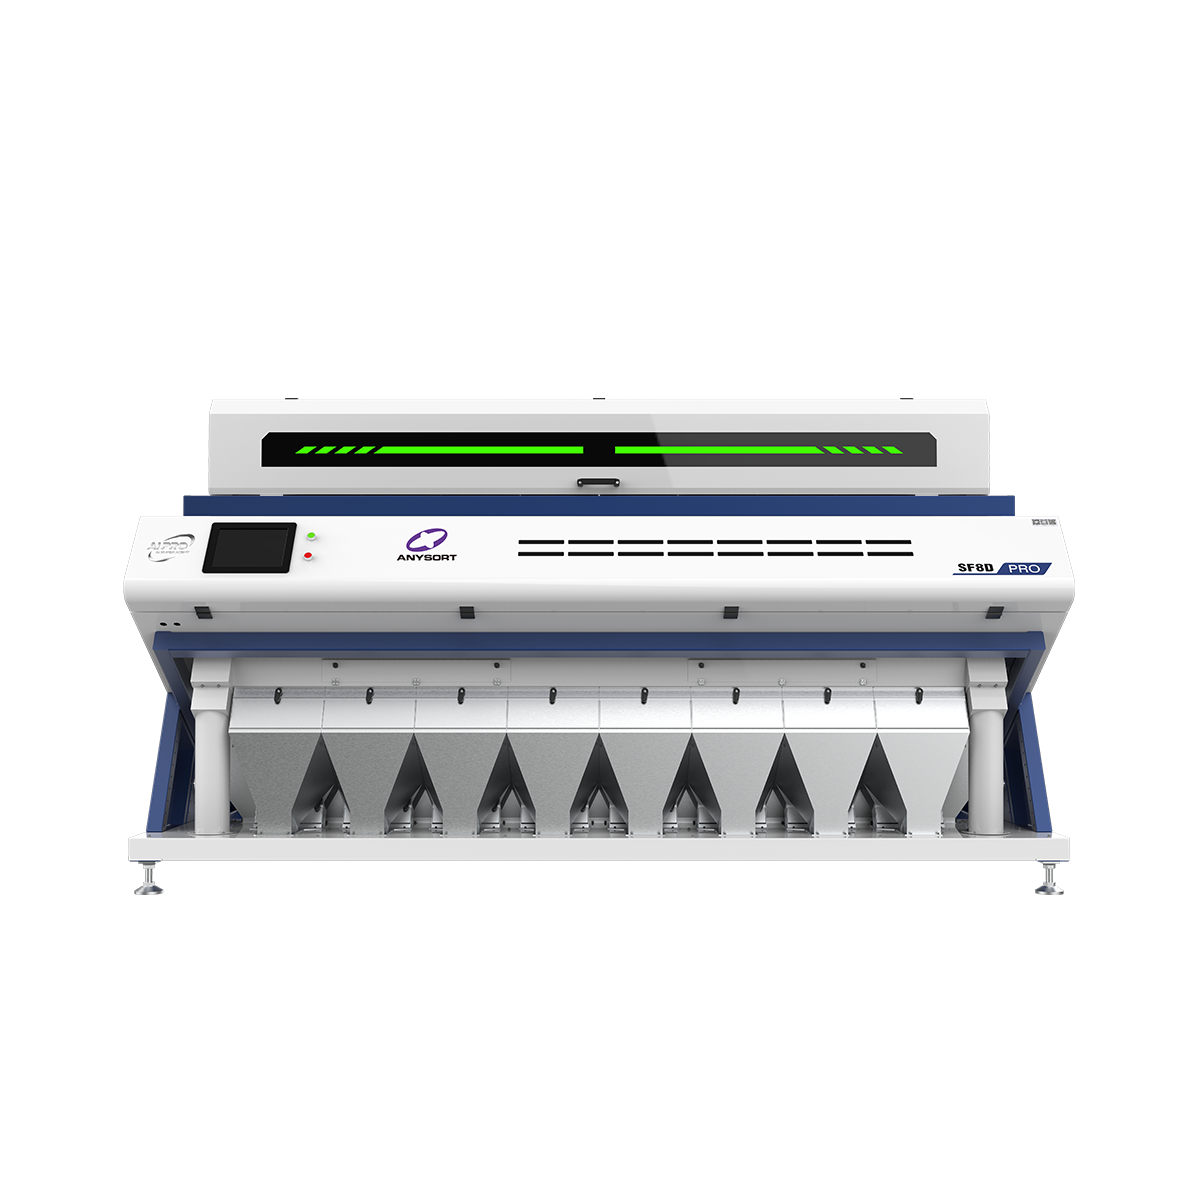
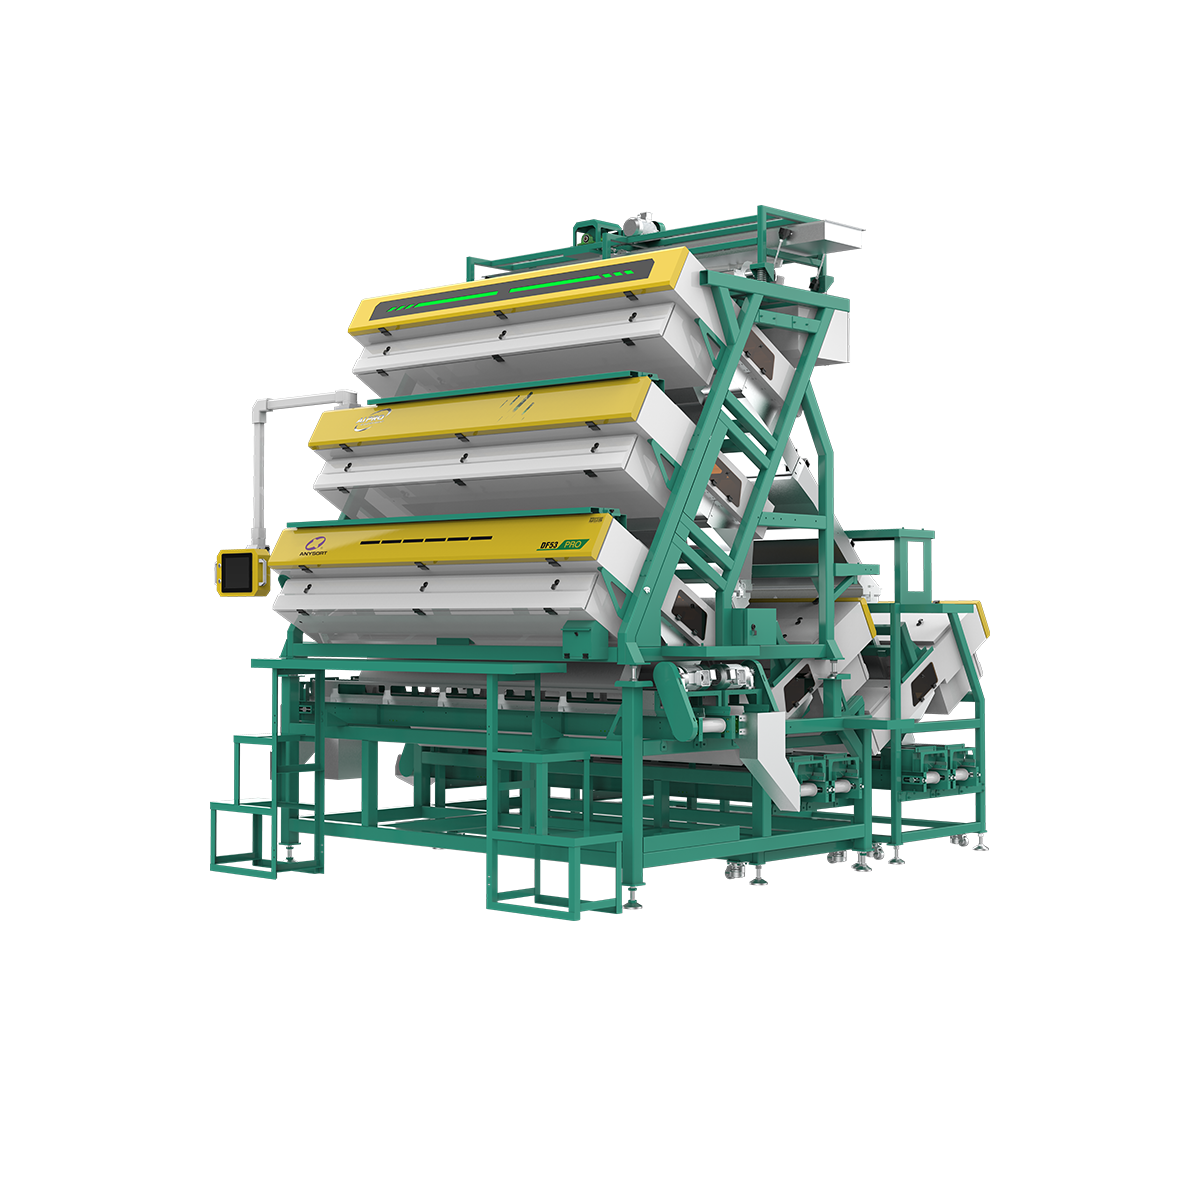
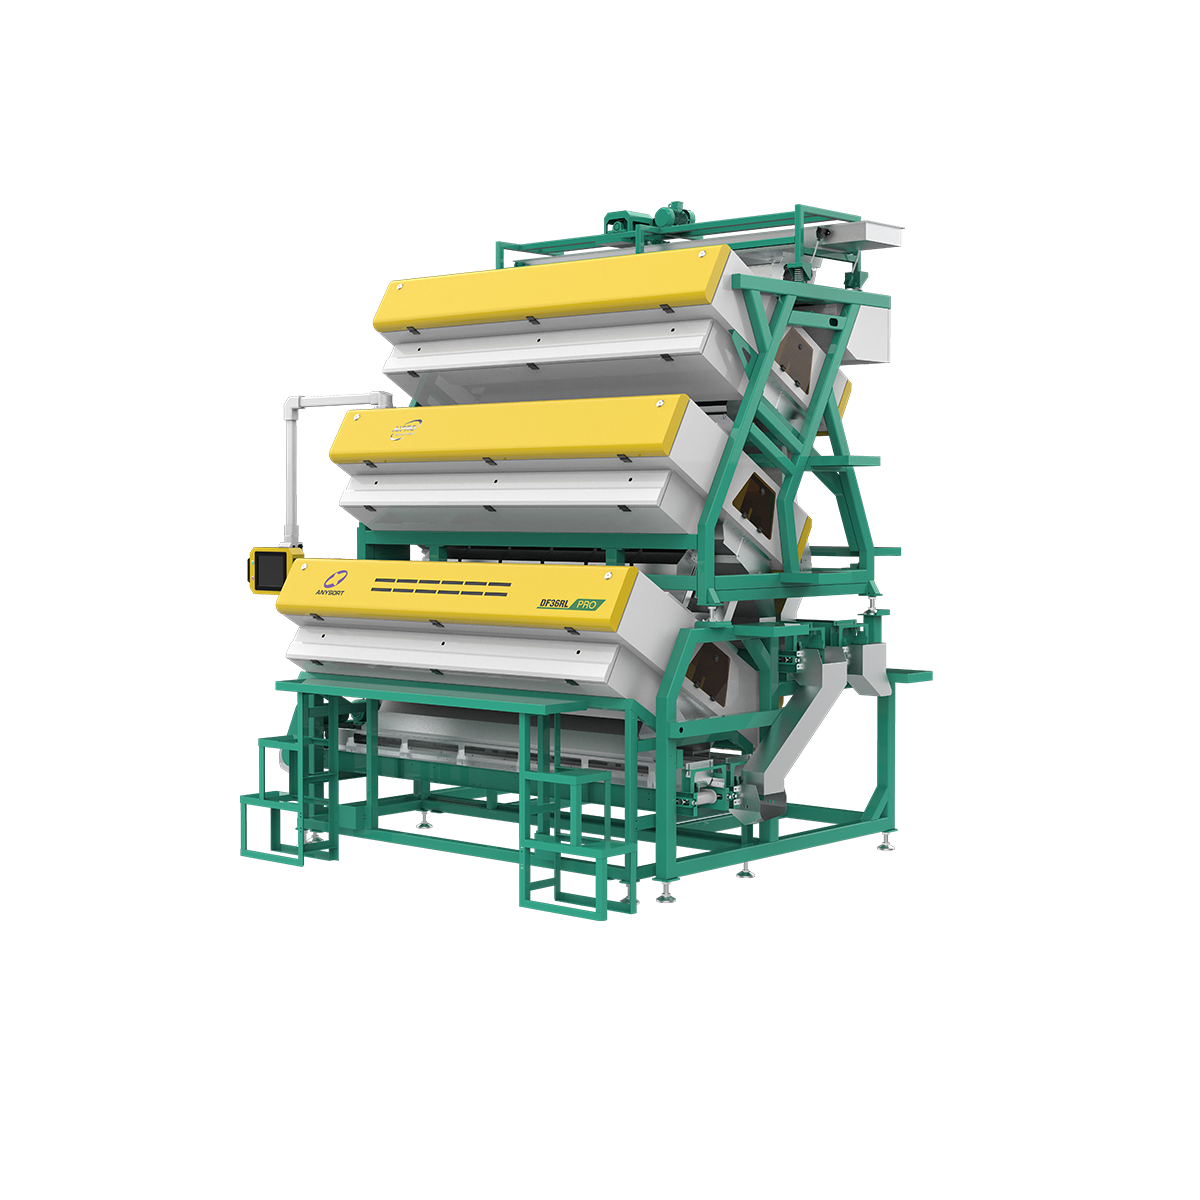
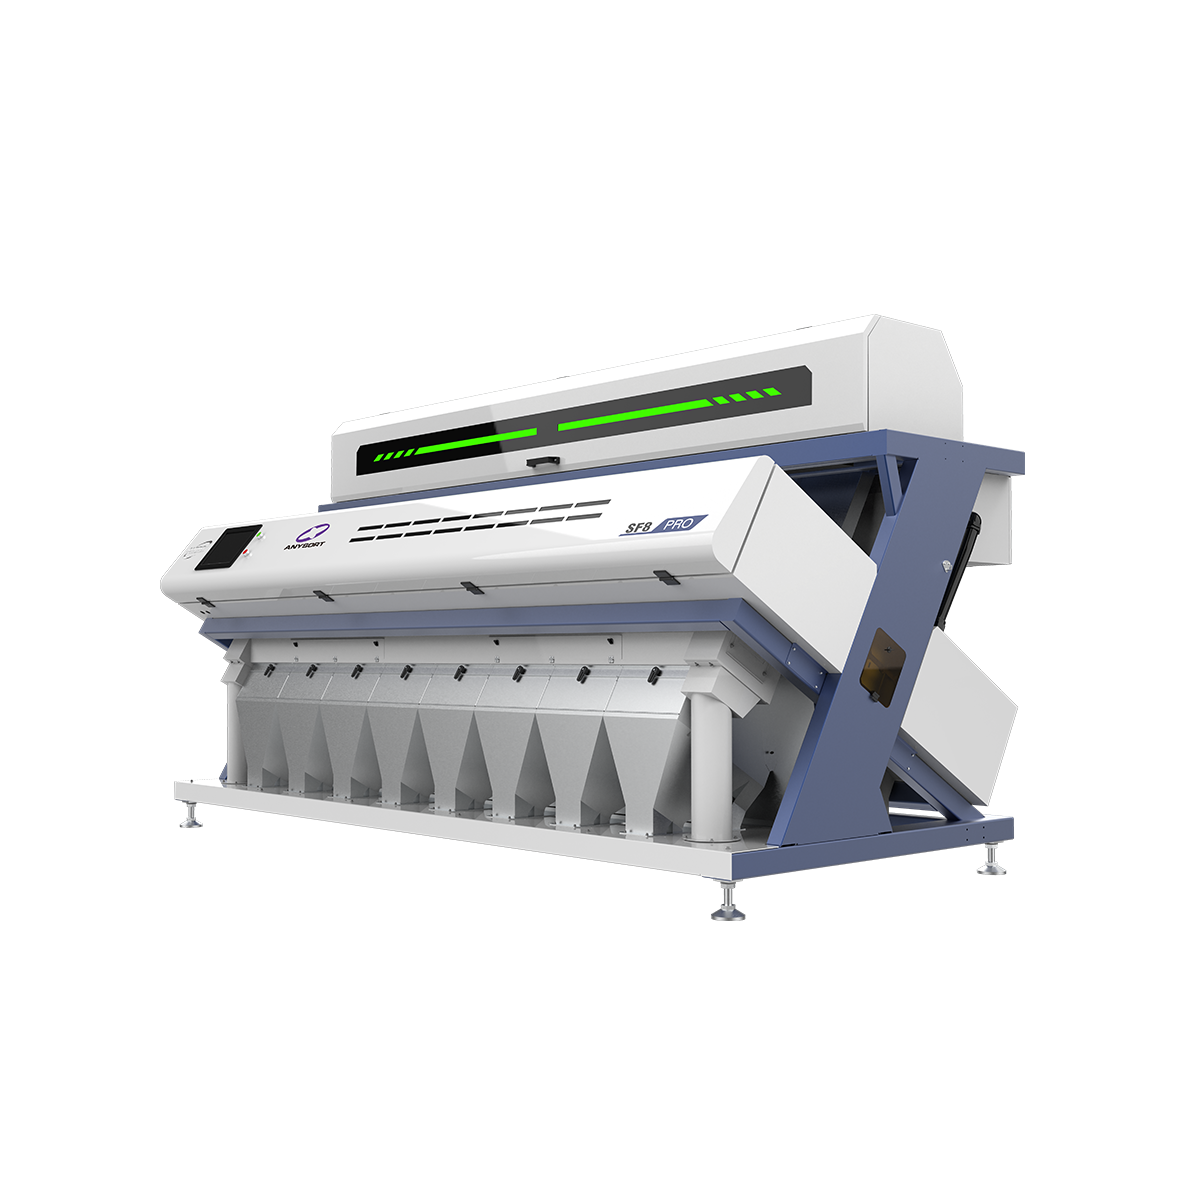
Best sorting machines represent cutting-edge technology designed to streamline material separation and organization across diverse industries. These best sorting machines utilize advanced optical sensors, artificial intelligence, and mechanical precision to categorize items by size, color, weight, and composition with remarkable accuracy. The primary function of best sorting machines involves automating the separation process, dramatically increasing throughput while maintaining consistent quality standards.
Modern best sorting machines incorporate sophisticated technological features including high-speed cameras, laser detection systems, and machine learning algorithms that continuously improve sorting accuracy. These systems process thousands of items per minute, reducing manual labor requirements and human error significantly. Best sorting machines find applications in recycling facilities, food processing plants, agricultural operations, manufacturing environments, and postal services.
The technological architecture of best sorting machines enables real-time decision-making through integrated computer vision systems. Operators can customize sorting parameters to meet specific requirements, making best sorting machines exceptionally versatile across different material types. Advanced best sorting machines feature modular designs, allowing businesses to scale operations as demand increases. Integration with existing production lines occurs seamlessly, minimizing disruption during implementation. These machines deliver exceptional performance metrics, processing diverse materials with precision that surpasses manual sorting capabilities by substantial margins.

 EN