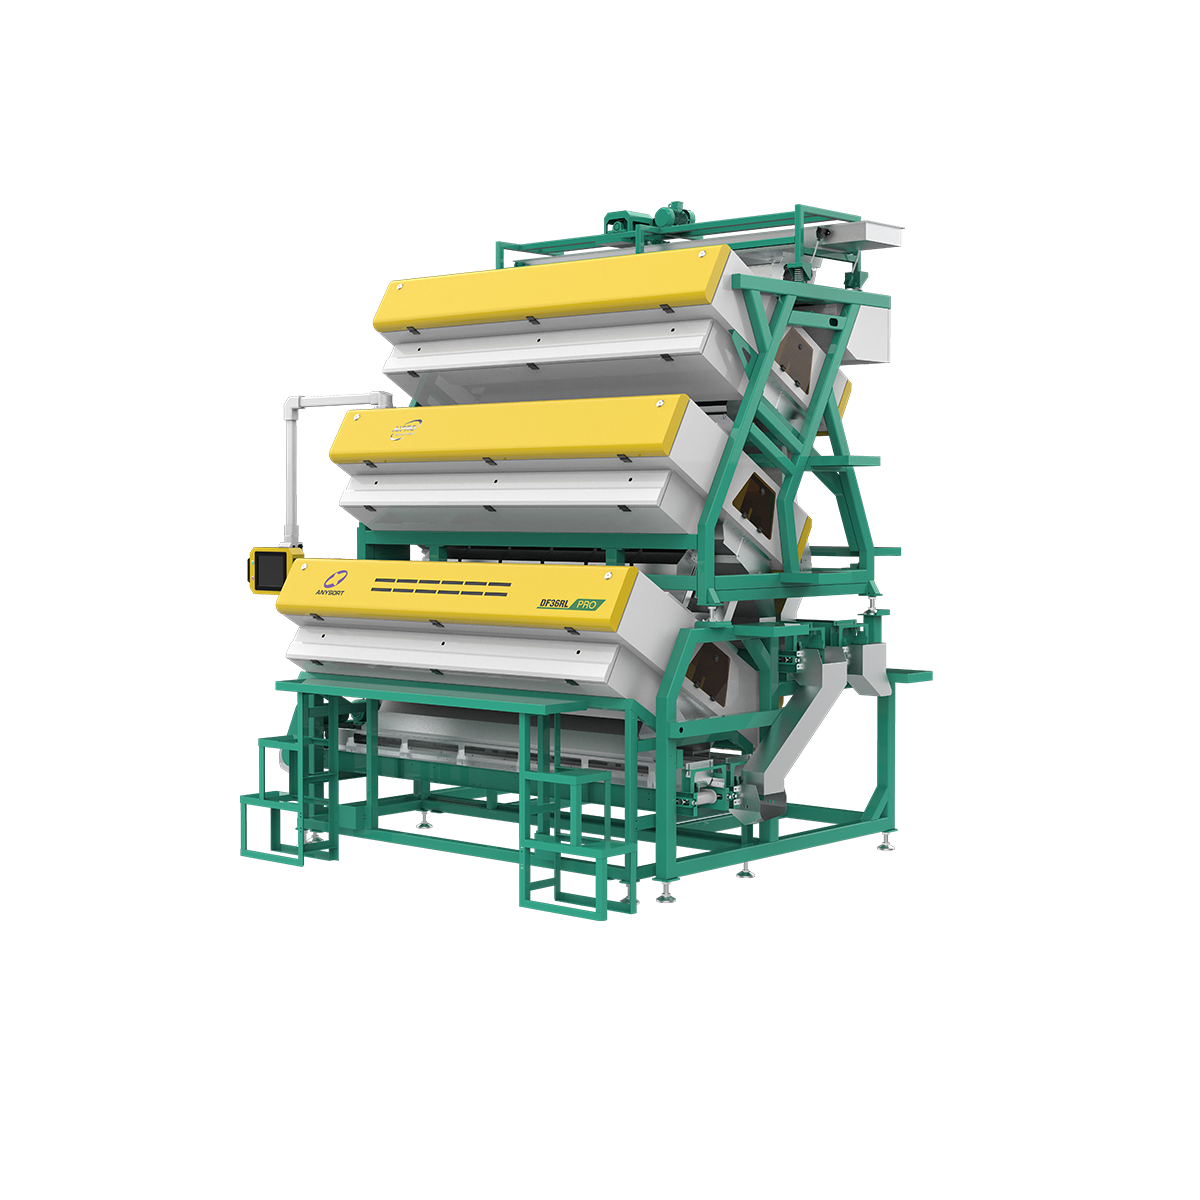
sorting equipment
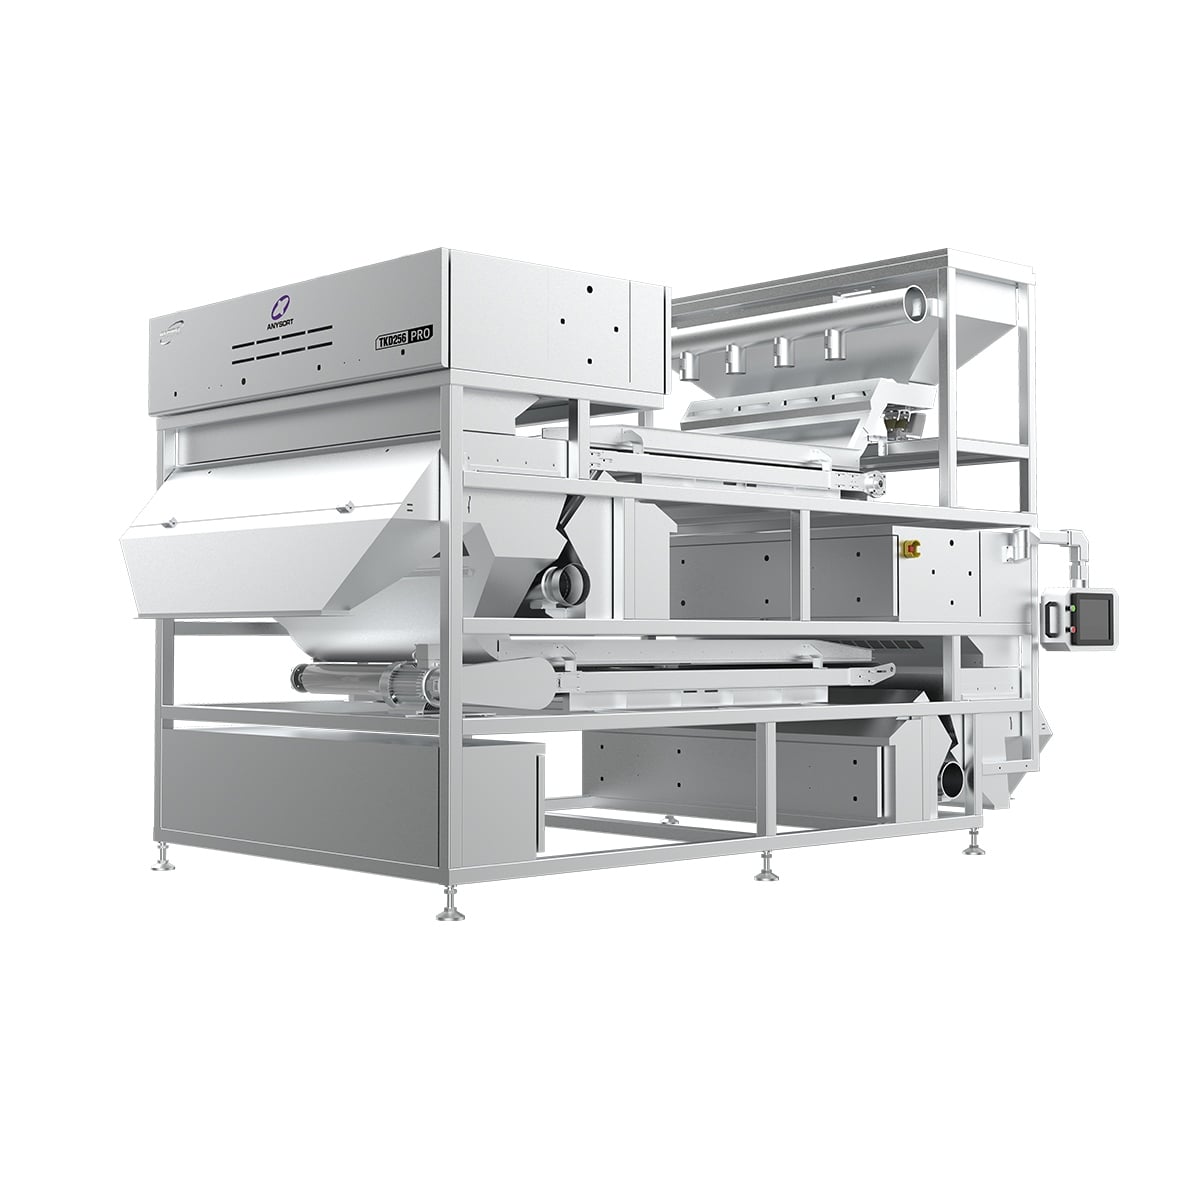
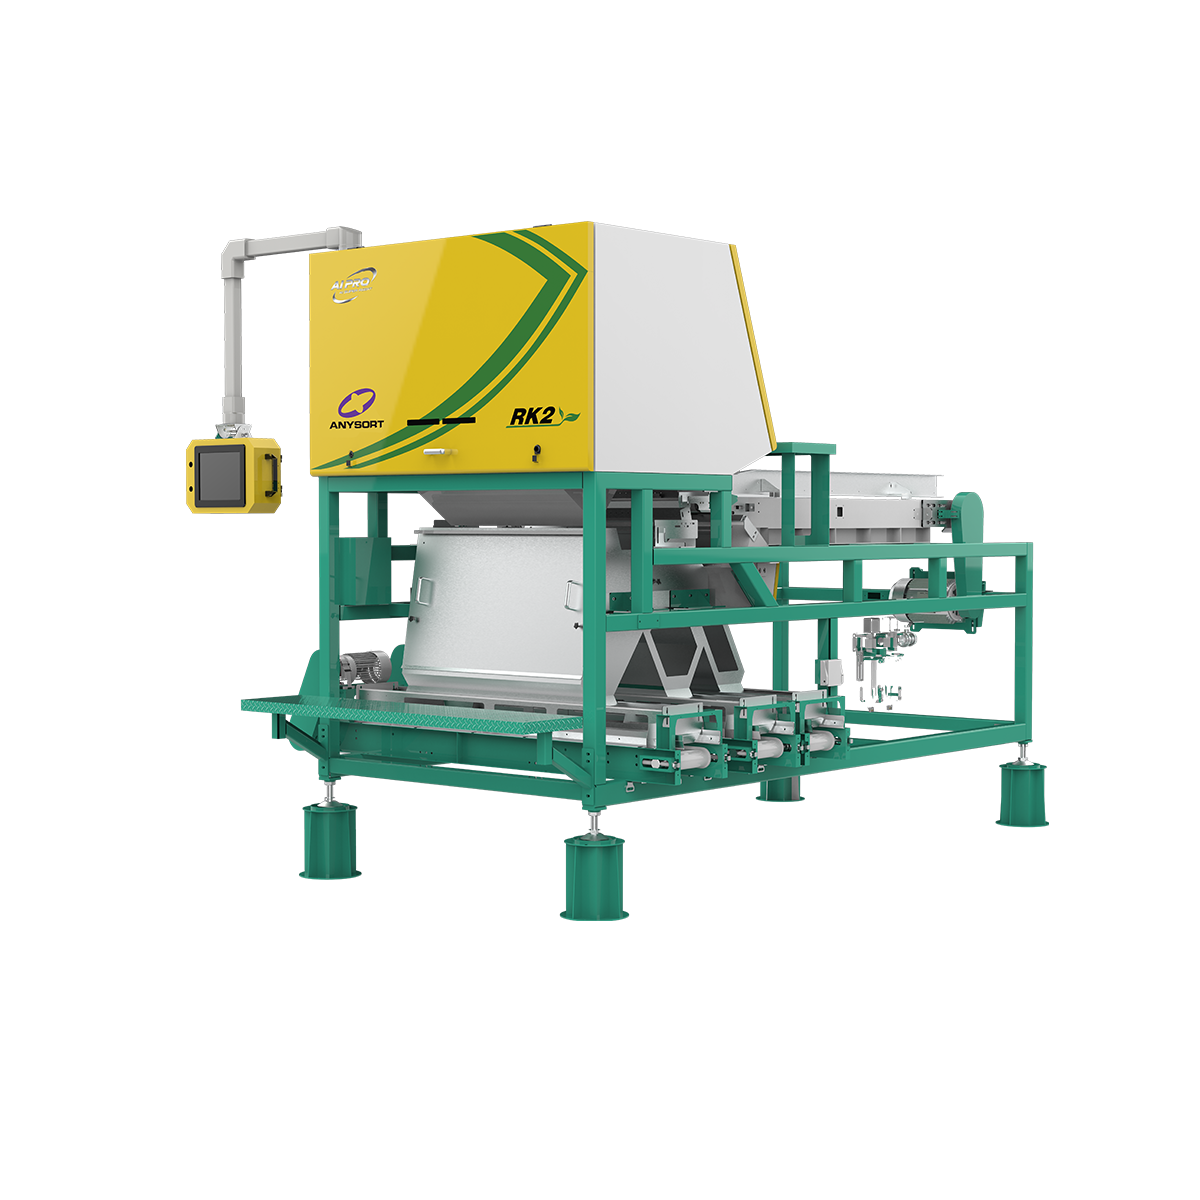
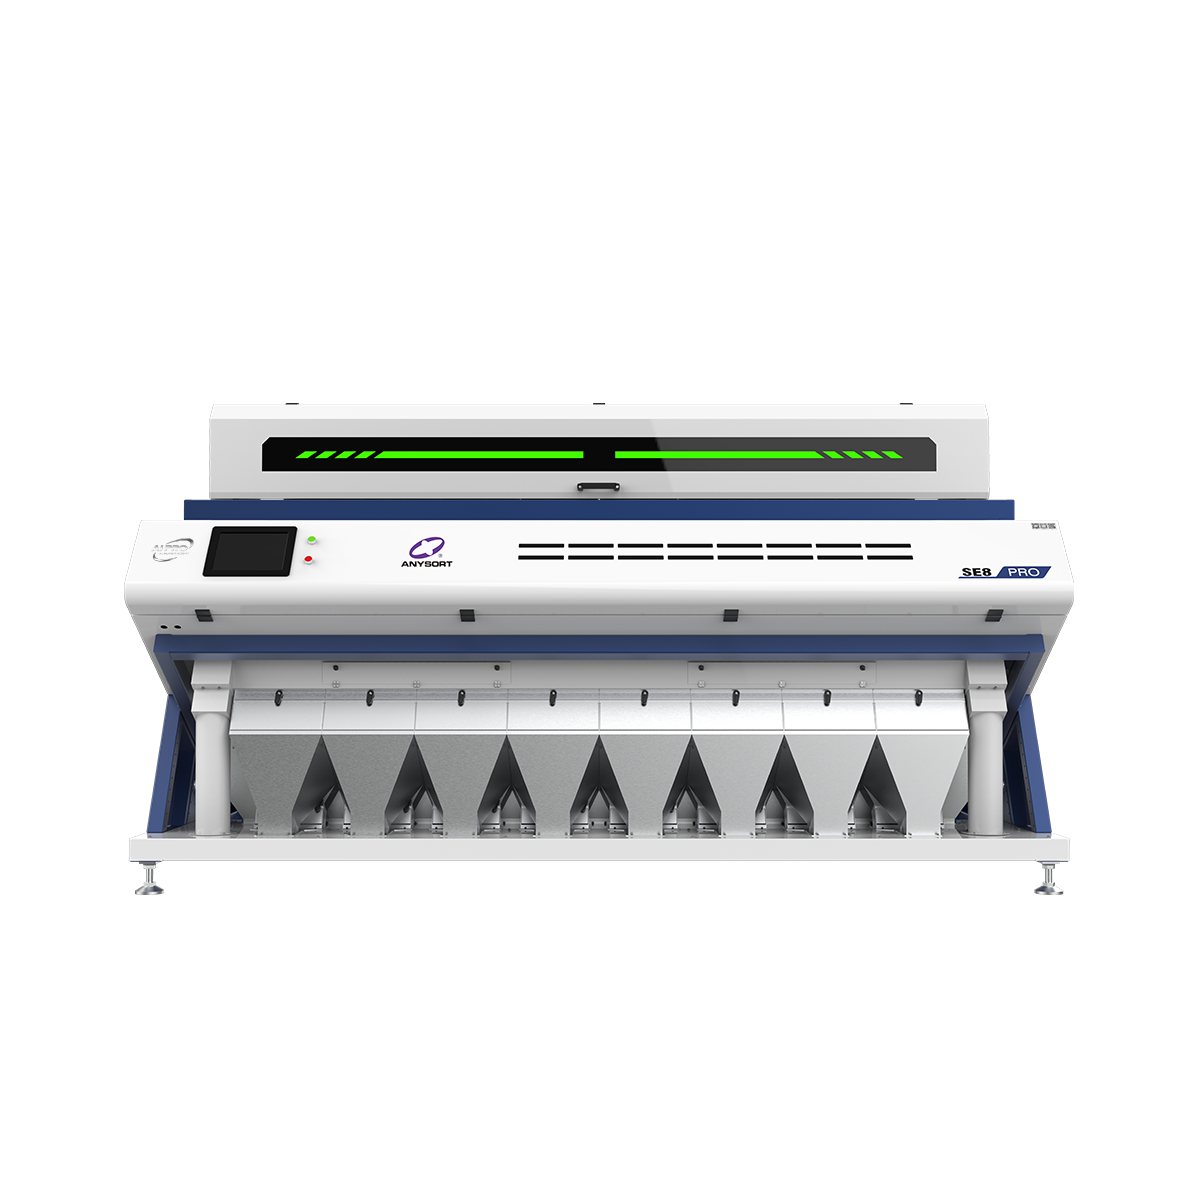
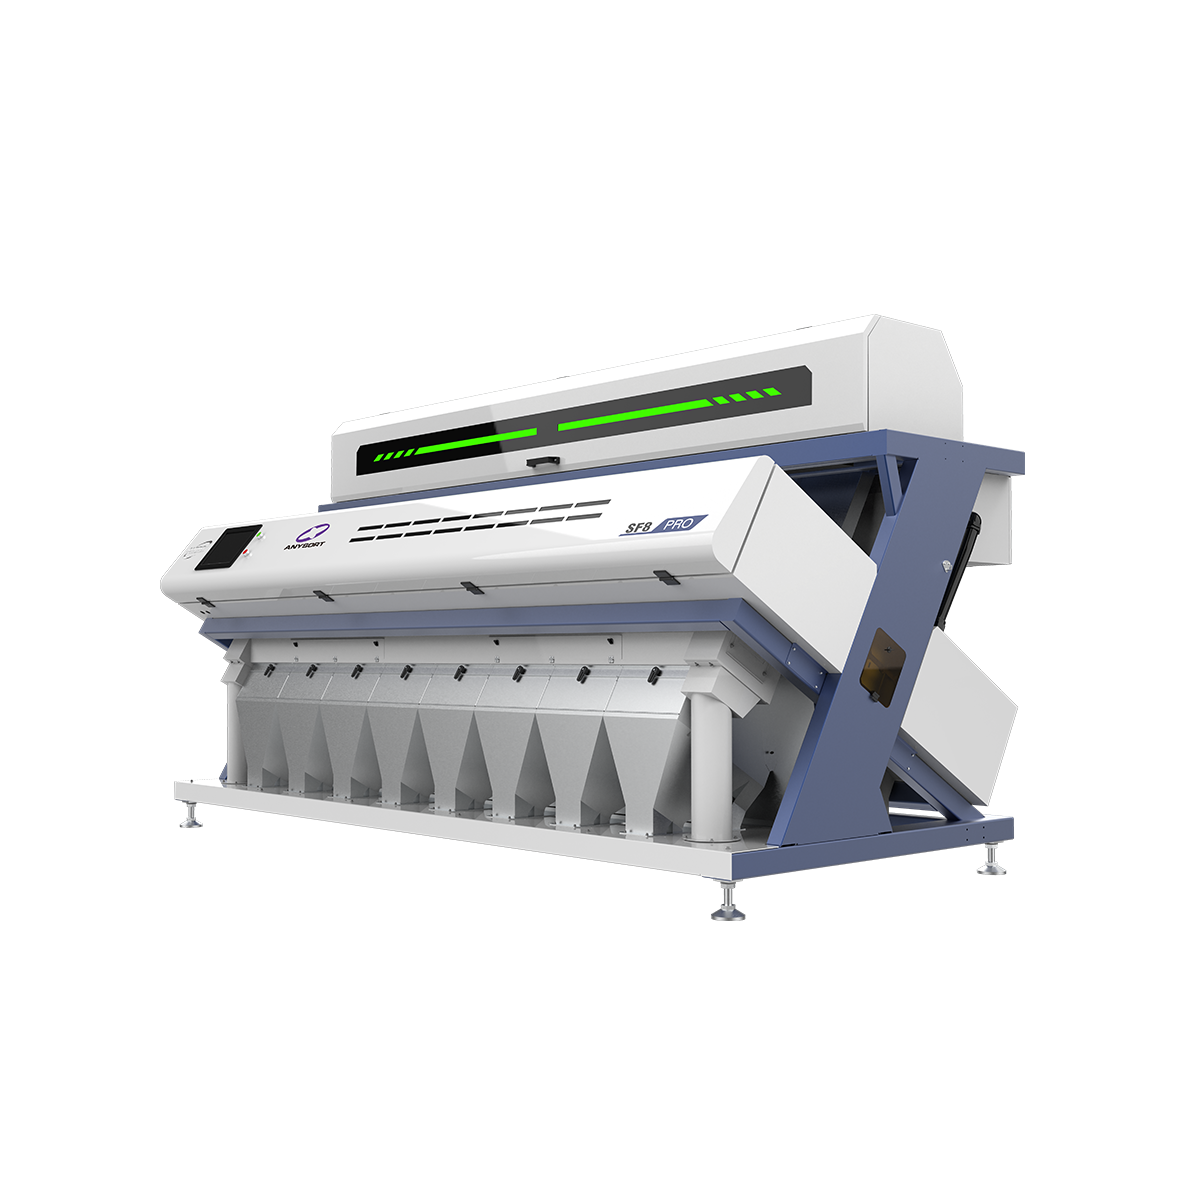
Sorting equipment represents a cornerstone technology in modern industrial operations, designed to streamline material handling and enhance operational efficiency across diverse sectors. This specialized machinery automates the process of categorizing, organizing, and separating items based on predetermined criteria, including size, weight, color, and destination. Modern sorting equipment utilizes advanced technological features such as optical scanning systems, artificial intelligence algorithms, and high-speed conveyor mechanisms to process thousands of items per hour with exceptional accuracy. The core function of sorting equipment involves receiving mixed batches of products and rapidly distributing them into appropriate categories or channels, eliminating manual labor and reducing human error significantly. Sorting equipment finds extensive applications in logistics and warehousing, where it accelerates package distribution to correct destinations. In the food industry, sorting equipment ensures quality control by removing defective products and contaminants. Manufacturing facilities rely on sorting equipment to organize components for assembly lines, while recycling centers depend on this technology to separate recyclable materials efficiently. The technological advancement in sorting equipment now includes machine learning capabilities, enabling systems to adapt and improve performance continuously. Real-time monitoring systems provide operators with comprehensive data about throughput rates, operational status, and maintenance needs. Whether handling e-commerce shipments, agricultural products, or industrial components, sorting equipment has become indispensable for businesses seeking competitive advantages through automation and precision.

 EN