Wheat Color Sorter | Grain Quality Sorting

All Categories

wheat color sorter

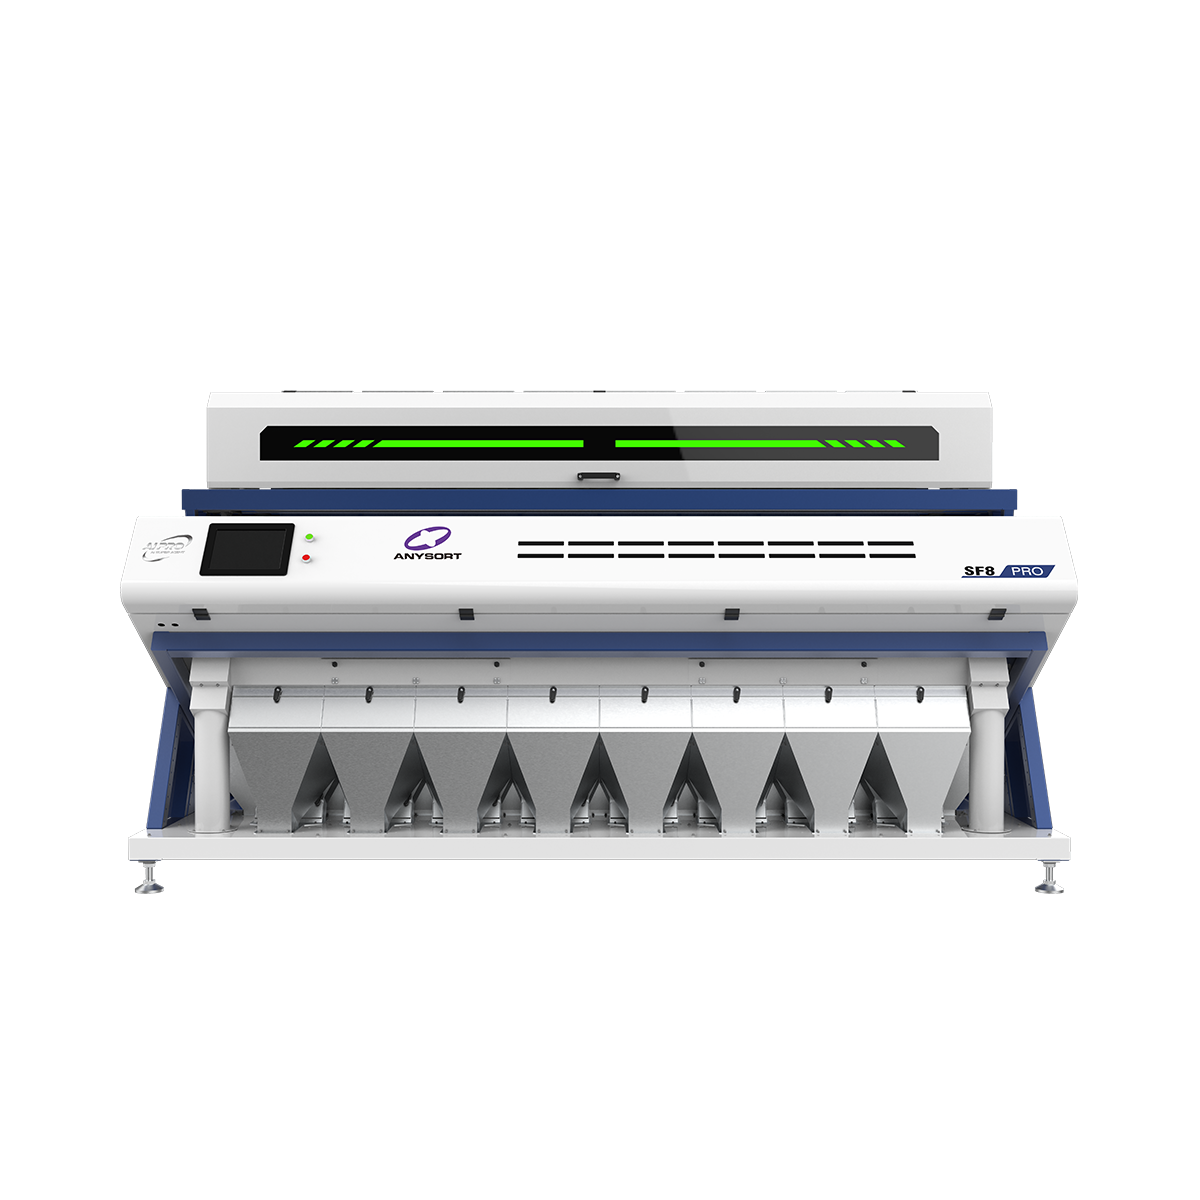
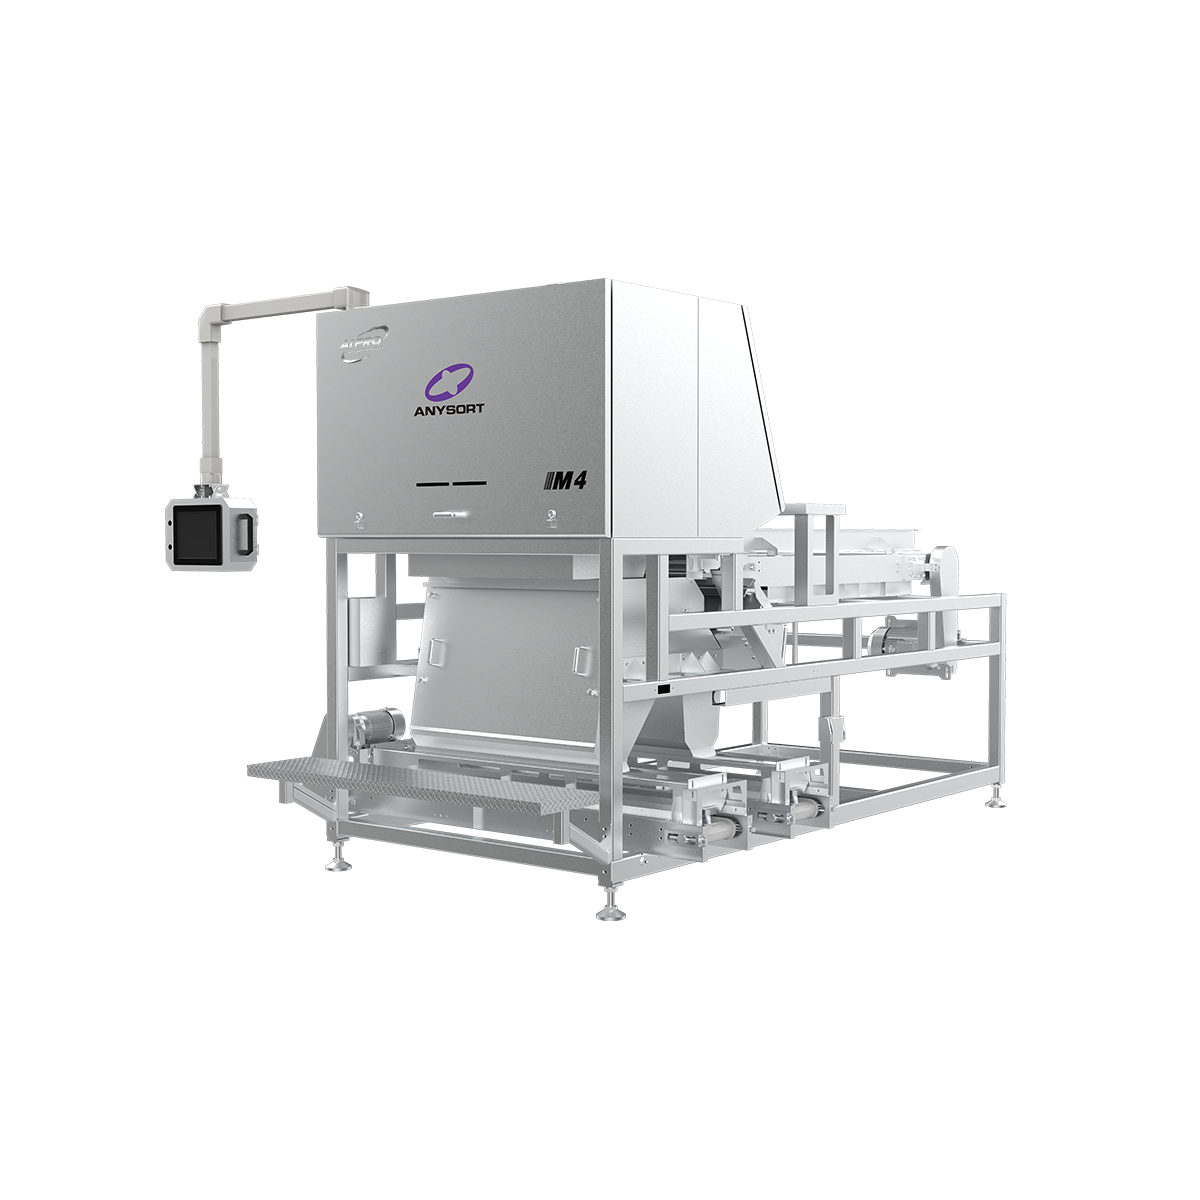
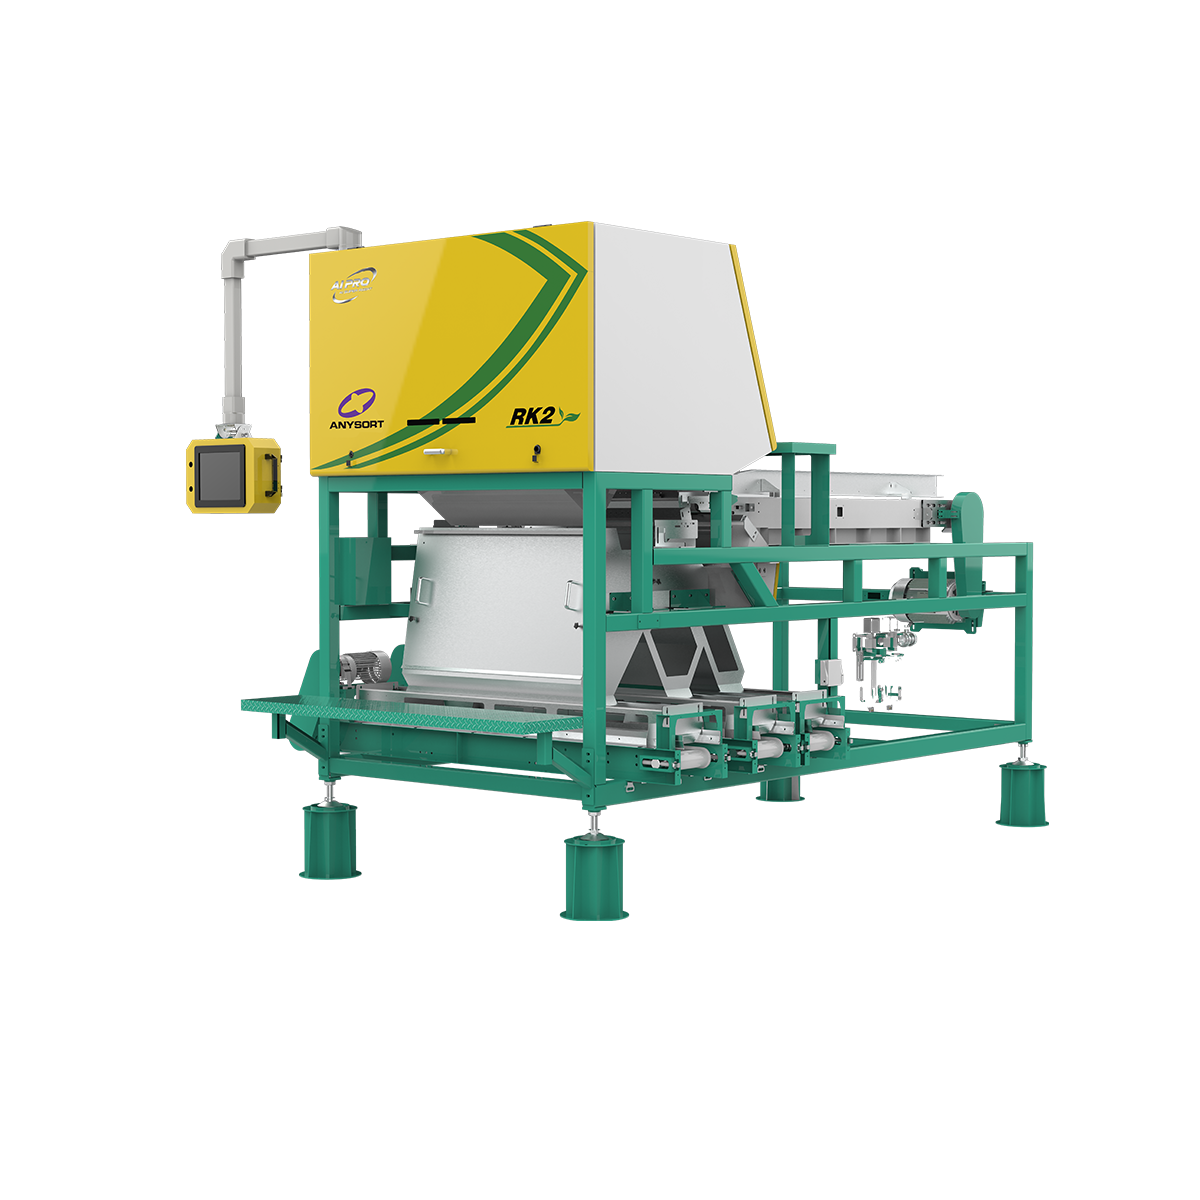
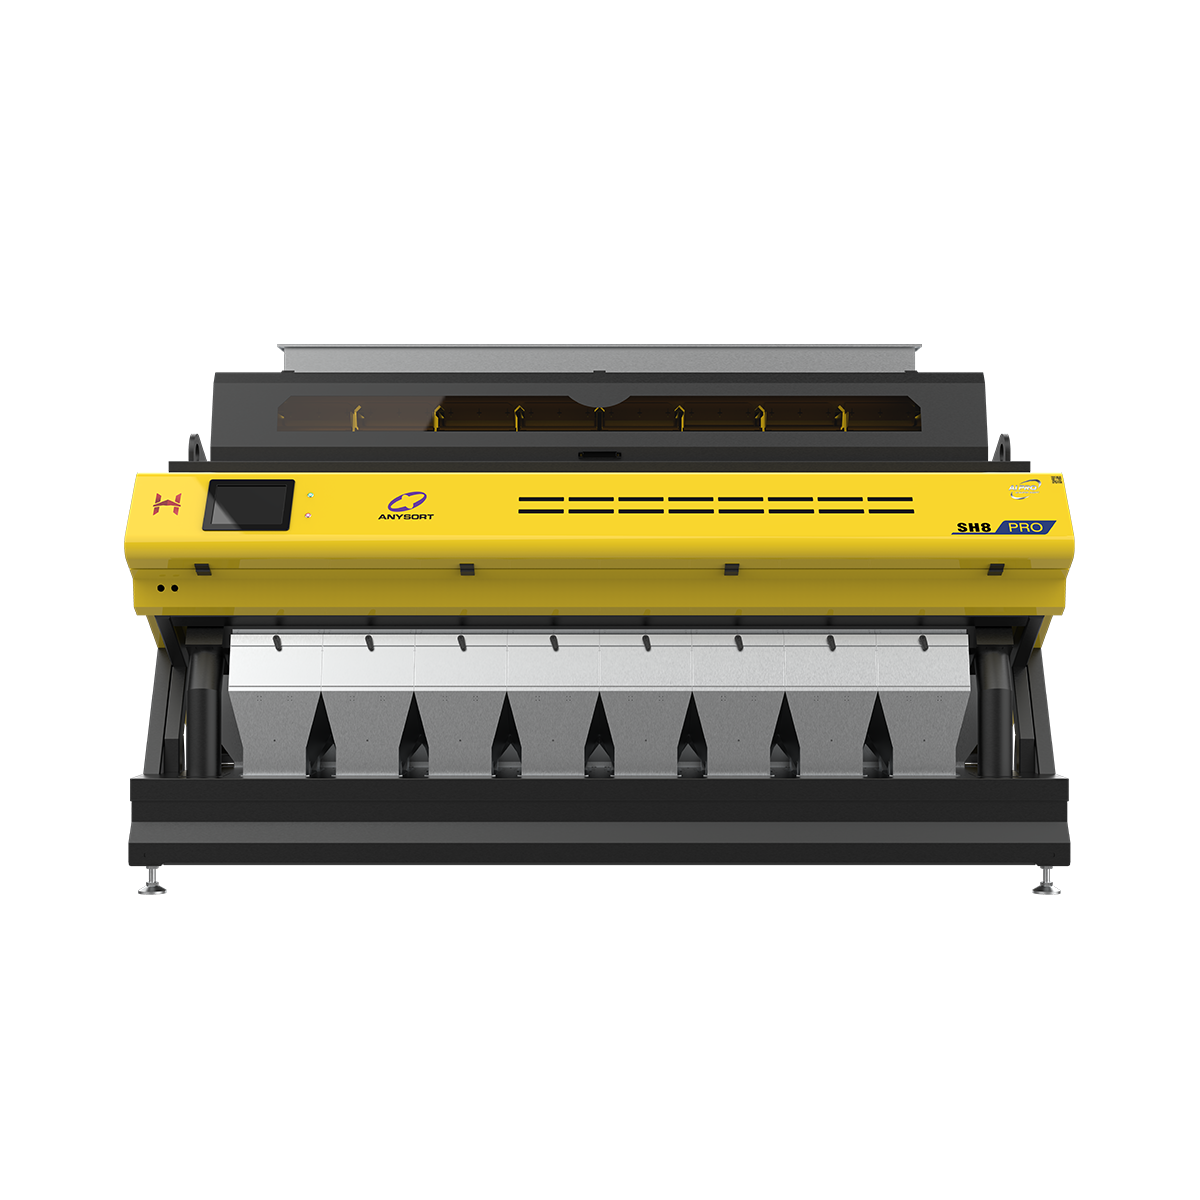
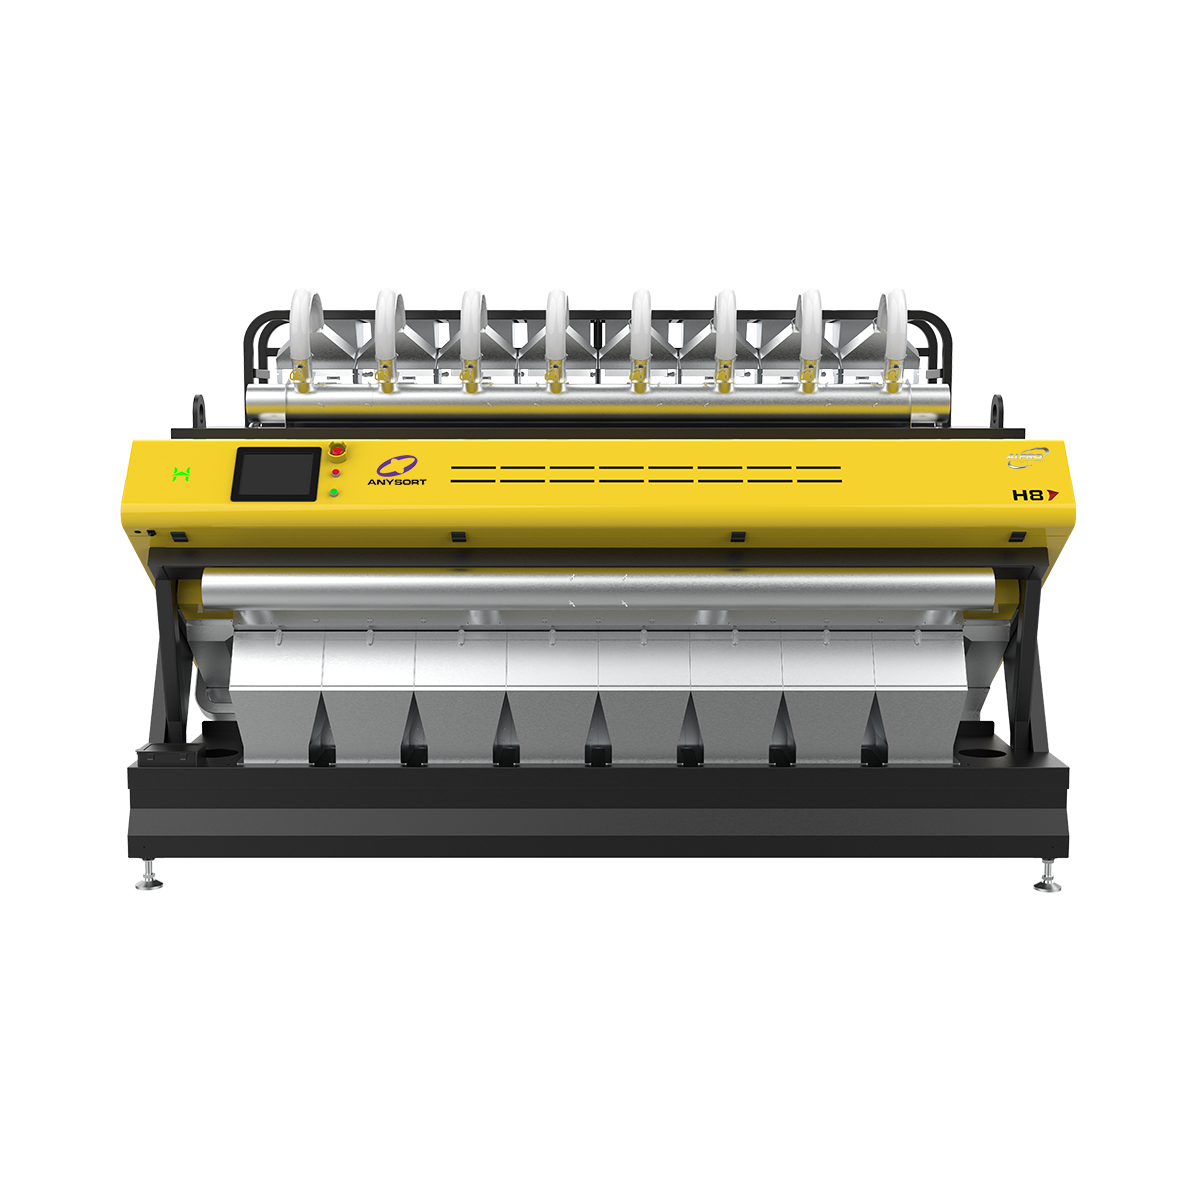
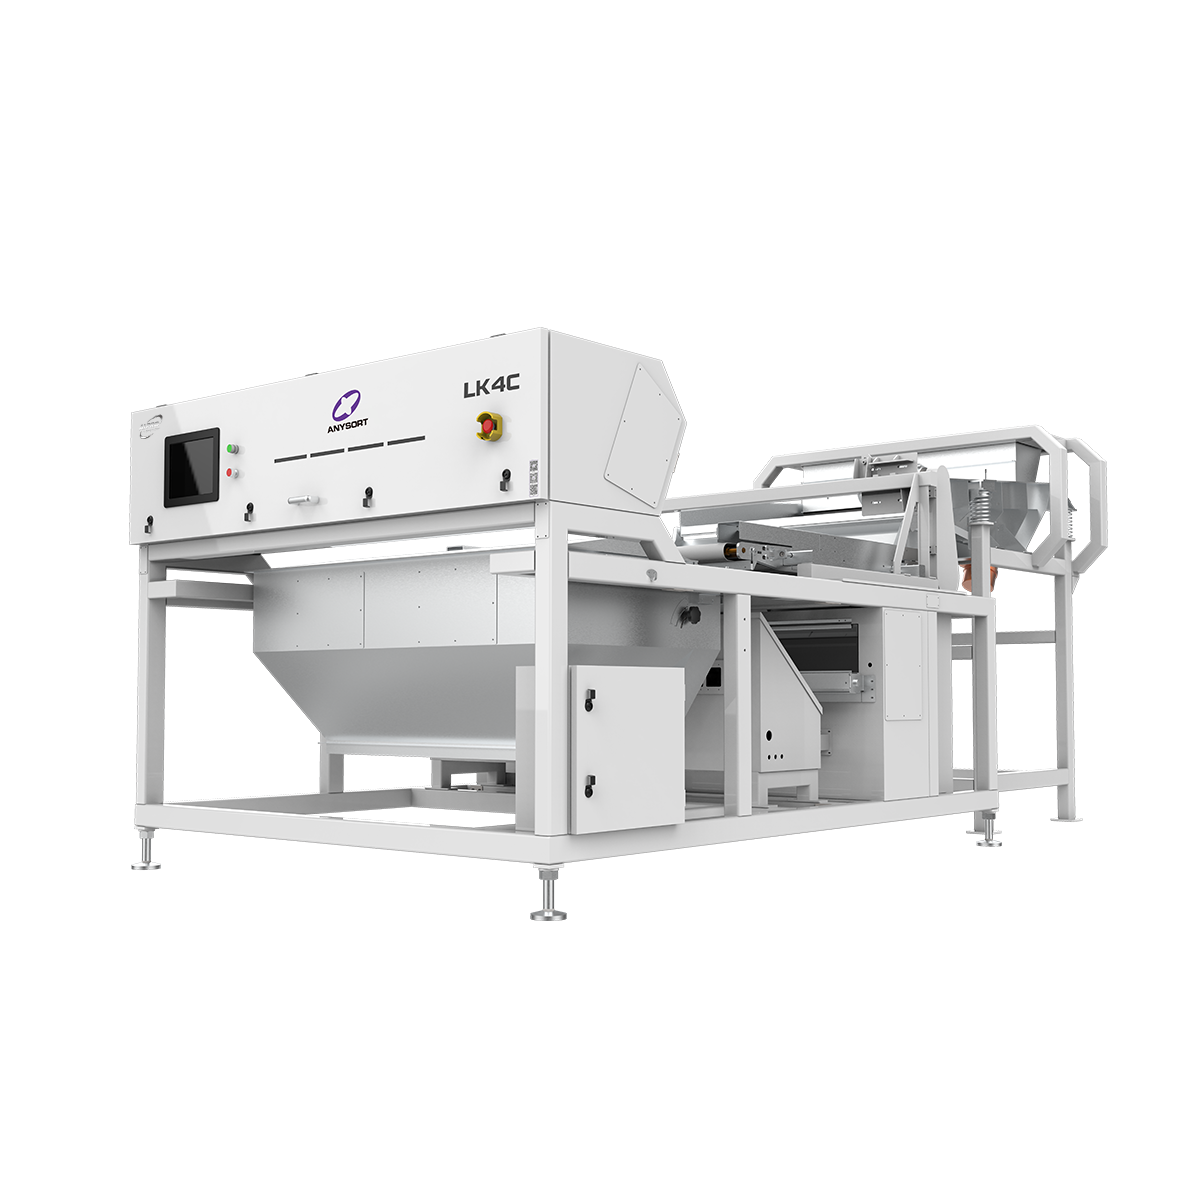
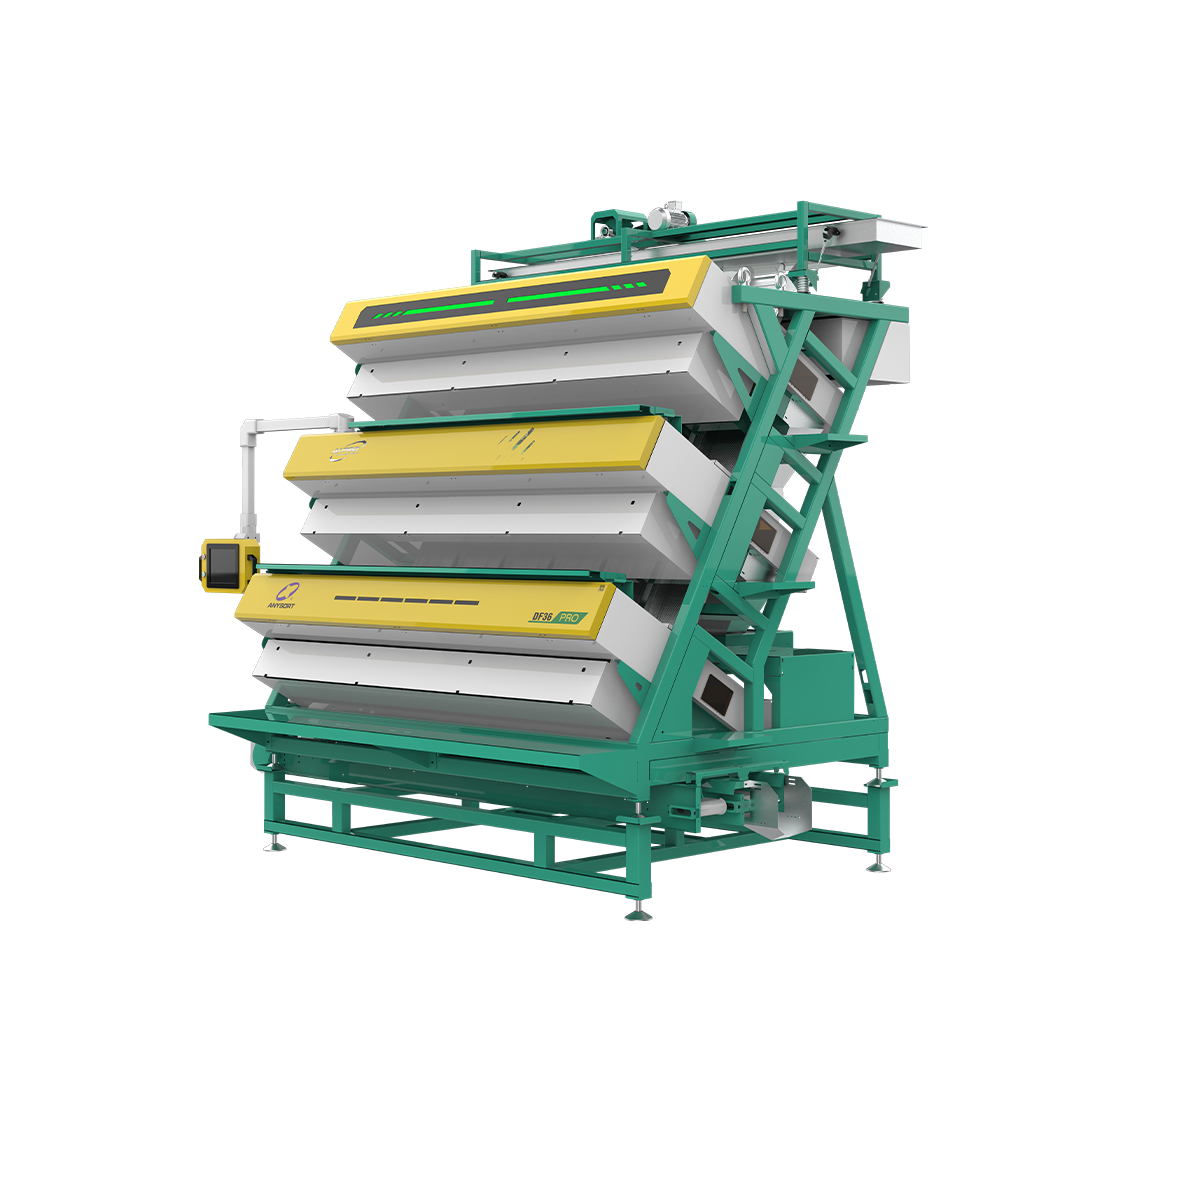
A wheat color sorter is an advanced optical sorting machine designed to automatically detect and separate wheat grains based on color variations and quality indicators. This innovative wheat color sorter technology uses high-speed cameras and sophisticated image processing algorithms to examine each grain individually, ensuring only premium-quality wheat reaches your final product. The wheat color sorter operates by directing wheat grains across a illuminated inspection chamber where sensors capture detailed color data. The system analyzes this information in milliseconds, identifying discolored grains, foreign materials, and damaged kernels with exceptional precision. Modern wheat color sorter equipment can process up to 15 tons of grain per hour while maintaining accuracy rates exceeding 99 percent. The wheat color sorter is equipped with adjustable ejection mechanisms that precisely remove defective grains using compressed air or mechanical systems. This technological advancement represents a significant upgrade from traditional manual sorting methods, which are time-consuming and inconsistent. The wheat color sorter integrates seamlessly into grain processing lines, connecting directly to cleaning equipment and storage systems. Its compact design allows installation in existing facilities without requiring extensive modifications. The wheat color sorter delivers consistent results regardless of lighting conditions or environmental factors, thanks to standardized LED illumination and temperature-controlled components. By implementing a wheat color sorter in your grain processing operation, you ensure product quality, reduce waste, and meet stringent market standards for premium wheat products.

New Products

The wheat color sorter delivers exceptional practical benefits that directly improve your grain processing operation and bottom line. First, this wheat color sorter significantly reduces manual labor requirements, as automated sorting handles thousands of grains per minute without human intervention or fatigue-related errors. Operators simply monitor the system rather than performing repetitive, eye-straining work. Second, your wheat color sorter achieves higher purity levels than manual sorting methods, ensuring only suitable grains pass through to packaging. This quality improvement directly impacts your product reputation and customer satisfaction. Third, implementing a wheat color sorter dramatically reduces waste by accurately identifying and removing only genuinely defective grains, maximizing your yield from each batch. Fourth, the wheat color sorter operates continuously throughout your production schedule, maintaining consistent output without slowdowns during peak processing seasons. Fifth, this wheat color sorter system reduces contamination risks by removing foreign objects and diseased grains that could compromise product safety. Sixth, investing in a wheat color sorter positions your business competitively in premium markets that demand superior grain quality. Seventh, the wheat color sorter's detailed sorting data provides valuable insights into your grain batches, helping identify supplier quality trends and processing improvements. Eighth, this technology reduces energy consumption compared to alternative quality-control methods. Ninth, a wheat color sorter investment typically recovers its cost within 1-2 years through improved product value and reduced waste. Finally, modern wheat color sorter equipment requires minimal maintenance, with easily replaceable components and intuitive operational interfaces designed for standard production staff.

Tips And Tricks

How Does Nuts Sorter Technology Ensure Quality?

19

Aug

How Does Nuts Sorter Technology Ensure Quality?

The global nuts processing industry relies on precision and consistency to meet strict quality standards and regulatory requirements. A nuts sorter has become indispensable for processors seeking to eliminate defects, contaminants, and substandard pr...
View More
How does optical sorting technology detect defective rice grains?

22

Aug

How does optical sorting technology detect defective rice grains?

Modern rice processing demands precision and consistency, which is why understanding the detection mechanisms behind advanced equipment has become essential for producers. A rice color sorter represents one of the most significant technological break...
View More
How Do Color Sorters Improve Product Quality?

26

Aug

How Do Color Sorters Improve Product Quality?

Product quality stands as a critical differentiator in competitive industrial markets, and achieving consistency at scale requires more than manual oversight. A color sorter represents one of the most effective technologies for identifying and removi...
View More
Top AI Color Sorter Manufacturers in China (2026)

30

Aug

Top AI Color Sorter Manufacturers in China (2026)

The global demand for precision sorting technology has surged dramatically, with color sorter machine manufacturers in China leading innovation across agricultural and industrial sectors. Chinese color sorter machine manufacturers have established th...
View More

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

wheat color sorter

Precision Optical Detection Technology

Precision Optical Detection Technology

The wheat color sorter employs cutting-edge optical sensor technology that scans every single grain passing through the machine. Using advanced LED lighting systems combined with high-resolution cameras, this wheat color sorter captures detailed color profiles of each kernel in fractions of a second. The system's artificial intelligence algorithms compare captured images against established quality parameters, identifying even subtle color deviations that indicate quality issues. This wheat color sorter technology distinguishes between naturally darker grains and genuinely defective ones, preventing unnecessary waste while maintaining strict quality standards. The precision detection capability of a wheat color sorter ensures that your final product meets buyer specifications consistently, grain after grain. This technological sophistication means your wheat color sorter eliminates subjective human judgment, replacing it with objective, measurable data-driven sorting decisions. Whether processing millions of grains daily or handling specialty batches, the wheat color sorter maintains unwavering accuracy that traditional sorting methods cannot match.
High-Speed Processing Capacity

High-Speed Processing Capacity

Speed represents a critical advantage of implementing a wheat color sorter in your operation. Modern wheat color sorter equipment processes grains at remarkable rates, handling 10 to 15 tons hourly while maintaining exceptional accuracy standards. This processing capacity means your wheat color sorter completes in minutes what would require hours of manual sorting work. The wheat color sorter's rapid throughput directly translates to increased production efficiency and reduced processing bottlenecks. Your facility can handle larger volumes without expanding workforce requirements, making the wheat color sorter an economically attractive investment. Processing speed does not compromise accuracy; instead, your wheat color sorter simultaneously maintains both high-volume capability and quality standards. This balance distinguishes premium wheat color sorter systems from basic alternatives. Facilities implementing a wheat color sorter report production increases of 30-50 percent, demonstrating the real-world productivity gains. The equipment operates continuously throughout production shifts, requiring minimal downtime and delivering consistent performance. Your wheat color sorter provides the speed necessary to meet demanding market timelines while maintaining the quality standards that command premium prices.
Reduced Waste and Maximum Yield Optimization

Reduced Waste and Maximum Yield Optimization

Economic benefits of using a wheat color sorter extend far beyond labor savings. Your wheat color sorter minimizes waste by making intelligent sorting decisions that preserve usable grain while removing only truly defective material. Traditional methods often discard marginal-quality grains that your wheat color sorter can correctly identify as acceptable, directly increasing your sellable product volume. This yield optimization means your wheat color sorter generates additional revenue from the same raw material input. Many operators report 2-5 percent yield increases after implementing a wheat color sorter system, representing substantial profit improvement. The wheat color sorter prevents expensive recalls and reputation damage by ensuring contaminated or defective grains never reach customers. Insurance and liability concerns diminish significantly when your wheat color sorter provides documented evidence of rigorous quality control. Additionally, your wheat color sorter reduces financial losses from weather-damaged crops or difficult harvest conditions by accurately identifying salvageable grains. The detailed sorting data your wheat color sorter generates helps optimize procurement strategies and supplier relationships. These combined economic advantages make the wheat color sorter investment one of the highest-return capital improvements available for grain processing facilities.

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

Copyright © 2026 Anhui Jiexun Optoelectronic Technology Co., Ltd. All rights reserved.  -  Privacy policy