Colour Sorter for Grain | Advanced Optical Sorting

All Categories

colour sorter for grain

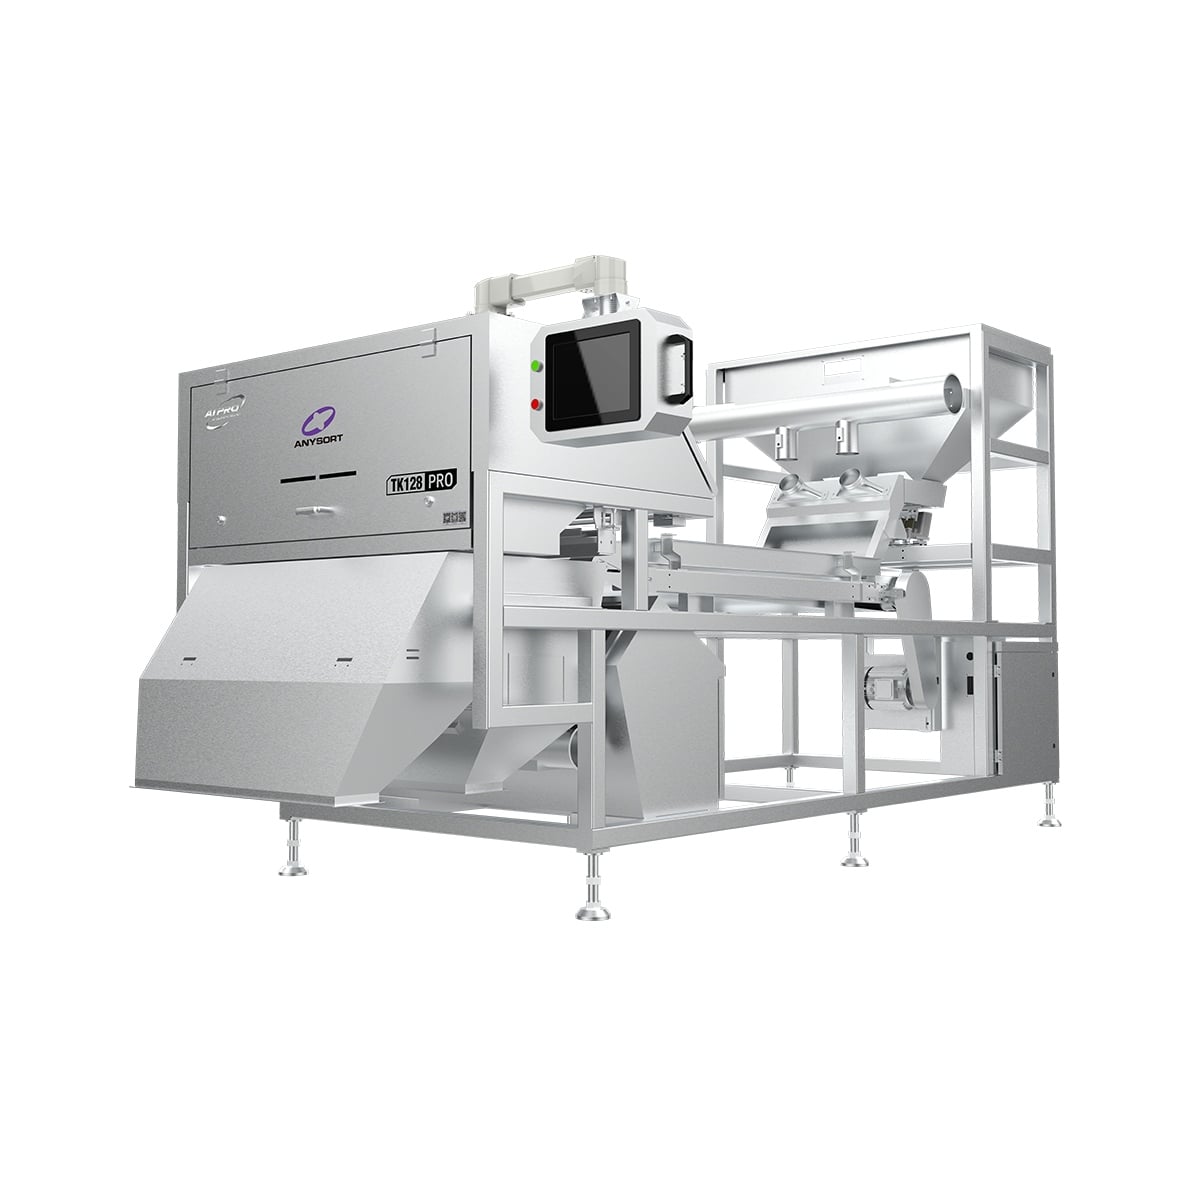
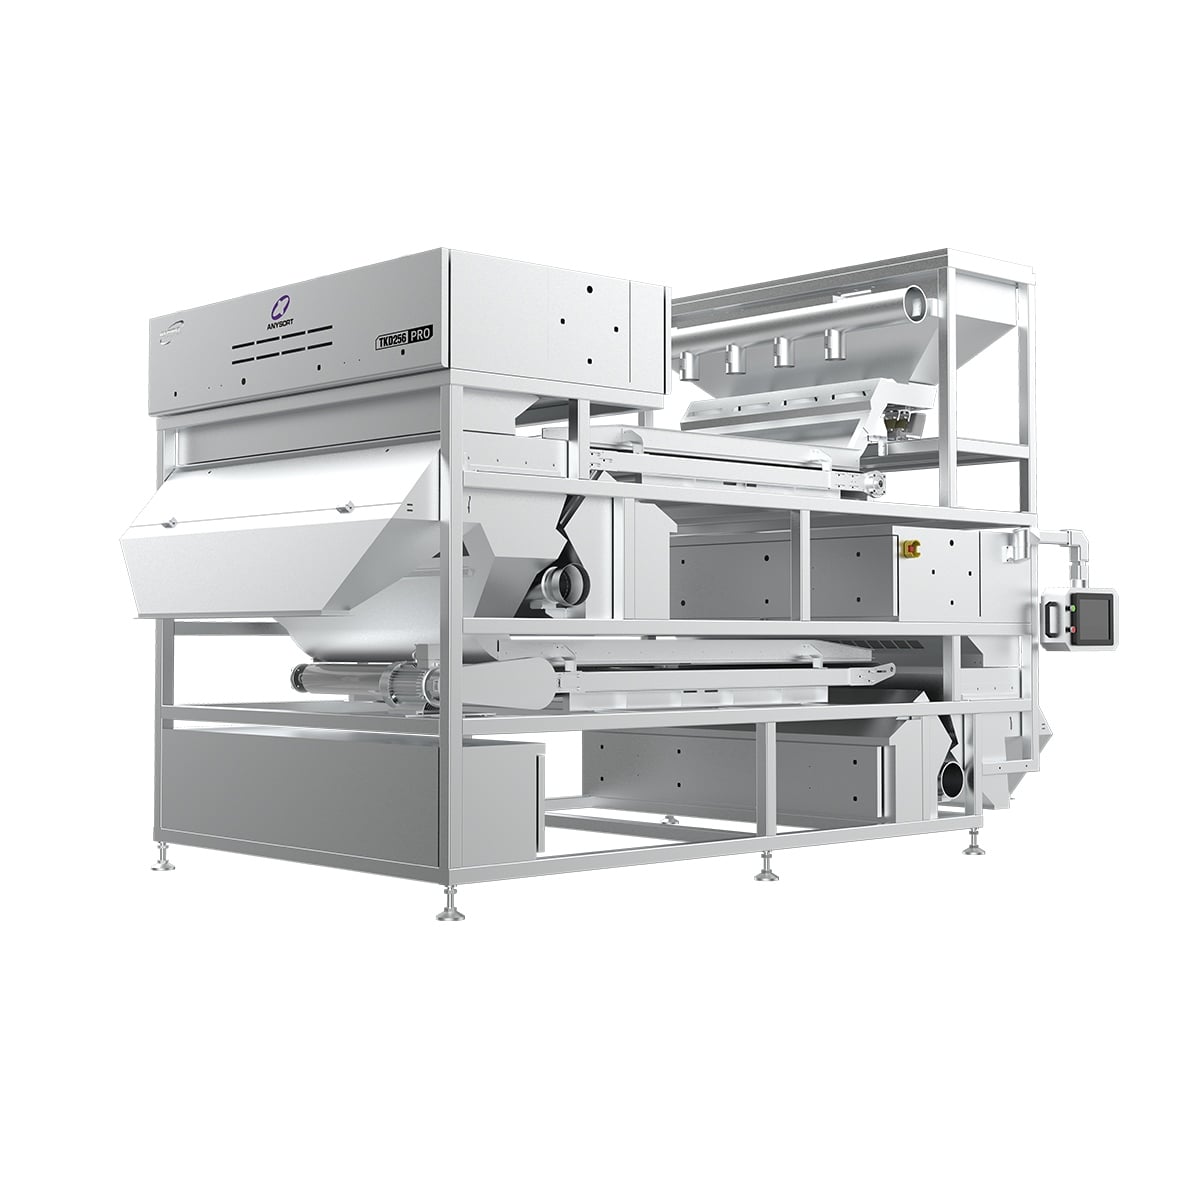
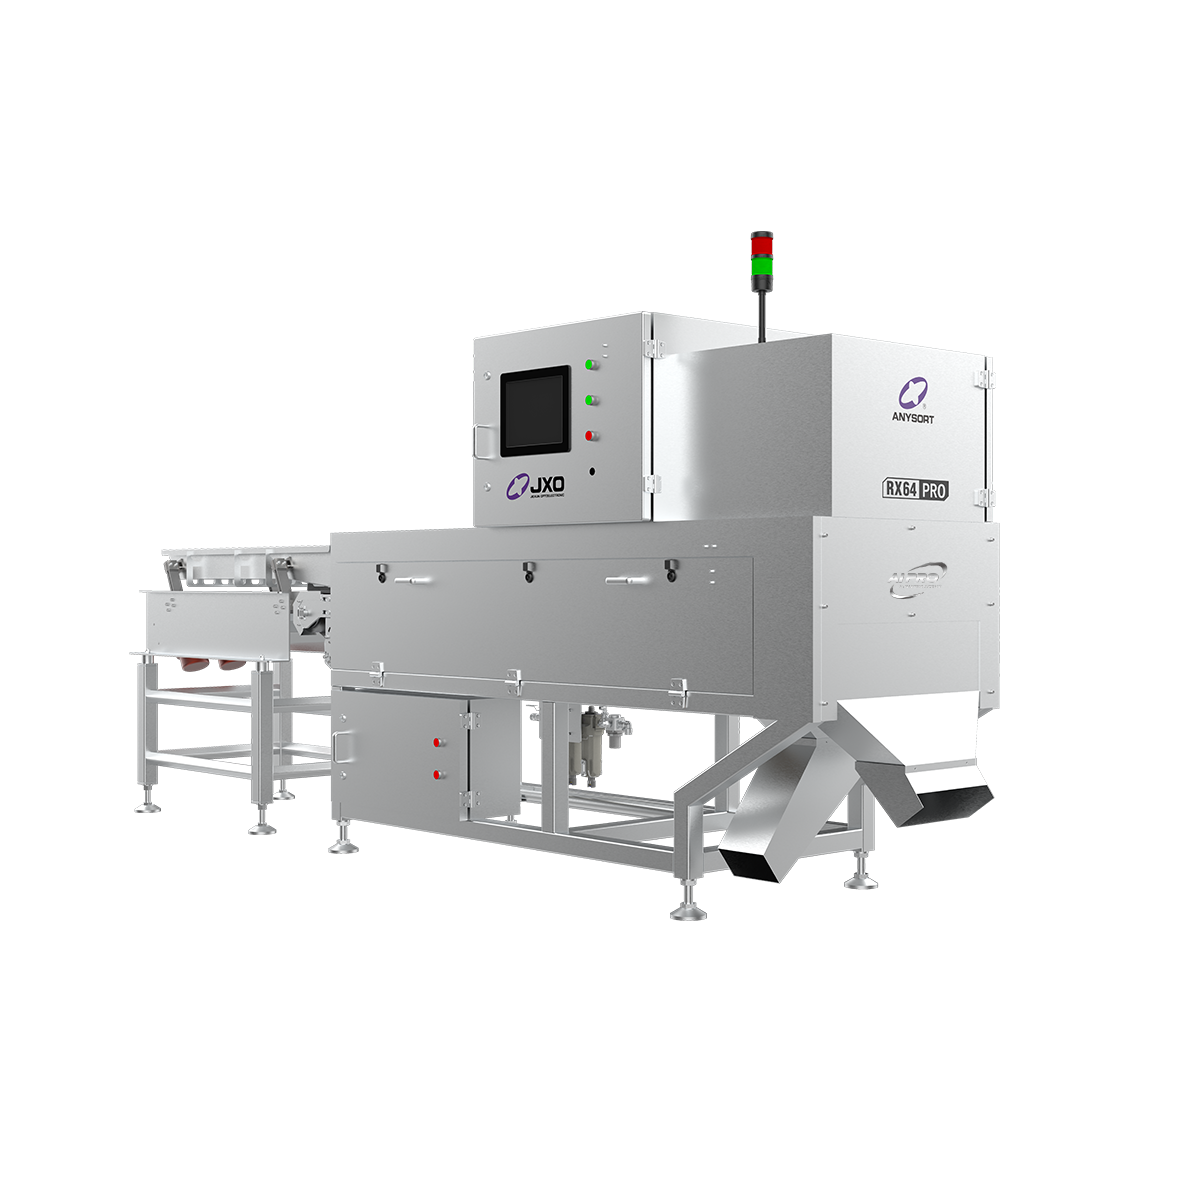
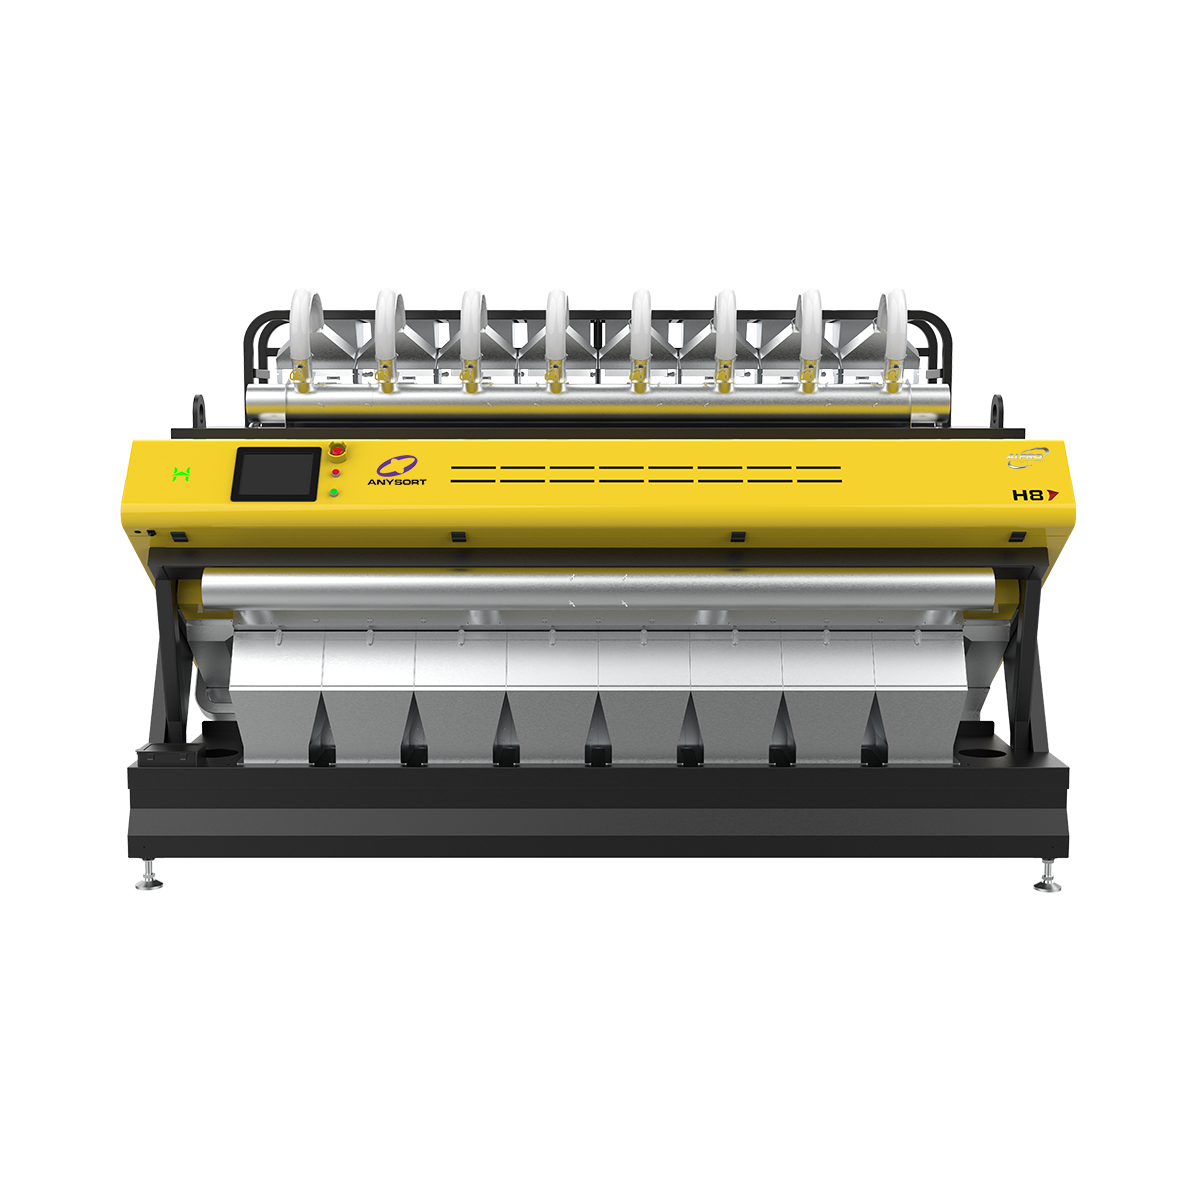
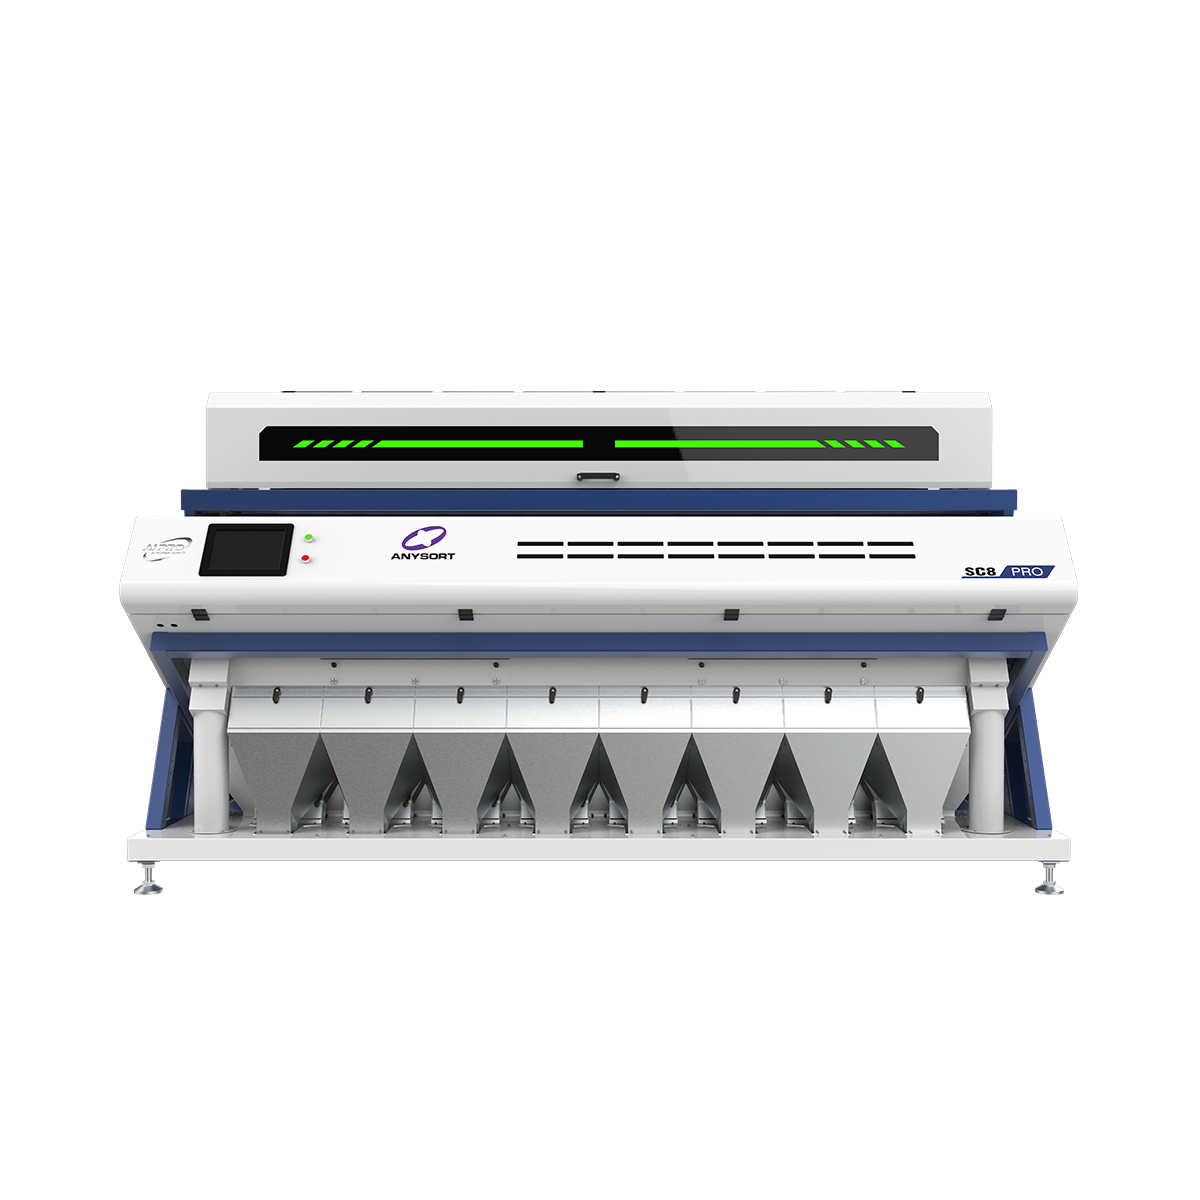
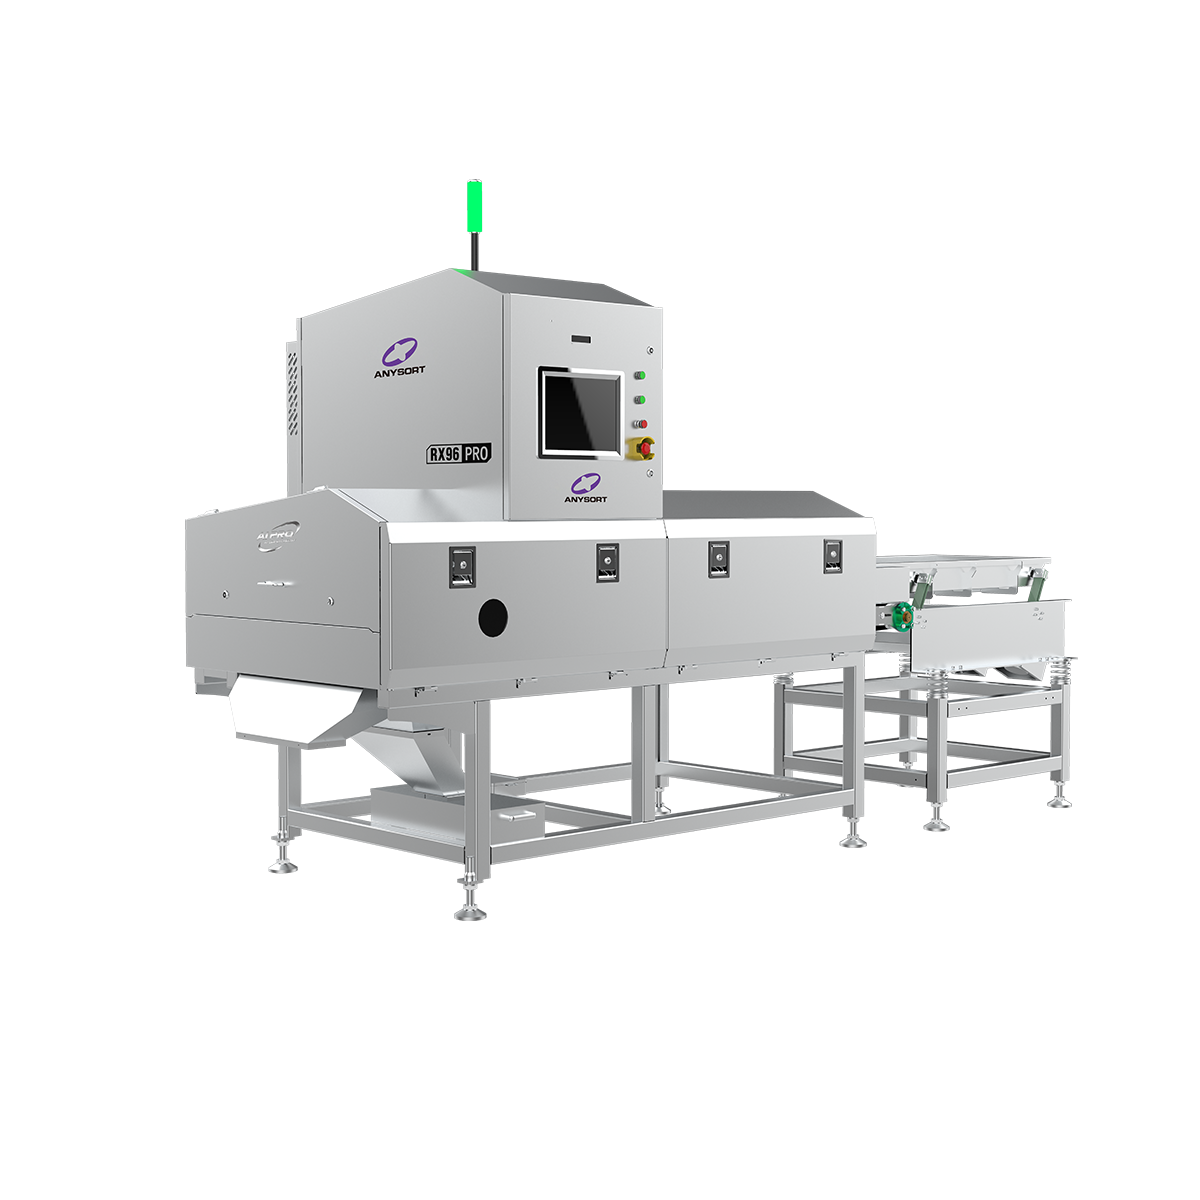
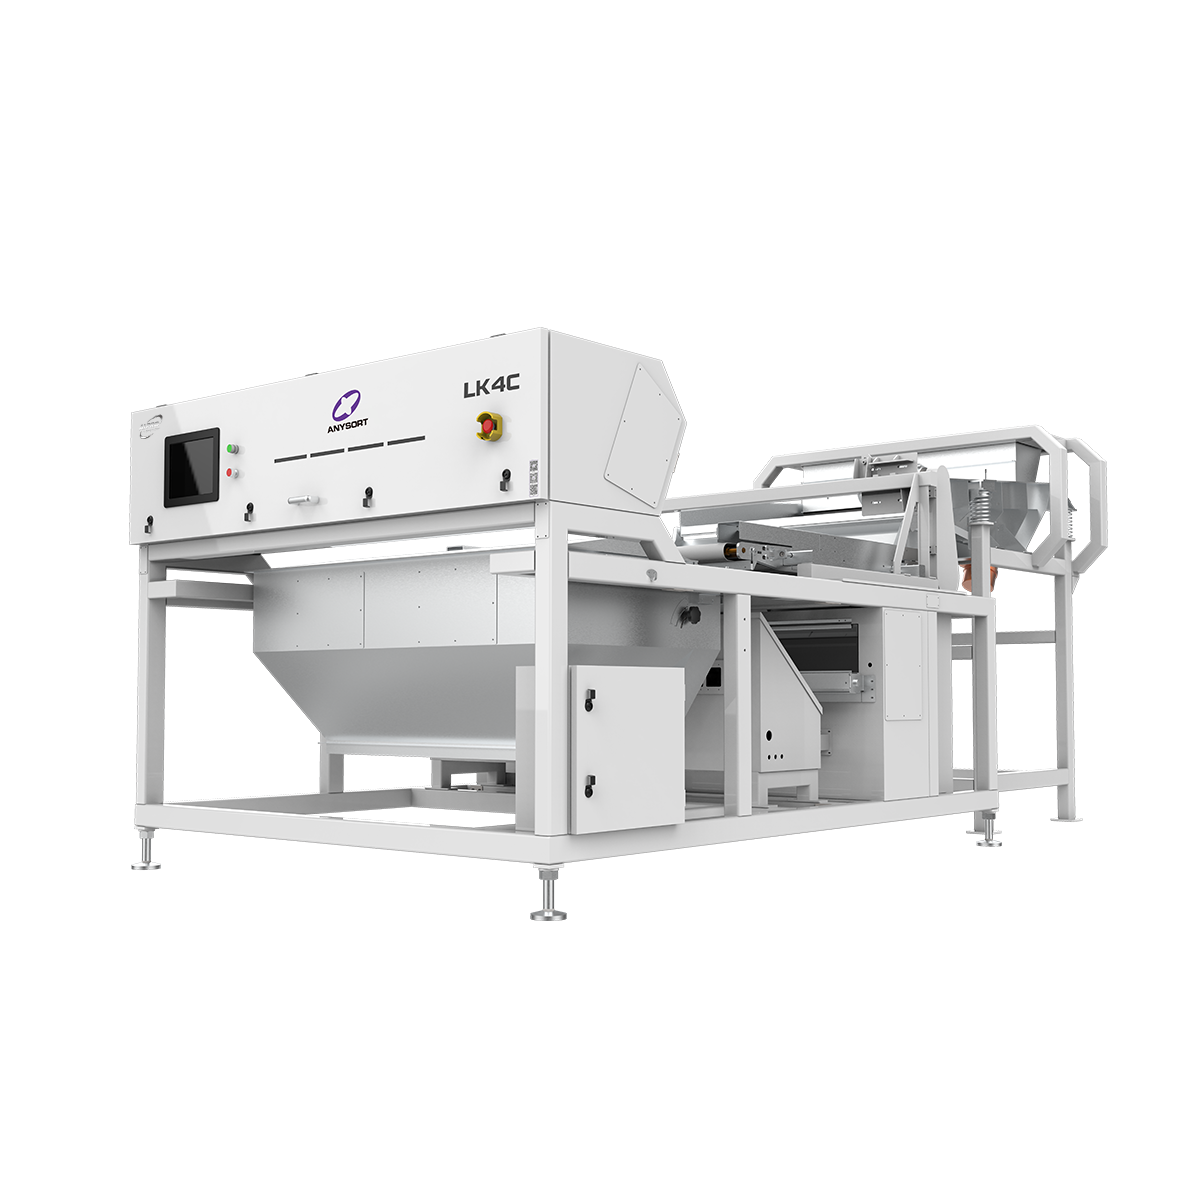
A colour sorter for grain represents a sophisticated optical sorting solution designed to enhance the quality and purity of grain processing operations. This advanced technology uses high-resolution cameras and artificial intelligence to detect and remove defective, discolored, or foreign particles from grain streams with exceptional precision. The colour sorter for grain operates by analyzing individual kernels as they pass through the sorting chamber, identifying variations in color, texture, and shape that indicate quality issues. Modern colour sorter for grain systems incorporate multi-spectral imaging technology that can distinguish between hundreds of color variations, ensuring only premium-grade grain reaches processing stages. These machines are equipped with powerful ejection mechanisms that remove unwanted particles in milliseconds, maintaining processing speed while guaranteeing superior output quality. The colour sorter for grain finds widespread application across wheat, rice, corn, barley, and specialty grain processing facilities. Its technological advancement includes real-time quality monitoring, adjustable sensitivity settings, and user-friendly interfaces that require minimal operator training. Processing capacity typically ranges from 3 to 25 tons per hour, depending on model specifications and grain type. The colour sorter for grain integrates seamlessly into existing production lines, connecting directly to upstream cleaning equipment and downstream packaging systems. Industries relying on this technology achieve significant improvements in product consistency, customer satisfaction, and market competitiveness. Whether for large-scale commercial operations or specialized grain production, the colour sorter for grain delivers reliable performance and consistent results that justify the investment through reduced waste and premium product quality.

New Product Releases

Investing in a colour sorter for grain provides transformative operational benefits that directly impact your bottom line. First, this equipment dramatically improves grain quality by removing damaged kernels, discolored grains, and foreign materials automatically. This means your final products meet stringent international standards consistently, enhancing your brand reputation and customer loyalty. The colour sorter for grain reduces manual sorting labor dramatically, freeing your workforce to focus on other critical production areas while decreasing operational costs substantially. Processing speed represents another major advantage—these systems handle large volumes without compromising quality, allowing you to increase throughput without adding production lines. Your business benefits from reduced waste and higher yield rates, directly translating to increased profitability per ton processed. The colour sorter for grain minimizes product loss during sorting, recovering valuable kernels that traditional methods discard, thereby maximizing resource efficiency. Customer satisfaction improves notably when you deliver consistently premium grain products, opening doors to high-value markets and premium pricing opportunities. Operational reliability is exceptional with minimal downtime, featuring robust construction and advanced diagnostics that prevent unexpected failures. The colour sorter for grain provides transparent sorting data through detailed reporting systems, allowing you to monitor product quality trends and make informed decisions. Maintenance requirements are straightforward, with replaceable components designed for easy access and quick service intervals. Environmental benefits emerge as waste reduction naturally follows precision sorting, supporting sustainability initiatives while lowering disposal costs. Whether processing bulk commodities or specialty grains, the colour sorter for grain adapts to diverse applications, providing flexible solutions that grow with your business needs and market demands.

Tips And Tricks

How Much Does a Color Sorter Machine Cost?

12

Aug

How Much Does a Color Sorter Machine Cost?

Understanding the investment required for a color sorter machine is essential for businesses in agriculture, food processing, and recycling sectors. The cost of a color sorter machine varies significantly based on capacity, technology sophistication,...
View More
How Can a Nuts Sorter Improve Your Production?

15

Aug

How Can a Nuts Sorter Improve Your Production?

A nuts sorter represents one of the most significant investments a food processing operation can make to enhance production quality and operational efficiency. The modern nuts sorter uses advanced imaging and sensor technology to identify and separat...
View More
How does optical sorting technology detect defective rice grains?

22

Aug

How does optical sorting technology detect defective rice grains?

Modern rice processing demands precision and consistency, which is why understanding the detection mechanisms behind advanced equipment has become essential for producers. A rice color sorter represents one of the most significant technological break...
View More
Top AI Color Sorter Manufacturers in China (2026)

30

Aug

Top AI Color Sorter Manufacturers in China (2026)

The global demand for precision sorting technology has surged dramatically, with color sorter machine manufacturers in China leading innovation across agricultural and industrial sectors. Chinese color sorter machine manufacturers have established th...
View More

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

colour sorter for grain

Advanced Optical Detection Technology

Advanced Optical Detection Technology

The colour sorter for grain utilizes cutting-edge multi-spectral imaging and artificial intelligence algorithms that analyze each kernel individually with remarkable accuracy. This technology captures detailed visual information across multiple color spectrums, enabling the detection of the most subtle defects and impurities invisible to the human eye. The colour sorter for grain's intelligent system learns and adapts to different grain varieties and seasonal variations, continuously optimizing detection accuracy. Real-time processing capabilities ensure that sorting decisions occur instantaneously as kernels move through the chamber at speeds exceeding 300 kilometers per hour. The system's high-resolution cameras and sophisticated software allow operators to set precise quality parameters, adjusting sensitivity levels to match specific market requirements or customer specifications. This technological advancement means you achieve exceptional purity levels while maintaining processing efficiency. The colour sorter for grain's detection capability extends beyond simple color variations to identify cracks, mold damage, insect damage, and density variations that indicate compromised quality. Operators receive comprehensive feedback through intuitive displays showing real-time sorting statistics, defect counts, and quality trends.
Maximum Processing Efficiency and Throughput

Maximum Processing Efficiency and Throughput

The colour sorter for grain delivers exceptional productivity that transforms your grain processing operations into high-performance facilities. These systems process grain at impressive speeds ranging from 3 to 25 tons per hour, depending on selected models and grain types, without sacrificing sorting accuracy or quality results. The continuous operation capability of the colour sorter for grain ensures that your production schedules remain uninterrupted, maximizing facility utilization and return on investment. Integration with existing production infrastructure occurs seamlessly, as the colour sorter for grain connects directly to preceding cleaning stages and downstream packaging equipment through standardized interfaces. This compatibility eliminates costly production line modifications while streamlining your entire workflow. The colour sorter for grain's energy-efficient design reduces operational costs compared to older sorting technologies, providing long-term savings despite initial capital investment. Automatic operation requires minimal human intervention, reducing labor requirements and associated wage costs while improving worker safety by eliminating manual sorting tasks.
Consistent Quality and Superior Purity Results

Consistent Quality and Superior Purity Results

Implementing a colour sorter for grain establishes reliable quality consistency that builds customer confidence and strengthens market position. The colour sorter for grain removes defective kernels, discolored grains, and foreign materials at rates exceeding 99.9 percent, ensuring your products meet the most demanding international quality standards. This precision sorting capability translates directly to premium product grades that command higher market prices and attract quality-conscious buyers. The colour sorter for grain enables strict compliance with food safety regulations and private certification requirements, protecting your business from liability while demonstrating commitment to quality. Reduced waste from the colour sorter for grain means higher yield rates per ton of raw grain processed, significantly improving profitability metrics. Product consistency becomes your competitive advantage, as customers receive identical quality regardless of processing batch or seasonal grain variations. The colour sorter for grain documentation and traceability features provide transparent quality records supporting audit requirements and customer verification needs.

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

Copyright © 2026 Anhui Jiexun Optoelectronic Technology Co., Ltd. All rights reserved.  -  Privacy policy