Cashew Color Sorter - Precision Sorting Technology

All Categories

cashew color sorter

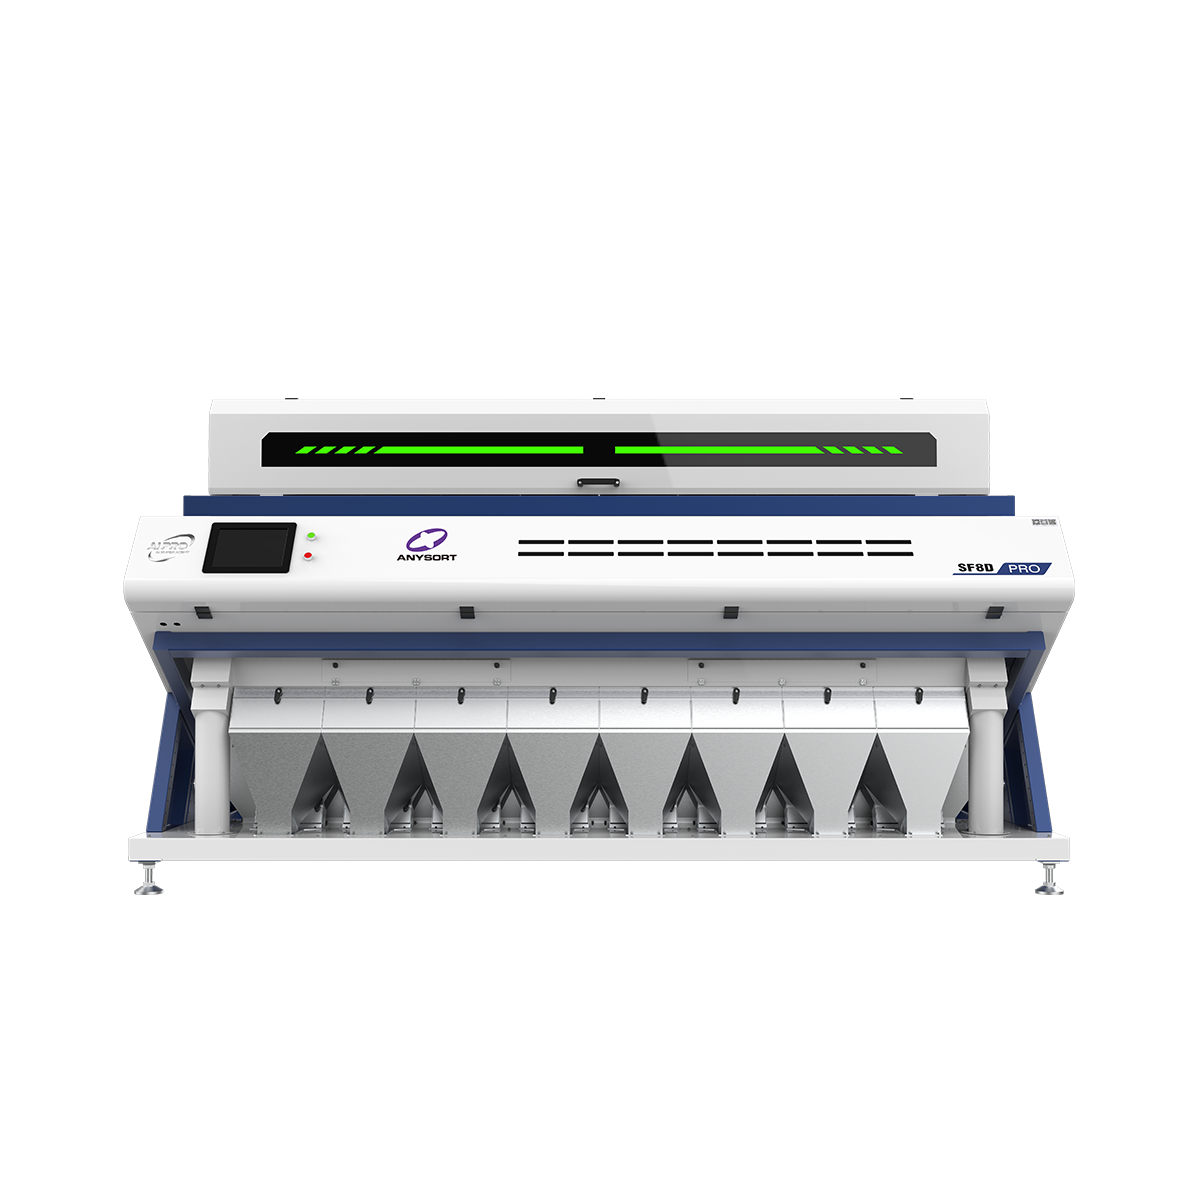
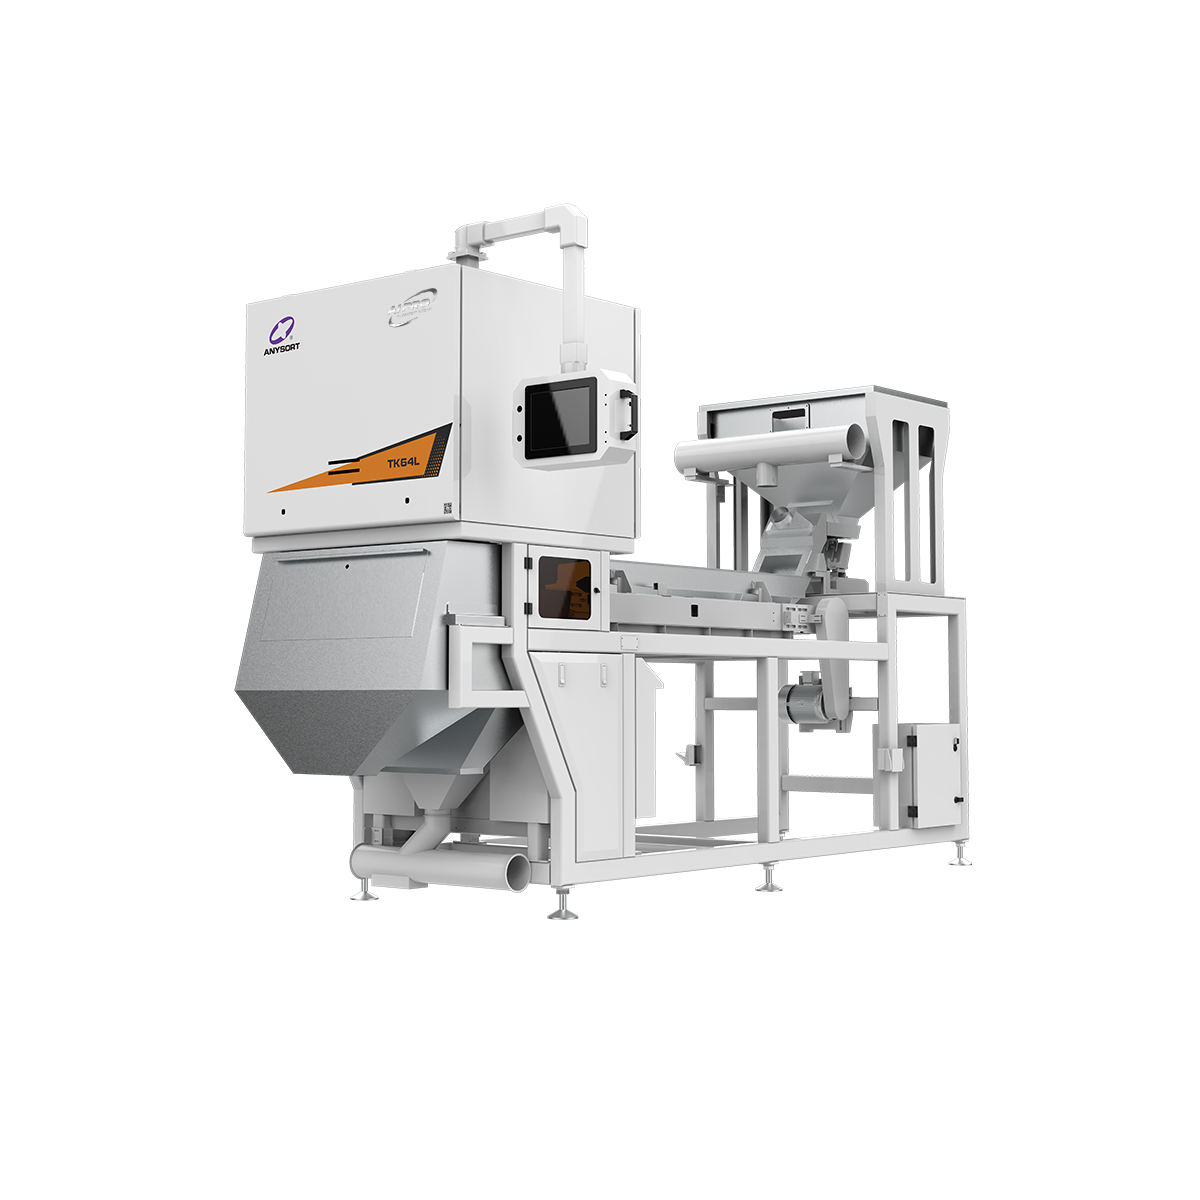
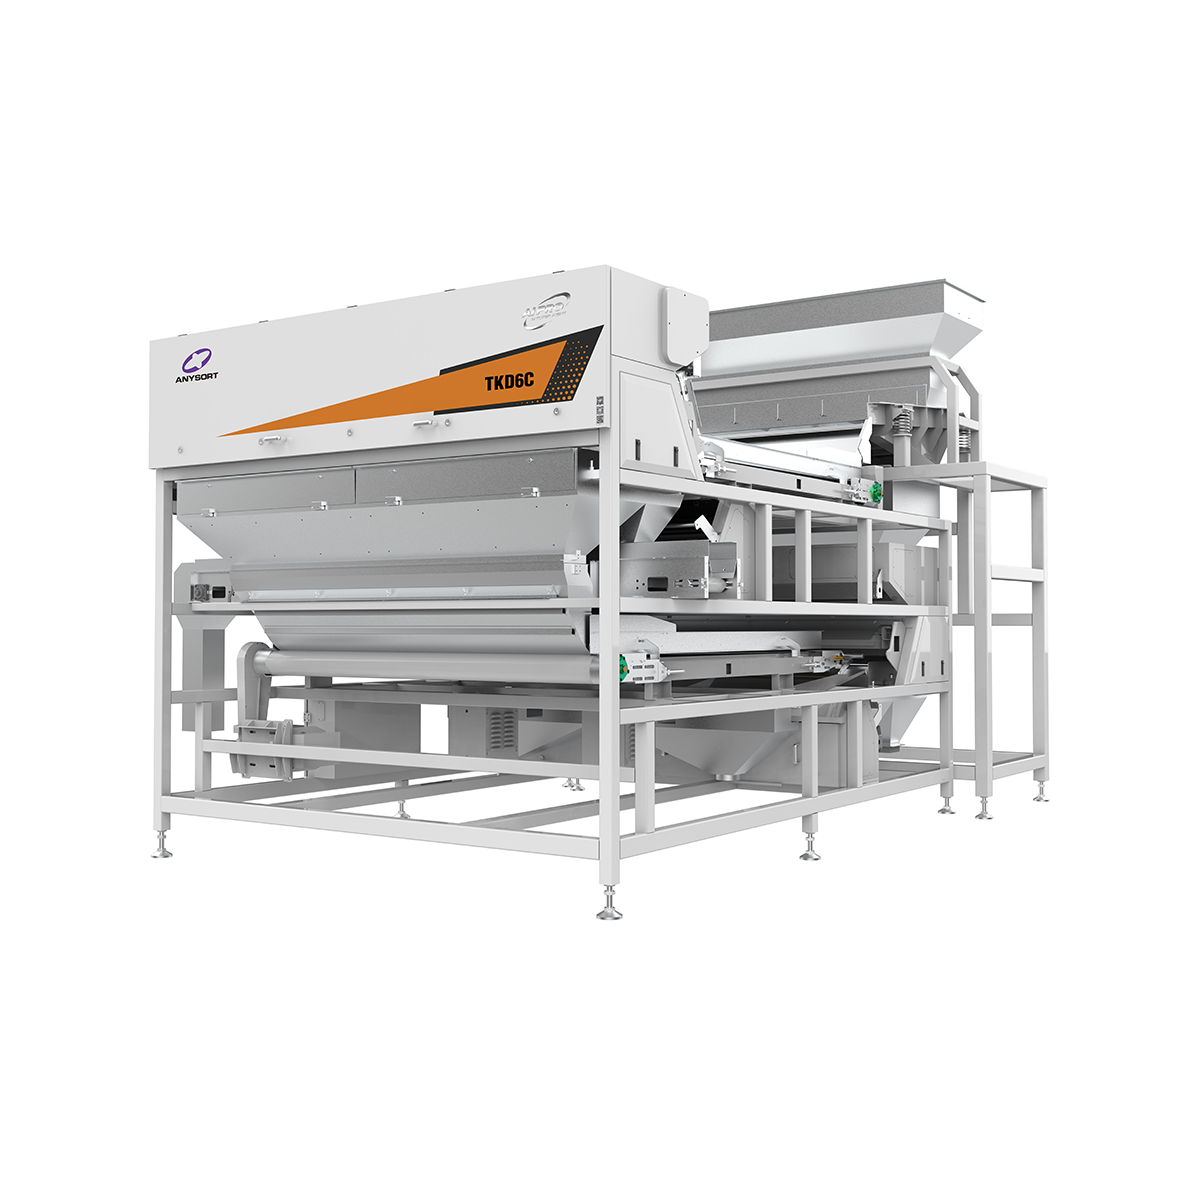
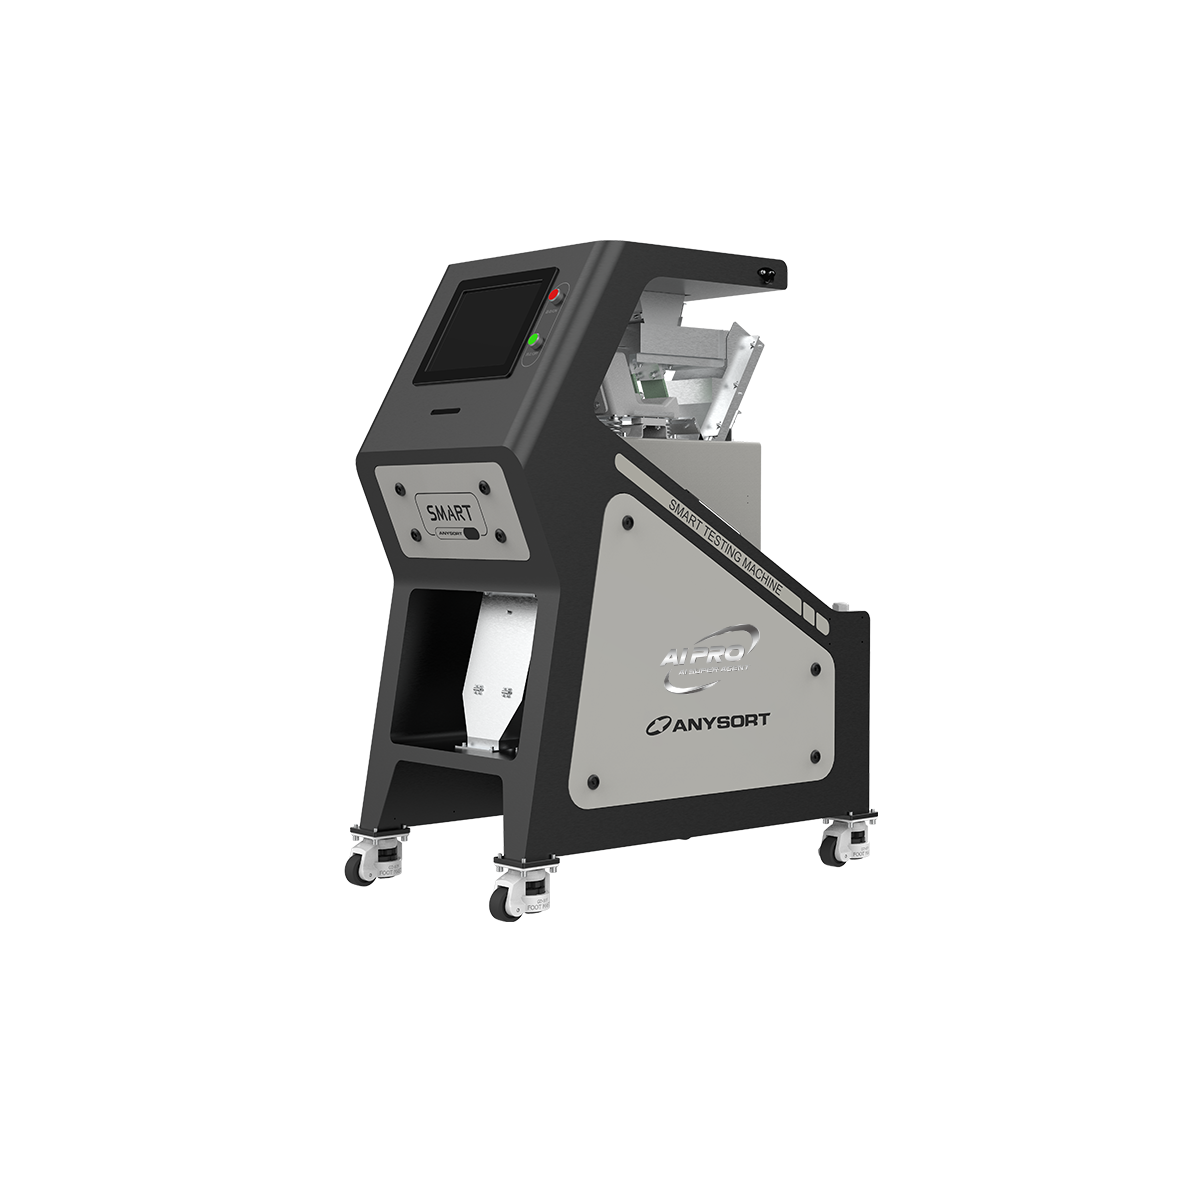
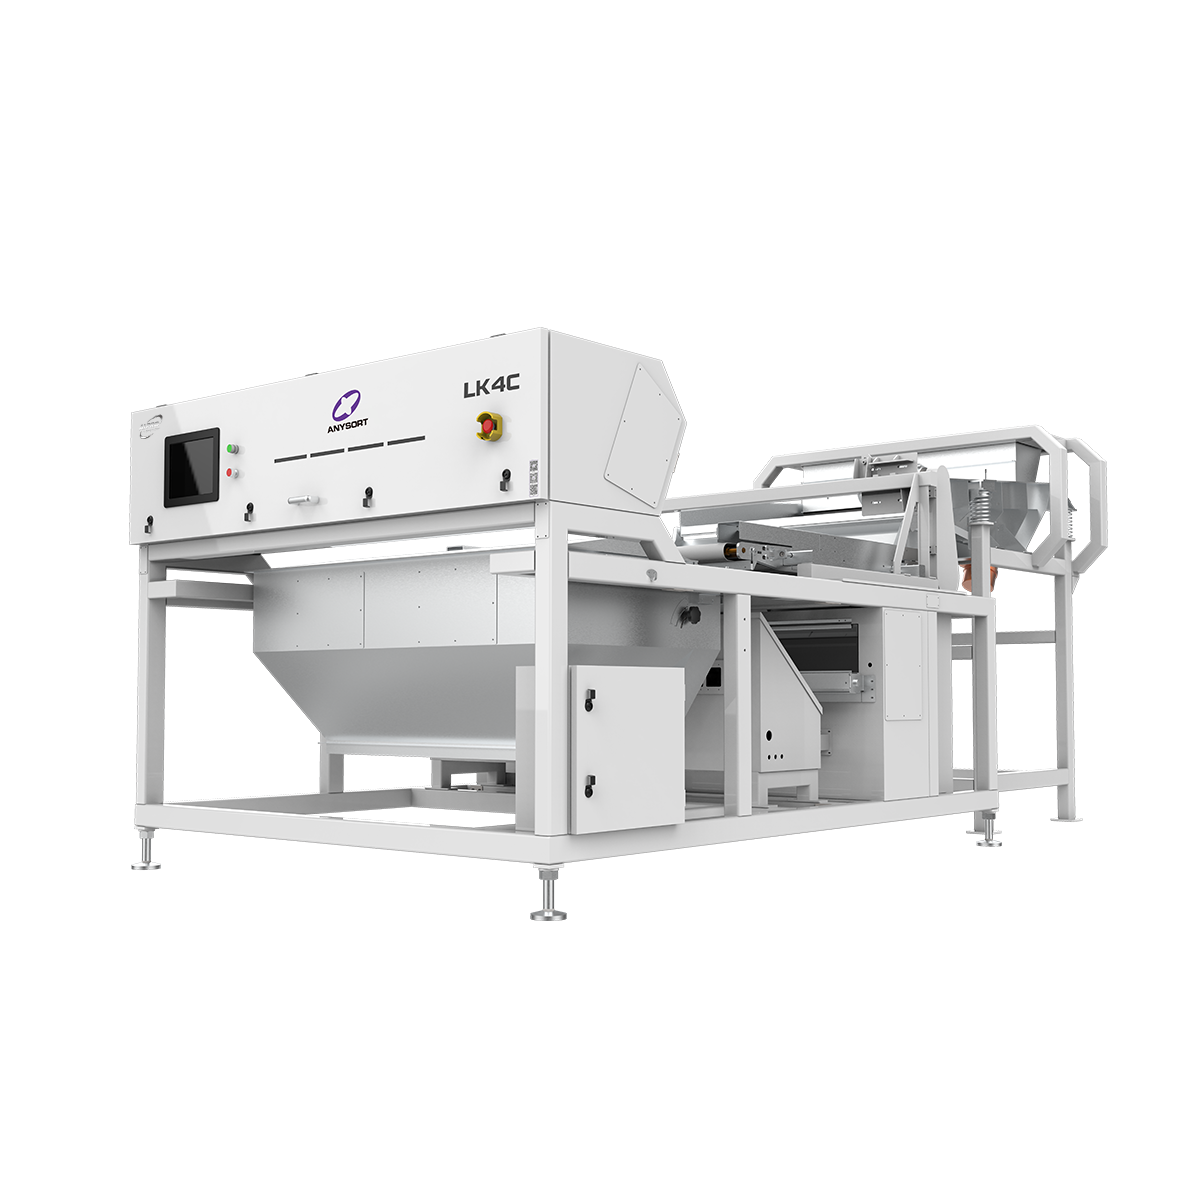
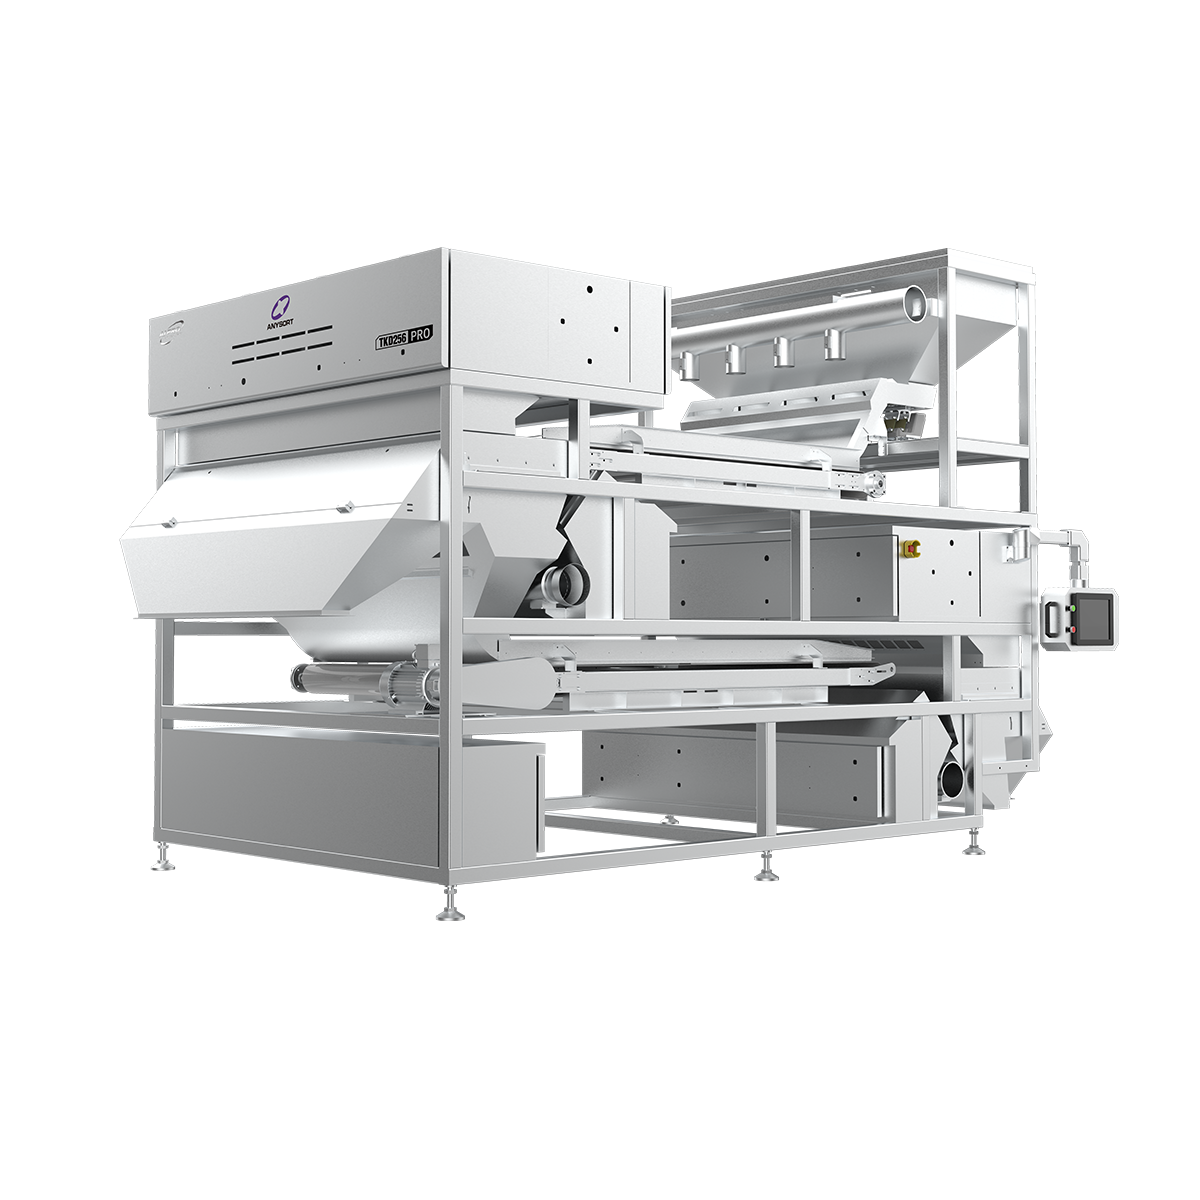
A cashew color sorter is an advanced optical sorting machine designed to automatically classify and separate cashews based on their color, size, and quality characteristics. This specialized equipment uses high-resolution camera systems and artificial intelligence technology to inspect each cashew individually as it moves through the sorting mechanism. The cashew color sorter identifies defects, discoloration, and quality variations that human inspectors might miss, ensuring only premium-grade cashews proceed to packaging. Modern cashew color sorter systems feature multiple channels that direct sorted nuts into different collection bins based on predetermined color standards and quality parameters. The technology incorporates LED lighting and sophisticated image analysis algorithms to detect even subtle color differences across large volumes of cashews. These machines process hundreds of kilograms per hour, significantly increasing efficiency compared to manual sorting methods. A cashew color sorter eliminates the inconsistencies associated with manual labor while maintaining consistent quality standards that satisfy international buyers. The equipment integrates seamlessly into existing processing lines, connecting with other machinery through automated conveyors and control systems. Industrial-grade construction ensures durability and reliable performance in demanding production environments. The cashew color sorter reduces waste, minimizes labor costs, and improves overall product marketability by delivering uniform, visually appealing cashews that meet strict commercial specifications.

New Product Recommendations

The cashew color sorter delivers substantial operational benefits that transform cashew processing facilities. First, this equipment dramatically increases sorting accuracy by detecting color variations and quality defects that trained human workers often overlook or process inconsistently. The cashew color sorter operates continuously without fatigue, maintaining uniform sorting standards throughout extended production shifts. By automating the quality control process, facilities reduce their dependence on large manual labor teams, significantly lowering personnel costs while improving workplace safety. Processing speed represents another major advantage, as a modern cashew color sorter handles significantly higher volumes than manual sorting, boosting facility throughput and profitability. The machine minimizes product waste by precisely identifying only genuinely defective cashews, allowing more nuts to reach the premium grade category. For exporters, a cashew color sorter ensures consistent product batches that meet international quality standards, enhancing customer satisfaction and brand reputation. The equipment reduces sorting errors that lead to customer complaints and returned shipments. Implementation of a cashew color sorter improves production efficiency while reducing operational costs per unit processed. Facility managers gain real-time data about product quality and sorting performance through the machine's integrated monitoring systems. The cashew color sorter provides competitive advantages in global markets where quality consistency determines buyer preferences. Investment in this technology yields rapid returns through increased productivity, reduced labor expenses, and improved product quality that commands premium pricing in international marketplaces.

Tips And Tricks

How to Choose the Right Tea Color Sorter for Your Needs?

01

Aug

How to Choose the Right Tea Color Sorter for Your Needs?

Selecting the right tea color sorter is one of the most critical decisions tea processors face when modernizing their operations. A tea color sorter directly impacts product quality, operational efficiency, and market competitiveness. The wrong choic...
View More
How Much Does a Color Sorter Machine Cost?

12

Aug

How Much Does a Color Sorter Machine Cost?

Understanding the investment required for a color sorter machine is essential for businesses in agriculture, food processing, and recycling sectors. The cost of a color sorter machine varies significantly based on capacity, technology sophistication,...
View More
How Can a Nuts Sorter Improve Your Production?

15

Aug

How Can a Nuts Sorter Improve Your Production?

A nuts sorter represents one of the most significant investments a food processing operation can make to enhance production quality and operational efficiency. The modern nuts sorter uses advanced imaging and sensor technology to identify and separat...
View More
Which factors should you consider when selecting a rice color sorter?

29

Aug

Which factors should you consider when selecting a rice color sorter?

Selecting the right rice color sorter is a critical decision that directly impacts your grain processing efficiency, product quality, and long-term profitability. A rice color sorter removes discolored, damaged, and foreign particles from rice batche...
View More

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

cashew color sorter

Precision Optical Technology for Flawless Sorting

Precision Optical Technology for Flawless Sorting

The cashew color sorter employs advanced optical imaging combined with artificial intelligence to achieve unprecedented sorting precision. High-resolution cameras capture detailed images of each cashew from multiple angles, analyzing color gradations, surface texture, and potential defects in milliseconds. The machine's AI algorithms compare each nut against established quality parameters, making consistent decisions without human bias or variation. This precision eliminates the subjectivity inherent in manual sorting, where different workers apply varying standards. The cashew color sorter identifies defects invisible to the naked eye, including internal discoloration and quality issues that develop during processing. By achieving such high accuracy, the machine reduces premium-grade cashews lost to overly strict manual sorting while rejecting genuinely defective nuts. Facilities using a cashew color sorter report significant improvements in product consistency and customer satisfaction. The technology ensures that exported cashew batches meet the stringent international quality requirements demanded by premium buyers worldwide.
High-Capacity Processing for Maximum Productivity

High-Capacity Processing for Maximum Productivity

A cashew color sorter processes hundreds of kilograms of cashews daily, vastly outpacing manual sorting capabilities and dramatically increasing facility throughput. The machine maintains consistent processing speed throughout entire production runs without requiring breaks or rest periods. This continuous operation multiplies annual processing capacity, allowing facilities to handle larger contracts and generate substantially higher revenues. The cashew color sorter efficiently handles peak season demands when cashew volumes surge, preventing processing bottlenecks. Multiple sorting channels enable simultaneous categorization into various quality grades, further accelerating throughput. Production managers can adjust processing parameters to optimize speed versus accuracy based on specific operational needs. The high-capacity cashew color sorter represents an economical solution for facilities seeking to expand production without proportionally increasing facility size or overhead expenses. By processing more product in less time, the equipment delivers superior return on investment compared to traditional sorting methods, making it an attractive option for ambitious cashew processors.
Cost Reduction Through Automation and Efficiency

Cost Reduction Through Automation and Efficiency

Implementing a cashew color sorter generates immediate cost savings by eliminating expensive manual labor requirements while simultaneously increasing output volumes. Facilities reduce operational expenses associated with recruiting, training, and supervising large sorting teams. The cashew color sorter operates with minimal ongoing maintenance, featuring robust industrial construction designed for demanding processing environments. Energy consumption remains reasonable relative to the processing capacity delivered, providing favorable operational economics. Reduced product waste directly improves profit margins, as fewer cashews are unnecessarily rejected during automated sorting. The cashew color sorter decreases customer complaints and returns, which impose significant costs through reverse logistics and reputation damage. By delivering consistent, high-quality products, the machine enables facilities to command premium pricing and expand customer bases. Investment costs for a cashew color sorter generate rapid payback periods through cumulative savings from reduced labor, waste reduction, and improved product value. Facility managers achieve greater profitability and competitiveness in challenging global markets.

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

Copyright © 2026 Anhui Jiexun Optoelectronic Technology Co., Ltd. All rights reserved.  -  Privacy policy