Corn Sorting | Precision Grain Classification

All Categories

corn sorting

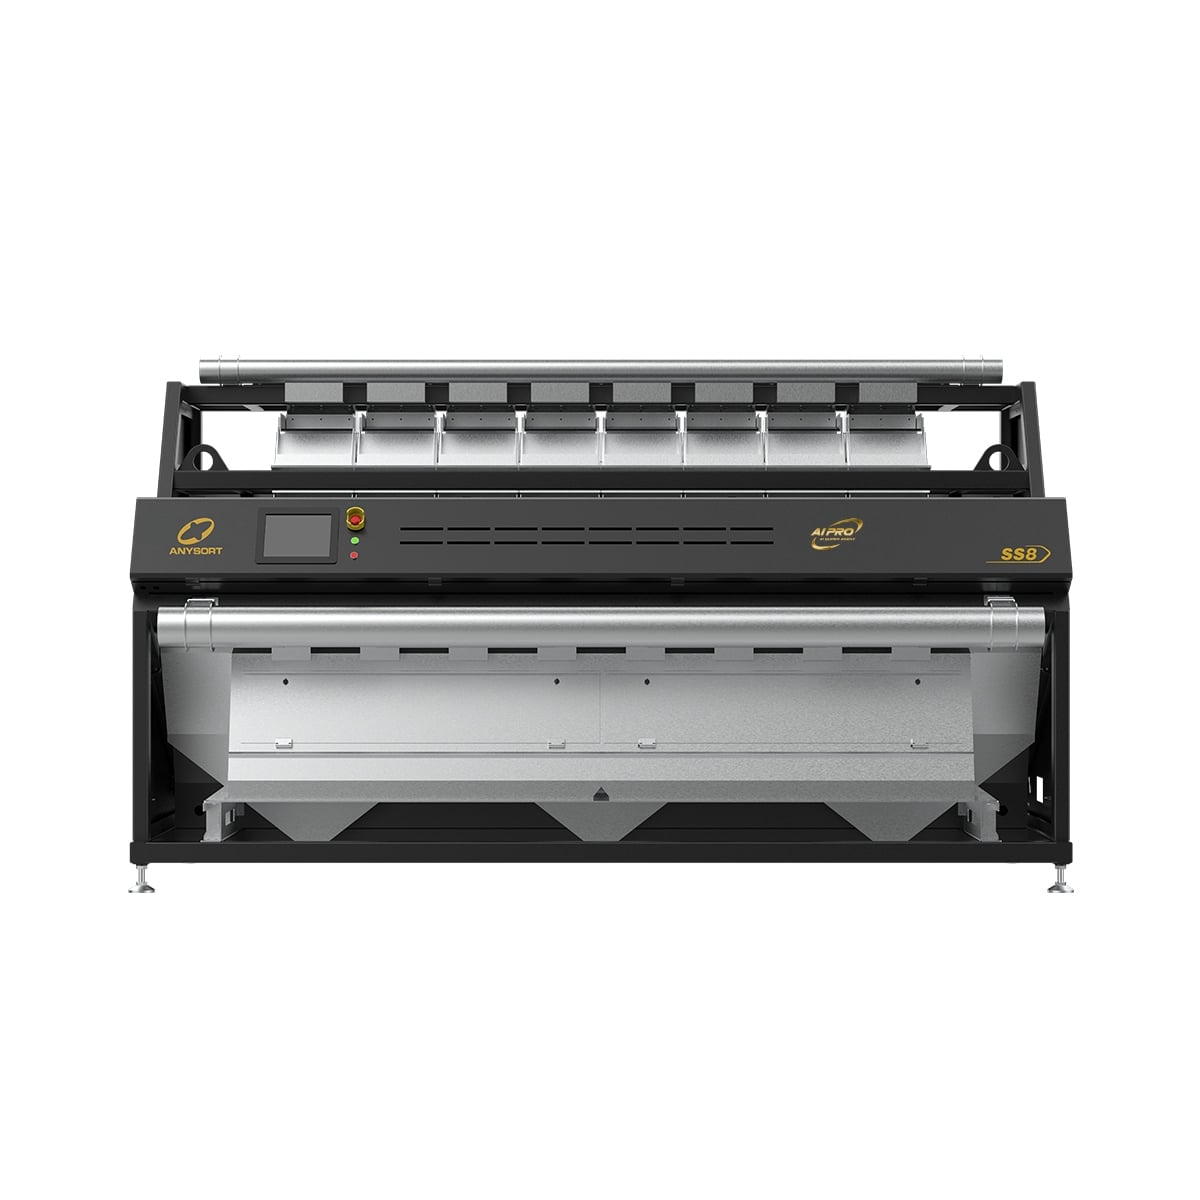
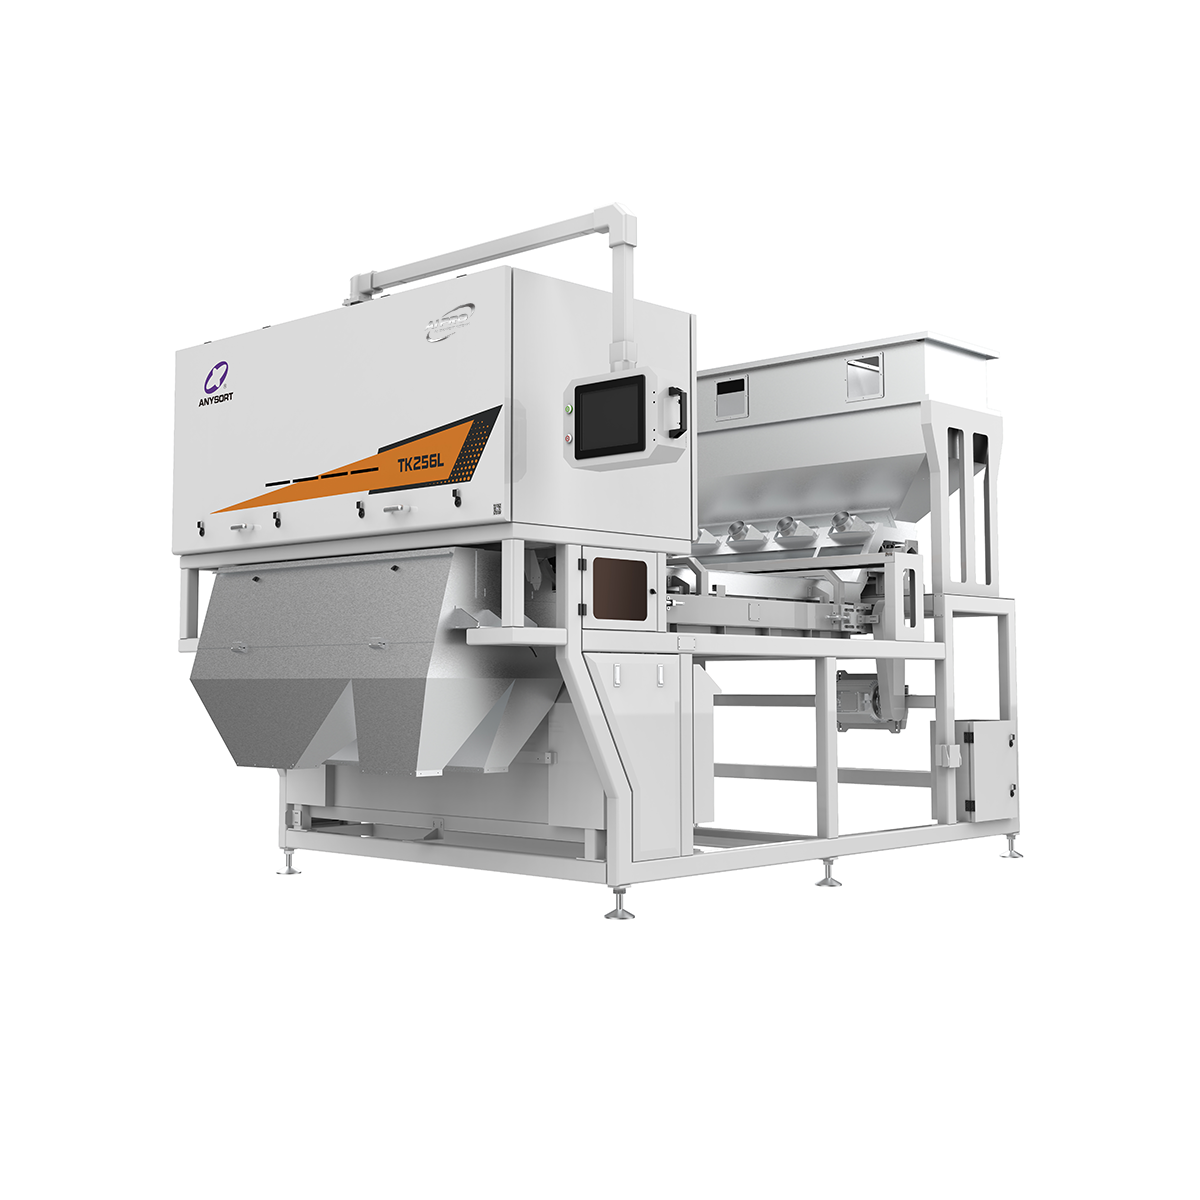
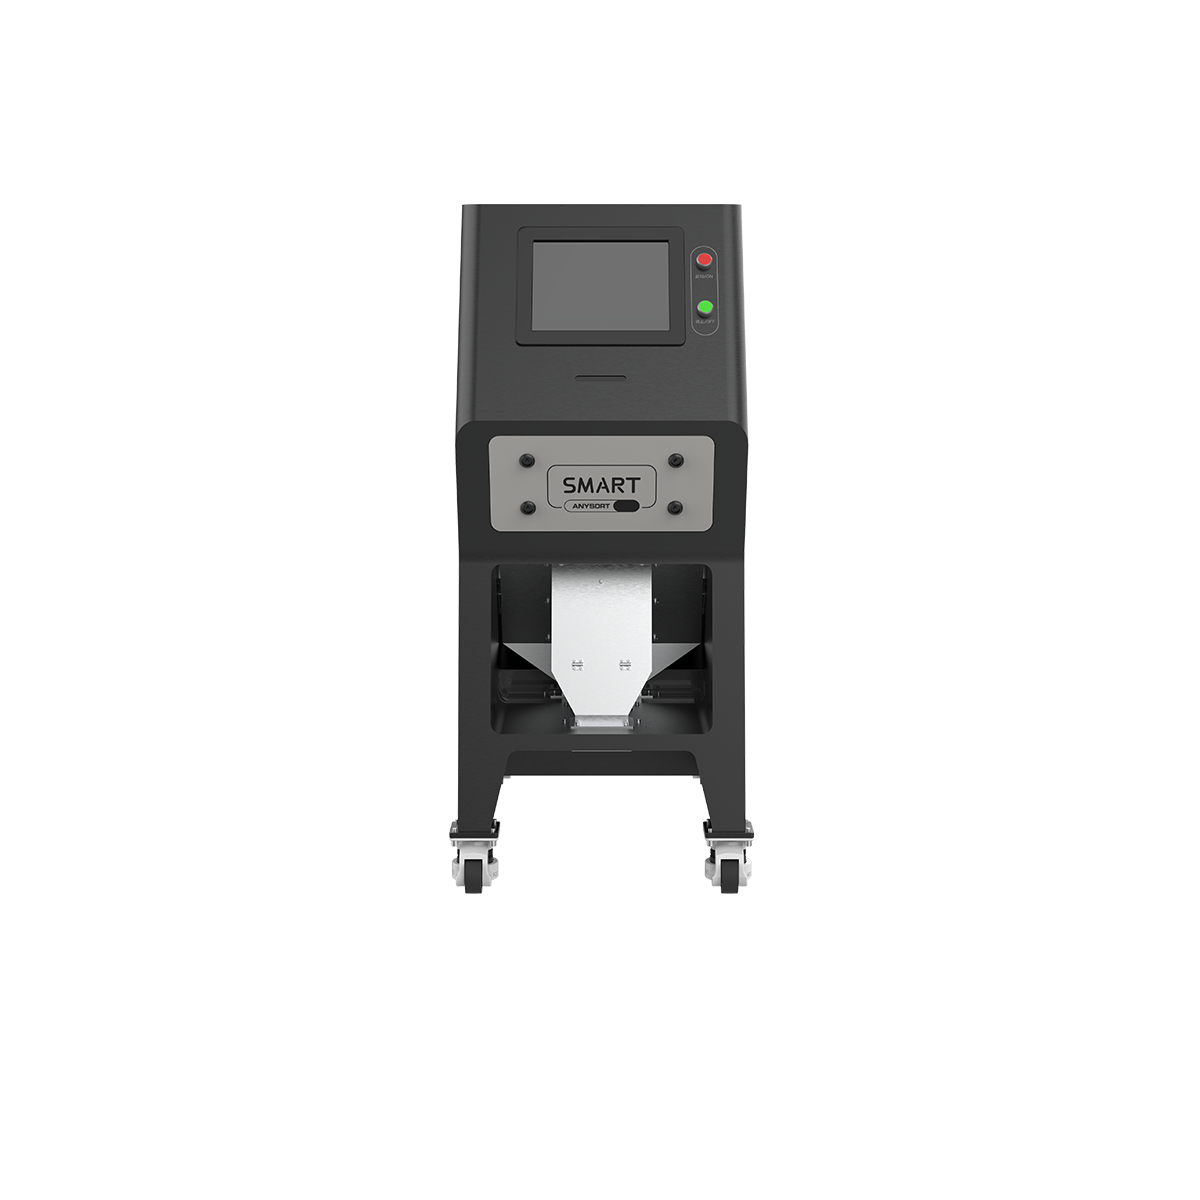
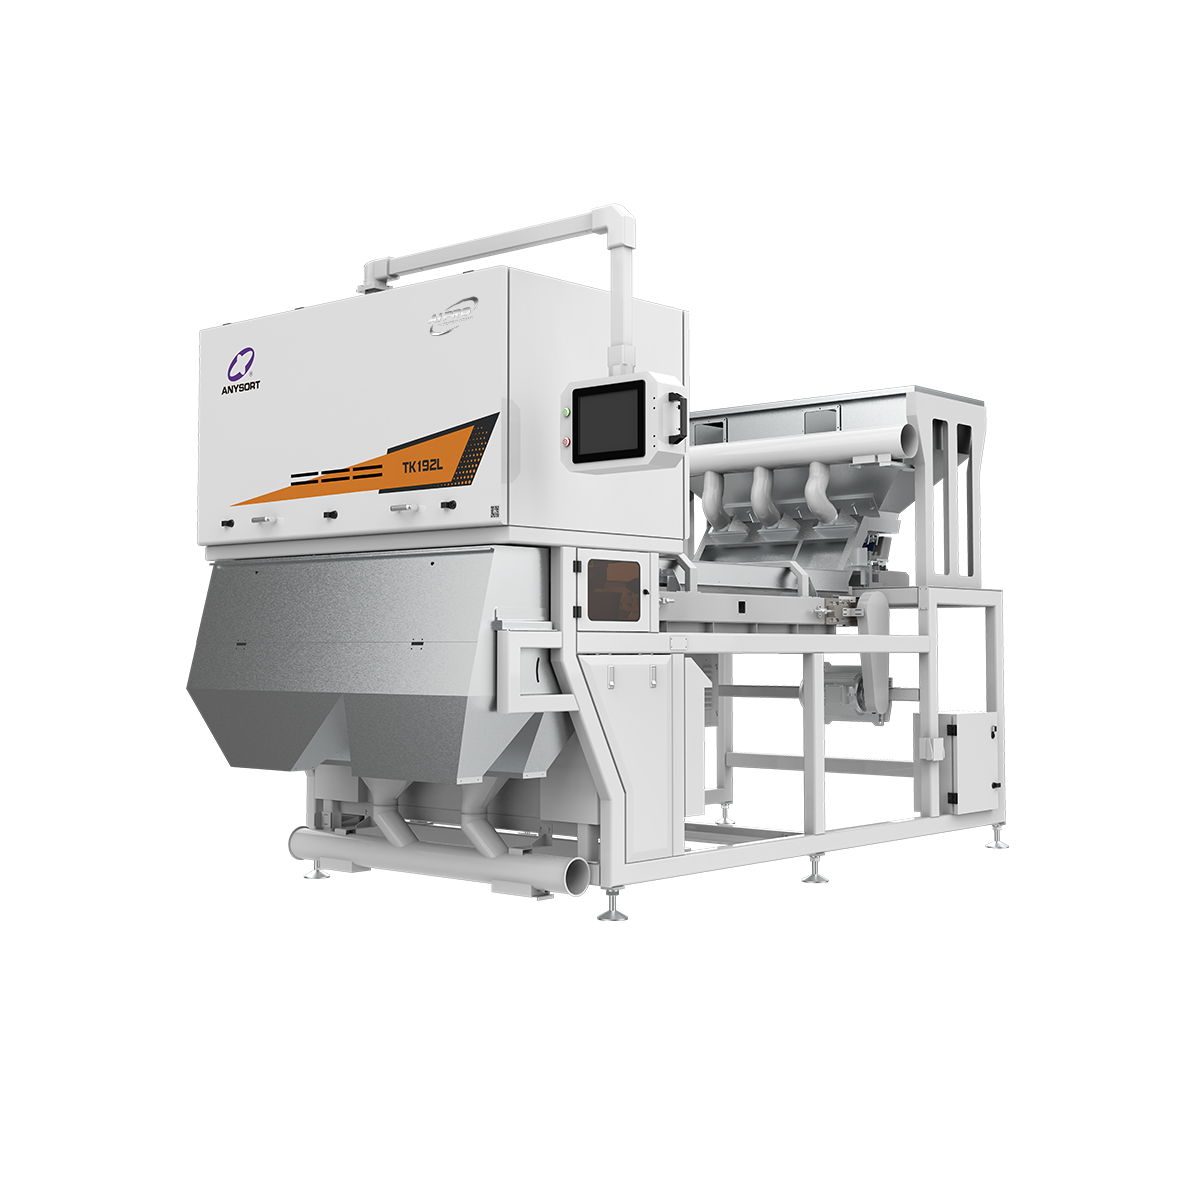
Corn sorting technology represents a sophisticated automated solution designed to separate and grade corn kernels based on quality, size, color, and condition. Modern corn sorting systems utilize advanced optical scanning and artificial intelligence to identify defects, foreign materials, and inconsistencies with remarkable precision. The process begins when corn passes through a hopper into the sorting chamber, where high-resolution cameras capture detailed images of each kernel. These images are analyzed in milliseconds to categorize corn according to predetermined quality standards. Corn sorting machines can process thousands of kernels per minute, dramatically improving efficiency compared to manual selection methods. The technology employs sophisticated algorithms that learn and adapt to various corn varieties and growing conditions, ensuring consistent results regardless of seasonal variations. Advanced corn sorting equipment features multiple ejection systems that automatically remove substandard kernels with pneumatic precision. The integration of machine learning allows corn sorting systems to continuously improve accuracy and reduce waste. Modern facilities implement corn sorting as a critical step in post-harvest processing, ensuring only premium-grade corn reaches market. Whether processing corn for food production, animal feed, or industrial applications, corn sorting technology delivers unmatched reliability and performance. The systems are designed for easy integration into existing production lines and require minimal operator training. Investment in professional corn sorting equipment significantly enhances product quality and market competitiveness for agricultural businesses.

New Product Releases

Implementing corn sorting technology delivers substantial practical benefits that directly improve your bottom line and operational efficiency. First, corn sorting dramatically reduces processing time by automating what would otherwise require extensive manual labor. Your team can focus on other critical tasks while machines handle the repetitive, time-consuming work of evaluating thousands of kernels. Corn sorting ensures consistent quality output, which means your customers receive reliable products meeting exact specifications every single time. This consistency builds brand reputation and customer loyalty, ultimately increasing repeat business and market share. The technology eliminates human error and fatigue that naturally occur with manual sorting, resulting in far fewer mistakes and better quality control. Corn sorting systems pay for themselves through reduced waste and improved yield, as damaged or inferior kernels are identified and removed before reaching expensive processing stages. Your operation gains a significant competitive advantage by delivering higher quality products than competitors still relying on outdated manual methods. Corn sorting equipment reduces labor costs substantially, allowing you to maintain profitability even when production volumes fluctuate. The systems work continuously without breaks or quality degradation, maximizing throughput and facility utilization. Safety improves across your operation since workers avoid repetitive strain injuries associated with manual sorting. Environmental benefits emerge as corn sorting minimizes waste sent to landfills by maximizing usable product recovery. The technology adapts to different corn varieties and market requirements, providing flexibility for diversified agricultural operations. Long-term investment in corn sorting technology positions your business for sustainable growth and enhanced market position in an increasingly competitive industry.

Tips And Tricks

How to Choose the Right Tea Color Sorter for Your Needs?

01

Aug

How to Choose the Right Tea Color Sorter for Your Needs?

Selecting the right tea color sorter is one of the most critical decisions tea processors face when modernizing their operations. A tea color sorter directly impacts product quality, operational efficiency, and market competitiveness. The wrong choic...
View More
How Much Does a Color Sorter Machine Cost?

12

Aug

How Much Does a Color Sorter Machine Cost?

Understanding the investment required for a color sorter machine is essential for businesses in agriculture, food processing, and recycling sectors. The cost of a color sorter machine varies significantly based on capacity, technology sophistication,...
View More
How Can a Nuts Sorter Improve Your Production?

15

Aug

How Can a Nuts Sorter Improve Your Production?

A nuts sorter represents one of the most significant investments a food processing operation can make to enhance production quality and operational efficiency. The modern nuts sorter uses advanced imaging and sensor technology to identify and separat...
View More
How does optical sorting technology detect defective rice grains?

22

Aug

How does optical sorting technology detect defective rice grains?

Modern rice processing demands precision and consistency, which is why understanding the detection mechanisms behind advanced equipment has become essential for producers. A rice color sorter represents one of the most significant technological break...
View More

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

corn sorting

Precision Quality Detection for Superior Results

Precision Quality Detection for Superior Results

Modern corn sorting employs cutting-edge optical imaging technology that captures detailed visual data of every single kernel processing through the system. The high-resolution cameras work in conjunction with artificial intelligence algorithms to detect even the most subtle defects including cracks, discoloration, mold, and foreign particles that human eyes might miss. This precision corn sorting capability ensures that only kernels meeting your exact quality specifications advance to the next processing stage. The detection accuracy exceeds 99 percent, dramatically reducing the risk of substandard products reaching your customers. Advanced corn sorting systems can identify quality issues invisible to the naked eye, such as internal damage and moisture content variations. The technology learns from patterns within your specific operation, continuously refining detection parameters to match your unique requirements. By implementing comprehensive corn sorting, you guarantee consistent product quality that builds customer trust and supports premium pricing strategies. This precision directly translates to reduced returns, fewer customer complaints, and enhanced brand reputation in competitive markets.
High-Speed Processing Capacity and Efficiency

High-Speed Processing Capacity and Efficiency

Corn sorting systems process up to ten thousand kernels per minute, delivering throughput that far exceeds manual sorting capabilities. This exceptional speed allows your facility to process significantly larger volumes without proportionally increasing labor costs or facility expansion. The automatic corn sorting eliminates bottlenecks that traditionally slow agricultural processing operations. Your production line maintains consistent velocity regardless of kernel size variations or environmental conditions. Sophisticated pneumatic ejection systems instantaneously remove substandard kernels while maintaining perfect separation from acceptable product. The efficiency of modern corn sorting technology means you can serve larger customer bases and pursue new market opportunities previously constrained by processing capacity limitations. Reduced processing time translates directly to faster inventory turnover and improved cash flow for your business. The systems operate continuously without scheduled breaks, holidays, or vacation periods, maximizing your annual production capacity. Implementation of professional corn sorting enables your facility to achieve economies of scale that significantly improve profit margins. The high-speed corn sorting capability particularly benefits operations processing multiple corn varieties simultaneously or serving diverse market segments.
Smart Integration and Adaptable Technology

Smart Integration and Adaptable Technology

Contemporary corn sorting systems seamlessly integrate into existing production lines with minimal disruption to current operations. The technology features modular design that allows customization based on your specific facility layout and production requirements. Advanced corn sorting equipment connects to your facility management systems via digital platforms for real-time monitoring and data collection. Operators can adjust sorting parameters instantly through intuitive control interfaces without requiring specialized technical expertise. The adaptive corn sorting algorithms learn from your operation's unique characteristics, continuously optimizing performance and accuracy. Integration capabilities include compatibility with various hopper designs, conveyor systems, and downstream processing equipment. Your facility gains detailed analytics about product quality trends, waste reduction opportunities, and production efficiency metrics. Modern corn sorting systems provide predictive maintenance alerts, preventing unexpected downtime and service disruptions. The technology supports multiple output channels allowing simultaneous sorting into different quality grades or product categories. Flexible corn sorting solutions accommodate seasonal variations in crop characteristics and market demand fluctuations without requiring equipment modifications.

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

Copyright © 2026 Anhui Jiexun Optoelectronic Technology Co., Ltd. All rights reserved.  -  Privacy policy