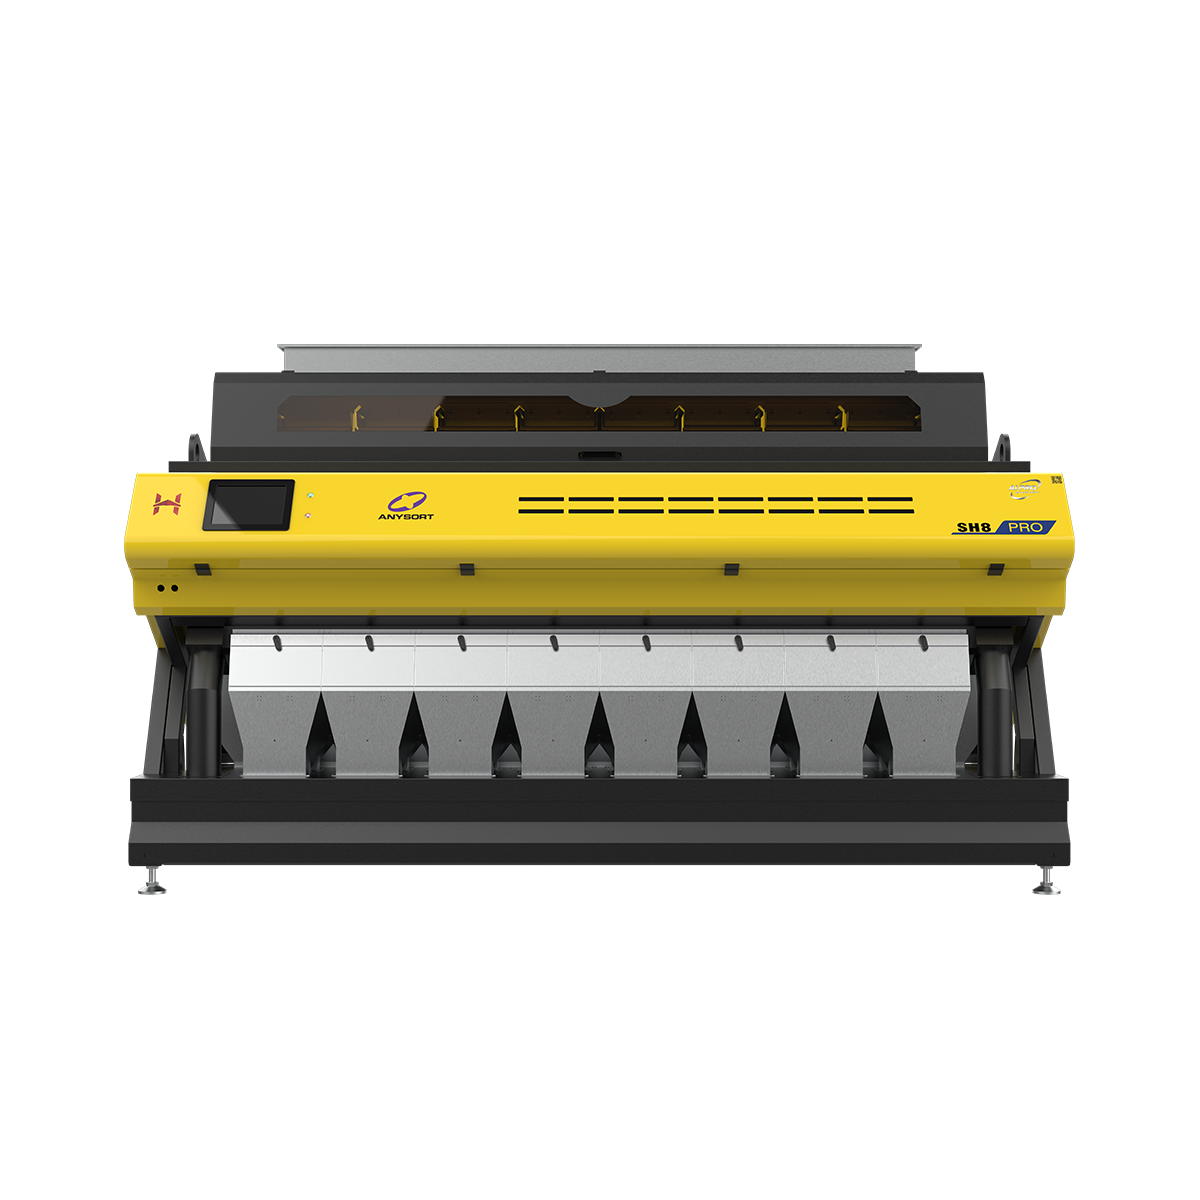
color sorter corn
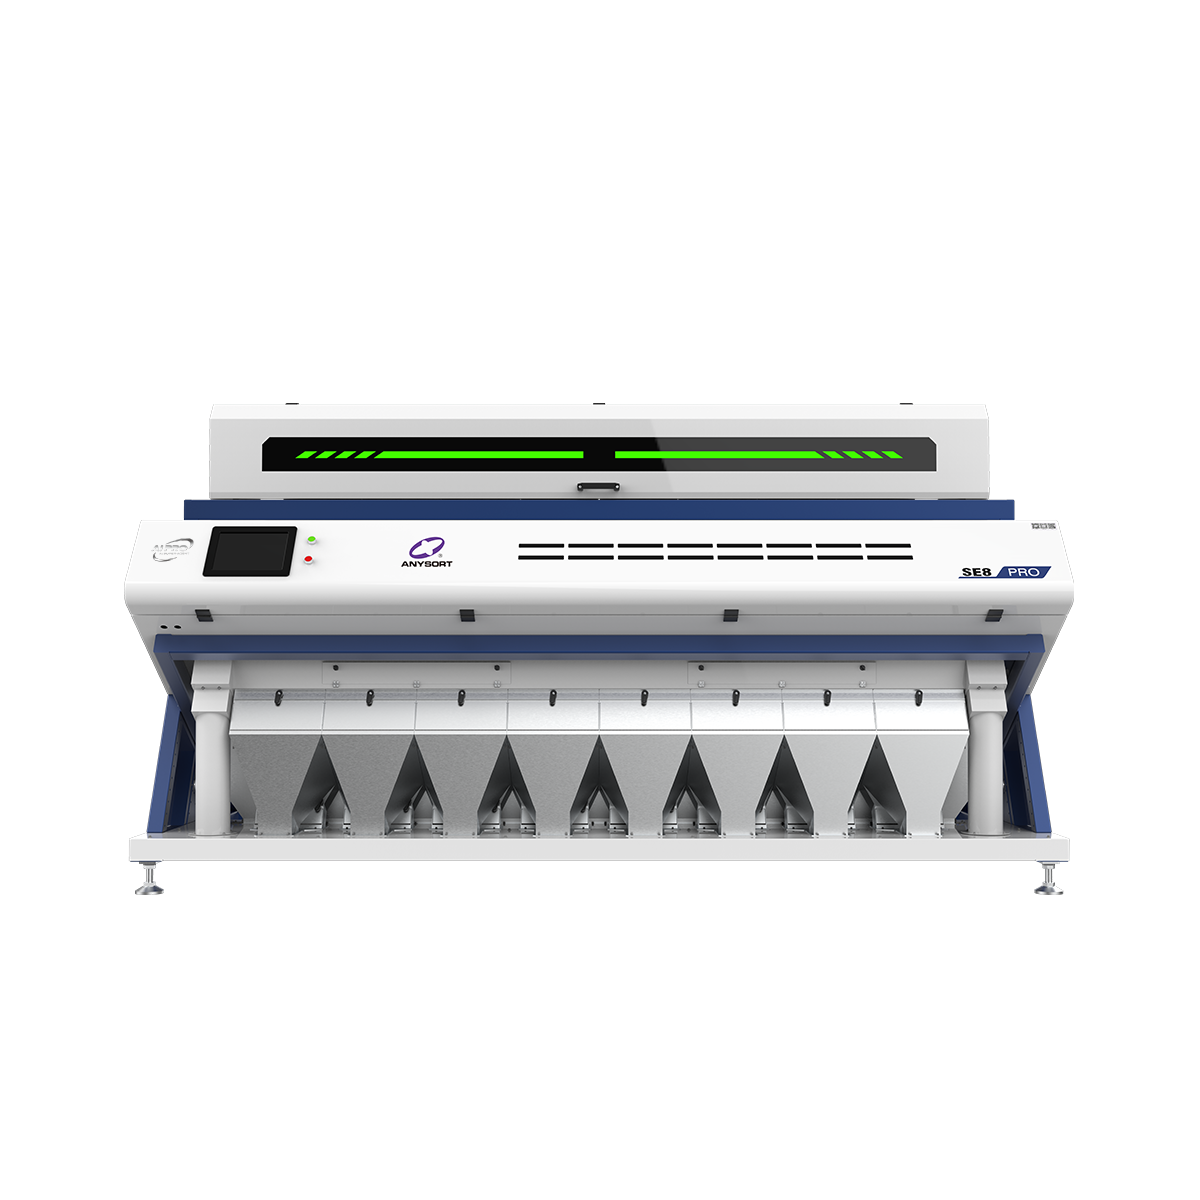
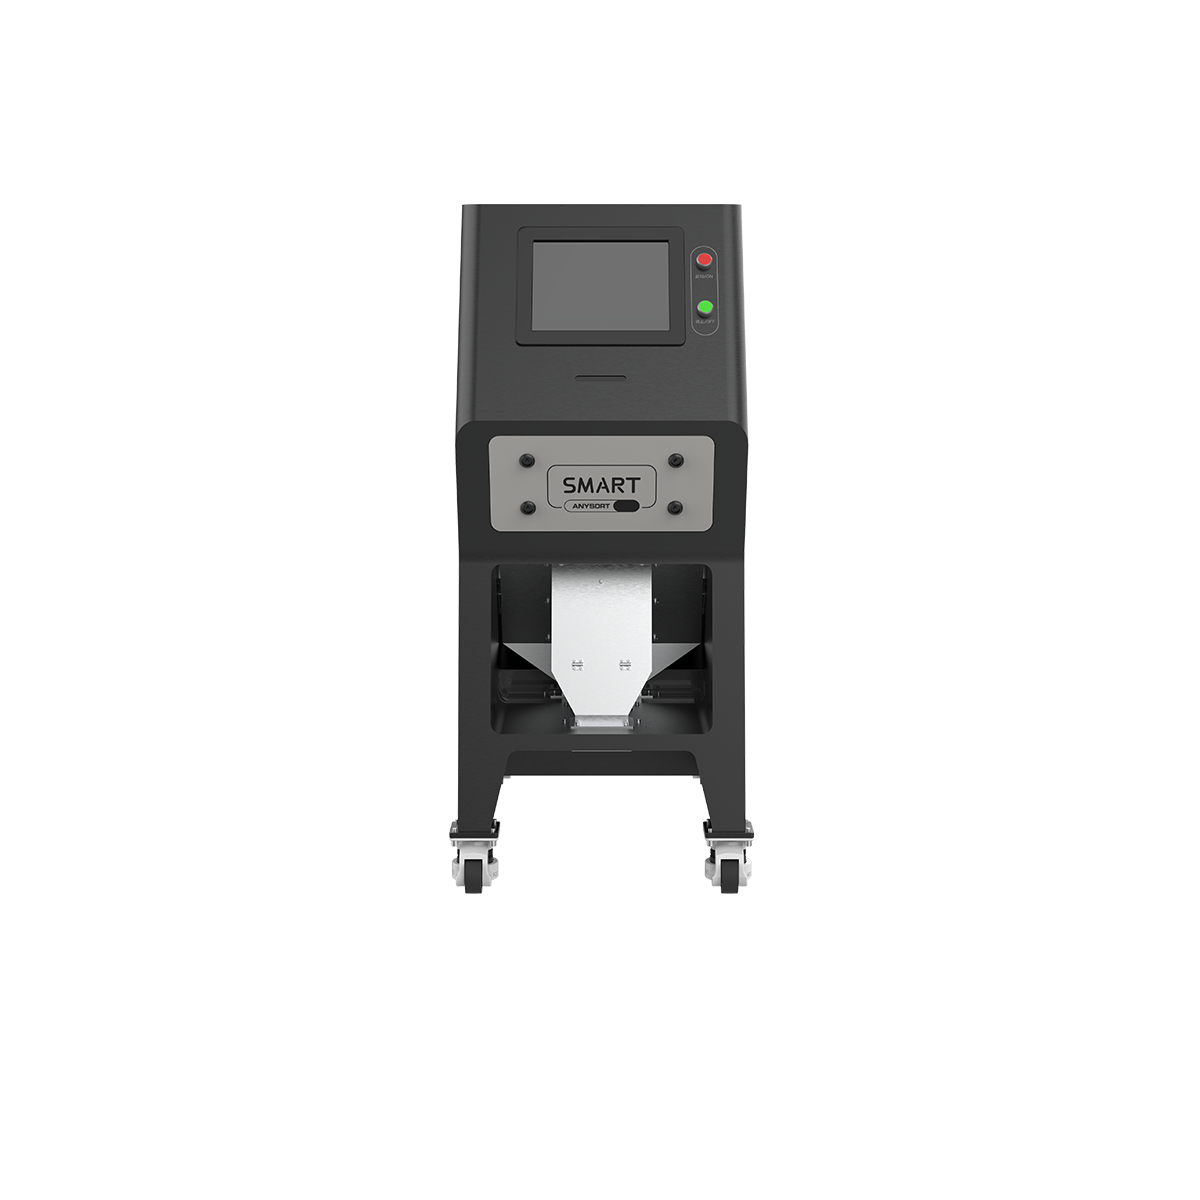
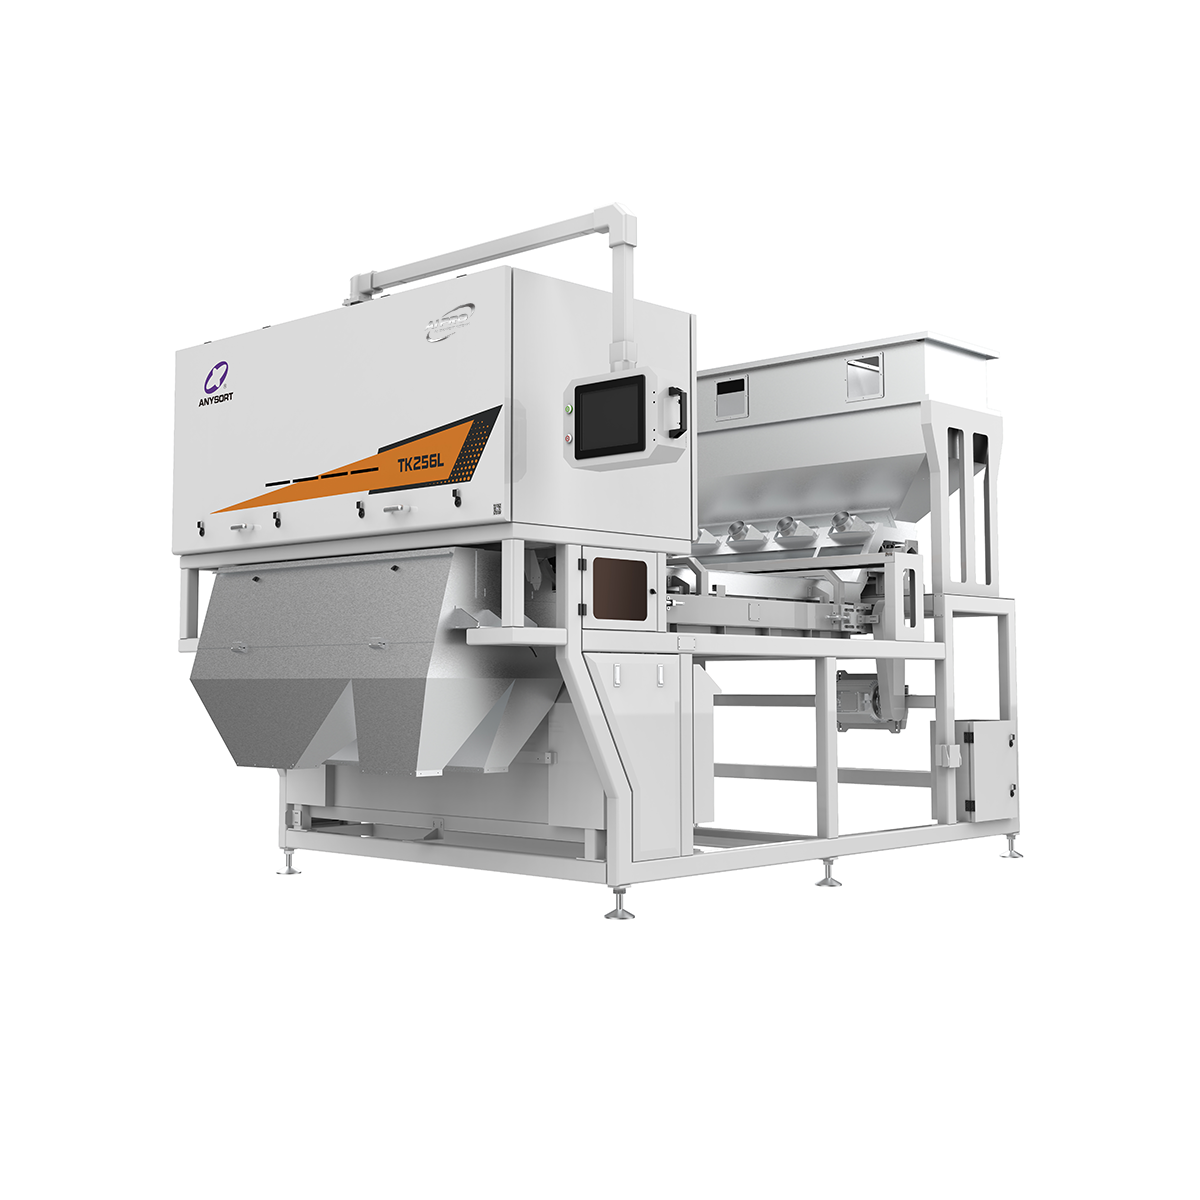
A color sorter corn is an advanced optical sorting machine designed to automatically separate corn kernels based on their color, quality, and physical characteristics. This innovative technology uses high-resolution cameras and sophisticated artificial intelligence algorithms to inspect each kernel individually as it passes through the sorting chamber. The color sorter corn identifies and removes discolored, damaged, moldy, or foreign materials with remarkable precision and speed.
The primary function of a color sorter corn is to enhance the quality of corn products destined for food processing, animal feed, and industrial applications. By removing inferior kernels before processing, the color sorter corn ensures that only premium-grade corn reaches your production line. The machine operates through a multi-stage process: kernels are fed into the hopper, spread across a conveyor belt, scanned by optical sensors, and then precisely ejected into separate collection bins based on predefined quality standards.
Key technological features of a color sorter corn include real-time image processing, adjustable sorting parameters, and automated rejection systems. Modern color sorter corn equipment incorporates machine learning technology that continuously improves sorting accuracy over time. The system can process thousands of kernels per minute while maintaining exceptional accuracy rates exceeding ninety-eight percent. Additionally, the color sorter corn integrates user-friendly control panels that allow operators to customize sorting criteria for different corn varieties and end-use applications, making it an invaluable asset for corn processing facilities worldwide.

 EN