Color Sort Machine | Advanced Optical Sorting

All Categories

color sort machine

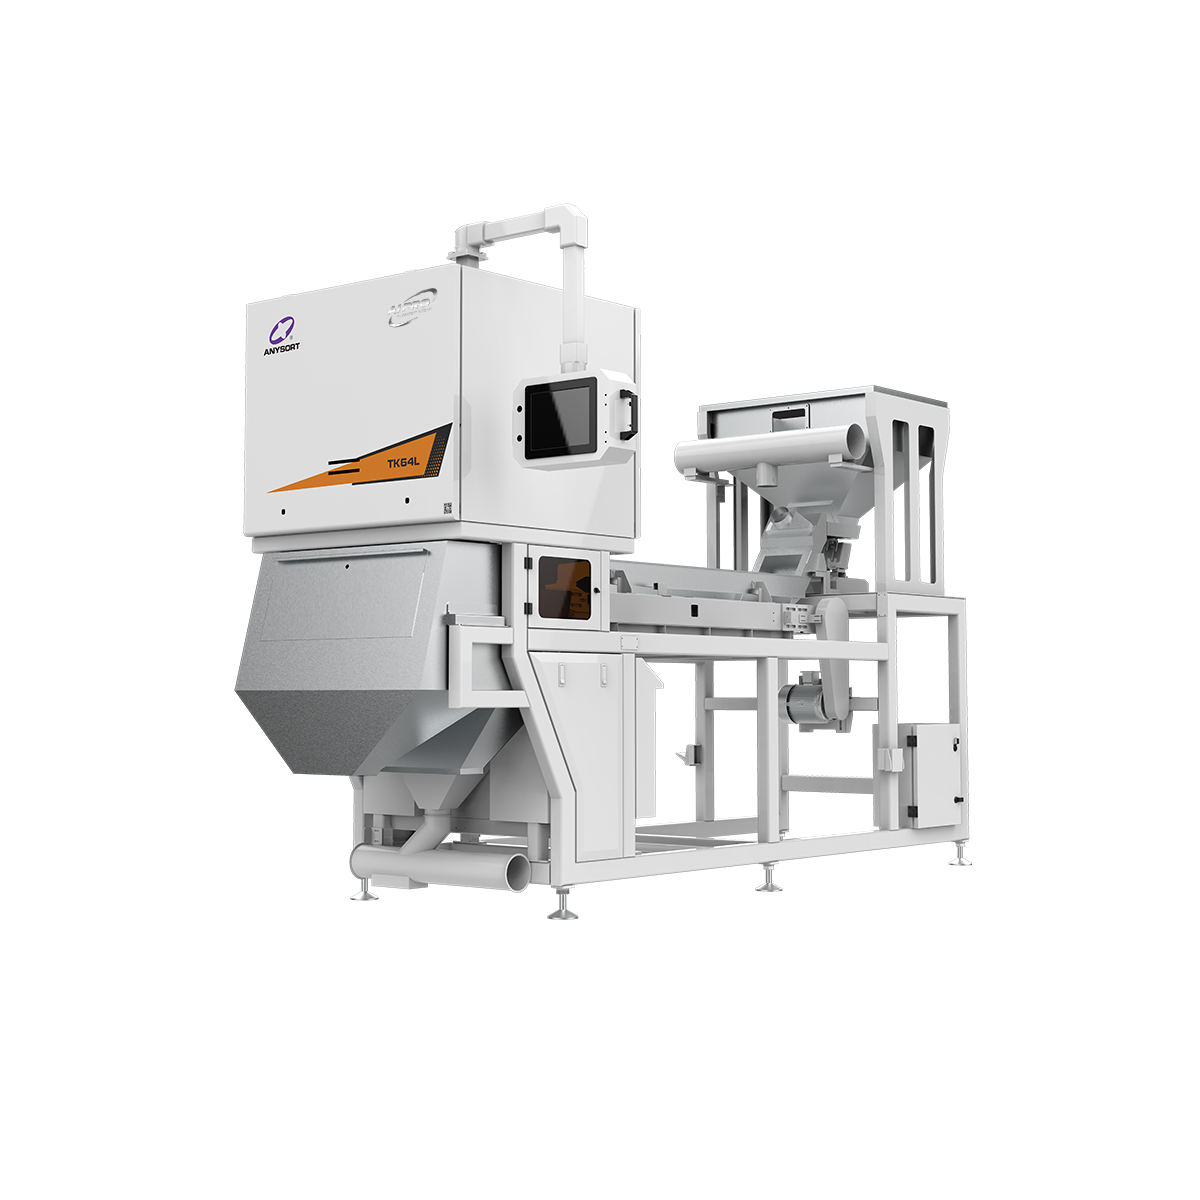
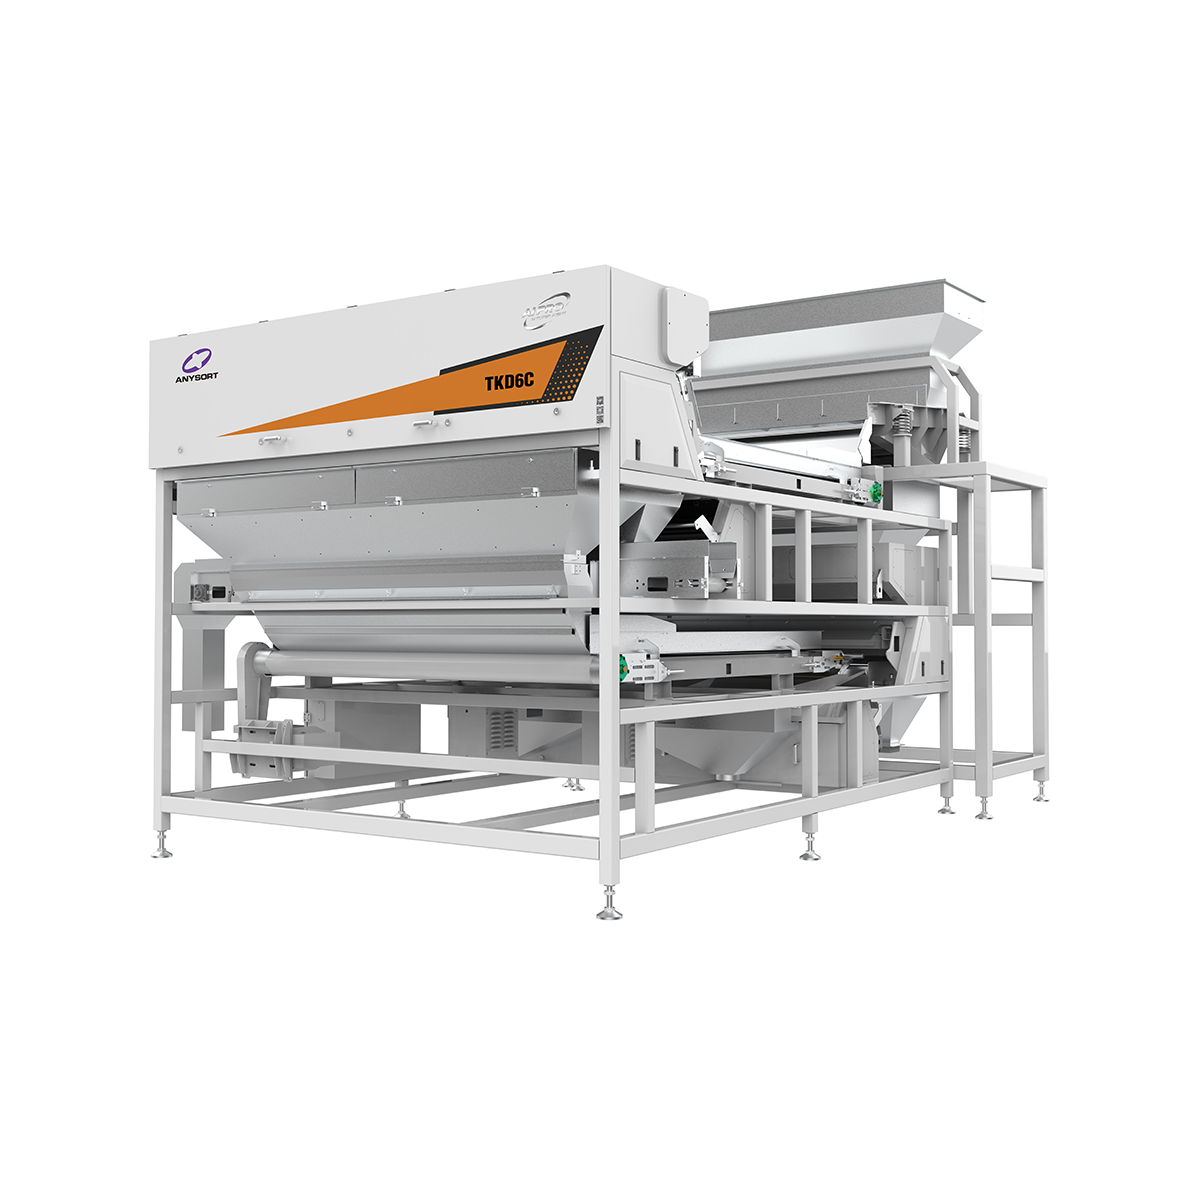
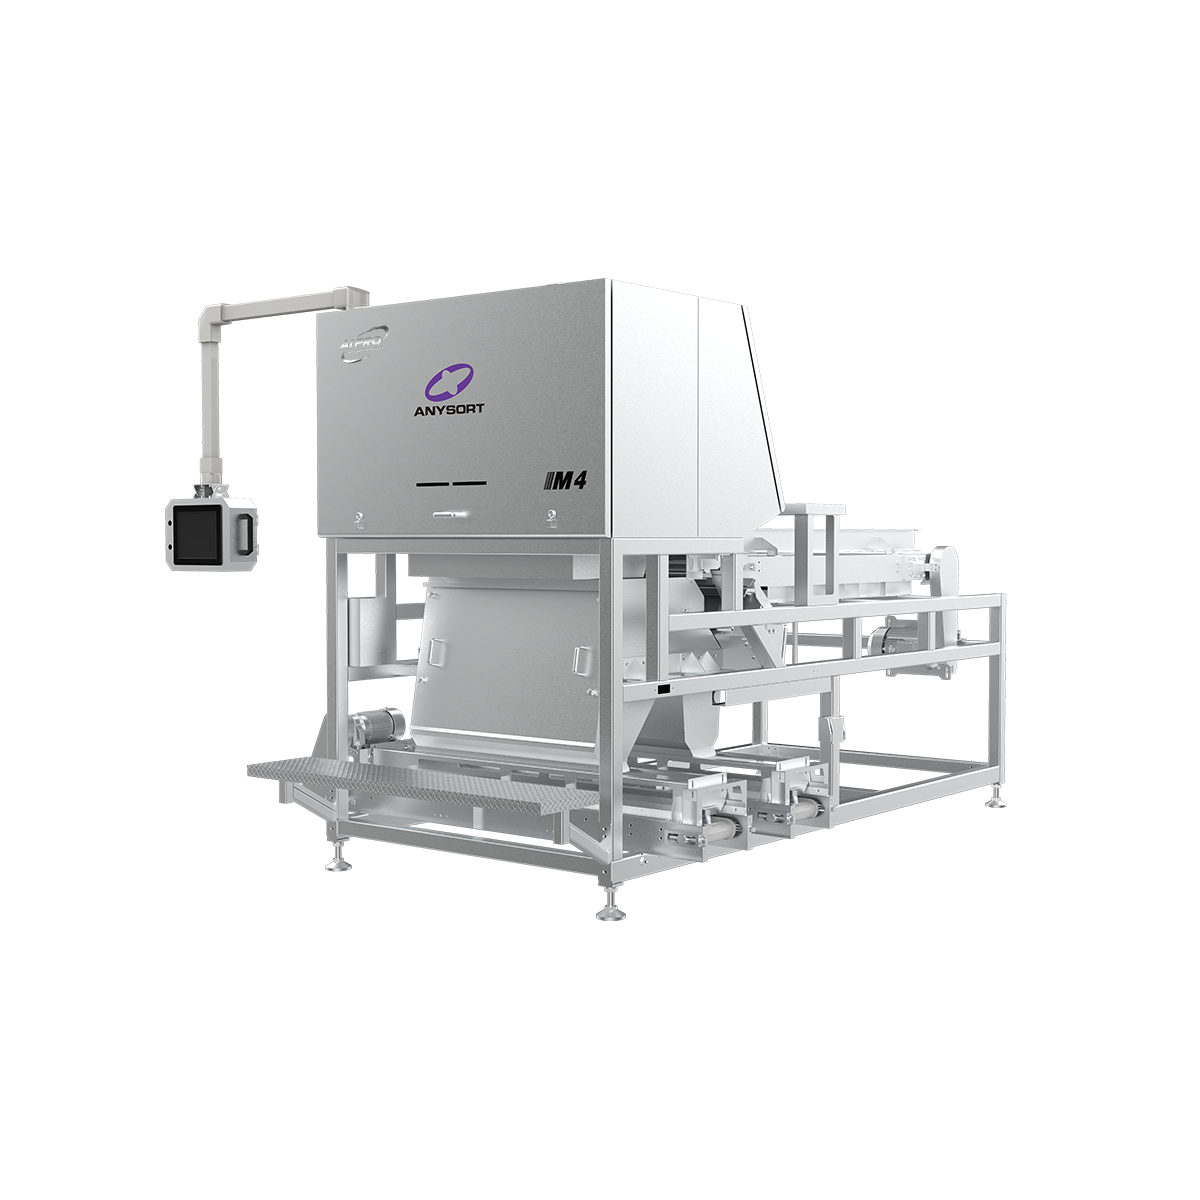
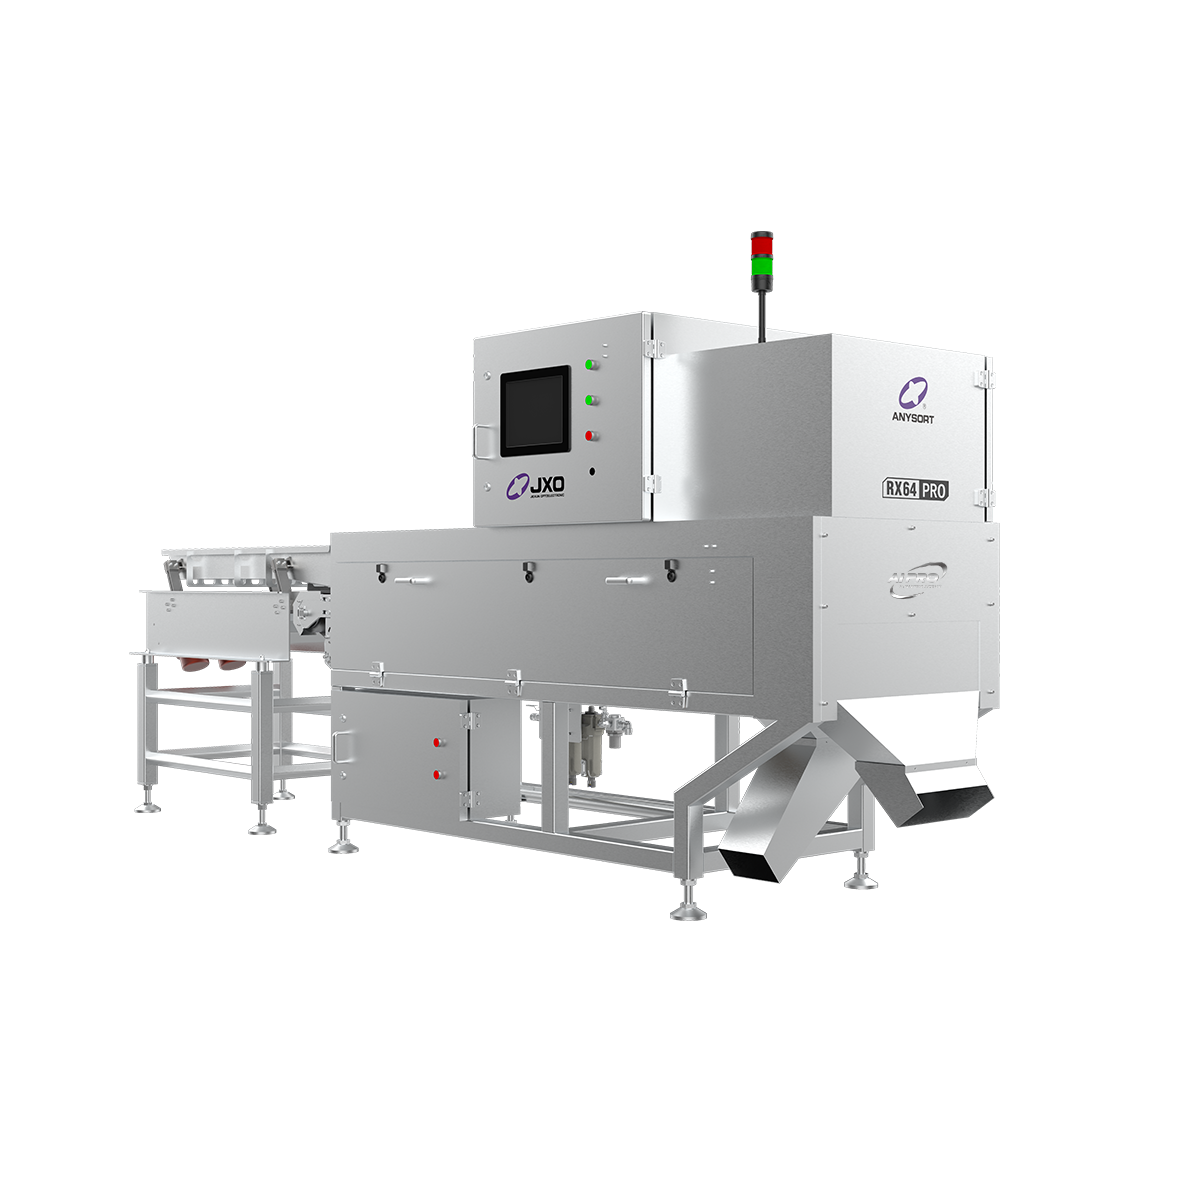
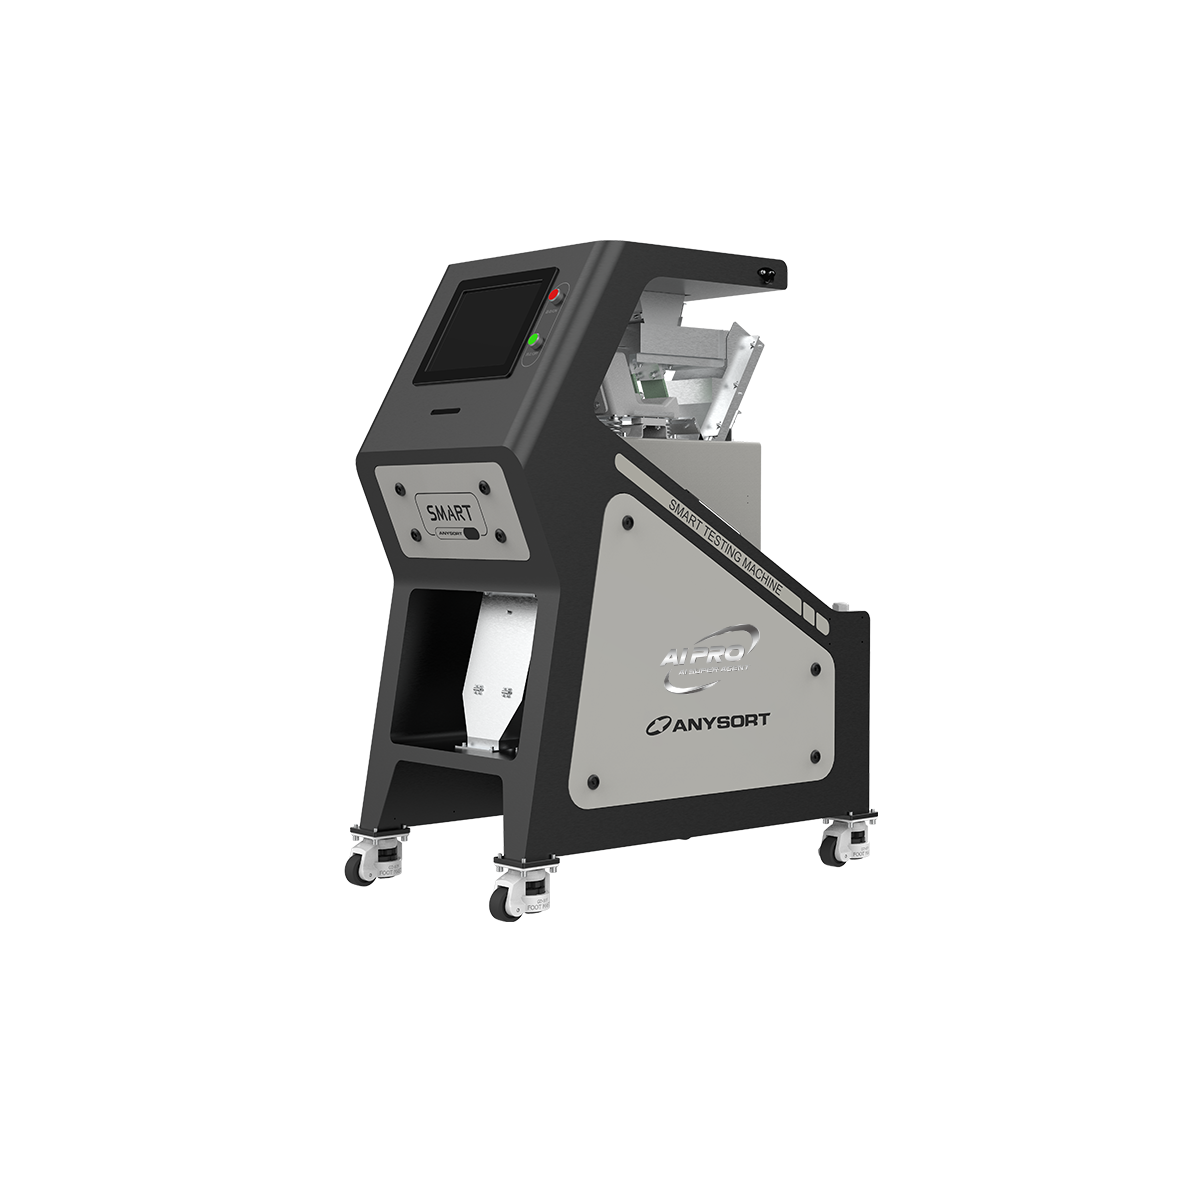
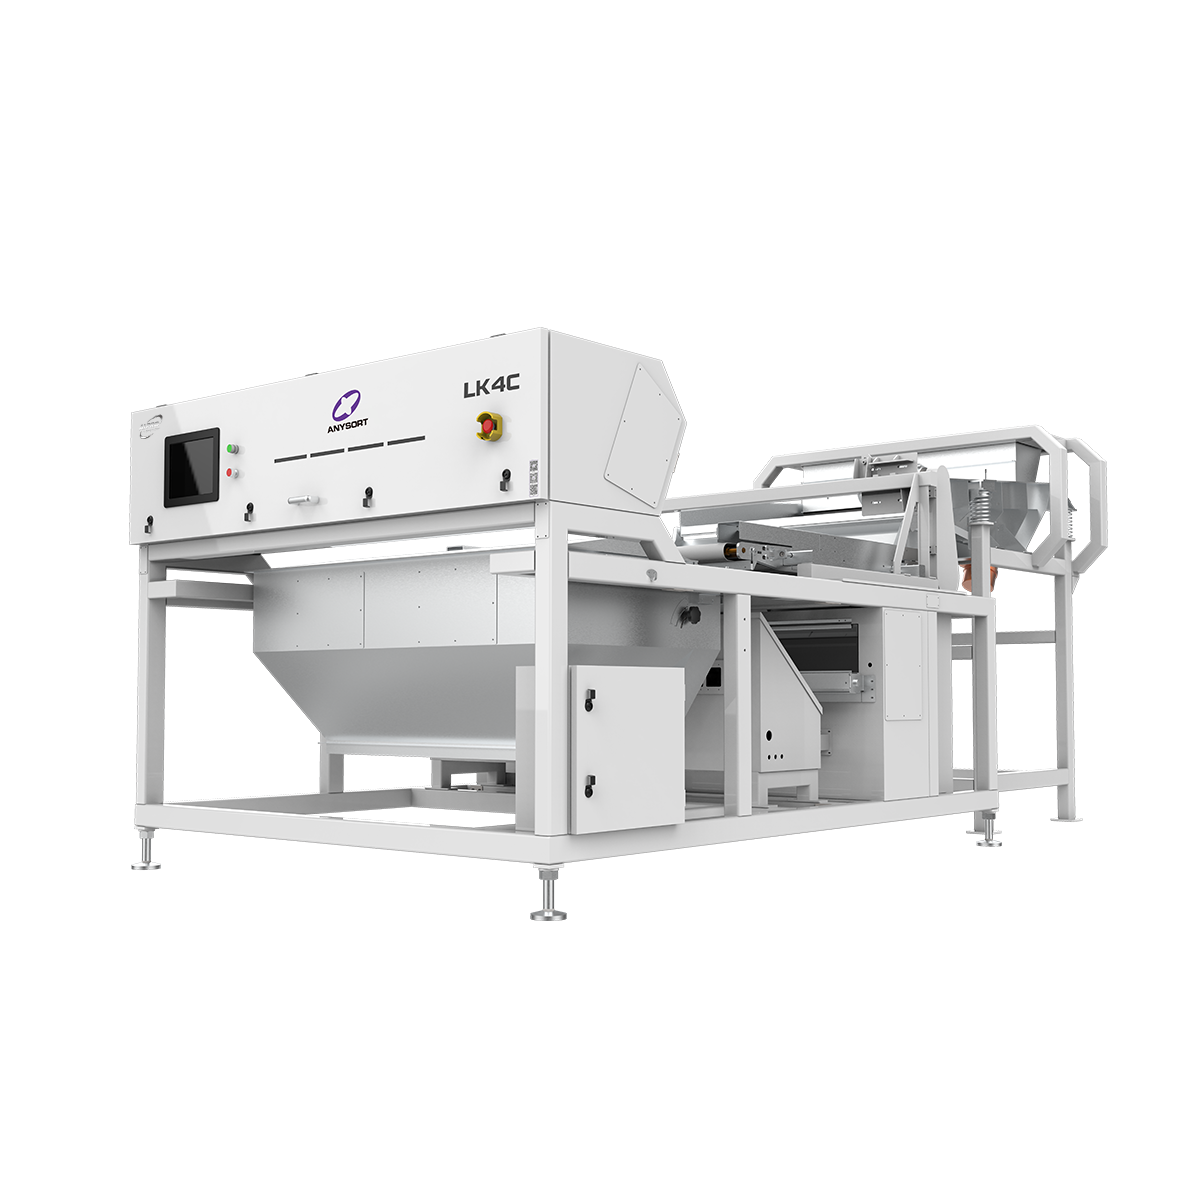
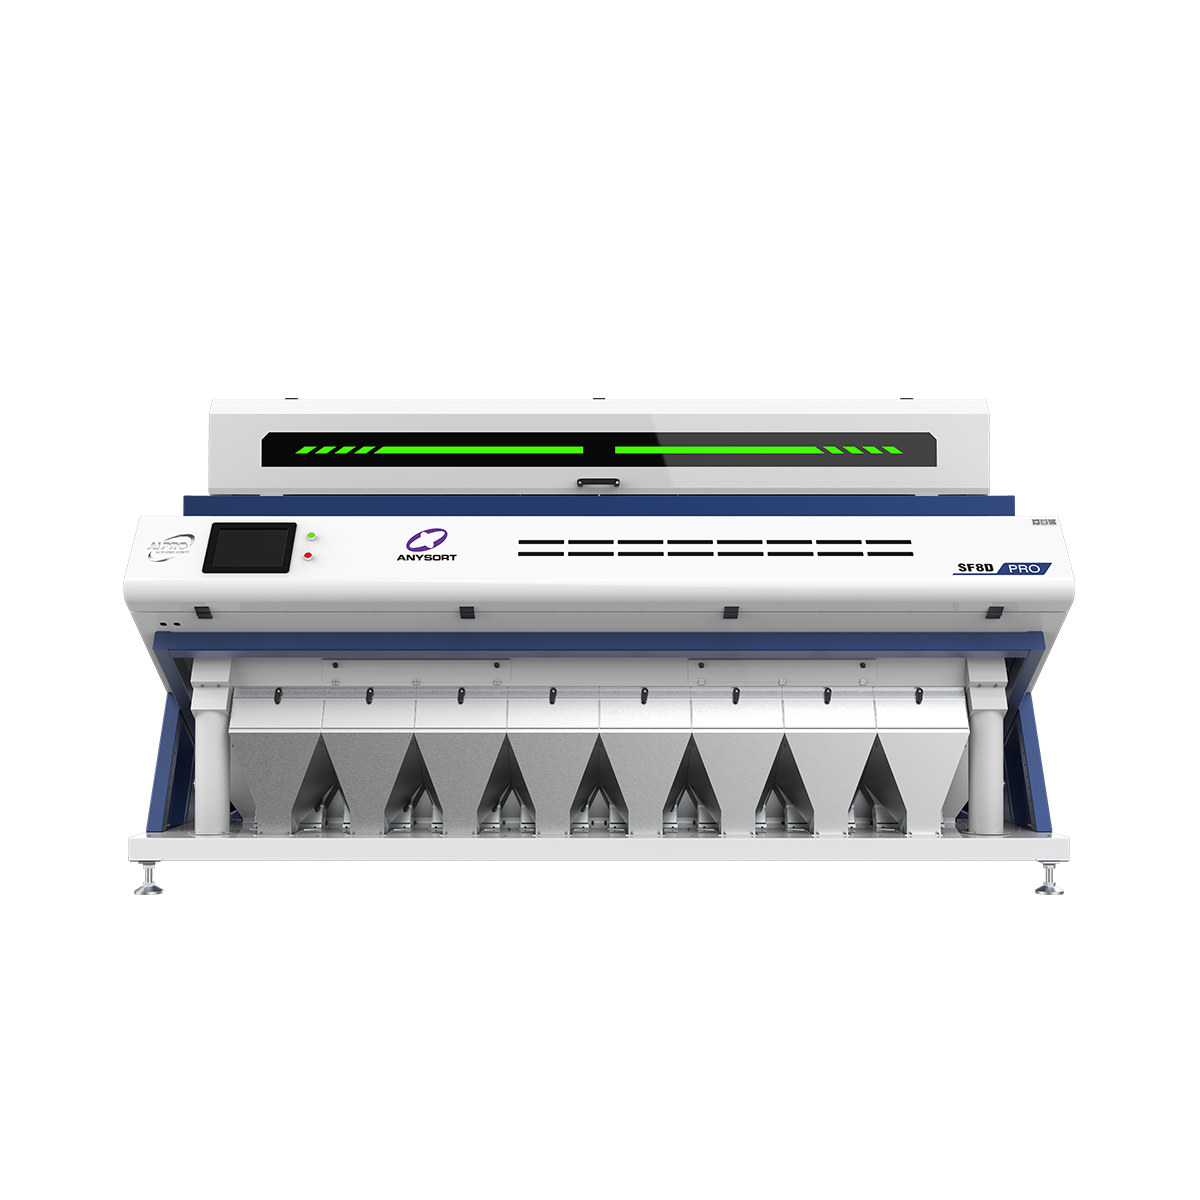
A color sort machine is an advanced optical sorting system designed to separate materials based on color characteristics with exceptional precision and speed. This innovative equipment uses cutting-edge camera technology and artificial intelligence to identify and categorize items by their color properties, making it an indispensable tool across multiple industries. The color sort machine operates through a sophisticated process where materials pass through detection zones equipped with high-resolution cameras that capture detailed images. These images are processed by intelligent algorithms that analyze color data in real-time, comparing each item against predetermined color standards and specifications. Once analysis is complete, the color sort machine uses pneumatic or mechanical ejectors to direct materials into appropriate collection bins or chutes based on their color classification. Modern color sort machine systems feature adjustable sensitivity settings, allowing operators to fine-tune sorting accuracy according to specific material requirements. The technology behind contemporary color sort machine equipment includes multi-spectral imaging, which can detect subtle color variations invisible to the human eye. This capability makes the color sort machine particularly valuable for quality control applications where consistency is critical. The color sort machine can process hundreds of tons of material daily, dramatically improving efficiency compared to manual sorting methods. Integration with factory automation systems allows the color sort machine to communicate data seamlessly with other equipment, creating fully optimized production lines. Industries ranging from food processing to recycling operations depend on color sort machine technology to maintain product quality, enhance profitability, and reduce waste throughout their operations.

Popular Products

The color sort machine delivers transformative benefits that directly impact your operational efficiency and bottom line. First, this equipment dramatically increases sorting speed, processing material far faster than manual labor while maintaining consistent accuracy levels that human workers cannot match. A color sort machine eliminates costly sorting errors that would otherwise result in product contamination or quality issues, protecting your brand reputation and customer satisfaction. The color sort machine operates continuously without fatigue, maintaining peak performance throughout entire production cycles, which means your facility gains substantial productivity gains without requiring additional workforce expansion. Labor cost reduction represents another compelling advantage of implementing a color sort machine system. By automating the sorting process, your company reduces dependence on manual workers for repetitive tasks, allowing staff to focus on higher-value responsibilities while the color sort machine handles classification duties. The color sort machine provides real-time sorting data and performance metrics, giving managers complete visibility into production quality and material flow. This transparency enables data-driven decision-making that optimizes your entire operation. Environmental benefits accompany the color sort machine technology, as precise sorting minimizes waste by ensuring every suitable piece gets properly classified and utilized. The color sort machine requires minimal maintenance compared to alternative sorting methods, keeping downtime and repair costs low. Implementation of a color sort machine typically generates quick return on investment through efficiency gains and waste reduction. The versatility of a color sort machine means it adapts to various material types, from agricultural products to plastic waste, making it valuable across diverse industries. Companies using a color sort machine gain competitive advantages through superior product consistency and faster market response times.

Latest News

How Can a Nuts Sorter Improve Your Production?

15

Aug

How Can a Nuts Sorter Improve Your Production?

A nuts sorter represents one of the most significant investments a food processing operation can make to enhance production quality and operational efficiency. The modern nuts sorter uses advanced imaging and sensor technology to identify and separat...
View More
How Does Nuts Sorter Technology Ensure Quality?

19

Aug

How Does Nuts Sorter Technology Ensure Quality?

The global nuts processing industry relies on precision and consistency to meet strict quality standards and regulatory requirements. A nuts sorter has become indispensable for processors seeking to eliminate defects, contaminants, and substandard pr...
View More
How Do Color Sorters Improve Product Quality?

26

Aug

How Do Color Sorters Improve Product Quality?

Product quality stands as a critical differentiator in competitive industrial markets, and achieving consistency at scale requires more than manual oversight. A color sorter represents one of the most effective technologies for identifying and removi...
View More
Which factors should you consider when selecting a rice color sorter?

29

Aug

Which factors should you consider when selecting a rice color sorter?

Selecting the right rice color sorter is a critical decision that directly impacts your grain processing efficiency, product quality, and long-term profitability. A rice color sorter removes discolored, damaged, and foreign particles from rice batche...
View More

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

color sort machine

Advanced Optical Detection Technology

Advanced Optical Detection Technology

The color sort machine incorporates state-of-the-art optical sensors and high-resolution cameras that capture precise color information across the full spectrum. This technology enables the color sort machine to distinguish between hundreds of individual color variations, even detecting subtle shades that appear identical to human observers. The advanced imaging system within each color sort machine operates at incredible speeds, analyzing material in milliseconds to ensure rapid throughput without sacrificing accuracy. The color sort machine's optical detection works seamlessly across different material types, sizes, and conditions, adapting automatically to changing environmental lighting. Real-time processing power embedded in the color sort machine allows immediate sorting decisions, preventing material jams and ensuring smooth operation. The sophisticated algorithms powering the color sort machine continuously learn and adjust, improving accuracy over time as the system processes more material and refines its color recognition capabilities.
High-Capacity Processing Performance

High-Capacity Processing Performance

Modern color sort machine systems handle tremendous material volumes, processing hundreds of tons daily while maintaining exceptional sorting precision. The color sort machine achieves this impressive throughput through optimized conveyor systems and rapid ejection mechanisms that work in perfect synchronization. Facilities implementing a color sort machine experience minimal production bottlenecks since this equipment matches or exceeds the speed of upstream processes. The color sort machine design minimizes material damage during sorting, protecting product integrity and value throughout the classification process. Scalable architecture means your color sort machine system grows with your business needs, easily adapting to increased production demands. The color sort machine provides consistent performance across extended operating sessions, delivering reliable results that support continuous production schedules without requiring frequent stoppages for calibration or maintenance.
Intelligent Data Analytics Integration

Intelligent Data Analytics Integration

Every color sort machine generates valuable operational data that provides unprecedented insight into your production quality and efficiency metrics. The color sort machine system captures detailed sorting statistics, color distribution patterns, and material rejection rates that inform strategic business decisions. Integration capabilities allow your color sort machine to connect with existing factory management systems, creating unified data ecosystems that optimize entire production lines. Real-time dashboards powered by color sort machine data enable managers to monitor performance instantly and identify potential issues before they impact production. Historical data collected by the color sort machine reveals trends that highlight improvement opportunities and guide equipment optimization strategies. Advanced reporting features in the color sort machine software help identify contamination sources, track material consistency, and benchmark performance against industry standards, supporting continuous improvement initiatives throughout your organization.

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

Copyright © 2026 Anhui Jiexun Optoelectronic Technology Co., Ltd. All rights reserved.  -  Privacy policy