Grain Color Sorter: Advanced Optical Sorting

All Categories

grain color sorter

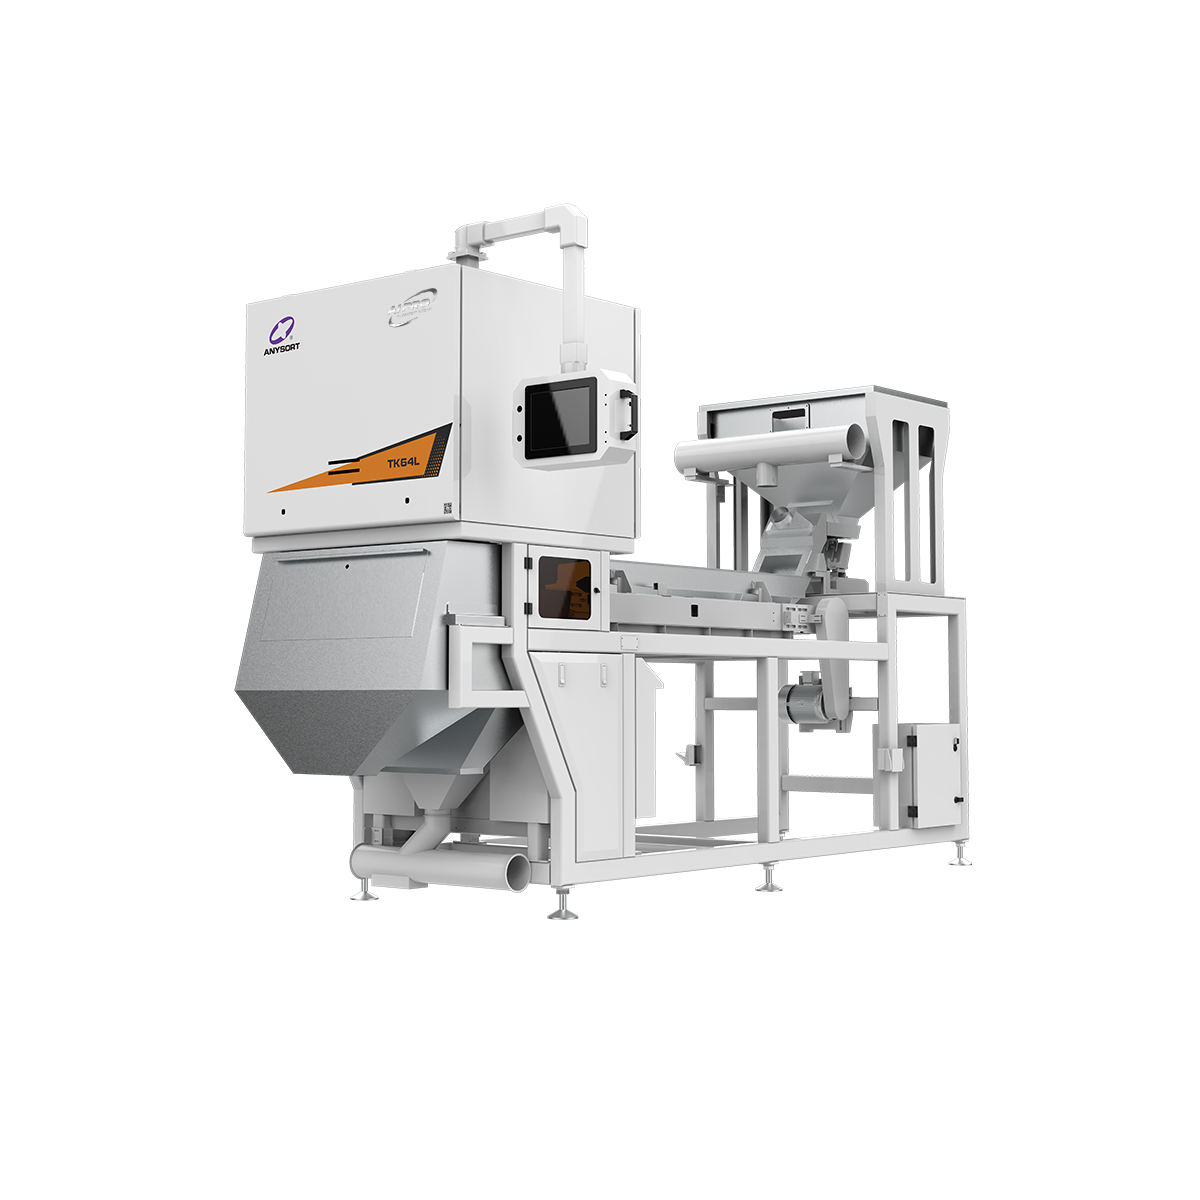
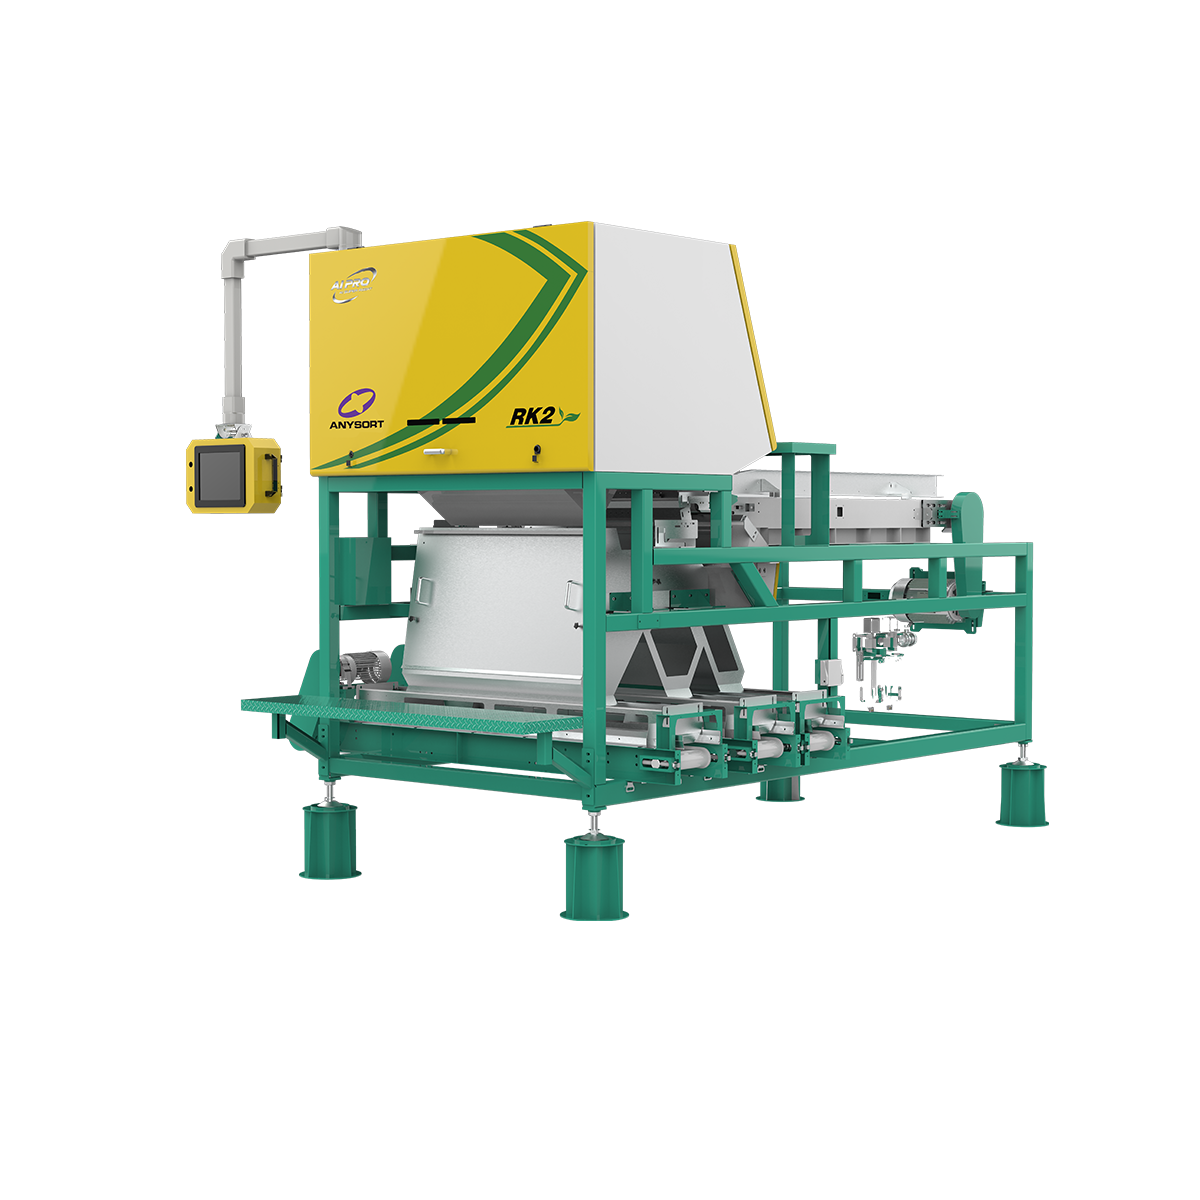
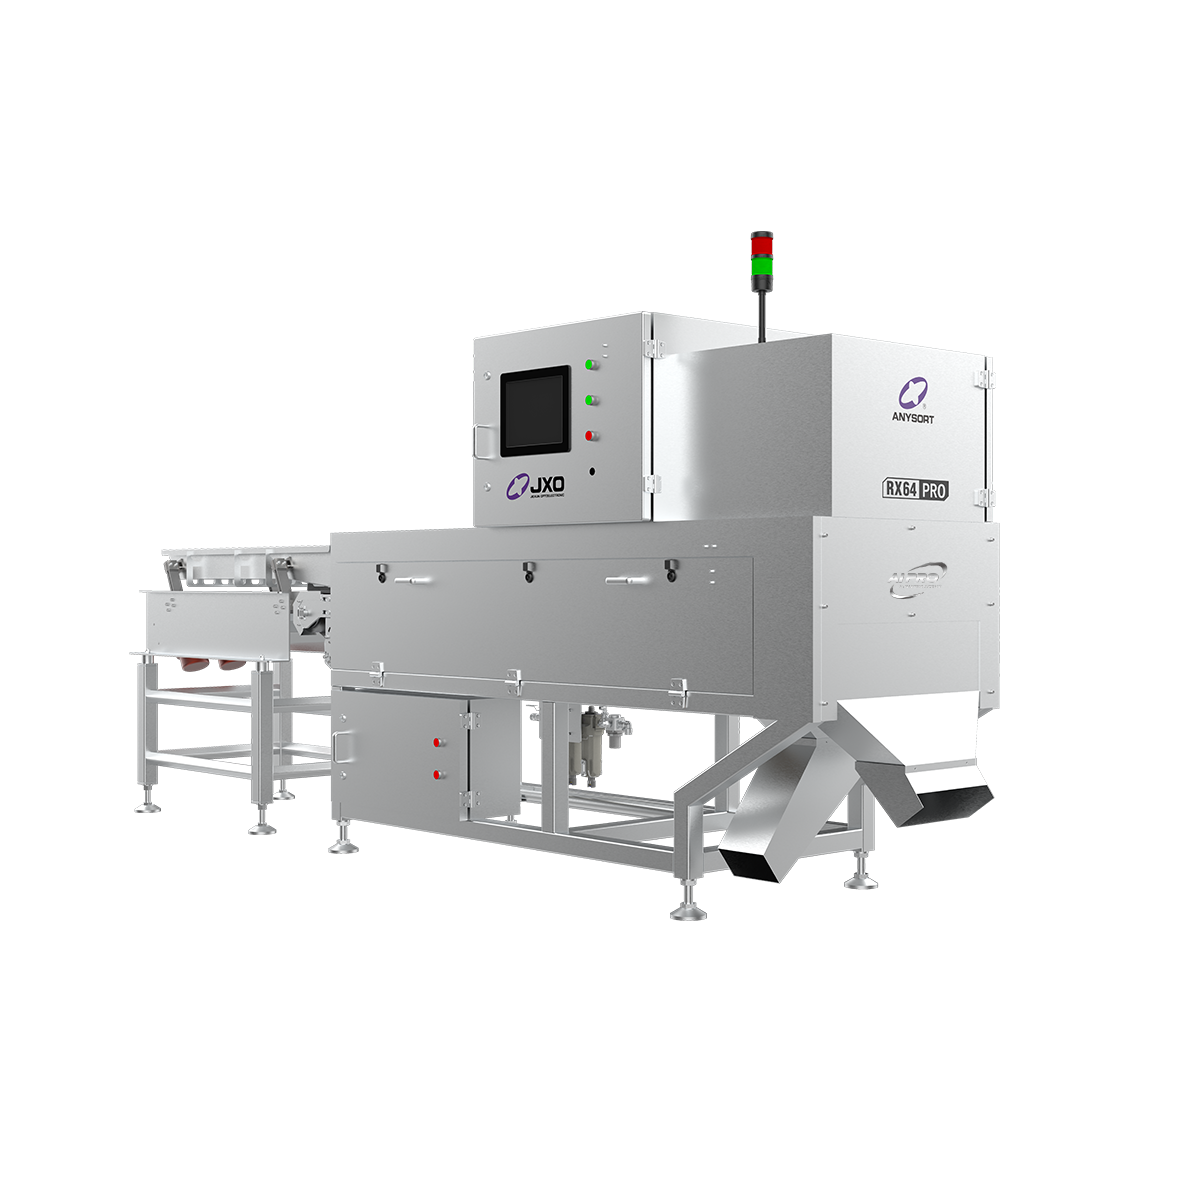
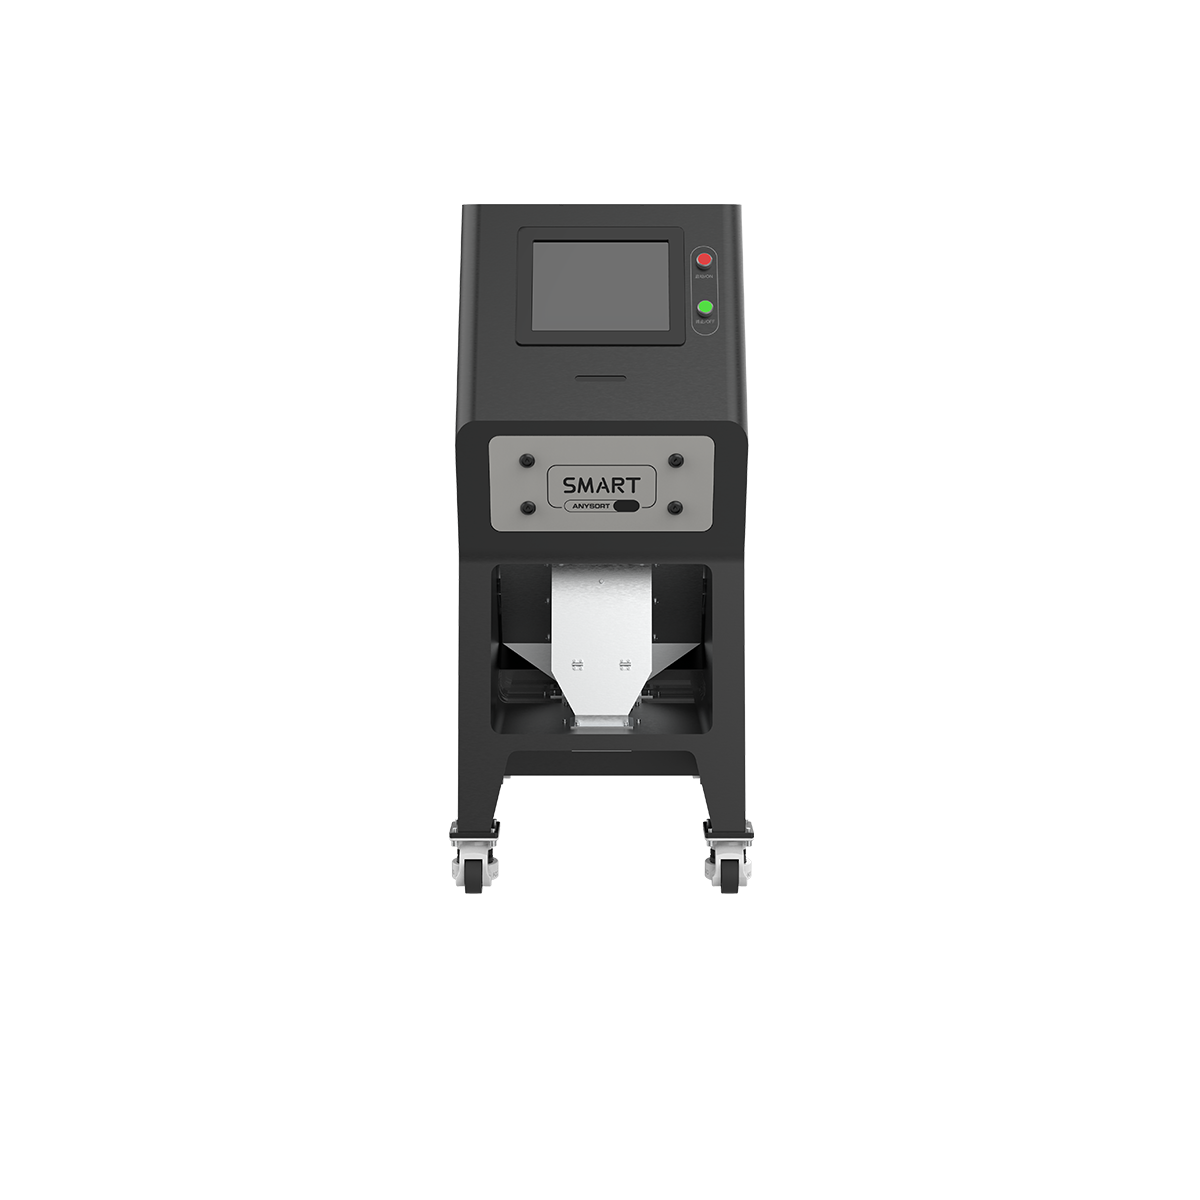
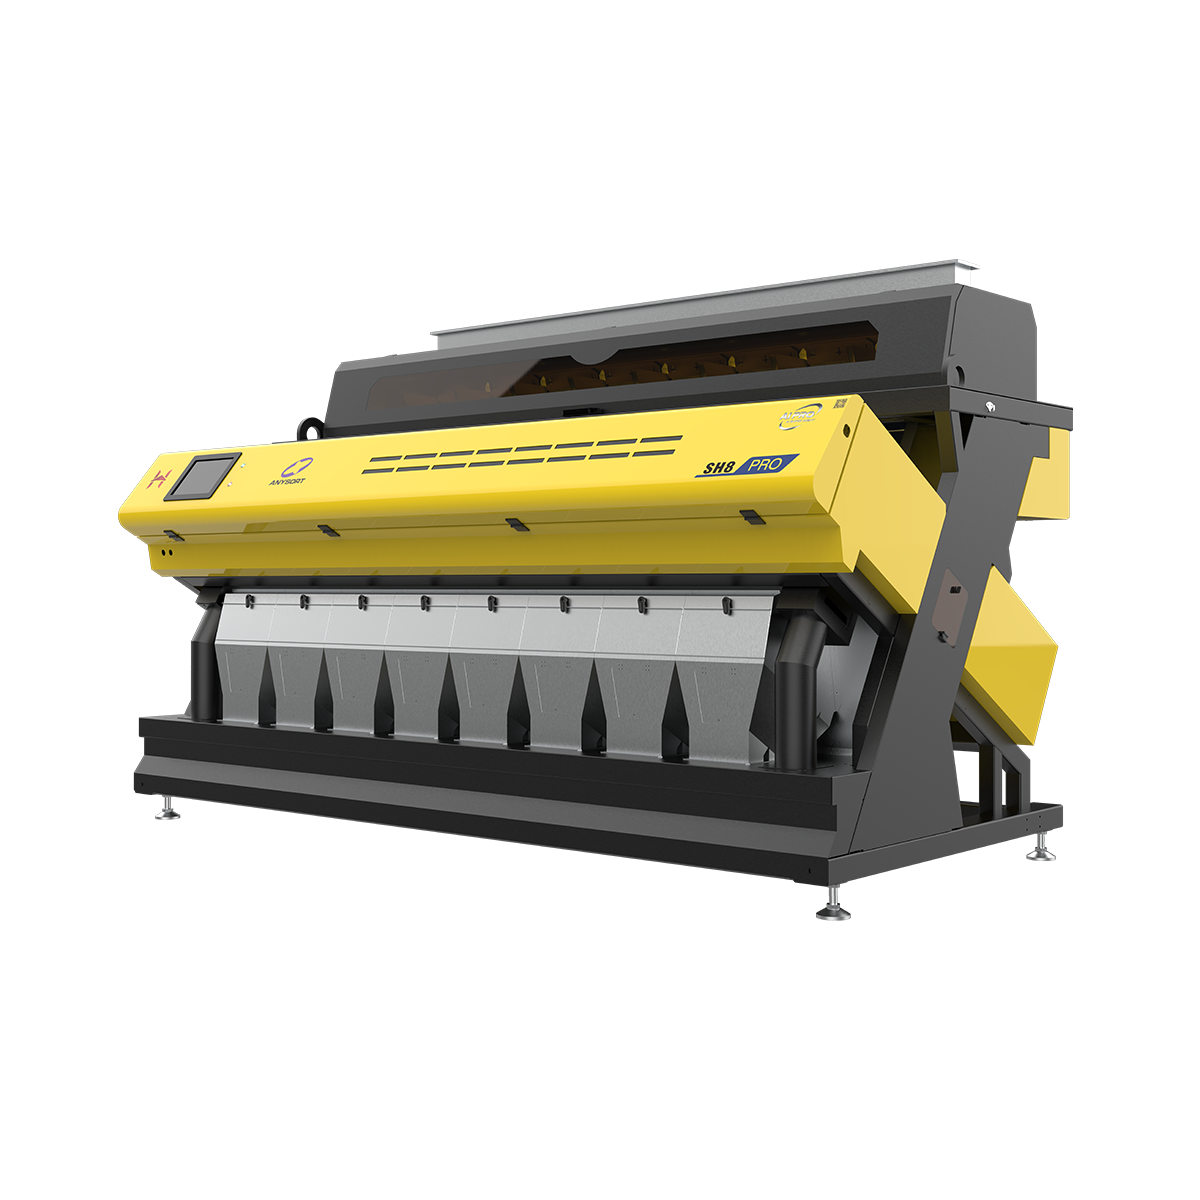
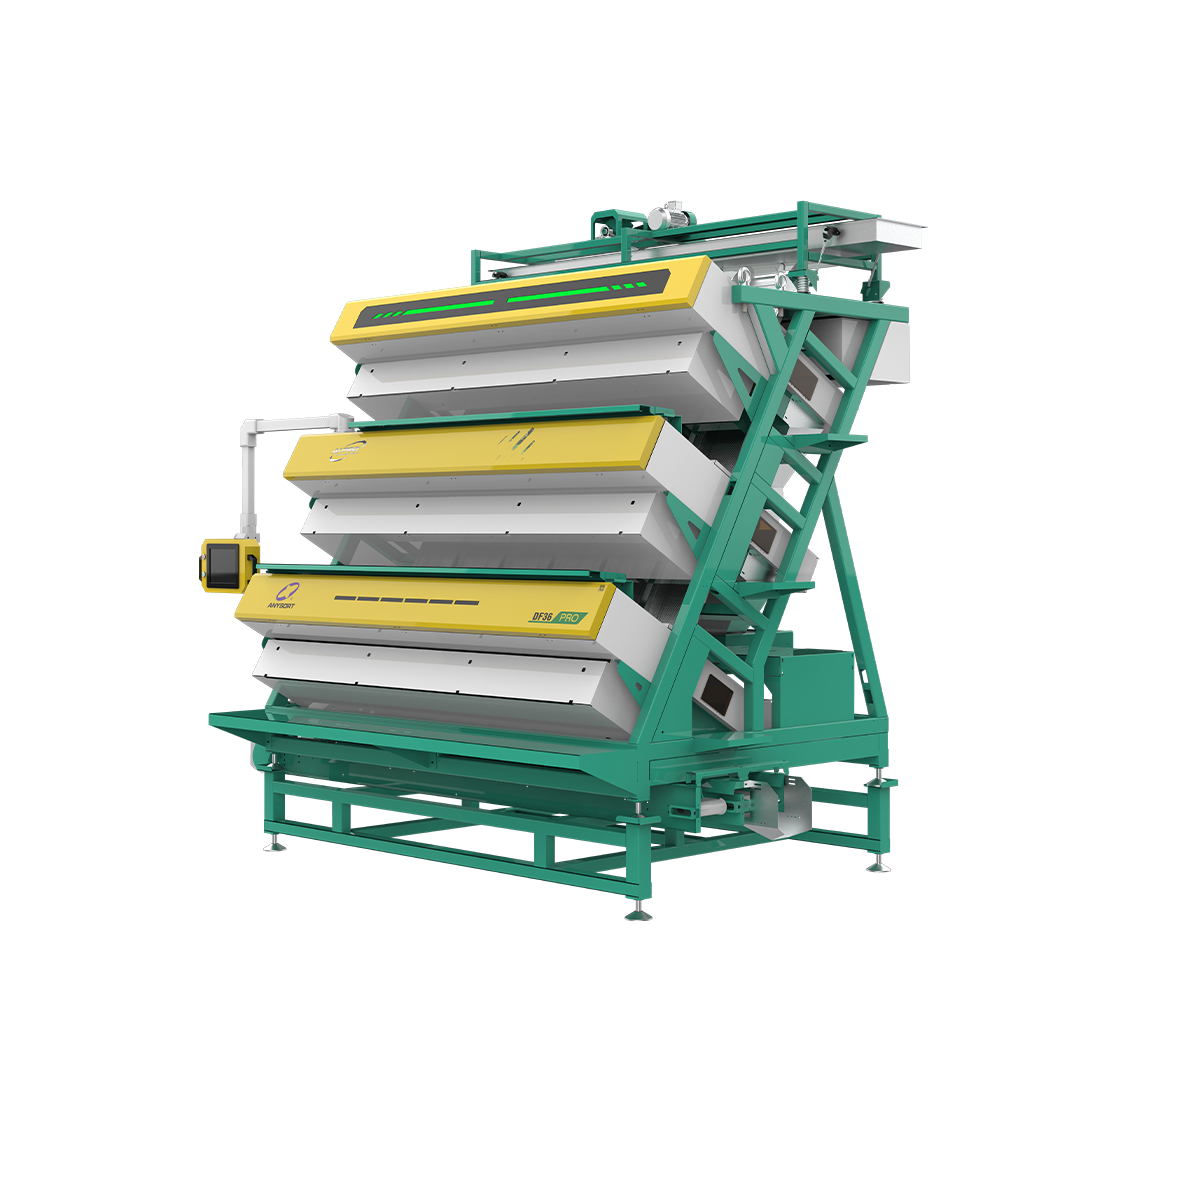
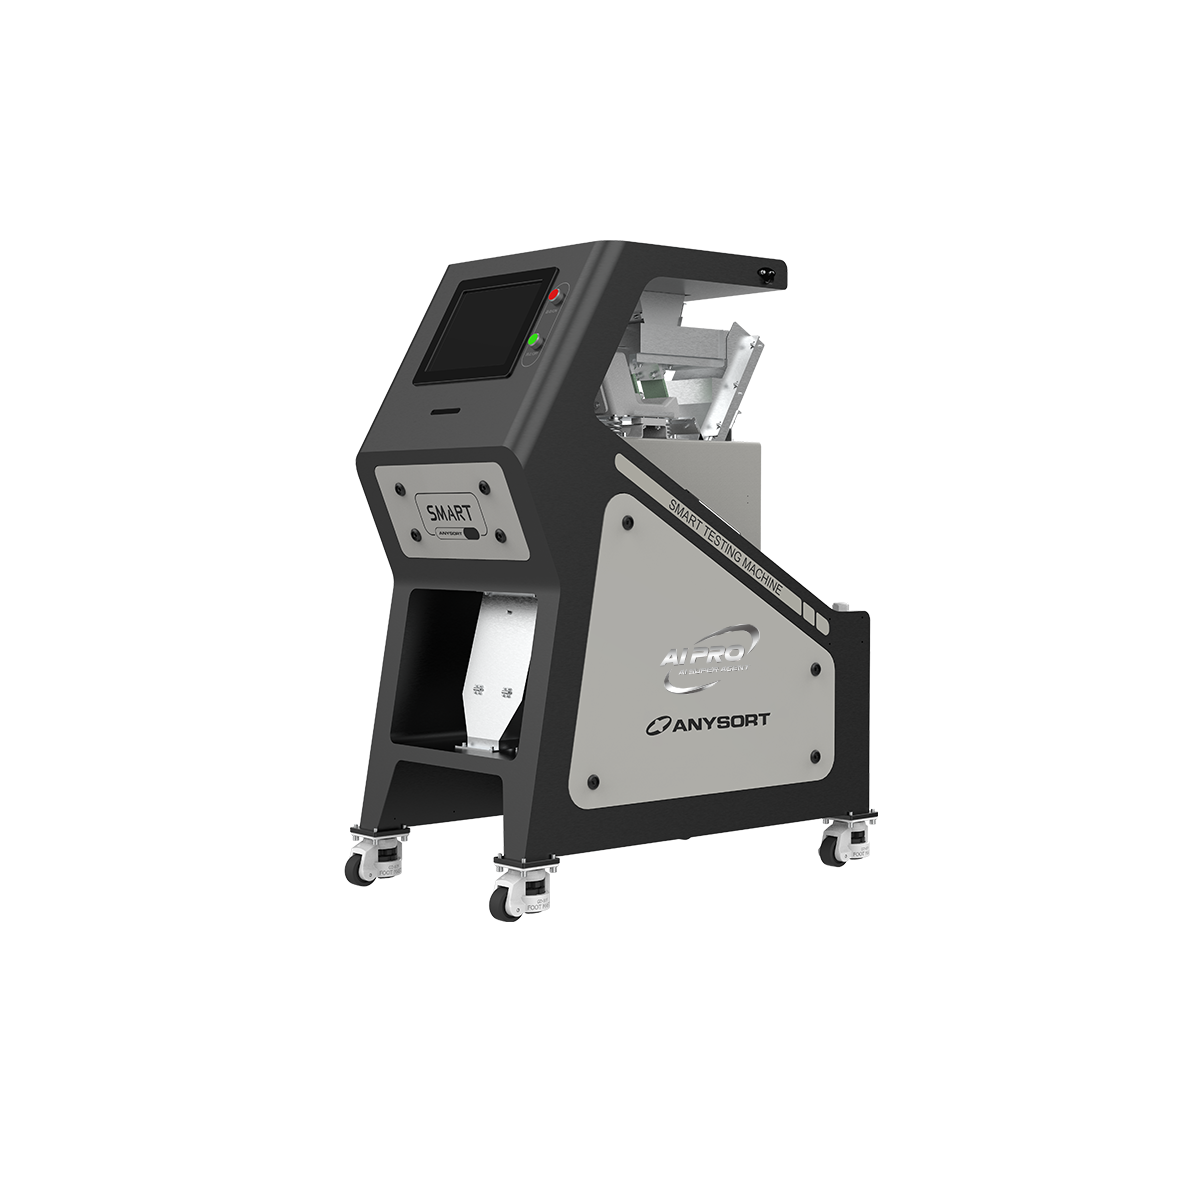
A grain color sorter is an advanced optical sorting machine designed to improve grain quality by identifying and removing discolored, damaged, or foreign particles from bulk grain shipments. This sophisticated grain color sorter uses high-resolution cameras and artificial intelligence technology to scan each grain individually at remarkable speeds, achieving sorting accuracy rates exceeding 99 percent. The grain color sorter operates by directing grain through illuminated channels where specialized sensors detect color variations, size inconsistencies, and surface defects that human inspectors would miss. Modern grain color sorter systems process hundreds of kilograms per hour while maintaining exceptional precision. The technology behind a grain color sorter includes spectral imaging, LED lighting systems, and machine learning algorithms that continuously improve detection capabilities. Applications for the grain color sorter span across various industries including rice mills, wheat processing facilities, legume producers, and food manufacturers. The grain color sorter eliminates contaminated kernels, preserves premium grain quality, and reduces waste throughout production cycles. Agricultural operations rely on the grain color sorter to meet international food safety standards and maintain market competitiveness. Installation of a grain color sorter typically requires minimal modifications to existing processing lines. The grain color sorter delivers consistent performance across different grain types and processing volumes.

Popular Products

The grain color sorter delivers substantial operational improvements that directly benefit grain processing businesses of all sizes. By implementing a grain color sorter, companies eliminate defective grains automatically, significantly reducing labor costs associated with manual sorting while dramatically improving output consistency. The grain color sorter removes contaminated material before packaging, protecting brand reputation and ensuring customer satisfaction with every purchase. Processing efficiency increases substantially when using a grain color sorter because machines work continuously without fatigue, maintaining constant quality standards throughout production shifts. The grain color sorter maximizes revenue by transforming partially acceptable grain batches into premium products commanding higher market prices. Investment in a grain color sorter reduces product liability risks by removing dangerous contaminants including stones, insects, and disease-carrying particles before distribution. Grain producers using a grain color sorter achieve faster processing cycles, enabling increased throughput without proportional increases in facility overhead. The grain color sorter adapts easily to different grain varieties, allowing facilities to process multiple commodities without recalibration. Environmental benefits emerge when a grain color sorter identifies and separates recyclable or compostable materials from primary grain streams. The grain color sorter provides detailed reporting on batch quality metrics, helping managers optimize purchasing decisions and identify supplier issues. Customer demand for contamination-free products makes the grain color sorter an essential investment for competitive market positioning. Maintenance requirements for a grain color sorter remain minimal, featuring quick-change components and accessible design for routine service.

Latest News

How to Choose the Right Tea Color Sorter for Your Needs?

01

Aug

How to Choose the Right Tea Color Sorter for Your Needs?

Selecting the right tea color sorter is one of the most critical decisions tea processors face when modernizing their operations. A tea color sorter directly impacts product quality, operational efficiency, and market competitiveness. The wrong choic...
View More
How Does Nuts Sorter Technology Ensure Quality?

19

Aug

How Does Nuts Sorter Technology Ensure Quality?

The global nuts processing industry relies on precision and consistency to meet strict quality standards and regulatory requirements. A nuts sorter has become indispensable for processors seeking to eliminate defects, contaminants, and substandard pr...
View More
How Do Color Sorters Improve Product Quality?

26

Aug

How Do Color Sorters Improve Product Quality?

Product quality stands as a critical differentiator in competitive industrial markets, and achieving consistency at scale requires more than manual oversight. A color sorter represents one of the most effective technologies for identifying and removi...
View More
Which factors should you consider when selecting a rice color sorter?

29

Aug

Which factors should you consider when selecting a rice color sorter?

Selecting the right rice color sorter is a critical decision that directly impacts your grain processing efficiency, product quality, and long-term profitability. A rice color sorter removes discolored, damaged, and foreign particles from rice batche...
View More

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

grain color sorter

Advanced Optical Detection Technology

Advanced Optical Detection Technology

The grain color sorter incorporates cutting-edge optical detection systems that identify grain quality characteristics invisible to the human eye. Each kernel passes through precisely calibrated lighting chambers where multiple cameras capture detailed images from various angles simultaneously. The grain color sorter's imaging technology distinguishes between subtle color variations, surface blemishes, and structural abnormalities with exceptional accuracy. Artificial intelligence algorithms within the grain color sorter process thousands of images per second, making instantaneous sorting decisions for individual grains. This sophisticated detection system in the grain color sorter ensures that premium-grade grains separate cleanly from substandard material. The technology allows a grain color sorter to identify and remove chalky kernels, broken pieces, damaged seeds, and discolored grains automatically. Advanced spectral analysis within the grain color sorter detects chemical composition variations that indicate spoilage or contamination. The grain color sorter's optical system operates reliably under varying ambient light conditions, maintaining consistent performance regardless of facility environment. Users benefit from the grain color sorter's ability to handle diverse grain types without manual adjustments between commodity batches.
High-Speed Processing Capacity

High-Speed Processing Capacity

Modern grain color sorter equipment processes grain at industrial scale while maintaining exceptional sorting accuracy that manual methods cannot achieve. The grain color sorter handles processing volumes reaching hundreds of kilograms per hour, dramatically accelerating production timelines for bulk grain operations. Speed advantages of the grain color sorter translate directly into reduced processing costs and increased facility throughput without expansion investments. The grain color sorter maintains this impressive processing velocity while detecting minute defects that would require complete production line shutdowns if discovered later during quality checks. High-capacity grain color sorter systems enable facilities to process entire harvests within compressed timeframes, supporting seasonal operations effectively. The grain color sorter's speed eliminates bottlenecks that traditionally constrained grain processing facilities managing multiple product batches daily. Investment in a grain color sorter dramatically improves return on processing equipment because facilities achieve substantially higher daily output volumes. Processing speed improvements from the grain color sorter allow facilities to accept larger client orders confidently, expanding market opportunities. The grain color sorter's consistent throughput enables predictable production scheduling, facilitating better coordination with shipping and storage operations.
Cost Reduction and Quality Assurance

Cost Reduction and Quality Assurance

Implementing a grain color sorter significantly reduces operational expenses by eliminating labor-intensive manual sorting procedures requiring extensive employee oversight. The grain color sorter automatically achieves quality consistency that reduces waste and transforms marginal grain batches into sellable products, maximizing profitability. Grain color sorter technology removes contamination before packaging, preventing costly product recalls and regulatory compliance issues that damage brand reputation. The grain color sorter reduces insurance expenses and liability exposure by ensuring batch safety before customer distribution. Investment in the grain color sorter generates positive return on investment within months through waste reduction, efficiency gains, and premium-grade product premiums. The grain color sorter decreases quality-related customer complaints, eliminating expensive customer service burden and repeat shipments. Automated sorting through the grain color sorter ensures consistent product quality that strengthens customer relationships and increases repeat business. The grain color sorter allows facilities to maintain pricing competitiveness while improving profit margins simultaneously. Energy-efficient grain color sorter designs minimize operational expenses while maintaining sorting performance standards that manual alternatives cannot sustain consistently.

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

Copyright © 2026 Anhui Jiexun Optoelectronic Technology Co., Ltd. All rights reserved.  -  Privacy policy