Colour Sorter Machine Price Guide

All Categories

colour sorter machine price

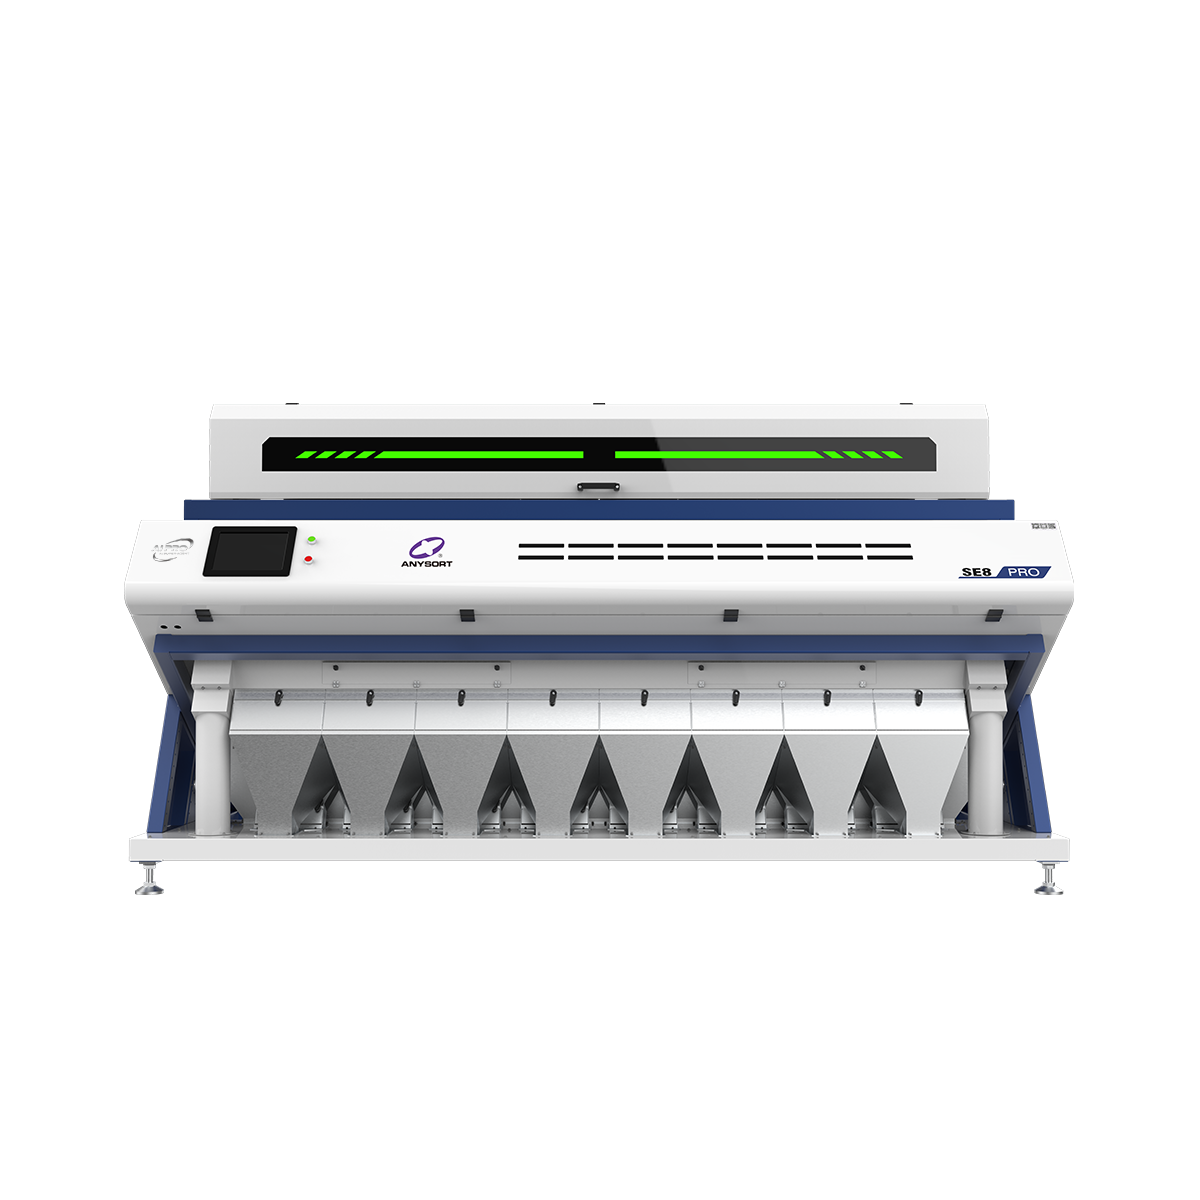
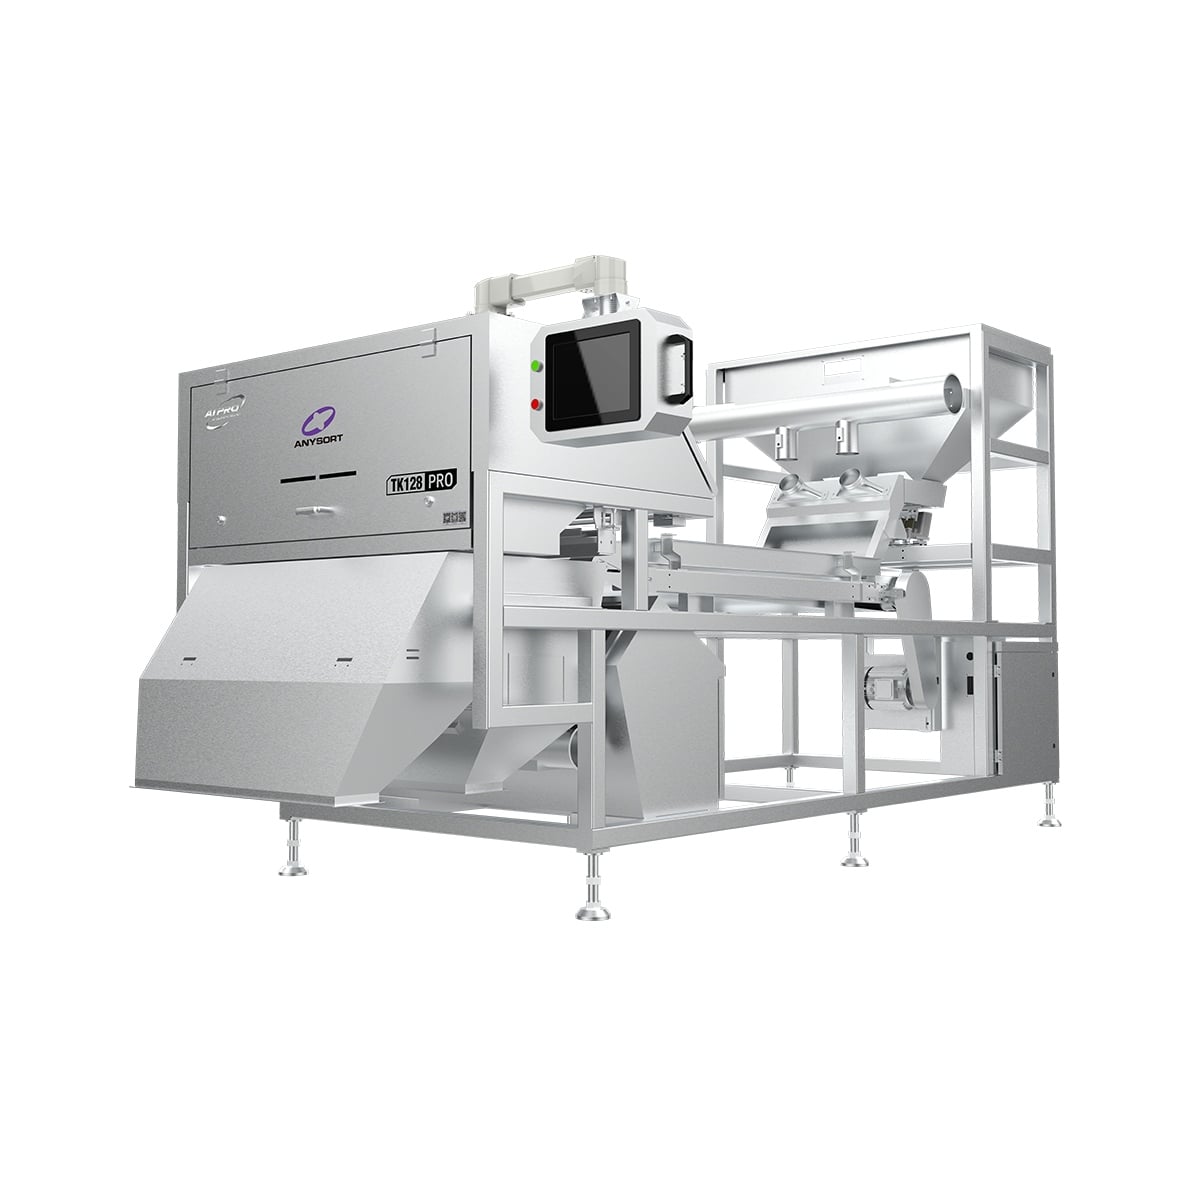
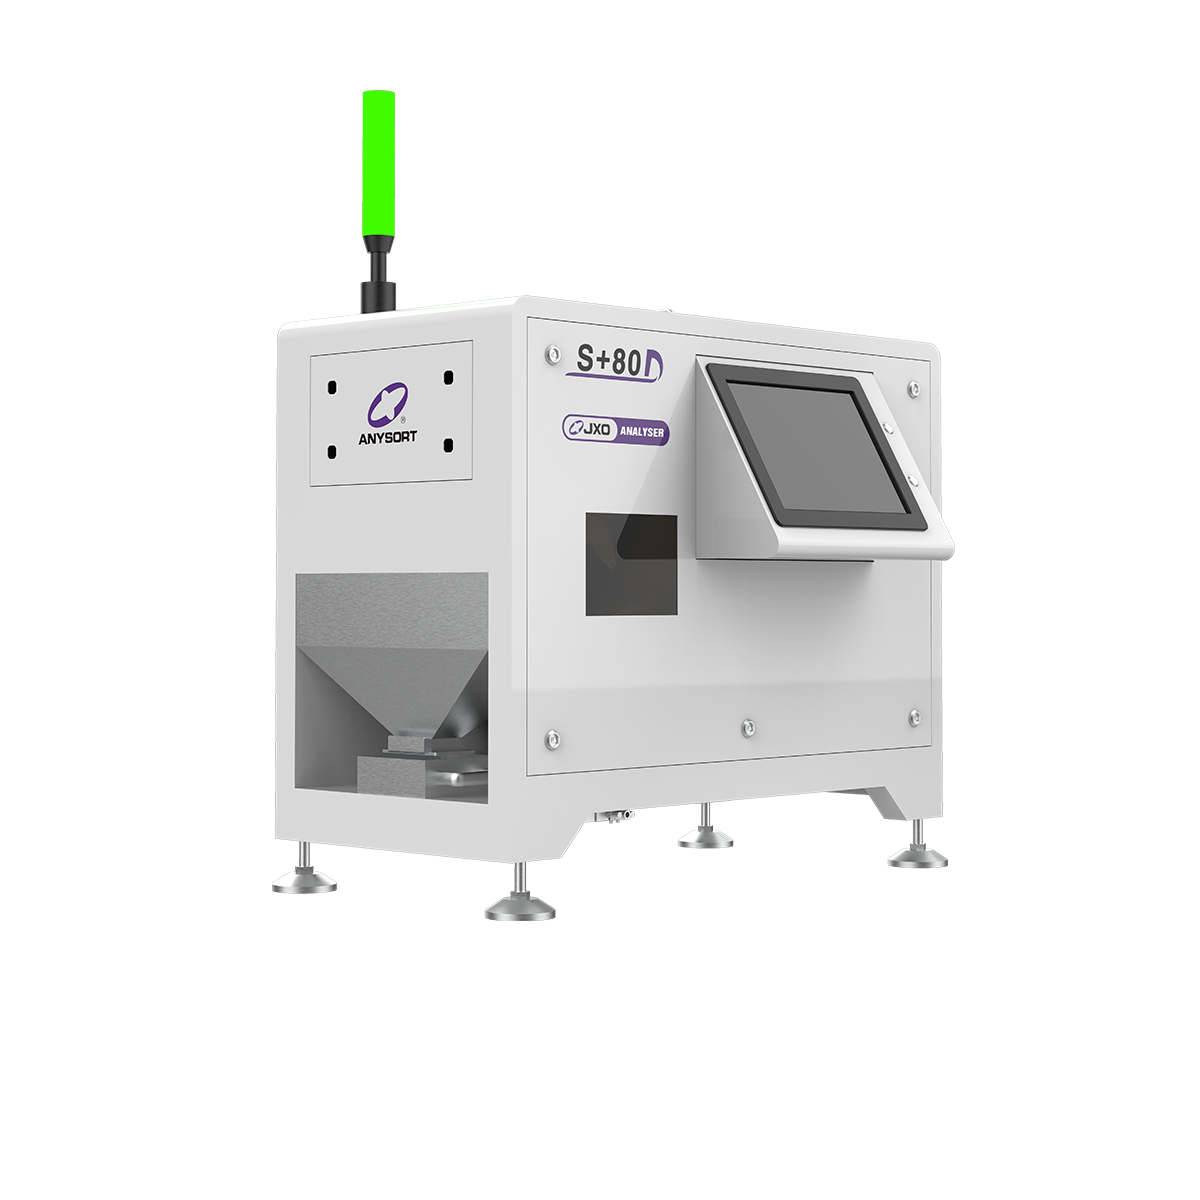
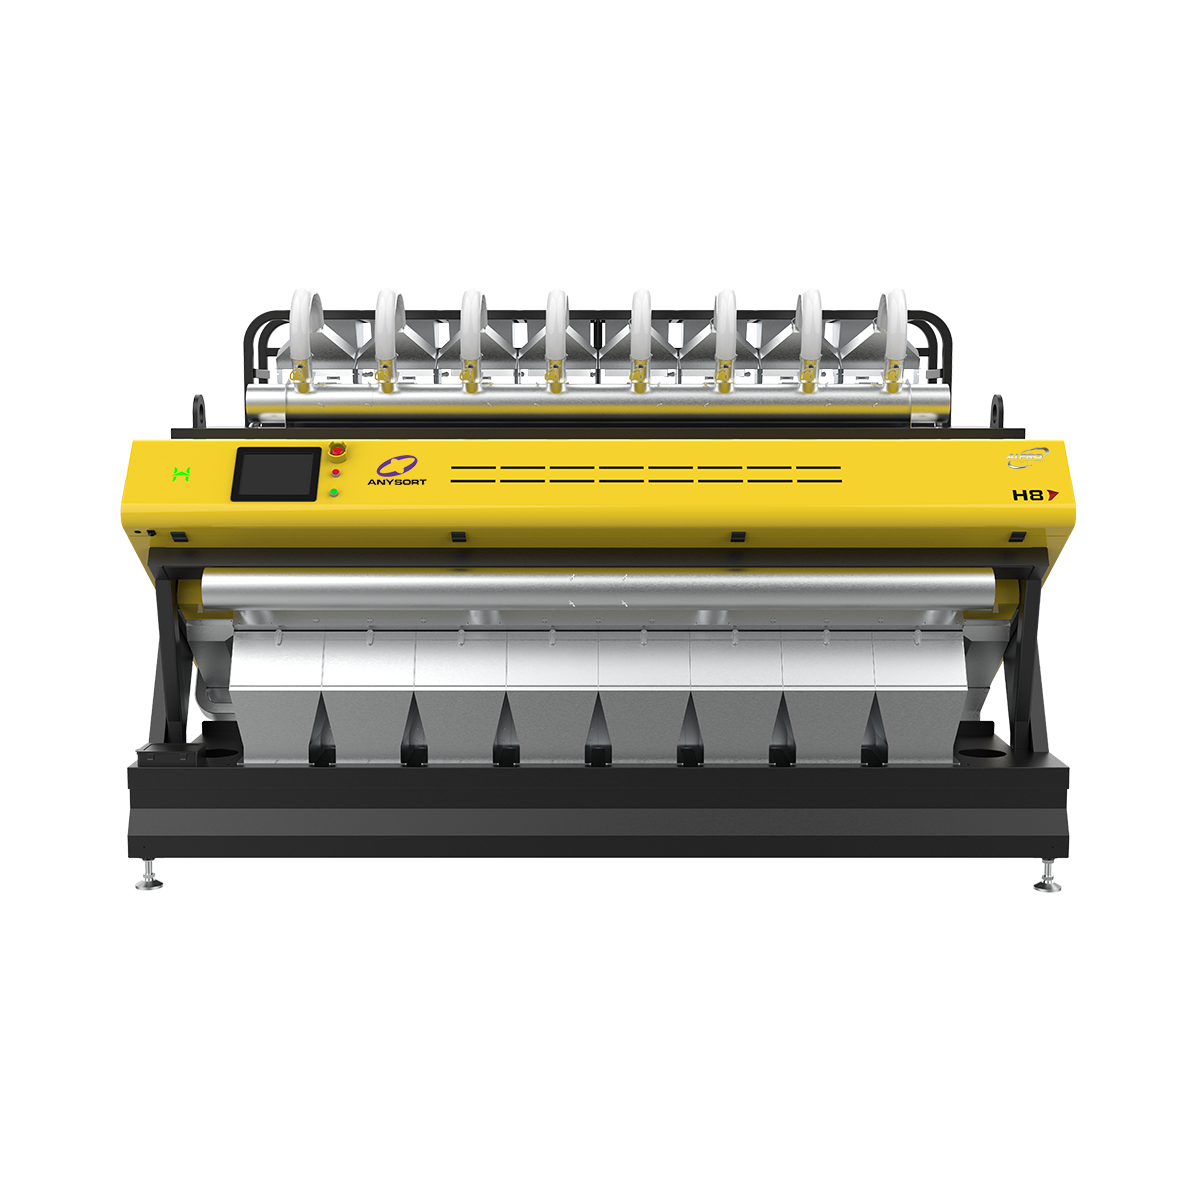
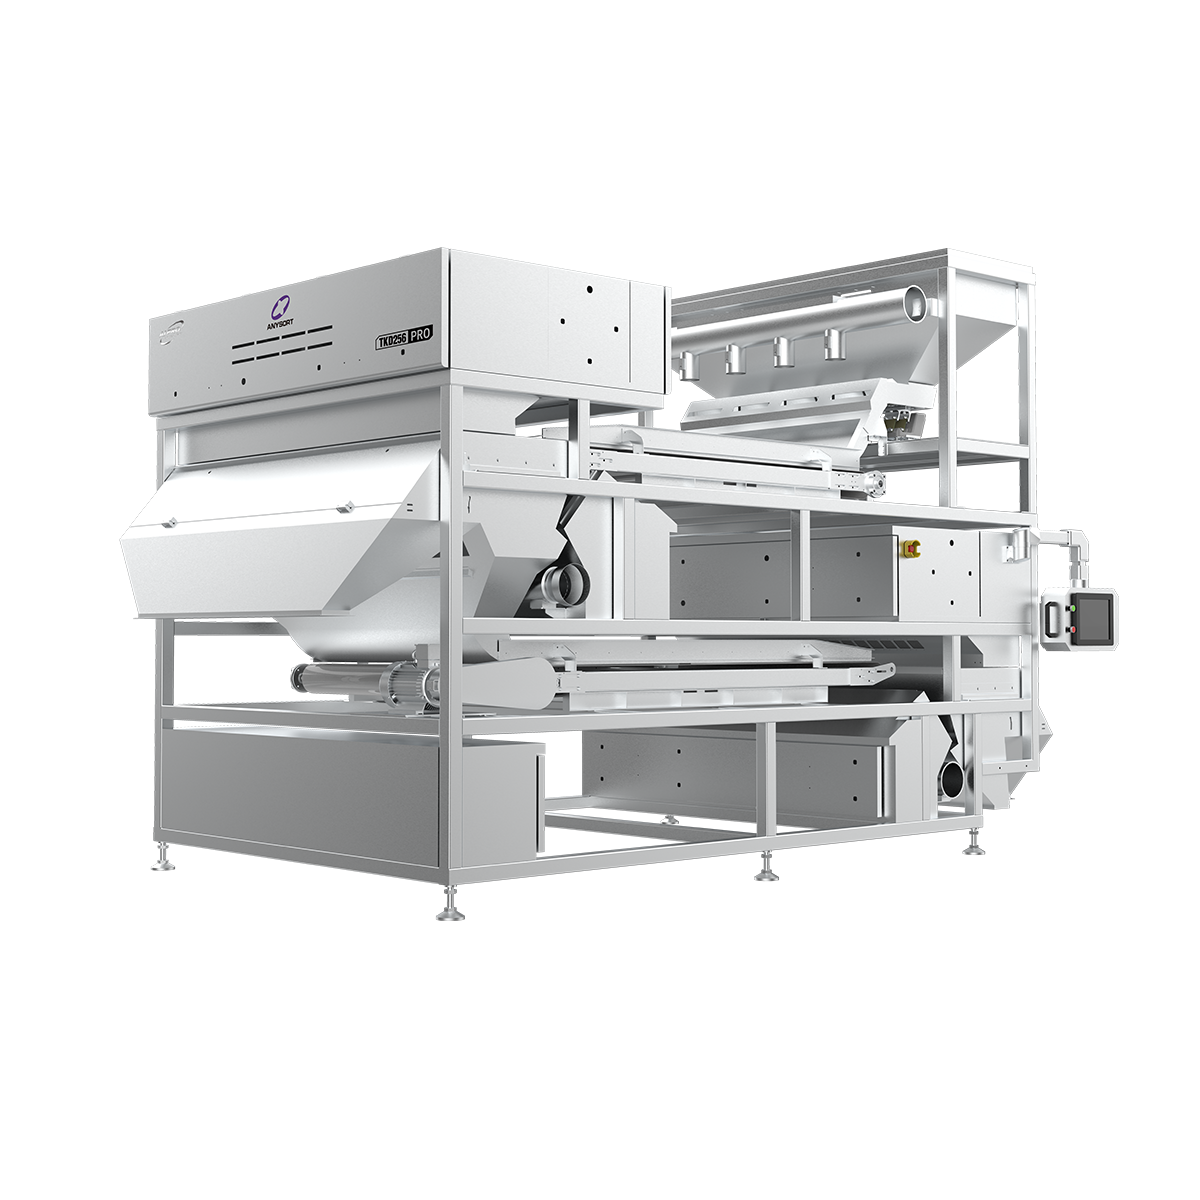
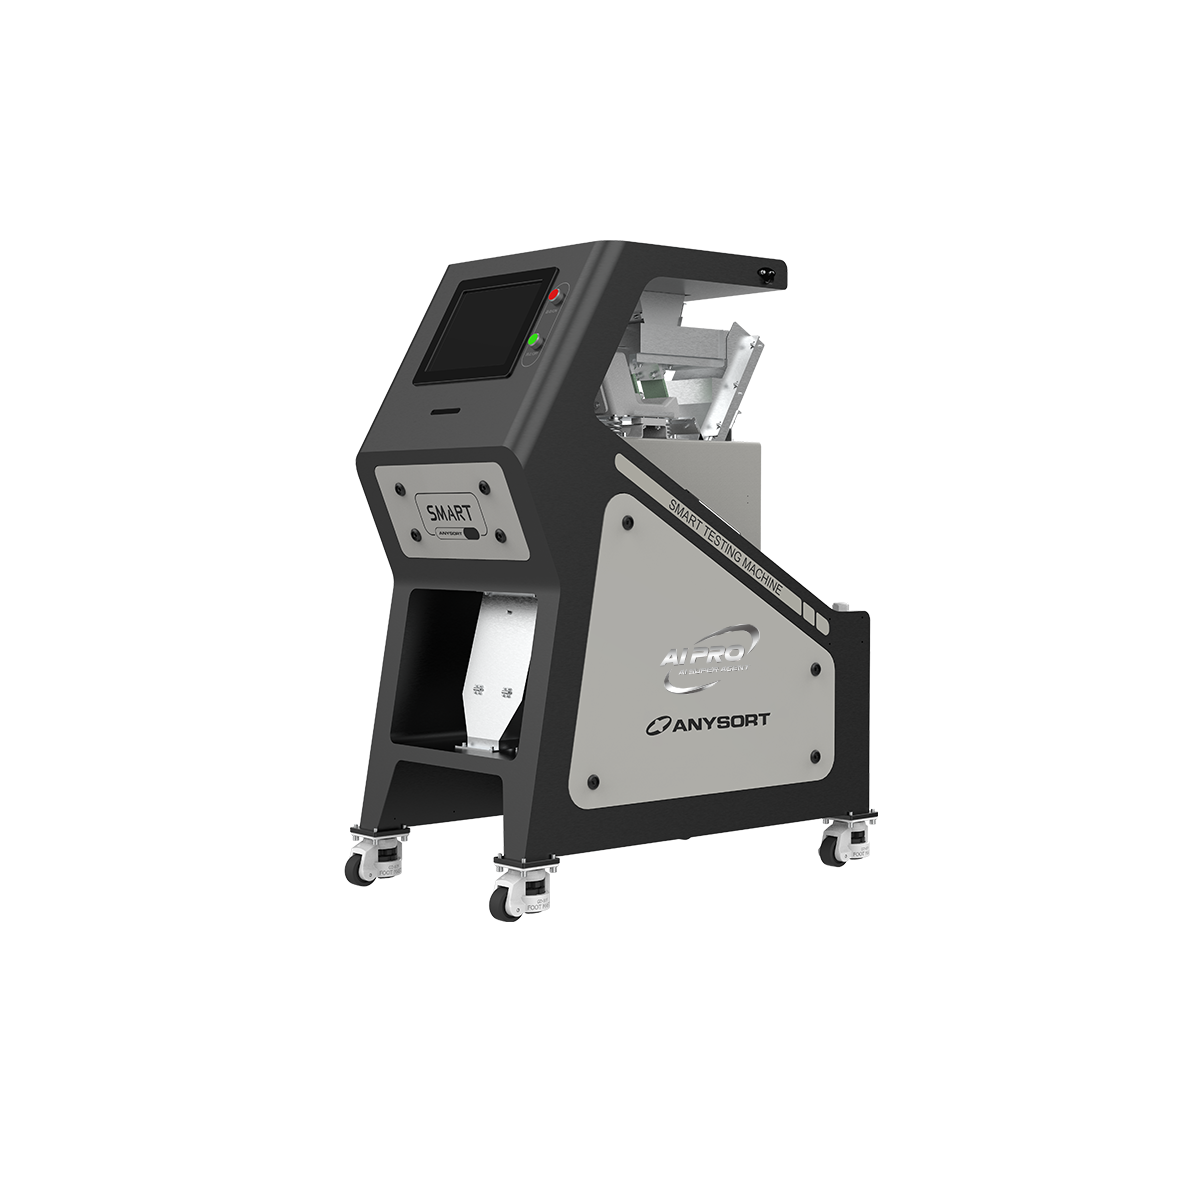
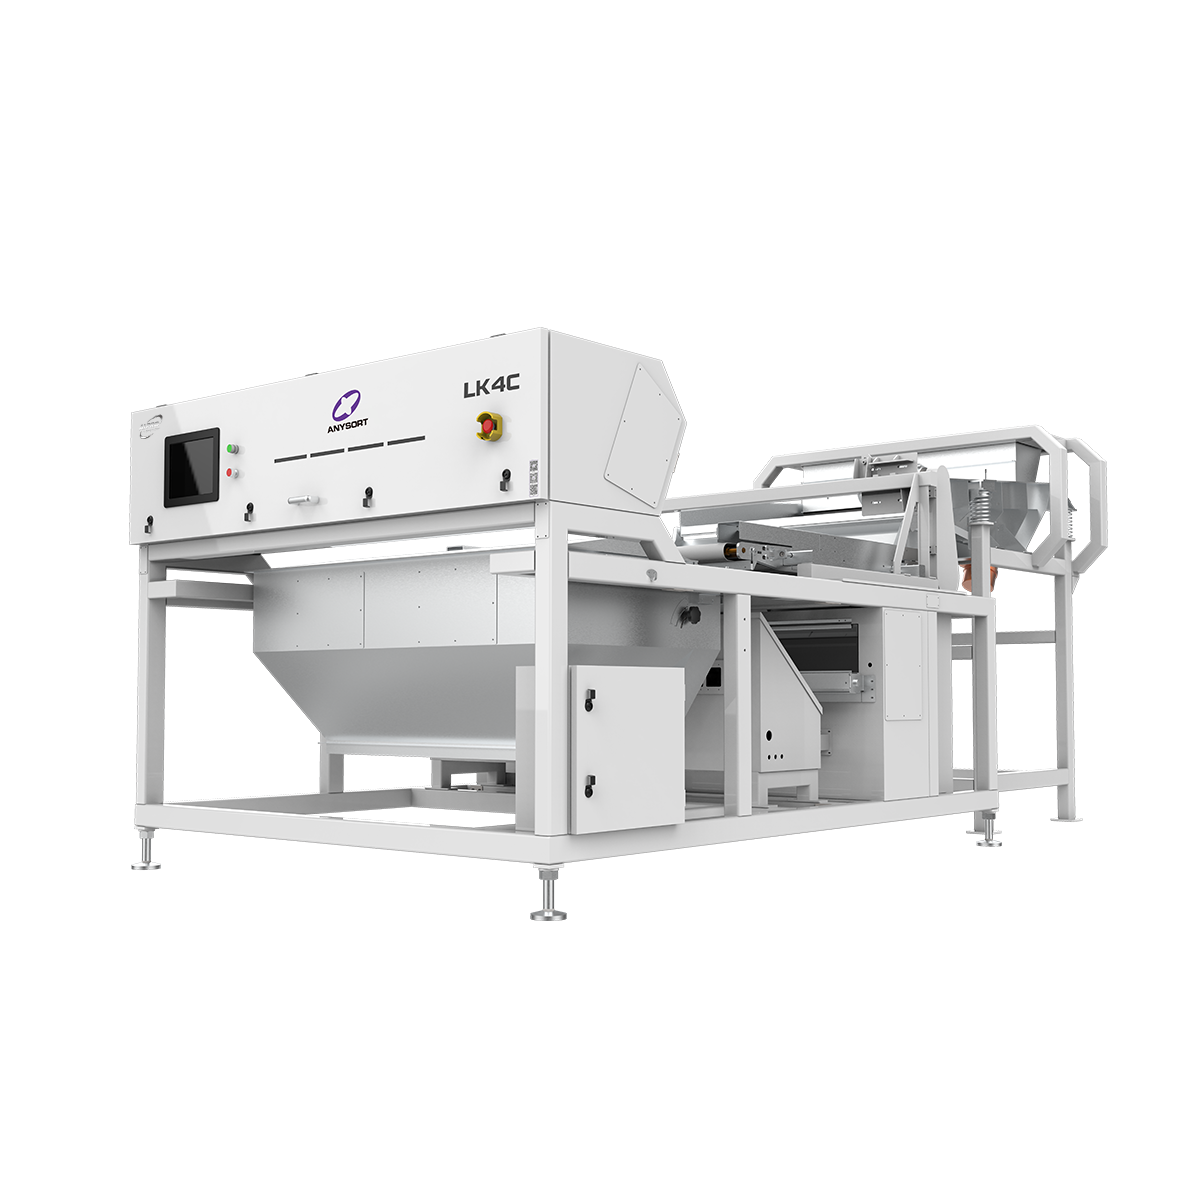
A colour sorter machine price represents an investment in advanced optical sorting technology designed to enhance product quality and operational efficiency. These machines use sophisticated camera systems and artificial intelligence to identify and separate materials based on color, size, and shape characteristics. Understanding colour sorter machine price is essential for businesses considering automation in food processing, recycling, agriculture, and mineral industries. Modern colour sorter machines integrate high-speed processors that analyze thousands of particles per second, delivering exceptional accuracy in sorting tasks. The colour sorter machine price varies based on capacity, sorting speed, and technological sophistication. Entry-level models start at more affordable rates, while premium systems with advanced features command higher investments. These machines feature multiple sensor types, including RGB and multispectral cameras, enabling precise detection of material variations invisible to human inspection. The colour sorter machine price reflects the engineering complexity and reliability built into each unit. Installation requires minimal space, and integration with existing production lines occurs seamlessly through standard interfaces. Applications span diverse sectors: rice and grain sorting, plastic recycling separation, mineral classification, and pharmaceutical quality control. The colour sorter machine price investment pays dividends through reduced manual labor, decreased product waste, and improved output consistency. Manufacturers worldwide recognize these machines as essential components of modern production facilities seeking competitive advantages in quality and efficiency standards.

New Product Recommendations

Investing in a colour sorter machine price solution delivers substantial operational and financial benefits for manufacturing enterprises. The primary advantage centers on accuracy—these machines achieve sorting precision exceeding 99.9 percent, eliminating defective products that manual inspection might miss. This translates directly into enhanced product quality and reduced customer complaints, strengthening brand reputation. Cost reduction emerges as another compelling reason to evaluate colour sorter machine price options. By automating repetitive sorting tasks, businesses dramatically decrease labor expenses while maintaining consistent output quality. Employees transition from monotonous manual work to higher-value roles, improving workplace satisfaction and reducing turnover rates. The colour sorter machine price investment quickly recovers through reduced operational costs and increased productivity. Speed represents a transformative advantage. Modern colour sorters process materials at rates reaching 200 tons per hour, vastly outpacing human capability. This acceleration enables businesses to expand production capacity without proportional increases in facility size or staffing requirements. Understanding colour sorter machine price becomes crucial when calculating return-on-investment timelines. Contamination prevention constitutes another critical benefit. Colour sorter technology removes foreign materials, allergens, and defective items that pose safety risks. This compliance advantage proves invaluable in food processing and pharmaceutical industries where regulatory standards demand absolute purity. Operational flexibility improves significantly with colour sorter machines. Programmable sorting parameters accommodate diverse product types and quality standards. Facilities process multiple product varieties on single equipment, maximizing resource utilization. When evaluating colour sorter machine price, businesses gain comprehensive solutions adaptable to evolving market demands and product specifications.

Latest News

How can rice color sorters improve grain quality?

08

Aug

How can rice color sorters improve grain quality?

Rice color sorters represent a transformative technology in modern grain processing, fundamentally changing how producers maintain and enhance the quality of their rice output. By utilizing advanced optical scanning and artificial intelligence, a ric...
View More
How Does Nuts Sorter Technology Ensure Quality?

19

Aug

How Does Nuts Sorter Technology Ensure Quality?

The global nuts processing industry relies on precision and consistency to meet strict quality standards and regulatory requirements. A nuts sorter has become indispensable for processors seeking to eliminate defects, contaminants, and substandard pr...
View More
How does optical sorting technology detect defective rice grains?

22

Aug

How does optical sorting technology detect defective rice grains?

Modern rice processing demands precision and consistency, which is why understanding the detection mechanisms behind advanced equipment has become essential for producers. A rice color sorter represents one of the most significant technological break...
View More
Top AI Color Sorter Manufacturers in China (2026)

30

Aug

Top AI Color Sorter Manufacturers in China (2026)

The global demand for precision sorting technology has surged dramatically, with color sorter machine manufacturers in China leading innovation across agricultural and industrial sectors. Chinese color sorter machine manufacturers have established th...
View More

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

colour sorter machine price

Advanced Optical Technology for Superior Sorting Accuracy

Advanced Optical Technology for Superior Sorting Accuracy

Colour sorter machines employ cutting-edge optical systems with multiple high-resolution cameras capturing detailed product characteristics simultaneously. The colour sorter machine price reflects advanced imaging technology that delivers exceptional sorting accuracy. These systems analyze color gradients, surface defects, and dimensional variations with precision reaching 99.9 percent accuracy rates. Real-time processing enables instantaneous sorting decisions without production slowdowns. The investment in colour sorter machine price proves worthwhile when considering the dramatic reduction in defective products reaching customers. Agricultural processors benefit enormously from this technology, eliminating discolored grains and foreign materials that compromise product quality. Food manufacturers gain regulatory compliance assurance while maintaining premium product standards. The sophisticated algorithms embedded within these machines continuously improve through machine learning capabilities, adapting to subtle product variations automatically.
Rapid Processing Speed and Increased Production Capacity

Rapid Processing Speed and Increased Production Capacity

Modern colour sorter machines process materials at extraordinary speeds, typically handling 200 tons hourly or more depending on product type and machine specifications. Understanding colour sorter machine price becomes essential when calculating productivity improvements and capacity expansion potential. These high-speed capabilities eliminate production bottlenecks that plague manual sorting operations. Businesses achieve remarkable throughput increases without expanding physical infrastructure proportionally. The colour sorter machine price investment enables companies to meet growing market demands while maintaining consistent quality standards. Manufacturing facilities experience significant competitive advantages through accelerated production timelines. Recycling operations particularly benefit from rapid processing speeds, handling massive material volumes efficiently. Mineral processing industries gain substantial advantages in extracting valuable materials while managing waste streams effectively. The investment translates into faster order fulfillment and improved customer satisfaction through reliable delivery schedules.
Cost Savings Through Labor Reduction and Operational Efficiency

Cost Savings Through Labor Reduction and Operational Efficiency

Colour sorter machine price investments generate substantial financial returns by minimizing manual labor requirements in repetitive sorting tasks. Facilities reassign workers to skilled positions requiring human judgment and problem-solving abilities. This organizational restructuring improves employee morale while reducing turnover and recruitment expenses significantly. The colour sorter machine price becomes financially justified through quantifiable labor cost reductions within twelve to twenty-four months. Energy efficiency in modern machines further reduces operational expenses compared to maintaining large manual sorting teams. Decreased product waste directly improves profit margins while reducing environmental impact. Quality improvements eliminate costly customer returns and refund expenses. The colour sorter machine price analysis reveals that comprehensive cost savings extend beyond direct labor reduction, encompassing waste reduction, energy efficiency, and enhanced product value. Companies gain competitive pricing advantages through improved operational efficiency, enabling market share growth.

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

Copyright © 2026 Anhui Jiexun Optoelectronic Technology Co., Ltd. All rights reserved.  -  Privacy policy