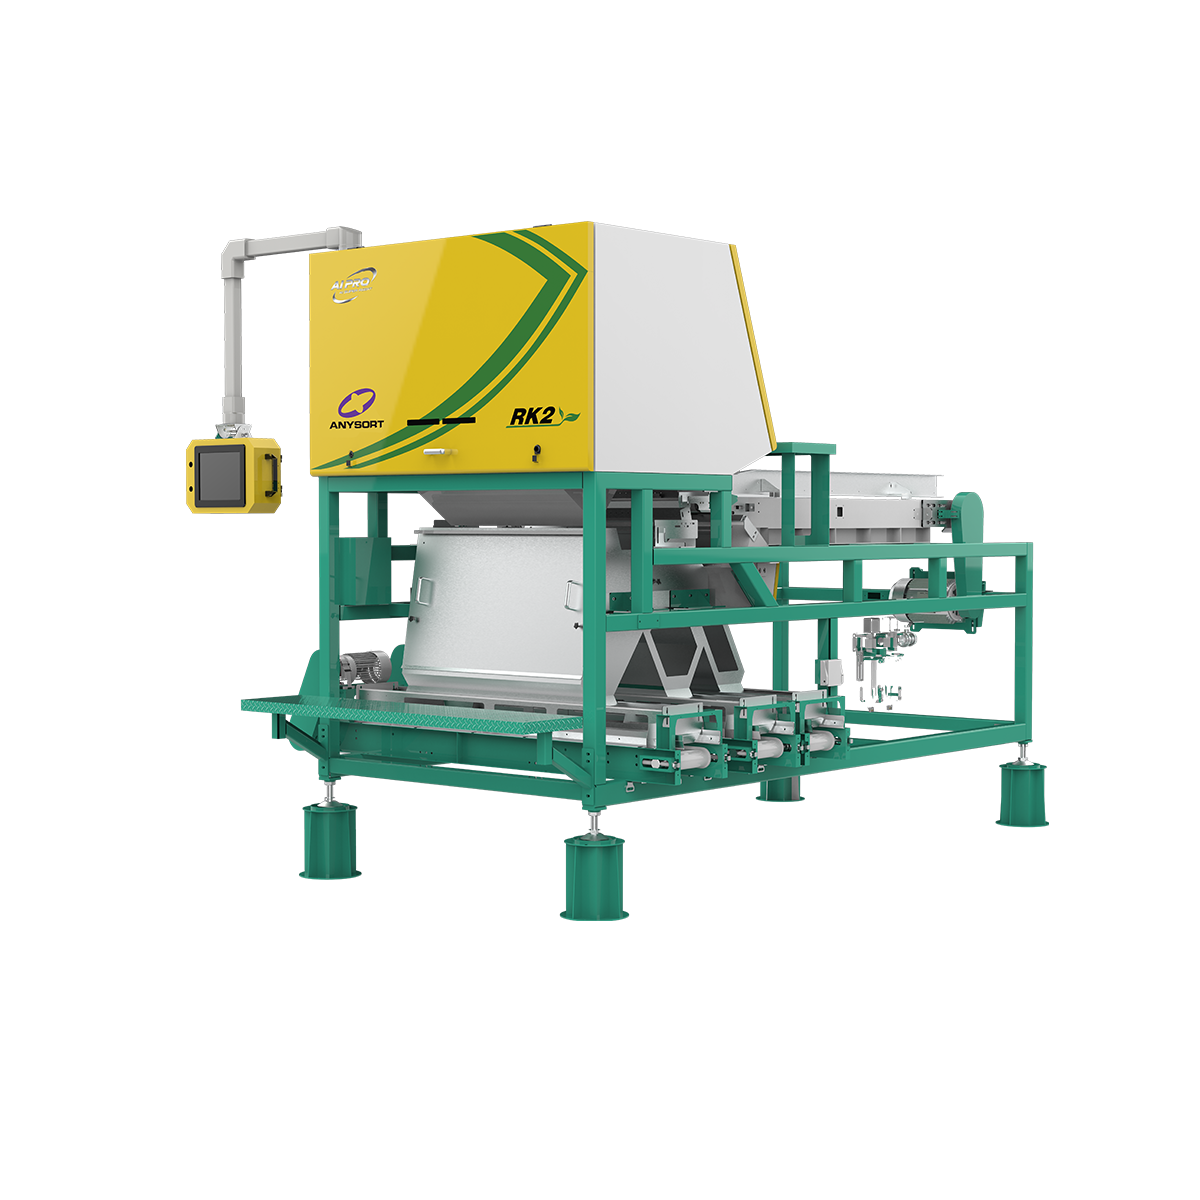
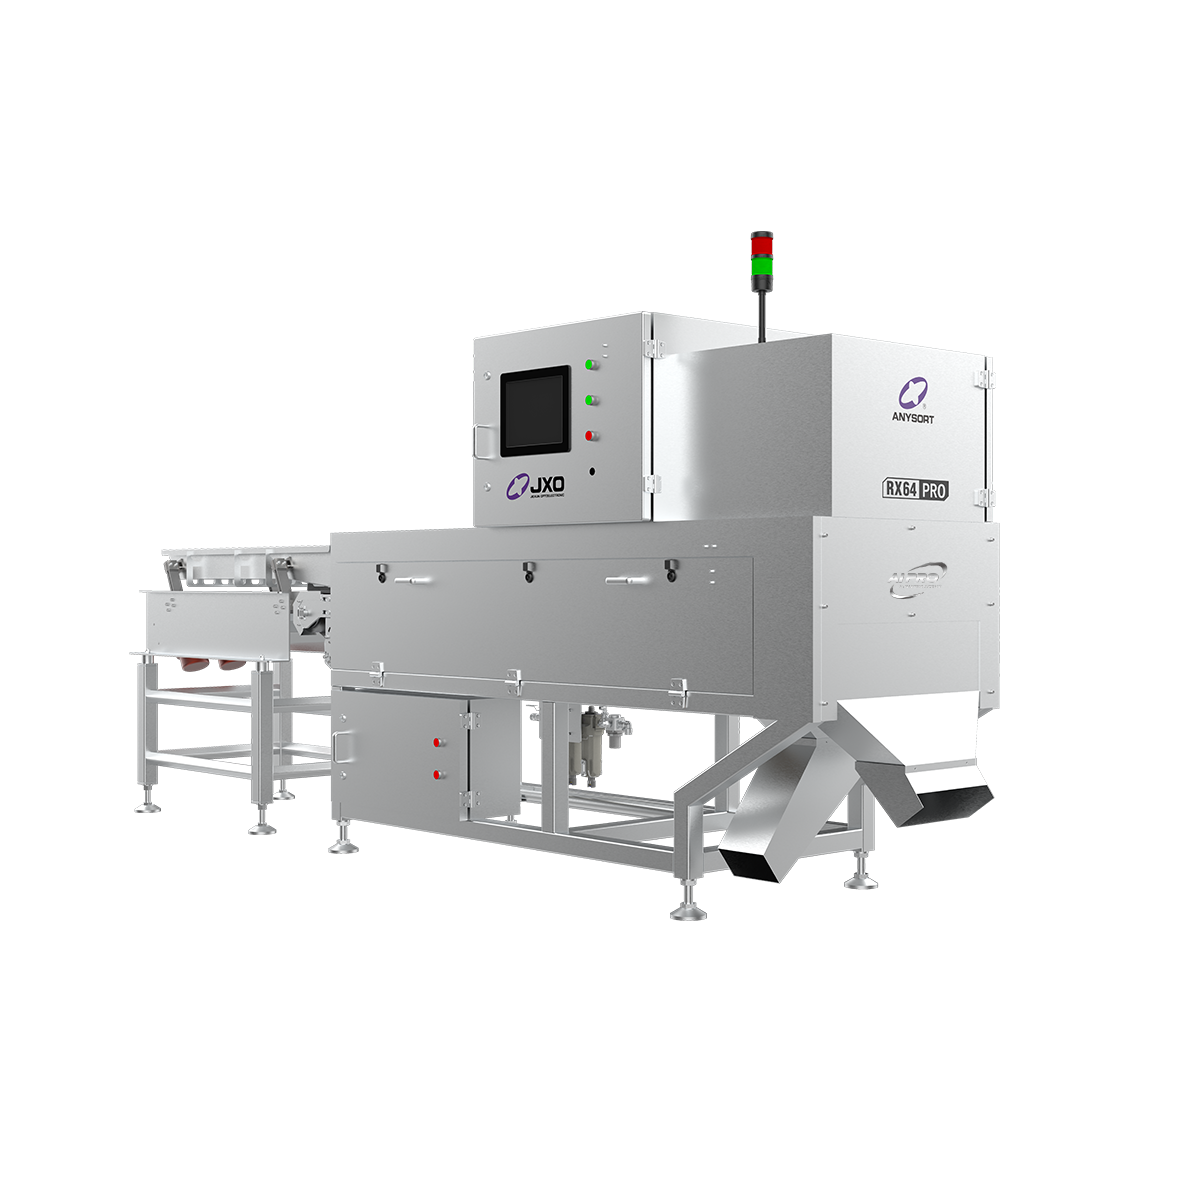
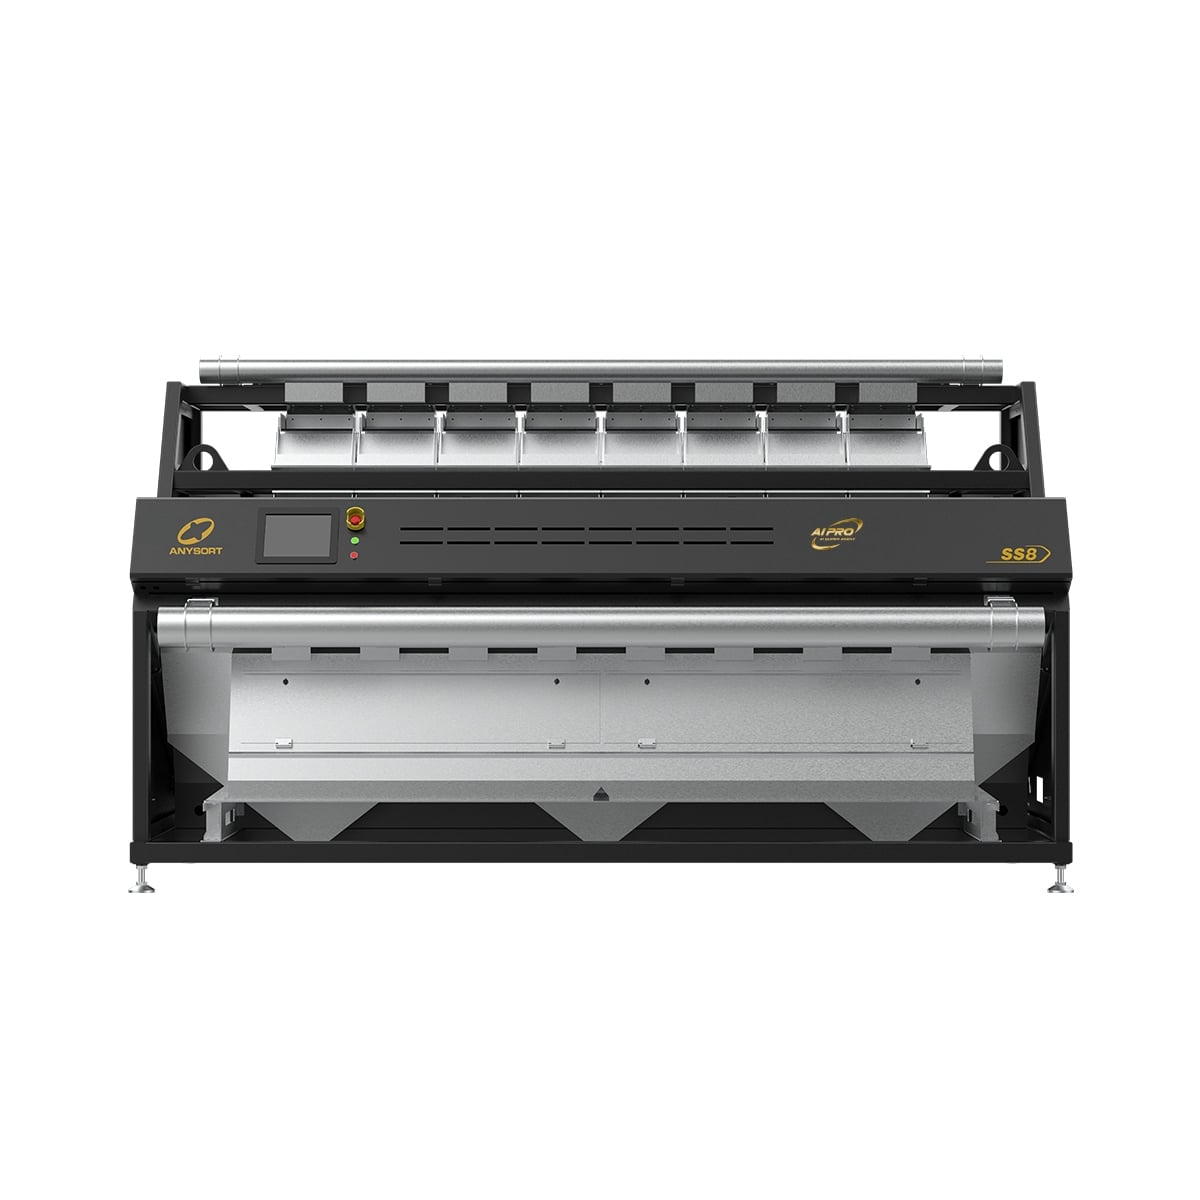
color sorting machines
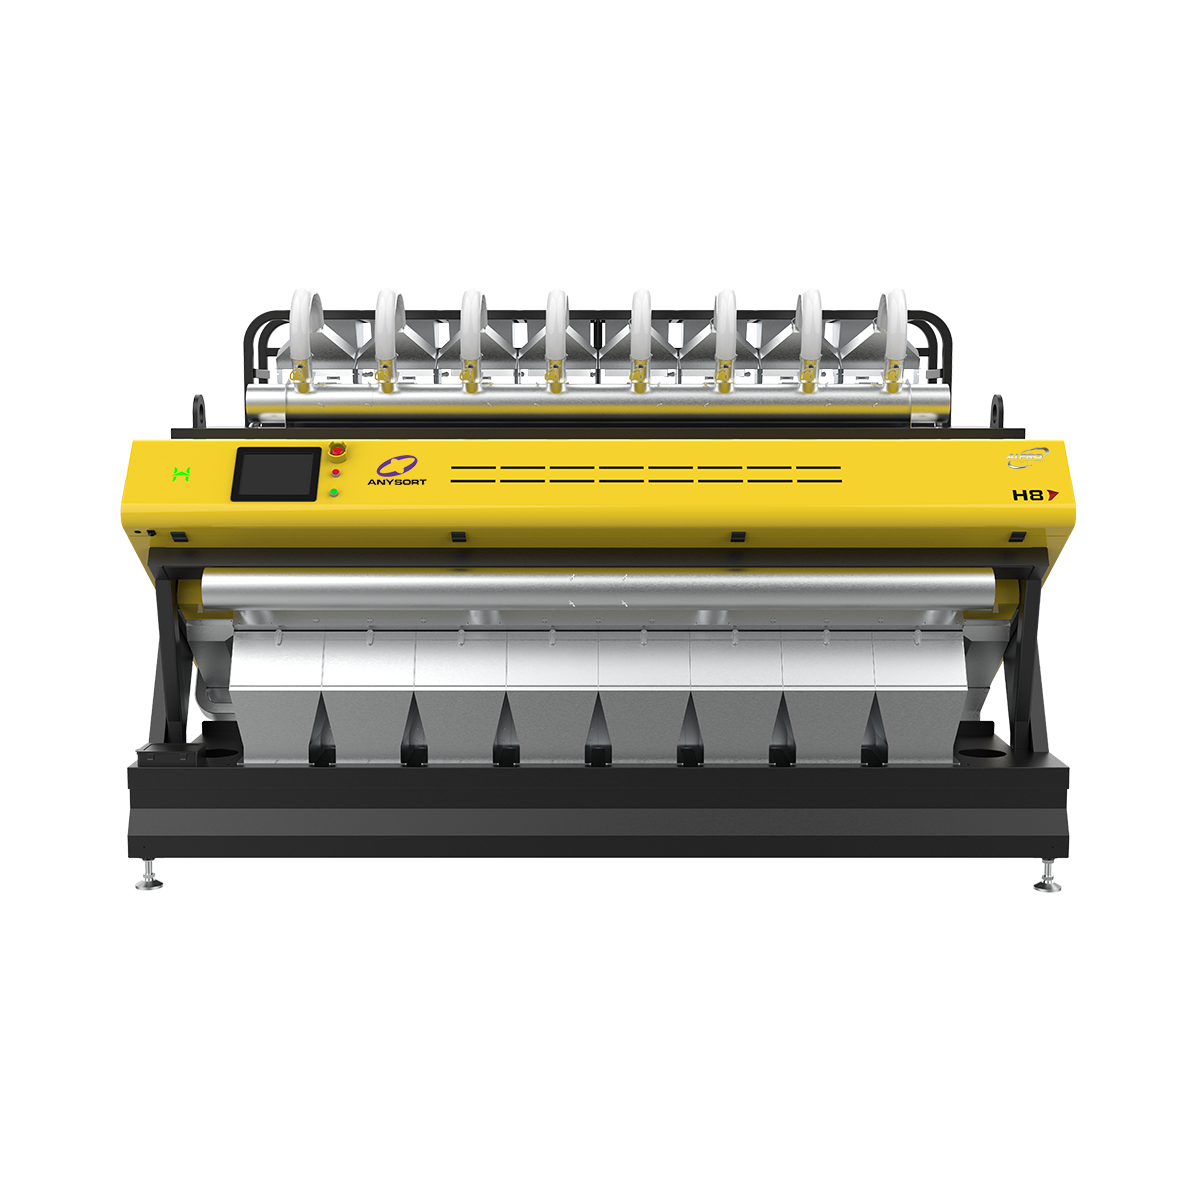
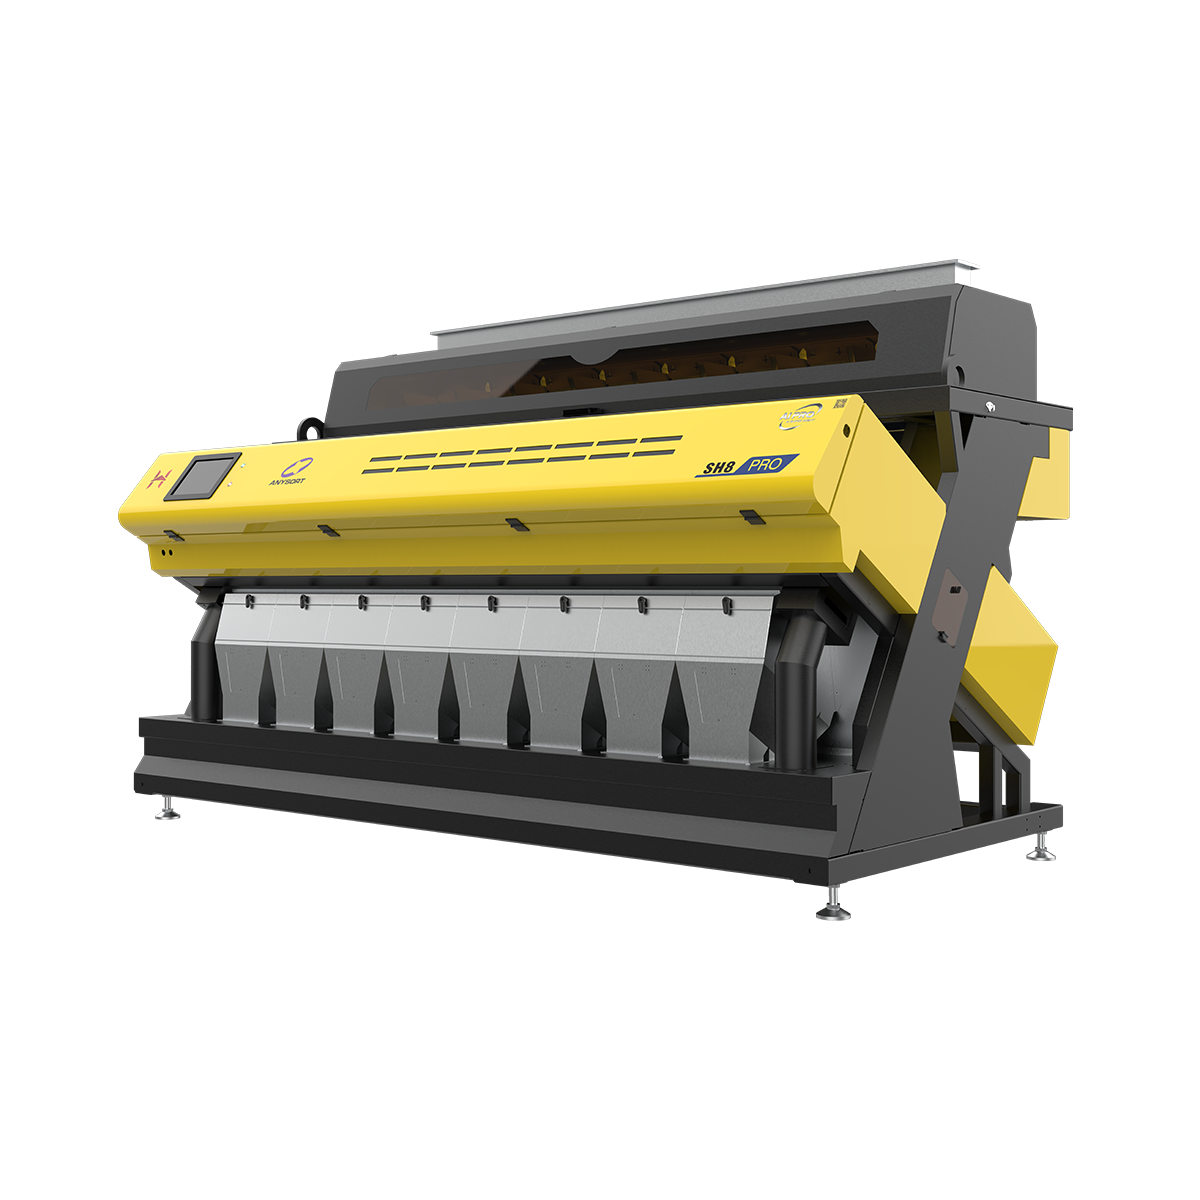
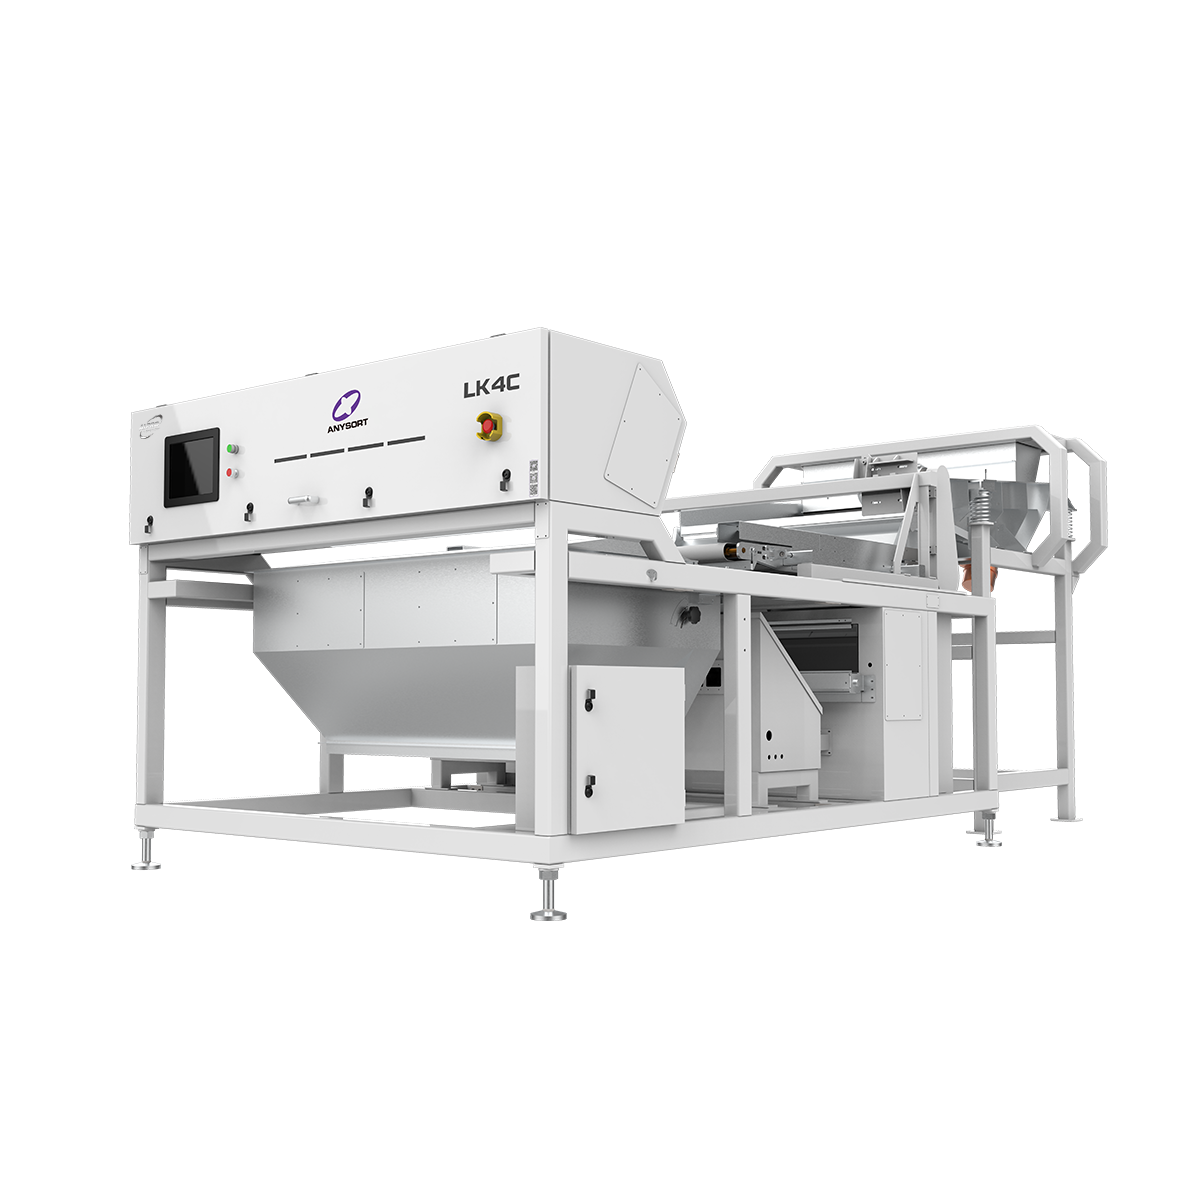
Color sorting machines represent advanced optical technology designed to automatically separate and grade materials based on color specifications. These sophisticated systems utilize high-resolution cameras and artificial intelligence to identify and categorize items with exceptional precision. Color sorting machines have become indispensable in numerous industries, from food processing to recycling and agriculture.
The primary function of color sorting machines is to remove defective, discolored, or foreign materials from production streams. Using LED lighting and specialized sensors, these machines scan each item individually, comparing colors against predefined standards. Color sorting machines process materials at impressive speeds, often handling thousands of items per minute without compromising accuracy.
Technologically, color sorting machines incorporate advanced features including multi-spectral imaging, machine learning algorithms, and pneumatic ejection systems. The systems employ sophisticated software that continuously adapts to variations in material properties and lighting conditions. Color sorting machines utilize real-time data processing to make instantaneous sorting decisions, ensuring consistent quality control throughout production cycles.
Applications for color sorting machines span diverse sectors. In the food industry, they inspect grains, nuts, coffee beans, and dried fruits. Agricultural producers use color sorting machines for seed cleaning and crop sorting. Recycling facilities deploy these machines for plastic and material separation. Manufacturing environments benefit from color sorting machines for quality assurance and defect detection, making them essential investment for companies prioritizing product excellence and operational efficiency.

 EN