cashew color sorter machine factories
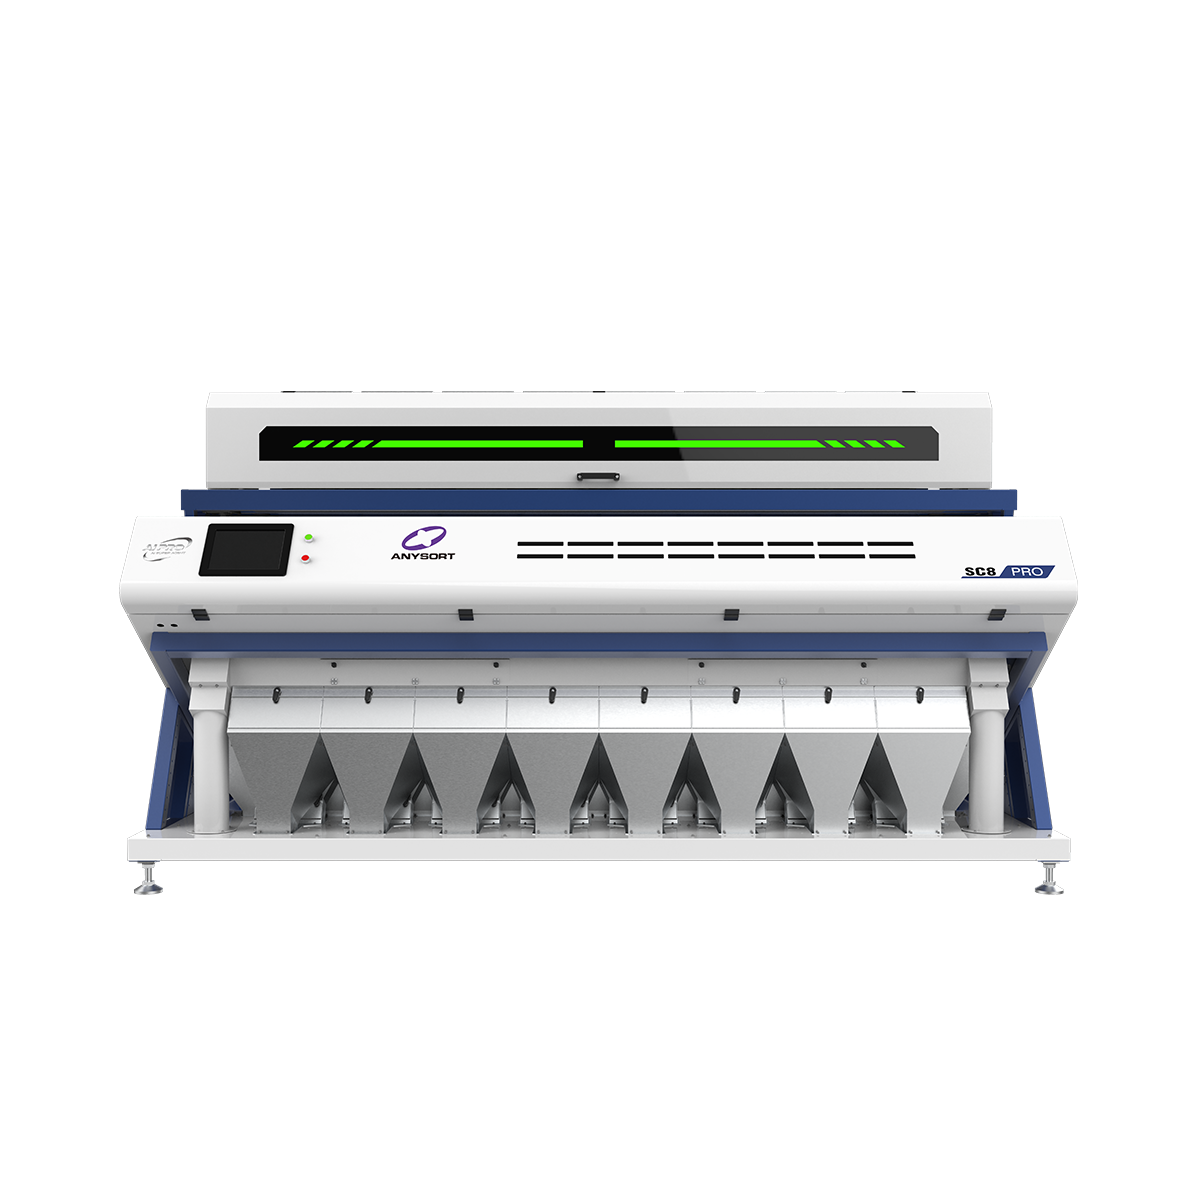
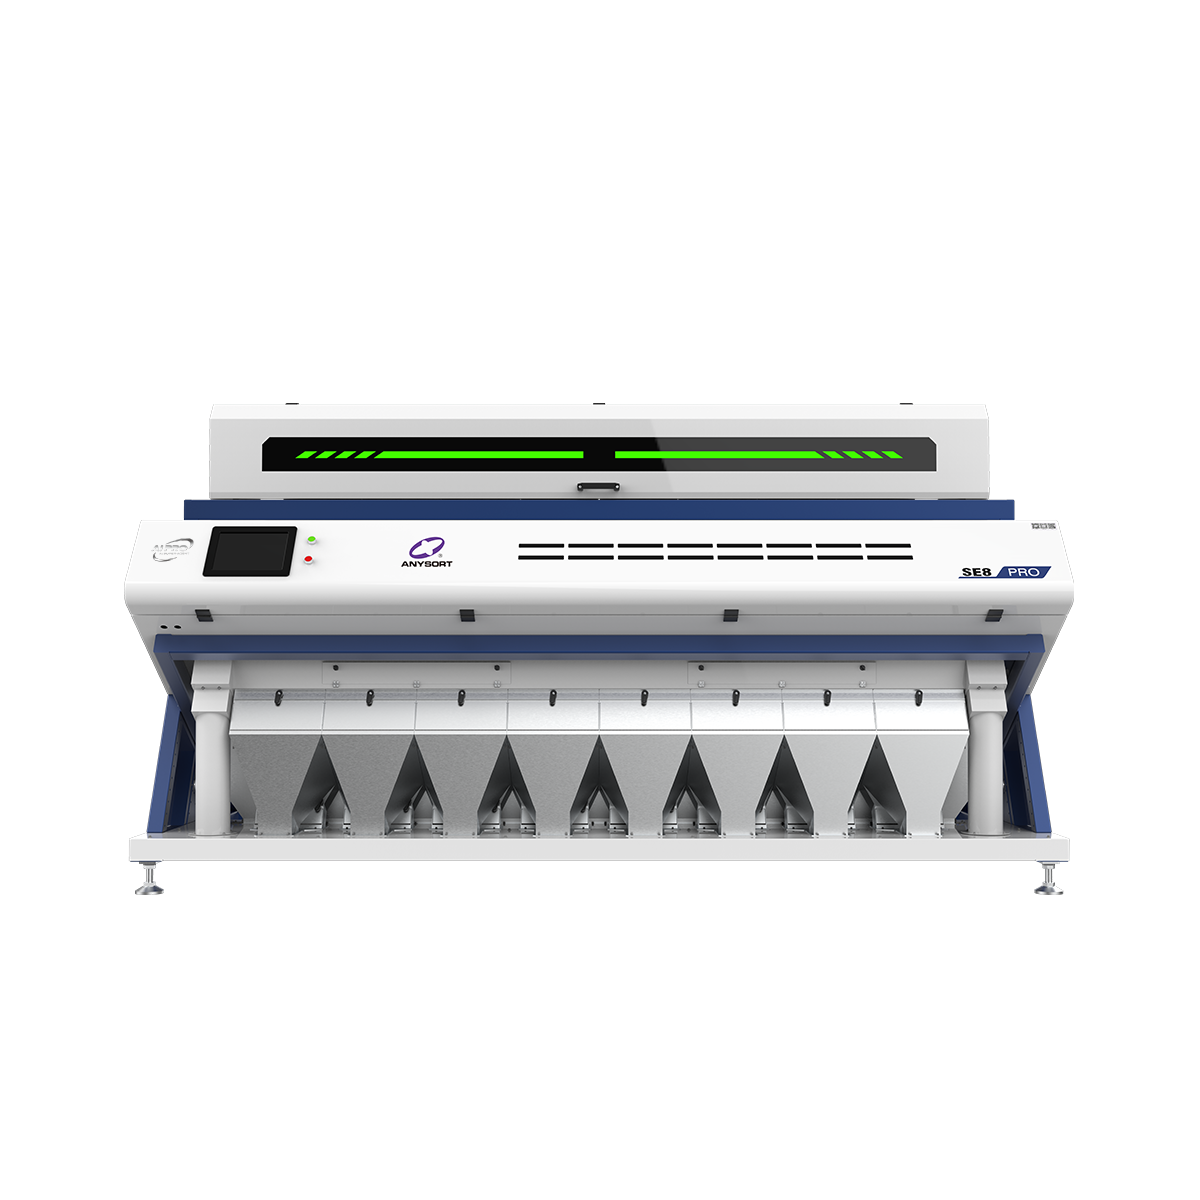
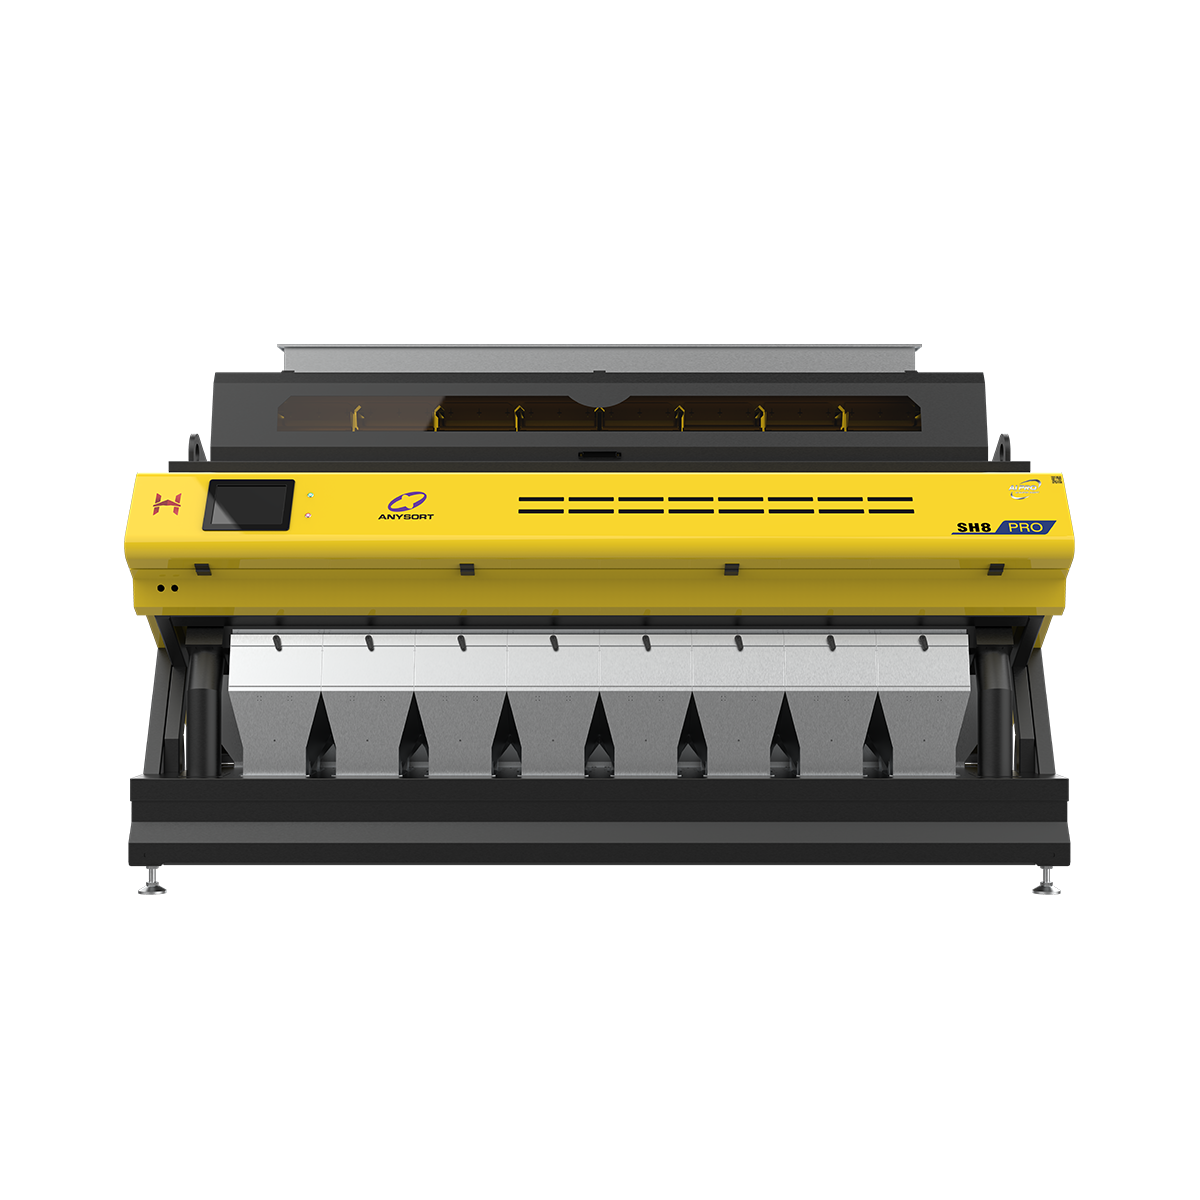
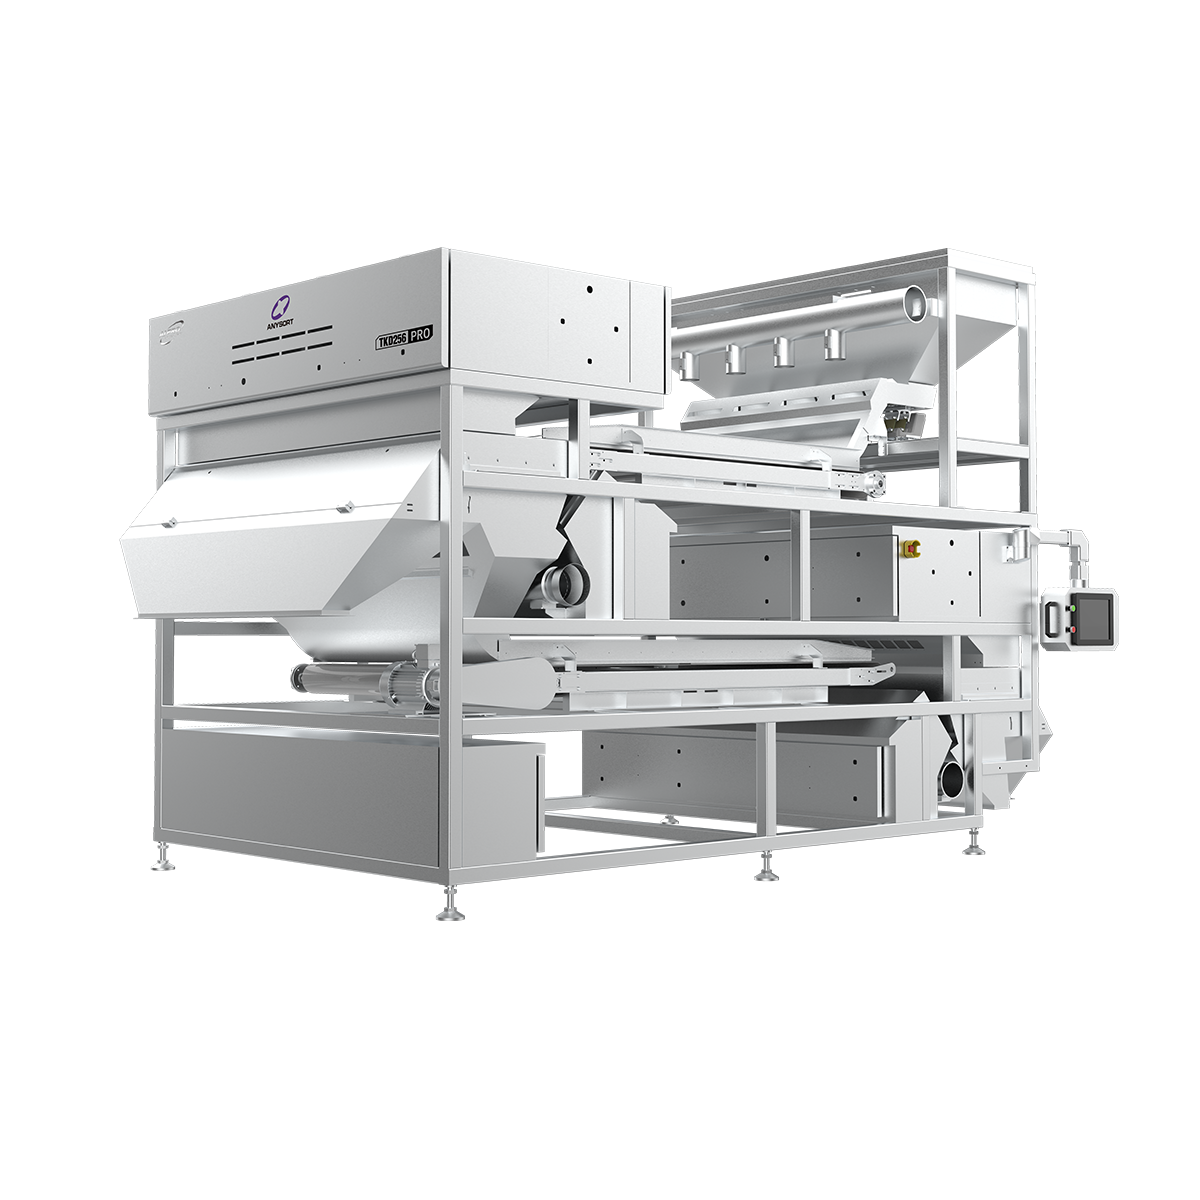
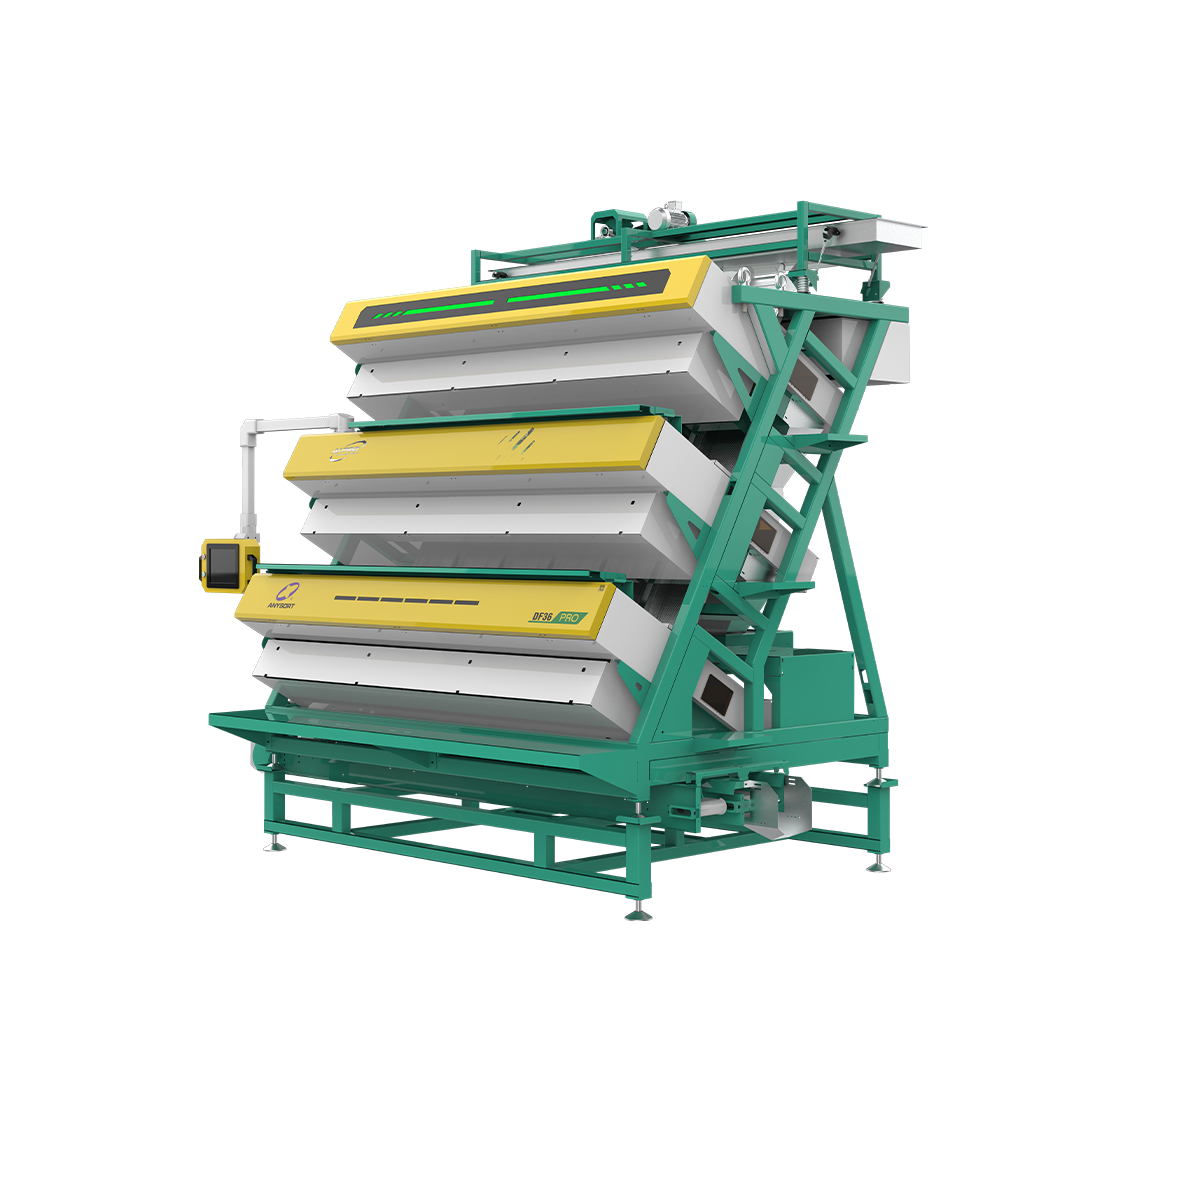
Cashew color sorter machine factories represent the pinnacle of modern agricultural processing technology, designed specifically to enhance the efficiency and quality of cashew nut sorting operations. These specialized facilities manufacture sophisticated color sorting equipment that utilizes advanced optical recognition systems to categorize cashews based on their color, size, and quality characteristics. The primary function of cashew color sorter machine factories is to produce reliable machinery that separates premium-grade cashews from lower-quality nuts with exceptional accuracy and speed. These machines operate using cutting-edge computer vision technology combined with artificial intelligence algorithms that identify subtle color variations invisible to the human eye. Cashew color sorter machine factories integrate multiple technological features including high-resolution cameras, intelligent sorting gates, and automated reject systems that work seamlessly together. The equipment produced by cashew color sorter machine factories can process thousands of cashews per hour while maintaining consistent quality standards. Applications span across commercial processing plants, export-oriented facilities, and integrated nut production complexes worldwide. The machinery produced addresses critical industry challenges including labor shortages, quality inconsistencies, and production bottlenecks. By choosing products from reputable cashew color sorter machine factories, operators gain access to equipment that significantly reduces processing time and waste while improving overall productivity and profitability.

 EN