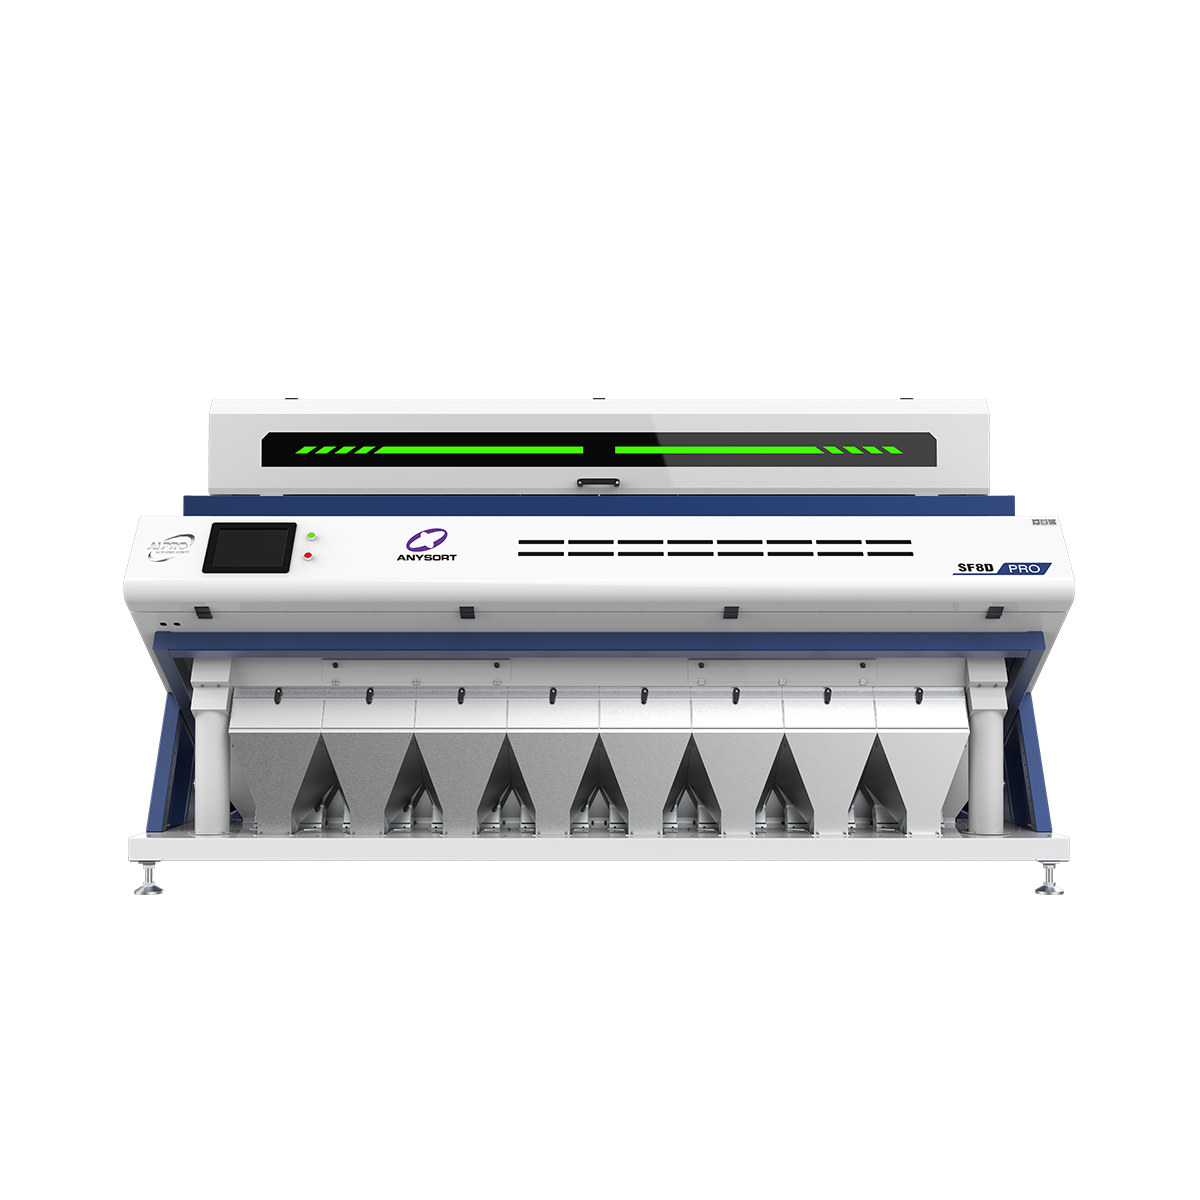
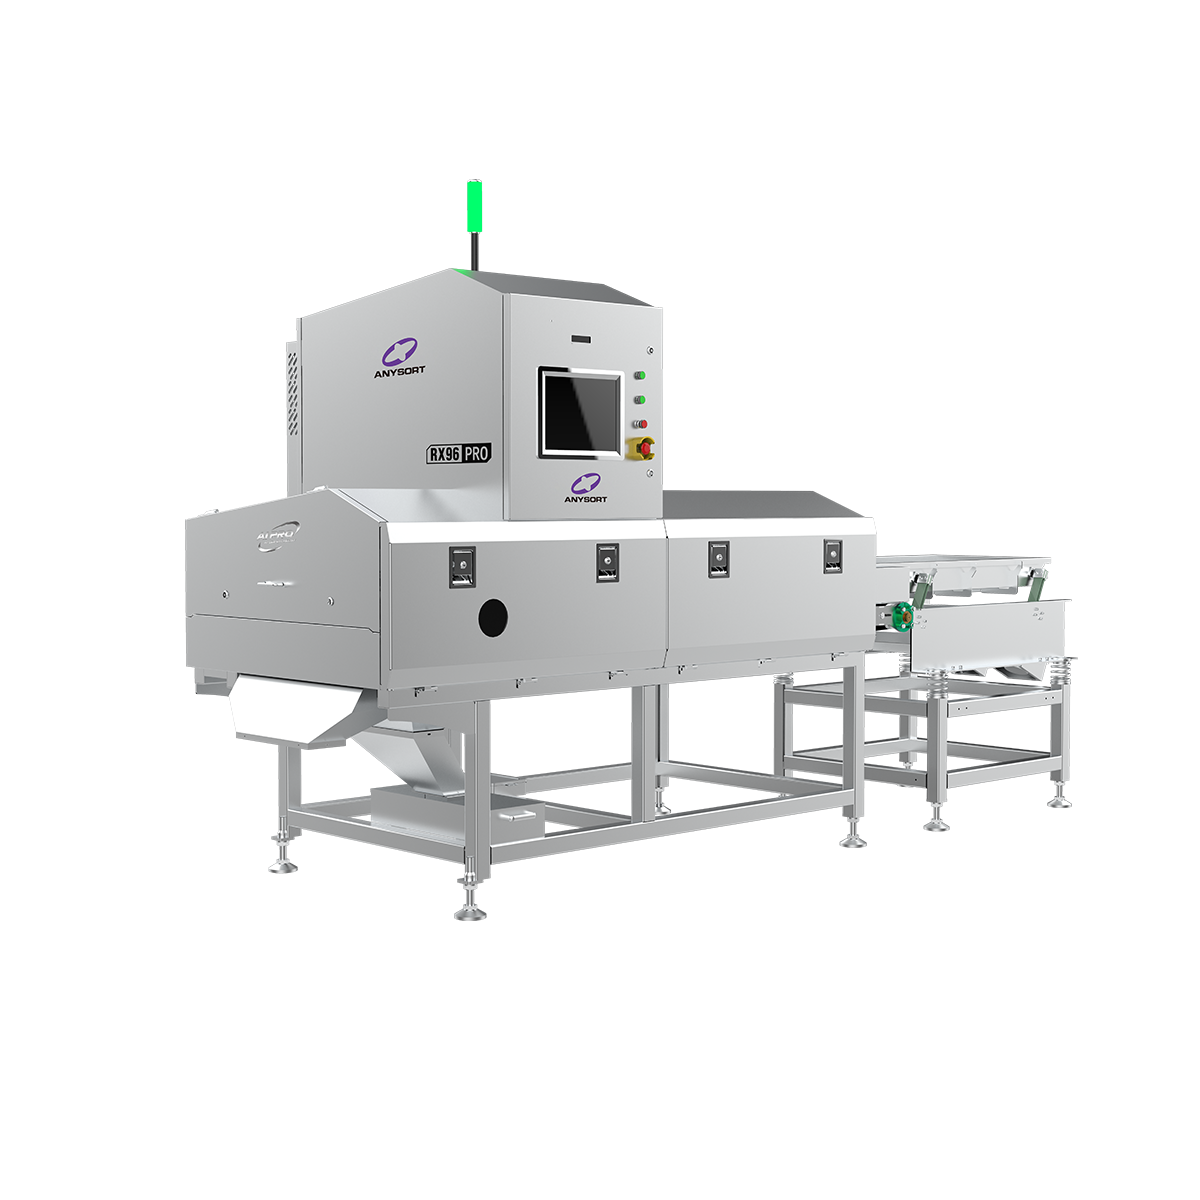
color sorter machine manufacturer
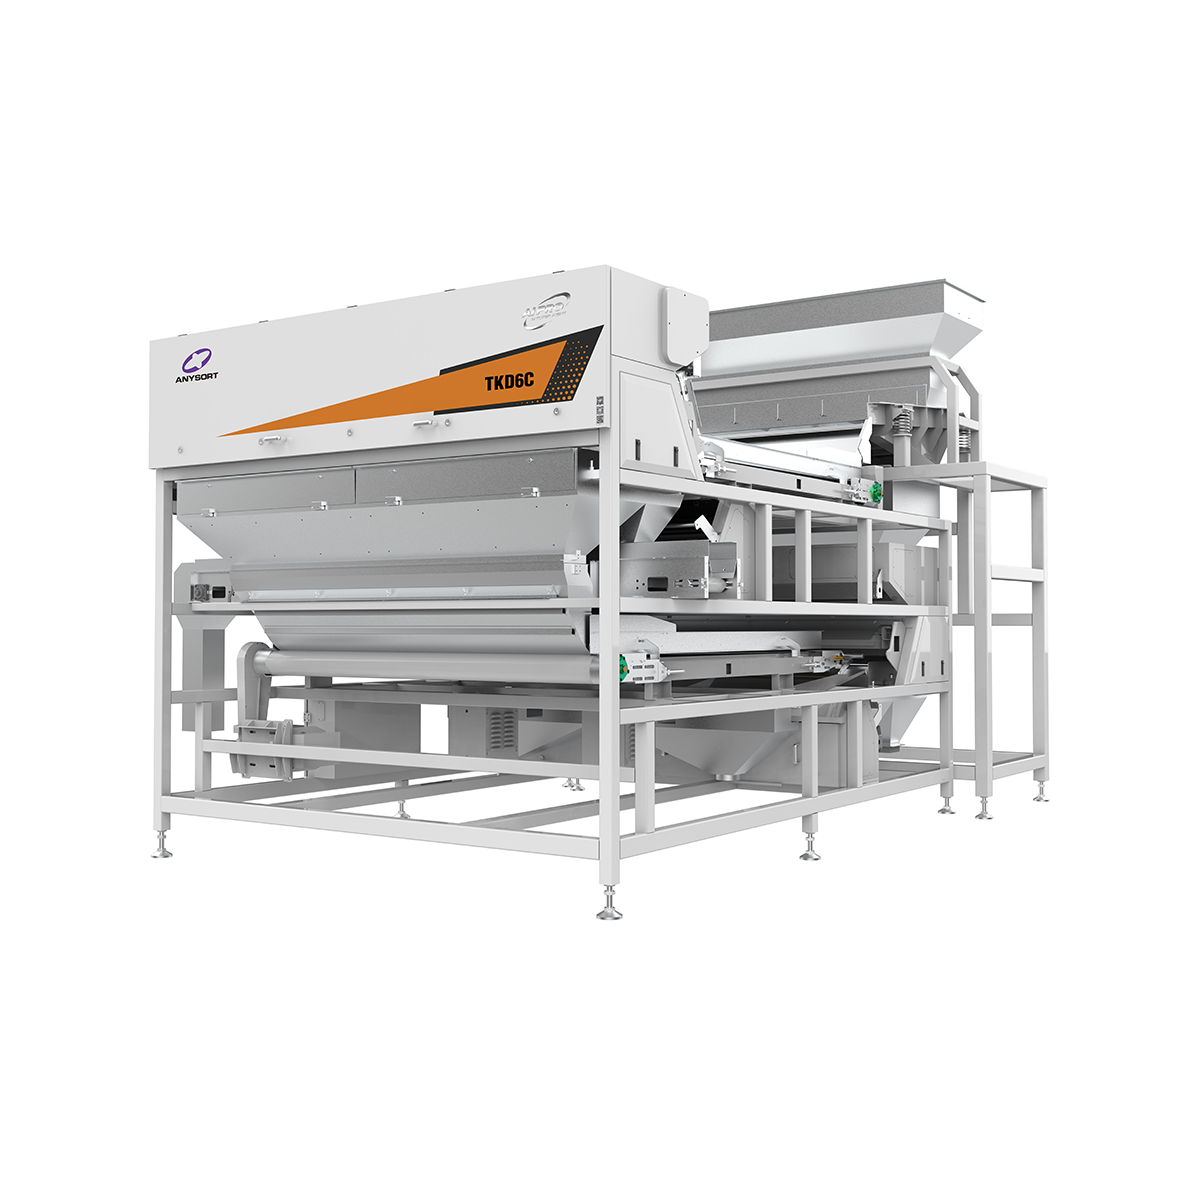
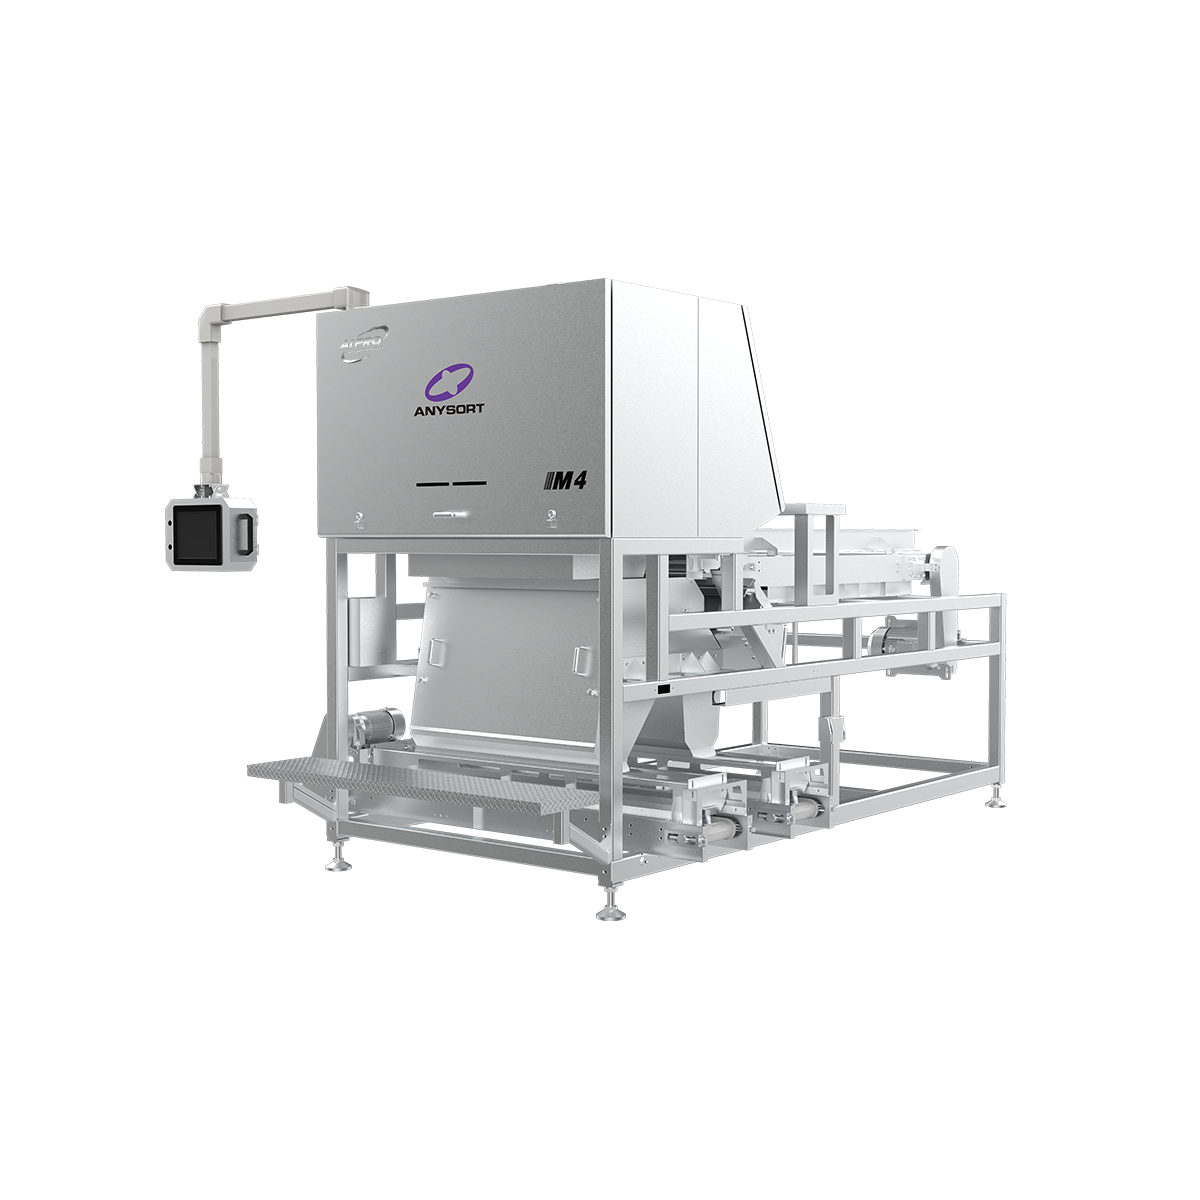
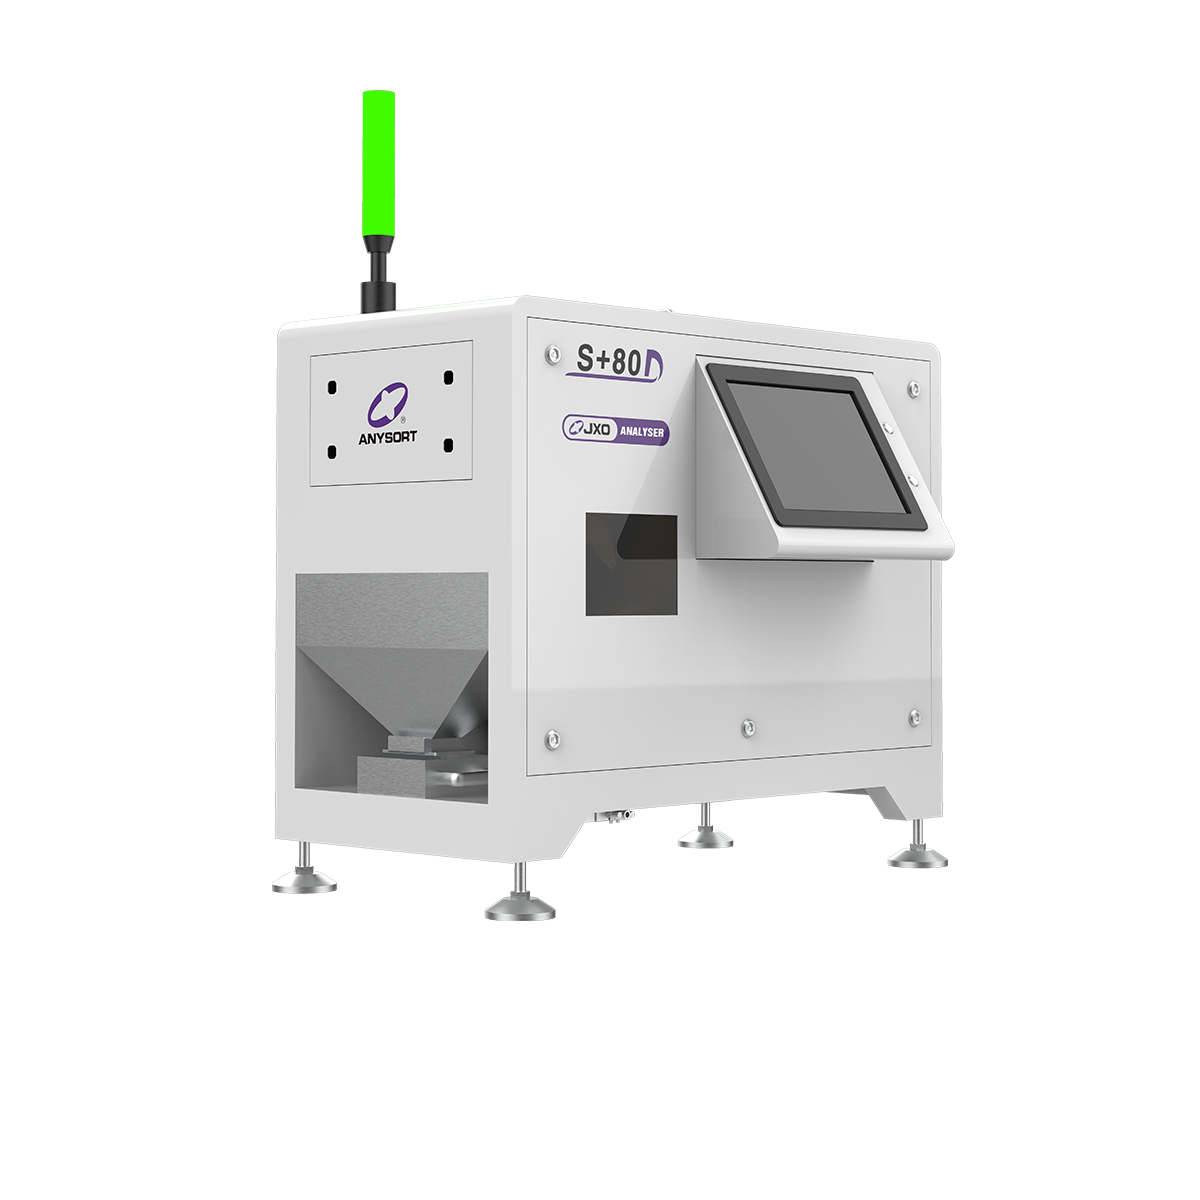
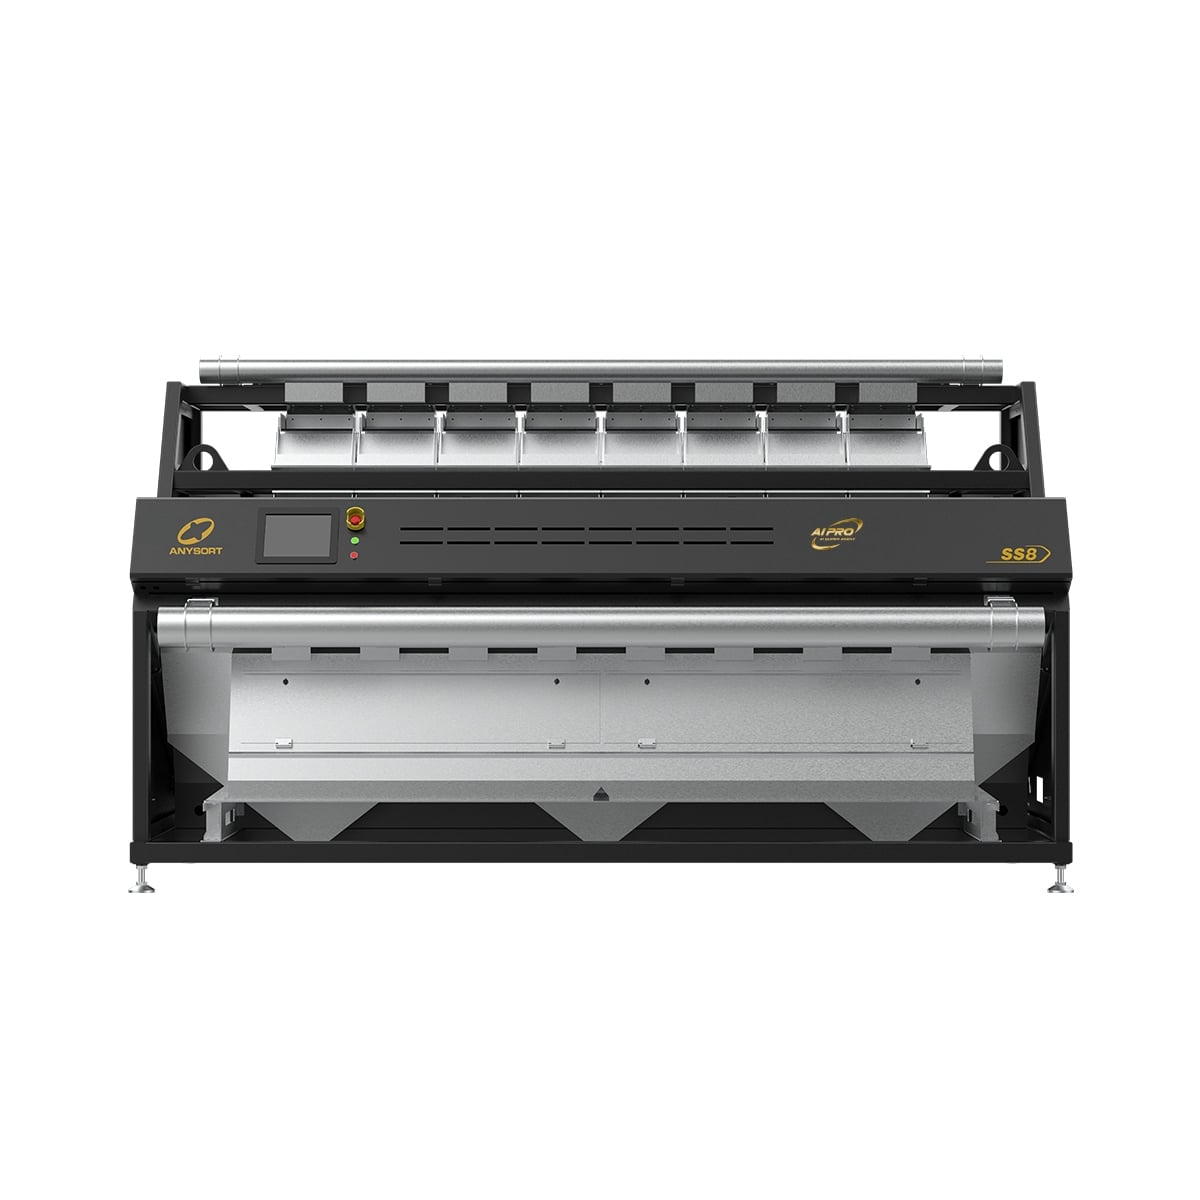
A color sorter machine manufacturer specializes in producing advanced optical sorting equipment designed to enhance product quality and efficiency across multiple industries. These machines utilize sophisticated color recognition technology to automatically separate materials based on chromatic properties, ensuring superior sorting accuracy that manual processes cannot achieve.
The color sorter machine manufacturer develops systems equipped with high-resolution cameras, intelligent lighting systems, and precision ejection mechanisms. These technological features work in harmony to detect subtle color variations and remove defective items from production lines at remarkable speeds. Modern color sorter machines can process thousands of items per minute while maintaining consistent accuracy rates exceeding 99 percent.
Applications for color sorter machine manufacturer equipment span agriculture, food processing, recycling, mining, and plastic industries. In agricultural settings, these machines sort grains, seeds, and nuts by color and quality. Food processing facilities use them to ensure product consistency and remove contaminated items. Recycling operations leverage this technology to separate different plastic types, while mining companies employ color sorters to identify valuable minerals and gemstones.
The color sorter machine manufacturer integrates artificial intelligence and machine learning algorithms into their systems, enabling adaptive sorting capabilities that improve over time. These innovations reduce operational costs while increasing throughput and product quality. Investment in a color sorter machine manufacturer's equipment represents a strategic choice for businesses seeking competitive advantages through automation and precision quality control technology.

 EN