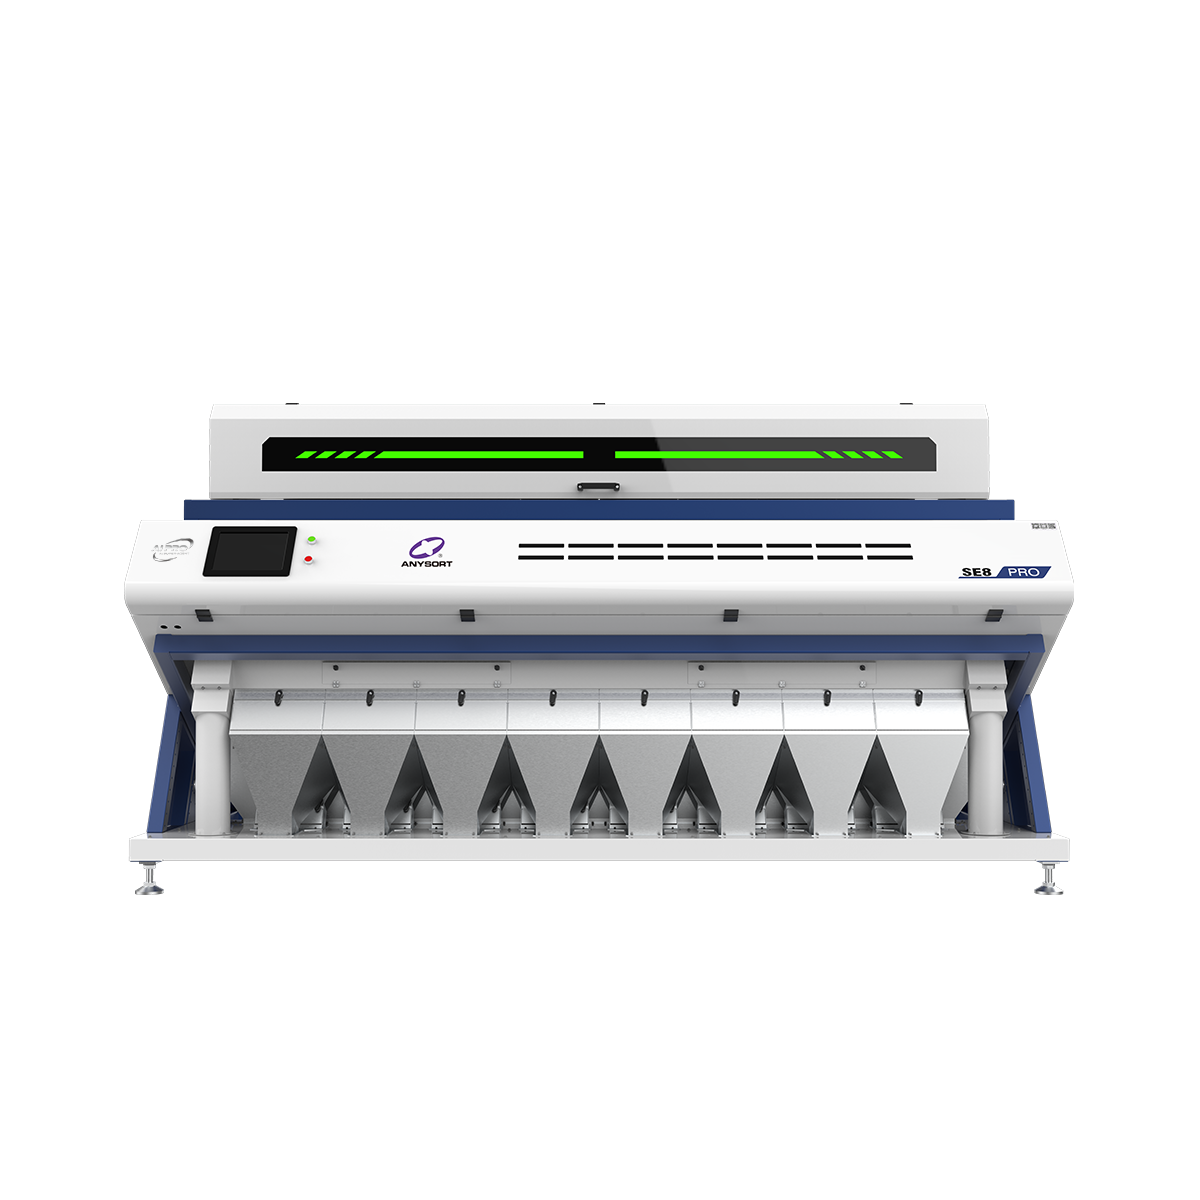
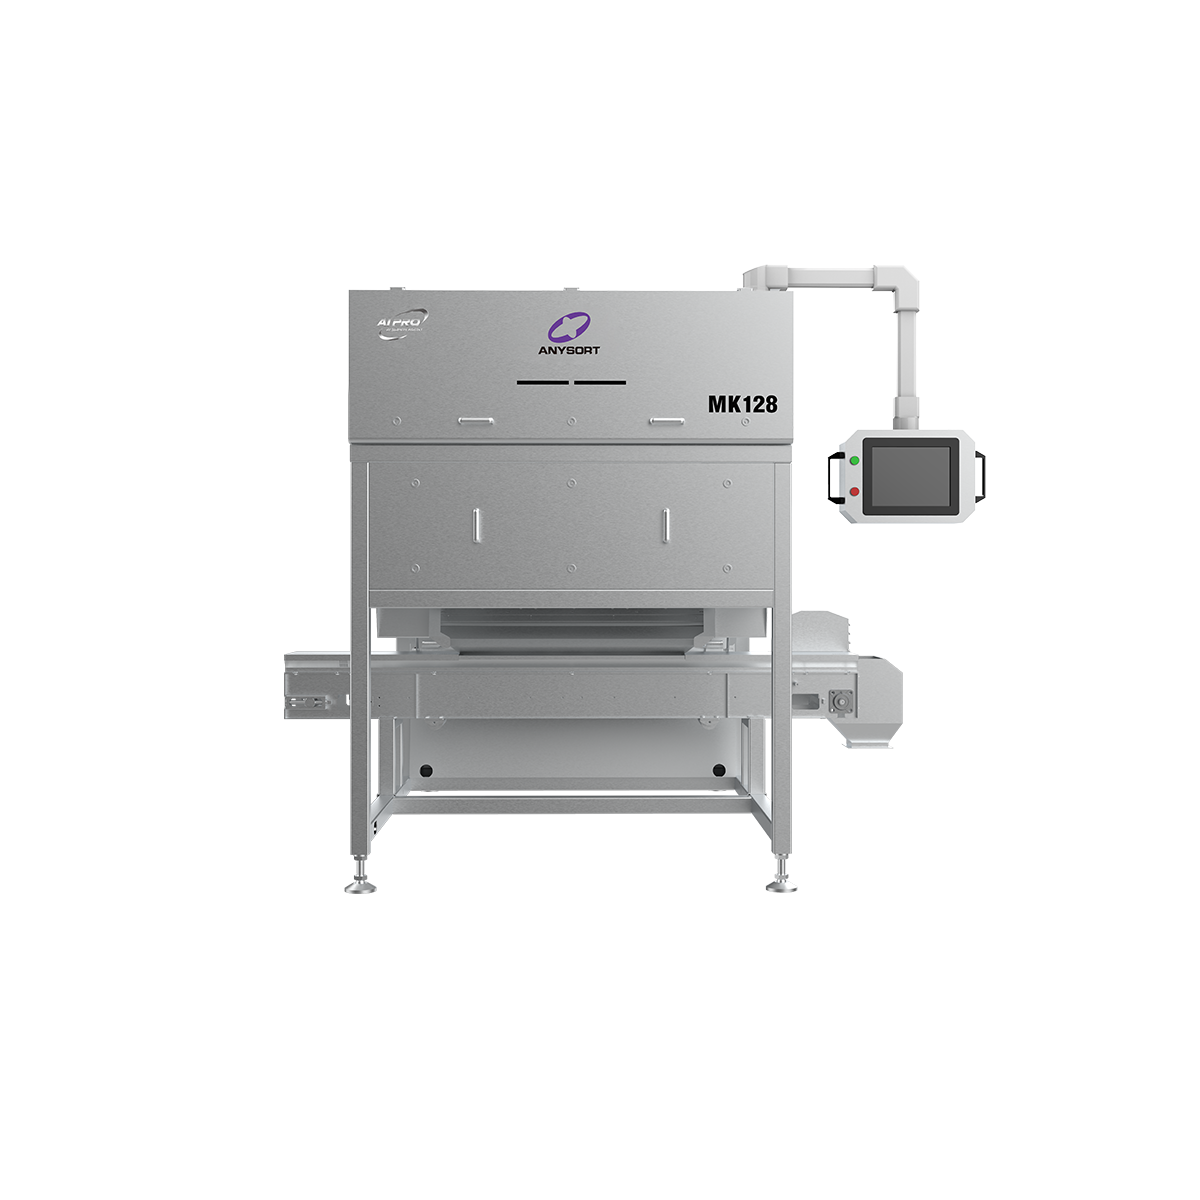
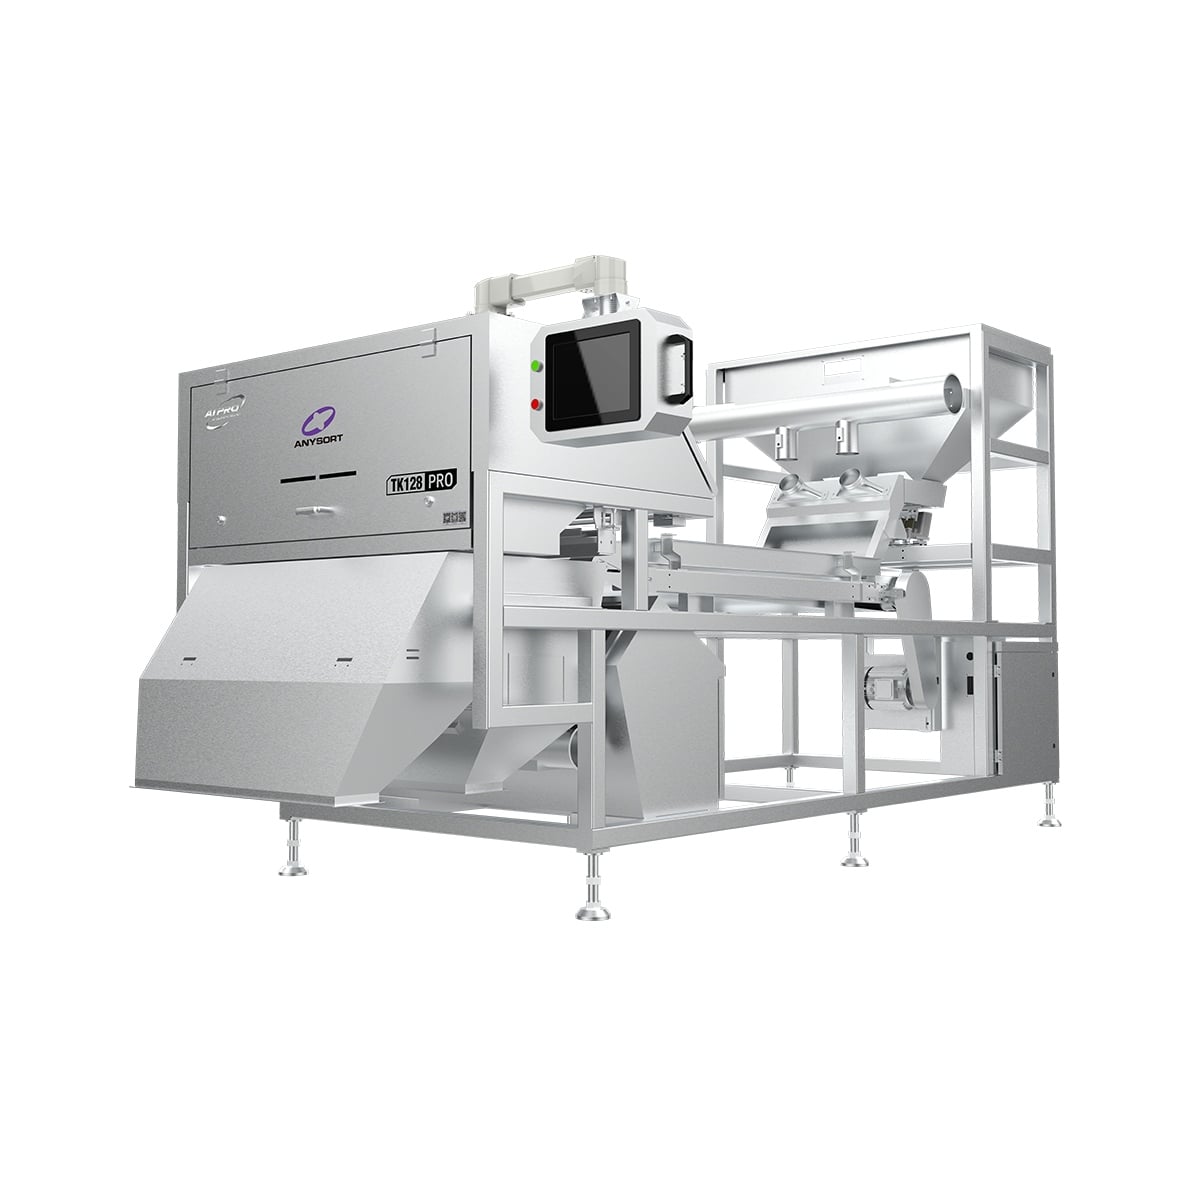
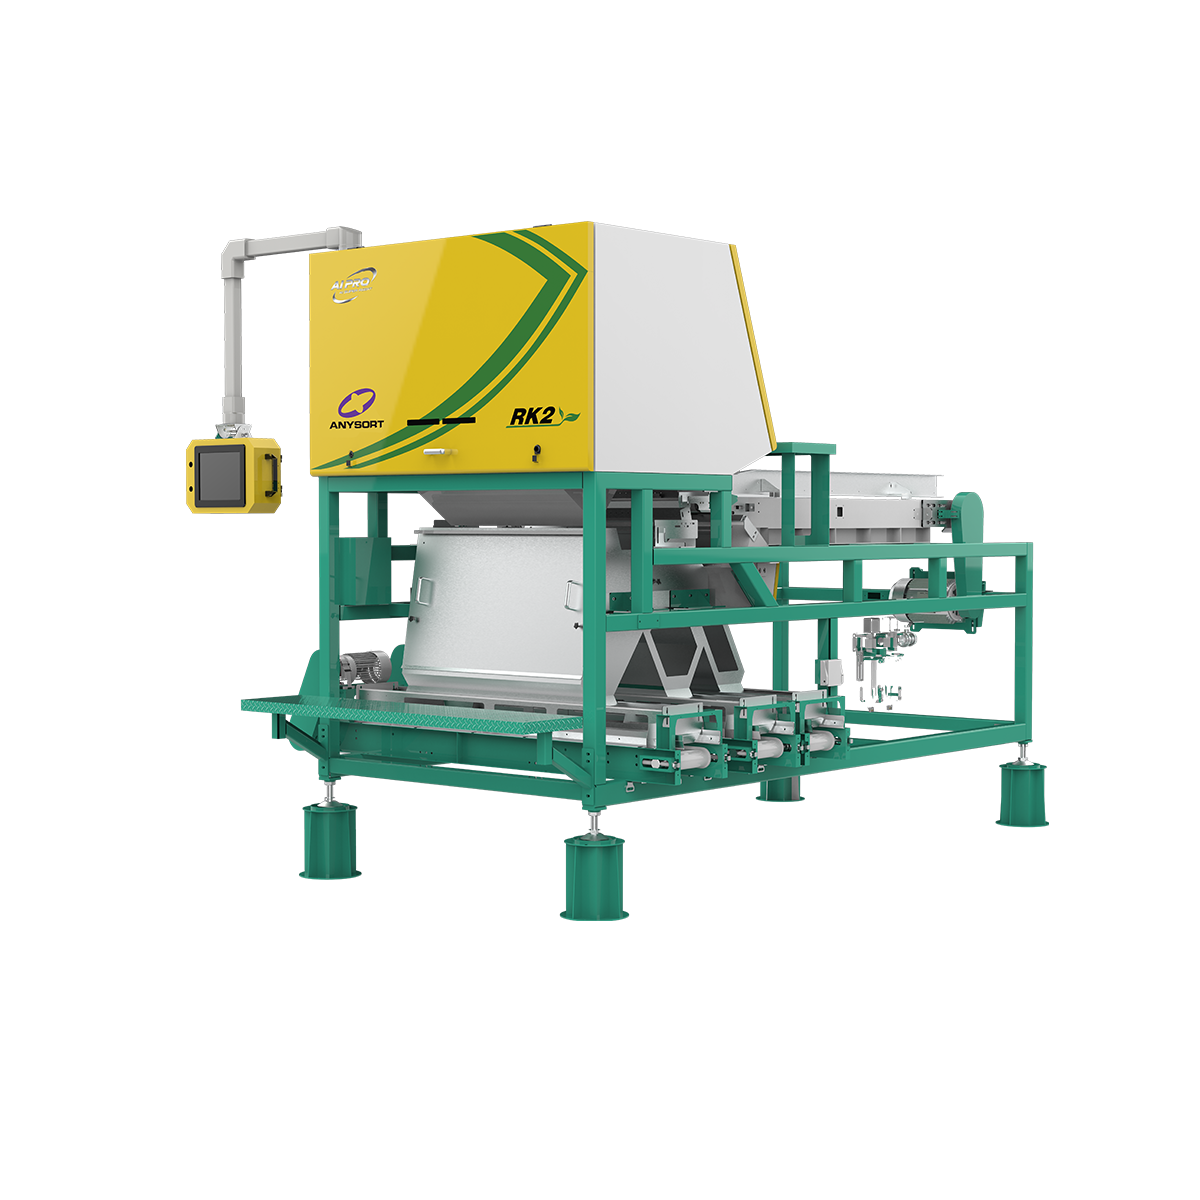
Professional Color Sorter Rice Machine

All Categories

color sorter rice

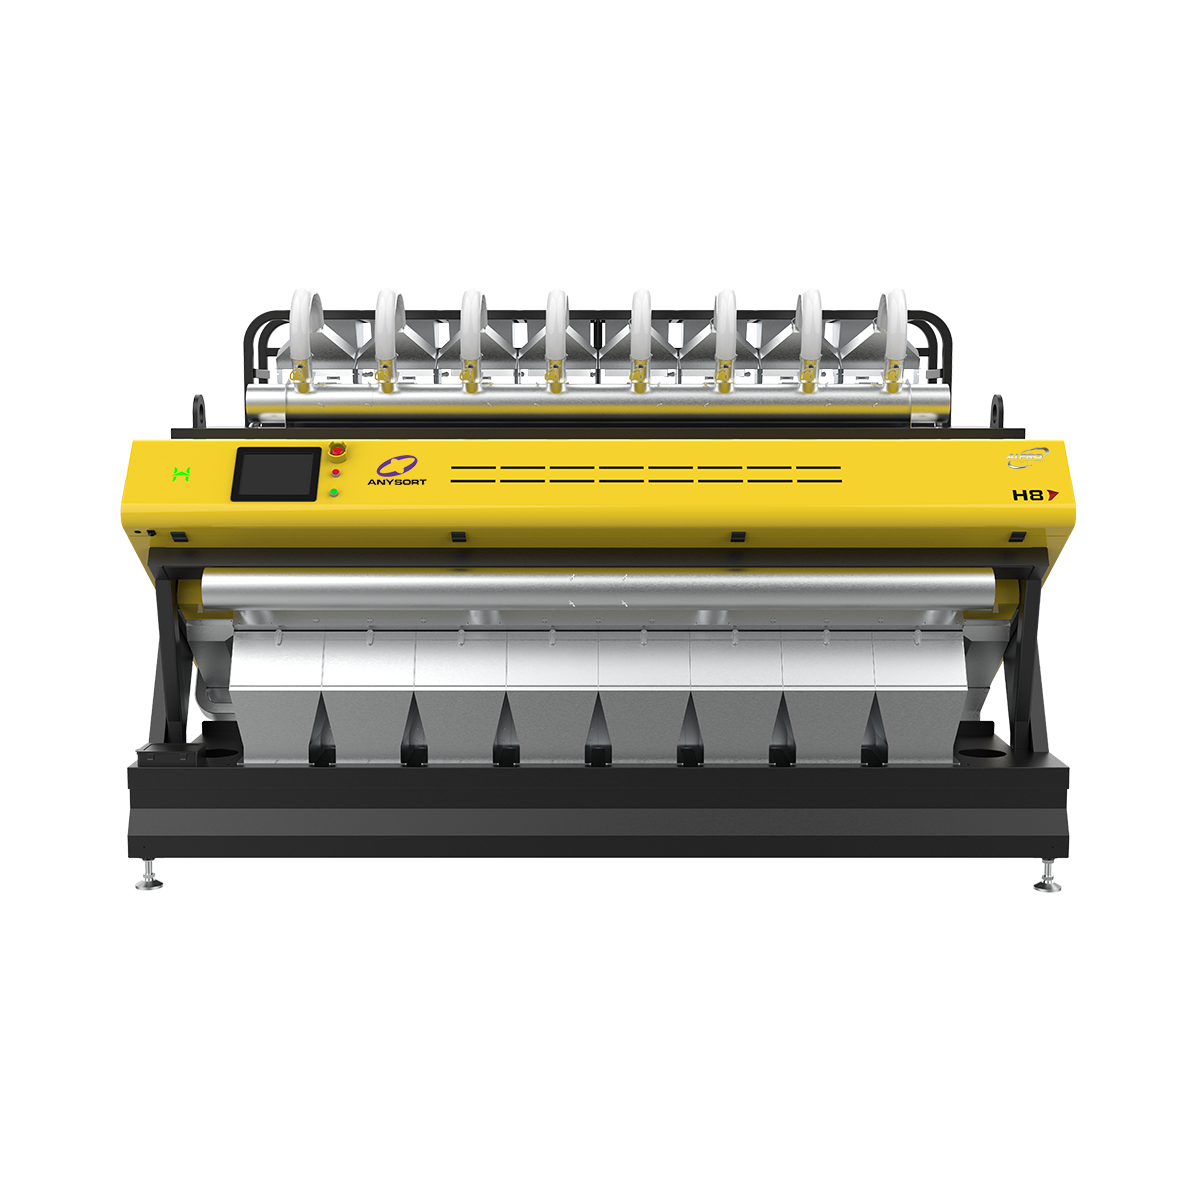
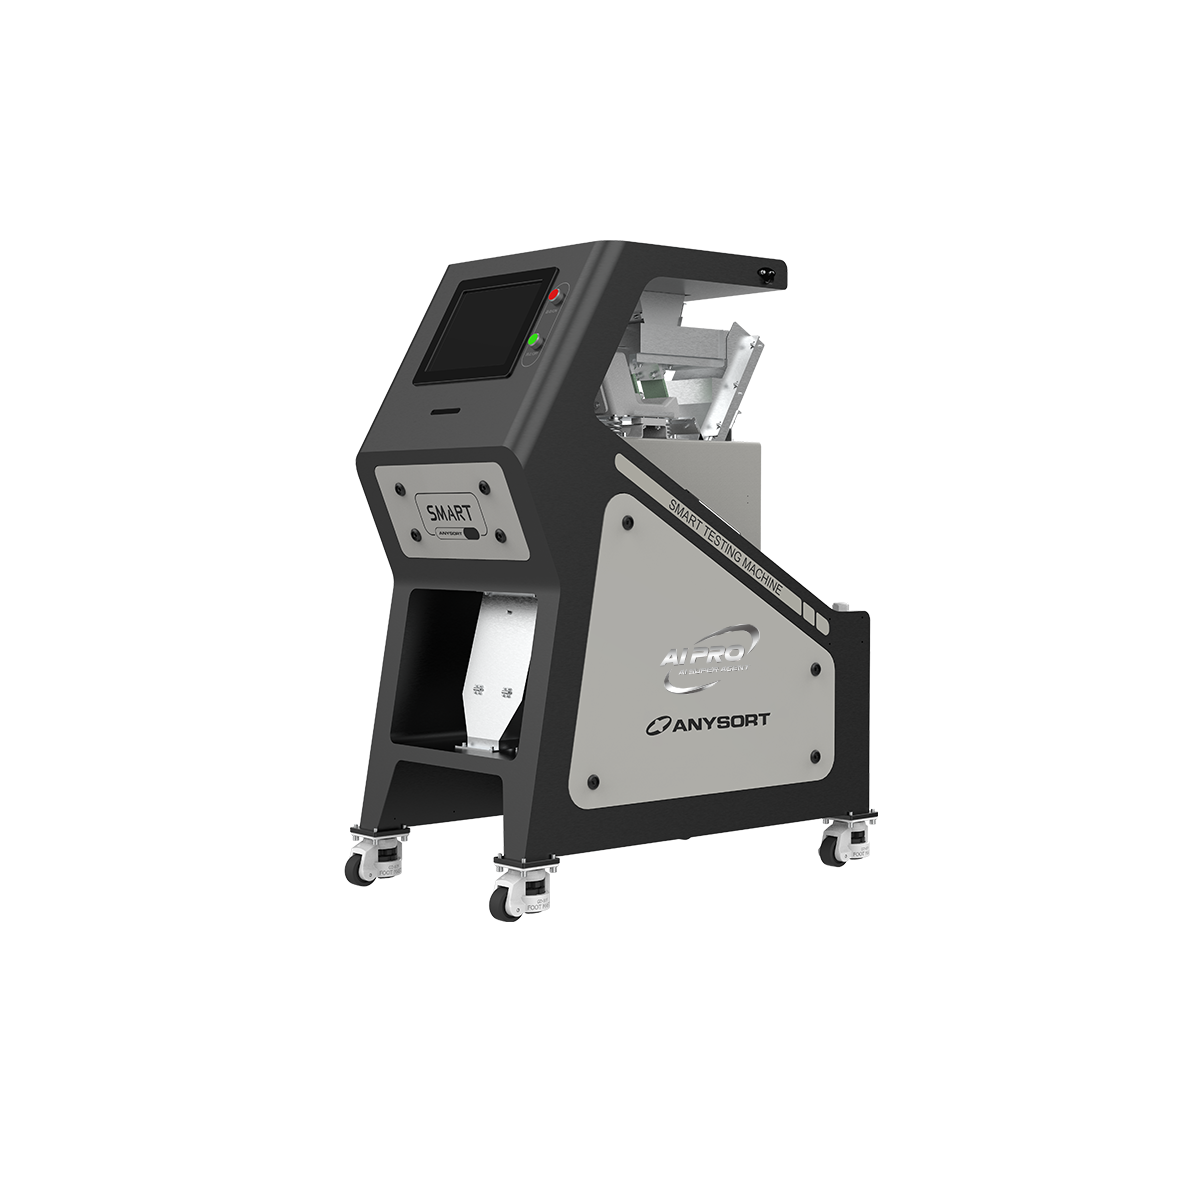
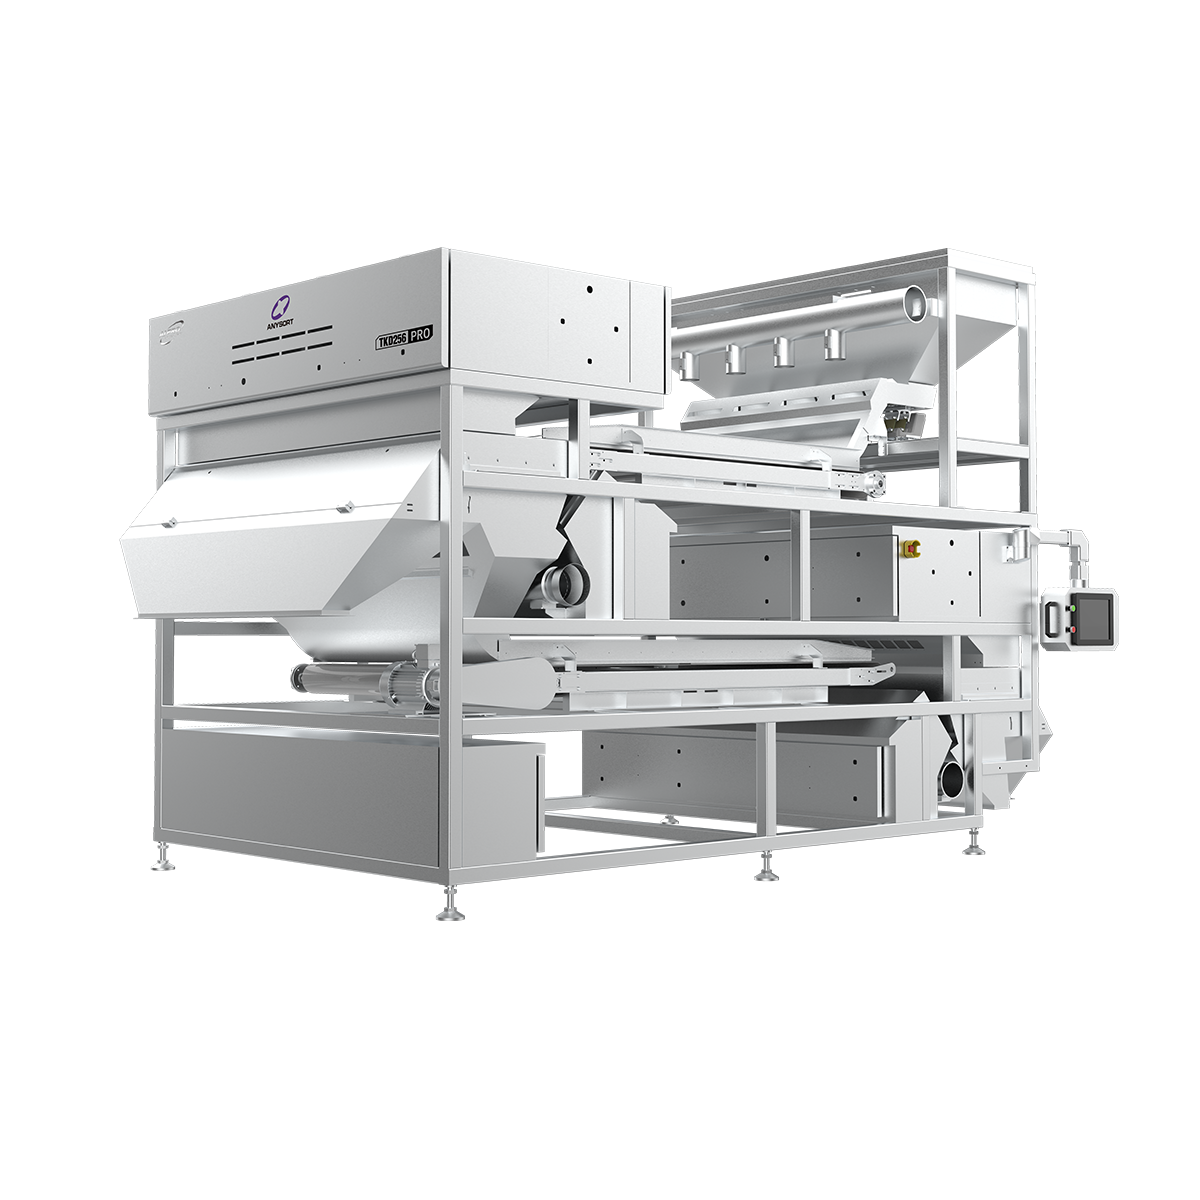
A color sorter rice is an advanced optical sorting machine designed to automatically detect and remove defective grains from rice batches. This innovative technology uses high-speed cameras and sophisticated image recognition algorithms to identify discolored, damaged, or foreign particles in rice during processing. The color sorter rice system operates by passing grains through a detection chamber where LED lighting illuminates each particle for precise analysis. The primary function of a color sorter rice machine is to improve rice quality by separating premium grains from inferior ones based on color, size, and texture characteristics. Modern color sorter rice equipment can process large volumes, handling thousands of grains per second with exceptional accuracy. The technology ensures consistent quality standards while minimizing waste during the sorting process. Key technological features include advanced sensor systems, pneumatic ejection mechanisms, and intelligent processing software. A professional color sorter rice unit integrates real-time data monitoring and automated calibration capabilities. These machines work seamlessly in commercial rice mills, processing facilities, and agricultural enterprises seeking to enhance product quality and market competitiveness. Applications of color sorter rice technology span across various industries, from large-scale rice mills to export-oriented businesses. The color sorter rice system helps producers meet strict international quality standards while reducing manual labor requirements. Investment in color sorter rice equipment represents a strategic decision for businesses committed to delivering superior rice products consistently.

New Products

Choosing a color sorter rice system delivers substantial operational and commercial benefits for rice processing businesses. This technology dramatically improves product quality by automatically removing discolored, broken, and contaminated grains that manual inspection might miss. The color sorter rice machine ensures every batch meets rigorous quality standards, building customer trust and brand reputation. Operationally, a color sorter rice unit significantly reduces labor costs by automating the sorting process. Rather than employing teams of workers for manual grain inspection, businesses deploy the color sorter rice equipment to handle this demanding task efficiently and consistently. This automation frees staff to focus on other critical production activities while maintaining superior output quality. The color sorter rice technology maximizes profitability by minimizing waste and product loss. By accurately identifying premium grains and separating defective material, the color sorter rice system increases the percentage of sellable product from each harvest. This translates directly into higher revenue and improved profit margins for rice producers and processors. Implementing a color sorter rice solution enhances market competitiveness. Modern buyers demand consistent, high-quality rice products, and the color sorter rice equipment helps businesses meet these expectations reliably. Whether serving domestic markets or export customers, the color sorter rice investment demonstrates commitment to quality excellence. Additionally, the color sorter rice system provides valuable production data and insights. Real-time monitoring capabilities allow operators to track sorting performance and make informed decisions about processing parameters. This data-driven approach supports continuous improvement initiatives and operational optimization. The color sorter rice equipment ultimately becomes an essential tool for achieving business growth and customer satisfaction in the competitive rice industry.

Latest News

How Much Does a Color Sorter Machine Cost?

12

Aug

How Much Does a Color Sorter Machine Cost?

Understanding the investment required for a color sorter machine is essential for businesses in agriculture, food processing, and recycling sectors. The cost of a color sorter machine varies significantly based on capacity, technology sophistication,...
View More
How Does Nuts Sorter Technology Ensure Quality?

19

Aug

How Does Nuts Sorter Technology Ensure Quality?

The global nuts processing industry relies on precision and consistency to meet strict quality standards and regulatory requirements. A nuts sorter has become indispensable for processors seeking to eliminate defects, contaminants, and substandard pr...
View More
How Do Color Sorters Improve Product Quality?

26

Aug

How Do Color Sorters Improve Product Quality?

Product quality stands as a critical differentiator in competitive industrial markets, and achieving consistency at scale requires more than manual oversight. A color sorter represents one of the most effective technologies for identifying and removi...
View More
Top AI Color Sorter Manufacturers in China (2026)

30

Aug

Top AI Color Sorter Manufacturers in China (2026)

The global demand for precision sorting technology has surged dramatically, with color sorter machine manufacturers in China leading innovation across agricultural and industrial sectors. Chinese color sorter machine manufacturers have established th...
View More

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

color sorter rice

Precision Optical Detection Technology

Precision Optical Detection Technology

The color sorter rice machine utilizes cutting-edge optical detection systems that analyze grain characteristics with remarkable precision. Using advanced LED lighting and high-resolution cameras, the color sorter rice equipment captures detailed images of individual grains as they pass through the sorting chamber. The sophisticated image processing software instantly compares each grain against predefined quality standards, identifying even subtle variations in color, texture, and appearance that human eyes might overlook. This color sorter rice technology eliminates guesswork from quality control, ensuring absolutely consistent results across every batch processed. The optical detection system operates at extraordinary speeds, analyzing thousands of grains per minute without compromising accuracy. Businesses using the color sorter rice system benefit from objective, repeatable sorting criteria that eliminate human bias and error variability.
High-Speed Processing Capacity

High-Speed Processing Capacity

The color sorter rice system excels at handling massive processing volumes without sacrificing quality or accuracy. Modern color sorter rice equipment processes grains at speeds reaching hundreds of kilograms per hour, making it ideal for commercial rice mills and large-scale facilities. This impressive throughput means businesses can sort significantly larger quantities than traditional manual methods allow, dramatically improving operational efficiency. The color sorter rice machine maintains consistent sorting precision even during extended operation periods, ensuring reliability throughout full production days. Users of the color sorter rice equipment experience reduced bottlenecks and improved production scheduling flexibility. The high-speed capability of the color sorter rice system translates to faster order fulfillment and improved customer delivery timelines. Facilities investing in the color sorter rice technology gain substantial competitive advantages through increased daily output capacity and enhanced responsiveness to market demand.
Waste Reduction and Yield Maximization

Waste Reduction and Yield Maximization

Implementing a color sorter rice system directly increases the percentage of marketable grain recovered from each processing batch. The color sorter rice equipment precisely separates premium grains from defective material, recovering valuable product that manual sorting might inadvertently discard. This color sorter rice technology significantly reduces overall waste percentages, transforming marginal grain into profitable inventory. By maximizing the proportion of sellable product, the color sorter rice system increases revenue per ton of processed rice. The color sorter rice equipment helps processors meet stringent quality standards while maintaining higher yield rates than competing technologies. This combination of quality assurance and yield optimization creates powerful financial returns on the color sorter rice investment. Businesses deploying the color sorter rice system experience measurable improvements in profitability and resource efficiency throughout their operations.

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

Copyright © 2026 Anhui Jiexun Optoelectronic Technology Co., Ltd. All rights reserved.  -  Privacy policy