Colour Sorter Machine | Precision Sorting

All Categories

colour sorter machine

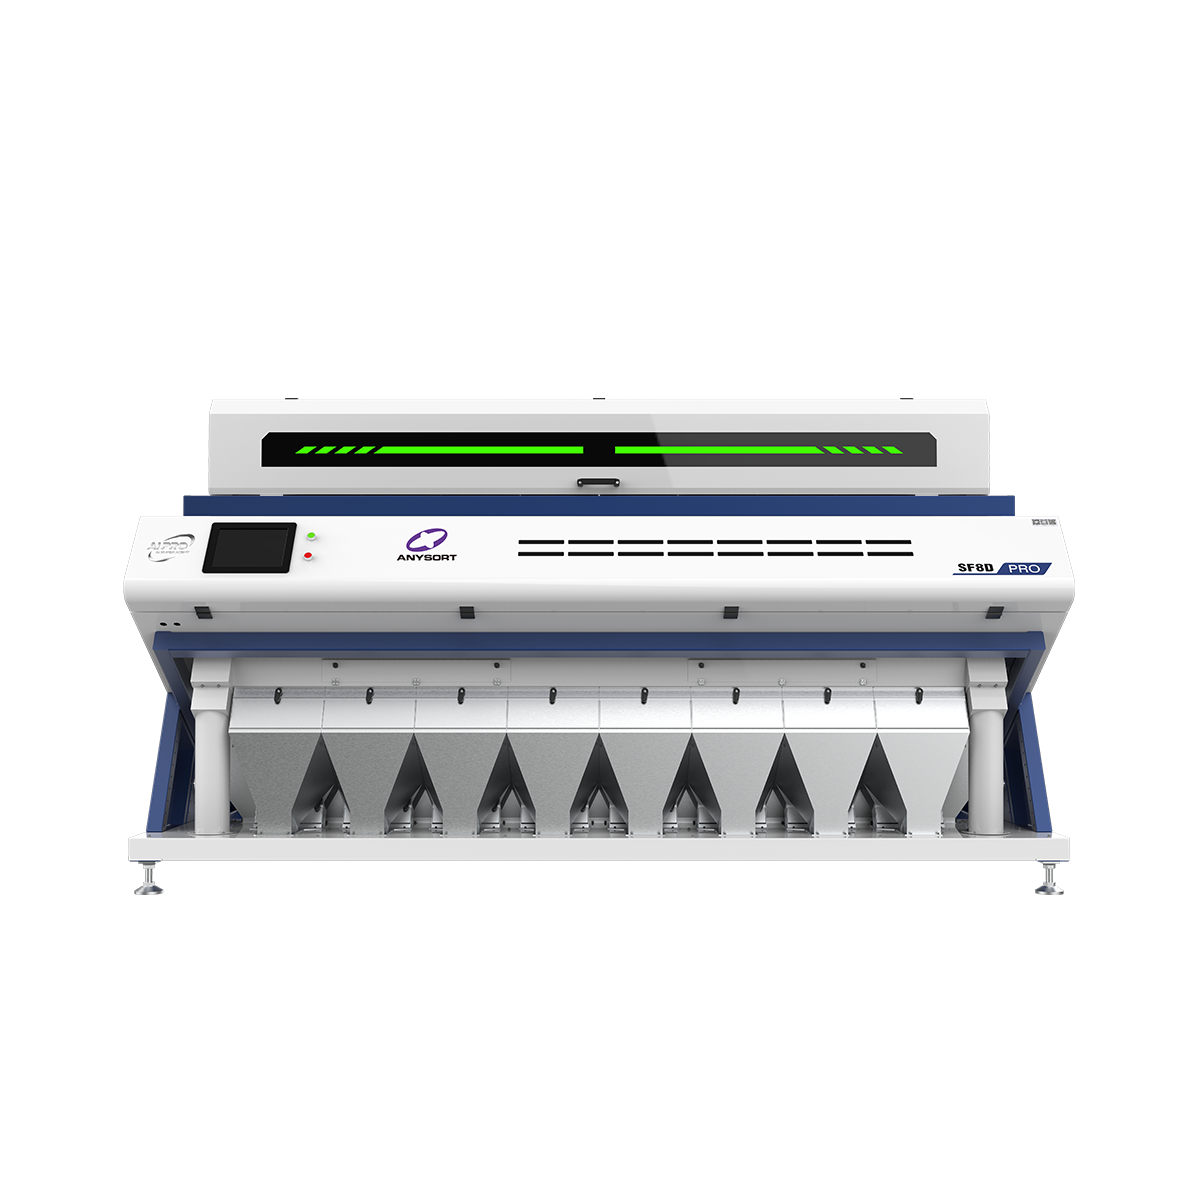
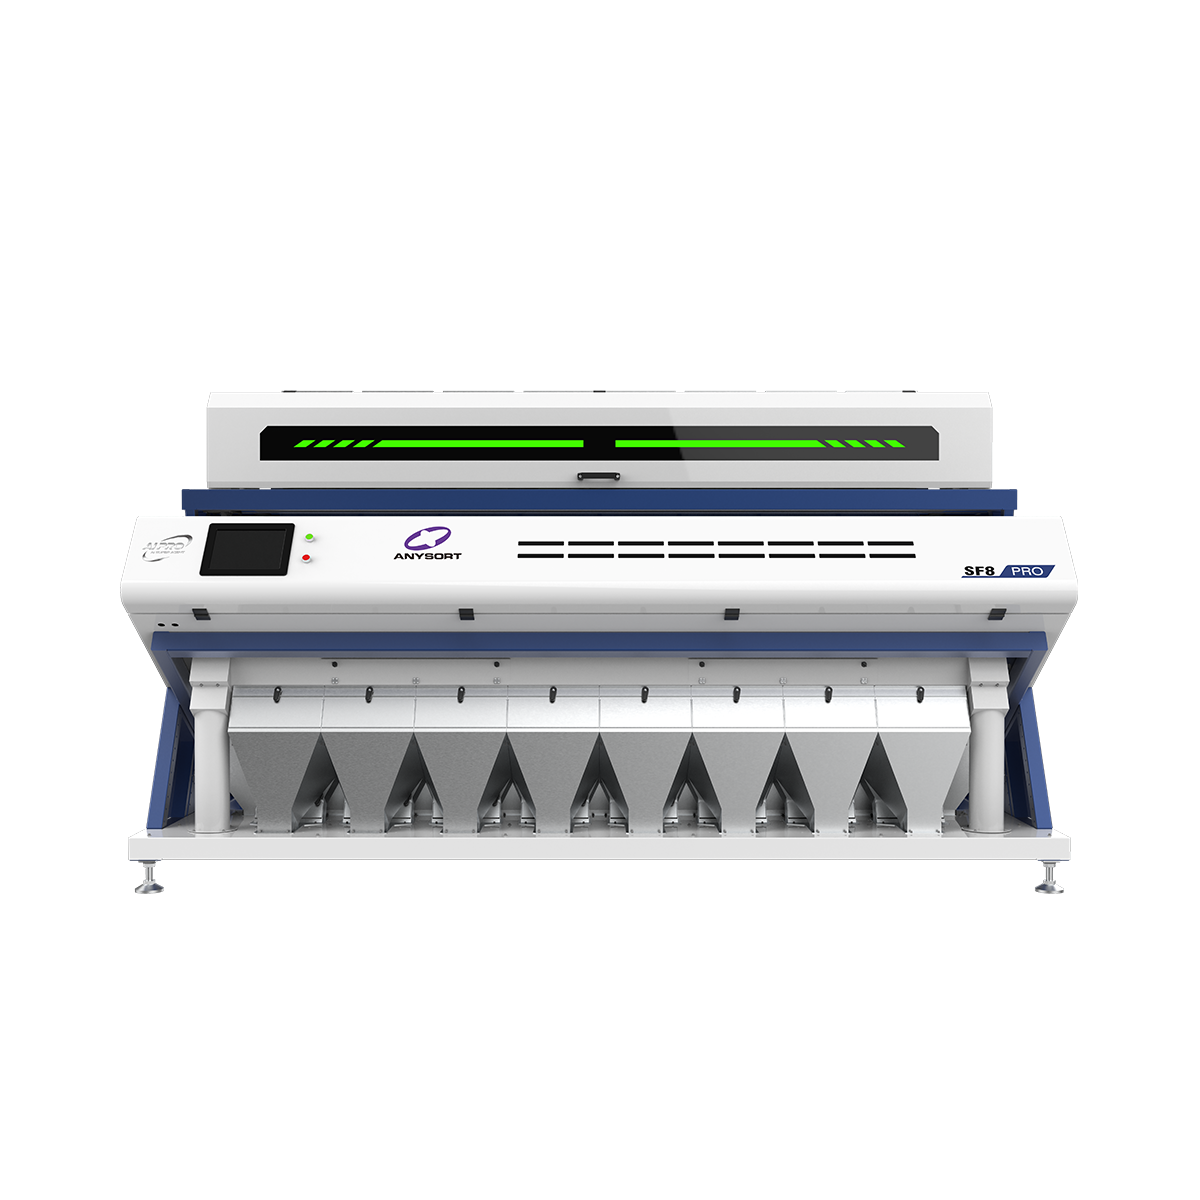
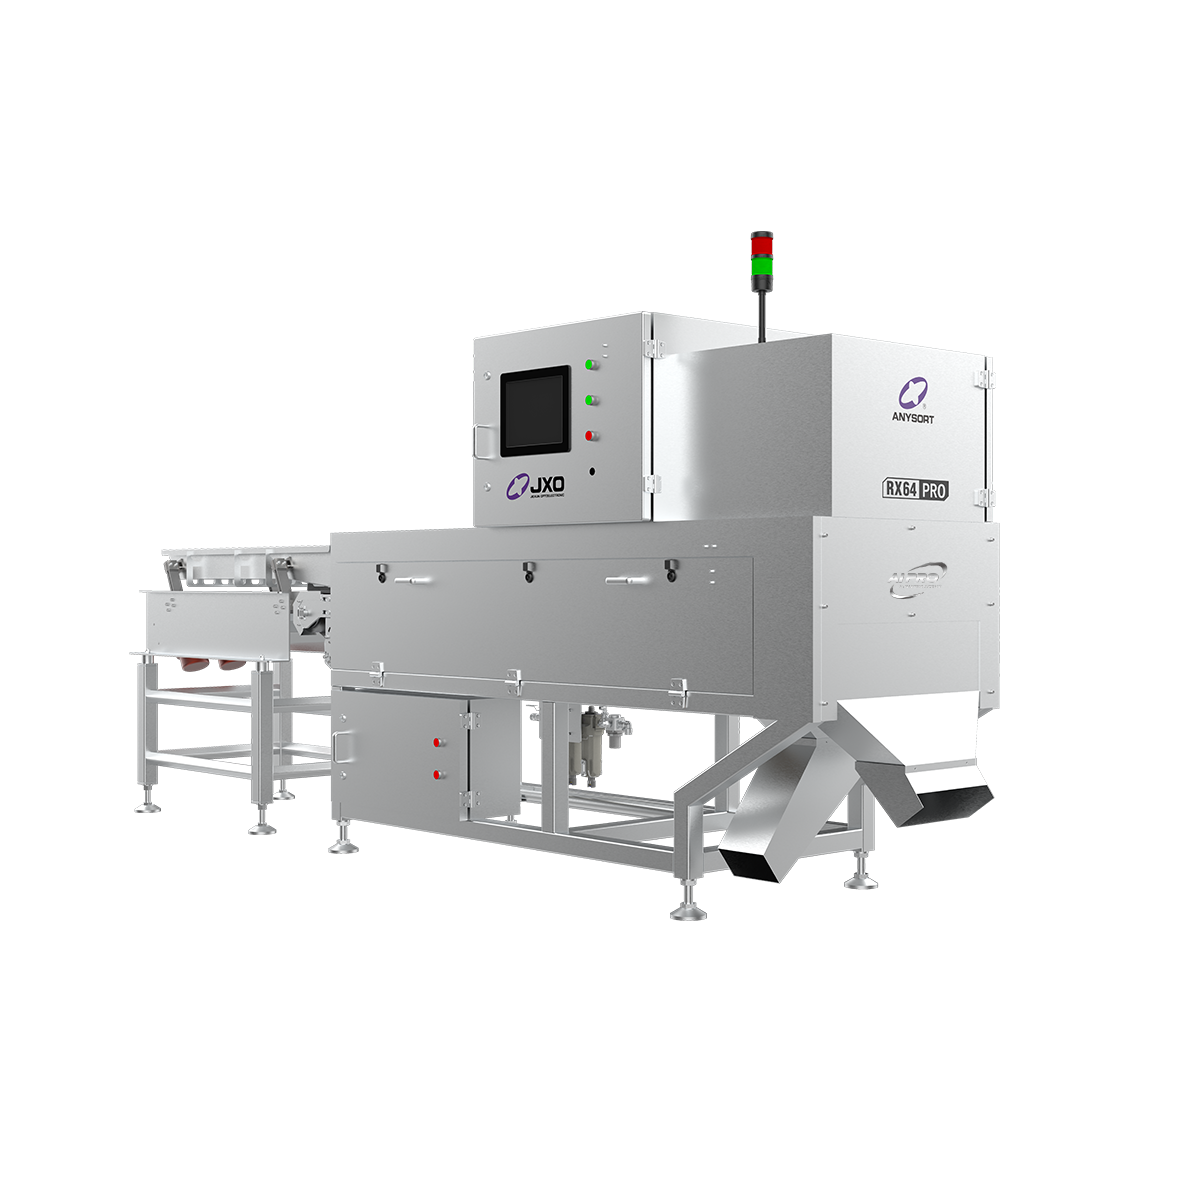
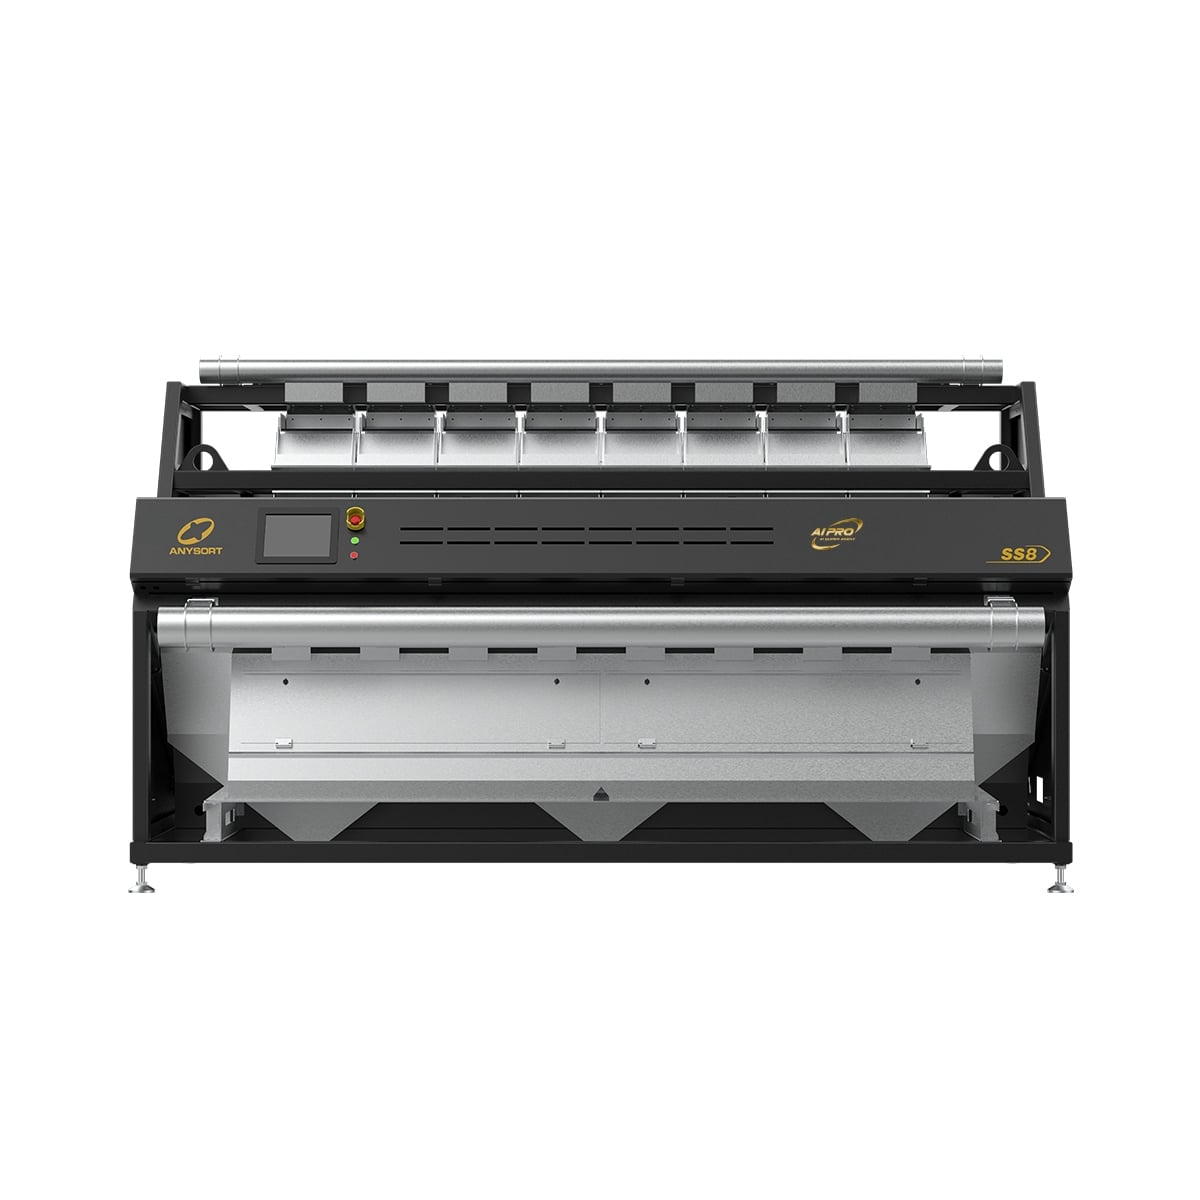
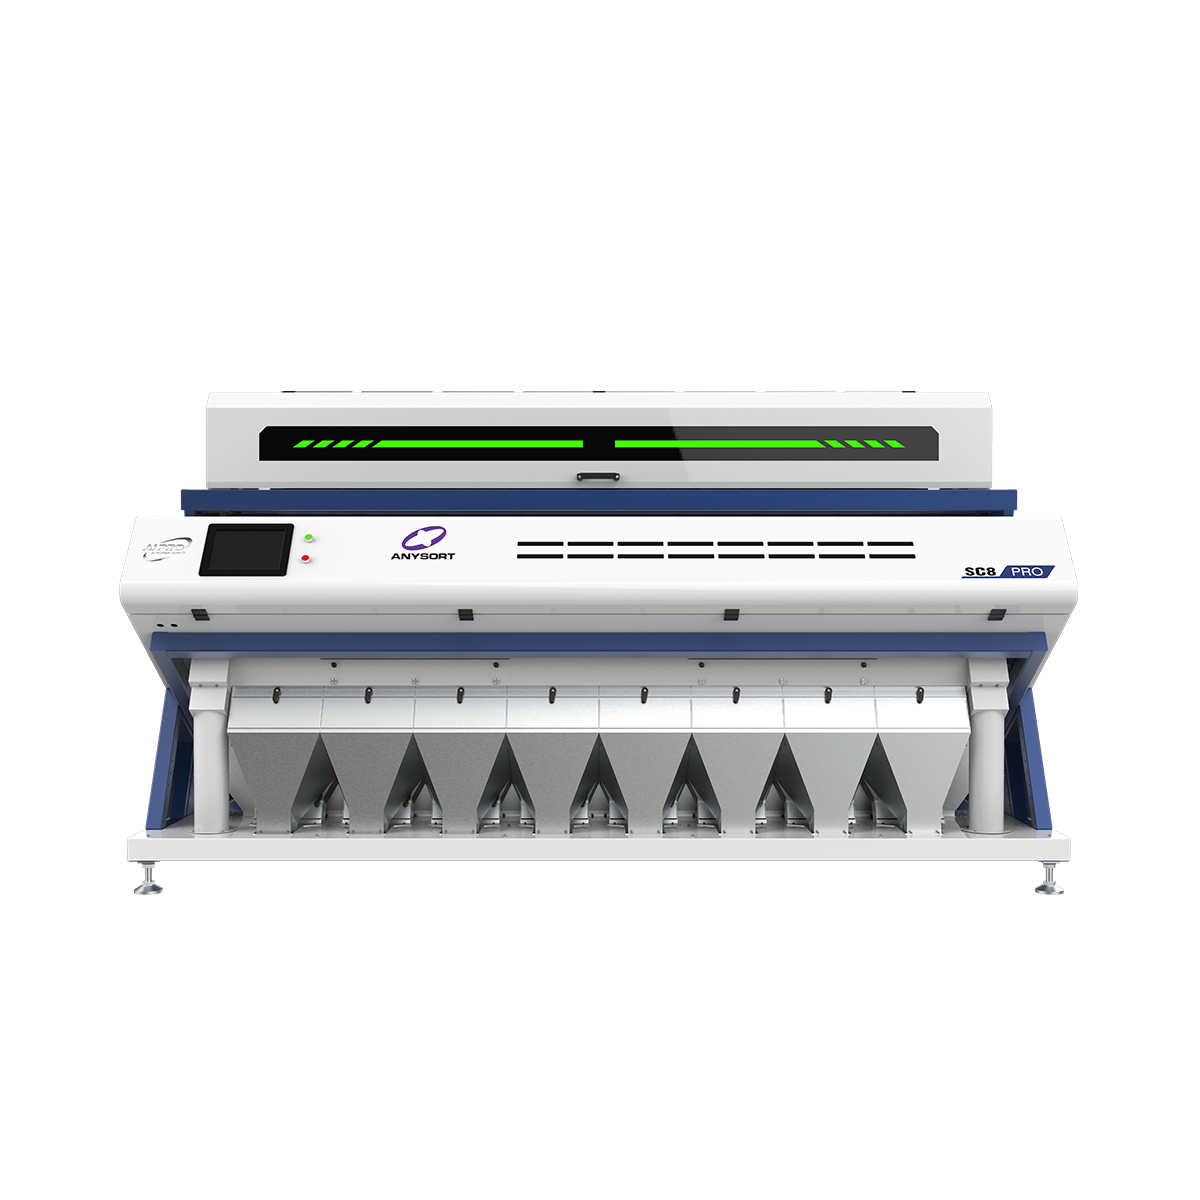
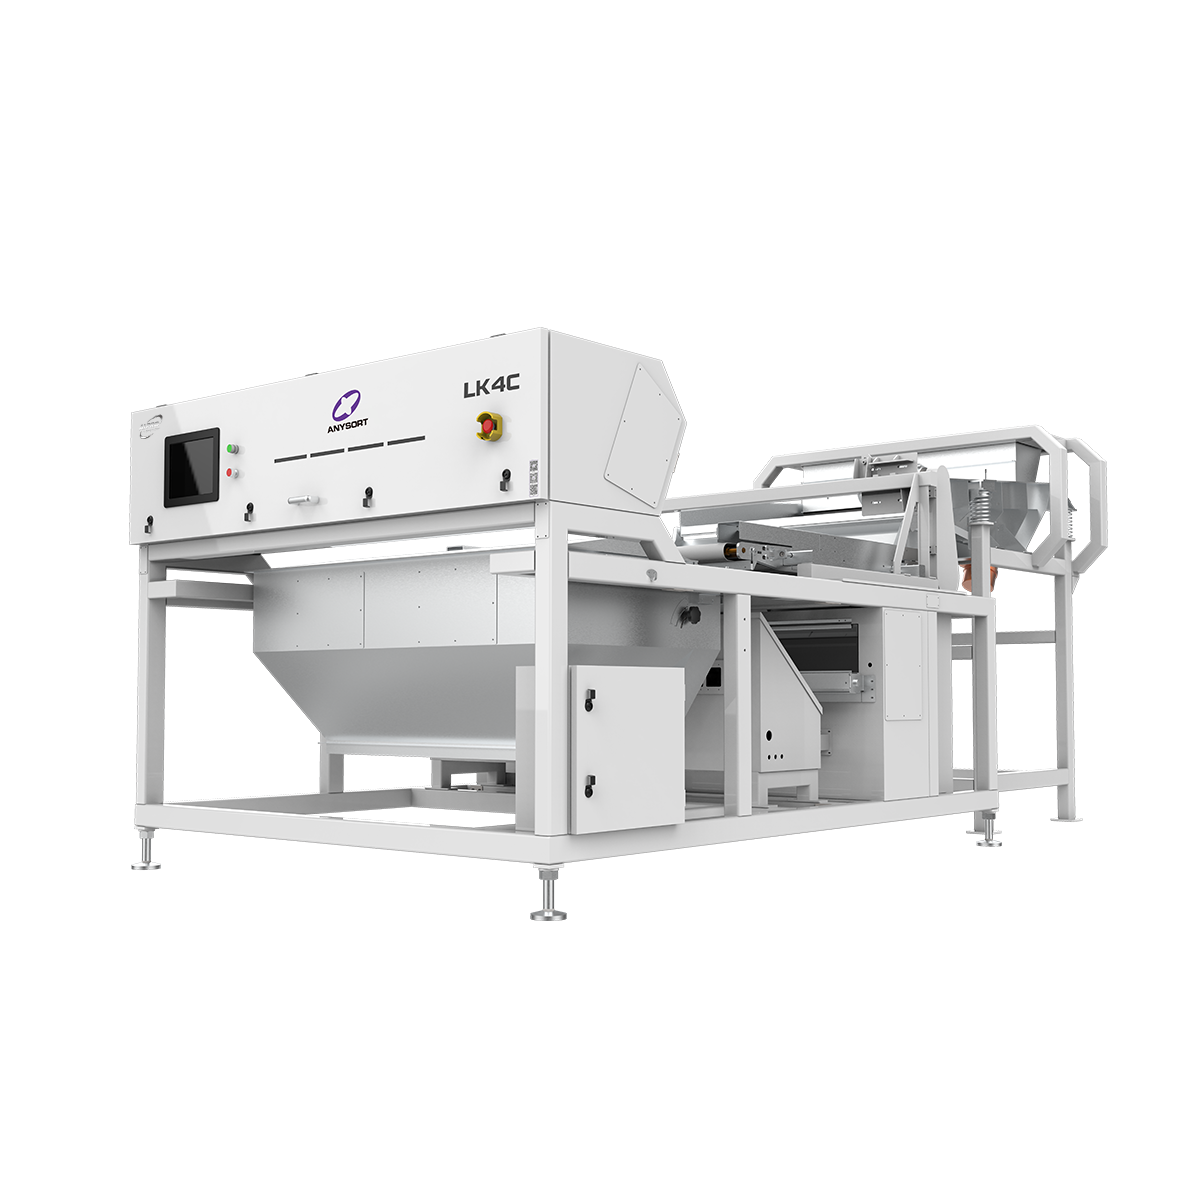
A colour sorter machine is an advanced optical sorting system designed to automatically detect, categorize, and separate materials based on their color properties. This sophisticated equipment utilizes high-speed cameras, advanced sensors, and artificial intelligence technology to achieve precise sorting accuracy at industrial scales. The colour sorter machine represents a significant advancement in material processing, offering unparalleled efficiency compared to manual sorting methods. The primary function of a colour sorter machine involves scanning materials as they pass through the sorting chamber, capturing detailed color information, and using machine learning algorithms to identify defects, contamination, or quality variations. Once identified, the colour sorter machine activates pneumatic ejection mechanisms to remove unwanted items with millisecond precision. This automated process ensures consistent quality control and significantly increases throughput capacity. Technologically, the colour sorter machine integrates multiple components including LED illumination systems, high-resolution imaging sensors, and rapid-response ejection valves. The colour sorter machine operates continuously, processing thousands of items per minute while maintaining exceptional accuracy levels. Modern colour sorter machines feature customizable sorting parameters, allowing operators to adjust sensitivity settings based on specific material requirements and quality standards, making this equipment versatile across numerous industries.

Popular Products

The colour sorter machine delivers substantial operational and financial benefits for businesses seeking to enhance productivity and maintain consistent product quality. By automating the sorting process, the colour sorter machine eliminates human error and fatigue-related inconsistencies, ensuring every item meets established quality criteria. This reliability translates directly into improved customer satisfaction and reduced product returns. Operationally, the colour sorter machine dramatically increases processing capacity by handling thousands of items hourly, far exceeding manual sorting rates. Businesses utilizing a colour sorter machine experience reduced labor costs associated with manual inspection while simultaneously freeing employees to focus on more specialized tasks. The colour sorter machine operates continuously without breaks, maximizing production throughput and meeting demanding market timelines. For manufacturers, the colour sorter machine provides critical quality assurance by identifying defects invisible to the human eye. This capability protects brand reputation and prevents substandard products from reaching consumers. The colour sorter machine's consistent performance establishes trust with customers and regulatory bodies alike. The colour sorter machine proves highly suitable for industries including food processing, agriculture, recycling, minerals, and manufacturing. In food applications, the colour sorter machine removes discolored grains, damaged nuts, and foreign particles with exceptional precision. Agricultural producers benefit from crop quality improvement, while recycling facilities use the colour sorter machine to streamline material separation processes. The colour sorter machine's adaptability across applications makes it an intelligent investment for diverse business sectors seeking operational excellence and competitive advantage in their respective markets.

Practical Tips

How to Choose the Right Tea Color Sorter for Your Needs?

01

Aug

How to Choose the Right Tea Color Sorter for Your Needs?

Selecting the right tea color sorter is one of the most critical decisions tea processors face when modernizing their operations. A tea color sorter directly impacts product quality, operational efficiency, and market competitiveness. The wrong choic...
View More
How Can a Nuts Sorter Improve Your Production?

15

Aug

How Can a Nuts Sorter Improve Your Production?

A nuts sorter represents one of the most significant investments a food processing operation can make to enhance production quality and operational efficiency. The modern nuts sorter uses advanced imaging and sensor technology to identify and separat...
View More
How Do Color Sorters Improve Product Quality?

26

Aug

How Do Color Sorters Improve Product Quality?

Product quality stands as a critical differentiator in competitive industrial markets, and achieving consistency at scale requires more than manual oversight. A color sorter represents one of the most effective technologies for identifying and removi...
View More
Which factors should you consider when selecting a rice color sorter?

29

Aug

Which factors should you consider when selecting a rice color sorter?

Selecting the right rice color sorter is a critical decision that directly impacts your grain processing efficiency, product quality, and long-term profitability. A rice color sorter removes discolored, damaged, and foreign particles from rice batche...
View More

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

colour sorter machine

Precision Optical Detection Technology

Precision Optical Detection Technology

The colour sorter machine employs cutting-edge optical detection systems that capture thousands of color variations per second with extraordinary accuracy. High-resolution cameras mounted within the colour sorter machine work in conjunction with sophisticated lighting systems to examine each item individually. This technology enables the colour sorter machine to distinguish between subtle color differences that human inspectors would miss, ensuring only premium-quality items advance through production lines. The precision capabilities of the colour sorter machine make it invaluable for quality-sensitive industries. Food processors rely on the colour sorter machine to remove discolored items, foreign objects, and contaminated materials that could compromise product safety. The colour sorter machine maintains consistency across batches, delivering uniform quality that builds consumer confidence and brand loyalty. This advanced detection technology represents a crucial competitive advantage for businesses operating in quality-conscious markets.
High-Speed Processing and Maximum Throughput

High-Speed Processing and Maximum Throughput

Modern colour sorter machines process materials at remarkable speeds, handling thousands of items per minute while maintaining exceptional sorting accuracy. The colour sorter machine's ability to work continuously without fatigue ensures uninterrupted production flow, dramatically improving facility efficiency. By implementing a colour sorter machine, businesses increase output capacity without proportional increases in facility space or labor requirements. The operational efficiency delivered by the colour sorter machine directly impacts bottom-line profitability. Facilities utilizing the colour sorter machine reduce production cycles, meet tight deadlines, and respond quickly to market demands. Whether processing agricultural commodities, minerals, or manufactured goods, the colour sorter machine accelerates material flow through production systems. The colour sorter machine's high-speed sorting capability enables businesses to scale operations, increase market share, and maintain competitiveness in fast-paced industries where production efficiency determines market success and profitability.
Versatile Applications Across Multiple Industries

Versatile Applications Across Multiple Industries

The colour sorter machine demonstrates remarkable adaptability across diverse industrial sectors, making it a strategic investment for various business types. In agriculture, the colour sorter machine enhances crop quality by removing discolored grains and defective products. Food manufacturers depend on the colour sorter machine to ensure safety and consistency in processed items. Recycling operations utilize the colour sorter machine to separate materials by color, streamlining resource recovery processes. The colour sorter machine serves mining and mineral industries by categorizing ore based on color characteristics, improving mineral concentration. Manufacturing facilities employ the colour sorter machine for quality control across finished products. This broad applicability means businesses in different sectors gain significant value from the colour sorter machine investment. The colour sorter machine's flexible programming accommodates industry-specific requirements, allowing operators to customize sorting parameters for different materials and quality standards.

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

Copyright © 2026 Anhui Jiexun Optoelectronic Technology Co., Ltd. All rights reserved.  -  Privacy policy