color sorter
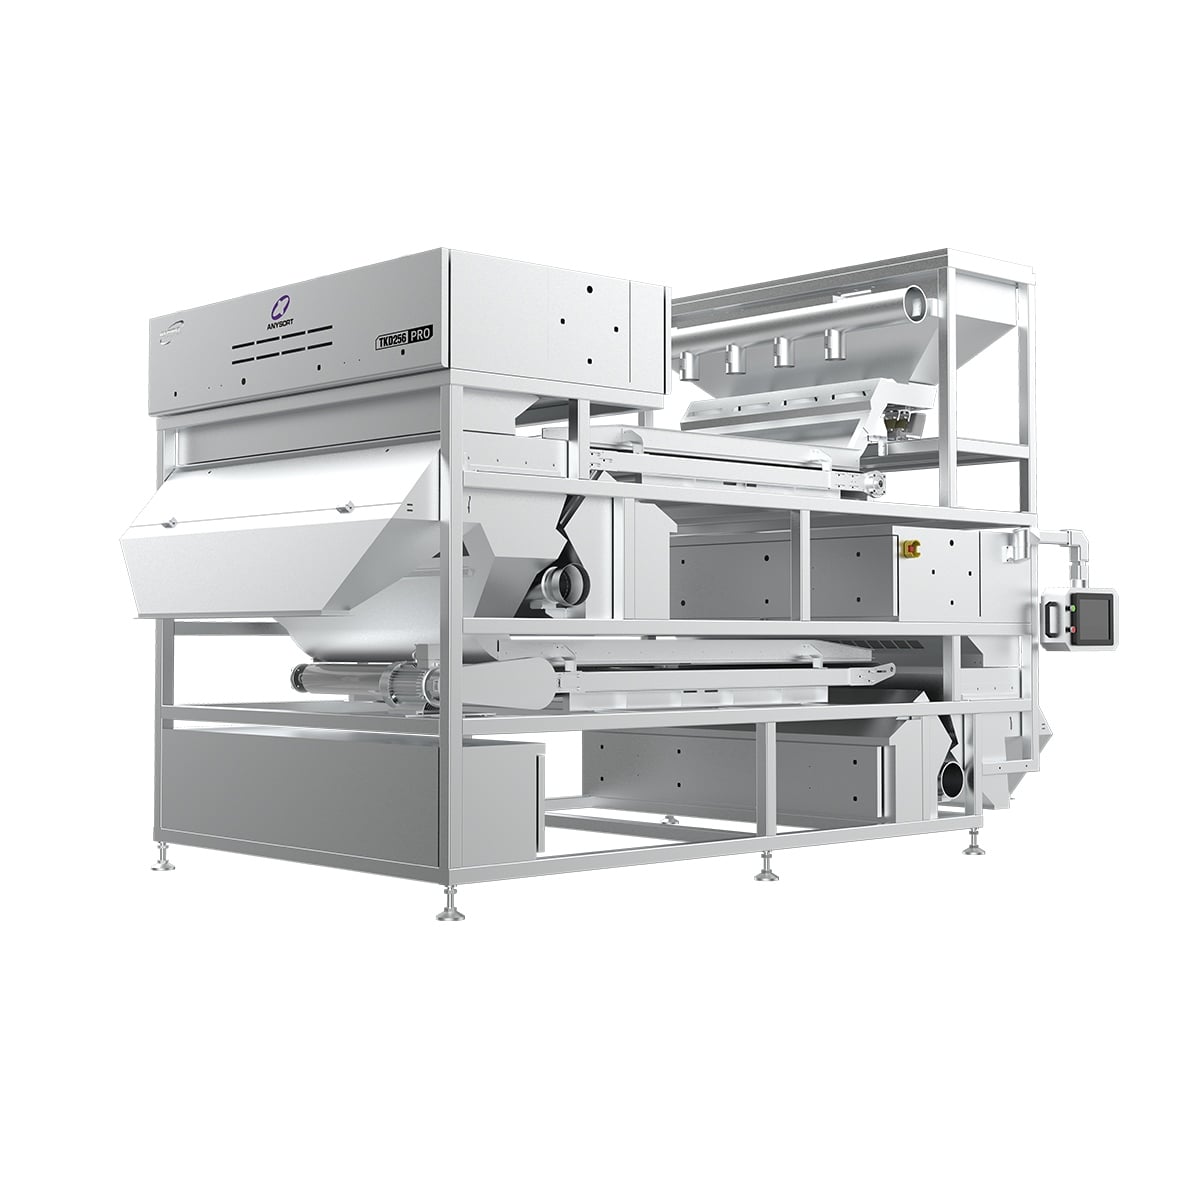
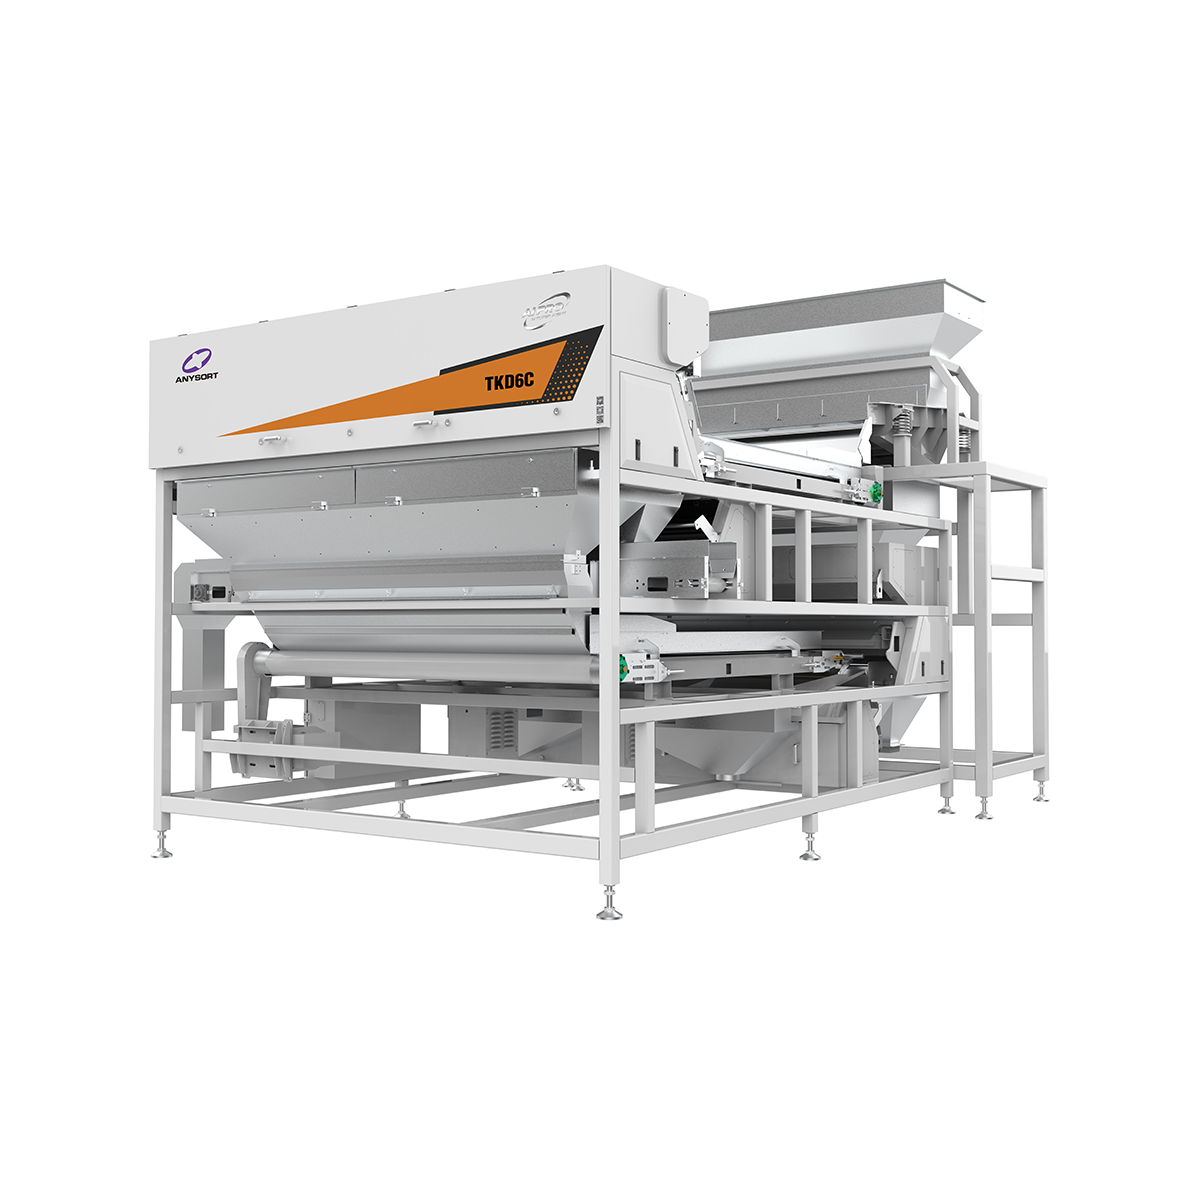
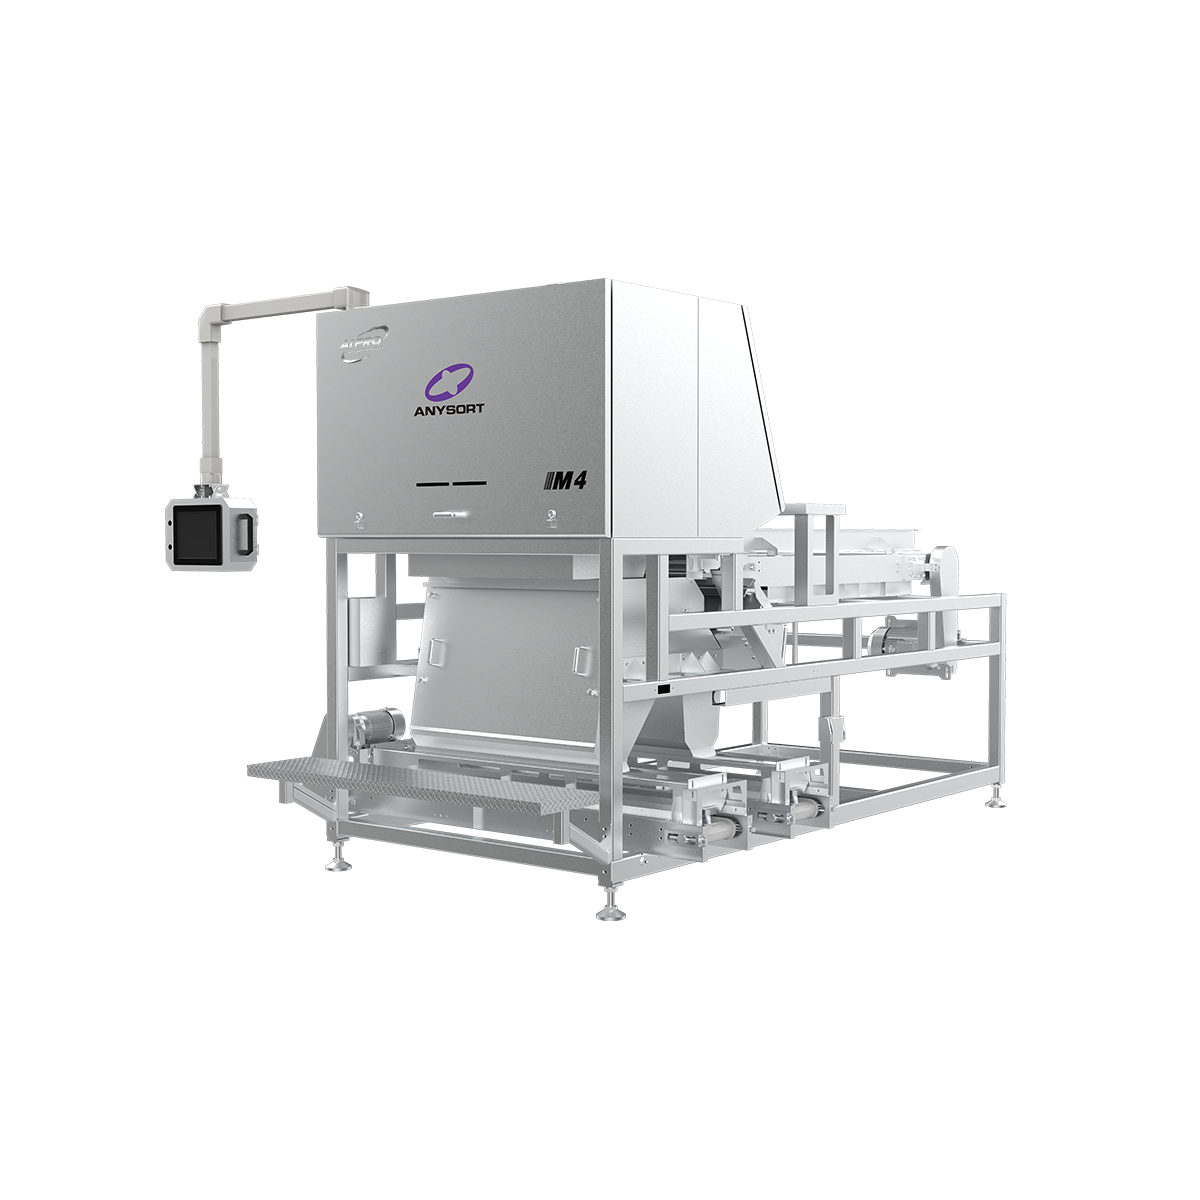
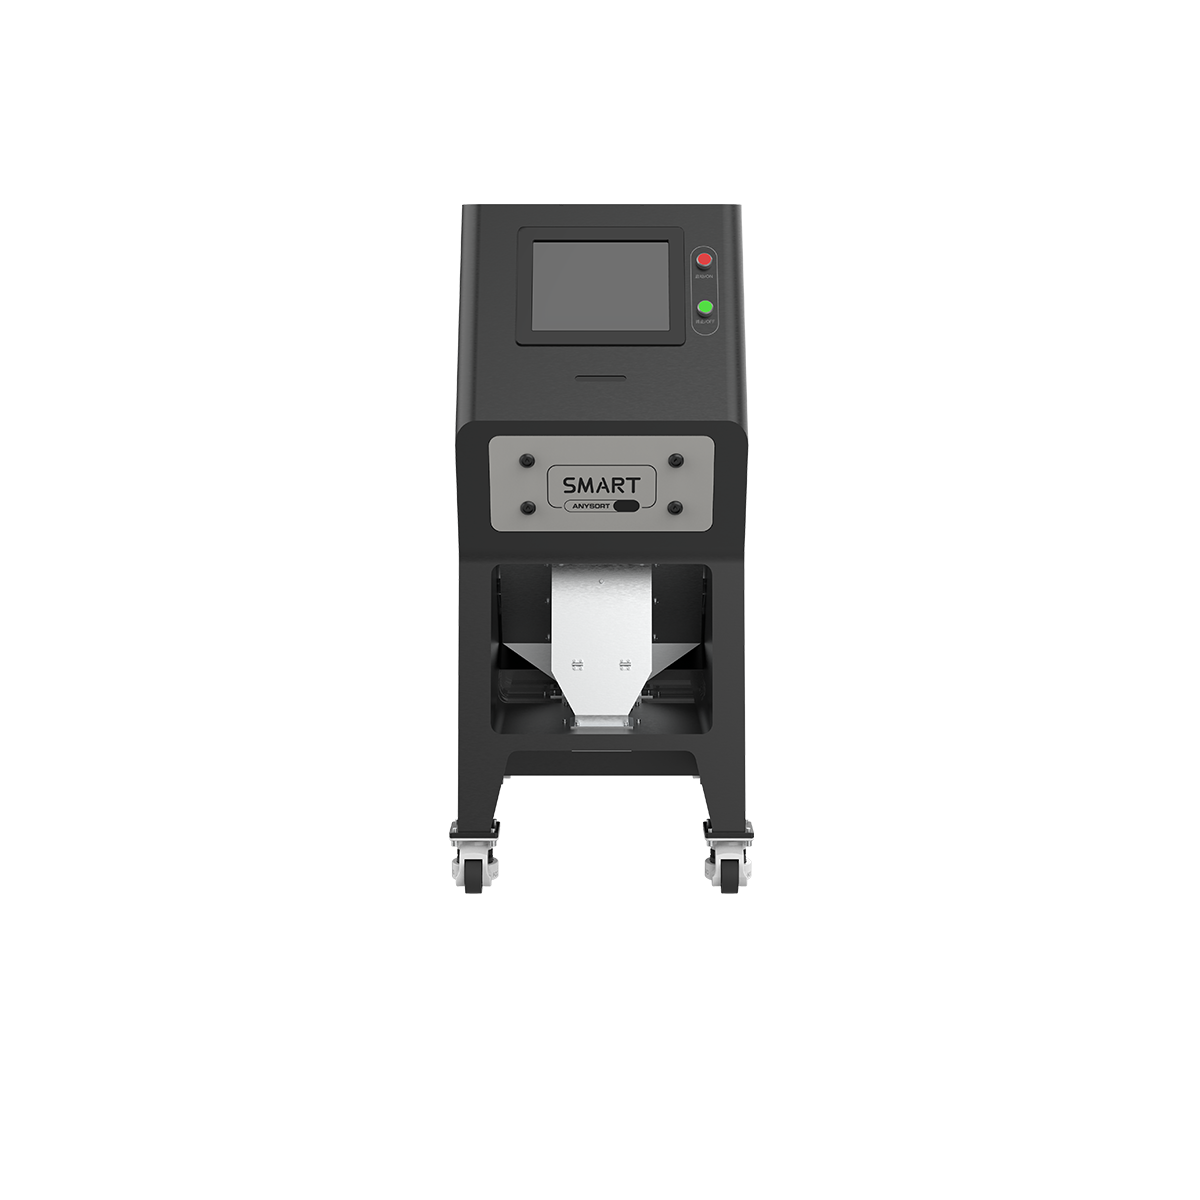
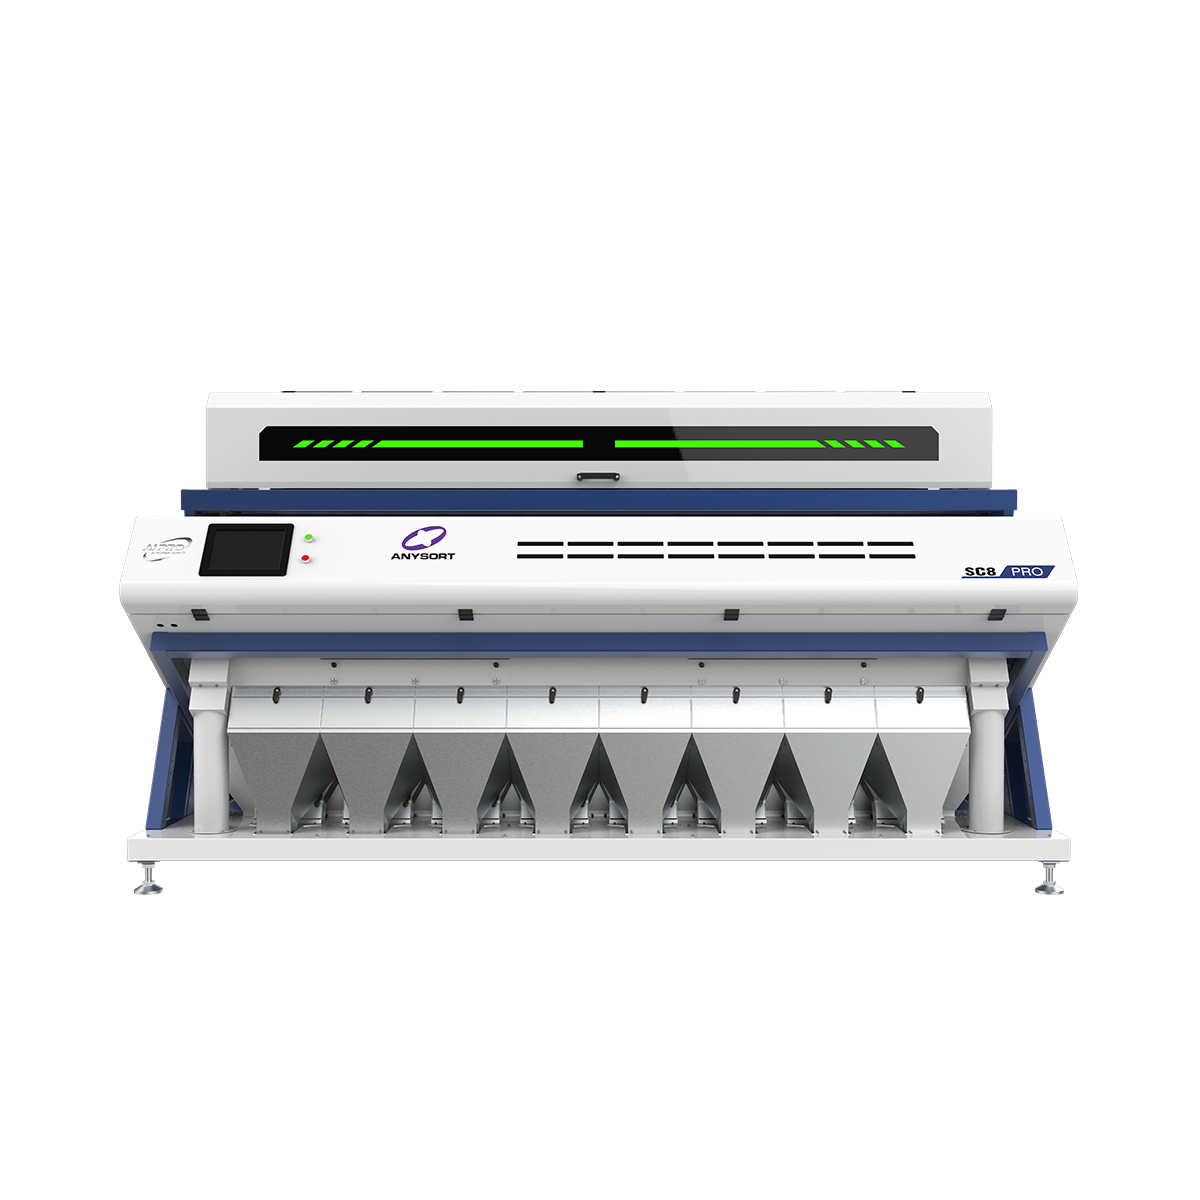
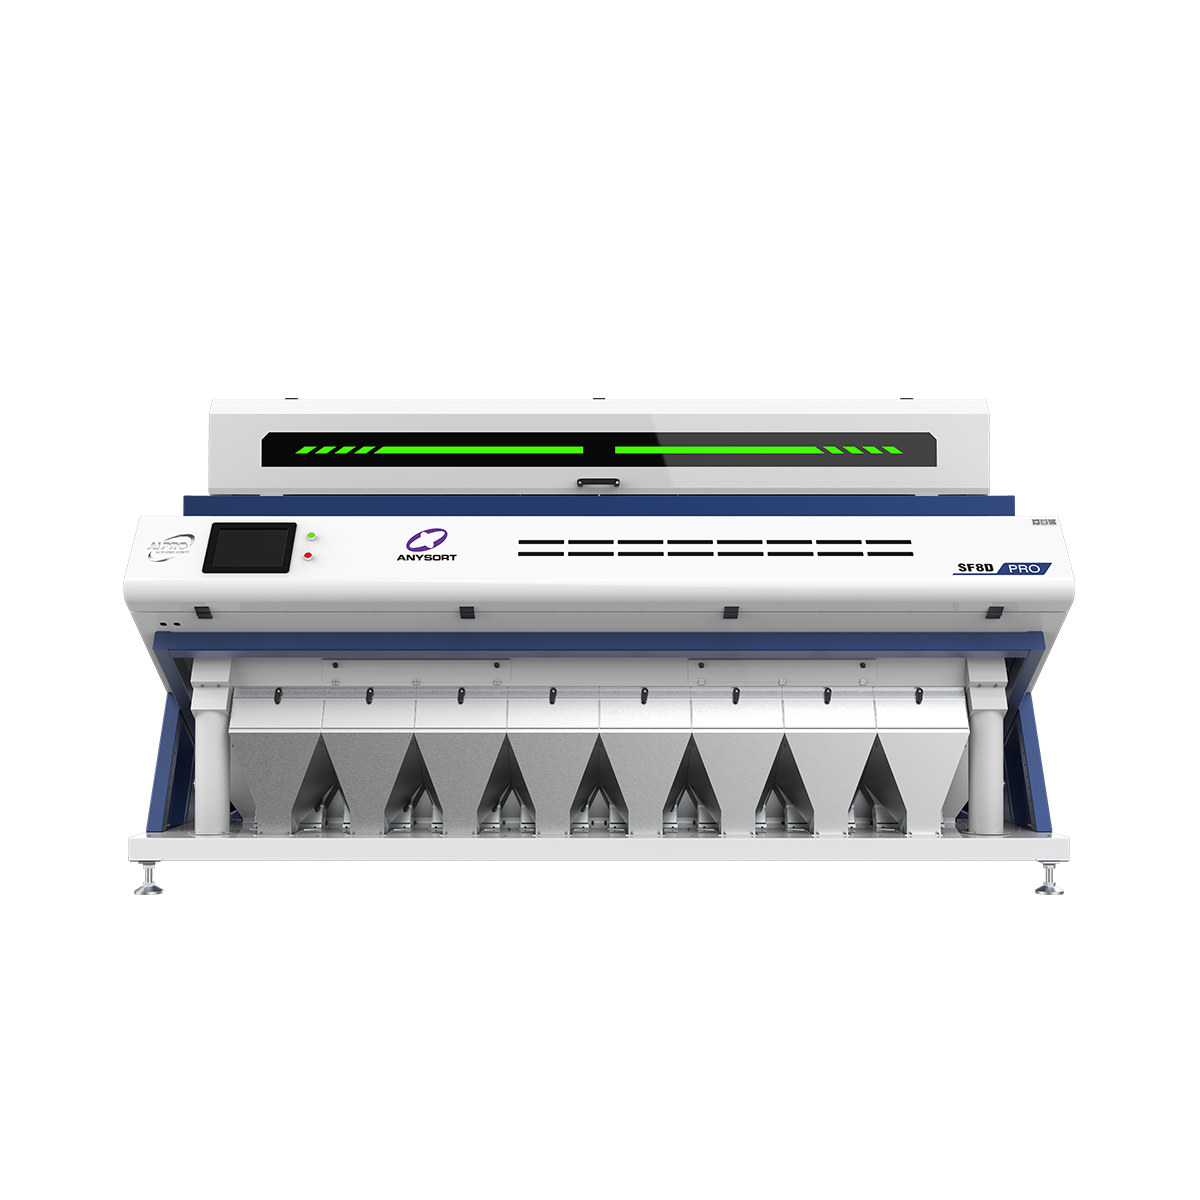
A color sorter is an advanced optical sorting machine designed to automatically separate and grade materials based on color differences and quality characteristics. This innovative equipment uses high-resolution cameras and sophisticated image processing technology to identify and remove defective items, foreign materials, and discolored particles from bulk materials with exceptional precision. The color sorter operates by capturing images of each particle as it passes through the sorting chamber, analyzing these images against predefined quality standards, and using pneumatic ejectors to divert unacceptable items into waste streams. Color sorter technology has revolutionized material processing across multiple industries by dramatically improving product quality while reducing manual labor costs. These machines can process hundreds of kilograms per hour, making them indispensable for high-volume operations. The color sorter employs advanced sensors that detect minute color variations invisible to the human eye, ensuring consistent quality control. Common applications include rice and grain processing, where the color sorter removes discolored kernels and foreign particles; plastic recycling, where it sorts different plastic types by color; and coffee bean processing, where it eliminates defective beans. Modern color sorter systems feature touchscreen interfaces, real-time monitoring capabilities, and data logging functions that allow operators to track sorting performance and adjust parameters instantly. The technology represents a significant investment in operational efficiency, delivering rapid return on investment through reduced waste, improved product consistency, and enhanced customer satisfaction. Whether processing agricultural commodities or recycled materials, the color sorter remains an essential component of modern production facilities.

 EN