Color Sorter Price: Quality Sorting Solutions

All Categories

color sorter price

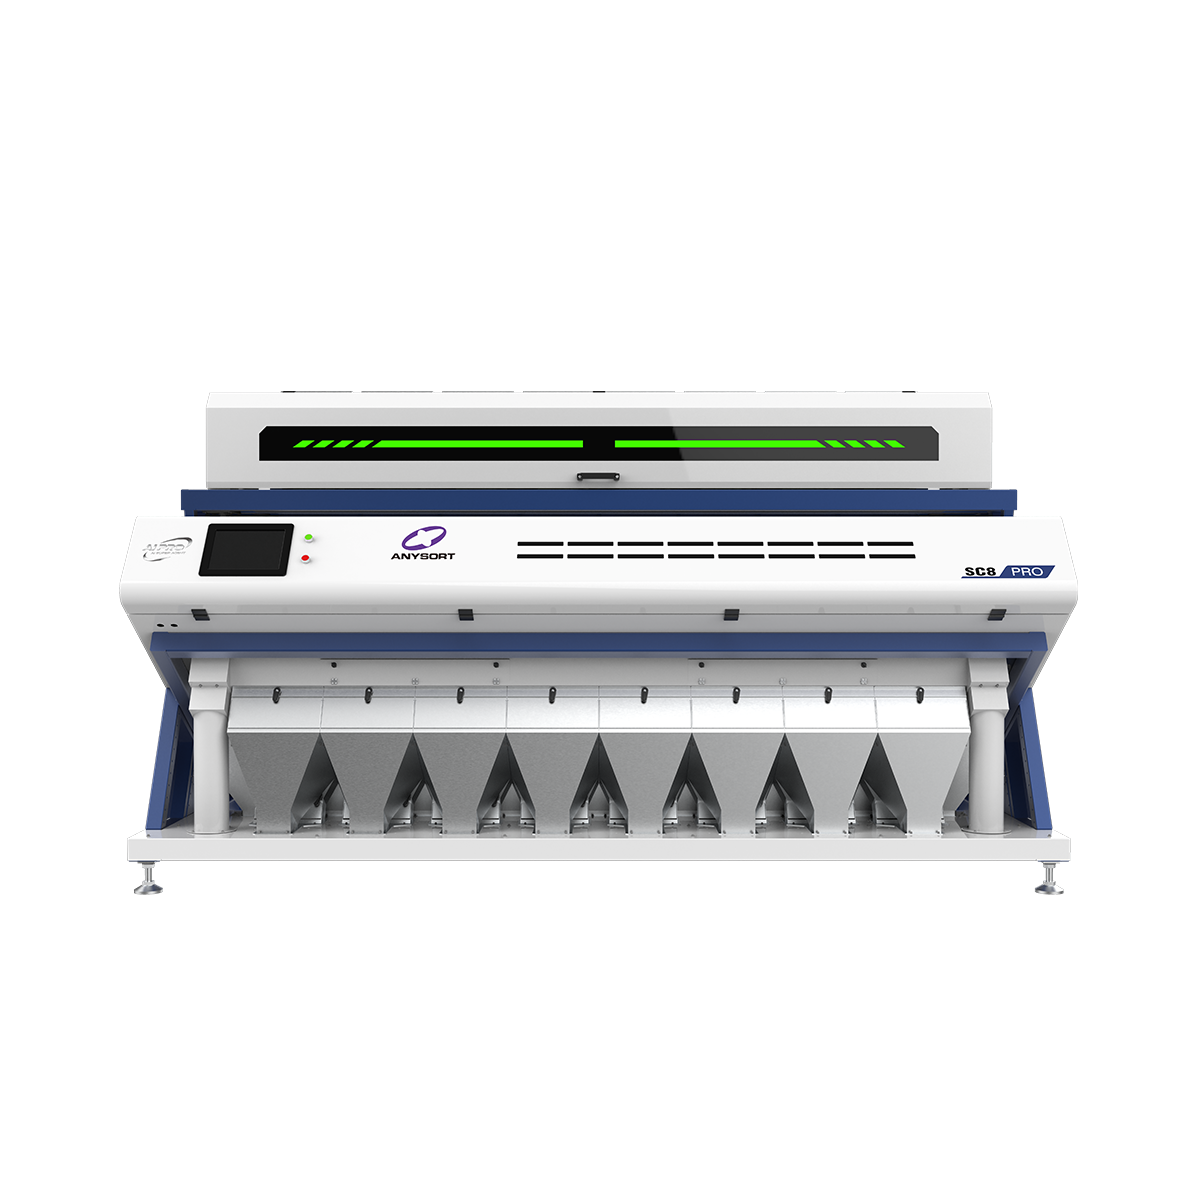
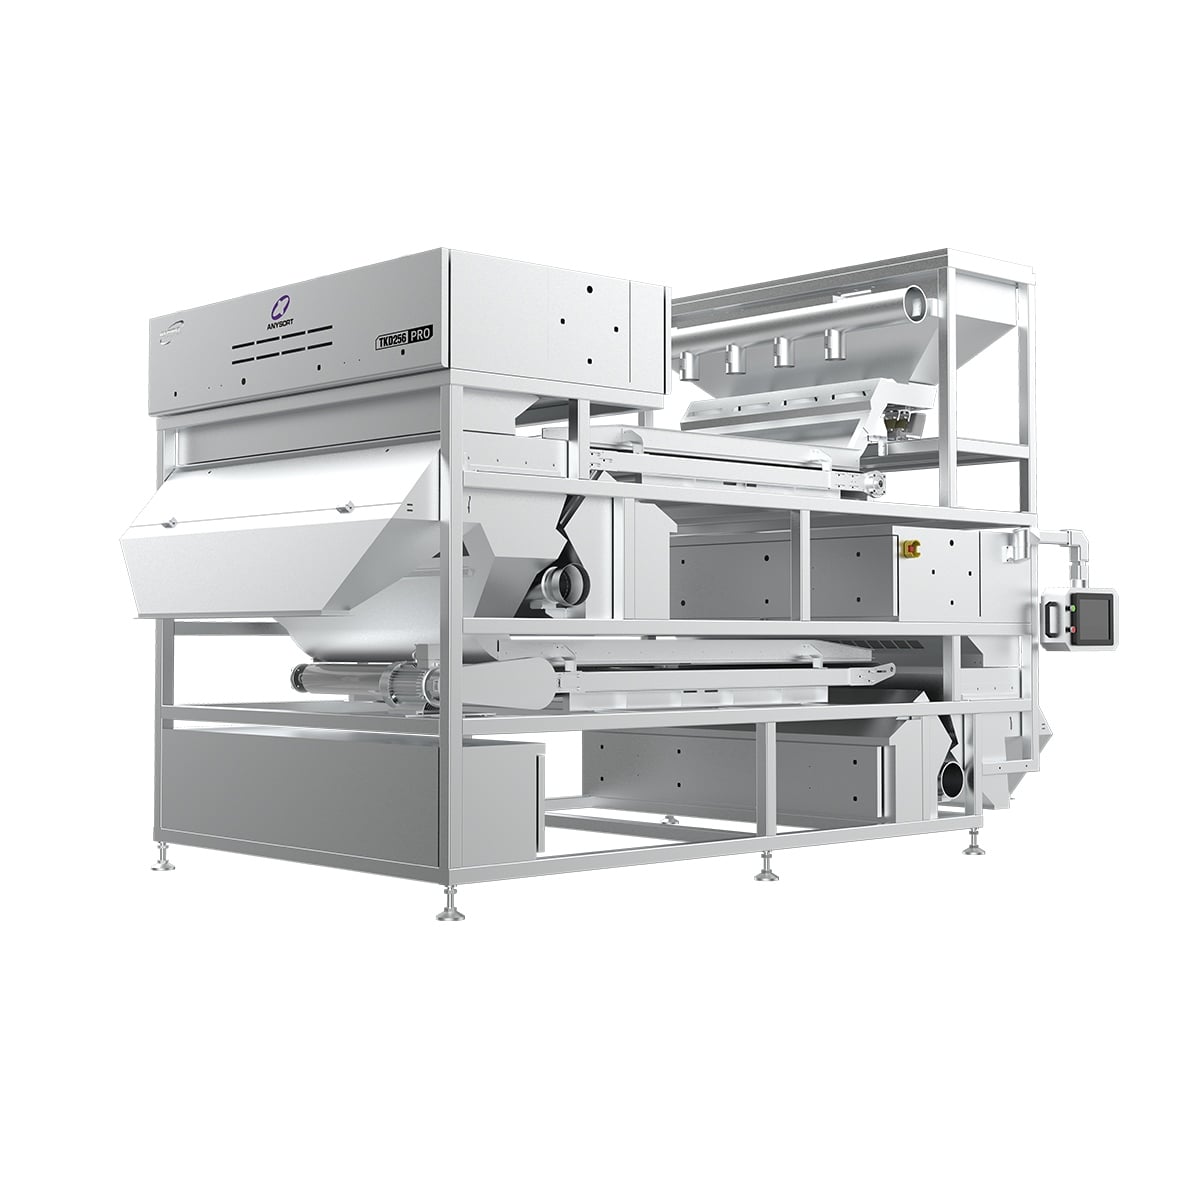
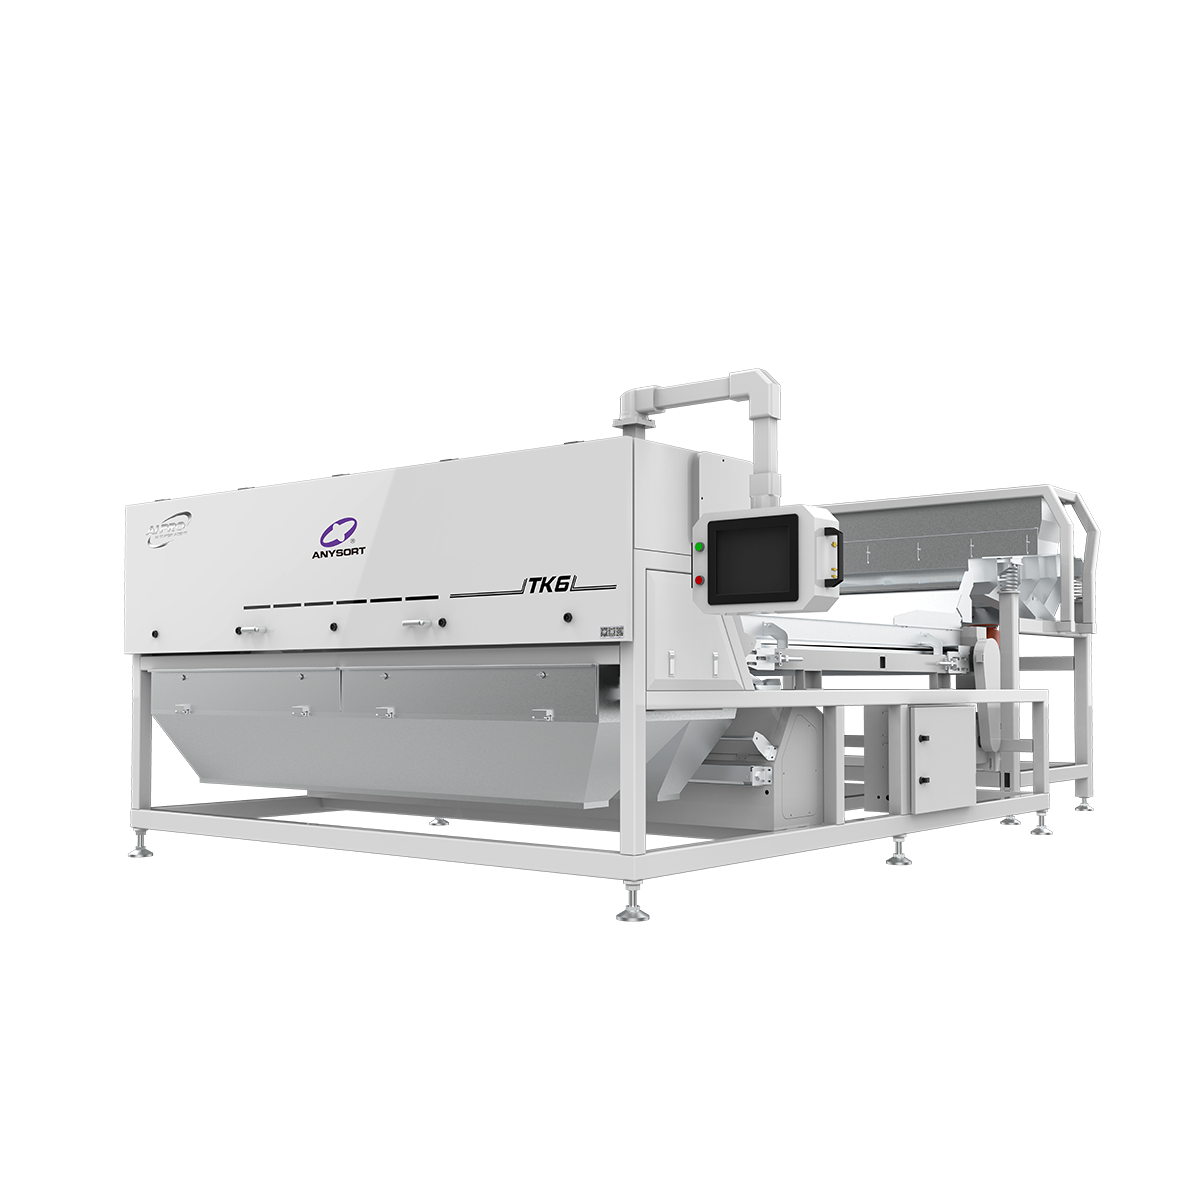
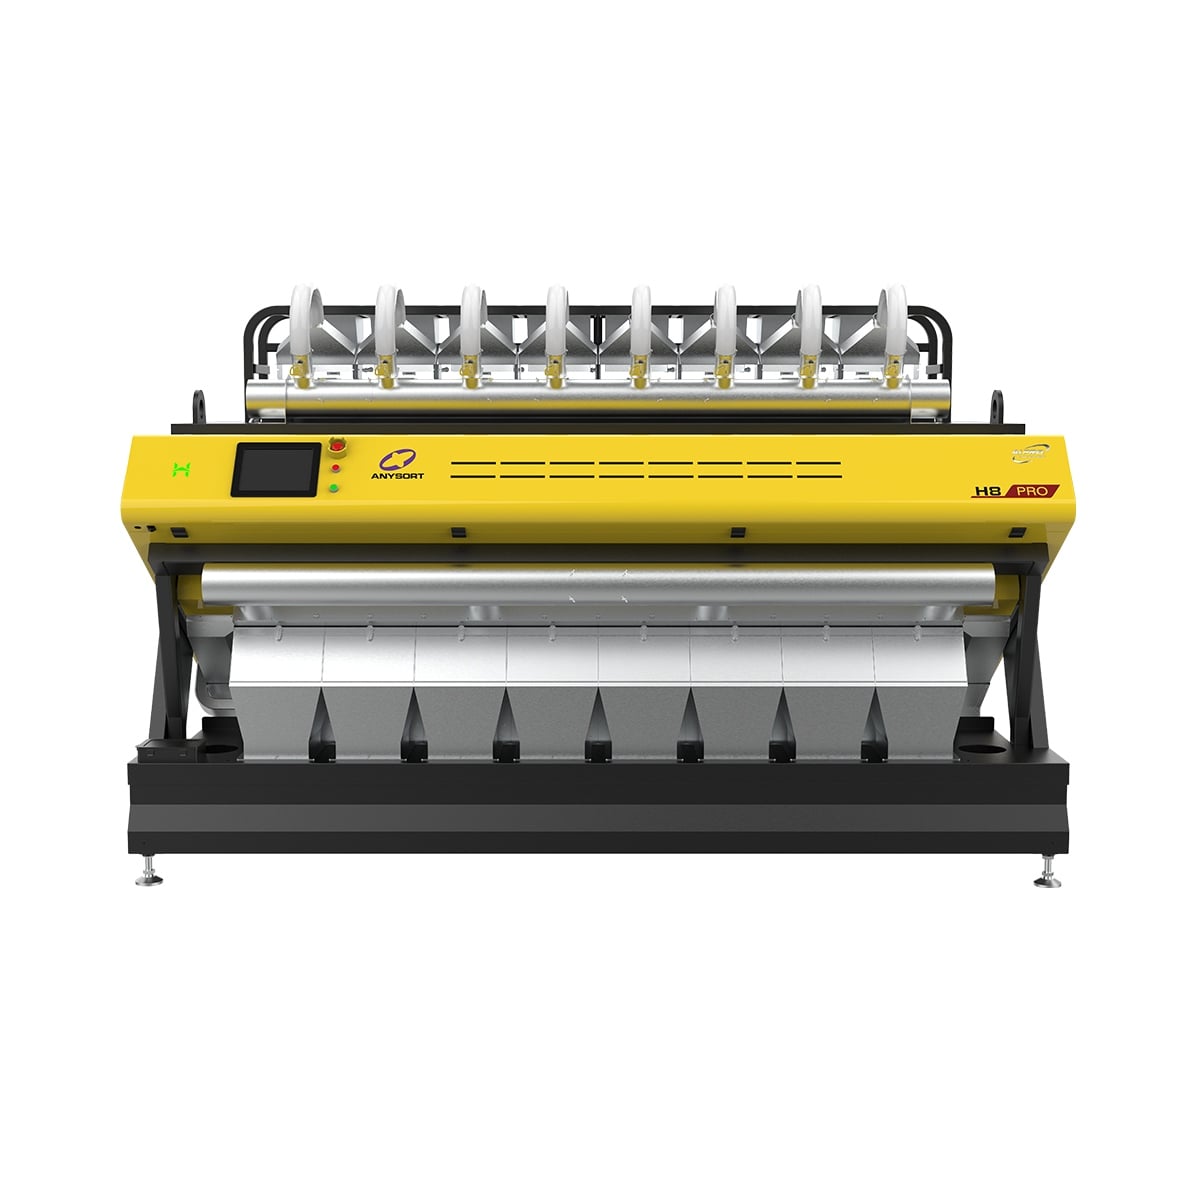
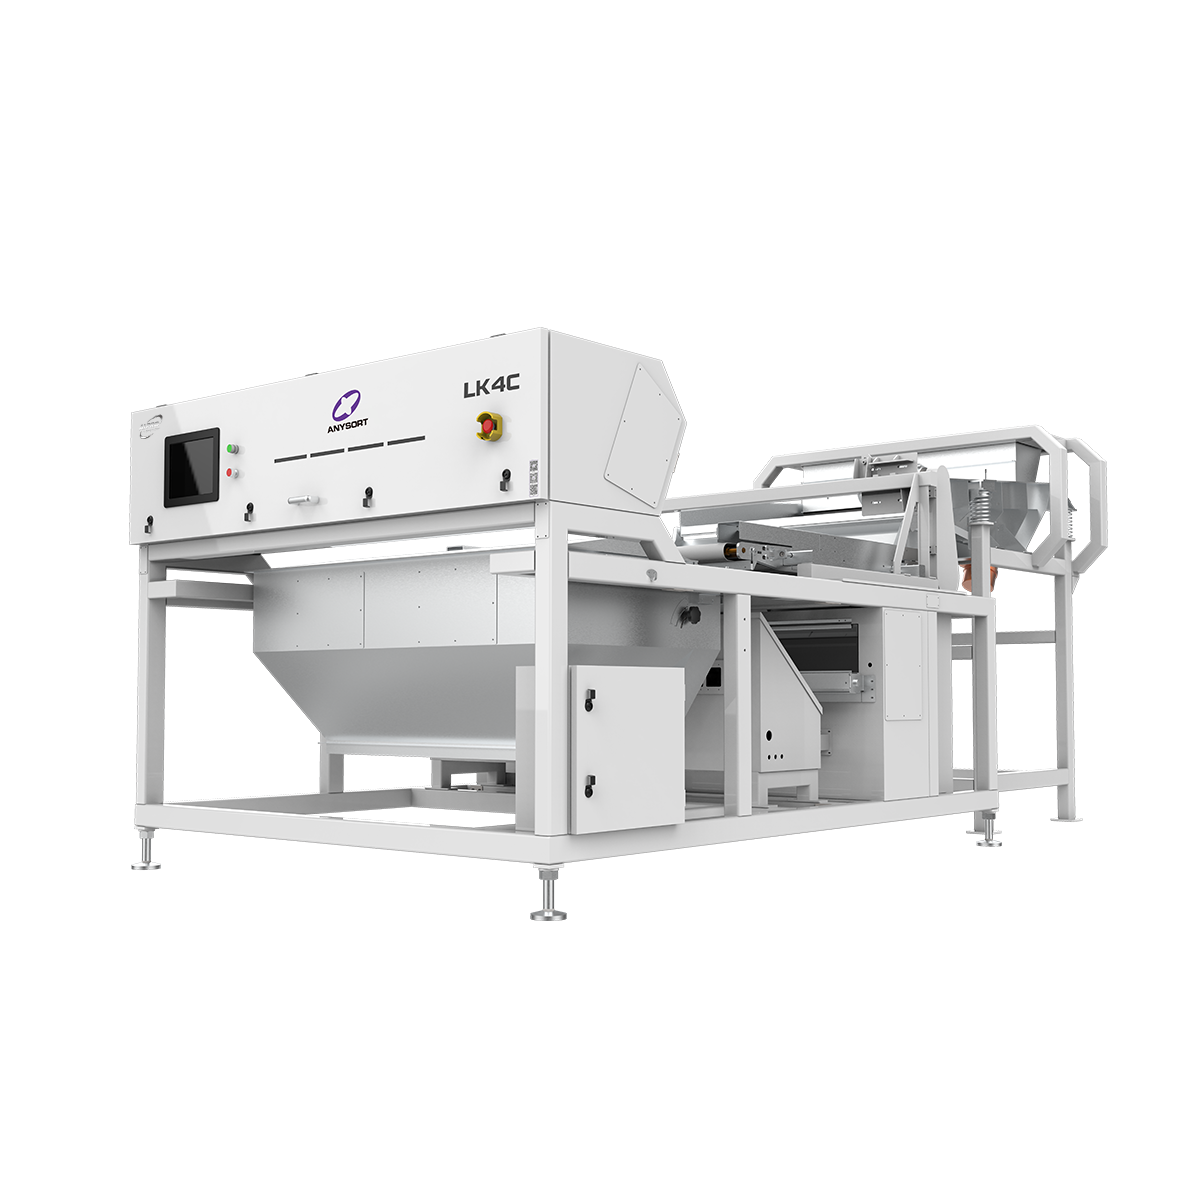
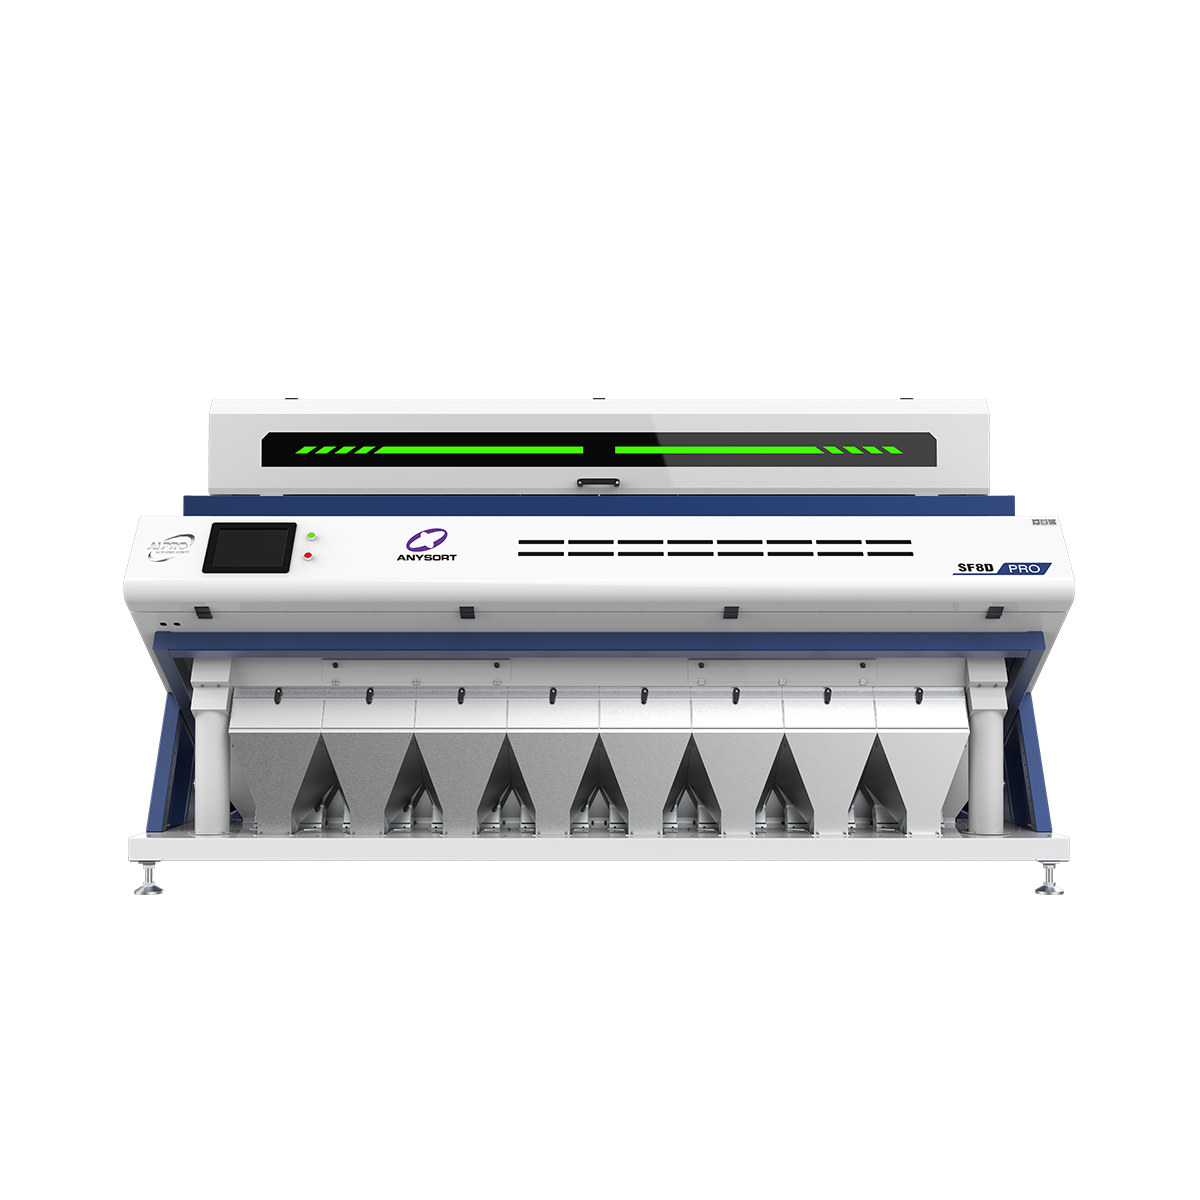
Color sorter price represents a crucial investment consideration for businesses seeking advanced grain and material sorting solutions. A color sorter is an automated optical machine that uses sophisticated imaging technology to identify and separate materials based on color characteristics, making it indispensable in food processing, recycling, and agricultural industries. Understanding color sorter price helps buyers make informed purchasing decisions that align with their operational needs and budget constraints. Modern color sorter price structures reflect the advanced technological features embedded within these machines. High-speed cameras capture thousands of images per second, while artificial intelligence algorithms analyze each particle's color profile with remarkable precision. The ejection mechanism uses compressed air to remove defective items at incredible velocities, ensuring contamination-free end products. Color sorter price variations depend on sorting capacity, which ranges from several tons per hour to industrial-scale operations processing hundreds of tons daily. The practical applications justifying color sorter price investments span multiple industries. In rice processing facilities, color sorters eliminate discolored grains and foreign materials. Coffee processors rely on color sorter technology to achieve consistent bean quality. Plastic recycling operations use color sorters to separate materials by type and shade. Nut and seed producers implement color sorter solutions to guarantee product uniformity and safety. Each application demonstrates why understanding color sorter price represents essential business knowledge for procurement professionals and facility managers seeking efficiency improvements and quality assurance.

New Product Releases

Investing in a color sorter price-appropriate system delivers substantial operational benefits that justify the capital expenditure through measurable returns. The primary advantage centers on dramatic quality improvement—color sorters eliminate defective materials with accuracy exceeding ninety-five percent, ensuring only premium products reach customers. This quality consistency strengthens brand reputation and reduces liability concerns associated with contaminated shipments. Operational efficiency gains represent another compelling reason to evaluate color sorter price investments carefully. These machines process materials continuously at high speeds without fatigue, dramatically increasing throughput compared to manual sorting methods. Labor cost reductions follow naturally, as one color sorter replaces multiple workers while maintaining superior accuracy. Companies report productivity increases of three hundred to five hundred percent after color sorter implementation, making the color sorter price easily recoverable within months of operation. The versatility factor significantly impacts long-term color sorter price value. Modern systems handle diverse materials—grains, legumes, nuts, coffee beans, plastic pellets, and recycled materials—requiring only software adjustments between applications. This flexibility enables businesses to maximize equipment utilization across multiple product lines, spreading the initial color sorter price investment across various revenue streams. Maintenance advantages further strengthen the color sorter price proposition. Contemporary systems feature self-diagnostic capabilities that identify wear patterns before failures occur, minimizing unexpected downtime. The machines operate with minimal moving parts compared to mechanical alternatives, reducing maintenance expenses significantly. Environmental benefits emerge as well, since color sorters eliminate chemical-based sorting methods while reducing waste streams. When evaluating color sorter price options, these operational advantages combine to create compelling financial justification for technology adoption, ensuring businesses achieve superior returns on their sorting equipment investments.

Practical Tips

How Much Does a Color Sorter Machine Cost?

12

Aug

How Much Does a Color Sorter Machine Cost?

Understanding the investment required for a color sorter machine is essential for businesses in agriculture, food processing, and recycling sectors. The cost of a color sorter machine varies significantly based on capacity, technology sophistication,...
View More
How Can a Nuts Sorter Improve Your Production?

15

Aug

How Can a Nuts Sorter Improve Your Production?

A nuts sorter represents one of the most significant investments a food processing operation can make to enhance production quality and operational efficiency. The modern nuts sorter uses advanced imaging and sensor technology to identify and separat...
View More
How does optical sorting technology detect defective rice grains?

22

Aug

How does optical sorting technology detect defective rice grains?

Modern rice processing demands precision and consistency, which is why understanding the detection mechanisms behind advanced equipment has become essential for producers. A rice color sorter represents one of the most significant technological break...
View More
Which factors should you consider when selecting a rice color sorter?

29

Aug

Which factors should you consider when selecting a rice color sorter?

Selecting the right rice color sorter is a critical decision that directly impacts your grain processing efficiency, product quality, and long-term profitability. A rice color sorter removes discolored, damaged, and foreign particles from rice batche...
View More

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

color sorter price

Precision Sorting Technology That Maximizes Color Sorter Price Value

Precision Sorting Technology That Maximizes Color Sorter Price Value

Advanced optical recognition systems represent the core technology justifying color sorter price investments. These machines employ multiple high-resolution cameras positioned at various angles to capture comprehensive product imaging data. Sophisticated spectral analysis capabilities distinguish subtle color variations invisible to human eyes, enabling detection of defects, discoloration, and foreign materials with exceptional precision. The color sorter price reflects integration of cutting-edge sensor arrays that function reliably across different lighting conditions and material types. Real-time image processing occurs at remarkable speeds—analyzing thousands of particles per second—ensuring zero production lag. Machine learning algorithms continuously improve detection accuracy by learning from sorted materials, making the color sorter price increasingly valuable over time. This technological sophistication transforms waste reduction into measurable cost savings, directly offsetting the initial color sorter price while delivering consistent quality outcomes that manual sorting cannot achieve.
High-Capacity Processing Justifying Color Sorter Price Investment

High-Capacity Processing Justifying Color Sorter Price Investment

Throughput capacity significantly influences color sorter price comparisons and purchasing decisions. Contemporary models process between five and one hundred tons per hour, depending on configuration and material type. This exceptional processing speed means businesses can sort massive volumes without requiring extended operational hours or weekend shifts. The color sorter price correlates directly with capacity specifications, with industrial-grade systems commanding premium pricing justified by superior production volumes. Modular designs enable businesses to start with smaller capacity units and scale upward as demand increases, optimizing the color sorter price relative to actual processing requirements. High-capacity operations dramatically reduce per-unit sorting costs, making the color sorter price economically attractive even for smaller businesses. Advanced conveyor integration ensures seamless material flow, preventing bottlenecks that would compromise throughput. Companies implementing high-capacity color sorters report production increases exceeding previous manual sorting achievements by remarkable margins, confirming that paying a higher color sorter price for capacity delivers substantial operational advantages.
Durability and Reliability Features Supporting Color Sorter Price ROI

Durability and Reliability Features Supporting Color Sorter Price ROI

Industrial-grade construction ensures color sorters justify their price through years of dependable performance. Premium materials resist corrosion, dust accumulation, and material abrasion that plague sorting equipment in demanding environments. Sealed optical components protect sensitive cameras and sensors from contamination, while robust ejection mechanisms withstand continuous operation without degradation. The color sorter price reflects engineering standards designed for twenty-four-hour operation in harsh processing facilities. Preventive maintenance protocols minimize unexpected failures that would disrupt production schedules and compromise profitability. Comprehensive warranty coverage and readily available spare parts support long-term equipment reliability. Manufacturers design color sorters for lifespan extending ten to fifteen years, meaning the color sorter price amortizes across thousands of operational hours. Built-in redundancy systems ensure continued functionality even when individual components require servicing. This emphasis on durability transforms the color sorter price from a mere equipment cost into a long-term productivity investment that consistently delivers reliable performance across varied processing environments and challenging operational conditions.

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

Copyright © 2026 Anhui Jiexun Optoelectronic Technology Co., Ltd. All rights reserved.  -  Privacy policy