Cashew Kernel Grading Machine for Quality Sorting

All Categories

cashew kernel grading machine

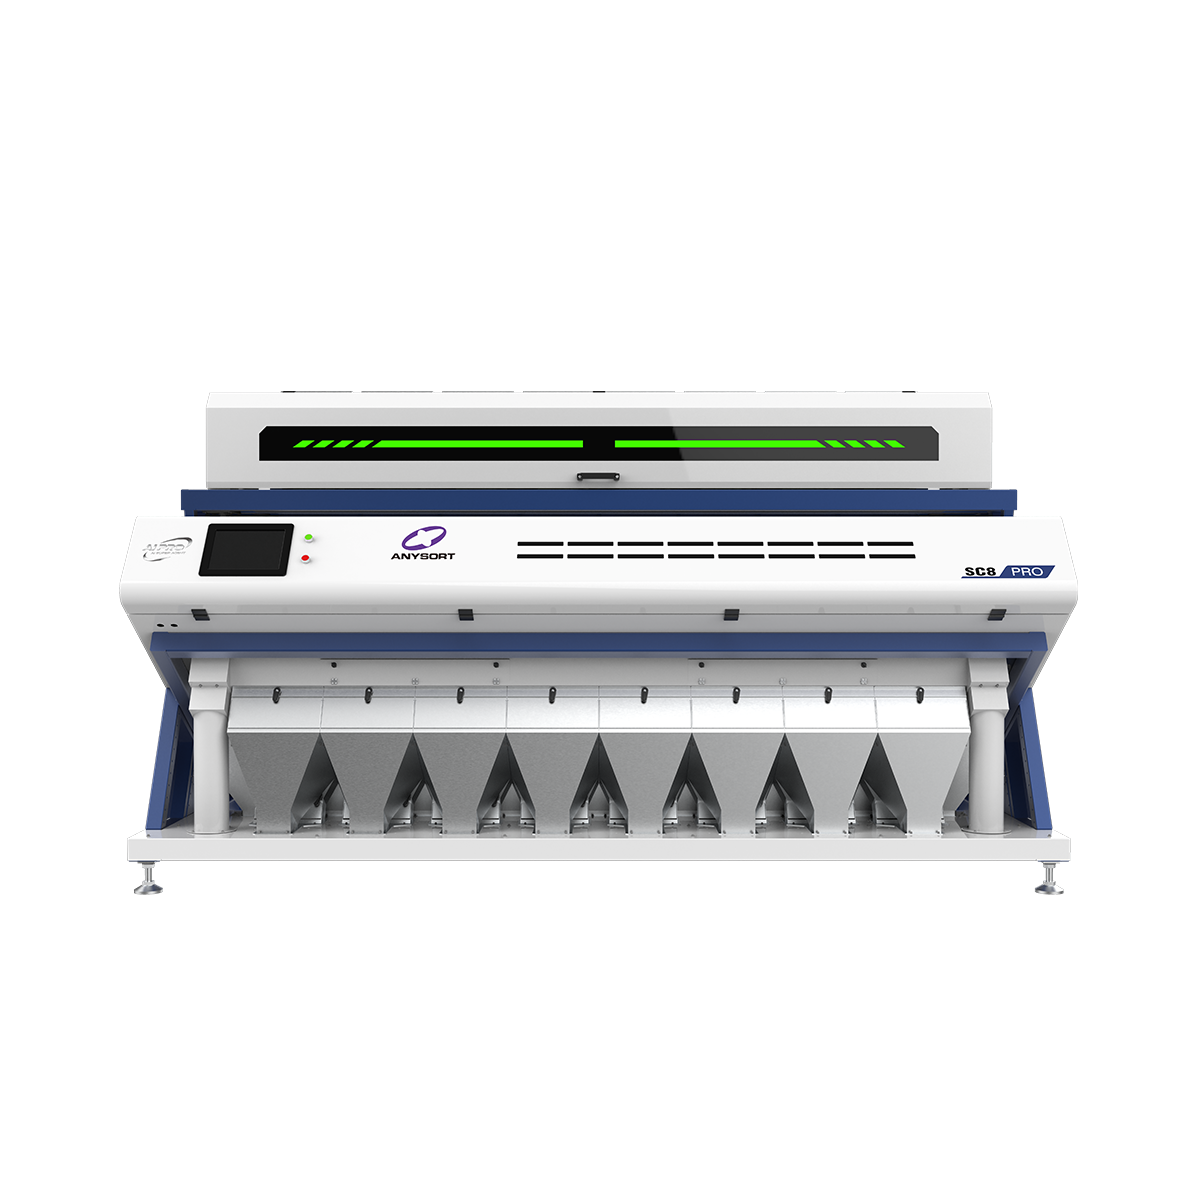
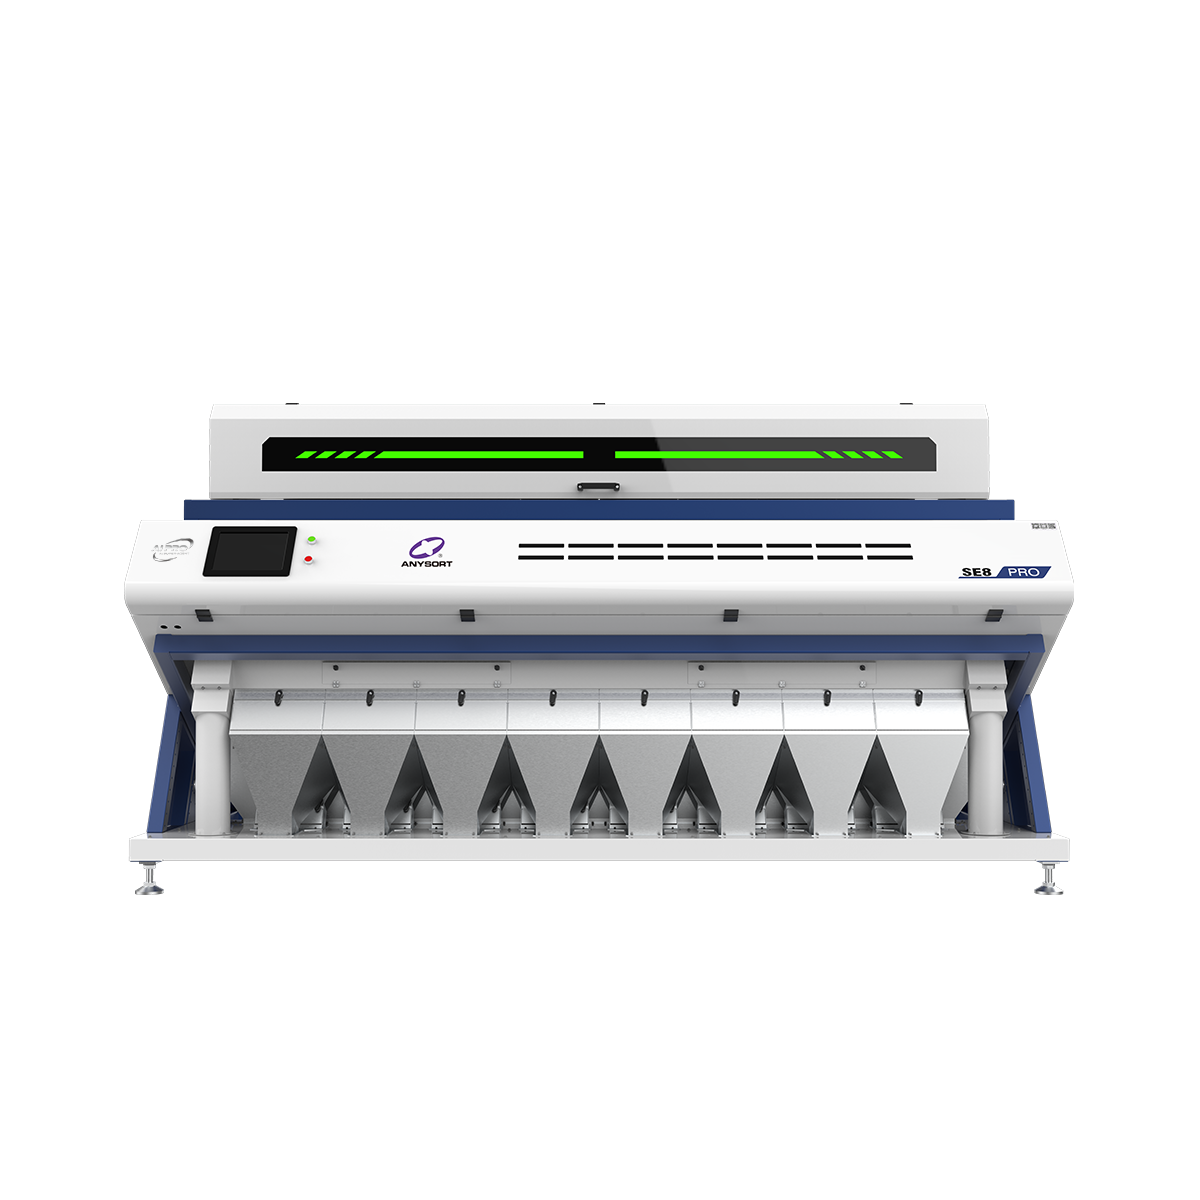
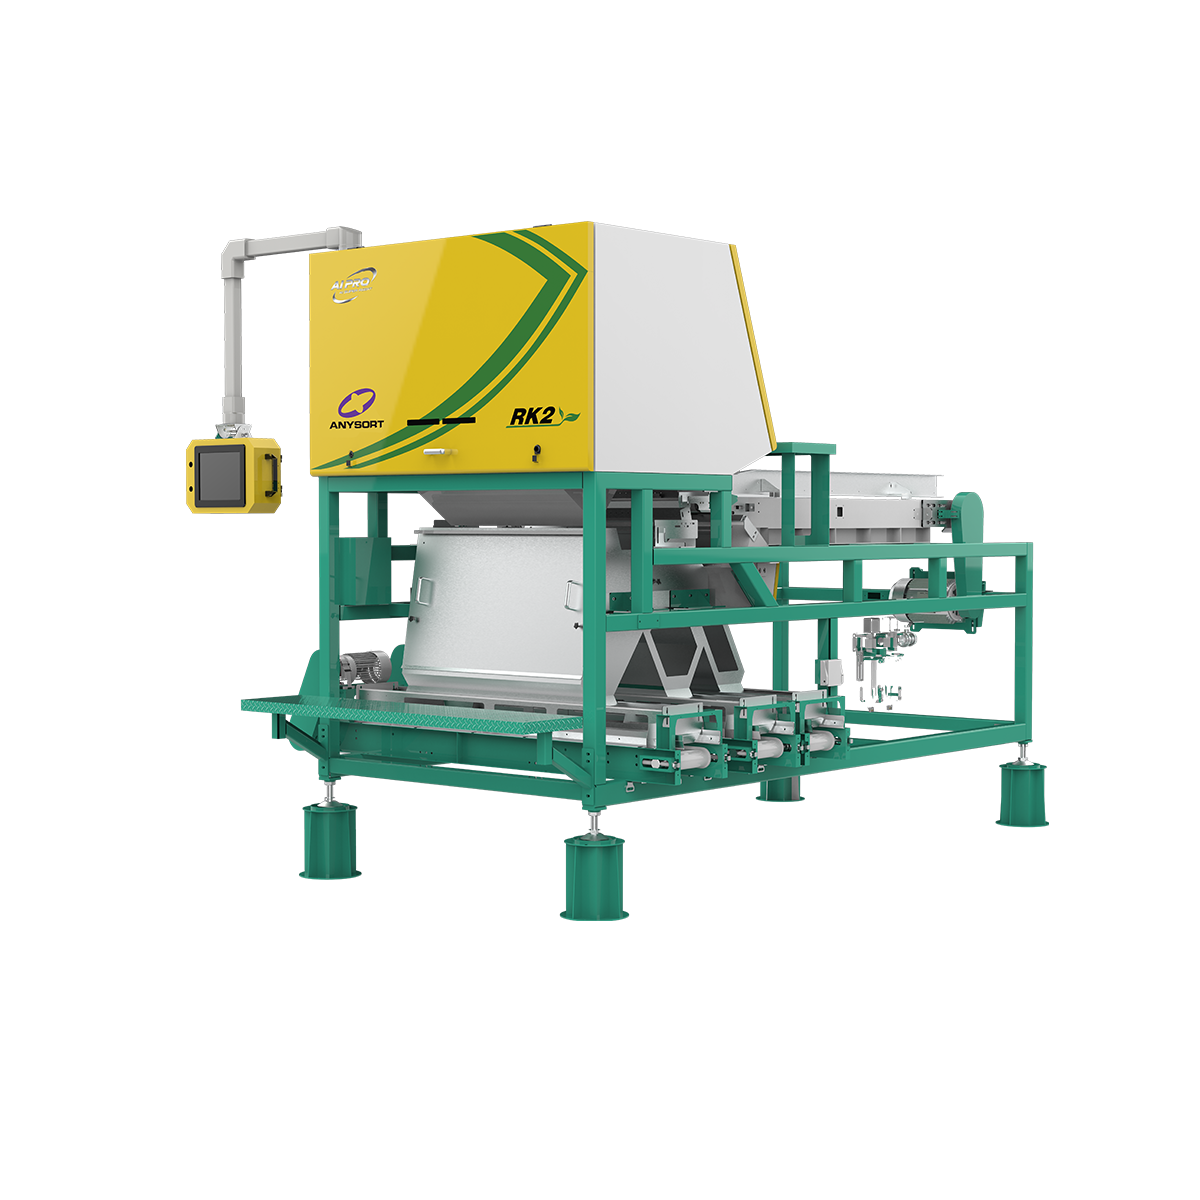
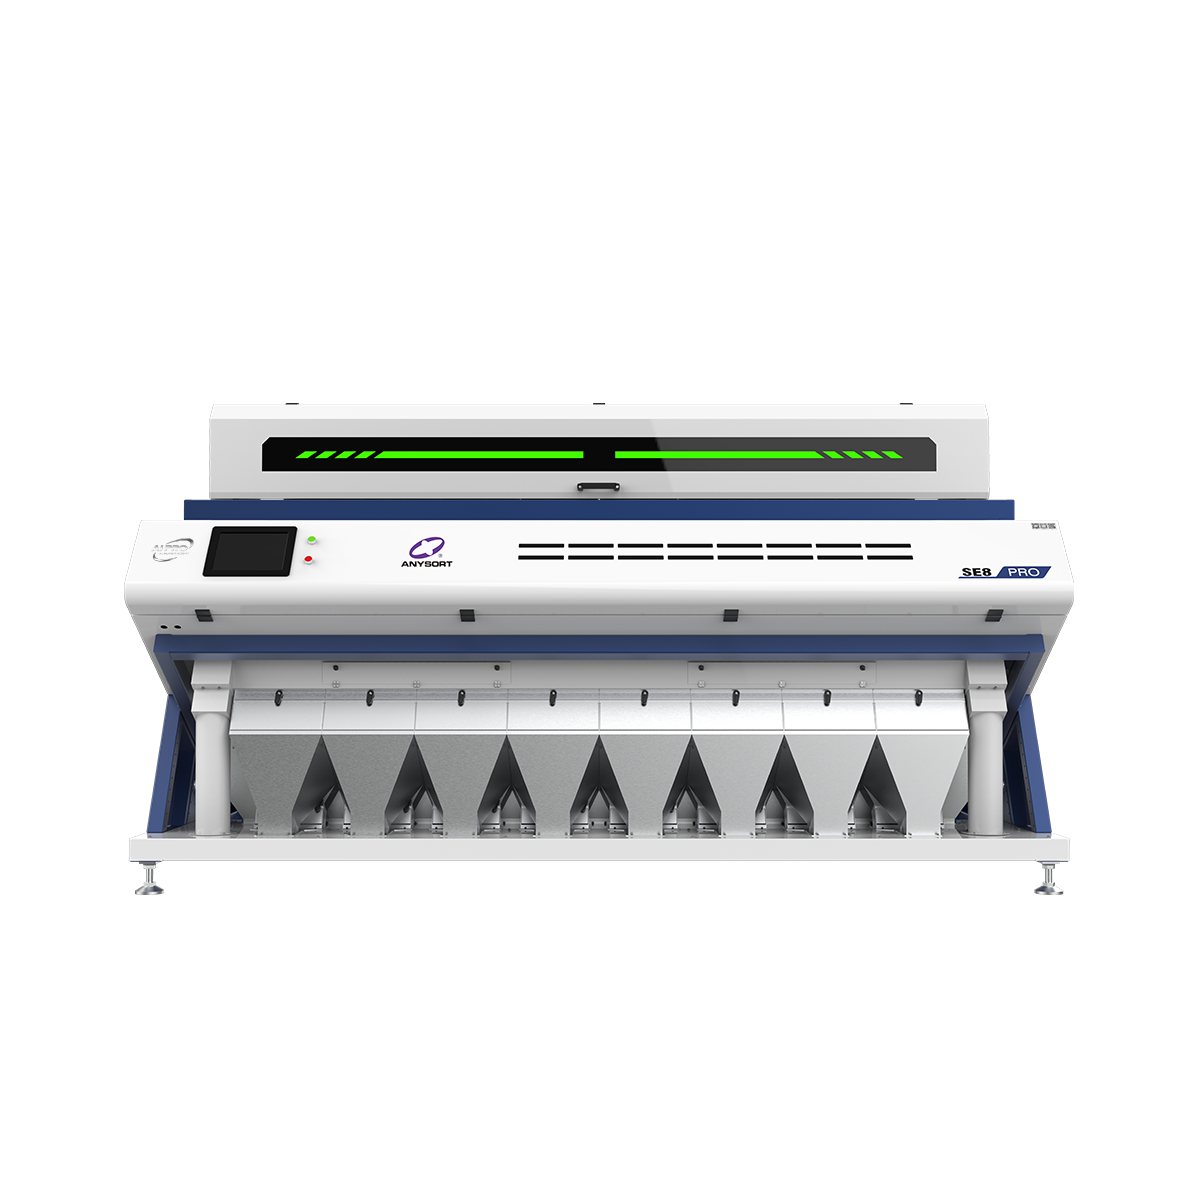
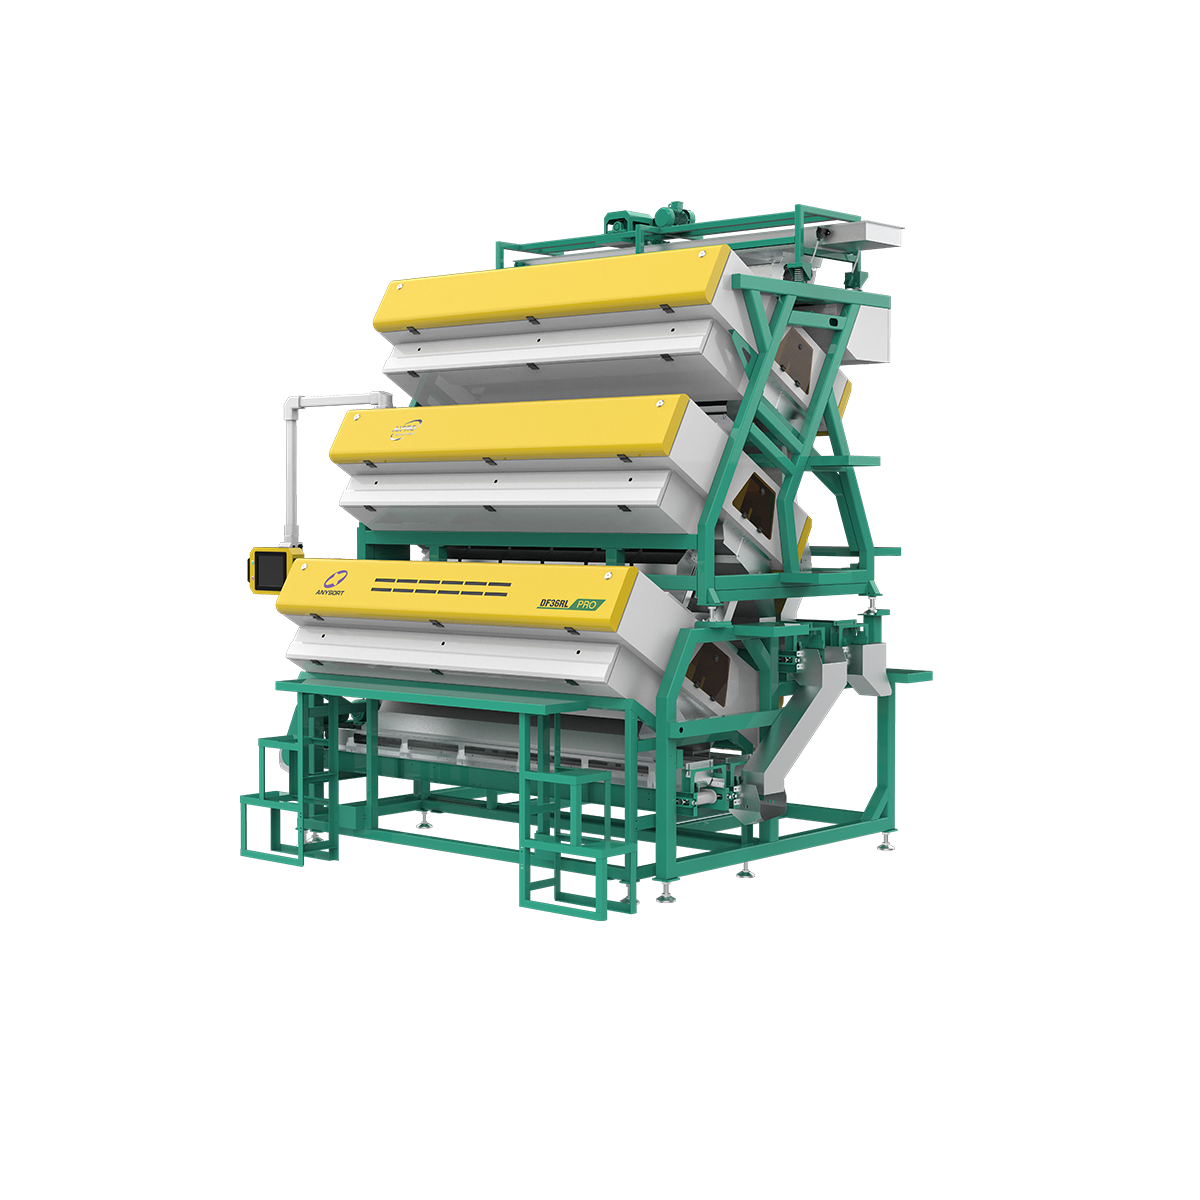
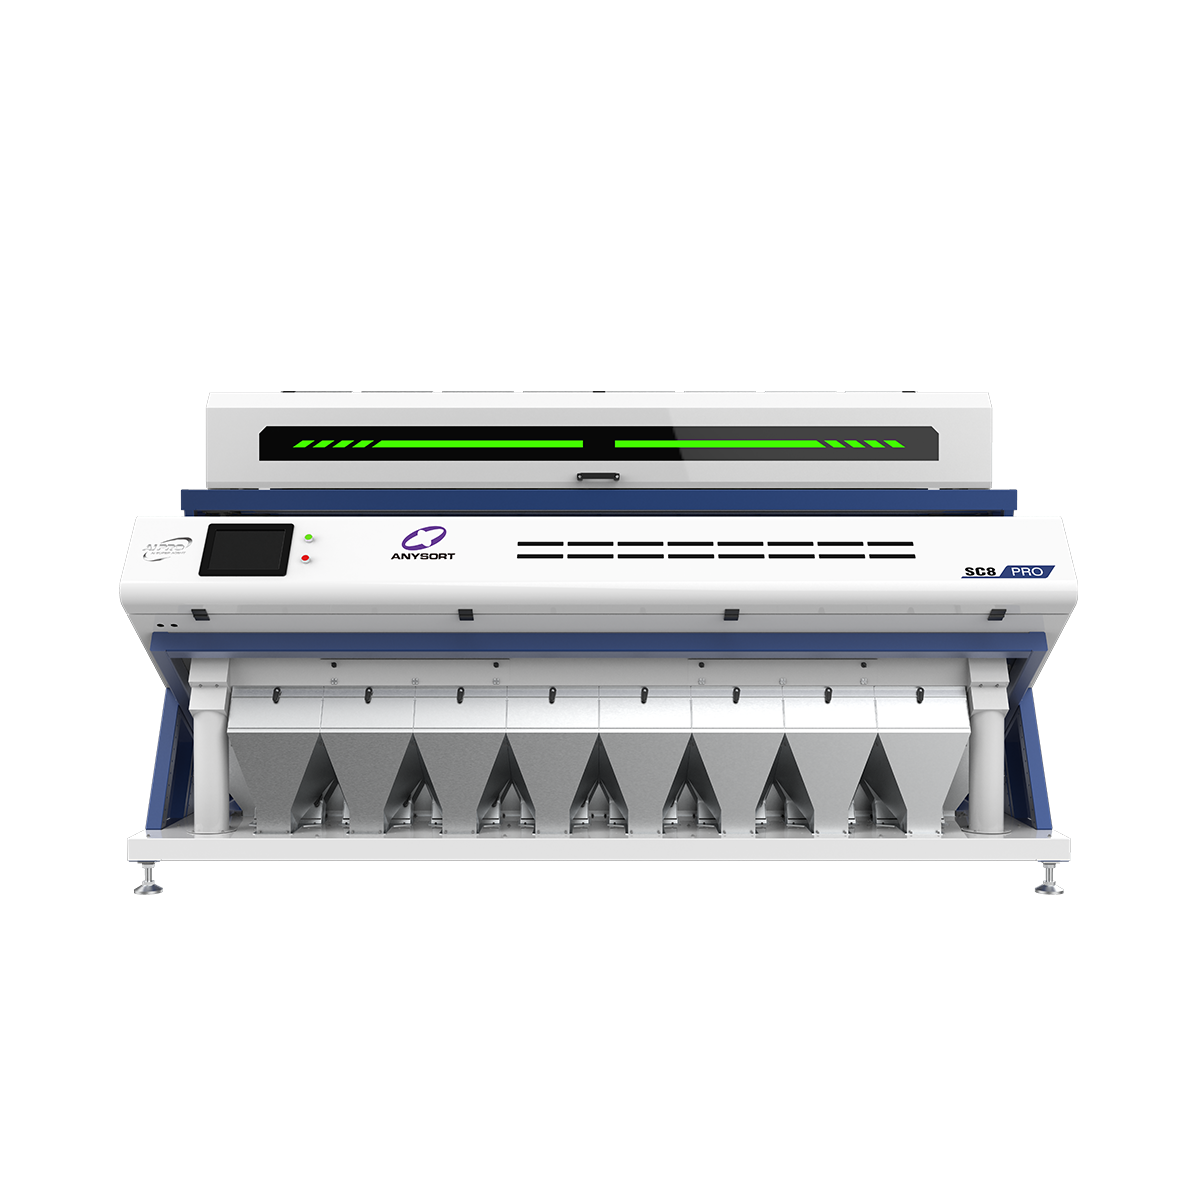
A cashew kernel grading machine is an advanced automated system designed to sort and classify cashew kernels based on size, quality, and condition. This specialized equipment plays a crucial role in cashew processing facilities worldwide, ensuring consistent product standards and maximizing yield efficiency. The cashew kernel grading machine utilizes sophisticated optical sensors and precise mechanical mechanisms to evaluate each kernel individually, separating them into distinct categories for different market demands. The primary function of a cashew kernel grading machine is to eliminate defective, discolored, or undersized kernels while organizing acceptable products into uniform grades. Modern cashew kernel grading machines employ multi-dimensional scanning technology that detects surface imperfections, moisture content variations, and dimensional inconsistencies with remarkable accuracy. These machines can process hundreds of kilograms per hour, significantly reducing manual labor requirements and human error in the sorting process. Technological features of contemporary cashew kernel grading machines include intelligent sorting algorithms, real-time quality monitoring systems, and customizable grading parameters. The equipment integrates seamlessly with existing production lines, featuring user-friendly control panels and automated data logging capabilities. Applications span commercial cashew processing operations, export-oriented facilities, and large-scale agricultural enterprises seeking premium product consistency and enhanced market competitiveness through reliable cashew kernel grading machine technology.

New Product Releases

The cashew kernel grading machine delivers substantial operational and economic benefits to processing facilities and businesses handling cashew products. First, this equipment dramatically increases sorting accuracy and efficiency compared to manual grading methods, reducing labor costs while improving product consistency and meeting strict international quality standards. Operators can process significantly larger quantities daily, transforming production capacity and enabling facilities to fulfill larger orders reliably. Implementing a cashew kernel grading machine minimizes product waste by identifying marginal kernels that manual workers might overlook or misclassify. This precision directly impacts profitability, as proper grading ensures premium kernels command higher market prices while lower-grade materials find appropriate secondary markets. The machine's automated approach eliminates subjective human judgment, guaranteeing standardized results across every production batch, which builds customer confidence and strengthens brand reputation. Operational benefits include reduced employee fatigue and injury risks associated with repetitive manual sorting tasks. The cashew kernel grading machine operates continuously throughout production shifts, maintaining consistent performance without performance degradation. Facility managers gain valuable data insights through built-in tracking systems that monitor production metrics, quality distributions, and equipment performance. The cashew kernel grading machine proves particularly suitable for export-focused operations where international buyers demand rigid quality specifications and traceability documentation. Businesses experience faster return on investment through improved efficiency and reduced material losses. Enhanced product consistency opens opportunities for premium market positioning and long-term customer contracts, ultimately strengthening competitive advantage in the global cashew market.

Latest News

How Can a Nuts Sorter Improve Your Production?

15

Aug

How Can a Nuts Sorter Improve Your Production?

A nuts sorter represents one of the most significant investments a food processing operation can make to enhance production quality and operational efficiency. The modern nuts sorter uses advanced imaging and sensor technology to identify and separat...
View More
How Does Nuts Sorter Technology Ensure Quality?

19

Aug

How Does Nuts Sorter Technology Ensure Quality?

The global nuts processing industry relies on precision and consistency to meet strict quality standards and regulatory requirements. A nuts sorter has become indispensable for processors seeking to eliminate defects, contaminants, and substandard pr...
View More
How Do Color Sorters Improve Product Quality?

26

Aug

How Do Color Sorters Improve Product Quality?

Product quality stands as a critical differentiator in competitive industrial markets, and achieving consistency at scale requires more than manual oversight. A color sorter represents one of the most effective technologies for identifying and removi...
View More
Which factors should you consider when selecting a rice color sorter?

29

Aug

Which factors should you consider when selecting a rice color sorter?

Selecting the right rice color sorter is a critical decision that directly impacts your grain processing efficiency, product quality, and long-term profitability. A rice color sorter removes discolored, damaged, and foreign particles from rice batche...
View More

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

cashew kernel grading machine

Advanced Optical Sorting Technology

Advanced Optical Sorting Technology

The cashew kernel grading machine incorporates cutting-edge optical scanning systems that analyze each kernel's surface characteristics with exceptional precision. High-resolution cameras capture detailed images while sophisticated software algorithms evaluate color consistency, surface texture, and physical defects simultaneously. This advanced cashew kernel grading machine technology detects minute imperfections invisible to human inspectors, ensuring only premium-quality kernels advance to packaging. The optical system operates at lightning-fast speeds, processing hundreds of kernels per minute without sacrificing accuracy. Facilities benefit from dramatically improved product quality consistency, as the machine applies identical evaluation standards throughout every processing session. This technological advantage directly translates into higher market prices for graded products and reduced customer complaints regarding quality deviations.
High-Capacity Processing Performance

High-Capacity Processing Performance

Modern cashew kernel grading machine models deliver exceptional throughput capabilities that significantly exceed manual sorting methods. Capable of processing 500 to 1000 kilograms per hour depending on specific model specifications, the cashew kernel grading machine enables facilities to meet demanding production schedules and large customer orders efficiently. This impressive capacity allows processing facilities to reduce overall production timelines while maintaining premium quality standards throughout. The equipment operates reliably during extended shifts without performance degradation, ensuring consistent results from morning through evening operations. High processing capacity directly reduces per-unit production costs, improving profit margins substantially. Businesses can expand market reach and accept larger contracts confidently, knowing their cashew kernel grading machine can reliably handle increased volume demands without compromising quality or causing operational bottlenecks.
Customizable Grading Parameters and Easy Integration

Customizable Grading Parameters and Easy Integration

The cashew kernel grading machine features flexible sorting criteria that operators can adjust according to specific market requirements and customer specifications. Intuitive control panels allow rapid reconfiguration between different grade standards without requiring technical expertise or lengthy downtime. This adaptability ensures the cashew kernel grading machine serves diverse business needs, from premium export markets to domestic bulk distribution channels. Integration with existing production line infrastructure occurs seamlessly, as the equipment connects to upstream cleaning systems and downstream packaging stations effortlessly. Real-time data logging provides comprehensive production records for quality assurance documentation and regulatory compliance purposes. Operators access performance metrics and sorting statistics through user-friendly dashboards, enabling informed decisions about production adjustments and maintenance scheduling for sustained operational excellence.

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

Copyright © 2026 Anhui Jiexun Optoelectronic Technology Co., Ltd. All rights reserved.  -  Privacy policy