Industrial Sorting Machine Solutions

All Categories

industrial sorting machine

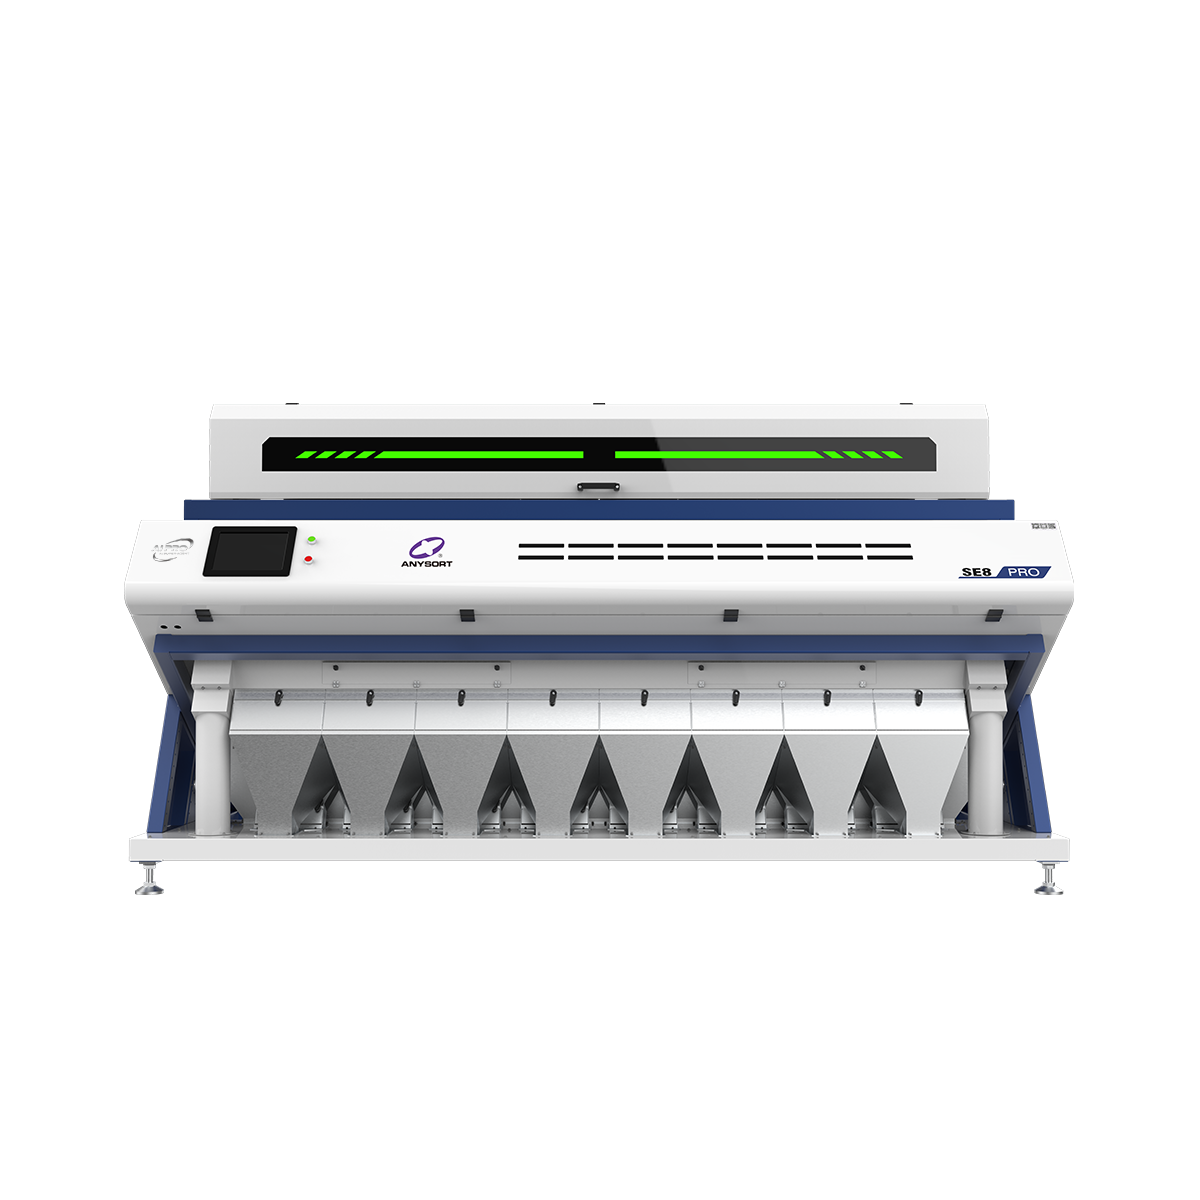
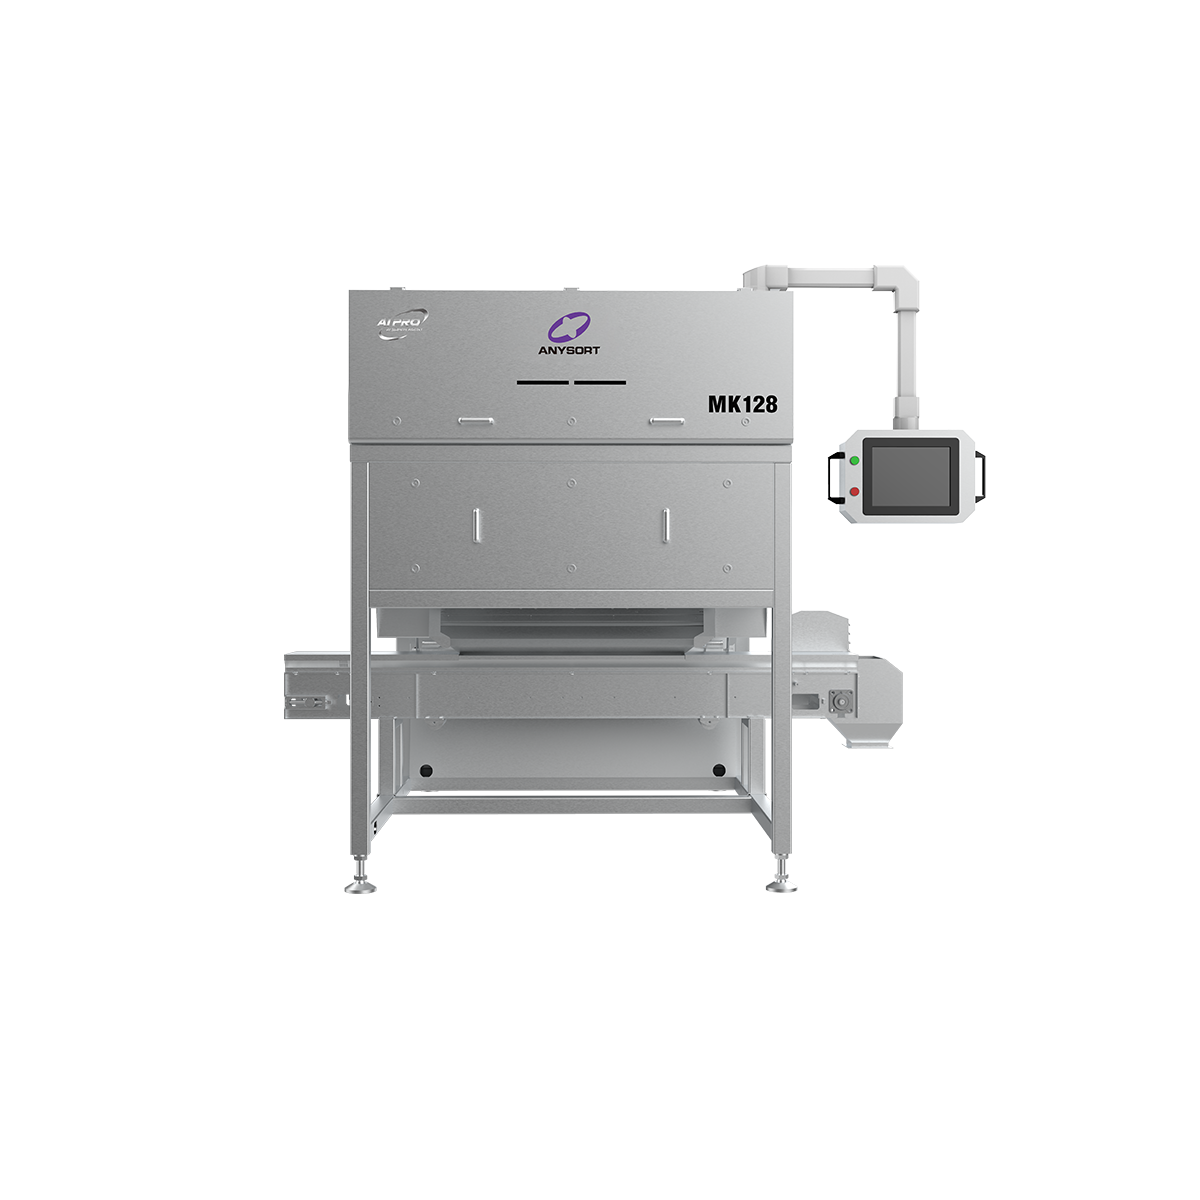
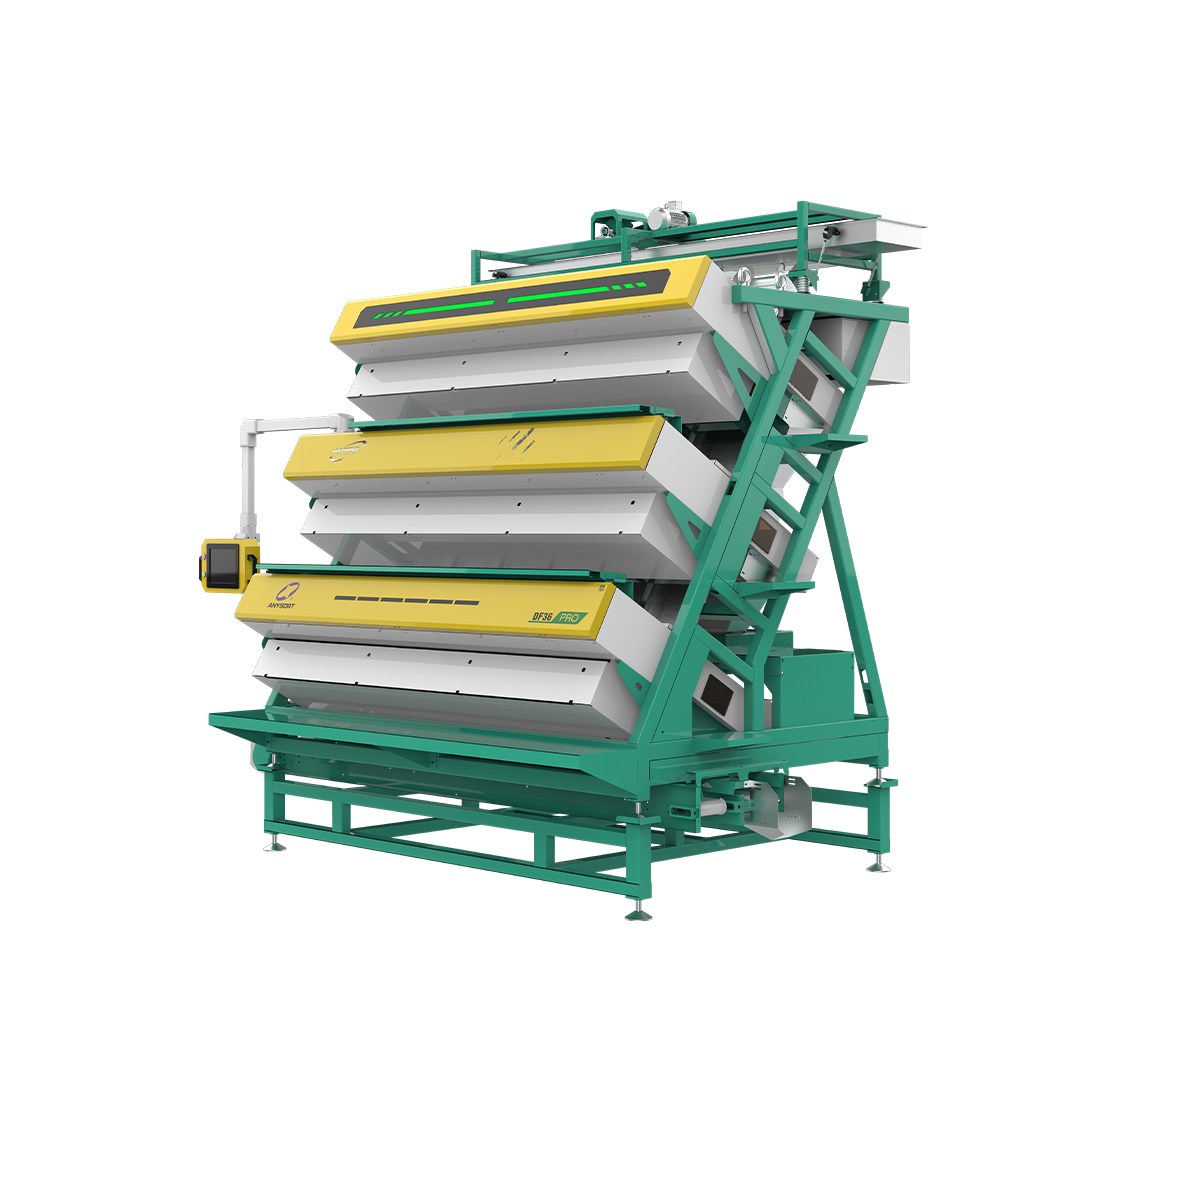
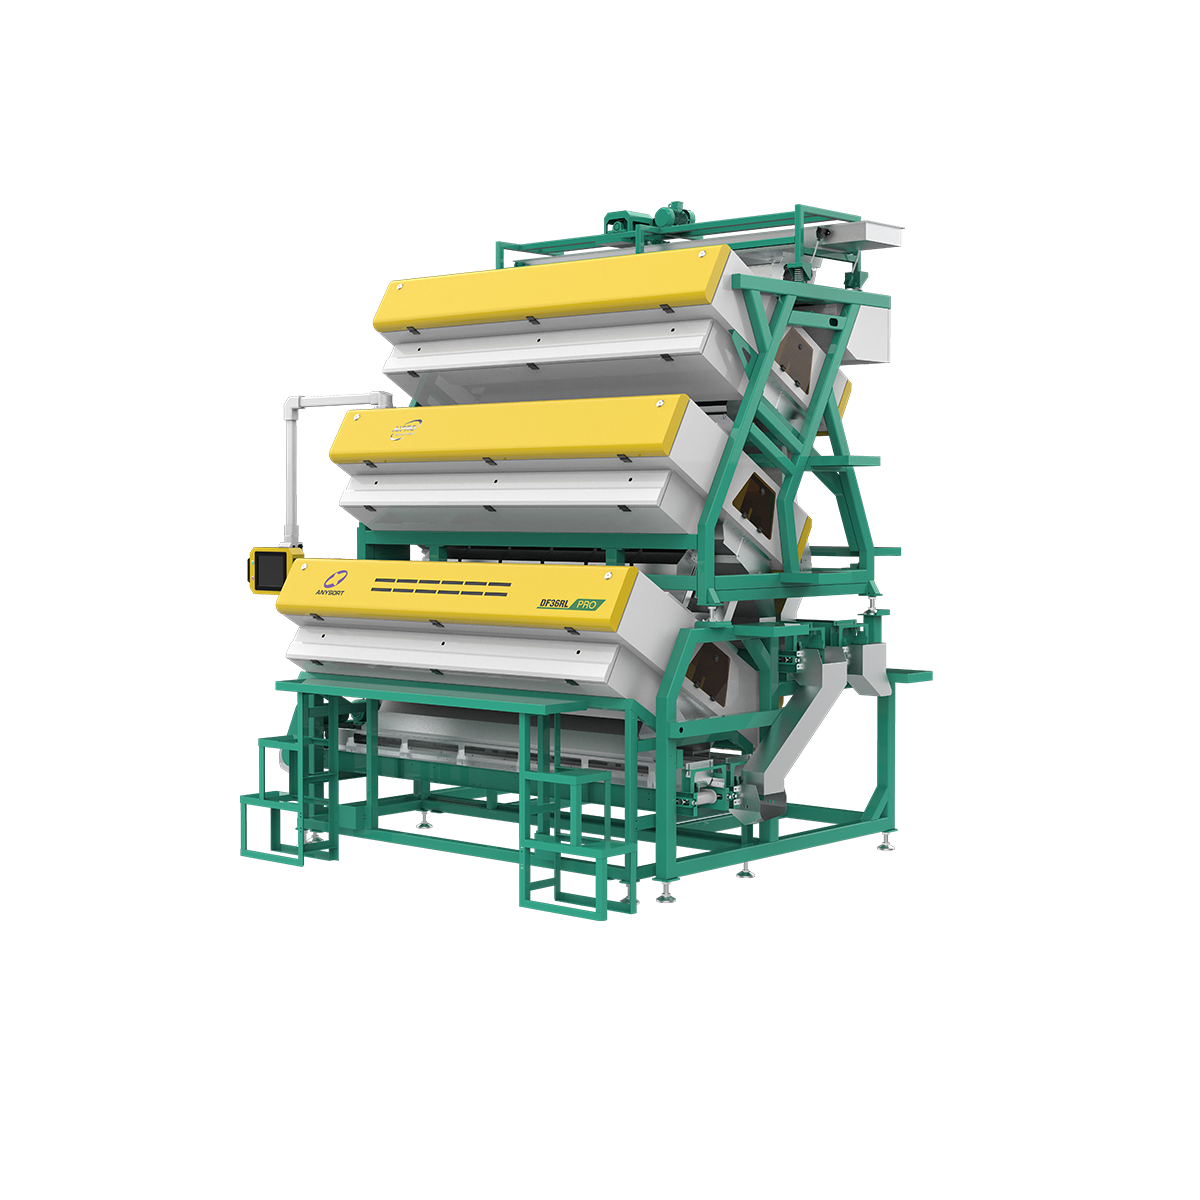
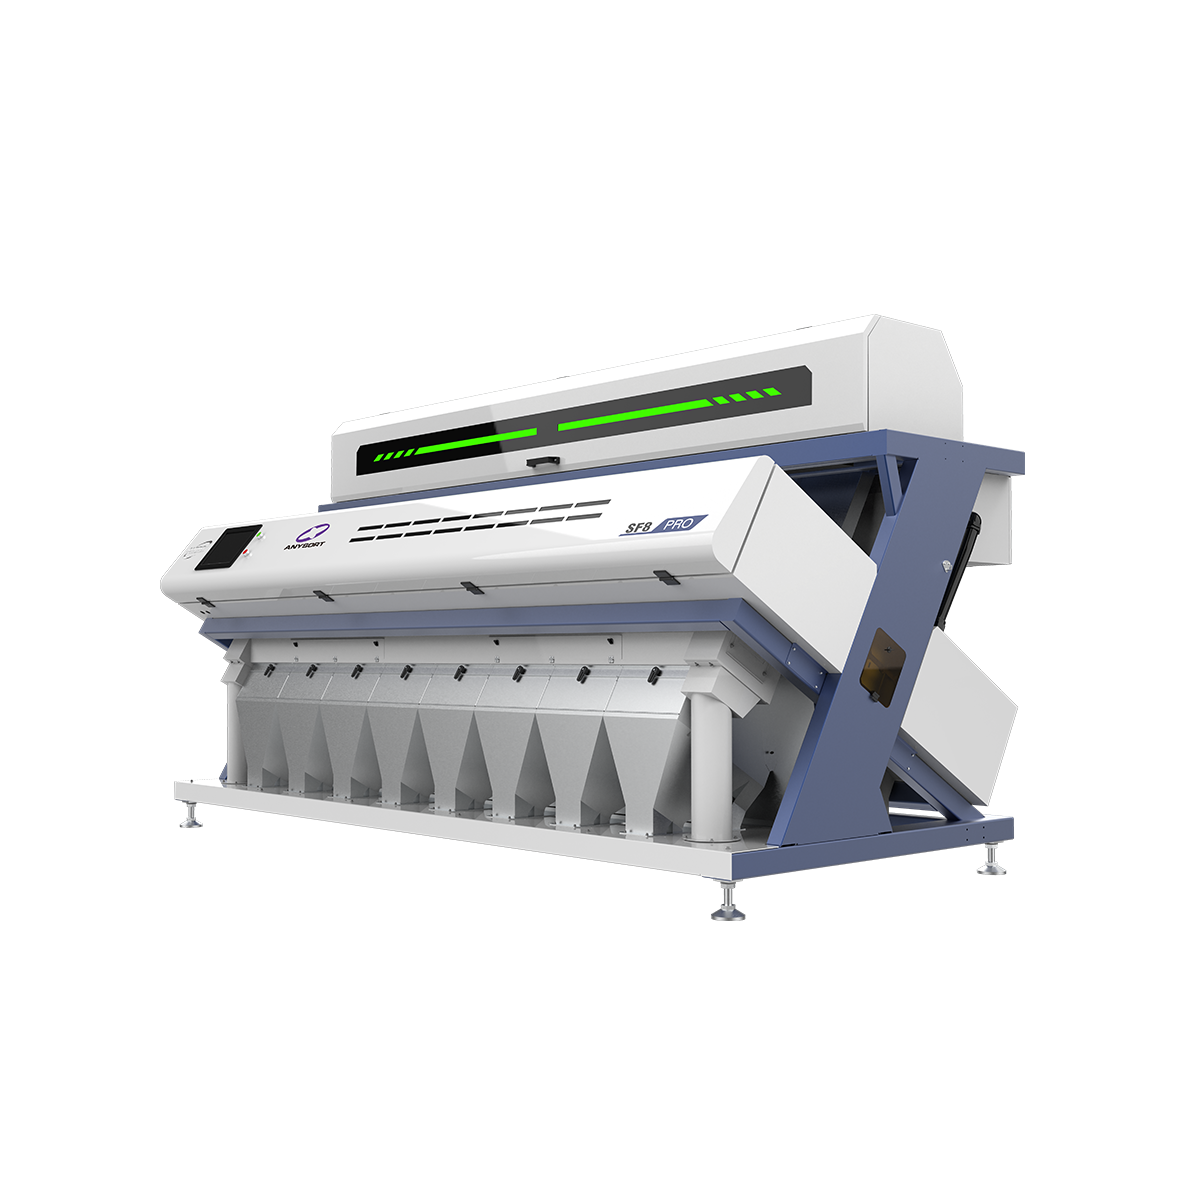
An industrial sorting machine is a sophisticated automated system designed to classify, separate, and organize materials based on specific criteria such as size, weight, color, density, or composition. These machines represent a critical advancement in modern manufacturing and processing operations across multiple industries. The industrial sorting machine utilizes cutting-edge sensor technology, including optical cameras, infrared detectors, and weight sensors, to identify and categorize items with exceptional precision and speed. Modern industrial sorting machines can process thousands of items per hour, dramatically improving operational efficiency compared to manual sorting methods. The technology behind an industrial sorting machine incorporates artificial intelligence and machine learning algorithms that enable continuous improvement and adaptation to various material types. These machines feature robust construction materials designed to withstand harsh industrial environments while maintaining consistent performance. An industrial sorting machine typically includes multiple discharge chutes or collection bins that direct sorted materials to designated locations. The system operates through a conveyor belt mechanism that moves materials past detection sensors, which analyze each item in milliseconds. Applications for the industrial sorting machine span across recycling facilities, food processing plants, mining operations, pharmaceutical manufacturing, and agricultural processing. The versatility of an industrial sorting machine makes it an indispensable tool for businesses seeking to maximize productivity and minimize waste. Installation of an industrial sorting machine requires minimal operational training, as most systems feature intuitive control interfaces and automated operation modes. The investment in an industrial sorting machine typically yields rapid return on investment through reduced labor costs and increased throughput.

Popular Products

Industrial sorting machines deliver transformative operational benefits that directly impact your bottom line and competitive positioning. The primary advantage of an industrial sorting machine lies in its remarkable speed and accuracy, processing materials far faster than human workers while maintaining superior consistency. By implementing an industrial sorting machine, companies dramatically reduce labor costs associated with manual sorting operations, allowing staff to focus on higher-value tasks. The industrial sorting machine minimizes sorting errors through advanced sensor technology, ensuring product quality and reducing waste materials that would otherwise require reprocessing. Operational efficiency gains from an industrial sorting machine translate directly into increased production capacity without requiring additional facility space or infrastructure investment. These machines enhance worker safety by removing employees from repetitive, physically demanding sorting tasks that can cause long-term health issues. An industrial sorting machine operates continuously throughout shifts, providing 24/7 productivity without fatigue-related performance degradation. The technology enables real-time data collection and reporting, providing valuable insights into material composition and production metrics. Companies utilizing an industrial sorting machine achieve better compliance with quality standards and regulatory requirements across their respective industries. The flexibility of an industrial sorting machine allows rapid reconfiguration for different material types, making it suitable for diverse product lines. Environmental benefits include significant waste reduction and improved recycling rates, supporting corporate sustainability initiatives. The automation provided by an industrial sorting machine creates competitive advantages through improved product consistency and faster market delivery. Maintenance requirements remain minimal compared to alternative sorting technologies, reducing downtime and associated productivity losses. Investment protection comes through scalable system designs that grow with your business needs without complete equipment replacement.

Latest News

How Can a Nuts Sorter Improve Your Production?

15

Aug

How Can a Nuts Sorter Improve Your Production?

A nuts sorter represents one of the most significant investments a food processing operation can make to enhance production quality and operational efficiency. The modern nuts sorter uses advanced imaging and sensor technology to identify and separat...
View More
How Does Nuts Sorter Technology Ensure Quality?

19

Aug

How Does Nuts Sorter Technology Ensure Quality?

The global nuts processing industry relies on precision and consistency to meet strict quality standards and regulatory requirements. A nuts sorter has become indispensable for processors seeking to eliminate defects, contaminants, and substandard pr...
View More
How Do Color Sorters Improve Product Quality?

26

Aug

How Do Color Sorters Improve Product Quality?

Product quality stands as a critical differentiator in competitive industrial markets, and achieving consistency at scale requires more than manual oversight. A color sorter represents one of the most effective technologies for identifying and removi...
View More
Top AI Color Sorter Manufacturers in China (2026)

30

Aug

Top AI Color Sorter Manufacturers in China (2026)

The global demand for precision sorting technology has surged dramatically, with color sorter machine manufacturers in China leading innovation across agricultural and industrial sectors. Chinese color sorter machine manufacturers have established th...
View More

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

industrial sorting machine

Advanced Sensor Technology for Precise Material Classification

Advanced Sensor Technology for Precise Material Classification

Modern industrial sorting machines incorporate sophisticated multi-sensor detection systems that identify materials with exceptional accuracy. These systems utilize optical scanners, infrared technology, and weight measurement devices working in perfect synchronization to analyze each item passing through the industrial sorting machine. The advanced sensors detect subtle differences in material properties that human eyes cannot distinguish, enabling consistent and reliable sorting across varying material batches. An industrial sorting machine equipped with this technology can differentiate between similar-looking materials, ensuring contamination-free output streams. The sensor arrays process information instantaneously, making real-time sorting decisions at speeds exceeding 500 items per minute. Integration with artificial intelligence algorithms allows the industrial sorting machine to learn and adapt to new material characteristics automatically. This technological sophistication ensures that your industrial sorting machine maintains peak performance regardless of material variations or environmental changes. The precision achieved by these sensors directly translates to improved product quality and enhanced customer satisfaction.
Exceptional Throughput and Production Capacity Enhancement

Exceptional Throughput and Production Capacity Enhancement

An industrial sorting machine dramatically increases production capacity by processing materials at speeds impossible for manual operations. Facilities implementing an industrial sorting machine consistently report throughput increases of 300-500 percent compared to previous sorting methods. The continuous operation capability of an industrial sorting machine means your facility maintains constant productivity throughout all working hours without fatigue-related slowdowns. Unlike human sorters who require breaks and experience performance deterioration, an industrial sorting machine maintains consistent speed and accuracy throughout extended operational periods. This enhanced throughput directly reduces per-unit processing costs and improves overall facility profitability. An industrial sorting machine's capacity allows businesses to accept larger orders and expand market reach without infrastructure expansion. The reliability of an industrial sorting machine ensures predictable production scheduling and improved delivery timeframes. Companies using an industrial sorting machine achieve significant competitive advantages through faster order fulfillment and enhanced customer responsiveness throughout their supply chains.
Cost Reduction and Rapid Return on Investment

Cost Reduction and Rapid Return on Investment

Implementing an industrial sorting machine delivers substantial financial benefits through multiple cost reduction mechanisms. The primary savings derive from dramatically reduced labor requirements, as an industrial sorting machine replaces numerous manual sorting positions. An industrial sorting machine typically pays for itself within 18-36 months through labor cost elimination and increased production efficiency. Beyond labor savings, an industrial sorting machine minimizes material waste through superior accuracy and reduces reprocessing costs significantly. Energy consumption remains reasonable despite continuous operation, as modern industrial sorting machine designs incorporate efficiency optimization features. The durability and reliability of an industrial sorting machine reduce unexpected maintenance expenses compared to aging manual processes. An industrial sorting machine enables companies to reduce quality control expenses through consistent, reliable output that meets strict specifications. The scalability of an industrial sorting machine technology allows businesses to expand operations cost-effectively as demand increases. These comprehensive financial advantages make an industrial sorting machine one of the highest-return investments available for manufacturing facilities.

Get a Free Quote

Our representative will contact you soon.
Required Product
Name
Email
WhatsApp
Message
0/1000

Copyright © 2026 Anhui Jiexun Optoelectronic Technology Co., Ltd. All rights reserved.  -  Privacy policy